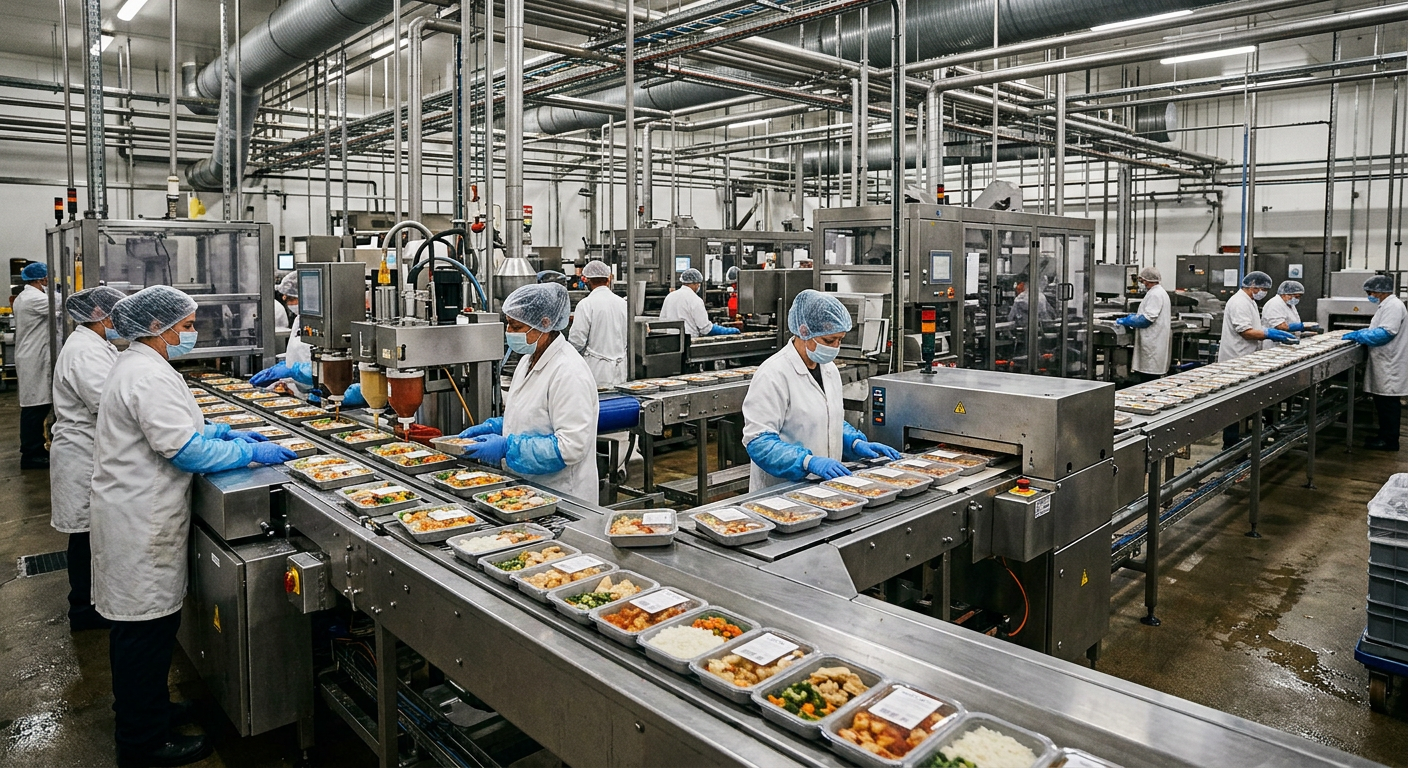
Clean-in-Place Systems for Beverage Production
[trp_language language=”en_US”]
Clean-in-place systems are the backbone of hygienic beverage manufacturing in the United States. A well-designed CIP program cleans tanks, lines, valves, pumps, heat exchangers, and fillers without disassembly, helping beverage plants reduce downtime, protect flavor, meet FDA and third-party audit expectations, and control water, chemical, and labor costs. For U.S. producers in markets such as beer, spirits, dairy beverages, juice, kombucha, carbonated soft drinks, and aseptic RTD products, CIP performance directly affects shelf life, brand protection, and plant profitability.
Across major production hubs such as North Carolina, California, Texas, Illinois, Wisconsin, Pennsylvania, and Georgia, beverage manufacturers are modernizing sanitation systems to support higher throughput and tighter compliance. Plants shipping through trade corridors near the Port of Los Angeles, Port of Long Beach, Port of Houston, Savannah, Newark, and Chicago distribution networks are under pressure to keep lines available, especially in co-packing and multi-SKU operations. That makes CIP system design a capital decision, not just a sanitation task.
For companies planning expansion, retrofit, or greenfield projects, CIP should be considered alongside utilities, automation, vessel sizing, wastewater loading, and production scheduling. Firms such as Disruptive Process Solutions approach beverage projects with a business-first engineering mindset, aligning sanitation infrastructure with throughput, product mix, and long-term operating cost rather than simply specifying oversized hardware. That approach is especially valuable when a syrup room, cellar, blending area, pasteurization loop, or filling hall must support future growth.
Quick Answer

A beverage CIP system is an engineered cleaning loop that circulates water, caustic, acid, sanitizers, and rinse solutions through process equipment at controlled time, temperature, flow, and concentration. Its goal is to remove beverage soils, reduce microbial risk, verify cleanliness, and return equipment to production-ready condition without manual teardown. In the United States, the best CIP systems are designed around product chemistry, line geometry, sanitary standards, automation needs, water reuse strategy, and validation requirements.
For most beverage operations, successful CIP depends on five basics: correct chemical selection, turbulent flow, sufficient temperature, proper contact time, and validated coverage of all product-contact surfaces. If one of those factors is weak, cleaning results become inconsistent. A plant may pass visual inspection but still fail ATP checks, microbial swabs, or taste panels due to residual sugar films, protein buildup, flavor carryover, or biofilm formation.
| CIP Decision Area | Why It Matters | Typical U.S. Beverage Impact |
|---|---|---|
| Product soil type | Determines chemistry and cycle design | Prevents undercleaning and flavor carryover |
| Equipment geometry | Affects flow, spray coverage, and drainability | Reduces shadow zones and residue traps |
| Automation level | Improves repeatability and recordkeeping | Supports audits and faster changeovers |
| Water reuse design | Lowers utility and discharge costs | Important in California, Texas, and drought-sensitive regions |
| Validation plan | Confirms real cleanliness, not assumptions | Protects shelf life and customer standards |
| Future capacity | Avoids bottlenecks after expansion | Critical for co-packers and seasonal beverage demand |
The table above shows why CIP selection should be tied to business outcomes. A cheaper system can become expensive if it lengthens changeovers, wastes water, or creates sanitation failures. Conversely, a right-sized system can improve uptime, limit labor exposure, and support faster product transitions.
How Clean-in-Place Systems Work in Beverage Production

In beverage production, CIP typically begins when product is pushed out or recovered from a tank or line. The system then runs a programmed sequence that may include pre-rinse, caustic wash, intermediate rinse, acid wash, final rinse, sanitation, and verification. Automated skids use conductivity, temperature, flow, level, and return sensors to confirm each step. Recipes can be tailored for fermenters, BBTs, syrup lines, UHT loops, blending tanks, fillers, or transfer pipelines.
The cleaning action depends on the classic four factors known across hygienic processing: chemistry, temperature, mechanical action, and time. Beverage plants also need strong control of the fifth factor: concentration verification. Inline conductivity meters are commonly used to distinguish water from chemical return and to support recovery of reusable caustic or acid. Advanced systems add SCADA-based recipe control, data logging, alarm management, and production integration.
In practical terms, a U.S. bottling or brewing facility may operate one central CIP room feeding multiple circuits, or smaller dedicated skids close to the process area. A filler may have short, frequent cycles between SKU changes, while a fermenter or blend tank may run a longer sequence with stronger chemical exposure. High-risk products like dairy beverages, protein drinks, and aseptic formulations usually require more rigorous validation than standard carbonated soft drinks or filtered spirits.
The line chart reflects a realistic growth pattern in CIP upgrade activity across the U.S. beverage market. Rising sanitation expectations, labor pressure, product diversification, and sustainability targets are pushing more manufacturers toward automated and better-instrumented cleaning systems.
Beverage-Specific Soil Types: Sugars, Acids, Proteins & Oils

Beverage soils vary dramatically by product category, which is why a single generic CIP recipe rarely works across an entire plant. Sugary drinks leave sticky carbohydrate films that attract microbes and harden if heat dries them on surfaces. Juices and functional beverages often contain pectin, pulp fines, natural color compounds, and fruit acids. Dairy-based beverages leave protein and fat residues that can denature on hot surfaces and resist simple rinsing. Flavor emulsions, botanical extracts, and some nutraceutical ingredients may introduce oils, gums, and stabilizers that require specialized detergents.
Acidic products are not necessarily self-cleaning. Citric acid, malic acid, phosphoric acid, and fermentation byproducts can interact with minerals or packaging-area residues to form deposits over time. In breweries and kombucha plants, yeast films, hop resins, krausen rings, and organic stone require targeted cycle design. In spirits and distillation environments, sugars, mash solids, congeners, and caramel color residues may build up in tanks, transfer lines, and blend systems.
| Beverage Category | Primary Soil | Cleaning Challenge | Common Chemistry Approach |
|---|---|---|---|
| Carbonated soft drinks | Sugars and syrups | Sticky films in blend and fill systems | Warm caustic with strong rinse control |
| Juices | Pectin, pulp, acids | Organic films and color carryover | Caustic plus periodic acid cycle |
| Dairy beverages | Proteins and fats | Denatured deposits and microbial risk | Alkaline wash, acid descaling, validation-heavy program |
| Beer | Yeast, proteins, hop resins | Tank rings and biofilm risk | Caustic wash with sanitizer verification |
| Kombucha | Yeast, acids, biofilm-forming residues | Fermentation variability | Flexible recipes and close ATP monitoring |
| Protein RTD | Protein, oil, stabilizers | Difficult heat-set residues | High-performance alkaline program and strict microbiology |
The table illustrates why recipe-based CIP matters. A protein RTD line near Chicago or a cold-fill juice plant in Florida should not be cleaned with the same parameters used for a filtered seltzer line in Arizona. Soil mapping by product family is often the first step in designing an efficient sanitation program.
CIP Process Steps for Tanks, Pipelines & Filling Equipment
While details vary, most beverage CIP programs follow a predictable sequence. First is product recovery or push-out using air, water, or pigging where appropriate. Next comes a pre-rinse to remove gross residue. A caustic wash follows to dissolve organic soils. Many systems then run an intermediate rinse before an acid cycle to remove mineral scale and neutralize alkaline carryover. A final rinse, optional sanitizer, and line release complete the process. Critical equipment may also require post-CIP sterile air drying or aseptic hold procedures.
Tanks rely on spray devices, return flow control, full drainability, and coverage of manways, agitators, vent filters, and upper shell regions. Pipelines need enough velocity to maintain turbulent flow, especially through tees, valve manifolds, meters, and dead-leg-prone areas. Filling equipment demands special attention because nozzles, bowls, product paths, cap chutes, and change parts may include complex geometries where residual product can persist.
| Equipment | Key CIP Requirement | Typical Risk if Missed | Recommended Control Point |
|---|---|---|---|
| Mixing tank | Spray coverage and full drainability | Residue under top fittings | Flow and return temperature |
| Fermenter | Wall wetting and gas-side hygiene | Yeast or biofilm persistence | Recipe-controlled cycle and ATP verification |
| Pipeline | Turbulent velocity through all branches | Sugar film or flavor carryover | Flow rate and return conductivity |
| Heat exchanger | Controlled chemistry and temperature | Fouling and reduced heat transfer | Differential pressure and cycle history |
| Filler | Coverage of product-contact internals | Microbial contamination at packaging point | Validated filler recipe and swab plan |
| Bright tank | Low-foam cleaning and complete rinse-out | Sanitizer or chemical residuals | Conductivity endpoint and final rinse confirmation |
The process table shows that each asset class has different failure modes. In real U.S. plants, sanitation issues are often caused not by chemistry selection alone but by poor flow balance, incomplete return routing, valve misalignment, or filler circuits that were never fully validated after a line modification.
From a technology standpoint, modern beverage projects increasingly combine CIP skids with PLC programming, recipe management, and SCADA dashboards. This is where an engineering partner with automation and process expertise matters. DPS, for example, supports structural, mechanical, plumbing, electrical, process, and controls engineering, which helps align CIP with utilities, blending, pasteurization, fermentation, carbonation, water treatment, and packaging integration rather than treating sanitation as an isolated utility.
Sanitary Design Standards: 3-A, EHEDG & BPE Compliance
Sanitary design begins before the first cleaning cycle ever runs. If equipment contains dead legs, poor welds, non-drainable piping, hollow rollers, rough finishes, incorrect gasket materials, or inaccessible instrument tees, even the best CIP chemistry may not achieve repeatable results. That is why beverage manufacturers in the United States increasingly reference sanitary frameworks such as 3-A principles, EHEDG design guidance, and ASME BPE expectations where hygienic detail is critical.
3-A criteria are widely recognized in dairy and hygienic process applications. EHEDG is especially useful for evaluating cleanability and hygienic engineering practices. BPE is often associated with high-purity and bioprocess environments, but many of its principles on drainability, surface finish, documentation, and fabrication quality are relevant to aseptic or highly sensitive beverage systems. Plants do not always need every standard at every node, but they should understand how each applies to product risk.
| Standard or Guidance | Main Focus | Best Fit in Beverage Plants | Benefit |
|---|---|---|---|
| 3-A | Hygienic equipment design | Dairy, high-care processing, sanitary skids | Improved cleanability and audit confidence |
| EHEDG | Hygienic engineering and validation | Complex process areas and design review | Reduced contamination risk |
| ASME BPE | Bioprocess and high-purity fabrication | Aseptic and sensitive beverage applications | Better documentation and finish control |
| FDA cGMP principles | Food safety and process control | All U.S. beverage operations | Regulatory alignment |
| SQF or BRC expectations | Verification and system discipline | Co-packers and branded suppliers | Retail and customer acceptance |
| Internal corporate standards | Company-specific performance rules | Multi-site beverage groups | Consistency across facilities |
This comparison highlights a practical point: compliance is not just about paperwork. It shapes weld quality, pipe slope, instrument placement, valve selection, cleanout coverage, and maintenance access. Those design decisions influence every CIP outcome for years after startup.
Centralized vs. Decentralized CIP for Multi-Line Beverage Plants
In a multi-line facility, one of the biggest strategic decisions is whether to install a centralized CIP room or decentralized skids near process zones. Centralized systems can reduce duplicate equipment, simplify chemical management, and support solution recovery. They are often attractive in large breweries, co-pack plants, and integrated beverage campuses with multiple tank farms and packaging lines. However, they also require careful circuit design, valve matrix control, longer piping runs, and scheduling discipline.
Decentralized CIP systems place smaller skids closer to the equipment they serve. This can shorten cycles, reduce distribution losses, and increase flexibility for isolated operations such as aseptic blending, cellar cleaning, or a dedicated dairy beverage suite. The tradeoff is more equipment to maintain and, in some cases, less opportunity for chemical recovery.
The bar chart shows that CIP demand is strong across beverage categories, with especially high modernization pressure in dairy beverages, beer, and fast-growing RTD segments. Multi-line co-pack operations often lead this demand because cleaning flexibility directly impacts changeover economics.
| Configuration | Strength | Limitation | Best Use Case |
|---|---|---|---|
| Centralized CIP | Shared chemical and utility efficiency | Complex routing and scheduling | Large beverage campuses |
| Decentralized CIP | Fast local response and shorter runs | More skids to maintain | Segmented or high-risk process areas |
| Hybrid model | Balances flexibility and cost | Requires clear scope definition | Growing multi-line plants |
| Dedicated filler CIP | Protects packaging uptime | Extra capital cost | High-speed filling halls |
| Dedicated aseptic CIP | Higher hygiene assurance | Separate validation burden | UHT and sterile applications |
| Portable CIP unit | Low initial capital | Limited scalability and repeatability | Pilot or very small operations |
The comparison shows why buying advice must be tied to plant reality. A beverage site in Dallas with multiple syrup rooms and fillers may benefit from a hybrid architecture, while a compact craft plant in Oregon may prefer a simpler skid. Location matters too: facilities in high-cost utility regions or wastewater-constrained municipalities often prioritize recovery and reuse features earlier in the capital planning process.
As a service capability, DPS works across feasibility, capital planning, owner’s representation, project management, general contracting, installation, and integration. For clients expanding from one line to several, that end-to-end model can help evaluate whether CIP should be centralized, decentralized, or phased, while keeping construction, controls, utilities, and schedule aligned.
Validation Requirements: ATP Testing & Microbiological Verification
No CIP system should be accepted on visual appearance alone. Validation confirms that the cleaning process consistently produces acceptable hygienic outcomes. In beverage operations, common tools include ATP testing, allergen swabs where relevant, conductivity confirmation, temperature records, concentration checks, microbiological swabbing, rinse water testing, and periodic teardown inspections for hard-to-clean components.
ATP testing is useful for rapid feedback after cleaning, especially during startup, troubleshooting, and changeover verification. However, ATP does not replace microbiological testing. A surface can have low ATP and still present microbial risk if biofilms, niches, or post-clean contamination exist. Microbiological verification remains essential for dairy beverages, aseptic systems, low-acid high-risk products, and customer-audited co-packing operations.
Validation should also include worst-case scenarios: longest line paths, lowest-flow circuits, highest-soil products, overnight holds, and seasonal temperature variation. Plants in humid Gulf Coast climates such as Houston or New Orleans may see different environmental pressure than facilities in dry inland regions. That matters for filler rooms, hose handling, and post-CIP exposure.
The area chart shows how plants are moving from manual checks toward digitally recorded validation. This trend is expected to continue through 2026 as audit readiness, labor constraints, and traceability requirements increase.
| Validation Tool | What It Confirms | Speed | Best Use |
|---|---|---|---|
| ATP swab | Organic residue presence | Fast | Routine release checks |
| Microbiological swab | Microbial contamination | Slow | Risk-based verification and trend analysis |
| Conductivity record | Chemical/rinse transition | Real time | Automated cycle control |
| Temperature log | Thermal cleaning performance | Real time | Recipe compliance |
| Chemical titration | Detergent concentration | Moderate | Confirm solution strength |
| Teardown inspection | Physical residue in hidden areas | Slow | Periodic deep verification |
This table shows that no single tool is enough on its own. Effective validation layers fast release methods with periodic deeper verification. Plants that only swab external surfaces or only monitor conductivity are missing part of the picture.
Water Conservation & Wastewater Reduction Strategies
Water and wastewater costs are becoming major CIP design drivers in the United States, especially in California, Arizona, Colorado, parts of Texas, and municipalities with strict discharge permits. Beverage plants can reduce environmental impact and operating cost through recovered final rinse water, conductivity-based cutover, optimized line volume calculations, pigging for product recovery, chemical reuse, low-volume spray devices where appropriate, and automatic shutdown logic for incomplete circuits.
Wastewater reduction is not just about volume. It also concerns pH swings, BOD, COD, sugar loading, suspended solids, and temperature. A plant discharging high-strength syrup residues near Atlanta or Los Angeles may face very different sewer surcharges than a smaller brewery in the Midwest. CIP design should therefore be coordinated with pretreatment, equalization, recovery tanks, and production scheduling.
Manufacturing capability also matters here. DPS designs and supplies custom process equipment including tanks up to 12,000 gallons and custom CIP systems, which can be tailored to plant-specific recovery goals instead of forcing a one-size-fits-all skid. For beverage manufacturers scaling capacity, custom design may yield better utility efficiency than adapting a generic package unit.
The comparison chart illustrates a common market reality: packaged skids may lower initial cost, but custom-engineered systems often outperform them in water reduction, recovery, automation, and long-term scalability. Buyers should compare lifecycle cost, not only purchase price.
Common Mistakes in Beverage CIP & How to Avoid Them
The most common CIP mistake is assuming that a cycle that worked for one product will work for all products. Another frequent issue is neglecting sanitary design during expansion projects. A new branch line, meter, or valve cluster can create a cleaning blind spot that did not exist before. Plants also underestimate the importance of instrument calibration, especially conductivity and temperature sensors that determine chemical strength and cycle completion.
Other mistakes include oversized rinse times, undersized return pumps, poor spray device selection, lack of documented riboflavin or coverage testing where needed, failure to separate allergen or dairy circuits, insufficient operator training, and weak post-CIP hold controls. On fillers, manual workarounds often hide fundamental design issues. If operators repeatedly remove parts for hand cleaning that were intended to be CIP’d, the system may not be truly clean-in-place.
| Common Mistake | Operational Consequence | Prevention Strategy |
|---|---|---|
| One recipe for all products | Residue carryover or overcleaning | Create product-family CIP recipes |
| Poor line velocity | Incomplete soil removal | Verify hydraulic design and flow targets |
| Ignoring dead legs | Persistent contamination niches | Review hygienic layout during design and retrofit |
| Uncalibrated sensors | Bad chemical concentration data | Use routine calibration and audit trails |
| No validation trend review | Hidden decline in sanitation performance | Track ATP and microbiology over time |
| Water-only cost focus | Higher total lifecycle expense | Evaluate downtime, labor, chemicals, and wastewater too |
The lesson from the table is simple: CIP problems are usually system problems, not just sanitation crew problems. They involve engineering, operations, maintenance, automation, and management decisions. This is one reason why beverage companies often benefit from integrators that can connect process design, utilities, controls, and execution in one model.
In practice, a profitable CIP project often starts with a plant assessment. That may include mapping current circuits, measuring cycle duration, identifying rinse losses, reviewing microbiological trends, and evaluating future production goals. A co-packer in the Southeast running energy drinks, teas, and juice blends may have completely different sanitation economics than a craft distillery in Kentucky or a dairy beverage plant in Wisconsin. Local suppliers, chemical partners, utilities, and municipal discharge rules all influence the right answer.
For manufacturers evaluating partners, it is useful to work with firms that understand both technology and execution. DPS serves beverage and food manufacturers across all 50 states and Canada, bringing process engineering, capital planning, installation, commissioning, and system integration experience across fermentation, distillation, pasteurization, aseptic processing, blending, filtration, carbonation, water treatment, and utility systems. That range helps ensure the CIP system supports the whole plant, not just a single asset.
FAQ
What is the ideal CIP frequency in beverage production?
It depends on product type, hold time, process temperature, and risk level. High-protein, dairy, and aseptic lines typically need more frequent or more rigorous cleaning than filtered or low-residue beverage systems.
Can one CIP system clean tanks, pipelines, and fillers?
Yes, but only if the system is properly sized and the circuits are engineered for each equipment type. Many plants use separate recipes or dedicated skids for fillers or aseptic areas.
How do U.S. beverage plants reduce CIP water usage?
Common strategies include final-rinse recovery, conductivity-based cutover, product recovery before rinse, chemical reuse, and optimized recipe times. Wastewater pretreatment should be reviewed at the same time.
Is ATP testing enough to validate cleaning?
No. ATP is a fast screening tool, but it should be combined with microbiological verification, chemistry checks, temperature records, and periodic inspection of hard-to-clean components.
What is better: centralized or decentralized CIP?
Neither is always better. Large multi-line plants often use centralized or hybrid systems, while smaller or high-risk zones may benefit from decentralized skids. The best option depends on layout, product mix, utilities, and expansion plans.
Do breweries and distilleries need the same CIP design as dairy beverage plants?
No. Brewing and distilling typically deal with yeast, sugars, and organic residues, while dairy beverages add protein and fat challenges that require stricter validation and often more demanding chemistry.
How important is sanitary design compared with cleaning chemistry?
Both are critical. Poorly designed equipment cannot be made reliably clean by stronger chemicals alone. Drainability, weld quality, dead-leg control, and surface finish are foundational.
What should buyers ask before purchasing a CIP system?
Ask about hydraulic assumptions, recipe flexibility, recovery options, automation depth, validation strategy, future line additions, maintenance support, and integration with utilities and controls.
What trends will shape beverage CIP through 2026?
Expect more digital validation, stronger sustainability requirements, smarter water reuse, greater SCADA integration, predictive maintenance, tighter hygienic documentation, and more scrutiny on wastewater loading and energy use.
Looking ahead to 2026, U.S. beverage manufacturers will likely see CIP become more data-driven and more closely tied to ESG, municipal water constraints, labor efficiency, and retailer-driven food safety expectations. Digital recipe enforcement, remote support, automated reporting, and recovery-focused utility design will move from optional upgrades to standard project requirements. Plants that align CIP with growth planning now will be better positioned for expansion, compliance, and profitability in the years ahead.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

