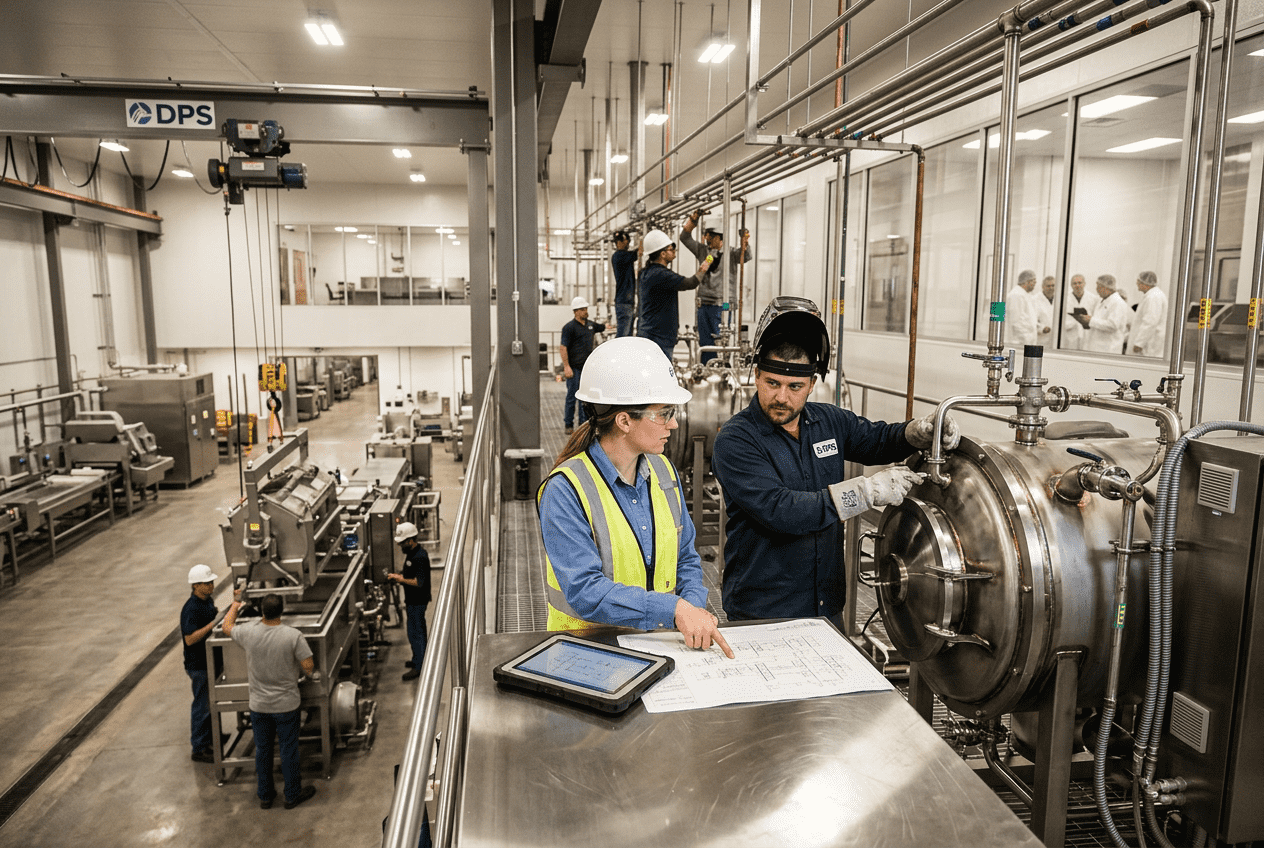
Sanitary Process Equipment Manufacturer
[trp_language language=”en_US”]
Sanitary Equipment Manufacturing Guide in the United States
For food, beverage, dairy, aseptic, and high-care processing, a sanitary process equipment manufacturer is not simply a fabricator of tanks, skids, piping, and vessels. In the United States market, the right manufacturer must understand hygienic engineering, regulatory expectations, material control, weld quality, clean-in-place performance, documentation, and long-term plant profitability. Buyers in hubs such as Chicago, Dallas, Los Angeles, Charlotte, Atlanta, Houston, Seattle, and the Northeast corridor increasingly evaluate suppliers not only on price, but on cleanability, validation support, integration capability, and lifecycle risk.
That matters because poorly designed sanitary equipment can create contamination harborage, excessive water and chemical use, difficult inspections, microbiological risk, shorter production runs, and costly downtime. By contrast, well-executed hygienic design supports faster changeovers, more reliable CIP, better product quality, easier audits, and stronger capital returns. For processors shipping across the United States through ports and logistics nodes such as Long Beach, Savannah, Newark, and Houston, consistency and compliance are business-critical.
Quick Answer

A sanitary process equipment manufacturer designs and builds equipment so product contact surfaces can be cleaned effectively, drained fully, inspected easily, and maintained without contamination risk. In the United States, the best suppliers typically demonstrate experience with 3-A sanitary standards, awareness of EHEDG guidance where applicable, polished and passivated stainless surfaces, traceable materials, validated CIP performance, compliant elastomers, and documented quality systems. Buyers should verify weld maps, surface finish records, MTRs, heat numbers, passivation reports, drainability, spray device coverage, and final acceptance testing before purchase.
Typical sanitary equipment categories include storage tanks, blending vessels, process skids, CIP systems, heat transfer packages, piping manifolds, fermentation tanks, dosing systems, marination systems, and clean utility modules. The strongest manufacturers also support engineering, installation, controls integration, commissioning, and post-startup optimization rather than only selling hardware.
| Decision Area | What to Verify | Why It Matters | Risk if Ignored |
|---|---|---|---|
| Hygienic geometry | Self-draining slopes, no dead legs, clean weld transitions | Reduces microbial harborage and retained product | Contamination and longer cleaning cycles |
| Surface finish | Measured Ra values, polish method, documentation | Improves cleanability and consistency | Biofilm formation and difficult inspection |
| Materials | 316L or specified alloy, MTRs, heat traceability | Supports corrosion resistance and audit readiness | Unknown metallurgy and premature failure |
| CIP design | Spray device coverage, drainability, velocity criteria | Ensures repeatable cleaning performance | Incomplete cleaning and excessive chemical use |
| Seals and gaskets | FDA compliant compounds, temperature and chemical compatibility | Protects product and reduces maintenance issues | Swelling, cracking, leaks, contamination |
| Quality system | WPS/PQR, weld logs, FAT, passivation records, QA checks | Proves consistent manufacturing control | Rework, delays, and failed audits |
The table above summarizes the six most important buying checks. In practice, processors should review each item during quotation, submittal, fabrication, FAT, site acceptance, and early production support.
What Sanitary Design Means in Process Equipment Manufacturing

Sanitary design means every feature of the equipment is intentionally engineered to prevent contamination and to allow effective cleaning, rinsing, and inspection. It applies to vessels, piping, fittings, skids, pumps, valves, instrumentation connections, agitators, access ports, supports, and control interfaces. In sanitary manufacturing, small geometric details have large consequences. A badly oriented nozzle, a recessed instrument port, or a flat vessel bottom can create a cleanability problem that remains for the entire life of the asset.
At a practical level, sanitary design usually includes smooth product contact surfaces, crevice-free joins, orbital or high-quality GTAW welds, fully drainable lines, properly selected elastomers, hygienic valves and instrumentation, minimum horizontal ledges, and structures that do not trap moisture. For plants operating under FDA, USDA, SQF, BRC, or customer-specific quality programs, sanitary design also supports more efficient verification and easier documentation.
In the United States, sanitary design expectations vary somewhat by sector. Dairy, cultured products, aseptic beverages, infant nutrition, sauces, prepared foods, protein processing, and brewery applications all require hygienic thinking, but cleaning chemistry, temperatures, microbial concerns, and process residence times can differ. A manufacturer that only builds polished tanks may not be enough. Buyers often need a partner able to integrate process knowledge with fabrication quality.
This is where an engineering-led company brings added value. Disruptive Process Solutions approaches sanitary systems from the plant performance side as well as the equipment side. Its technological capabilities include process, mechanical, electrical, controls, and automation expertise for complete systems, which helps align hygienic equipment geometry with actual flow paths, cleaning sequences, PLC logic, and production objectives. That system-level perspective is especially useful when equipment must fit brownfield plants with limited space or legacy utilities.
3-A Sanitary Standards vs. EHEDG Guidelines: Key Differences

Buyers often ask whether 3-A or EHEDG is “better.” The real answer is that they serve related but different purposes. In the United States, 3-A Sanitary Standards are widely recognized in dairy and many food and beverage applications. EHEDG guidance is influential internationally and is often used for broader hygienic engineering interpretation, design philosophy, and cleaning validation thinking. Many sophisticated manufacturers understand both frameworks and can discuss where each is relevant.
| Topic | 3-A Focus | EHEDG Focus | Practical Buying Insight |
|---|---|---|---|
| Geographic relevance | Strong U.S. recognition | Strong European influence | U.S. plants often prioritize 3-A, exporters may ask for both perspectives |
| Primary use | Equipment standardization and accepted sanitary construction | Hygienic design guidance and cleaning performance concepts | Use 3-A for acceptance language and EHEDG for deeper design review |
| Industry presence | Very common in dairy and liquid food processing | Broad hygienic engineering reference across sectors | Application drives which framework dominates |
| Documentation style | Specific equipment-oriented criteria | Guideline-based engineering interpretation | Manufacturers should explain compliance clearly |
| Cleanability emphasis | Strong sanitary construction expectations | Strong attention to hygienic detail and validation concepts | Ask for actual CIP evidence, not just claims |
| Buyer takeaway | Good benchmark for U.S. sanitary acceptance | Good benchmark for advanced hygienic design review | Best suppliers can translate both into practical fabrication decisions |
The point of comparison is not to create a standards debate. It is to confirm whether the manufacturer can explain why a branch connection angle, seal groove profile, spray device placement, or internal weld contour supports hygienic operation. A credible supplier will discuss product characteristics, viscosity, temperature, cleaning chemistry, target run length, inspection needs, and the real operating environment.
For processors selling nationally from major production corridors such as the Midwest, the Southeast, and California, harmonizing sanitary practices across multiple sites is increasingly important. Standardizing around documented hygienic design criteria can improve procurement consistency and reduce startup surprises.
The line chart illustrates a realistic growth trend in hygienic equipment demand in the United States, driven by automation, food safety expectations, reshoring of production capacity, and increased investment in beverage, protein, and prepared food manufacturing.
Self-Draining Design, Elimination of Dead Legs & Cleanability Principles
Self-draining design is one of the most important indicators of sanitary quality. If product, water, or cleaning solution remains trapped after production or CIP, that residue can dilute the next batch, support microbial growth, stain surfaces, or create inconsistent analytical results. Good sanitary equipment should drain by gravity in its installed orientation, not only in an idealized shop drawing.
Dead legs are sections of piping or connection geometry where flow is weak or stagnant. They can occur at branches, instruments, valve clusters, sample points, unused tees, oversized spool sections, and poorly positioned outlet nozzles. In hygienic systems, dead legs are minimized because they are difficult to clean reliably. Even when a system appears polished, bad flow architecture can undermine sanitary performance.
Cleanability also depends on velocity, turbulence, spray impact, coverage, contact time, temperature, chemistry, and surface condition. A tank with perfect polish but poor spray device placement may still fail to clean. Likewise, a well-designed CIP skid will not rescue a vessel with internal obstructions or poor drain geometry.
| Design Principle | Preferred Practice | Benefit | Common Red Flag |
|---|---|---|---|
| Bottom geometry | Sloped or formed for complete drainage | Reduces retained liquid | Flat low points |
| Branch connections | Short, flow-swept, correctly oriented | Minimizes stagnation | Long instrument stubs |
| Spray coverage | Validated overlap and wetting | Improves tank cleaning | Shadowed internal areas |
| Valve manifolds | Compact, drainable, serviceable | Safer changeovers | Complex clusters with trapped pockets |
| Weld transitions | Smooth and flush | Less residue retention | Undercut, pits, sugaring |
| Installed orientation | Designed for actual field slope and access | Real-world drainability | Shop-only assumptions |
The table above shows that cleanability is not one feature but a combination of geometry, fabrication discipline, and installation accuracy. This is why design-build and field integration experience matters. A skid can leave the shop in excellent condition yet lose sanitary performance if field supports, piping pitch, or utility tie-ins are handled poorly.
Disruptive Process Solutions is useful to mention here because its service capabilities extend beyond engineering drawings. Through its design-build-manage model, the company supports process design, project execution, installation, and system integration, helping sanitary intent survive from concept through startup. Processors can learn more about its project approach through its engineering and integration services.
Surface Finish Specifications: Ra <0.8 μm and Passivation Requirements
Surface finish is one of the most misunderstood sanitary requirements in process equipment procurement. Buyers often specify a finish number but fail to ask how it was achieved, where it was measured, whether welds were blended properly, or whether post-fabrication contamination was controlled. For many hygienic applications, a surface roughness around Ra <0.8 μm is a common target for product contact areas, though actual requirements vary with product sensitivity, regulatory expectations, and customer standards.
Lower roughness values can improve cleanability, but finish alone does not guarantee sanitary performance. The polishing method, directionality, weld condition, heat tint removal, and passive layer restoration also matter. Stainless steel that has been mechanically worked, welded, or contaminated by free iron may require proper cleaning and passivation to restore corrosion resistance and improve long-term reliability.
Passivation is especially important in plants exposed to aggressive cleaning chemistries, chlorides, temperature cycling, or humid coastal environments such as Gulf Coast and West Coast facilities. Over time, poor passivation practices can contribute to corrosion, staining, or reduced service life.
| Surface Topic | Best Practice | Evidence to Request | Operational Benefit |
|---|---|---|---|
| Base metal finish | Specified Ra target for contact surfaces | Mill or shop finish records | Consistent cleanability |
| Weld finishing | Flush, blended, no pits or discoloration | Borescope photos or inspection logs | Less residue retention |
| Measurement | Calibrated profilometer readings | Surface roughness report | Verifiable acceptance criteria |
| Heat tint removal | Proper post-weld treatment | QA inspection record | Improved corrosion resistance |
| Passivation | Documented chemical treatment and rinse control | Passivation certificate | Stronger oxide layer |
| Protection after fabrication | Clean handling, wrapping, storage | Packaging and shipping procedure | Prevents field contamination before startup |
This table is useful because it connects roughness numbers to actual proof points. A serious manufacturer should be comfortable discussing how finish is measured, which areas are sampled, what weld acceptance criteria apply, and how passive layer restoration is verified within its QA system.
Manufacturing capability also matters here. Disruptive Process Solutions designs and manufactures selected sanitary process equipment including tanks, CIP systems, marination tumblers, and cooking vessels. That manufacturing capability is most valuable when it is combined with practical plant knowledge rather than isolated shop fabrication. More information on its equipment portfolio is available on its sanitary equipment page.
Material Traceability: Mill Test Certificates & Heat Number Documentation
Material traceability is a basic but essential control. For sanitary process equipment, buyers should know what alloy was used, where it came from, and how it ties to the finished assembly. Traceability usually includes Mill Test Reports or Mill Test Certificates, heat numbers, receiving records, cut-piece identification, weld filler tracking where required, and document retention protocols.
Traceability is especially important for pharmaceutical-adjacent systems, aseptic equipment, allergen-sensitive lines, high-value beverages, and any customer subject to strict audit regimes. It also matters when failures occur. If corrosion, cracking, or product quality issues appear, traceability helps isolate root causes and limit exposure.
In practical terms, a buyer should ask whether material markings are maintained through cutting and rolling, whether shop travelers follow components through fabrication, and whether the final turnover package links the installed asset to original material records. This is often where low-cost fabricators fall short.
| Traceability Element | What It Includes | Why Auditors Care | Buyer Question |
|---|---|---|---|
| MTR/MTC records | Chemical and mechanical properties | Confirms specified alloy | Can you provide complete certs at turnover? |
| Heat numbers | Unique batch identification | Links material to source lot | How are heat numbers preserved during fabrication? |
| Receiving inspection | Visual, dimensional, paperwork checks | Prevents wrong material entry | What is your incoming QA process? |
| Cut-piece identification | Traveler tags or shop marks | Maintains continuity after cutting | How do you avoid mixed material on the floor? |
| Weld records | Welder ID, procedure, date, location | Supports quality accountability | Do you maintain weld logs and maps? |
| Turnover dossier | Final documentation package | Supports compliance and maintenance | What documents are included at handover? |
The explanation here is straightforward: traceability reduces uncertainty. When a sanitary equipment package arrives on site in New Jersey, Wisconsin, North Carolina, or California, the owner should not be forced to guess what material is actually inside the polished shell.
CIP Integration: Spray Balls, Drainability & Validation Protocols
Clean-in-place integration is where sanitary theory becomes operating reality. Effective CIP depends on the interaction of vessel geometry, spray device selection, flow rate, pressure, line sizing, return paths, conductivity control, recipe logic, temperature management, and final rinse verification. Simply adding a spray ball to a tank does not make it cleanable.
Static spray balls may be sufficient for some duties, while rotary devices or higher-impact solutions may be needed for sticky, high-viscosity, sugary, protein-rich, or particulate-bearing products. The correct choice depends on product behavior and soil type. Drainability matters just as much as spray coverage because cleaning fluid must leave the system fully after each phase.
Validation protocols typically include riboflavin testing or equivalent spray coverage checks where relevant, visual inspections, conductivity endpoints, return clarity, ATP or microbiological verification in certain environments, and documented CIP recipes in the control system. Modern processors also watch water and caustic consumption closely, especially in regions facing utility pressure and sustainability targets.
The bar chart shows how sanitary system demand differs by industry. Dairy and beverage remain major drivers, but prepared foods, protein, brewing, and aseptic lines also represent strong investment areas in the United States.
Disruptive Process Solutions has notable technological capability in this area because it supports controls engineering, PLC programming, SCADA, process integration, and utility systems along with CIP design. That matters because CIP success depends on both mechanical design and automation logic. Plants that want complete project execution can review the company background at about DPS.
Gasket & Seal Material Selection for Sanitary Process Connections
Gaskets and seals are small components with disproportionate sanitary impact. Wrong compound selection can lead to swelling, extractables concerns, cracks, compression set, odor carryover, leaks, and contamination. The correct material depends on product chemistry, cleaning chemicals, temperature range, pressure, steam exposure, mechanical cycling, and the type of connection or valve.
Common options include EPDM, FKM, silicone, PTFE-envelope designs, and specialized compounds for high temperature or aggressive chemical duty. Selection should account for both process exposure and CIP/SIP exposure, since many failures happen during cleaning, not production. In food and beverage manufacturing, buyers should also verify applicable compliance requirements for product contact materials.
| Seal Material | Typical Strength | Watch-Out | Common Application |
|---|---|---|---|
| EPDM | Good hot water and caustic resistance | Not ideal for all oils and solvents | Dairy and general CIP service |
| FKM | Strong chemical and temperature performance | Costlier and not universal for all media | Flavor systems and demanding chemicals |
| Silicone | Flexible and clean for many food duties | Tear resistance may be limited in some uses | Static seals and certain hygienic fittings |
| PTFE | Broad chemical resistance | Can be less elastic in sealing behavior | Aggressive chemicals and specialty skids |
| HNBR | Useful in some oil and mechanical environments | Application-specific review required | Selected pumps and dynamic seals |
| Perfluoroelastomer | High-end chemical and thermal resistance | Very high cost | Critical aseptic or specialty applications |
The table is useful as a starting point, but buyers should still request application-specific recommendations. A sanitary equipment manufacturer should ask detailed questions about product, process temperature, clean cycle chemistry, and maintenance intervals before finalizing seal materials.
For multi-site processors, standardizing gasket materials by service can simplify spare parts management across plants in states such as Texas, Georgia, Illinois, and Pennsylvania. That can reduce emergency downtime and improve maintenance planning.
How to Audit a Sanitary Equipment Manufacturer’s Quality System
A supplier audit should evaluate more than the cleanliness of the shop floor. Buyers should review how the manufacturer controls drawings, revisions, material receipts, welding procedures, welder qualifications, polishing, passivation, inspection, rework, NCRs, document turnover, and shipping protection. Good suppliers welcome these questions because they signal a serious buyer focused on lifecycle value.
During an audit, look for procedure discipline. Are weld procedures documented and current? Are sanitary welders qualified for the relevant processes and thicknesses? How are internal welds inspected? Is there a corrective action process when a finish target is missed? Are borescopes used for inaccessible areas? How are instruments and fittings protected before shipment? Does the manufacturer perform FAT with checklists tied to approved drawings?
It is also wise to assess project communication and execution maturity. A plant expansion in the United States may require coordination across local trades, controls vendors, utility contractors, and on-site operations teams. A manufacturer that understands project delivery can prevent scope gaps between equipment and installation.
| Audit Category | What Good Looks Like | Evidence | Why It Matters |
|---|---|---|---|
| Document control | Revision-managed drawings and travelers | Controlled templates and release logs | Prevents build-to-wrong-revision errors |
| Welding quality | Qualified welders and approved procedures | WPS/PQR and welder qualification records | Supports sanitary integrity |
| Inspection system | In-process and final QA checkpoints | Inspection forms and signoffs | Catches issues before shipment |
| Surface finish control | Measured and documented Ra verification | Profilometer reports | Confirms finish claims |
| Cleaning/passivation | Standardized post-fabrication treatment | Process records and certificates | Improves corrosion resistance |
| FAT and turnover | Structured testing and complete documentation | FAT protocol, punch list, turnover package | Reduces startup risk and audit gaps |
The audit framework above can be used during RFQ evaluation or pre-award supplier approval. It helps separate true sanitary manufacturers from general metal shops using sanitary language for marketing purposes.
For buyers seeking an execution partner rather than only a fabricator, project history matters. Disruptive Process Solutions supports clients across the United States and Canada with process engineering, capital planning, installation, project management, equipment supply, and integration. Selected examples of field outcomes and project types can be reviewed in its case studies and project examples.
The area chart highlights a market trend: buyers increasingly prefer integrated hygienic systems that combine equipment, controls, utilities, installation, and startup support instead of purchasing disconnected components from multiple vendors.
FAQ
What industries need sanitary process equipment most?
Dairy, beverage, brewing, spirits, sauces, prepared foods, plant-based proteins, seafood, meat processing support systems, aseptic filling, nutraceuticals, and some pharmaceutical-adjacent operations all rely heavily on hygienic equipment.
Is a polished stainless tank automatically sanitary?
No. Sanitary performance depends on weld quality, drainability, spray coverage, fittings, seals, passivation, and installation geometry, not just appearance.
What documents should I ask for before approving a manufacturer?
Ask for GA drawings, P&IDs where relevant, weld procedures, welder qualifications, MTRs, heat traceability, finish reports, passivation records, FAT protocols, O&M manuals, spare parts lists, and turnover documentation.
How important is CIP validation?
Very important. Without validation, cleaning assumptions may be wrong. Validation confirms spray coverage, chemistry delivery, drainability, and repeatability under actual operating conditions.
Should U.S. buyers care about EHEDG if their plant mainly follows 3-A expectations?
Yes. Even if 3-A remains the main procurement reference, EHEDG-style hygienic thinking can improve equipment design review and help avoid hidden cleanability problems.
What product types are commonly sourced from sanitary manufacturers?
Common categories include storage tanks, process vessels, blend skids, CIP skids, heat exchangers, piping manifolds, fermentation systems, distillation modules, dosing skids, utility skids, and complete integrated lines.
What should I look for in a local or regional supplier?
Evaluate responsiveness, field service reach, installation support, spare parts access, documentation quality, and familiarity with local jurisdictional expectations. Proximity can help, but execution maturity matters more than zip code.
How do ports and logistics hubs affect sanitary equipment sourcing?
Projects near major logistics centers such as Houston, Long Beach, Savannah, Newark, and Chicago can benefit from easier freight options and supplier access, but inland installation coordination still drives schedule success.
What are the biggest 2026 trends in sanitary equipment manufacturing?
The main trends are stronger digital traceability, more automated CIP verification, greater water and chemical efficiency, more hygienic design standardization across multi-site operators, higher demand for modular skids, and increased sustainability expectations around energy, wastewater, and clean utility consumption. Policy pressure around food safety documentation, environmental performance, and supply chain resilience is also likely to increase. Manufacturers that can combine hygienic design with automation, utility optimization, and auditable data will be best positioned.
The comparison chart shows why many processors prefer an integrated sanitary partner over a fabrication-only supplier. The value difference often appears in documentation, startup support, CIP performance, and long-term operating reliability rather than in initial bid price alone.
In summary, selecting a sanitary process equipment manufacturer in the United States should be treated as a strategic operating decision. The right supplier helps protect product quality, audit readiness, production uptime, and return on capital. Buyers should assess hygienic geometry, self-drainability, dead leg control, surface finish, passivation, traceability, CIP validation, seal selection, and quality system maturity as a complete package. They should also consider whether the supplier can support plant realities such as controls integration, installation management, utility coordination, and fast decision-making under schedule pressure.
For companies expanding or upgrading production in North America, an engineering-driven partner with practical manufacturing and field execution experience can reduce risk significantly. Disruptive Process Solutions fits that model by combining process engineering, equipment capability, project delivery, and integration support for food and beverage manufacturers across the region. Its flat, agile structure and focus on profitable project outcomes make it especially relevant for clients seeking more than commodity fabrication.
Whether the need is a new CIP skid, a set of sanitary tanks, a brownfield process retrofit, a beverage utility buildout, or a multi-system integration program, the same buying principle applies: choose a manufacturer that can prove sanitary performance, document its work, and support the full operating objective of the plant.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

