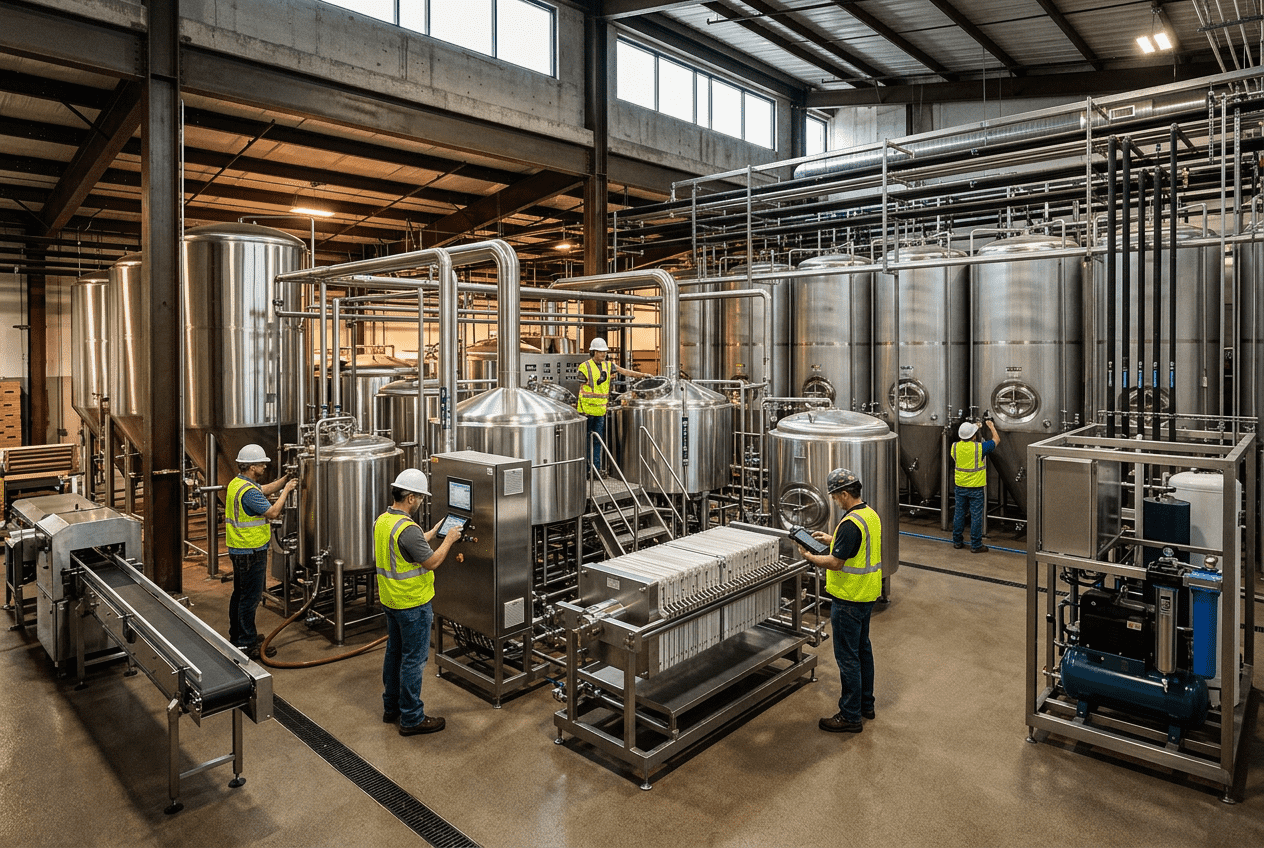
Ready-to-Drink Beverage Manufacturing Solutions
[trp_language language=”en_US”]
RTD Beverage Manufacturing Strategies in the United States
Ready-to-drink beverage manufacturing in the United States requires more than a filler and a formula. Successful RTD programs depend on water treatment, ingredient handling, thermal processing, packaging selection, microbiological control, cost discipline, and a facility layout designed for profitable scale. Whether a brand is launching canned cold brew in Austin, shelf-stable protein shakes in Chicago, juice blends near the Port of Los Angeles, or functional beverages distributed through New Jersey and Atlanta, the best results come from aligning product design with processing technology, distribution realities, and capital planning from day one.
Quick Answer

RTD beverage manufacturing solutions combine process engineering, batching, thermal treatment, filling, packaging, utilities, automation, quality assurance, and distribution planning into one integrated production model. In the United States, the right solution depends on product acidity, ingredients, desired shelf life, sales channel, expected run rate, and whether the brand will use a contract manufacturer or build in-house capacity.
For most brands, the fastest path to market is to validate the formulation, processing method, and packaging format before making major capital commitments. For growing operators and co-packers, the highest-value investment is usually not a single machine but a well-designed system: syrup rooms, CIP, pasteurization or aseptic capability, tankage, utilities, controls, and plant flow that support both current volumes and future expansion.
Manufacturers evaluating new capacity often benefit from working with a partner that understands both engineering and commercial performance. Disruptive Process Solutions approaches these projects from a profitability-first perspective, helping food and beverage operators structure smart capital programs rather than simply buying equipment in isolation.
The RTD Manufacturing Process: From Water Treatment to Packaged Product

The RTD manufacturing process begins with water, because water quality affects flavor, microbiological risk, process consistency, and equipment life. In the United States, many facilities treat municipal or well water with carbon filtration, softening, reverse osmosis, UV disinfection, and ozone or other sanitizing methods depending on the beverage profile. A sports drink line in Phoenix may prioritize mineral consistency and taste neutrality, while a tea bottler in North Carolina may balance flavor retention with local source characteristics.
After water treatment, ingredients move into a controlled batch preparation environment. This can include dry ingredient handling, liquid ingredient receiving, syrup blending, hydration, heating, high-shear mixing, inline metering, homogenization, deaeration, and carbonation where needed. Product is then routed to the relevant processing step such as HTST pasteurization, tunnel pasteurization, retort, or aseptic sterilization and fill.
Once filled into cans, PET, glass, cartons, or pouches, the beverage is coded, inspected, packed, palletized, and released based on QA protocols. Each step has to support not only food safety but also throughput and line efficiency. In high-volume U.S. markets like Southern California, Dallas-Fort Worth, and central Pennsylvania, the biggest hidden losses often come from poor material flow, undersized utilities, changeover delays, and weak integration between process and packaging systems.
| Process Stage | Primary Purpose | Typical Equipment | Main Risk if Underspecified | U.S. Operational Consideration | Business Impact |
|---|---|---|---|---|---|
| Water treatment | Stabilize source water quality | RO, carbon filters, UV, ozone | Flavor inconsistency, scale, microbial risk | Varies by municipal source and region | Brand inconsistency and rework |
| Ingredient receiving | Protect raw material integrity | Totes, pumps, dust collection, unload stations | Contamination, handling loss | Supplier lead times may vary by port region | Delays and yield loss |
| Batch preparation | Create repeatable formulation | Mix tanks, load cells, high-shear mixers | Poor dispersion, inaccurate dosing | Labor skill level affects repeatability | Off-spec product |
| Thermal or aseptic process | Control pathogens and spoilage organisms | HTST, UHT, retort, aseptic system | Shelf-life failure | Method tied to channel and product type | Recalls or reduced market access |
| Filling and closure | Protect product during packaging | Can filler, PET filler, carton filler | Oxygen pickup, leaks, contamination | Line choice depends on retailer requirements | Spoilage and returns |
| Secondary packaging | Prepare for warehouse and transport | Case packer, tray packer, palletizer | Damage in transit | E-commerce and club formats differ widely | Distribution inefficiency |
The table above shows why RTD production should be engineered as a continuous system rather than a collection of disconnected machines. A line may have enough filler speed on paper but still underperform if upstream batching, CIP recovery, or cooling capacity is weak.
Contract Manufacturing vs In-House Production: Strategic Considerations

One of the most important choices for an RTD brand is whether to work with a co-packer or build internal manufacturing. Contract manufacturing can lower initial capital exposure, accelerate launch timing, and provide access to specialized process capabilities such as aseptic packaging or retort. This approach is often ideal for emerging brands selling through regional grocery, convenience, or direct-to-consumer channels.
In-house production makes sense when volume is stable, margins justify capital investment, proprietary process control matters, or the product portfolio is too complex for shared-line scheduling. Companies distributing through major U.S. chains from Miami to Seattle often move to owned production when freight costs, service requirements, and speed-to-market outweigh co-packing flexibility.
The right decision depends on product complexity, minimum run sizes, warehousing strategy, geographic reach, quality requirements, and tolerance for operational risk. Brands with dairy-based, low-acid, or particulate-containing drinks may find that suitable contract capacity is limited. In those cases, a structured engineering review and phased capital plan can create a better long-term outcome.
For companies considering plant expansion, utility upgrades, or a new production line, process engineering and capital planning services can clarify the true bottlenecks before money is committed. Sometimes the most profitable answer is new capacity; other times it is controls optimization, better CIP sequencing, or a redesigned tank farm.
| Decision Factor | Contract Manufacturing | In-House Production | Best Fit Scenario | Key Risk | Strategic Note |
|---|---|---|---|---|---|
| Capital requirement | Low upfront | High upfront | Early-stage launch | Higher unit cost | Useful for proof of concept |
| Speed to market | Usually faster | Slower to build | Retail launch window | Co-packer scheduling delays | Secure production slots early |
| Process control | Shared standards | Full control | Complex formulations | Execution burden shifts to owner | Critical for premium quality claims |
| Scalability | Depends on partner capacity | Designed to target scale | Long-term volume growth | Overbuilding or underbuilding | Phased expansion is often best |
| Confidentiality | Moderate | High | Proprietary formulations | Internal QA burden | Important for IP-sensitive products |
| Gross margin potential | Lower at scale | Higher at scale | Mature national brand | Capital recovery pressure | Requires disciplined utilization |
This comparison is most useful when matched to actual distribution lanes and channel economics. For example, a brand shipping from a Midwest co-packer to West Coast natural retailers may discover freight is eroding margin faster than expected. In-house production near inland hubs like Kansas City or Memphis can improve reach, while coastal sites near Long Beach, Savannah, or Newark may better support import-heavy ingredient programs.
Beverage Processing Technologies: Pasteurization, UHT, Aseptic, and Retort
Processing technology determines shelf life, product quality, packaging options, and plant complexity. Acidified beverages, teas, juices, dairy beverages, plant-based drinks, and functional RTDs all have different microbial and stability demands. The four most common approaches are pasteurization, UHT, aseptic processing, and retort.
HTST and flash pasteurization are common for products that will be hot-filled or rapidly filled after heat treatment. Tunnel pasteurization is widely used in packaged beverages, especially in glass and cans. UHT extends shelf life by heating product at very high temperature for a short time, but it is most effective when paired with aseptic handling and filling. Retort is valuable for highly shelf-stable packaged products, especially where particulates, dense formulas, or certain food-service applications are involved.
The right technology is not simply the most advanced one. It is the one that fits the beverage, the package, the sales channel, and the economics. A low-acid protein shake sold nationally through ambient distribution may justify UHT and aseptic fill. A refrigerated kombucha line in Portland may be better served by different process controls. A nutraceutical beverage in glass for specialty retail may fit tunnel pasteurization better than aseptic conversion.
| Technology | Typical Use | Shelf-Life Potential | Packaging Compatibility | Capital Complexity | Main Advantage |
|---|---|---|---|---|---|
| HTST / Flash Pasteurization | Juices, teas, acid beverages | Moderate | PET, glass, cans with proper fill strategy | Medium | Good balance of quality and cost |
| Tunnel Pasteurization | Packaged carbonated or still beverages | Moderate to high | Cans and glass | Medium | Post-fill treatment |
| UHT | Dairy, plant-based, nutrition drinks | High | Usually paired with aseptic packaging | High | Long ambient shelf life |
| Aseptic Processing | Sensitive shelf-stable products | High | Cartons, bottles, specialty formats | Very high | Quality retention and shelf stability |
| Retort | Dense beverages, culinary liquids, specialty packs | Very high | Cans, pouches, trays, some bottles | High | Strong lethality assurance |
| HPP support model | Premium refrigerated beverages | Moderate refrigerated | Flexible bottles and select packs | Medium to high | Cold-processed positioning |
The chart below illustrates how U.S. demand for processing methods differs by category. Shelf-stable nutrition and functional products continue to shift demand toward aseptic and UHT, while premium refrigerated categories keep HPP and chilled pasteurized systems relevant.
On the technology side, DPS supports beverage systems that include pasteurization, UHT, retort, aseptic integration, filtration, carbonation, inline Brix control, water treatment, automation, and SCADA. This breadth matters because beverage projects fail when thermal systems, utilities, controls, and packaging are designed separately instead of as one operating platform.
Ingredient Handling and Batch Preparation for RTD Production
Ingredient handling is where many RTD lines gain or lose efficiency. Functional beverages, energy drinks, coffee-based RTDs, dairy alternatives, and enhanced waters often use a mix of powders, sweeteners, acids, flavors, concentrates, vitamins, emulsions, and stabilizers. These materials require appropriate receiving, storage, metering, hydration, and allergen or sanitation controls.
Dry handling systems should reduce dust, improve operator safety, and support accurate dosing. Liquid ingredient systems should account for viscosity, temperature sensitivity, tote or drum changeovers, and transfer sanitation. For emulsified or protein-rich products, high-shear mixing and homogenization become essential. For sugar-reduced beverages, sweetener sequencing and flavor masking can affect both batch consistency and sensory quality.
Batch preparation also has to support repeatability across shifts and plants. Load cells, recipe automation, inline Brix monitoring, conductivity tracking in CIP, and historian data allow managers to reduce giveaway and tighten specifications. In busy co-packing regions such as the Midwest and Southeast, these controls often separate profitable plants from plants that appear busy but suffer from chronic yield loss.
When manufacturers need purpose-built tanks, CIP skids, or integrated process components, custom process equipment solutions can be a practical way to align equipment with the actual formulation and sanitation demands of the line.
| Ingredient Type | Handling Need | Common Equipment | Critical Control Point | Typical Failure Mode | Improvement Opportunity |
|---|---|---|---|---|---|
| Powders | Dust control and accurate dosing | Sack dump, vacuum transfer, hopper | Lot control and dispersion | Clumping or loss | Automated transfer and pre-wet systems |
| Sweeteners | Viscosity and temperature management | Heated tanks, meters, pumps | Dose accuracy | Brix drift | Inline metering |
| Acids and flavors | Small-volume precision | Day tanks, dosing pumps | Recipe sequence | Flavor imbalance | Recipe automation |
| Proteins | Hydration and shear control | High-shear mixer, homogenizer | Foaming and solubility | Texture defects | Optimized hydrate time |
| Concentrates | Temperature stability | Totes, transfer pumps | Sanitary transfer | Microbial contamination | Closed transfer systems |
| Functional actives | Traceability and potency | Precision dosing, lot tracking | Micro-dose validation | Out-of-spec claim levels | Automated verification |
This table highlights a recurring issue in RTD operations: the formulation may be excellent in the lab but unstable in production if ingredient handling was not engineered for real run conditions. Scale-up should always include mixing energy, residence time, heat history, and cleanability.
Quality Assurance: Microbial Testing, Shelf Life Validation, and Brix Control
Quality assurance is not a final inspection task; it is a design discipline. RTD beverage QA in the United States must align formulation, processing, packaging, sanitation, environmental monitoring, release criteria, and regulatory expectations. Microbial testing should fit the product type and hazard profile. Shelf-life studies should evaluate not only microbiological stability but flavor drift, separation, color change, nutrient retention, carbonation, and package interaction over time.
Brix control is especially important in sweetened, juice-based, and concentrate-driven products because even small deviations affect taste, nutrition panels, and cost of goods. Inline Brix instruments, calibrated lab checks, and robust recipe control can reduce variability. In functional beverages, pH and active-content verification often matter just as much.
For shelf-stable products, validation should include challenge studies where appropriate, process authority review, thermal mapping, closure integrity, and warehouse simulation. This is especially important for brands shipping across varied climates from Florida humidity to Arizona heat to upper Midwest winter conditions.
DPS has experience supporting FDA, USDA, SQF, and BRC-driven environments, which matters for operators building systems that need to pass audits, maintain sanitation integrity, and scale cleanly across product lines.
| QA Measure | What It Verifies | Typical Frequency | Relevant Products | Business Value | If Neglected |
|---|---|---|---|---|---|
| Microbial testing | Pathogen and spoilage control | Lot-based and environmental routine | All RTD categories | Safety and compliance | Recall exposure |
| Brix measurement | Sugar solids consistency | Batch and inline | Juice, tea, energy, soft drinks | Taste and cost control | Off-spec flavor and giveaway |
| pH verification | Acid control and process fit | Every batch | Acidified drinks | Safety margin | Shelf-life failure |
| Shelf-life study | Performance over time | Per SKU and packaging change | All distributed products | Distribution confidence | Retail complaints |
| Seal and closure integrity | Package security | Shift checks and validation | Cans, bottles, cartons, pouches | Leak and oxidation control | Returns and spoilage |
| CIP verification | Sanitation effectiveness | Every clean cycle | All process lines | Hygiene and uptime | Biofilm and contamination risk |
The explanation behind these controls is straightforward: every QA variable is tied directly to margin. A rejected batch, a short shelf life, or excessive product giveaway can erase the value of a seemingly efficient line.
Packaging Format Selection for RTD Distribution Channels
Packaging selection shapes not only consumer appeal but also processing method, freight profile, retailer acceptance, and sustainability performance. Cans remain strong for sparkling waters, cocktails, coffee, tea, and energy beverages because they stack efficiently, chill quickly, and fit convenience and club channels. PET is still common for juices, teas, and still beverages, although recycling expectations continue to influence resin selection and lightweighting.
Aseptic cartons are attractive for ambient nutrition and plant-based drinks, especially in grocery and food-service channels. Glass can support premium positioning but adds freight cost and breakage risk. Flexible pouches may fit certain kids, sports, or value formats but require careful compatibility assessment.
Distribution channel matters. A single-serve bottle for c-store in Houston may not be the right format for e-commerce fulfillment in California or club multipacks in the Midwest. Warehouse temperature, pallet pattern stability, retailer shelf dimensions, and returns handling all affect the final choice.
| Packaging Format | Best Channel Fit | Process Compatibility | Freight Efficiency | Sustainability Position | Common Trade-Off |
|---|---|---|---|---|---|
| Aluminum can | Convenience, club, grocery | Carbonated, still, pasteurized | High | Strong recyclability story | Dent sensitivity |
| PET bottle | Mass retail, grocery, c-store | Hot fill, cold fill, some aseptic | High | Improving with recycled content | Heat and oxygen limitations |
| Glass bottle | Premium retail, food service | Pasteurized products | Low | Reusable/recyclable in some systems | Weight and breakage |
| Aseptic carton | Ambient grocery, nutrition, schools | Aseptic and UHT | High | Good cube efficiency | Specialized filling infrastructure |
| Pouch | Kids, sports, export niches | Hot fill or retort depending design | High | Lightweight | Recycling challenges |
| Multi-serve HDPE or specialty bottle | Food service, refrigerated | Cold fill or pasteurized | Medium | Varies by resin stream | Shorter shelf-life fit |
Below is a comparison chart showing relative market attractiveness by packaging type for broad U.S. RTD distribution use cases.
Manufacturing capability must match packaging ambition. DPS supports complete system integration from process utilities and controls to physical installation, which is particularly valuable when a beverage producer is adding a new package format without disrupting existing operations.
Three S Trends: Shelf-Stable, Sustainable, and Single-Serve RTD Manufacturing
Three trends are reshaping the U.S. RTD landscape: shelf-stable, sustainable, and single-serve. Shelf-stable products continue gaining traction because they simplify distribution, reduce cold-chain cost, and open national retail reach. This is driving interest in UHT, aseptic, retort, and improved ambient packaging formats.
Sustainability is influencing both engineering and procurement. Manufacturers are under pressure to reduce water consumption, chemical use, packaging weight, utility intensity, and waste. In 2026, the strongest plants will combine efficient CIP recovery, heat recovery, smart compressed air management, recyclable or reduced-material packaging, and better production scheduling to cut changeover waste.
Single-serve remains powerful because U.S. consumers value portability, portion control, and convenience. This trend is particularly strong in convenience stores, airports, stadiums, campus retail, and grab-and-go grocery environments. Cities like New York, Chicago, and Los Angeles continue to reward fast-moving single-serve formats, especially in functional hydration, energy, coffee, and protein categories.
Policy and market trends are also shaping the future. Extended producer responsibility discussions, stricter sustainability reporting, retailer packaging standards, and growing scrutiny of ingredient claims will push beverage producers to invest in traceability, automation, efficient utilities, and better package design.
The area chart shows why future-ready RTD manufacturing in the United States is less about one trend and more about convergence. The plants that win will be flexible enough to produce shelf-stable products, efficient enough to meet sustainability goals, and agile enough to serve high-velocity single-serve channels.
Cost Structure and Profitability Analysis for RTD Manufacturing
RTD profitability depends on more than unit conversion cost. The full cost structure includes ingredients, packaging, labor, utilities, quality testing, sanitation chemicals, downtime, changeover loss, freight, warehousing, spoilage, depreciation, and working capital. In many U.S. beverage operations, packaging is the largest single cost element after ingredients, followed by labor and utilities depending on the process type.
Aseptic and UHT systems can improve distribution economics by eliminating refrigeration and extending shelf life, but they require higher capital and technical discipline. Retort adds flexibility in some applications but can influence package cost and throughput. Hot fill and conventional pasteurized systems may be more economical for certain acid products at regional scale.
Plant design has a direct effect on margin. Poor equipment placement increases labor. Inadequate tankage creates filler starvation. Weak automation increases giveaway. Underbuilt utilities reduce uptime. A properly engineered project often produces profit gains that far exceed the savings from choosing the cheapest equipment vendor.
This is where DPS is differentiated operationally. Its approach combines design, build, and execution management with a business-minded view of capital efficiency. The firm works across North America on beverage, food, aseptic, and process utility projects, helping manufacturers plan facilities that can reach first-year profitability instead of becoming expensive bottlenecks.
| Cost Category | Typical Share of RTD COGS | Main Drivers | High-Risk Scenario | Optimization Lever | Margin Impact |
|---|---|---|---|---|---|
| Ingredients | 20% to 40% | Sweeteners, proteins, actives, concentrates | Commodity volatility | Formula and yield control | High |
| Packaging | 25% to 45% | Cans, bottles, cartons, closures, trays | Minimum order pricing | Format rationalization | Very high |
| Labor | 8% to 18% | Staffing model, skill level, overtime | Manual changeovers | Automation and line design | Medium to high |
| Utilities | 4% to 12% | Steam, chilled water, compressed air, water | Inefficient thermal systems | Heat recovery and controls | Medium |
| QA and sanitation | 2% to 8% | Testing, CIP, chemicals | Excessive clean time | CIP optimization | Medium |
| Freight and warehousing | 8% to 20% | Network design, package density, distance | Remote co-packer dependence | Plant location strategy | Very high |
This table is a reminder that the cheapest manufacturing option is not always the most profitable one. Freight from one side of the country to the other, especially for heavier glass or low-cube formats, can quickly erase savings from lower copacking rates.
Manufacturers seeking evidence of how integrated project execution performs in the field can review selected process and facility case studies that reflect practical challenges such as utility infrastructure, layout optimization, and scalable beverage operations.
FAQ
What is the best processing method for a new RTD beverage?
The best method depends on pH, formulation, particulates, shelf-life target, package type, and distribution model. Acid beverages may fit pasteurization or hot fill, while low-acid dairy or plant-based products often need UHT with aseptic handling.
When should a brand move from a co-packer to its own plant?
Usually when annual volume is high enough to support equipment utilization, margins are compressed by co-packing and freight, or the brand needs tighter quality and scheduling control. A phased economic model should be built before committing capital.
How important is water treatment in RTD manufacturing?
It is foundational. Water chemistry affects taste, stability, thermal performance, and equipment maintenance. Regional source variation across the United States makes site-specific treatment design essential.
Which package is best for national distribution?
There is no universal answer, but cans, PET, and aseptic cartons are the most common choices for national reach because they balance channel acceptance, freight efficiency, and consumer convenience.
What quality metrics should be monitored on every batch?
At minimum, manufacturers typically monitor Brix, pH, sensory profile, fill volume, package integrity, coding, and relevant microbiological indicators based on the hazard profile.
What are the biggest hidden costs in RTD production?
Common hidden costs include downtime, product giveaway, sanitation overruns, poor line balancing, freight inefficiency, changeover waste, and underbuilt utilities that choke production capacity.
How is 2026 expected to change RTD manufacturing in the United States?
Expect more shelf-stable product launches, stronger sustainability requirements, wider use of automation and recipe control, tighter packaging scrutiny, and continued growth of single-serve convenience formats.
What kind of partner should a manufacturer look for?
A strong partner should understand process engineering, utilities, installation, compliance, automation, project execution, and commercial reality. The best teams help clients avoid misallocated capital, not just purchase machinery.
Across the United States, from beverage corridors in California and Texas to manufacturing centers in the Carolinas, Ohio, and the upper Midwest, RTD success comes from disciplined integration. The product, process, package, utility system, and business model must all support each other. Companies that plan this early can enter the market faster, protect shelf life, control cost, and scale with confidence.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

