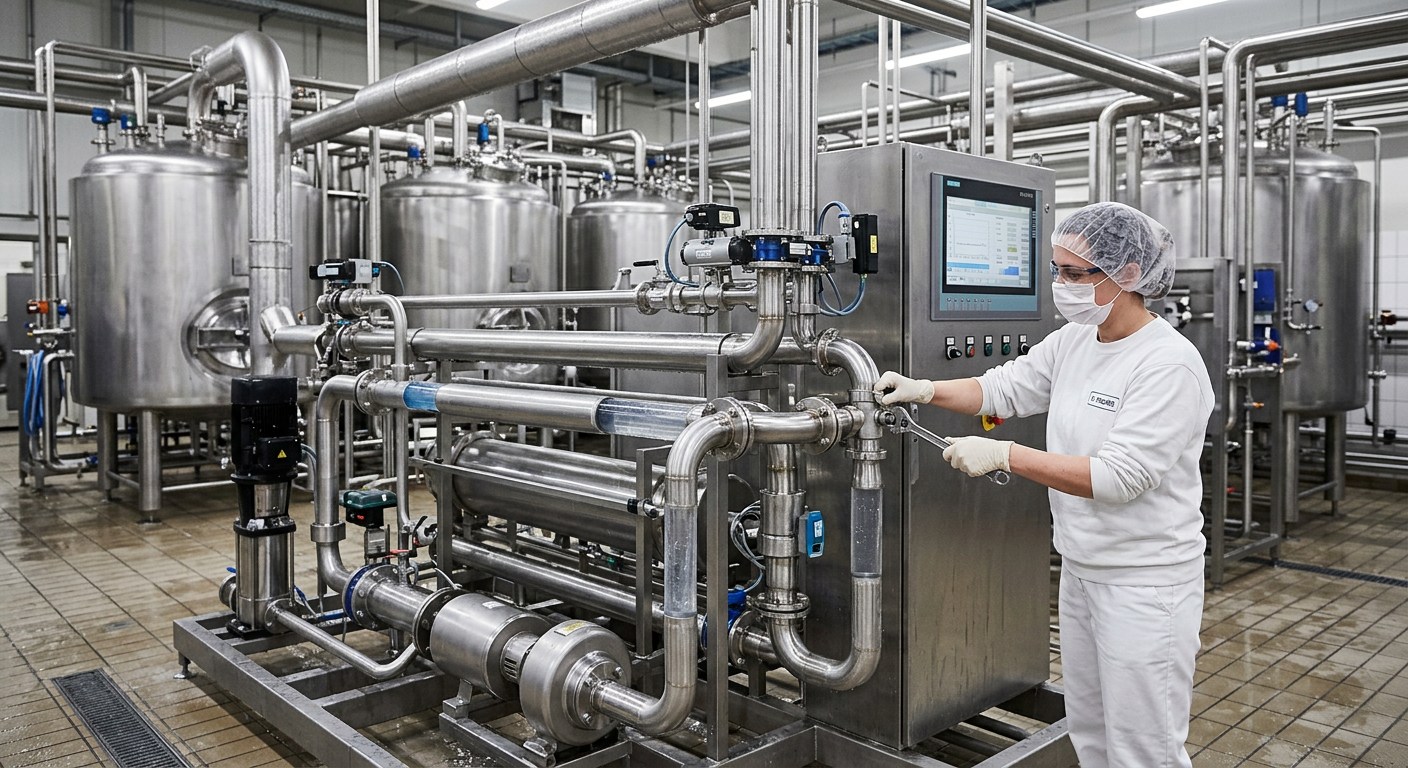
5 Essential Components of Industrial Pasta Production Line Design
[trp_language language=”en_US”]
Industrial Pasta Line Design Guide for the United States
Designing an industrial pasta production line is not only about choosing an extruder and a dryer. In the United States, successful projects depend on how well the full system is engineered around product quality, throughput, sanitation, labor efficiency, utilities, and future expansion. For manufacturers producing dry pasta, fresh pasta, macaroni, long-cut pasta, or short-cut shapes, the most important design elements are vacuum extrusion, controlled drying, reliable raw material handling, fast die changeovers, gentle cooling and stabilization, integrated packaging, and sanitary equipment design with validated cleaning practices.
Those seven building blocks affect almost every commercial outcome: texture, cooking tolerance, breakage rate, moisture stability, labor cost, yield, shelf life, and SKU flexibility. They also shape how a facility performs in major U.S. food manufacturing regions such as Chicago, Minneapolis, Kansas City, Fresno, Dallas-Fort Worth, and the Carolinas, where ingredient logistics, utilities, and labor realities vary by market. Companies serving retail, foodservice, private label, school nutrition, meal kits, and contract manufacturing need line designs that fit their real business model, not just an equipment brochure.
This guide explains what buyers, plant managers, engineers, and operations leaders should evaluate when planning a new line, expanding a facility, or modernizing legacy equipment. It also highlights how integrated engineering and execution can reduce capital waste and improve profitability over the long term.
Quick Answer

The five most critical components in industrial pasta production line design are actually part of a wider integrated system: raw material receiving and storage, vacuum extrusion and forming, drying or thermal stabilization, post-forming handling and cooling, and end-of-line packaging under sanitary conditions. In practice, the best-performing U.S. pasta plants treat these as one engineered process rather than separate machines.
For dry pasta, the core priority is moisture control from semolina storage through extrusion, pre-drying, final drying, tempering, cooling, and packaging. For fresh pasta, the priorities shift toward dough consistency, microbial control, cold chain strategy, fast cleaning, and packaging atmosphere. Macaroni and other short-cut formats require strong cutter synchronization and die management, while spaghetti, linguine, and similar long-cut products require careful strand handling, hanging or spreading systems, and controlled stabilization to preserve shape.
Buyers in the United States should also assess utility loads, sanitation access, labor needs, spare parts availability, automation integration, and whether the line can support future product diversification. A system that looks cheaper on paper can become more expensive if it creates higher breakage, slower changeovers, poor drying uniformity, or cleaning downtime.
| Design Area | Primary Goal | Main Risk if Undersized | Main Risk if Overdesigned | Best Fit Products | Key KPI |
|---|---|---|---|---|---|
| Semolina handling | Stable ingredient flow and quality | Bridging, contamination, dust losses | Unnecessary capital cost | All pasta types | Feed consistency |
| Vacuum extrusion | Dense, uniform dough structure | Air pockets, weak texture | High energy use | Dry and fresh pasta | Product density |
| Drying system | Moisture reduction and stability | Cracks, uneven moisture | Excess dwell time | Dry pasta | Final moisture |
| Cooling conveyor | Shape retention after forming or drying | Deformation, sticking | Excess floor space | Short-cut and filled pasta | Breakage rate |
| Packaging integration | Throughput and shelf-life protection | Bottlenecks, product damage | Idle packaging capacity | Fresh and dry pasta | OEE |
| Sanitary design and CIP | Food safety and uptime | Microbial harborage | Complex maintenance | Fresh pasta especially | Cleaning validation |
The table above shows why line design decisions must be balanced. The goal is not to maximize one machine specification. The goal is to create a profitable and reliable production system.
Vacuum Extruder Technology for High-Quality Pasta and Macaroni

Vacuum extrusion is the heart of most industrial pasta and macaroni lines because it directly influences dough density, color, mechanical strength, and finished cooking performance. By removing entrained air before and during extrusion, the process helps create a more homogeneous dough matrix. That matters for both premium quality and line efficiency. In the United States, where plants often run multiple SKU families under tight labor constraints, extruder reliability and process stability are especially valuable.
For macaroni, elbows, shells, rotini, penne, and other short-cut products, vacuum extrusion supports more consistent wall thickness and lower breakage downstream. For spaghetti and long-cut formats, it helps maintain uniform strand structure and smoother surface finish. Manufacturers targeting retail shelves in high-volume corridors such as the Northeast, Midwest, and Southern distribution networks often use vacuum extrusion to reduce cosmetic defects and improve pack appearance.
Key design factors include barrel geometry, screw profile, vacuum chamber performance, dough hydration control, product temperature management, and die material selection. Bronze dies may support a rougher artisanal surface preferred for sauce adhesion, while Teflon-type surfaces may support smoother output and faster production. The correct choice depends on the market position of the product and the needs of the packaging line.
Automation is equally important. Extruders should be tied into recipe management, load monitoring, motor protection, feed rate control, and upstream ingredient dosing. A well-integrated system can reduce startup losses and help plants move more quickly between formulations such as standard semolina pasta, enriched pasta, whole wheat, gluten-free blends, or pulse-based products.
| Extruder Feature | Operational Benefit | Quality Impact | Maintenance Consideration | Best Use Case | Buyer Note |
|---|---|---|---|---|---|
| Vacuum chamber | Air removal | Improves density | Seal inspection required | Premium dry pasta | Critical for consistent texture |
| Variable-speed screw | Flexible throughput | Better process control | Drive calibration | Multi-SKU plants | Useful for co-packers |
| Water dosing control | Stable hydration | Reduces defects | Sensor verification | Fresh and dry lines | High ROI feature |
| Thermal management | Prevents overheating | Protects dough quality | Cooling circuit upkeep | High-output plants | Important in warm climates |
| Quick-change die mount | Shorter changeovers | Maintains alignment | Clamp wear checks | Frequent product switches | Supports SKU growth |
| Integrated controls | Recipe repeatability | Stable lot quality | PLC support needed | Enterprise operations | Prefer open architecture |
The best extruder selection is tied to the entire plant concept. A line designed for grocery private label in Chicago may optimize for output and low scrap, while a premium specialty producer near Los Angeles may prioritize texture, visual differentiation, and smaller batch flexibility. In both cases, vacuum extrusion remains a central technology decision.
Drying System Design with Temperature and Humidity Control

For dry pasta, the drying system is often the largest determinant of final product stability. It is also one of the most misunderstood parts of line design. Drying is not simply hot air exposure. It is a staged, carefully controlled thermal and mass-transfer process in which temperature, humidity, air velocity, dwell time, and product loading must stay in balance.
Improper drying can cause stress cracks, case hardening, poor cooking behavior, uneven color, or moisture variation within the same batch. U.S. plants shipping long distances from manufacturing hubs such as Kansas City, St. Louis, or Memphis to national distribution centers need robust drying profiles to ensure the product survives transportation and warehousing without excessive breakage.
Short-cut pasta usually tolerates different airflow strategies than long-cut pasta, which may require hanging or specially supported handling during critical stages. Product formulation also matters. Whole grain, protein-fortified, legume-based, and gluten-free products often need different moisture removal curves than conventional semolina pasta.
Modern drying systems should include zoned controls, humidity feedback, air recirculation logic, and data logging. Integration with SCADA improves traceability and helps operators diagnose issues quickly. Energy recovery systems are increasingly important as U.S. processors face pressure to improve sustainability and utility efficiency heading into 2026 and beyond.
| Drying Stage | Purpose | Control Variable | Common Failure Mode | Best Monitoring Tool | Impact on Shelf Life |
|---|---|---|---|---|---|
| Pre-drying | Surface stabilization | Air velocity | Surface stickiness | Airflow sensors | Moderate |
| Primary drying | Bulk moisture reduction | Temperature | Stress cracking | Zoned temperature control | High |
| Humidity balancing | Internal moisture equalization | Relative humidity | Case hardening | RH probes | High |
| Final drying | Target moisture achievement | Dwell time | Overdrying brittleness | Moisture analyzer | Very high |
| Tempering | Moisture uniformity | Residence time | Lot inconsistency | Data logging | High |
| Cooling | Packaging readiness | Product temperature | Condensation risk | Infrared temperature checks | Moderate |
The chart and table illustrate why drying design deserves system-level attention. Temperature alone is never enough. The most reliable plants control the full moisture pathway.
Raw Material Handling and Semolina Storage Silo Engineering
Raw material handling sets the foundation for line stability. Semolina, flour, specialty grains, minor ingredients, and process water all need controlled delivery to the mixer or extruder feed system. Poor silo and conveying design can create erratic feed rates, ingredient segregation, dust hazards, and contamination risk long before the product reaches the die.
In the United States, many pasta plants source semolina through inland rail networks, truck lanes, or port-adjacent distribution channels linked to places such as New Orleans, Savannah, Houston, and the Great Lakes region. This means receiving design should reflect actual supply chain patterns, not generic assumptions. A facility near Minneapolis may receive and buffer materials differently than a processor near the Port of Los Angeles or New Jersey logistics corridor.
Engineered silo systems should consider live load, bridging tendencies, refill frequency, dust collection, sanitary access, load cells, pneumatic or mechanical conveying, and allergen segregation where applicable. For plants running both standard semolina and alternative blends, ingredient changeover planning becomes just as important as capacity.
Good raw material systems also support labor reduction. Automated transfer, recipe-controlled batching, and closed conveying can improve operator safety while reducing the chance of ingredient handling errors. When paired with ERP or production planning systems, these designs help plants forecast replenishment and reduce downtime caused by ingredient shortages.
| Raw Material System Element | Function | Engineering Priority | Risk if Poorly Designed | Suitable Facility Type | Practical Note |
|---|---|---|---|---|---|
| Semolina silo | Bulk storage | Flowability | Bridging and inconsistent feed | Large dry pasta plants | Use proper cone geometry |
| Minor ingredient hopper | Micro-dosing | Accuracy | Formula drift | Fortified or specialty lines | Integrate with recipe control |
| Pneumatic conveying | Closed transfer | Line sizing | Particle damage or plugs | Centralized ingredient rooms | Check air-to-product ratio |
| Dust collection | Safety and sanitation | Capture efficiency | Explosion and hygiene issues | All dry ingredient sites | Coordinate with NFPA planning |
| Load cell batching | Weigh control | Calibration | Batch inconsistency | Automated plants | Supports traceability |
| Water conditioning skid | Stable hydration water | Temperature and quality | Dough inconsistency | Fresh and dry pasta | Often overlooked in budgeting |
For many buyers, raw material handling appears less exciting than the extruder or dryer, but it often determines whether the line performs consistently every shift.
Die Changeover Systems for Short-Cut and Long-Cut Pasta Flexibility
SKU proliferation is a reality in the U.S. market. Retailers ask for more shapes, private label buyers want flexibility, and foodservice channels demand different pack and format combinations. That is why die changeover systems are a major design criterion, especially for plants serving both short-cut and long-cut pasta categories.
Fast, repeatable die changes reduce downtime, improve labor efficiency, and support smaller production campaigns without major efficiency losses. They also reduce the risk of alignment errors that can create dimensional defects, cutter problems, or excessive scrap. Plants with older manual die handling often underestimate how much hidden labor and startup waste they are carrying.
For short-cut products, changeover design should coordinate the die, cutter head, knife settings, and downstream transfer geometry. For long-cut products, strand management and hanger or spreader alignment may require a different support strategy. Some facilities justify modular tooling carts, heated die staging, or lift-assist systems to improve ergonomics and shorten sanitation windows.
Buyers should also think about spare die strategy, product family grouping, and whether automation can store recipe-specific settings. This matters most in plants producing mixed portfolios for grocery chains, club stores, and regional brands.
The demand mix above helps explain why flexibility has become more valuable. Through 2026, plants that can switch formats quickly without sacrificing quality are likely to be more competitive.
Cooling and Stabilization Conveyor Design for Shape Retention
After extrusion, cutting, pre-drying, cooking, or final drying, pasta products often need a controlled cooling and stabilization step before packaging or the next process stage. This area is easy to undervalue, yet it has a direct effect on shape retention, surface condition, and breakage.
Short-cut pasta can chip or deform if transferred while still thermally unstable. Fresh filled pasta can stick, flatten, or lose seal integrity if handling is too aggressive. Long-cut products can become tangled or uneven if post-process support is poor. Cooling and stabilization conveyors should therefore be designed around product geometry, temperature profile, line speed, and accumulation needs.
Important considerations include belt style, sanitation accessibility, ambient versus conditioned air, vibration control, product depth, transfer heights, and whether inspection or metal detection is integrated in the same zone. In humid climates such as the Gulf Coast or Southeast, condensation management and room air control may become especially important for packaging readiness.
Facilities producing multiple product families often benefit from modular conveyor sections and adjustable guides. This is particularly true for co-manufacturers and prepared foods operations pairing pasta production with sauces or meal assembly.
| Cooling/Stabilization Design Choice | Why It Matters | Benefit | Risk if Ignored | Ideal Product Type | Operational Tip |
|---|---|---|---|---|---|
| Open mesh belt | Air exposure | Faster cooling | Small product drop-through | Dry short-cut pasta | Match aperture to shape size |
| Solid sanitary belt | Gentle support | Less marking | Slower cooling | Fresh pasta | Use with washdown design |
| Multi-zone conveyor | Thermal staging | Better stabilization | Higher control complexity | Premium lines | Useful before cartoning |
| Low-drop transfers | Breakage reduction | Higher yield | Product chipping | Fragile shapes | Review every transition point |
| Air knife integration | Surface conditioning | Improved pack readiness | Product movement issues | Drying exit zones | Validate with trials |
| Accumulation buffer | Packaging decoupling | Fewer line stops | Space use | High-speed plants | Strong ROI in automated sites |
When plants experience unexplained downstream breakage, the root cause is often in transfer, cooling, or accumulation design rather than in the extruder itself.
Packaging Line Integration for Fresh and Dry Pasta Products
Packaging line integration is where many capital projects either prove their value or expose their weaknesses. Even a well-designed upstream process can underperform if baggers, weighers, fillers, tray sealers, cartoners, case packers, and palletizing systems are not synchronized with the actual product flow.
Dry pasta packaging typically emphasizes speed, product count or weight accuracy, dust management, seal quality, and gentle handling. Fresh pasta packaging may add modified atmosphere packaging, refrigeration compatibility, and stricter hygienic zoning. Different sales channels also matter. Club store packs, foodservice bulk formats, and retail shelf-ready cartons all impose different equipment and layout needs.
In large U.S. logistics markets such as Atlanta, Dallas, Columbus, and Southern California, packaging choices can influence freight efficiency and retailer compliance. That makes line integration a commercial decision as much as an engineering one. Plants that expect future automation should also leave room for robotic case packing, automated guided vehicles, or warehouse integration.
| Packaging Format | Typical Product | Main Equipment | Critical Design Factor | Common Bottleneck | Best Channel |
|---|---|---|---|---|---|
| Pillow bag | Dry short-cut pasta | VFFS bagger | Weight consistency | Infeed surging | Retail |
| Carton with inner bag | Macaroni and spaghetti | Cartoner plus bagger | Carton timing | Carton jams | Grocery |
| Bulk poly bag | Foodservice pasta | High-capacity filler | Dust control | Seal contamination | Foodservice |
| Tray sealed pack | Fresh pasta | Tray sealer | Gas control | Film handling | Refrigerated retail |
| Pouch with zipper | Premium specialty pasta | Pouch filler | Presentation and seal | Changeover time | Premium retail |
| Case-ready bundle | Long-cut pasta | Bundler/cartoner | Orientation control | Breakage at transfer | Club and wholesale |
The packaging table shows why end-of-line choices must be made early. Upstream design, room layout, and utilities are all affected by the final pack format.
Sanitary Design and CIP Protocols for Pasta Processing Equipment
Sanitary design is essential across all pasta operations, but it becomes especially critical for fresh pasta, filled pasta, protein-enriched formulations, and any line with rapid changeovers. Hygienic design reduces contamination risk, shortens cleaning time, and supports compliance with FDA expectations and customer audit standards such as SQF or BRC.
Effective sanitary design includes cleanable welds, drainable piping, elimination of harborage points, compatible gasket materials, accessible guards, sloped surfaces, and separation of dry and wet cleaning zones where needed. Not every part of a dry pasta line should be wet cleaned, so engineering teams need to define sanitation methods by area rather than applying one approach everywhere.
CIP protocols are most relevant for closed liquid systems, ingredient slurries, water circuits, and some fresh pasta or sauce-integrated applications. A strong CIP design considers time, temperature, chemistry, flow, return conductivity, tank sizing, and validation steps. Plants that add sauces, fillings, or integrated prepared meal components often need broader sanitary planning than pasta-only operations.
By 2026, sustainability and water management are becoming more important in sanitation planning. U.S. manufacturers are looking for ways to reduce water use, recover heat, optimize chemical dosing, and improve cleaning verification with sensors and digital records.
This comparison chart reflects what many U.S. buyers now prioritize when evaluating equipment suppliers and design partners. Sanitary access and service support rank almost as high as pure production capacity.
Our Company
For manufacturers planning new pasta capacity or modernizing an existing facility, the biggest challenge is often not one machine selection. It is connecting process design, building constraints, utilities, automation, installation, and startup into one accountable execution model. That is where Disruptive Process Solutions brings value.
From a technological capability standpoint, DPS supports process, mechanical, electrical, structural, plumbing, and controls engineering for food and beverage facilities across the United States and Canada. Its team develops integrated process solutions that tie together ingredient handling, utility systems, automation architecture, PLC programming, SCADA, CIP design, and production line optimization. That broad engineering base is especially useful when a pasta project includes supporting systems such as compressed air, process water, wastewater planning, steam, glycol, or room environmental controls. Learn more about the company’s approach on the about us page.
From a manufacturing capability standpoint, DPS also designs and supplies proprietary process equipment, including tanks and custom CIP systems, while coordinating complete integration with third-party equipment packages. This is valuable for pasta plants that need more than stand-alone machinery and instead require a balanced system architecture. Whether the line includes bulk ingredient storage, process vessels, sanitary transfer systems, or specialty support skids, the emphasis is on making equipment work as a unified manufacturing platform rather than a patchwork of vendors. More details are available in the company’s equipment portfolio.
From a service capability standpoint, DPS operates with a design-build-manage model that combines front-end planning, project engineering, general contractor coordination, installation oversight, and commissioning support. For pasta manufacturers, that means one partner can help evaluate feasibility, define capital scope, align utilities, manage local trades, and protect schedule execution from concept through startup. This model is particularly useful for brownfield retrofits, phased expansions, and high-speed production environments where downtime is expensive. You can review available engineering and integration services and see real project examples in these case studies.
A practical buying lesson from many food manufacturing projects is simple: the lowest equipment quote rarely creates the best total project outcome. Plants benefit more from disciplined scope definition, utility planning, sanitation strategy, and controls integration than from isolated line-item savings.
FAQ
What products can be made on an industrial pasta line?
Industrial lines can produce macaroni, elbows, penne, rotini, shells, spaghetti, linguine, fettuccine, fresh pasta sheets, filled pasta, and specialty formulations such as whole wheat, high-protein, legume-based, or gluten-free products. The final product family determines the line architecture.
What industries buy pasta production systems in the United States?
Typical buyers include branded food manufacturers, private label producers, co-packers, refrigerated meal manufacturers, institutional food suppliers, foodservice processors, and diversified prepared foods companies adding pasta capabilities.
How do I choose between a fresh pasta line and a dry pasta line?
The choice depends on your sales channel, shelf-life target, distribution model, and sanitation requirements. Dry pasta lines usually require more drying infrastructure and lower moisture packaging strategies. Fresh pasta lines require stronger hygienic zoning, faster cleaning, and refrigerated distribution planning.
What is the most important buying advice for first-time investors?
Start with the business case, not the machine catalog. Define annual volume, SKU count, shift pattern, package formats, utility limits, labor model, and expected expansion path. Then engineer the line backward from those requirements.
How important is local supplier support?
Very important. U.S. buyers should evaluate regional service responsiveness, spare parts access, controls support, and installation capability. A supplier with strong North American support can reduce risk during startup and future maintenance events.
Are there key market trends to watch through 2026?
Yes. The major trends include higher demand for flexible SKU production, more automation to address labor shortages, energy-efficient dryers, digital quality monitoring, better water and chemical management in sanitation, recyclable or reduced-material packaging, and stronger traceability expectations from retailers and regulators.
Can older pasta plants be upgraded instead of replaced?
Often yes. Common upgrades include controls modernization, die handling improvements, dryer optimization, conveyor replacement, packaging automation, and sanitation redesign. A good assessment can identify whether the bottleneck is mechanical, operational, or controls-based.
What should be included in a pasta line case study review?
Look for throughput achieved versus promised, final moisture consistency, startup timeline, changeover time, breakage rate, sanitation performance, packaging OEE, and whether the project met the intended financial target. These factors matter more than nominal machine speed.
Which U.S. regions are attractive for pasta manufacturing?
The Midwest remains strong for ingredient access and central distribution. The Southeast offers growth, labor access in some markets, and port connectivity. Texas supports broad logistics reach. California can serve specialty and premium segments with West Coast distribution advantages, though utility and labor economics must be carefully reviewed.
How many tables and charts should a capital planning team review?
As many as needed to make informed decisions, but they should cover product mix, throughput, utilities, sanitation, labor, and payback. Visual comparisons are useful only when they support a disciplined engineering basis.
In summary, high-quality industrial pasta production in the United States depends on designing the whole process around product behavior, sanitation, packaging, and long-term economics. Vacuum extrusion, controlled drying, engineered semolina handling, flexible die systems, careful cooling, integrated packaging, and validated sanitary design all work together. Companies that align those elements early are better positioned to deliver reliable quality, adapt to new product categories, and compete effectively in the U.S. market through 2026 and beyond.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

