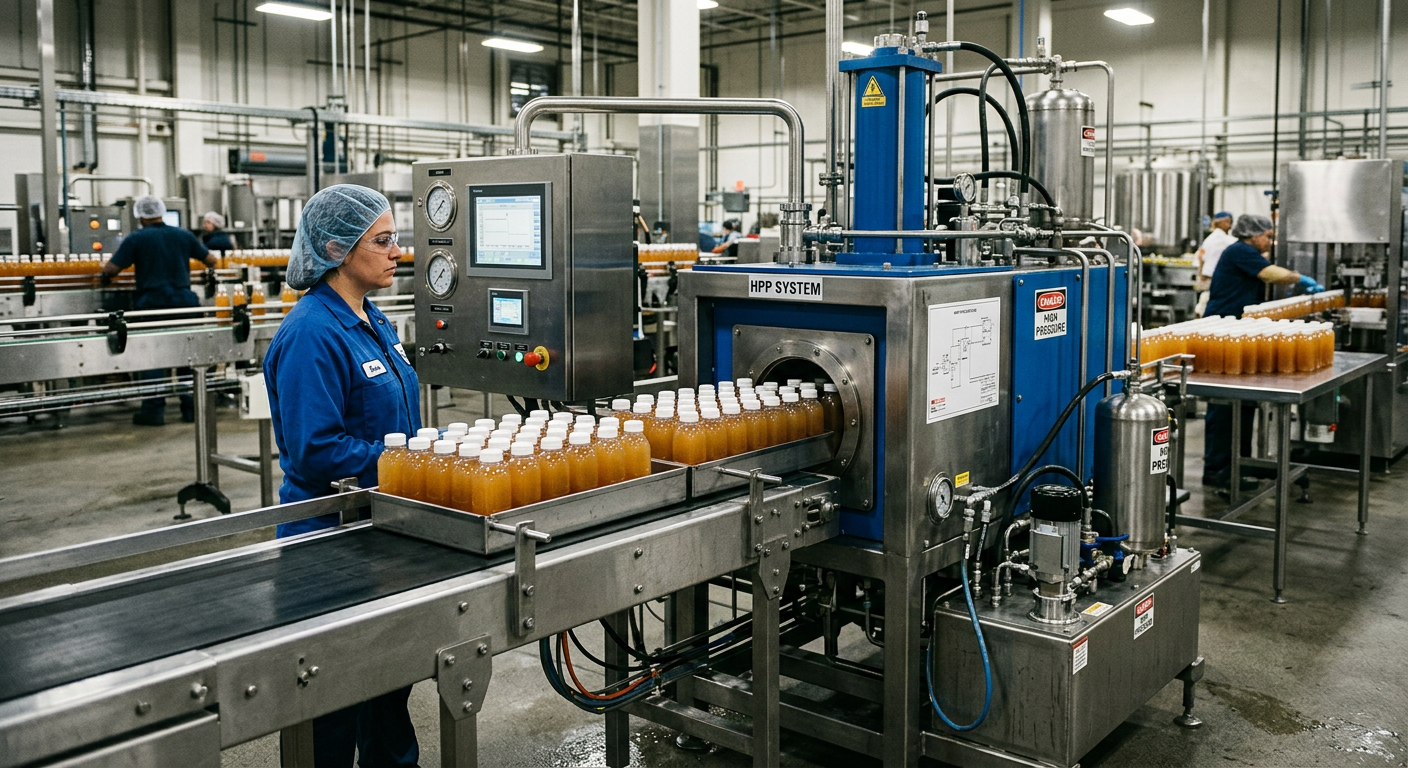
Aseptic Beverage Filling Systems
[trp_language language=”en_US”]
Aseptic Beverage Filling Systems for U.S. Manufacturers
Aseptic filling systems are designed to keep a commercially sterile product separate from environmental contamination from the moment the product leaves the sterilizer until the package is sealed. For beverage producers in the United States, that means sterilizing the product, sterilizing the package, maintaining a controlled filling zone, validating the process, and minimizing downtime that can compromise both throughput and sterility. These systems are widely used for shelf-stable dairy, plant-based beverages, nutraceutical drinks, teas, juices, low-acid formulations, and premium functional products that need long shelf life without refrigerated distribution.
Across the U.S. market, aseptic packaging continues to expand because brands want lower logistics costs, wider retail reach, and better flavor retention than some hot-fill alternatives. Producers shipping through Los Angeles, Long Beach, Savannah, Houston, Chicago, and the Northeast corridor increasingly evaluate aseptic lines not only on fill accuracy and sterility, but also on changeover time, utility efficiency, sustainability, operator ergonomics, and compatibility with upstream UHT and downstream secondary packaging.
For companies planning new capacity or retrofits, the decision is rarely about the filler alone. It also includes product formulation, clean utility design, CIP and SIP strategy, package sterilization technology, air handling, automation, validation, and project execution. That is why many manufacturers work with multidisciplinary partners that combine engineering, installation, equipment integration, and field project management. As a North American food and beverage engineering firm, Disruptive Process Solutions approaches aseptic projects with a design-build-manage model focused on profitability, risk reduction, and startup performance rather than simply placing equipment.
Quick Answer

Aseptic filling systems work by sterilizing the beverage, sterilizing the bottle or closure, and filling in a microbiologically controlled environment so the final sealed package remains commercially sterile. In the United States, the best system depends on product acidity, target output, package format, shelf-life goals, sanitation philosophy, and the amount of downtime a plant can tolerate during SKU changeovers.
In practical terms, a successful aseptic line usually combines five essentials:
- Reliable product sterilization, often via UHT or other validated thermal process
- Consistent package sterilization using hydrogen peroxide vapor, peracetic acid, e-beam, or related methods
- A tightly controlled aseptic chamber with filtered air, zoning, and hygiene barriers
- Automation that supports recipe control, traceability, alarm management, and repeatable CIP/SIP routines
- Documented validation through media fills, sterility testing, environmental monitoring, and maintenance discipline
For U.S. beverage manufacturers, the strongest return on investment often comes from matching the filler configuration to the business model. A high-volume co-packer near Dallas or Atlanta may prioritize integrated combiblock speed and low labor. A specialty nutrition producer in New Jersey or California may place greater value on flexible linear filling with easier package changes and smaller campaign sizes.
| Decision Area | Why It Matters | Typical U.S. Buyer Priority | Common Risk if Ignored |
|---|---|---|---|
| Product Sterility | Protects shelf life and consumer safety | Validated kill step and documented hold times | Microbial spoilage or recall exposure |
| Package Sterility | Prevents recontamination after UHT | Stable bottle and closure decontamination | Inconsistent package integrity |
| Throughput | Supports cost per case and distribution scale | Line speed matched to demand forecast | Underbuilt or oversized capital spend |
| Changeover Time | Affects OEE across multiple SKUs | Fast format and recipe transitions | Lost production windows |
| Validation Burden | Drives regulatory readiness and QA workload | Clear protocols and audit trails | Delayed startup or failed qualification |
| Integration | Links blow molding, filling, packing, and utilities | Single control philosophy and balanced capacity | Bottlenecks between unit operations |
The table above shows why aseptic line selection is both a technical and business decision. Many failed projects are not caused by bad equipment, but by poor alignment between demand profile, sanitation strategy, and facility infrastructure.
This line chart illustrates the steady growth trajectory expected for aseptic beverage equipment demand in the U.S. through 2029, supported by functional drinks, premium dairy alternatives, and wider shelf-stable distribution.
How Aseptic Filling Systems Work: Product and Package Sterilization

The basic principle is simple: sterilize the product, sterilize the packaging material, keep both separate from contamination, then seal immediately. The operational reality is more complex. Aseptic filling requires a complete chain of control from ingredient receiving to pallet discharge.
On the product side, beverages are commonly sterilized using UHT or ultra-clean thermal treatment. Product moves through heat exchangers, holding tubes, and sterile surge systems under carefully controlled time-temperature conditions. The treatment must be sufficient for commercial sterility while preserving flavor, color, nutrients, and viscosity. Once sterilized, the product moves through sterile piping and valves into the filler bowl or product path.
On the package side, bottles, caps, or preforms are decontaminated before entering the fill zone. The filler enclosure maintains positive pressure with HEPA-filtered air or equivalent sterile air management. Surfaces that contact sterile product must remain within validated aseptic boundaries. Any intervention, unplanned stop, or utility upset can trigger re-sterilization procedures depending on system design.
For U.S. plants, aseptic performance also depends on utility quality. Sterile air, clean steam, hot water, chemical dosing, condensate handling, HVAC, and control logic all matter. This is where engineering depth becomes critical. Through its process and project services, DPS supports clients with process engineering, controls integration, utility planning, and execution oversight so the sterile boundary is protected not just on paper, but in daily operations.
| Process Step | Main Function | Critical Control Point | Typical Monitoring Method |
|---|---|---|---|
| Ingredient Preparation | Blend to target formulation | Bioburden entering thermal treatment | Raw material QA and sanitation SOPs |
| UHT or Thermal Sterilization | Achieve commercial sterility | Time and temperature | Continuous recording and alarms |
| Sterile Holding | Buffer product before filling | Pressure and sterile integrity | Pressure trend and valve status |
| Package Decontamination | Sterilize bottle or preform | Chemical dose or energy delivery | Concentration, exposure, residual checks |
| Aseptic Filling | Fill without contamination | Environmental control | Air pressure, filtration, intervention logs |
| Cap Sterilization and Closure | Protect final package | Cap treatment consistency | Residue, torque, seal integrity tests |
| Post-Fill Inspection | Verify package quality | Seal and coding compliance | Vision systems and QA sampling |
This workflow table shows that aseptic filling is not a single machine function. It is a controlled sequence where each step must support the one after it. A weak cap sterilization step, for example, can erase the benefit of a perfectly controlled UHT system.
Types of Aseptic Fillers: Rotary, Linear, and Combiblock Configurations

Rotary, linear, and combiblock aseptic fillers each serve different production strategies. The right fit depends on speed, footprint, flexibility, operator skill, and whether the plant prefers integrated or modular architecture.
Rotary aseptic fillers are typically chosen for higher throughput. Their continuous motion design supports efficient handling of large bottle volumes and consistent filling at scale. They are common in large beverage plants serving national retailers or multi-region distribution from hubs such as the Midwest, Texas, or the Southeast.
Linear aseptic fillers are often favored when flexibility matters more than maximum speed. They can be attractive for specialty dairy beverages, functional formulations, and fast-growing brands with multiple bottle sizes or short production campaigns.
Combiblock systems integrate blow molding, sterilization, filling, and capping into a tighter production unit. For high-output PET applications, this can reduce material handling, contamination opportunities, and floor space. These systems are especially relevant when a producer is building a new greenfield plant and wants a streamlined operating model.
| Comparison Point | Rotary | Linear | Combiblock |
|---|---|---|---|
| Typical Speed Range | High | Low to medium | Medium to very high |
| SKU Flexibility | Moderate | High | Moderate |
| Footprint Efficiency | Good | Moderate | Excellent |
| Capital Intensity | High | Moderate | Very high |
| Best Use Case | Large-scale beverage production | Multi-SKU specialty runs | Integrated PET operations |
| Changeover Complexity | Moderate | Lower | Moderate to high |
| Operator Training Need | High | Moderate | High |
The table above highlights the tradeoffs. A plant in Chicago serving club retail may justify rotary or combiblock speed. A co-manufacturer near Charlotte or Phoenix with frequent changeovers may benefit from a linear setup that protects uptime across many customer formulas.
This comparison chart makes the decision easier to visualize. Rotary and combiblock units lead in throughput, while linear fillers typically score better in flexibility and changeover responsiveness.
Bottle Sterilization Technologies: H2O2 Vapor, Peracetic Acid, and E-Beam
Package sterilization is central to aseptic success. In PET and HDPE operations, three technologies frequently enter the conversation: hydrogen peroxide vapor, peracetic acid, and electron beam. Each offers specific advantages depending on package geometry, line speed, residual tolerance, validation strategy, and sustainability objectives.
Hydrogen peroxide vapor is widely used in aseptic filling because it provides proven microbial reduction and integrates well into many bottle and cap treatment systems. It requires close control of concentration, temperature, contact time, and residual removal.
Peracetic acid can be effective for bottle rinsing or surface decontamination strategies. It is often evaluated where wet sterilization approaches align with container design and sanitation preference. Plants must manage chemical handling, rinse validation, and wastewater considerations.
E-beam uses ionizing energy rather than wet chemistry. It can reduce chemical usage and support attractive sustainability messaging, but the suitability depends on package type, investment level, line architecture, and regulatory execution.
| Criteria | H2O2 Vapor | Peracetic Acid | E-Beam |
|---|---|---|---|
| Sterilization Method | Chemical vapor | Liquid chemical | Electron energy |
| Residual Management | Important | Important | Minimal chemical residual concern |
| Water Demand | Low to moderate | Moderate to high | Low |
| Validation Familiarity | Very established | Established | Growing adoption |
| Package Compatibility | Broad | Broad with process fit limits | Application dependent |
| Sustainability Appeal | Moderate | Moderate | High in low-chemical strategies |
| Capital Cost | Moderate | Moderate | Higher |
This comparison helps buyers frame the choice beyond simple sterilization effectiveness. In many U.S. projects, the deciding factor becomes total operating philosophy: chemical handling, utility load, validation comfort, line speed, and long-term environmental goals.
By 2026, more producers are expected to evaluate low-water and low-chemical sterilization options as sustainability reporting grows and corporate ESG goals tighten. In states such as California and Arizona, water stress can make package sterilization chemistry and rinsing requirements an even more important line-design variable.
Filler Changeover Efficiency: Reducing Downtime Between SKUs
For many American beverage plants, the true profit leak is not sterile failure but changeover loss. Aseptic lines increasingly run many bottle sizes, formulas, closures, and label programs. Every minute spent on format parts, recipe adjustments, rinse verification, and line clearance directly affects OEE.
The best changeover strategy begins in design. Standardized bottle families, rationalized cap platforms, servo-driven adjustments, guided setup, recipe management, and quick-release components all reduce downtime. So does a sensible zoning plan around fillers, depalletizers, cap feeders, buffer systems, and downstream packers.
Controls matter as much as mechanics. Modern HMI guidance, electronic work instructions, interlocked verification steps, and automated data capture shorten the transition between SKUs while reducing operator error. This is an area where DPS brings strong technological capability. Its teams support controls engineering, PLC programming, SCADA integration, and project execution that connect aseptic processing with utilities, blending, packaging, and line-wide performance goals. That matters when a client needs capacity gains without automatically buying a larger line.
| Downtime Reduction Lever | What It Improves | Typical Impact | Buyer Priority |
|---|---|---|---|
| Common bottle family design | Format part reduction | Shorter mechanical changeovers | High |
| Recipe-driven setup | Repeatability | Less operator adjustment time | High |
| Quick-connect product paths | Sanitation turnaround | Faster cleaning and verification | Medium |
| Automated cap handling settings | Closure accuracy | Reduced jam and rework risk | Medium |
| Line clearance workflow | QA release speed | Fewer missed checks | High |
| Operator cross-training | Execution consistency | Lower startup delays | High |
| Balanced downstream equipment | Flow continuity | Reduced post-changeover stops | High |
Plants serving club, grocery, and e-commerce channels from Tennessee, Ohio, or New Jersey often run tighter customer windows than before. Changeover efficiency is therefore a strategic issue, not just a maintenance one. When evaluating suppliers, ask for documented mean changeover times by bottle family and by product class, not just idealized demonstrations.
F0 Solution and CSIP: Advanced Productivity Technologies for Aseptic Lines
Advanced aseptic productivity increasingly depends on smart sterilization control. Two concepts frequently discussed are F0-based process strategies and CSIP, or clean/steam-in-place approaches that help preserve sterile integrity while reducing manual intervention.
F0 solutions use equivalent lethality concepts to quantify thermal impact in sterilization processes. In practical line design, this helps engineers align safety, product quality, and process efficiency. It can support more disciplined control of hold times, thermal treatment windows, and startup validation logic.
CSIP expands the idea of repeatable, automated hygienic recovery. Well-designed CIP and SIP sequences reduce human variability, shorten sanitation cycles, and improve documented compliance. This is especially valuable in high-value beverages where downtime can mean missed retail deliveries or expensive ingredient waste.
The 2026 trend is toward deeper digitalization: automated recipe management, electronic batch records, predictive maintenance alerts, remote troubleshooting, and utility optimization dashboards. Many large U.S. facilities are also incorporating energy tracking to compare steam, compressed air, water, and chemical consumption by SKU. These tools are most effective when they are integrated from the start rather than added as isolated software later.
The area chart shows the projected rise in advanced automation adoption. It reflects the market shift toward data-backed sanitation, sterility assurance, and productivity management across U.S. aseptic operations.
Integration with Aseptic Blow Molding and Preform Sterilization
Integration is often where major gains are won. When blow molding, preform sterilization, filling, capping, and secondary packaging are engineered as one system, contamination risk and handling losses can drop substantially. Integrated PET aseptic systems also help reduce floor space and simplify material flow.
Preform sterilization is especially relevant in compact, high-output lines. Instead of sterilizing full bottles after blow molding, some systems sterilize the preform before it is blown into shape inside a controlled process chain. This can improve process efficiency and support more streamlined equipment layouts.
For greenfield projects, integration should also extend to utilities, syrup rooms, blending, water treatment, compressed air, boilers, cooling systems, and plant controls. DPS brings notable manufacturing and technology capabilities here, including custom equipment supply, tanks, CIP systems, utility integration, structural-mechanical-electrical coordination, and controls architecture. For clients building or expanding co-packing capacity, this cross-functional capability helps prevent the common problem of a fast filler sitting idle because upstream or utility systems were undersized.
At the facility level, U.S. location matters. Plants near high-volume logistics corridors like I-85, I-35, the Inland Empire, Chicagoland, and the Port of Savannah may favor integrated aseptic PET systems that support large outbound flow. Plants serving regional specialty channels may value modularity more than absolute compactness.
Quality Control: Media Fill Testing and Sterility Validation Protocols
Aseptic systems are only as good as their validation program. Media fill testing, environmental monitoring, sterile boundary checks, package integrity verification, and sanitation validation all work together to demonstrate process control.
Media fill testing simulates production using a microbiological growth medium in place of actual product. The goal is to challenge the aseptic process under defined conditions and confirm that contamination does not occur. These trials should represent real operating risks, including line stops, interventions, and startup conditions where appropriate.
Sterility validation extends beyond a single trial. It includes thermal process validation, package decontamination studies, cap sterilization verification, residual testing, filter integrity testing, airflow confirmation, and documented SOP compliance. Strong programs are data-rich and repeatable.
| Validation Activity | Primary Objective | Typical Frequency | Evidence Generated |
|---|---|---|---|
| Media Fill | Challenge aseptic process integrity | Initial qualification and scheduled revalidation | Incubation and contamination results |
| Thermal Process Verification | Confirm lethality delivery | Routine and after major change | Recorded time-temperature data |
| Package Sterilization Study | Confirm surface decontamination | Startup and process change events | Micro reduction and residual records |
| Filter Integrity Testing | Protect sterile air and product path | Defined maintenance intervals | Pass/fail integrity reports |
| Environmental Monitoring | Assess controlled zone hygiene | Routine | Air and surface trend data |
| Closure Integrity Testing | Verify final package seal | Batch or campaign based | Torque, leak, and seal data |
| Operator Qualification | Reduce intervention risk | Initial and recurring | Training and competency records |
This table shows why sterility assurance must be procedural as well as mechanical. An aseptic filler can be well designed, but weak operator qualification or inconsistent environmental monitoring can still create unacceptable risk.
The bar chart shows how demand varies by industry segment. Nutraceutical and dairy-related applications remain particularly active because they combine high product value with strong shelf-life and distribution requirements.
Maintenance Best Practices for Sustained Aseptic Performance
Maintenance on aseptic lines is not just about reliability; it is part of sterility assurance. Worn seals, drifting sensors, damaged gaskets, poor lubrication practice, and delayed valve rebuilds can become contamination pathways or cause unnecessary shutdowns.
Best practices start with a preventive and predictive maintenance plan aligned to actual failure modes. Critical spares should include sterile valves, seals, filters, dosing components, cap handling wear parts, and instrumentation that can affect validation status. Utilities deserve equal attention. In many facilities, compressed air quality, steam quality, condensate behavior, and HVAC performance determine whether the filler can operate in control.
Service capability matters here. DPS supports clients not only with design, but also with installation management, owner representation, capital planning, integration, and project execution across the United States and Canada. Its lean structure can be useful for manufacturers that need fast decisions, practical field coordination, and a partner able to connect engineering intent with startup reality. Companies evaluating long-term aseptic investments should also review available process equipment capabilities and project examples from completed work in food and beverage environments.
| Maintenance Focus | Reason | Common Interval | Failure if Neglected |
|---|---|---|---|
| Seal and gasket inspection | Protect sterile boundary | Routine planned shutdowns | Leaks or contamination ingress |
| Valve rebuild program | Ensure aseptic switching reliability | Cycle or time based | Cross-contamination or downtime |
| Sensor calibration | Preserve validated parameters | Scheduled QA/maintenance cycle | False process confidence |
| HEPA and air handling checks | Maintain fill-zone hygiene | Defined PM intervals | Air quality degradation |
| Chemical dosing verification | Confirm package sterilization consistency | Routine | Under- or over-treatment |
| Capper inspection | Assure package closure integrity | Regular line maintenance | Seal failures and leaks |
| Utility system review | Support stable operations | Monthly to quarterly | Pressure, steam, or air upsets |
The explanation is straightforward: aseptic maintenance should be risk-based. Components tied directly to sterility, validated process control, or closure integrity deserve priority over generic mechanical routines.
Looking toward 2026 and beyond, predictive analytics and remote diagnostics will play a bigger role in aseptic maintenance. Plants that connect maintenance data with SCADA, sanitation records, and production events will be better positioned to reduce emergency downtime and extend component life without over-maintaining expensive parts.
For buyers comparing project partners in the U.S., it is worth asking whether the supplier understands the entire manufacturing environment or only the filler. The strongest outcomes usually come from teams that can connect process, utilities, automation, installation, and plant operations. A useful starting point is to review a provider’s case experience to see whether they have delivered integrated systems rather than isolated equipment placements.
FAQ
What beverages are best suited for aseptic filling systems?
Aseptic filling is commonly used for shelf-stable dairy drinks, plant-based beverages, juices, teas, nutrition products, broths, liquid foods, and premium functional formulations. It is especially attractive when cold-chain avoidance and long shelf life are important.
How is aseptic filling different from hot fill?
Hot fill relies on elevated product temperature in the package to control microorganisms, while aseptic filling sterilizes product and package separately before filling in a controlled sterile environment. Aseptic systems can better preserve sensory quality for many formulations and are often used for more heat-sensitive products.
Which filler type is best for a U.S. co-packer?
It depends on volume and SKU complexity. A high-volume co-packer with stable bottle families may prefer rotary or combiblock systems. A co-packer with many short runs and multiple customer formats may benefit from a linear filler with stronger changeover flexibility.
Is e-beam replacing chemical bottle sterilization?
Not universally. E-beam is gaining attention because it can reduce chemical use and water demand, but hydrogen peroxide vapor and peracetic acid remain well-established and widely used. The right choice depends on package format, cost, validation comfort, and sustainability goals.
What is the most overlooked issue in aseptic line projects?
Integration. Many projects focus on the filler but underestimate utilities, upstream blending, sterile air, controls logic, cap handling, and downstream packaging balance. Poor integration creates hidden bottlenecks and longer startup timelines.
How important is media fill testing?
It is critical. Media fills are one of the most important ways to demonstrate that the aseptic process can operate without contamination under defined challenge conditions. They should be part of a broader validation program, not treated as a one-time event.
How can manufacturers reduce changeover downtime?
Use common packaging platforms, recipe-driven setup, better HMI guidance, quick-release parts, stronger line clearance procedures, and balanced downstream systems. Standardization often delivers the fastest payback.
What should U.S. buyers ask before purchasing an aseptic system?
Ask about validated speed at your product viscosity, package sterilization method, mean changeover time, utility demand, media fill support, spare parts strategy, intervention recovery, cap sterilization method, controls integration, and service coverage in your region.
How do sustainability trends affect aseptic filling in 2026?
Expect more emphasis on low-water sterilization, energy-efficient UHT systems, chemical reduction, lightweight packaging, digital utility tracking, and designs that support ESG reporting. These trends are becoming more important in procurement decisions, especially for national brands and large co-manufacturers.
Who should manage a full aseptic expansion project?
Ideally, a partner that understands process engineering, utilities, automation, installation, and project execution together. For many U.S. manufacturers, that means selecting an engineering-led firm that can design, build, and manage the project with clear accountability from concept to startup.
In summary, aseptic filling systems succeed when sterility, productivity, and integration are treated as one operating strategy. For beverage companies in the United States, the best investment is not always the fastest machine. It is the system that best matches product risk, package format, labor capability, maintenance discipline, validation burden, and long-term growth plans.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

