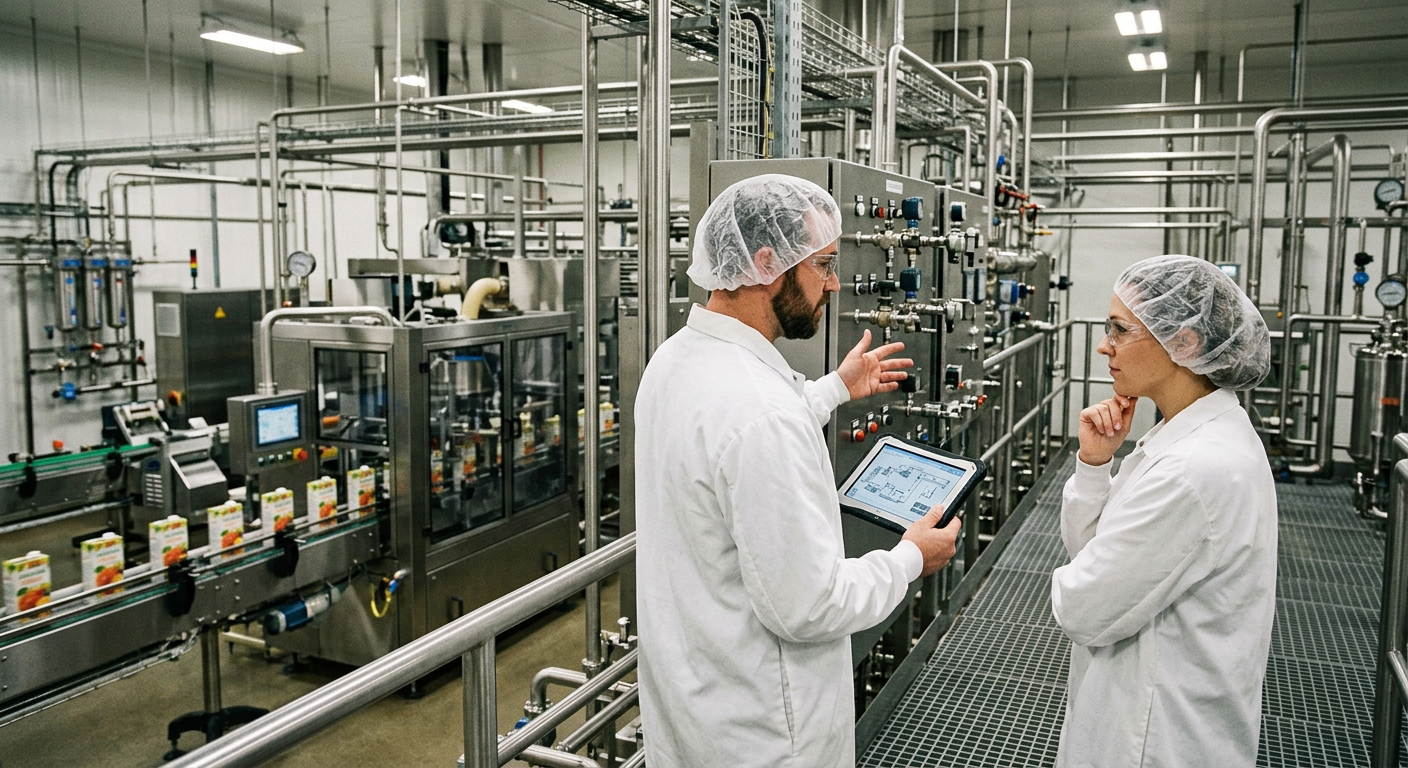
Beverage Syrup Room Design
[trp_language language=”en_US”]
A high-performing syrup room design in the United States should support safe ingredient handling, accurate Brix control, sanitary construction, efficient changeovers, and scalable production. The best designs reduce labor, shorten batch cycles, improve flavor consistency, and align with FDA, SQF, BRC, and sanitary design expectations. For beverage producers, co-packers, breweries, dairy beverage plants, and functional drink manufacturers, the syrup room is not just a utility area; it is a core production asset that directly affects yield, uptime, quality, and profitability.
Across U.S. beverage markets, especially in manufacturing hubs such as North Carolina, Texas, California, Illinois, Georgia, and New Jersey, syrup rooms are being redesigned to support more SKUs, more allergen-sensitive formulations, and tighter traceability. Facilities near major logistics corridors like the Port of Savannah, Port of Los Angeles, Port of Houston, and the Chicago rail network increasingly need syrup systems that can switch between carbonated soft drinks, energy drinks, teas, dairy-based beverages, flavored waters, and concentrates without excessive downtime.
For companies planning a greenfield plant, expansion, or retrofit, smart syrup room planning begins with process flow, not just equipment selection. That means matching dissolving technology to throughput, locating ingredient storage to reduce forklift traffic, engineering filtration and inline measurement into the process, and building a dedicated clean-in-place strategy around actual sanitation risk. This is where a partner with process, utility, controls, and installation experience can make a measurable difference. Companies looking to understand integrated food and beverage engineering support can review the DPS team approach and how project strategy is tied to manufacturing outcomes.
Quick Answer

The most effective beverage syrup room design balances four priorities: product quality, sanitary access, operational efficiency, and long-term expansion. In practice, this means separating dry ingredient receiving from finished syrup transfer, minimizing dead legs in piping, automating Brix verification, using dedicated allergen controls, and designing CIP circuits around vessel geometry and line routing. A small craft beverage plant may rely on flexible batch kettles and mobile totes, while a large co-packer may require continuous sugar dissolving, automated ingredient dosing, recirculating syrup loops, and recipe-driven SCADA integration.
In the United States, the right design also depends on local utility economics, labor availability, state-level permitting, and customer audit expectations. A plant in Southern California may prioritize water recovery and compact footprint. A Texas operation may focus on high-throughput sugar handling and summer cooling loads. A Northeast producer serving retail and foodservice channels may need wider formulation flexibility and more frequent flavor changeovers. Good design adapts to the commercial model, not the other way around.
| Design Priority | Why It Matters | Typical Equipment Impact | Operational Benefit | Risk If Ignored | Best Use Case |
|---|---|---|---|---|---|
| Layout flow | Reduces congestion and cross-traffic | Tank placement, pump routing, access aisles | Faster batching | Delays and safety incidents | All plant sizes |
| Brix accuracy | Controls sweetness and yield | Inline refractometers, metering | Consistent product | Off-spec syrup | Multi-SKU beverage plants |
| Sanitary design | Supports food safety and audits | 3-A compatible vessels, drainable piping | Cleaner system | Micro risk and rework | SQF and BRC facilities |
| Ingredient storage | Protects materials and traceability | Silos, tote stations, flavor rooms | Lower loss | Contamination and waste | Medium to large operations |
| Changeover control | Prevents allergen cross-contact | Segregated lines, validation steps | Safer production | Recall exposure | Functional and dairy beverages |
| Scalability | Supports future expansion | Spare ports, larger headers, automation | Lower future capex | Costly retrofit | Growth-stage co-packers |
The table above shows why syrup room performance is not driven by one machine alone. It comes from a complete system in which ingredients, controls, sanitation, utility support, and operator movement are all designed together.
Syrup Room Layout: Equipment Placement and Workflow Optimization

A well-planned syrup room layout starts with one question: how does material move from receiving to finished syrup delivery with the fewest unnecessary touches? In many U.S. plants, syrup room problems come from retrofits where new tanks were added wherever floor space was available. The result is poor operator visibility, long hose runs, awkward access to valves, overlapping forklift traffic, and sanitation blind spots.
Best practice is to create distinct zones for dry ingredient handling, liquid ingredient staging, sugar dissolving, blend make-up, filtration, finished syrup storage, and CIP support. Dry sugar or sweetener unloading should be physically separated from open liquid transfer points to limit dust and contamination. Flavor additions should occur in a controlled area with easy lot verification and spill containment. Finished syrup transfer to fillers or blend systems should avoid crossing raw ingredient traffic.
For high-throughput beverage operations, tanks are often arranged in a linear or U-shaped pattern to reduce pipe length and simplify automation. Operator walkways should support visual confirmation of sight glasses, load cells, manways, and instruments without forcing personnel to cross forklift paths. Maintenance access is equally important; pumps, strainers, valve clusters, and transmitters should be serviceable without dismantling half the room.
Workflow optimization also includes utility adjacency. Steam, hot water, chilled water, compressed air, electrical drops, and CIP return lines should be designed early. Plants in Charlotte, Dallas, Fresno, Milwaukee, and Atlanta often see better startup performance when syrup room engineering is coordinated with central utility planning rather than handled as a late-stage equipment package.
| Layout Zone | Primary Function | Recommended Placement | Key Sanitary Concern | Preferred Access Type | Expansion Consideration |
|---|---|---|---|---|---|
| Dry goods receiving | Sugar and powders intake | Near dock, isolated from syrup tanks | Dust control | Forklift and bag dump access | Add second dump station |
| Liquid concentrate staging | Sweeteners and juice bases | Near dosing manifold | Temperature stability | Pallet and tote access | Extra tote ports |
| Dissolving area | Sugar melting or sweetener blending | Central to batch flow | Drainability | Operator platform | Parallel vessel allowance |
| Flavor addition zone | Micro ingredients and flavors | Enclosed, low-traffic area | Cross-contact | Controlled personnel entry | Dedicated allergen booth |
| Finished syrup tanks | Hold and feed downstream | Near process discharge | Hold time control | Instrumentation clearance | Future tank pad space |
| CIP interface | Cleaning and sanitation | Adjacent but segregated | Backflow prevention | Utility service access | Additional circuits |
The table highlights a simple principle: physical placement should reflect risk and flow. A syrup room designed around process logic tends to perform better than one designed around convenience alone.
The market trend shown above reflects growing U.S. investment in automation, sanitation, and SKU flexibility. By 2026, many manufacturers are expected to prioritize retrofit-ready layouts with digital quality control and reduced water use.
Sugar Dissolution Systems: Batch Kettles vs Continuous Dissolving

Sugar dissolution is one of the most important design choices in a syrup room. The decision between batch kettles and continuous dissolving depends on throughput, recipe complexity, labor model, and consistency targets. Batch kettles remain popular in craft beverage plants and flexible co-manufacturing environments because they support frequent recipe changes and relatively simple operator oversight. They are especially common where production volumes are moderate and flavor variety is high.
Continuous dissolving systems are better suited for large facilities with stable demand and high sugar throughput. They reduce batch-to-batch variability, improve labor efficiency, and often integrate more effectively with continuous blending and filler supply systems. However, they require more precise upstream control, disciplined maintenance, and stronger automation integration.
Batch systems offer advantages when producers make syrups for soda, tea, lemonade, cocktail mixers, dairy beverages, or functional drinks in short runs. Operators can stage ingredients, verify dissolution visually, and hold product for release. Continuous systems are better for large carbonated soft drink lines, high-speed energy drink operations, or beverage campuses feeding multiple packaging lines from central syrup generation.
| Factor | Batch Kettles | Continuous Dissolving | Capital Cost | Labor Demand | Best Fit |
|---|---|---|---|---|---|
| Recipe flexibility | High | Moderate | Lower to moderate | Higher | Short-run and custom products |
| Throughput | Moderate | High | Moderate to high | Lower per gallon | Large beverage plants |
| Brix consistency | Good with controls | Very high | Depends on automation | Low intervention | Standardized products |
| Changeover speed | Moderate | Slower if line is complex | Varies | Procedure-sensitive | Stable portfolios |
| Footprint | Compact to moderate | Moderate to large | Site-dependent | Efficient flow | New builds |
| Maintenance complexity | Lower | Higher | Lower spare cost | Requires skilled support | Automated operations |
This comparison shows why no single dissolving system is universally best. U.S. buyers should evaluate annual volume, product count, labor cost, and sanitation schedule before selecting technology.
From a process engineering perspective, dissolving design also affects heating method, deaeration, foam management, and crystal control. Steam-jacketed vessels can provide reliable thermal input, but heat-sensitive ingredients may require more controlled profiles. Inline shear, recirculation rate, and transfer velocity all influence dissolution speed and final syrup clarity. A firm with integrated engineering and equipment experience can model these interactions early, which is one reason beverage processors often seek full-scope process and project services rather than buying isolated equipment pieces.
Ingredient Storage and Handling: Dry Goods, Liquid Concentrates, and Flavors
Ingredient storage planning is often underestimated in syrup room projects. Yet poor storage design causes some of the most expensive problems: lot control mistakes, temperature damage, manual handling inefficiency, and allergen exposure. In a modern U.S. syrup room, storage should be matched to ingredient behavior, not just purchasing format.
Dry goods such as granulated sugar, acidulants, stabilizers, and vitamin premixes require dust control, humidity management, and traceable dispensing. Large plants may use silos or supersack systems for sugar, while smaller facilities rely on bag dump stations with integrated dust collection. Liquid concentrates including corn syrup, juice bases, high-intensity sweeteners, and color systems often need tote, drum, or bulk tank storage with controlled temperature and transfer metering. Flavor compounds may require secure rooms, explosion-aware handling depending on solvents, and strict shelf-life rotation.
Facilities serving broad regional markets from hubs like Houston, Philadelphia, and Inland Empire distribution corridors frequently need mixed storage models because inbound ingredients arrive from multiple domestic and imported sources. This is especially true for co-packers producing both customer-owned formulas and house brands.
| Ingredient Type | Common Storage Method | Key Design Requirement | Handling Risk | Control Method | Typical Users |
|---|---|---|---|---|---|
| Granulated sugar | Silo, supersack, bag dump | Dust collection and dry environment | Caking and contamination | Closed conveying | Soft drinks and teas |
| Powder blends | Bag room or micro room | Lot traceability | Mis-weighing | Barcode verification | Functional beverages |
| Corn syrup or sweetener | Bulk tank or totes | Temperature management | Viscosity issues | Heated lines | High-volume plants |
| Juice concentrates | Drums, totes, chilled storage | Cold chain integrity | Flavor degradation | Temperature logging | Juices and RTD drinks |
| Flavors and colors | Controlled flavor room | Secure segregation | Cross-contact | Dedicated utensils | Multi-SKU plants |
| Allergen ingredients | Dedicated area | Physical separation | Recall risk | Changeover validation | Dairy and protein drinks |
The storage table makes clear that ingredient handling is both a quality and compliance issue. The right equipment must be paired with clear SOPs, labeling, and operator training.
Technologically, advanced syrup rooms increasingly integrate mass flow meters, load cell-based batching, barcode lot verification, recipe management, and SCADA-driven prompts. These capabilities reduce manual error and improve accountability. On the manufacturing side, custom tanks, transfer skids, and CIP modules tailored to plant-specific recipes often outperform generic layouts. For companies comparing system configurations, reviewing available process equipment options can help align storage and handling strategy with actual production goals.
Filtration and Clarification Systems for Syrup Preparation
Filtration and clarification are essential for visual quality, downstream equipment protection, and flavor stability. Even when ingredients arrive in good condition, sugar dust, undissolved crystals, foreign particles, and precipitation events can affect finished syrup. In high-speed beverage operations, these issues can lead to filler problems, poor appearance, and customer complaints.
The appropriate filtration train depends on product style. Standard sugar syrups may only require coarse protection followed by fine polishing. Juice-based or botanical products may need multi-stage filtration with larger particulate tolerance. Functional beverages with suspended nutrients require a careful balance between clarification and ingredient retention.
Common components include basket strainers, inline housings, duplex filters, bag filters, and cartridge systems. Clarification may also involve settling logic, controlled recirculation, or in some specialty applications, centrifugation or membrane-based separation. The critical design requirement is that filtration should improve quality without creating excessive pressure drop, line fouling, or sanitation difficulty.
Filter access and replacement logistics matter more than many teams expect. If operators must dismantle hard piping to change cartridges, maintenance time rises and sanitation risk follows. In audited U.S. plants, filter housing design should support easy inspection, complete drainage, and documented integrity checks where needed.
The bar chart indicates where filtration demand is strongest. Juice and dairy-related beverages typically require tighter solids management and more robust clarification strategies than simple flavored water applications.
Brix Control and Inline Refractometer Integration for Syrup Consistency
Brix control is one of the fastest ways to improve syrup consistency, yield, and brand reliability. Manual sampling still has a place for verification, but modern syrup rooms benefit most when inline refractometers are integrated into the control strategy. Real-time Brix measurement reduces overuse of sugar and sweeteners, shortens correction cycles, and improves confidence during startup, recirculation, and transfer.
In practice, inline refractometers work best when paired with stable flow conditions, correct installation angle, sanitary access, and recipe logic in the control system. They should not be treated as standalone devices. Instead, their readings should feed batch sequencing, alarms, trending, and automatic adjustment where appropriate. In U.S. multi-SKU operations, this is especially valuable because product portfolios often include standard-calorie, reduced-sugar, and specialty formulations with narrow tolerance windows.
Calibration planning is equally important. High-acid products, pulp-bearing formulations, and opaque ingredients may influence reading stability. A good design therefore includes sensor location review, bypass options where needed, and routine validation against lab instruments. Plants in regions with seasonal ambient swings, such as Arizona, Florida, or the Midwest, should also consider how temperature variation affects the process and instrument performance.
| Brix Control Method | Accuracy Level | Labor Requirement | Response Speed | Data Traceability | Recommended Use |
|---|---|---|---|---|---|
| Manual lab sampling only | Moderate | High | Slow | Limited | Small batch operations |
| Portable refractometer checks | Moderate to good | Moderate | Medium | Manual records | Flexible pilot systems |
| Inline refractometer with alarms | High | Low | Fast | Strong | Most commercial plants |
| Inline refractometer with closed-loop control | Very high | Low | Very fast | Excellent | High-volume standardized lines |
| Load cell batching plus inline verification | Very high | Low to moderate | Fast | Excellent | Complex recipe plants |
| Hybrid batch and manual confirmation | Good | Moderate | Medium | Good | Mid-size co-packers |
The chart and table together show why Brix automation is now a standard expectation in many U.S. syrup rooms. It supports both quality assurance and margin protection.
The trend shift toward inline automation is expected to accelerate through 2026 as labor constraints, traceability expectations, and formulation complexity continue to rise.
CIP System Design Dedicated to Syrup Room Equipment Sanitation
A dedicated CIP strategy is essential in a syrup room because sugar-rich environments are highly unforgiving when cleaning discipline is weak. Sticky residues, flavor carryover, microbial niches, and line fouling can quickly compromise production. Too often, facilities attempt to share a generic plant CIP loop across syrup generation, fillers, and unrelated process zones. While shared systems can work in some designs, syrup rooms often benefit from dedicated circuits or at least dedicated recipes, return logic, and validation steps.
Effective syrup room CIP design begins with circuit definition. Dissolvers, blend tanks, transfer lines, flavor addition manifolds, and finished syrup hold tanks may all have different cleaning needs. Spray device coverage, return velocity, conductivity targets, temperature, and contact time should be engineered around actual residue characteristics. Instrumentation for flow, conductivity, temperature, and return verification allows objective cleaning confirmation instead of guesswork.
Drainability is critical. Hygienic slope, valve orientation, minimal dead legs, and proper pump selection all determine whether a CIP loop truly cleans. If a tank outlet traps syrup or a branch line cannot fully drain, sanitation costs rise and product risk remains. Plants seeking reliable startup and audit performance usually benefit when CIP design is integrated early with tank fabrication, utility sizing, and controls.
Service capability matters here as much as engineering. A project partner that can design, install, automate, and commission the syrup room and its cleaning systems in a coordinated model typically shortens startup risk. That design-build-manage style is increasingly valued by U.S. manufacturers who want accountability from concept through execution, particularly in fast-moving beverage expansions and co-packing launches.
Allergen Management and Cross-Contact Prevention During Changeovers
Not every syrup room handles allergens, but for plants producing dairy-based beverages, protein drinks, botanical blends, nut-containing formulations, or specialty functional products, allergen control must be embedded into design and operations. The most effective approach is prevention by layout and process, not just end-of-run cleaning.
Physical segregation is the first layer. Allergen ingredients should have designated storage, weighing, utensils, and where justified, separate transfer paths. If dedicated piping is not economically feasible, validated cleaning procedures and production sequencing become essential. Many facilities run non-allergen products first, followed by increasingly complex or allergen-containing recipes, ending with a full validated changeover wash.
Documentation must support the physical system. Batch records, lot traceability, line clearance checks, label control, and sanitation verification all contribute to cross-contact prevention. For co-packers in particular, allergen transitions are a commercial issue as much as a compliance issue because customer confidence depends on reliable execution.
| Changeover Control | Purpose | Design Requirement | Verification Method | Typical Cost Impact | Recommended For |
|---|---|---|---|---|---|
| Production sequencing | Reduce cleaning frequency | Scheduling discipline | Batch review | Low | Most facilities |
| Dedicated utensils | Prevent ingredient mixing | Color coding and storage | Pre-op inspection | Low | Flavor and micro rooms |
| Segregated storage | Control allergen risk | Physical barriers | Warehouse audit | Moderate | Dairy and protein plants |
| Dedicated lines or hoses | Lower carryover | Separate transfer assets | Line identification | Moderate to high | High-risk products |
| Validated CIP cycle | Confirm cleaning effectiveness | Defined recipe and testing | Swab and rinse tests | Moderate | Shared systems |
| Line clearance SOP | Prevent wrong-product startup | Operator signoff steps | QA release | Low | All audited plants |
The table illustrates that allergen management is a layered system. Low-cost controls such as sequencing and utensil separation are valuable, but they work best when supported by equipment design and verified sanitation.
3-A Sanitary Standards and EHEDG Guidelines for Syrup Room Construction
Although syrup rooms are not identical to dairy systems, 3-A sanitary principles and EHEDG hygienic design guidance remain highly useful references for construction and equipment selection. In the U.S. market, owners, auditors, and engineering teams often apply these frameworks to improve cleanability, eliminate contamination harborage points, and support consistent validation.
For syrup room construction, key sanitary design elements include drainable piping, hygienic welds, suitable surface finishes, cleanable instrument connections, proper gasket selection, sloped tops where needed, and avoidance of difficult-to-clean hollow structures in high-risk zones. Floor design also matters. Proper slope to drains, chemical-resistant surfaces, and separation between wet and dry areas help reduce slips, standing water, and sanitation burden.
Equipment support frames, access platforms, and cable routing should be designed so they do not create hidden debris traps. Venting and air handling may also be important where powders, aromas, or moisture loads are significant. In high-care applications, room pressure relationships and enclosed ingredient handling can further reduce environmental risk.
By 2026, U.S. syrup room trends are likely to include stronger digital sanitation verification, more water-optimized CIP strategies, increased use of hygienic automation skids, and broader consideration of sustainability metrics during capital planning. Policy and customer pressure around water, chemical consumption, and energy intensity will likely influence future room design as strongly as throughput does today.
The comparison chart shows why many U.S. beverage manufacturers prefer integrated project delivery over piecemeal procurement when building or retrofitting syrup rooms. Stronger coordination usually means fewer field conflicts, cleaner startups, and better long-term scalability.
From a practical standpoint, manufacturers evaluating suppliers should look beyond brochure claims. Ask how the engineering team handles process design, utility coordination, automation, equipment fabrication, field installation, and commissioning. Ask whether custom tanks, CIP skids, and syrup modules can be fabricated to match plant realities. Ask for evidence of beverage, dairy beverage, and co-packing experience. For a look at executed work across industries, manufacturers can explore project case examples to understand how planning decisions translate into plant performance.
In technological capability, a strong partner should understand process engineering, controls integration, SCADA, PLC programming, inline Brix monitoring, filtration, utility design, and sanitary process routing. In manufacturing capability, it should be able to supply or coordinate custom tanks, CIP systems, and related process equipment built for hygienic operation and site-specific needs. In service capability, it should support feasibility, owner representation, capital planning, project management, installation oversight, startup, and cross-functional execution across the United States and Canada. That blend is especially relevant for clients who need business-minded engineering, not just a mechanical layout.
FAQ
What is the ideal syrup room size for a U.S. beverage plant?
There is no universal size. The right footprint depends on throughput, SKU count, ingredient variety, batch size, and whether future expansion is planned. A plant with three stable products may need less room than a co-packer with twenty rotating formulas and allergen controls.
Should a syrup room use batch or continuous production?
Batch is generally better for flexibility and lower initial complexity. Continuous dissolving is typically better for very high throughput and standardized products. Many growing plants start with batch systems and add continuous capability later.
Is inline Brix control worth the investment?
Yes, in most commercial operations. It improves consistency, reduces giveaway, shortens correction time, and supports digital records. The return is strongest in multi-SKU or high-volume plants.
How important is a dedicated CIP system?
Very important when syrup residue, flavor carryover, or allergen transitions are significant. A dedicated or carefully segmented CIP strategy reduces sanitation risk and improves production scheduling.
What sanitary standards should be considered?
U.S. plants commonly apply hygienic design principles informed by 3-A expectations, EHEDG guidance, FDA food safety requirements, and customer audit schemes such as SQF and BRC. Exact requirements depend on product category and market expectations.
How do beverage co-packers reduce changeover losses?
They use recipe sequencing, smart layout, dedicated ingredient controls, automated batching, validated cleaning, and operator-friendly access. Equipment placement and controls integration are often the biggest drivers of faster changeovers.
What future trends will shape syrup rooms in 2026?
Expect wider use of inline sensors, digital sanitation verification, sustainability-focused CIP design, stronger utility integration, lower-water cleaning strategies, more modular skid systems, and tighter data traceability tied to quality and customer audits.
What types of companies benefit most from professional syrup room design?
Soft drink producers, RTD beverage plants, juice processors, energy drink manufacturers, dairy beverage facilities, craft beverage operations, and large co-packers all benefit. The value is greatest when consistency, uptime, and scalability affect margin.
In the United States, syrup room design has become a strategic manufacturing decision rather than a narrow equipment purchase. The best systems connect layout, dissolving, storage, filtration, Brix control, sanitation, and compliance into one coherent production environment. When that happens, manufacturers gain more than a cleaner room; they gain faster startups, stronger audit readiness, better operator performance, lower waste, and a foundation for profitable growth.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

