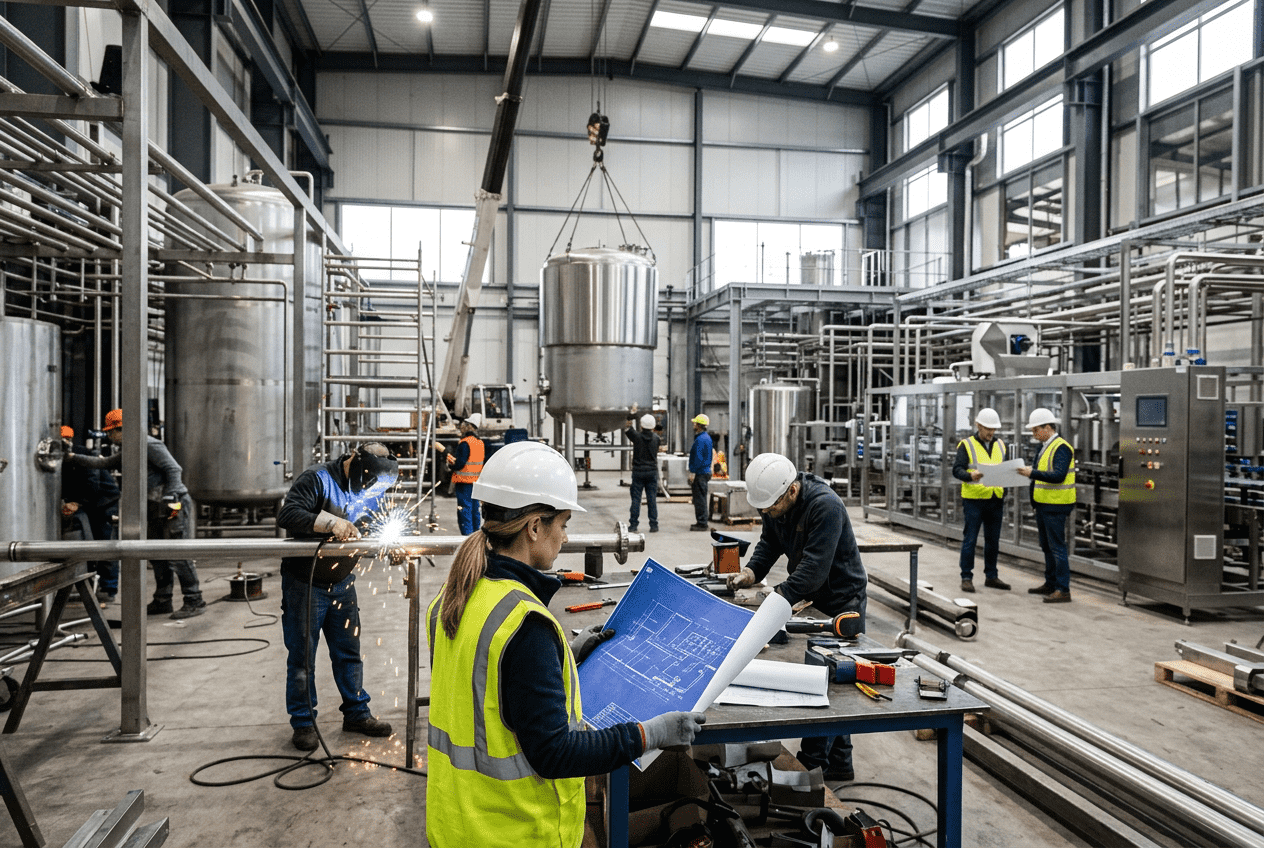
Canned Cocktail Production Line Design
[trp_language language=”en_US”]
Canned Cocktail Production Line Design in the United States
Designing a canned cocktail production line in the United States requires more than selecting a filler and seamer. A profitable ready-to-drink beverage system must align formulation, alcohol compliance, carbonation performance, microbiological stability, package labeling, utility sizing, flavor changeovers, and long-term operating cost. Whether the product is a vodka soda, tequila cocktail, whiskey highball, wine-based spritz, or malt-based RTD, the production line must deliver legal compliance, sensory consistency, and dependable throughput from blend tank to finished pallet.
Across the United States, growth in canned cocktails is strongest in retail corridors connected to major distribution and logistics hubs such as Los Angeles, Chicago, Dallas-Fort Worth, Atlanta, New York/New Jersey, Miami, and Seattle. Manufacturers near ports like Long Beach, Savannah, Houston, and Newark often gain freight advantages for imported spirits, sweeteners, cans, and flavor systems. At the same time, domestic co-packers and brand owners face increasing pressure to launch more SKUs with tighter margins and faster commercialization timelines.
Quick Answer

A United States canned cocktail production line typically includes water treatment, ingredient staging, batch blending, proofing and alcohol adjustment, in-line Brix and density verification, deaeration where needed, carbonation or nitrogen dosing, can rinsing, counter-pressure or equivalent low-oxygen filling, seaming, coding, package inspection, secondary packaging, and palletizing. The right line design depends on alcohol base, target ABV, carbonation level, shelf-life strategy, can size, flavor count, and whether the product will be tunnel pasteurized, flash treated, or cold filled with an approved preservative system.
For most projects, the best design approach is to begin with regulatory and product decisions first, then engineer the line backward from desired shelf stability and throughput. In practice, that means confirming TTB formula needs, ABV tolerance targets, microbiological risk profile, can format, anticipated distribution temperature, and changeover frequency before equipment is specified.
| Decision Area | Why It Matters | Typical Options | Risk if Missed | Who Owns It | Best Timing |
|---|---|---|---|---|---|
| Alcohol base | Drives taxation, formula, and labeling | Spirits, wine, malt, sugar brew | Regulatory redesign | Brand and compliance team | Concept stage |
| ABV target | Controls blend and legal tolerance | 4.5% to 12%+ | Out-of-spec product | Process and quality | Formula stage |
| Carbonation method | Affects mouthfeel and fill performance | Stone, in-line, nitrogen dosing | Foaming and poor pickup | Engineering and operations | Equipment design |
| Shelf-life strategy | Determines thermal or preservative approach | Tunnel pasteurization, cold fill | Spoilage and recalls | QA and process engineering | Before procurement |
| Package format | Changes filler, seamer, and packout | 202 slim, sleek, standard | Low OEE | Commercial and engineering | SKU planning |
| Flavor count | Impacts CIP and changeovers | Single SKU to multi-flavor | High downtime | Operations leadership | Line layout stage |
The table above shows why successful projects do not start with a filler quote alone. They start with a complete process and commercialization roadmap. Companies needing integrated engineering, equipment planning, and execution support often benefit from a partner that can combine processing, utilities, controls, and installation under one structure, such as the approach described in our company overview.
Canned Cocktail Production: Blending, Carbonation, and Canning Process Flow

The standard process flow begins with treated water, alcohol base, sweeteners, acidulants, flavors, colors, and functional ingredients entering a controlled batching system. Water quality is foundational. Reverse osmosis, carbon filtration, softening, and disinfection may be required depending on source water and flavor sensitivity. Spirits-based RTDs often expose mineral instability quickly, especially in clear beverages where haze is unacceptable.
Blending generally takes place in jacketed mix tanks or bright-style vessels sized to campaign length and line speed. A common sequence includes water charge, sweetener addition, acid and flavor dosing, alcohol addition, final proofing, mixing, in-process analytical checks, and hold for packaging. For products with juice, dairy, botanicals, or emulsified ingredients, shear requirements and ingredient hydration times should be validated through pilot work.
Carbonation is usually applied after blend standardization and before filling. A low temperature, low dissolved oxygen environment supports stable CO2 pickup and reduces foaming in the filler bowl. If a nitro-style mouthfeel is desired, the line may include nitrogen infusion, liquid nitrogen dosing, or a hybrid gas management strategy depending on the product profile and package presentation.
After carbonation, cans are depalletized, rinsed or ionized, filled, seamed, coded, inspected, packed, and palletized. Critical control points include dissolved oxygen, fill temperature, net contents, seam integrity, and package stability after thermal exposure if pasteurization is used.
| Step | Main Equipment | Primary Objective | Key Measurement | Common Issue | Design Note |
|---|---|---|---|---|---|
| Water treatment | RO, carbon, UV, storage | Consistent base water | Conductivity, hardness | Flavor drift | Match treatment to source water |
| Ingredient batching | Mix tank, load cells, dosing skids | Accurate formula build | Weight, Brix, pH | Incorrect sweetness | Automate dosing for repeatability |
| Alcohol proofing | Blend tank, density meter | Meet legal ABV | ABV, temperature | Out-of-spec proof | Use temperature compensation |
| Carbonation | Carb stone or in-line carbonator | Target gas volume | CO2 volumes | Foaming | Keep product cold |
| Filling and seaming | Can filler and seamer | Package integrity | Fill height, seam dimensions | Leaks, low fills | Control oxygen ingress |
| Stability treatment | Tunnel pasteurizer or cold chain setup | Shelf-life security | PU, preservative level | Micro growth | Validate by product type |
This flow is not one-size-fits-all. A low-acid cream cocktail needs a different risk strategy than a clear vodka soda. A co-packer running six flavors in one shift needs different tank logic than a single-SKU high-volume line. That is why integrated process design, utilities, automation, and commissioning matter as much as the canning block itself. Brands evaluating full system execution can review broader engineering and project services relevant to beverage facilities.
TTB Compliance and Formula Approval for Canned Cocktail Manufacturing

In the United States, canned cocktails sit at the intersection of manufacturing science and alcohol regulation. The Alcohol and Tobacco Tax and Trade Bureau, or TTB, governs many core requirements tied to formulation, class/type, labeling, tax category, and production records. The exact compliance path depends on whether the product is spirits-based, wine-based, or malt-based. It also depends on whether flavors, colors, juices, caffeine, sweeteners, or other ingredients trigger formula review.
For many projects, formula approval should be addressed before equipment layout is finalized. If a product must be reformulated because of class/type or ingredient restrictions, that change can affect tank residence time, carbonation behavior, thermal sensitivity, or packaging claims. It is much less expensive to resolve this in development than after purchase orders are issued.
Key compliance tasks often include confirming permit structure, determining formula filing needs, defining records for alcohol movement and usage, validating net contents and alcohol statements, and preparing label submissions where applicable. State-level registration, deposit laws, and distributor requirements add another layer beyond federal review, especially when launching in California, Texas, Florida, New York, Illinois, or multi-state retail programs.
| Compliance Topic | What to Review | Why It Affects Production | Typical Trigger | Operational Impact | Best Practice |
|---|---|---|---|---|---|
| Formula approval | Ingredients and process classification | May affect legal marketability | Flavors, colors, juices | Launch delay | Review before scale-up |
| COLA/label review | Mandatory label details | Artwork drives packaging order timing | New SKU launch | Scrapped labels or cans | Approve before print runs |
| Alcohol source records | Receiving and usage logs | Supports traceability | Spirits transfer | Audit risk | Link ERP and batch records |
| Tax classification | Product base and rate | Changes margin model | Base change from malt to spirits | Pricing issues | Model taxes early |
| State registrations | Sales territory rules | Affects launch sequence | Multi-state rollout | Inventory hold | Build a state matrix |
| Advertising claims | Nutrition, health, and ingredient claims | Must match formula reality | Low sugar or natural claims | Rework risk | Align legal and QA review |
The table makes clear that compliance is not a side task. It directly influences manufacturing, cost, and timing. Engineering teams that understand beverage processing and regulated production environments can help align process design with compliance milestones, preventing expensive late-stage changes.
Alcohol Content Control and ABV Consistency in Canned Cocktail Production
ABV consistency is one of the most important quality and legal metrics in canned cocktail manufacturing. Consumers expect every can to taste the same, distributors expect brand reliability, and regulators expect the declared alcohol content to be truthful and supportable. Small mistakes in proofing can become large deviations at scale, especially when high-proof alcohol is blended into large water phases or when density shifts occur due to sugar and temperature.
Strong ABV control starts with mass balance discipline. Alcohol storage, metering, transfer lines, and batch sequencing should be designed to reduce operator variability. Load cells, coriolis meters, density meters, and recipe-driven batch control all improve repeatability. Temperature correction matters because density changes can mislead proof determination if the measurement system is not properly compensated.
In a high-throughput line, the best practice is to verify ABV at multiple points: during batching, after final blend adjustment, and during packaged product release. Multi-flavor lines should also account for residual dilution or carryover during changeover, particularly when moving between low-ABV and high-ABV products.
| Control Area | Preferred Method | Reason | Failure Mode | Business Impact | Recommended Action |
|---|---|---|---|---|---|
| Alcohol receiving | Documented proof verification | Confirms supplier accuracy | Incorrect incoming strength | Batch deviation | Test each lot |
| Batch dosing | Mass-based dosing with interlocks | Higher precision | Overdose or underdose | Rework or dump | Automate critical additions |
| Temperature control | Compensated density reading | Reliable ABV calculation | Misread proof | Release delay | Calibrate routinely |
| Mixing uniformity | Validated agitation profile | Ensures homogeneity | Stratification | Variable can ABV | Establish mixing SOP |
| In-process QA | Hold and release checks | Catches deviations early | Line runs bad product | Large inventory exposure | Set batch checkpoints |
| Packaged verification | Retain sample program | Supports traceability | Post-fill drift unnoticed | Complaint risk | Trend by lot and SKU |
Facilities with advanced automation can link recipe management, lot tracking, and analytical verification into SCADA or batch control systems. This reduces hand-entry error and gives operations better visibility into yield, loss points, and exception handling. Companies seeking integrated processing and controls capabilities often evaluate custom equipment and systems that fit their exact throughput and product mix rather than forcing a generic line into a specialized beverage application.
Carbonation and Nitrogen Infusion Systems for RTD Cocktails
Carbonation in RTD cocktails is not just a sensory choice; it is a process engineering discipline. Carbon dioxide pickup depends on product temperature, pressure, contact time, alcohol content, sugar content, and turbulence. A simple vodka soda may target a crisp, sparkling profile, while a canned espresso martini or creamy cocktail may rely more on nitrogen structure or a low-gas smooth texture.
Common options include carbonating stones in bright or holding tanks, in-line carbonators integrated with heat exchangers, and liquid nitrogen dosing systems used for widget-free nitro presentation or package stiffening where appropriate. Each method has implications for capital cost, product flexibility, and line control complexity.
For low-foaming performance, product should usually be filled cold, with consistent pressure balance through the filler. Long transfer runs, poor insulation, and unstable tank pressure are frequent root causes of carbonation inconsistency. Nitrogen systems require equal attention to gas purity, dosing repeatability, and worker safety protocols.
The chart reflects how different RTD categories can drive different gas handling needs. High-volume sparkling categories typically justify tighter control over chilling, pressure regulation, and filler design. Nitro categories may need lower line speed initially until product behavior is fully characterized at commercial scale.
Can Filling and Seaming Equipment for Alcoholic Beverages
The filler and seamer are the commercial heart of a canned cocktail line. For alcoholic beverages, the system must protect flavor, manage dissolved gas, minimize oxygen pickup, and maintain seam integrity over shipping, warehousing, and retail handling. Equipment selection depends on speed target, package sizes, headspace strategy, product viscosity, and whether products are still, sparkling, or nitro-dosed.
Entry-level producers may start with compact monoblocks, while regional brands and co-packers usually move into higher-speed rotary systems with automated seam teardown checks, reject systems, and integrated rinse-fill-seam architecture. At larger scale, depalletizing, warmers or tunnel pasteurizers, case packing, and palletizing become essential parts of the performance equation.
Seam quality is non-negotiable. Double seam inspection, can-end compatibility, and routine teardown procedures should be built into the quality program from day one. Many product complaints attributed to flavor or age are actually package integrity failures caused by poor seams or hidden oxygen exposure.
| Equipment Area | Main Choice | Best For | Key Advantage | Main Limitation | Design Tip |
|---|---|---|---|---|---|
| Can depalletizer | Low-level or high-level | Continuous production | Reduces manual labor | Floor space | Match to can supply format |
| Rinser | Twist or air/ionized | Dust-sensitive products | Cleaner package entry | Water management | Validate sanitation method |
| Filler | Counter-pressure rotary | Carbonated RTDs | Better foam control | Higher capital cost | Size to future demand |
| Seamer | Integrated or standalone | All can types | Package integrity | Maintenance sensitivity | Track seam trends digitally |
| Inspection | Fill level, leak, code check | Higher QA environments | Reduces escape risk | Additional complexity | Integrate rejects cleanly |
| End-of-line | Case packer and palletizer | Regional and national supply | Labor efficiency | Capital and layout | Allow SKU flexibility |
For manufacturers expanding beyond pilot scale, the equipment must be considered together with utilities: compressed air, glycol or chilled water, steam if thermal processing is used, CIP, drains, floor loading, and electrical service. This is where beverage-focused engineering depth matters. DPS, for example, brings process, mechanical, electrical, controls, and utility integration into one project model, which helps avoid the frequent industry problem of buying equipment that the building cannot properly support.
Tunnel Pasteurization vs Cold Fill with Preservatives for Cocktail Stability
Stability strategy is one of the biggest design decisions in canned cocktail production. In broad terms, producers often compare tunnel pasteurization with cold fill using an acidified and preservative-supported formula. The correct answer depends on product composition, target shelf life, distribution conditions, and brand positioning.
Tunnel pasteurization offers a robust packaged-product lethality step and is particularly valuable when microbial risk is meaningful and refrigerated distribution is not assured. It is often favored for products containing juice, botanicals, or other ingredients that raise spoilage concerns. However, thermal load can affect flavor freshness, color, carbonation retention, and package water usage.
Cold fill with preservatives can preserve brighter top notes and reduce thermal stress, but only when the formulation, pH, hygienic design, sanitation, and validation package are strong enough. A weak sanitation program cannot be fixed by preservatives alone. Likewise, an aggressive thermal process cannot rescue poor package integrity.
| Factor | Tunnel Pasteurization | Cold Fill with Preservatives | Best Fit | Main Risk | Strategic Note |
|---|---|---|---|---|---|
| Microbial control | Strong packaged kill step | Depends on formula and sanitation | Higher-risk products | Underprocessing or contamination | Validate for each SKU |
| Flavor retention | May lose some freshness | Usually brighter flavor | Aroma-driven RTDs | Preservative taste perception | Test side by side |
| Capital cost | Higher equipment and utilities | Lower thermal capital | Smaller startups | Hidden QA burden | Compare full lifecycle cost |
| Water and energy | Higher usage | Lower direct thermal use | Sustainability goals | Inadequate environmental design | Recover utilities where possible |
| Distribution resilience | Better for ambient networks | Needs stronger controls | Wide geographic shipping | Warm chain abuse | Consider southern climate exposure |
| Operational complexity | Thermal process management | Formula discipline and hygiene focus | Depends on team skill set | Mismatch with workforce capability | Train for chosen pathway |
In the United States, products may travel through hot warehouses in Phoenix, humid docks in Savannah, or long truck routes through Texas and the Midwest. Stability decisions must reflect those realities, not just lab conditions. That is why pilot validation, shelf-life studies, and utility modeling should be part of the line design process.
Labeling Requirements: Alcohol Statements, Surgeon General Warnings, and Nutrition Facts
Labeling on canned cocktails must be handled with the same rigor as formulation. Mandatory content can include brand name, class or type where applicable, alcohol statement, net contents, producer or bottler information, government warning statement, and other regulated elements. Nutrition disclosure rules and facts panels may vary depending on product category and current regulatory framework, so every project should be reviewed for its exact labeling pathway.
Artwork errors are expensive because printed cans, shrink sleeves, cartons, trays, and digital assets are often ordered before the first full commercial run. A mislabeled alcohol statement or omitted warning language can delay launch, force destructive rework, or create compliance exposure in multiple states.
Brands should also think beyond mandatory text. UPC placement, date coding area, scuff resistance, and readability on curved can surfaces matter in real retail conditions. Products sold through grocery, convenience, and stadium channels need packaging that scans cleanly and communicates quickly.
Good practice is to run a cross-functional label review that includes legal, regulatory, quality, operations, and commercial stakeholders before final artwork release. This is especially important for lineups that include zero-sugar claims, low-calorie positioning, natural flavor language, or functional ingredients.
Line Design Considerations for Multi-Flavor Canned Cocktail Production
Multi-flavor production is where line design either creates long-term profit or long-term frustration. Brands now expect variety packs, seasonal launches, and fast-moving innovation pipelines. In the United States retail market, especially in chains that serve metropolitan areas like Chicago, Austin, Denver, and Charlotte, multi-flavor variety packs can materially increase shelf presence. But they also create operational complexity.
The first challenge is changeover time. Shared syrup, flavor, and alcohol paths must be designed to minimize trapped volume and simplify CIP. Pigging systems, dedicated flavor manifolds, smart valve matrices, and recipe-driven automation can dramatically reduce product loss and downtime. The second challenge is scheduling. A line that runs only one flavor efficiently may perform poorly when asked to switch six times per shift.
Layout matters as well. Adequate space for ingredient staging, can decoration change parts, quality checks, and repack work is essential. If variety packs are planned, secondary packaging equipment should be selected for pack pattern flexibility, not just single-SKU case output.
From a manufacturing capabilities standpoint, DPS supports facilities that need full-system integration, including tanks, CIP systems, blending platforms, utilities, and controls. The company also manufactures selected process equipment, which can be useful when standard catalog hardware does not match project goals. For brand owners and co-packers, that integrated capability can help bridge the gap between process design and real production behavior on the floor.
| Priority | Why It Matters | Typical Solution | Cost Impact | Operational Benefit | 2026 Trend |
|---|---|---|---|---|---|
| Fast changeovers | More SKU turns per day | Automated valve matrix | Moderate upfront | Higher uptime | AI-assisted scheduling |
| Flavor segregation | Prevents carryover | Dedicated dosing loops | Higher piping cost | Better flavor purity | Smart inline analyzers |
| CIP optimization | Reduces water and labor | Recipe-based CIP skids | Moderate | Reliable sanitation | Water recovery systems |
| Flexible packout | Supports variety packs | Modular case packing | Moderate to high | Retail adaptability | Robotic mixed-pack assembly |
| Digital traceability | Tracks lots by flavor | SCADA and MES links | Software investment | Faster investigations | Cloud quality analytics |
| Sustainability design | Lowers utility cost | Heat recovery and low-loss systems | Project dependent | Better lifecycle ROI | Carbon reporting readiness |
By 2026, three trends are likely to shape line design decisions even more strongly: smarter automation for changeovers, increased state and retailer scrutiny around packaging and disclosure, and stronger sustainability requirements tied to water, energy, and waste reduction. Facilities that invest early in utility efficiency, traceability, and modular expansion will generally be better positioned for both compliance and margin protection.
The comparison above illustrates a common issue in beverage projects: equipment-only buying can look cheaper initially, but often performs worse in flexibility, compliance readiness, and utility fit. That gap becomes costly after startup.
FAQ
What is the best can format for canned cocktails in the United States?
There is no universal best format. Slim and sleek cans often suit premium, lower-volume cocktails, while standard cans may offer broader equipment compatibility and lower supply risk. The right answer depends on brand positioning, line capability, and distributor preference.
Do all canned cocktails need TTB formula approval?
Not all products follow the same path. Approval needs depend on product base, ingredients, and regulatory classification. This should be reviewed before commercialization and before ordering packaging.
How do manufacturers keep ABV consistent from batch to batch?
They use controlled ingredient dosing, verified incoming alcohol strength, temperature-compensated analytics, validated mixing procedures, and documented QA release checks on both bulk and packaged product.
Is tunnel pasteurization always better than cold fill?
No. Tunnel pasteurization can provide stronger packaged-product stability for some formulas, but it may affect flavor and utilities. Cold fill can work well with the right formula, sanitation, and validation package.
What throughput should a startup plan for?
That depends on demand, SKU count, and co-packing versus owned production strategy. Many early-stage brands overbuy speed and underinvest in blending, utilities, and QA infrastructure. A balanced system is more important than a headline cans-per-minute number.
How important is can seam inspection?
It is critical. Seam defects can lead to leakage, oxygen ingress, reduced shelf life, and customer complaints. Seam monitoring should be routine, documented, and tied to preventive maintenance.
What should be included in a full project budget?
Not just processing and packaging equipment. Budget should include utilities, tanks, piping, controls, CIP, building modifications, drains, commissioning, spare parts, startup support, and contingency for compliance-driven changes.
How should a brand choose an engineering and integration partner?
Choose a team that understands beverage processing, alcohol compliance constraints, utilities, controls, installation, and commercialization timing. The strongest partners focus on total project profitability, not just equipment sales. For example, DPS serves food and beverage manufacturers across North America with a design-build-manage approach that combines technological capabilities such as process and controls engineering, manufacturing capabilities including custom tanks and CIP systems, and service capabilities spanning feasibility, owner’s representation, project management, installation, and commissioning. Readers can explore recent project case examples to see how integrated execution supports real production outcomes.
In summary, canned cocktail production line design in the United States is a multidisciplinary challenge involving market strategy, compliance, process science, packaging performance, and capital efficiency. The most successful producers design their systems around product reality: actual ingredients, actual logistics, actual quality standards, and actual growth plans. When that happens, the result is not simply a working line. It is a line that supports profitable scale.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

