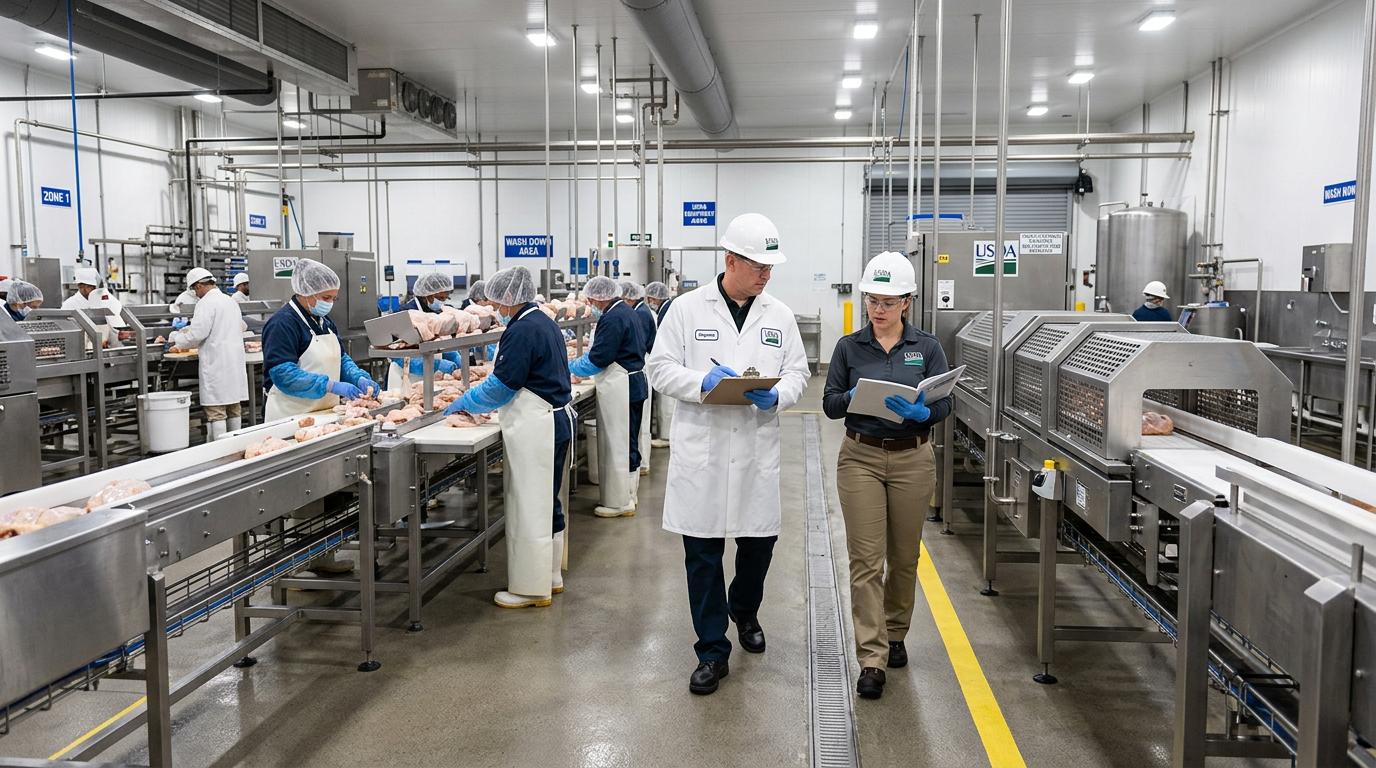
Food Facility HVAC Design Requirements: Pressure Zoning and Air Quality Control
[trp_language language=”en_US”]
Food facility HVAC design in the United States is not just about comfort. It is a production control system that protects product safety, manages condensation, separates raw and ready-to-eat spaces, supports sanitation, and reduces regulatory risk. In meat, dairy, beverage, prepared foods, aseptic, and packaging environments, the HVAC basis of design should align with process flow, USDA or FDA expectations, sanitation methods, worker density, utility loads, and the local climate. A plant in Houston faces moisture and latent load challenges that differ sharply from a dry operation in Fresno or a cold-storage project near Chicago. The right design balances pressure zoning, make-up air, exhaust capture, purge cycles, and air changes per hour so that product zones remain stable during production and recover quickly after washdown.
For U.S. manufacturers planning a new build, retrofit, or expansion, the most effective approach is to treat air quality control as part of the full process design rather than as a late-stage mechanical package. This is especially important in high-throughput corridors such as the Midwest protein belt, dairy operations in Wisconsin and Idaho, beverage hubs in North Carolina and California, and import-dependent processors near the ports of Los Angeles, Long Beach, Savannah, Houston, and New York/New Jersey. In these regions, production schedules, utility resilience, labor conditions, and sanitation windows all influence the HVAC strategy.
Quick Answer

The fast answer is this: a compliant and practical U.S. food plant HVAC design should maintain room temperatures suited to the product and process, control relative humidity to prevent condensation and microbial growth, keep clean or high-care areas under positive pressure relative to adjacent lower-hygiene rooms, place raw, wet, chemical, and waste zones under neutral or negative pressure where appropriate, replace all exhausted air with properly conditioned make-up air, and deliver enough air changes per hour to dilute moisture, heat, particles, and odors. It should also include purge modes after sanitation, filtration matched to zone risk, and energy recovery where cross-contamination can be prevented.
In market terms, demand for hygienic HVAC solutions is rising across U.S. food and beverage manufacturing because operators are expanding automation, increasing line speeds, improving shelf-life performance, and preparing for stricter scrutiny around condensation, allergen segregation, and environmental monitoring. Facilities making ready-to-drink beverages, cultured dairy, cooked proteins, sauces, nutraceutical foods, and aseptic products are investing in better room control because unstable air often causes rework, spoilage, corrosion, and downtime before it triggers any formal compliance issue.
From a buying perspective, owners should not purchase HVAC equipment as isolated rooftops, air handlers, or exhaust fans. They should buy a zone-based control strategy. That means defining the process map first, then identifying where product exposure occurs, where sanitation chemicals are used, where warm product enters cold rooms, and where forklift traffic or dock openings disturb pressure cascades. Facilities in Atlanta, Dallas, Minneapolis, and the Inland Empire often discover that airflow failures are caused less by undersized fans and more by layout conflicts between process exhaust, dock operations, and sanitation schedules.
Typical product types that drive different HVAC requirements include raw protein lines, cooked or ready-to-eat packaging rooms, cheese and yogurt spaces, dry ingredient blending rooms, retort and canning areas, spirit and brewing facilities, aseptic filling suites, and high-moisture produce processing. Each has a different moisture profile, sensible load, exhaust requirement, and contamination control target. The practical lesson is simple: the HVAC design must follow the product risk profile, not a generic building template.
The line chart above reflects the broader market direction many processors are seeing: HVAC spending is moving up as plants modernize utility systems, build higher-care rooms, and prepare for 2026 priorities around energy efficiency, low-leakage envelopes, digital monitoring, and more resilient sanitation recovery.
Temperature and Humidity Control Standards

Temperature and humidity targets in U.S. food plants should be set by process need, product exposure, employee occupancy, and condensation risk. There is no single universal room condition for every facility. For example, a ready-to-eat slicing room may be maintained at a much lower temperature than a dry packaging room, while a sauce blending area may allow higher temperatures but needs close humidity control during cleanup and startup. The aim is to keep room surfaces above dew point where possible, prevent sweating on pipes and ceilings, and maintain stable conditions that support quality and shelf life.
In humid climates such as Florida, the Gulf Coast, and the Carolinas, latent load is often the hidden driver of HVAC underperformance. Plants sometimes install enough cooling tonnage but not enough dehumidification capability, which leads to fogging, slippery floors, and recurring ceiling condensation after washdown. In cold northern markets like Wisconsin or Pennsylvania, the challenge can shift to balancing ventilation with winter make-up air heating while preventing uncomfortable drafts and frozen coils near dock-adjacent areas.
| Zone Type | Typical Temperature Range | Typical Relative Humidity | Main Objective | Primary Risk if Uncontrolled | Design Note |
|---|---|---|---|---|---|
| Raw protein fabrication | 45-55°F | 50-65% | Limit product warming | Short shelf life, condensation | High washdown load requires robust dehumidification |
| Ready-to-eat packaging | 38-50°F | 45-55% | High-care microbial control | Airborne contamination, sweating surfaces | Positive pressure and tight envelope are critical |
| Dairy processing | 40-60°F | 50-60% | Product stability | Condensation on overheads and fillers | Coordinate with CIP and tank vent loads |
| Dry blending | 65-75°F | 35-50% | Powder handling and flowability | Caking, dust accumulation | Dust control may outweigh cooling demand |
| Beverage filling | 60-75°F | 45-60% | Line efficiency and package integrity | Labeling issues, wet conveyors | Account for rinse tunnels and warm product entry |
| Cold dock staging | 35-45°F | 50-70% | Temperature continuity | Warm moist infiltration from docks | Use vestibules or air curtains where traffic is heavy |
The table gives broad working ranges rather than universal mandates. In practice, many owners should perform a dew-point-based analysis instead of relying only on dry-bulb temperature. That is especially true in washdown rooms, freezer approaches, and facilities that bring warm kettles, retort baskets, or recently cleaned equipment into cooler spaces. For processors evaluating a retrofit, one of the best buying questions is not “What tonnage do we need?” but “What dew point must the room maintain during the worst sanitation-to-startup transition?”
By 2026, more U.S. facilities are expected to adopt continuous environmental logging tied to SCADA or building automation systems, with alerts for dew point excursion, not just temperature excursion. This supports both quality assurance and utility optimization.
Positive and Negative Pressure Zoning

Pressure zoning is the backbone of hygienic airflow control. Positive pressure is typically used to protect cleaner or more sensitive spaces so air moves outward when doors open. Negative pressure is used to contain odors, moisture, raw aerosol, chemical vapors, or waste-related contaminants. The target is not extreme pressure but a stable cascade that supports the product and the sanitation plan.
As a rule, high-care packaging, post-lethality, aseptic support, and some ingredient prep rooms should be positive relative to adjacent corridors. Raw receiving, inedible handling, chemical storage, certain wash rooms, and some waste rooms are often neutral to negative. This zoning becomes more important as plants scale up in complex logistics nodes such as Kansas City, Memphis, and central New Jersey, where throughput and door traffic can repeatedly collapse room balance if the building envelope and control sequence are weak.
| Area | Preferred Pressure | Relative Direction | Reason | Operational Trigger | Common Mistake |
|---|---|---|---|---|---|
| RTE packaging room | Positive | Higher than corridor | Protect exposed finished product | Door openings, staffing shifts | Insufficient transfer air planning |
| Aseptic support room | Positive | Higher than adjacent support | Reduce airborne contamination | Filter loading, maintenance events | Ignoring door interlocks |
| Raw receiving | Neutral to negative | Lower than clean prep | Contain odors and raw contaminants | Dock door cycles | Uncontrolled dock infiltration |
| Waste handling | Negative | Lower than process hall | Contain odor and aerosol | Bin movement, washdown | Shared return air paths |
| Chemical storage | Negative | Lower than corridor | Protect staff and adjacent products | Dispensing and spill events | Too little dedicated exhaust |
| Clean utensil storage | Positive | Higher than wash area | Prevent recontamination | Sanitation shift turnover | Placing near wet exhaust source |
The correct pressure zoning approach also depends on industry segment. Protein plants need strong separation between raw and post-cook spaces. Beverage plants often focus on filler halls, syrup rooms, and packaging stability. Dairy projects require careful air separation around cultured product, fillers, and washdown zones. Dry ingredient and seasoning operations may emphasize dust migration more than wet aerosol control.
For U.S. owners seeking practical guidance, the best projects define pressure zones during process design, then carry them into architectural detailing, controls, and commissioning. Doors, strip curtains, dock seals, vestibules, trench locations, and sanitation hose storage can all influence the success of the pressure plan more than a fan schedule alone.
The bar chart illustrates how demand varies by sector. Protein, aseptic, and prepared foods frequently require the most deliberate pressure zoning because the consequences of poor airflow are immediate in sanitation, quality, and compliance performance.
Make-Up Air System Design
Every cubic foot of exhaust air removed from a food plant must be replaced. If make-up air is not properly sized, conditioned, and distributed, the facility will pull air through dock doors, roof leaks, wall penetrations, and personnel entries. That unplanned infiltration is one of the most common reasons plants lose humidity control, see inconsistent room temperatures, and fail to hold intended pressure cascades.
Good make-up air design starts with an accurate inventory of all exhaust sources: process hoods, kettle vents, packaging area exhaust, chemical rooms, wastewater pretreatment spaces, restroom exhaust, and sanitation purge modes. Next comes diversity analysis, because not all loads run at once. Then the engineer determines how much replacement air should be supplied directly to the exhausted room, how much can be transferred from cleaner adjacent areas, and how the air must be heated, cooled, filtered, and dehumidified for summer and winter design days.
| Design Factor | Why It Matters | Typical U.S. Concern | If Ignored | Recommended Practice | Who Should Review |
|---|---|---|---|---|---|
| Total exhaust inventory | Sets base replacement requirement | Multiple hidden small exhaust points | Building goes strongly negative | Verify every fan and hood in basis of design | Mechanical and process teams |
| Latent load | Controls moisture entering building | High outdoor dew point in South and Southeast | Condensation and mold risk | Size dehumidification for worst-case washdown recovery | Mechanical and QA |
| Outdoor air intake location | Protects supply cleanliness | Truck exhaust, cooling towers, waste areas | Odor and contamination entrainment | Separate intakes from contaminant sources | Mechanical and site planning |
| Filtration level | Matches supply air to zone risk | Dust, pollen, nearby agriculture | Filter bypass and dirty high-care rooms | Use staged filtration by zone class | Mechanical and food safety |
| Air distribution pattern | Determines actual room performance | High racks, process lines, forklifts | Short-circuiting and dead zones | Model diffuser placement around product path | Mechanical and operations |
| Control integration | Stabilizes pressure and temperature | Frequent startup and sanitation transitions | Manual overrides and drift | Link fans, dampers, and room sensors in BAS | Controls and maintenance |
Buyers should also ask whether the make-up air system is being selected for present production only or for the future plant state. In rapidly growing beverage and food campuses near Phoenix, Charlotte, or Columbus, short-term undersizing often forces costly rework within two or three years. Future-ready design may include spare fan capacity, coil allowances, floor space for added dehumidification, and control architecture that can absorb new lines.
Process Exhaust and Ventilation
Process exhaust is different from general building ventilation. Its job is to capture heat, vapor, smoke, steam, fumes, dust, and odors at or near the source before they spread into the room. In food and beverage plants, this can include cooking lines, smokehouses, blanchers, bottle rinse systems, CIP tank vents, mixing vessels, spirit processing, powder unloading, chemical dispensing, and wastewater pretreatment areas.
The right exhaust strategy depends on the contaminant type. Steam and thermal plume loads often need canopy or slot capture. Corrosive chemical areas may need dedicated resistant materials and no recirculation. Dry ingredient systems may need dust collection with explosion and housekeeping considerations. Fermentation and distillation spaces can bring carbon dioxide, ethanol vapor, and hazardous area implications into the ventilation discussion. Plants near major craft beverage clusters in Oregon, Colorado, and North Carolina often underestimate these interactions during expansion.
One of the best ways to reduce long-term cost is to distinguish between air that truly needs direct exhaust and air that can be managed through room conditioning, local capture, or controlled transfer. Over-exhausting a room increases make-up air and dehumidification requirements, especially in coastal climates.
| Exhaust Source | Typical Contaminant | Preferred Capture Method | Key Design Issue | Risk to Adjacent Areas | Commissioning Check |
|---|---|---|---|---|---|
| Cook kettles | Steam and heat | Canopy or close-capture hood | Plume rise and operator access | Condensation on ceilings | Capture during full-boil operation |
| CIP tank venting | Moisture and chemical vapor | Dedicated vent/exhaust | Material compatibility | Corrosion and odor transfer | Check during hot caustic cycle |
| Dry ingredient dump | Dust | Local collection hood | Source containment | Cross-contact and housekeeping burden | Observe visible dust escape |
| Wastewater pretreatment | Odor and corrosive gases | Dedicated negative room exhaust | Isolation from fresh air intakes | Odor complaints and equipment damage | Pressure verification at doors |
| Distillation area | Ethanol vapor and heat | Ventilation with hazard review | Code coordination | Safety event and vapor migration | Airflow balance under peak run |
| Bottle or can rinse zone | Mist and moisture | Localized exhaust or enclosure | Avoiding wet packaging line surfaces | Slip hazards and label problems | Startup humidity recovery |
For U.S. facilities sourcing local trade support, the strength of the regional contractor market matters. Areas with mature industrial mechanical trades, such as Chicago, Milwaukee, Cincinnati, Houston, and Southern California, often provide more experienced installers for hygienic ductwork and coordinated utility tie-ins. In thinner labor markets, owners benefit from a design-build partner that can direct local trades with clear performance criteria and startup accountability.
Clean-Up Purge Cycle Requirements
Many food plants focus on production airflow but overlook cleanup recovery. After sanitation, rooms may be loaded with moisture, chemical residue, elevated temperature, and wet surfaces. If the HVAC system cannot purge and recover the space before startup, operators can enter production with ceiling condensation, damp packaging materials, poor visibility, and unstable pressure. That creates quality and safety risk even when the process equipment itself is clean.
A purge cycle usually increases exhaust and/or outside air, adjusts supply air condition, and shifts room control setpoints for a defined period after washdown. The exact sequence depends on room size, sanitation chemistry, water use, drain layout, wall and ceiling insulation, and whether equipment remains warm during cleanup. High-moisture rooms in poultry, seafood, dairy, and prepared foods often need the most deliberate purge strategy.
| Room Type | Typical Purge Trigger | Main Goal | Approximate Recovery Focus | Control Feature | Operator Check |
|---|---|---|---|---|---|
| Raw washdown room | End of sanitation cycle | Remove moisture and odor | Fast dew point pull-down | Timed purge with humidity reset | No visible fog or sweating |
| RTE room | Pre-op release | Dry and protect high-care surfaces | Stabilize positive pressure | Pre-op verification mode | Pressure and surface dryness confirmed |
| Dairy filler space | CIP completion | Reduce vapor around fillers | Maintain equipment readiness | Interlocked purge with line status | No condensation near product path |
| Cook room | Post-shift washdown | Clear heat and steam | Vent sensible and latent load | High exhaust / high supply mode | Temperature returns to target |
| Chemical room | Spill response or transfer event | Personnel protection | Rapid contaminant dilution | Emergency boost exhaust | Alarm and airflow confirmation |
| Packaging hall | Wet cleaning or line rinse | Dry floor and line surfaces | Prevent packaging defects | Short-cycle dehumidification boost | Materials stay dry during startup |
Plants buying new HVAC systems should insist that purge sequences be documented in the controls narrative and tested during commissioning. It is not enough to install hardware. The system must demonstrate that it can bring the room from wet sanitation conditions back to production-ready conditions within the available turnaround time.
The area chart reflects a clear trend: U.S. processors are moving from simple timer-based washdown recovery to smarter purge control based on humidity, room pressure, and pre-op readiness. This is likely to accelerate through 2026 as labor costs and startup delays become more expensive.
Air Changes per Hour by Zone Type
Air changes per hour, or ACH, help quantify how often the air volume in a room is replaced. In food plants, ACH supports heat removal, moisture control, particle dilution, and pressure stability. There is no single universal ACH number for every room, because actual needs depend on room volume, contamination load, occupancy, and process equipment. Still, using zone-based ACH targets is one of the most useful ways to structure design and commissioning.
| Zone Type | Typical ACH Range | Why It May Be Higher | Why It May Be Lower | Pressure Strategy | Design Comment |
|---|---|---|---|---|---|
| RTE high-care room | 15-25 ACH | Product exposure and traffic | Tight enclosure and low heat load | Positive | Filtration and air pattern are as important as ACH |
| Raw processing room | 12-20 ACH | Washdown moisture and occupancy | Limited thermal load | Neutral or slightly negative to clean zones | Coordinate with sanitation schedule |
| Dairy filler room | 15-20 ACH | Moisture-sensitive packaging and product exposure | Stable enclosed equipment | Positive | Control dew point tightly around fillers |
| Dry blending room | 8-15 ACH | Dust control and personnel load | Strong local dust capture installed | Depends on cross-contact strategy | Do not replace source capture with ACH alone |
| Cook room | 10-18 ACH | Heat and steam generation | Strong localized exhaust at source | Usually neutral | General ventilation cannot fix poor hood capture |
| Waste room | 10-15 ACH | Odor and sanitation moisture | Low occupancy and enclosed handling | Negative | Keep separate from clean return paths |
These values should be checked against room function, process hazard, and local code considerations. A low-risk warehouse does not need the same ACH as a post-lethality slicing room, and an aggressive ACH number alone does not guarantee hygienic performance if diffuser throw, return placement, and pressure control are poor.
Applications across U.S. industries vary. Poultry and seafood plants often emphasize moisture removal and sanitation recovery. Bakery and dry mix sites focus more on dust and ingredient segregation. RTD beverage plants care about packaging line stability, line-side comfort, and utility efficiency. Pharmaceutical-adjacent food or nutraceutical operations may demand tighter environmental logging and more rigorous airflow verification.
Energy Recovery Ventilation Systems
Energy recovery ventilation can lower operating cost in food plants, but it must be applied carefully. The concept is simple: recover sensible and sometimes latent energy from exhaust air to precondition incoming outside air. The challenge is contamination control. In hygienic facilities, the designer must ensure that the recovery strategy does not create leakage or cross-contamination between dirty and clean air streams.
In many U.S. applications, runaround loops, glycol systems, or other separated recovery methods are favored where hygiene risk is high. In lower-risk utility or support spaces, other recovery options may be practical. The business case is strongest in locations with large temperature differences, high ventilation volumes, or expensive dehumidification, such as Minneapolis, Denver, Boston, Nashville, and much of the Southeast. Plants near ports and logistics corridors with long operating hours can also see strong returns if they run extensive outside-air systems continuously.
By 2026, the strongest trend will likely be selective energy recovery paired with real-time monitoring of pressure, filter loading, fan energy, and humidity performance. Owners are also showing more interest in heat pump integration, lower-carbon utility strategies, and advanced sequences that reduce simultaneous heating and cooling.
The comparison chart is a practical planning tool rather than a universal ranking. A system that is ideal for a beverage warehouse support area may be wrong for a high-care protein packaging suite. The right answer depends on hygiene class, climate, utility cost, maintenance skill, and contamination tolerance.
For buyers evaluating equipment options, this is where supplier comparison matters. Ask not only about nominal efficiency but also about cleanability, coil access, material durability, controls integration, freeze protection, and whether the supplier has documented food-plant experience in your climate region.
Our Company
For manufacturers that need help tying process, utilities, and building systems together, Disruptive Process Solutions brings a practical design-build-manage approach tailored to food and beverage production across the United States and Canada. Rather than treating HVAC as a standalone bid package, the team aligns air systems with production economics, sanitation realities, and long-term expansion planning. That is especially valuable for operators balancing speed, capital discipline, and compliance in competitive markets such as Texas, the Carolinas, California, the Midwest, and major logistics corridors.
On the technological side, DPS supports integrated engineering across mechanical, process, plumbing, electrical, structural, and controls disciplines. That means HVAC decisions can be coordinated with utility demand, automation logic, SCADA visibility, CIP systems, boilers, glycol, refrigeration, compressed air, and line performance. For processors planning higher-care rooms, aseptic support, beverage utilities, or protein expansions, this cross-functional capability reduces the common gap between process design intent and actual room behavior. You can learn more about the company background on the about us page.
On the manufacturing side, DPS also designs and supplies proprietary process equipment, including tanks, CIP systems, marination tumblers, and cooking vessels. That matters because room air control often depends on how the equipment operates, vents, cleans, and rejects heat. A project team that understands both the equipment and the environmental consequences can make better decisions about exhaust capture, make-up air, and purge recovery. Additional information is available through the company’s process equipment offering.
On the service side, DPS supports capital planning, feasibility work, owner’s representation, engineering, general contracting where licensed, installation management, and turnkey integration. This is useful for companies that need one partner to connect the basis of design to field execution and startup. Whether the job involves a beverage co-packing campus, a dairy upgrade, a protein relocation, or a rapid response retrofit, the focus remains on profitable project delivery and operational fit. You can review the broader engineering and project services and explore selected project case studies for examples of execution.
In real project terms, the most successful HVAC outcomes happen when the engineering team asks business questions early: Where is throughput constrained? Which rooms create the most downtime after sanitation? Is the bottleneck line-side comfort, condensation, utility cost, or contamination risk? That operating mindset is one reason many manufacturers prefer a partner that can challenge assumptions rather than simply price equipment.
FAQ
What is the most important HVAC principle in a U.S. food plant?
The most important principle is that airflow must support product protection and sanitation, not just comfort. Pressure zoning, dew point control, and source capture are usually more important than thermostat settings alone.
Do all food rooms need positive pressure?
No. Cleaner, higher-care, or post-lethality spaces often need positive pressure, but raw, waste, or chemical-related rooms may need neutral or negative pressure to contain contaminants and odors.
How do I know if my plant needs more dehumidification?
Signs include recurring condensation, wet ceilings, fog after washdown, damp packaging materials, slippery floors, or inability to recover rooms before startup. Gulf Coast and Southeast facilities are especially prone to this issue.
What ACH should I use for my project?
ACH should be based on room function and contamination load. High-care rooms may run substantially higher than warehouses or enclosed utility spaces. A zone-by-zone review is better than one blanket number.
Can energy recovery be used in hygienic food applications?
Yes, but system selection matters. Recovery approaches that separate air streams are often preferred in higher-risk applications. Hygiene risk, maintenance capability, and climate should guide the choice.
When should purge cycles be included?
Purge cycles should be included whenever sanitation adds major moisture, heat, or chemical vapor and the room must return to production conditions quickly. Wet protein, dairy, cook, and packaging spaces often benefit.
What should buyers ask during design review?
Ask for room-by-room temperature and humidity targets, pressure relationships, exhaust inventory, make-up air logic, purge sequences, ACH assumptions, filtration levels, and commissioning tests tied to actual production and sanitation scenarios.
Which industries benefit most from advanced food plant HVAC design?
Protein, dairy, aseptic, ready-to-drink beverage, prepared foods, and dry ingredient facilities all benefit, though the design priorities differ by process. Fast-growing sites near Chicago, Houston, Charlotte, Fresno, and major port regions often see the strongest return on improved environmental control.
How should a retrofit be prioritized?
Start with the highest-risk rooms and highest-cost failures: condensation hotspots, unstable high-care areas, sanitation recovery bottlenecks, and spaces where exhaust and make-up air are out of balance. A measured field assessment is often the best first step.
What are the biggest 2026 trends for food facility HVAC in the United States?
Expect more dew-point-driven controls, digital monitoring through BAS and SCADA, selective energy recovery, electrification where practical, stronger sustainability targets, and greater integration between process equipment design and room environmental control.
[/trp_language]
Complete Company Portfolio

About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share

