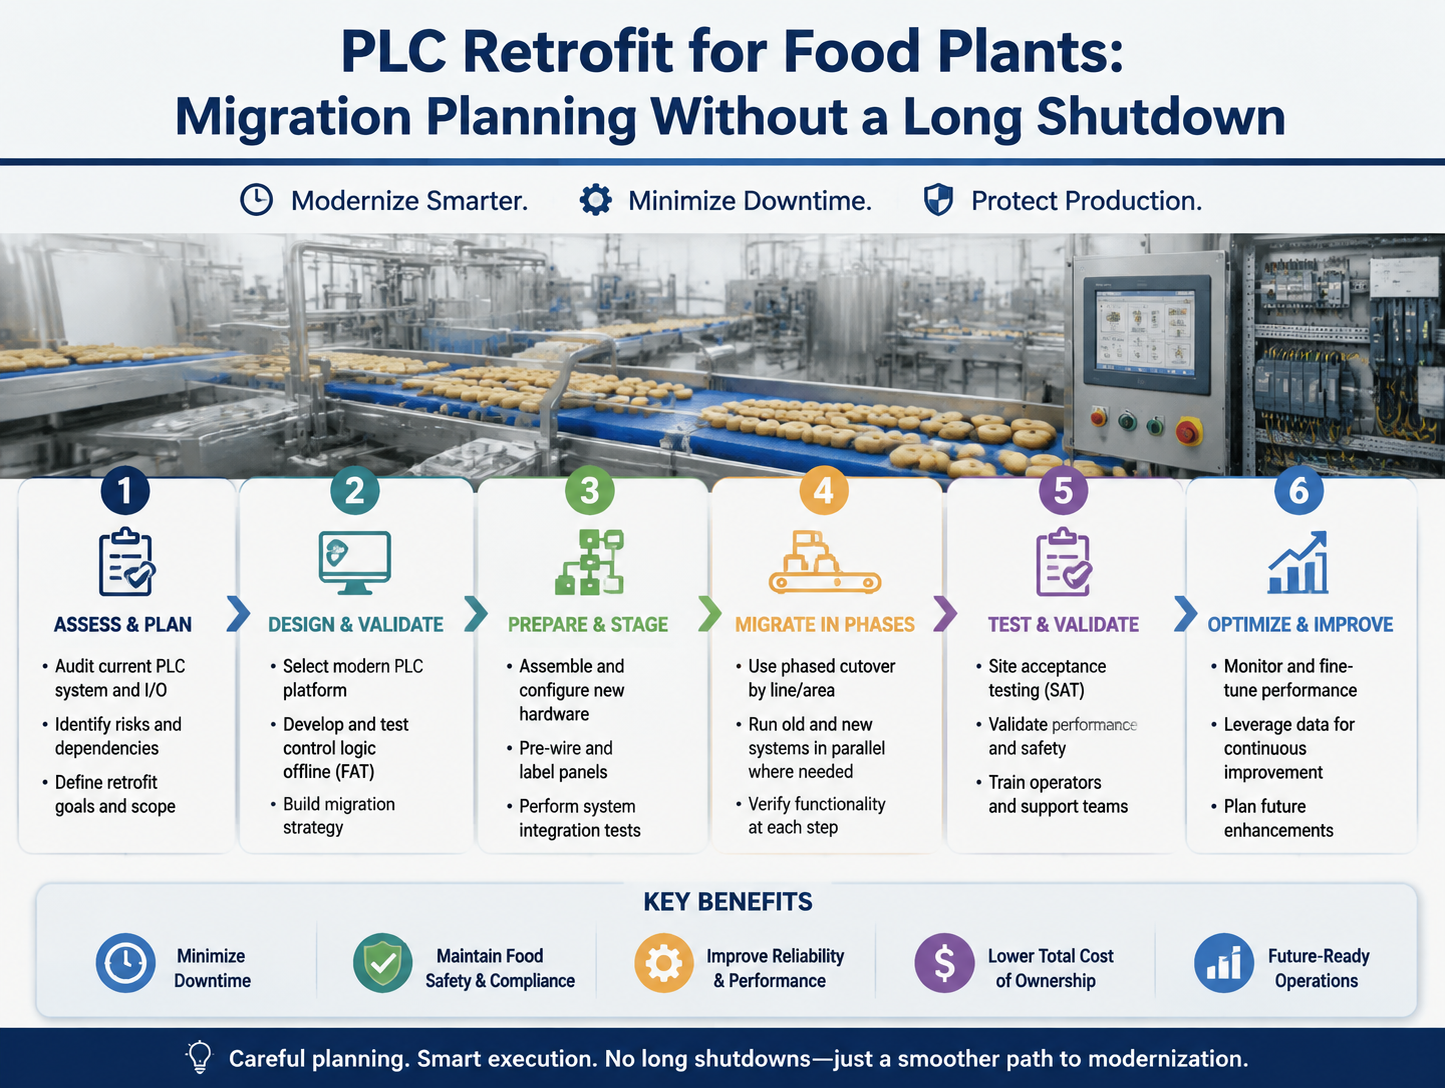
PLC Retrofit for Food Plants: Migration Planning Without a Long Shutdown
[trp_language language=”en_US”]
PLC Retrofit for Food Plants: A Practical U.S. Migration Guide
Quick Answer

A PLC retrofit for a food plant replaces or modernizes obsolete programmable logic controllers, operator interfaces, control networks, electrical panels, and production data systems without requiring a prolonged plant shutdown. The goal is not simply to install newer hardware. A successful food manufacturing controls retrofit improves reliability, sanitation support, batch consistency, traceability, operator usability, maintenance response time, and future production capacity.
For U.S. food and beverage manufacturers, a retrofit should begin with an operational and business case rather than a hardware list. The best migration plan identifies the production constraints that are costing the plant money, determines which assets can be upgraded during sanitation windows or scheduled maintenance, and establishes a phased commissioning strategy. This reduces the risk of an extended outage while preserving food safety controls and production continuity.
Disruptive Process Solutions (DPS) helps processors develop retrofit programs that connect capital decisions to measurable operating outcomes. Whether a facility is running legacy Allen-Bradley, Siemens, Modicon, GE, Omron, or mixed-vendor controls, the objective is to create a supportable, secure, and scalable automation platform that fits the plant’s production requirements.
Typical PLC retrofit priorities include:
- Replacing unsupported PLC processors, I/O racks, power supplies, and communication cards.
- Consolidating inconsistent HMIs and improving operator navigation.
- Adding recipe, batch, CIP, alarm, and downtime data functions.
- Connecting processing, packaging, utilities, and quality systems.
- Reducing unplanned downtime caused by failed legacy components.
- Improving access to spare parts, documentation, and remote support.
- Building cybersecurity controls into plant-floor architecture.
What Is a Food Plant PLC Retrofit?

A food plant PLC retrofit is the engineered replacement, redesign, or modernization of the automation layer that controls a manufacturing process. The scope can range from replacing one unsupported PLC in a packaging line to updating an entire facility’s process control, supervisory control, electrical distribution, network architecture, historian, and recipe management environment.
Unlike a simple “like-for-like” controls replacement, a food industry automation retrofit should account for how the line actually runs. A legacy system may have undocumented program changes, bypassed safety logic, manual recipe workarounds, unreliable signals, or disconnected utilities. Modernization is an opportunity to correct these issues before they become chronic production losses or compliance risks.
Food plants commonly retrofit controls in facilities producing prepared meals, sauces, dressings, dairy products, protein products, beverages, shelf-stable products, frozen foods, baked goods, ingredients, and co-packed consumer packaged goods. In high-throughput markets such as Chicago, Dallas-Fort Worth, Atlanta, Los Angeles, New Jersey, Central California, and the Carolinas, plants often need upgrades that fit tightly scheduled production calendars.
A retrofit can include a single production cell or multiple systems:
| Retrofit Scope | Typical Assets | Primary Business Objective | Common Shutdown Strategy |
|---|---|---|---|
| Machine-level upgrade | PLC, HMI, drives, sensors | Restore maintainability and uptime | Weekend or planned sanitation window |
| Packaging line modernization | Conveyors, fillers, checkweighers, case packers | Reduce stops and improve line visibility | Phased by machine or line segment |
| Process skid retrofit | Mixing, cooking, pasteurization, batching skids | Improve recipe accuracy and process control | Parallel build and short cutover |
| CIP controls upgrade | Tanks, pumps, valves, conductivity, temperature | Improve cleanability and cleaning records | Scheduled maintenance interval |
| Utilities controls integration | Boilers, refrigeration, compressed air, water | Increase reliability and energy visibility | Staged by utility system |
| Plant-wide SCADA migration | Servers, historians, networks, operator stations | Standardize operations and data management | Phased by area, with parallel operation |
Each scope calls for a different migration plan. The most successful projects separate what must be changed during downtime from what can be engineered, panel-built, configured, tested, and validated while the plant continues to run.
At ports and distribution hubs such as Savannah, Georgia; Houston, Texas; Long Beach, California; Newark, New Jersey; and Memphis, Tennessee, production interruptions can rapidly affect inventory commitments and outbound logistics. For these facilities, PLC migration planning must align with raw material availability, cold storage capacity, customer demand, labor coverage, and carrier schedules.
Operational Problems the System Should Solve

Before selecting a PLC family, manufacturers should define the operational problems the retrofit must solve. Replacing obsolete hardware without resolving process logic, operator workflow, or maintenance constraints can preserve the same inefficiencies in a newer panel.
Common warning signs include frequent nuisance trips, no available spare processors, repeated HMI failures, undocumented field changes, inconsistent product quality, extended sanitation cycles, poor alarm response, manual production records, and limited visibility into downtime. A plant may also have difficulty recruiting technicians willing to support outdated software platforms.
| Operational Problem | Likely Root Cause | Retrofit Response | Expected Operational Benefit |
|---|---|---|---|
| Frequent line stops | Obsolete PLC hardware or weak fault diagnostics | Modern PLC, organized code, fault logging | Faster troubleshooting and fewer repeat failures |
| Inconsistent batches | Manual additions and uncontrolled recipe changes | Recipe permissions, sequencing, verification | Better repeatability and reduced rework |
| Long CIP cycles | Fixed timing, poor instrumentation, valve issues | Conductivity logic, flow confirmation, reporting | More reliable cleaning and utility optimization |
| Operators miss alarms | Alarm floods and weak HMI design | Alarm rationalization and priority standards | Improved response to meaningful events |
| Lost production history | Paper records or isolated local HMIs | Historian, batch records, downtime tracking | Faster investigations and better decisions |
| Limited parts availability | End-of-life processors, drives, and modules | Supported platform and critical spares plan | Lower risk of extended outage |
| Inability to scale output | Control bottlenecks and manual sequencing | Logic optimization and capacity analysis | Higher throughput without unnecessary equipment |
The table should become the basis of the project’s functional requirements specification. It is also useful when presenting a capital request to leadership, because it connects technical deficiencies to production, labor, quality, and risk outcomes.
For example, a processor may initially believe it needs a major capacity expansion to increase output. A controls assessment can reveal that poor sequencing, excessive equipment interlocks, slow setpoint changes, or inadequate buffer management are the actual bottlenecks. DPS has seen situations where PLC programming improvements created significant throughput gains before new equipment was required.
PLC, HMI, SCADA, Network, and Data Architecture
A resilient food plant control system uses layers. The PLC controls the equipment in real time. The HMI gives operators a clear way to run and troubleshoot the process. SCADA provides supervisory visibility across multiple lines or areas. The industrial network connects devices securely. Data systems collect meaningful production, quality, utility, and maintenance information.
DPS brings technological capabilities in PLC programming, electrical and controls engineering, SCADA development, recipe management, energy monitoring, process integration, and automation commissioning. The architecture should be selected based on risk, available maintenance skills, installed equipment, plant standards, and expansion plans—not simply on the newest available platform.
| Architecture Layer | Typical Components | Food Plant Function | Design Consideration |
|---|---|---|---|
| Field layer | Sensors, valves, motors, VFDs, transmitters | Measures and actuates physical process conditions | Use hygienic, serviceable, documented instruments |
| Control layer | PLCs, remote I/O, safety controllers | Executes interlocks, sequences, and machine logic | Specify supported hardware and spare capacity |
| Operator layer | HMIs, industrial PCs, mobile terminals | Supports operation, maintenance, and diagnostics | Use consistent graphics and role-based access |
| Supervisory layer | SCADA, alarm servers, reporting tools | Coordinates areas and visualizes plant performance | Design for availability and controlled changes |
| Data layer | Historian, SQL database, MES interface | Stores production, batch, utility, and event data | Define retention, ownership, and backup practices | Enterprise interface | ERP, quality, warehouse, cloud analytics | Shares approved operational information | Segment IT/OT networks and limit exposure |
A robust migration often retains selected field devices if they are reliable and compatible, while replacing the control processor, I/O infrastructure, HMI, and network. This can reduce cost and shorten downtime. However, field devices should be evaluated individually. An old temperature transmitter, control valve positioner, or VFD may create hidden reliability problems that undermine the value of a new PLC system.
For process applications such as blending, thermal processing, fermentation, cooking, retort, cheese production, sauce manufacturing, and aseptic processing, the control architecture should provide clear separation between automatic sequences, manual operations, permissives, safety functions, and quality-critical control loops.
The following illustrative planning trend shows how food manufacturers are shifting retrofit spending from emergency hardware replacement toward connected, data-enabled controls modernization.
This trend does not mean every plant needs a large enterprise platform. A small co-packer may need a focused PLC/HMI upgrade with secure remote support and batch reporting, while a multi-site processor may need common standards, historian integration, and portfolio-level production analytics.
Learn more about DPS automation and controls engineering services for food and beverage facilities.
Recipe, Batch, Alarm, and Traceability Requirements
Recipe and batch control are central to a food plant retrofit whenever product quality depends on repeatable ingredients, temperatures, timing, agitation, pressure, fill volume, cook profiles, or cleaning parameters. A modern system should control who can create, approve, download, and modify recipes. It should also record what was actually executed during production.
For manufacturers operating under FDA, USDA, SQF, BRCGS, customer-specific, or internal quality requirements, traceability must be engineered into the process rather than reconstructed after an issue occurs. The right solution can connect lot numbers, ingredient additions, process parameters, operator actions, alarms, quality checks, and finished-goods records.
| Requirement | Recommended Automation Function | Data to Capture | Business Value |
|---|---|---|---|
| Recipe control | Versioned recipe management | Setpoints, steps, approvals, revisions | Prevents unauthorized or incorrect formulas |
| Batch execution | Sequenced production phases | Start/end time, steps, exceptions | Improves repeatability and investigations |
| Ingredient verification | Barcode, scale, or operator confirmation | Lot, quantity, supplier, timestamp | Strengthens material traceability |
| Critical process records | Historian and electronic reporting | Temperature, flow, pressure, dwell time | Supports quality review and compliance |
| Alarm management | Prioritized alarms with acknowledgment | Event, priority, user, response time | Reduces alarm fatigue and improves response | CIP verification | Automated CIP reporting | Time, temperature, conductivity, flow | Documents cleaning execution |
| Downtime classification | Reason-code workflow | Stop duration, cause, comments | Identifies recurring production losses |
Alarm modernization deserves particular attention. Many legacy systems treat every event as equally urgent. That creates alarm floods during a fault, making it difficult for operators to identify the true initiating cause. A retrofit should define alarm priorities, deadbands, delays, suppression rules, response guidance, and acknowledgment expectations. Operators need alarms that are actionable, not merely numerous.
Traceability requirements vary by product type. A dairy facility may prioritize pasteurization records and allergen changeover verification. A protein processor may focus on raw material lots, cook temperatures, yield, and packaging records. A sauce or dressing manufacturer may need strong control of formula revisions, ingredient additions, Brix, pH, and allergen handling. In each case, data design should follow the hazard analysis and operational workflow.
Integration with Existing Equipment and Utilities
Most food plants are not blank-slate facilities. They operate with a mix of equipment vintages, OEM controls, field modifications, packaged skids, utility systems, and manually operated processes. A PLC retrofit must integrate this reality rather than assume every asset can be standardized immediately.
Manufacturing capabilities at DPS include process equipment design and integration for tanks, CIP systems, cooking vessels, marination systems, pasteurization, blending, utilities, thermal processing, refrigeration interfaces, water treatment, and production support systems. This process knowledge matters because a controls project is only effective when the automation logic reflects the physical process, cleaning requirements, mechanical constraints, and operator actions.
For example, a new PLC controlling a CIP system must understand tank levels, chemical concentration, return conductivity, supply temperature, flow verification, pump protection, valve feedback, circuit routing, and production release logic. It must also coordinate with process equipment so that cleaning does not begin while a product path remains active.
| Existing System | Typical Integration Challenge | Retrofit Method | Key Verification Point |
|---|---|---|---|
| Legacy process skid | Limited drawings and unknown program logic | Field survey, I/O checkout, controlled migration | All process states operate as intended |
| OEM packaging equipment | Proprietary controls and limited access | Use defined communication interface | Fault, run, speed, and count signals are accurate |
| CIP system | Mixed manual and automated valve operation | Upgrade sequence logic and instrumentation | Cleaning parameters and circuit isolation are proven |
| Boiler and steam system | Separate vendor control packages | Read approved data and alarms into SCADA | Utility status is visible without unsafe control overlap |
| Refrigeration system | High consequence of communication loss | Segmented interface and alarm integration | Independent safety and operating logic remain intact | Water and wastewater | Variable loads and limited instrumentation | Add trending, level, flow, and pump controls | Capacity and discharge performance are monitored | Warehouse systems | Need for lot and production synchronization | Controlled MES or ERP data exchange | Data transfer is validated and secure |
Integration planning should include a detailed I/O list, communication map, cause-and-effect matrix, panel schedule, network diagram, operating narratives, and responsibility matrix. The plant also needs a clear decision about which vendor packages remain autonomous and which functions should be brought under common supervisory control.
Facilities upgrading sanitation infrastructure can pair controls modernization with new or expanded custom CIP systems for food processing. Integrating CIP controls, process valves, tanks, and production schedules early often avoids costly rework later.
Cybersecurity, Validation, and Compliance Considerations
Food manufacturing controls are operational technology systems. They require a cybersecurity approach that protects production availability, food safety functions, intellectual property, recipes, and plant data. Cybersecurity should be designed into the PLC retrofit from the start rather than added after commissioning.
Practical controls include network segmentation between IT and OT environments, managed industrial switches, firewalls, asset inventory, role-based access, strong authentication, remote-access approval procedures, backup management, patch governance, and incident response planning. The appropriate level of protection depends on plant size, connectivity, customer requirements, and operational risk.
Validation is equally important. A retrofit should be documented and tested in a manner appropriate to the product, process, and regulatory environment. The project team should establish what evidence is needed before production release: design review, factory acceptance testing, site acceptance testing, I/O checkout, dry runs, water runs, product trials, alarm testing, backup recovery testing, and operator training records.
Compliance does not come from a PLC brand. It comes from disciplined system design, documented controls, verified operation, controlled changes, and trained personnel. FDA-regulated, USDA-inspected, SQF-certified, BRCGS-certified, and customer-audited facilities may have different documentation needs, but all benefit from clear electronic records and reliable operating procedures.
The demand pattern above is an illustrative planning index. Beverage and protein facilities often prioritize uptime, high-speed packaging integration, thermal-process records, and utilities. Prepared foods, sauces, and dairy plants frequently place additional emphasis on recipe management, allergen control, batch documentation, and CIP verification.
Budget, Downtime, and Automation ROI
The cost of a PLC retrofit depends on the number of control panels, I/O points, field devices, safety circuits, network components, HMI screens, SCADA functions, data requirements, documentation quality, and commissioning constraints. The least expensive initial quote is not always the lowest-cost project. An under-scoped retrofit can create missed functionality, emergency field changes, delayed start-up, and recurring maintenance problems.
For many food plants, the largest value drivers are avoided downtime, higher throughput, reduced scrap, faster changeovers, less manual reporting, reduced maintenance risk, and improved process consistency. A retrofit budget should compare the full cost of continuing with legacy controls against the staged cost of modernization.
| ROI Category | Measurement Method | Typical Retrofit Lever | Decision-Making Use |
|---|---|---|---|
| Unplanned downtime | Hours lost and contribution margin impact | Reliable hardware and better diagnostics | Quantifies cost of failure risk |
| Throughput | Units, pounds, or cases per hour | Sequence optimization and line balancing | Shows capacity unlocked before expansion |
| Labor efficiency | Manual tasks per shift and overtime | Automated reports, recipes, and changeovers | Supports workforce planning |
| Scrap and rework | Yield loss, holds, and disposal cost | Accurate controls and batch verification | Connects automation to quality margin |
| Maintenance cost | Emergency repairs, parts, contractor time | Supported components and documentation | Reduces reactive spending | Utility consumption | Steam, water, compressed air, refrigeration use | Trending and optimized process logic | Supports sustainability goals | Compliance exposure | Audit findings, record gaps, investigation time | Electronic records and controlled access | Reduces operational and reputational risk |
Downtime planning is where retrofit projects are won or lost. The recommended approach is to perform as much work as possible before the production cutover. This includes field surveys, panel fabrication, off-line programming, HMI development, simulation, factory acceptance testing, cable preparation, labeling, documentation, and operator training.
During the outage, the team should follow a detailed cutover schedule with named owners, test points, spares, rollback criteria, and escalation contacts. In plants with limited shutdown windows, systems can be migrated by area, panel, machine group, or utility subsystem. Temporary gateways or parallel control arrangements may be used when technically appropriate and safe.
By 2026 and beyond, food manufacturers are expected to place greater value on phased modernization, energy-aware operations, digital batch records, secure remote support, and systems that can adapt to labor constraints. Sustainability initiatives will increasingly affect automation decisions through water use, chemical use, refrigeration optimization, waste reduction, and utility monitoring.
How DPS Delivers Food Plant PLC Retrofits
DPS delivers PLC retrofit food plant projects through a practical Design Build Manage approach. The process begins with understanding the client’s commercial objectives, operational pain points, production constraints, available capital, and risk tolerance. The final solution may include controls modernization alone, or it may be coordinated with process upgrades, utility work, equipment relocation, capacity expansion, or sanitation improvements.
DPS service capabilities include process engineering and design, capital planning, owner’s representation, project management, general contracting support, equipment supply, controls integration, installation coordination, commissioning, and start-up support. This full-scope approach allows food and beverage manufacturers to manage complex projects with fewer gaps between the process, mechanical, electrical, and automation disciplines.
The DPS project method is designed to support facilities across the United States and Canada, including processors operating in Raleigh-Durham, Charlotte, Atlanta, Nashville, Chicago, Minneapolis, Dallas, Houston, Denver, Phoenix, Seattle, Los Angeles, and the Central Valley. DPS combines a lean project-focused team with a vetted network of local trades and specialized partners.
- Assess: Review current controls, electrical infrastructure, process risk, documentation, production losses, and spare-parts exposure.
- Define: Create a functional scope that identifies mandatory replacement items, desired improvements, future expansion requirements, and compliance needs.
- Engineer: Develop control narratives, P&IDs, I/O lists, network architecture, panel designs, HMI standards, and test plans.
- Build: Fabricate panels, configure software, stage equipment, test controls off-line, and prepare field installation packages.
- Install: Coordinate electrical, mechanical, controls, and production teams around a documented shutdown and cutover plan.
- Commission: Complete I/O checks, dry testing, water testing, product trials, training, documentation, backups, and final turnover.
- Optimize: Use production data and operator feedback to tune sequences, alarm settings, downtime codes, and reporting after start-up.
Clients seeking a broader facility roadmap can also use DPS food process engineering and design services to align controls investments with future capacity, sanitation, utility, and equipment plans.
DPS is particularly effective when a retrofit must support profitability rather than merely replace hardware. The team evaluates whether a programming correction, process adjustment, utility change, or targeted equipment modification can remove a bottleneck before recommending a larger capital expenditure.
This comparison is an illustrative planning framework, not a vendor rating. It demonstrates why processors should compare retrofit partners on engineering depth, process knowledge, shutdown execution, documentation, and commissioning support—not only on equipment pricing.
FAQ
How long does a food plant PLC retrofit take?
Planning, engineering, panel fabrication, programming, and testing may take several weeks or months depending on scope. The actual production outage can often be limited to a weekend, sanitation window, or phased series of short shutdowns when the project is thoroughly prepared in advance.
Can a PLC be replaced without changing all field devices?
Yes. Many projects retain motors, valves, sensors, drives, and OEM packages that remain reliable and compatible. However, field devices should be surveyed and tested because unreliable instrumentation can limit the benefit of a new PLC system.
Should a plant standardize on one PLC manufacturer?
Standardization can simplify training, spare parts, programming standards, and long-term support. However, the decision should consider existing installed assets, local support, OEM constraints, lifecycle status, cybersecurity needs, and plant-specific technical skills.
What is the best time to schedule a controls retrofit?
The best time is usually a planned maintenance shutdown, seasonal production gap, major sanitation period, or coordinated equipment installation. Plants should avoid scheduling a high-risk cutover during peak demand periods unless a detailed contingency plan is in place.
How does a retrofit improve food safety?
A properly engineered retrofit can improve control of critical parameters, recipe execution, CIP verification, alarm response, electronic records, access permissions, and traceability. It does not replace food safety programs, but it can strengthen the consistency and documentation of those programs.
Can PLC retrofit work improve capacity without buying new equipment?
Often, yes. Improved sequencing, reduced interlock delays, better line coordination, accurate setpoints, improved operator visibility, and faster fault recovery can remove production constraints. A controls assessment should be completed before assuming a major equipment expansion is necessary.
What documentation should be included in a PLC retrofit?
At minimum, the project should include current and updated electrical drawings, network diagrams, I/O lists, PLC and HMI backups, operating narratives, alarm lists, panel schedules, test records, training materials, spare-parts recommendations, and change-control documentation.
What should food manufacturers ask before selecting a retrofit partner?
Ask about food and beverage process experience, controls platform knowledge, electrical and network engineering capabilities, field installation coordination, shutdown planning, FAT and SAT procedures, cybersecurity practices, documentation standards, commissioning resources, and post-start-up support.
[/trp_language]
Complete Company Portfolio
About the Author: Disruptive Process Solutions (DPS)
The DPS team combines process engineering expertise with real-world food and beverage manufacturing experience. Our content focuses on process optimization, production efficiency, facility improvements, and practical solutions that help manufacturers operate more effectively in a rapidly evolving industry.
Share