-
Food Processing Equipment Relocation
Relocating food processing equipment is not just a moving job. It is an engineering, compliance, sanitation, controls, utilities, and startup project that directly affects product safety, plant uptime, labor efficiency, and capital return. In the United States, successful food equipment relocation requires disciplined planning from the first equipment assessment through final commissioning, quality verification, and production ramp-up. For manufacturers moving lines between cities such as Chicago, Dallas, Los Angeles, Atlanta, Charlotte, Houston, or Toronto-linked North American networks, the biggest risk is rarely transportation alone. The real risk is losing hygienic integrity, process capability, throughput, or regulatory readiness after the equipment arrives. Disruptive Process Solutions, or DPS, supports food and beverage manufacturers across North America with a design-build-manage approach that connects engineering, installation, utility integration, controls, and startup under one accountable team. That matters when a relocation includes pasteurizers, retorts, fillers, conveyors, blending skids, cooking systems, CIP loops, compressed air, steam, refrigeration, and SCADA integration. Whether the project involves a plant consolidation in the Midwest, a line transfer from California to Texas, or a capacity expansion near the Port of Savannah or the Inland Empire logistics corridor, the relocation strategy must protect production continuity and future profitability. Food processing equipment relocation in the United States should be handled as a turnkey capital project rather than a simple rigging task. The best outcomes come from combining pre-move condition assessment, utility mapping, controlled electrical and controls disconnection, sanitary packaging for transport, qualified reinstallation, precision alignment, calibration, HACCP and preventive controls review, and final startup documentation. This approach reduces contamination risk, startup delays, hidden repair costs, and compliance gaps. If you are moving a single machine or an entire processing line, the practical sequence is straightforward: For plants operating under FDA, USDA, SQF, BRC, or customer-specific audit requirements, relocation should also include documented startup protocols, maintenance baseline checks, spare parts planning, and training for operations and sanitation teams. The table above shows why relocation is a staged process. Every phase has a different owner, a different failure mode, and a direct effect on production readiness. Food manufacturers in the United States relocate a wide range of assets, from stand-alone vessels to complete integrated process systems. Some moves are part of mergers or plant consolidation programs. Others happen when a producer outgrows an older facility, adds co-packing capacity, or repurposes idle equipment from one region to another. In high-cost markets such as Southern California, New Jersey, and the Pacific Northwest, it is common to relocate selected equipment to lower-cost production hubs in Texas, the Carolinas, Tennessee, or the Midwest. DPS supports moves involving both food and beverage assets, with technological capabilities that extend across thermal processing, aseptic systems, dairy, protein, sauce, ingredient, beverage, and packaging operations. This includes utility-heavy systems such as steam, chilled water, glycol, compressed air, water treatment, and CIP, along with automation layers like PLCs, SCADA, recipe management, and batch controls. This table matters because not all assets carry the same relocation risk. A conveyor move is usually simpler than a retort move, and a pasteurizer or aseptic filler requires far more documentation, validation, and utility coordination than a stand-alone tank. In many projects, equipment is only part of the scope. The move also involves structural modifications, drains, trenching, utility rack rerouting, controls cabinet relocation, chilled water balancing, compressed air quality checks, and plant layout redesign. That is where a partner with broad food engineering and installation services becomes more valuable than a basic hauling contractor. From a market perspective, the U.S. relocation environment remains active because manufacturers are rebalancing supply chains near major interstate corridors, rail hubs, and ports such as Houston, Long Beach, Newark, Savannah, and Charleston. Plants serving grocery, club, foodservice, and private label channels often choose relocation when lead times for new equipment are too long or when redeploying existing assets produces a faster payback. The growth trend above reflects the practical reality of the market: more manufacturers are treating relocation as a strategic capacity tool rather than a last-resort decision. Before any disconnect begins, each asset should be evaluated for structural condition, sanitary design suitability, spare parts availability, code fit, and startup risk. A common mistake is assuming that because equipment runs today, it is worth relocating tomorrow. In reality, older frames may be corroded, obsolete PLC platforms may be unsupported, and worn valves, seals, or drives may trigger a costly restart failure. A strong assessment includes mechanical inspection, utility demand review, controls backup, process suitability review, and total cost comparison between move and replacement. For food plants, product-contact surfaces, weld quality, dead legs, drainability, gaskets, and cleanability deserve special attention. The purpose of this assessment is not only technical. It is financial. A line that costs $600,000 to relocate but only has three to five reliable years left may be a poor capital decision. DPS is known for approaching these projects like an operations-minded advisor rather than a yes-only contractor. That means recommending process changes, controls optimization, or selective replacement when those choices improve long-term profitability. In some cases, a line move also becomes an opportunity to redesign the process flow. For example, a sauce line moving from a cramped Northeast facility to a larger Tennessee or North Carolina site may gain better ingredient handling, fewer forklift crossings, improved allergen segregation, and cleaner personnel traffic patterns. Those gains often deliver more value than the move itself. Although hygienic design language is often discussed globally, U.S. manufacturers should apply FDA, USDA, SQF, BRC, and customer sanitation expectations at the destination facility. The main objective after relocation is to verify that the reinstalled equipment still meets hygienic design intent and that the CIP system can clean all product-contact surfaces effectively after piping routes, tank elevations, and loop lengths have changed. Reinstallation verification should examine slope, drainability, dead legs, gasket compression, access for inspection, weld condition, passivation status when needed, and separation from non-sanitary utilities. Even a well-moved system can fail hygiene expectations if the destination floor has poor drainage or if maintenance creates inaccessible valve clusters. CIP re-integration is especially critical when moving blending systems, tanks, heat exchangers, fillers, and transfer circuits. New routing can change flow velocity, return temperature, chemical contact time, and pump performance. A loop that cleaned effectively in California may underperform after installation in Ohio if pipe runs are longer or elevation losses are higher. This verification stage is where technological capabilities matter. DPS supports sanitary process systems that include pasteurization, aseptic processing, retort, blending, fermentation, water treatment, and complete utility integration, so hygienic performance is addressed alongside mechanical installation and controls startup rather than as an afterthought. Manufacturers considering upgrades during relocation often combine the move with CIP modernization, tank addition, new instrumentation, or replacement of hard-to-clean legacy components. Information on available process equipment solutions can help teams decide whether to re-use existing skids, supplement them with new components, or redesign the sanitary loop entirely. Electrical and controls work is one of the most underestimated parts of food equipment relocation. A machine can be mechanically simple to move yet extremely difficult to restart if cable labeling is poor, VFD parameters are lost, remote I/O mappings are undocumented, or HMI recipes are not backed up. In highly automated plants, controls failures can add weeks to startup schedules. Best practice is to assign specialized teams for lockout-tagout planning, controls backup, panel isolation, instrumentation tagging, cable management, and re-energization procedures. This is especially important for integrated packaging lines, batching systems, and plants with networked SCADA layers. Transportation itself should be engineered around sanitary and mechanical protection. Stainless surfaces need proper wrapping, instruments need shock protection, and rotating equipment often requires stabilization. Cross-country moves between hubs such as Chicago and Phoenix, or Seattle and Dallas, may also require climate-aware packaging and route planning. The bar chart highlights which sectors tend to generate strong relocation activity. Beverage, protein, and dairy projects often lead because their equipment carries high capital value and can justify carefully managed redeployment. From a service standpoint, DPS executes projects through coordinated engineering, installation, and integration management. That includes process, mechanical, plumbing, electrical, structural, and controls coordination, plus management of local trades when jurisdictions require regional execution support. This model reduces handoff losses between electrical contractors, riggers, programmers, and utilities installers. Manufacturers should also think about insurance, route constraints, and loading conditions. Equipment moved through the Port of Houston, New Jersey logistics corridors, or West Coast intermodal networks may face different lead times, permitting needs, and rigging sequences than short-haul interstate moves. Once equipment is physically set, it must be restored to operating precision. This stage is often where relocation projects either recover full performance or suffer chronic problems. Misalignment can lead to premature bearing failure, leaks, poor fill accuracy, inconsistent cook times, packaging jams, inaccurate temperature control, and weak OEE. Precision restoration includes laser alignment, leveling, anchor verification, chain and belt tensioning, valve stroke checks, flowmeter verification, pressure transmitter calibration, load cell testing, recipe confirmation, and motion synchronization across line segments. For thermal equipment, temperature sensors and control loops should be checked before any process challenge test begins. The explanation here is simple: even if equipment survives transport perfectly, small geometric or instrument errors can reduce capacity and quality. In food manufacturing, those issues quickly become waste, customer complaints, or sanitation downtime. Relocation also creates a prime opportunity for modernization. Many U.S. plants use the move to update sensors, replace old HMIs, install more reliable drives, improve data capture, and refine automation logic. That approach aligns with 2026 trends: smarter diagnostics, digital maintenance dashboards, energy monitoring, and easier integration with enterprise systems. After reinstallation, food safety controls must be revalidated in the context of the new facility. The equipment may be the same, but the hazards can change because of new traffic patterns, utility conditions, zoning, water quality, environmental loads, or line speeds. For plants operating with HACCP, HARPC, preventive controls, USDA plans, or customer standards, relocation should trigger a documented review of critical control points and prerequisite programs. Examples include rechecking pasteurization hold times, retort parameters, allergen segregation procedures, metal detection or X-ray performance, sanitation verification, compressed air quality, and environmental monitoring plans. A destination facility in humid Gulf Coast conditions may need different condensation control strategies than a dry Mountain West plant. A protein line moved into a mixed-product facility may require stronger zoning and sanitation barriers than before. The area chart illustrates a major trend: manufacturers increasingly prefer validated relocations that include startup proof, sanitation review, and documentation rather than simple mechanical set-and-leave work. Case experience across North America shows that revalidation is one of the strongest predictors of a smooth commercial restart. A project may appear complete when the line runs water, but production success depends on proving that the process still delivers safe product at target speed, quality, and yield. DPS has built a reputation for integrating process engineering with startup execution, especially in regulated environments where FDA, USDA, SQF, and BRC expectations must be addressed together. Real-world examples of project execution philosophy and outcomes can be seen through selected food and beverage case studies, where business value and technical performance are both part of the result. In the United States, re-approval after relocation generally involves facility permits, utility reviews, inspection readiness, pressure vessel considerations, electrical compliance, process documentation updates, and food safety record revisions rather than a single “Factory Act” process. The principle remains the same: relocated equipment must be documented well enough for internal approval, authority review, insurer expectations, and third-party audits. Documentation should cover as-built layouts, P&IDs, electrical one-lines, I/O lists, panel schedules, controls backups, calibration records, commissioning reports, sanitation verification, SOP updates, and training records. If the move involves boilers, pressure systems, ammonia or refrigerant connections, or structural changes, additional local and state documentation may apply. Plants in jurisdictions such as California, Texas, Illinois, North Carolina, Georgia, and New York may encounter different combinations of electrical, building, fire, wastewater, and environmental review requirements. That is why local coordination matters, especially when relocating equipment into older facilities with legacy infrastructure. The explanation is practical: the more complete the documentation package, the faster the destination facility can move from installation to dependable routine production. Food equipment relocation often fails at the handoffs. The rigger says the electrician will tag it. The electrician says the controls team has the backups. The mechanical installer says sanitation verification is outside scope. The plant then loses days or weeks sorting out gaps. A single-point turnkey model avoids that fragmentation. With one accountable lead, equipment assessment, engineering, scheduling, utility design, controls backup, transport coordination, reinstallation, startup, and documentation are managed as one system. That reduces scope disputes and makes schedule recovery easier when field conditions change. DPS is structured for this kind of execution. Its service capabilities include engineering, project and program management, owner’s representation, general contracting or GC-equivalent coordination, physical installation, utility integration, controls work, and commissioning. Its manufacturing capabilities add value because the company can supply selected proprietary assets such as tanks, CIP systems, tumblers, and cooking vessels when a relocation reveals gaps or when replacement is smarter than repair. More about the team and its operating philosophy is available on the company overview page. For buyers comparing options, the smartest evaluation criteria are not just move price. Look at total downtime, startup guarantee approach, utility integration experience, food safety understanding, controls depth, documentation standards, and willingness to challenge weak assumptions. The lowest bid can become the highest-cost outcome if the line misses launch dates or operates below planned throughput. In the U.S. market, this advantage is especially visible in multi-line relocations, brownfield expansions, and projects where the destination site needs new utilities, sanitary zoning updates, or process redesign. It is also important for co-packers and fast-growth brands that cannot afford extended downtime. The comparison chart reinforces what many plant leaders already know from experience: coordination quality often determines whether a relocation protects revenue or disrupts it. Looking toward 2026, three trends will shape future relocation projects in the United States. First, automation modernization will increasingly be bundled into line moves, especially where legacy PLC platforms limit capacity. Second, sustainability goals will push more companies to reuse selected equipment rather than scrap it, while upgrading motors, heat recovery, water systems, and CIP efficiency. Third, policy and customer expectations will continue to raise the bar on traceability, documentation, energy performance, hygienic design, and auditable startup records. How long does food processing equipment relocation usually take?It depends on scope. A single skid may move in days, while a full line or plant transfer can take several weeks to several months when engineering, permits, utilities, and validation are included. Is relocating used food equipment always cheaper than buying new?No. The right answer depends on asset condition, controls obsolescence, utility compatibility, sanitation upgrades, and the cost of downtime. A pre-move assessment is essential. What industries most often relocate equipment in the United States?Dairy, beverage, protein, prepared foods, sauces, ingredient manufacturing, aseptic operations, and co-packing are among the most active sectors. Can packaging lines be relocated without losing line speed?Yes, if synchronization, controls backup, mechanical alignment, sensor calibration, and trial runs are managed correctly. Line speed losses usually come from weak recommissioning, not from the move itself. What documentation should plant managers ask for?Ask for condition reports, equipment tagging, utility maps, controls backups, as-built drawings, calibration records, commissioning reports, sanitation verification, and operator training documentation. Do CIP systems need to be revalidated after a move?Yes. Any change in piping length, elevation, valve arrangement, pump performance, or utility supply can affect cleaning effectiveness. Should we upgrade controls during relocation?Often yes. A move is one of the best times to replace obsolete PLCs, HMIs, drives, and networks because the equipment is already offline and being re-integrated. What local factors matter when relocating to a new U.S. region?Labor availability, utility costs, water quality, wastewater rules, climate conditions, access to interstate routes, port proximity, and local permitting timelines all affect the success of the move. Why choose DPS for a relocation project?DPS brings together technological capabilities in process and controls engineering, manufacturing capabilities in selected sanitary equipment supply, and service capabilities spanning design, installation, integration, and startup. That combination helps food and beverage manufacturers protect schedule, compliance, and ROI under one coordinated execution model. What is the first step if we are considering a move?Start with a structured assessment of the equipment, the destination facility, utility gaps, sanitation implications, and the financial case for move versus replace. That early discipline usually creates the biggest savings. -
5 Pillars of Integrated Pest Management for Food Facilities
Food facilities in the United States cannot treat pest control as a side task. In meat plants, dairies, bakeries, beverage operations, frozen food sites, dry ingredient warehouses, and co-packing plants, pest activity can quickly become a food safety event, an audit nonconformance, or a production disruption. Integrated pest management works best when it is built into operations, maintenance, sanitation, and capital planning rather than handled only through reactive spraying or emergency callouts. Across major production corridors such as Chicago, Atlanta, Dallas-Fort Worth, Los Angeles, the Research Triangle, the Inland Empire, Kansas City, and the New Jersey port region, facilities face similar pressures: tighter third-party audits, more traceability expectations, more supplier scrutiny, and rising costs tied to waste, shutdowns, and customer complaints. A practical pest program in this environment depends on structured risk assessment, exclusion, monitoring, documentation, sanitation alignment, and trend-based corrective action. The fastest way to strengthen integrated pest management in a U.S. food facility is to focus on seven operating priorities: identify the exact pest species, rank risk by process area, close structural entry points, position monitoring devices based on traffic and biology, document bait activity precisely, connect findings to sanitation and harbor reduction, and review trend data monthly with both the plant team and the pest contractor. Facilities that do this consistently typically reduce repeat findings, improve audit confidence, and avoid the expensive cycle of emergency treatments and recurring contamination risk. For most processors, the best buying decision is not simply choosing the lowest-cost pest service. It is selecting a program that can stand up to FDA, USDA, SQF, and BRC expectations while matching the realities of the plant layout, ingredient profile, traffic flow, and utility design. High-moisture beverage plants, raw protein operations, and dry goods warehouses each need different monitoring density, different sanitation controls, and different structural priorities. The table above shows why strong programs are cross-functional. Pest prevention touches building envelope design, floor drainage, air balance, traffic management, dock operation, waste handling, water control, and record discipline. That matters especially for facilities moving product through ports and distribution lanes tied to Savannah, Long Beach, Houston, Newark, and Seattle, where inbound and outbound traffic raises exposure. Integrated pest management starts with knowing exactly what is present. “Rodent activity” is too broad. A roof rat issue at a warm coastal beverage plant in Southern California behaves differently from a house mouse problem in a dry bakery warehouse in Ohio, and both differ from stored product insect pressure in a grain-based ingredient facility near Kansas City. Correct identification determines where to inspect, what attractants to remove, how far pests travel, and what monitoring tools make sense. In U.S. food plants, the most common categories include commensal rodents, flies, cockroaches, ants, occasional invaders, and stored product insects such as Indian meal moths, cigarette beetles, flour beetles, and warehouse beetles. Each category has a distinct biology. Flies often indicate drainage, decaying residues, wet waste, or door-management issues. Stored product insects may point to older inventory, spills under equipment, or infested incoming raw materials. Rodents usually reveal structural gaps, dock discipline failures, vegetation contact, or poor waste container control. Risk assessment should map the site by vulnerability, not just by square footage. Raw receiving, ingredient storage, packaging storage, processing rooms, utility spaces, employee welfare areas, roof penetrations, and exterior waste zones all deserve different ratings. The highest concern areas are normally high-care rooms, exposed product zones, allergen-sensitive storage, and packaging areas immediately upstream of filling or sealing. The practical lesson from this table is that not all captures mean the same thing. One warehouse beetle in a pheromone trap may justify a receiving review. One mouse in a high-care corridor may demand immediate escalation, line inspection, structural repair, and temporary segregation steps. Plants should define response thresholds in writing by species and zone. Risk assessment is also influenced by product type. A ready-to-drink beverage facility with syrup rooms and sweet residues is vulnerable to flies and ants. A protein plant with wet cleaning, warm byproduct streams, and dock traffic may face fly pressure and rodent attraction. A dry powder operation can see stored product insects from raw material movement. This is where plant design and engineering matter: zoning, drainage slope, wall penetrations, ceiling access, utility routing, and hygienic equipment support all affect pest risk over the long term. Exclusion is often the highest-return investment in integrated pest management because it addresses the entry pathway instead of only treating the symptom. In the United States, many food plants occupy converted industrial buildings, older warehouses, or expanded campuses where multiple construction phases created envelope weaknesses. Loading docks, personnel doors, roof penetrations, pipe chases, expansion joints, roll-up doors, and wall-floor interfaces are common failure points. A useful exclusion review should include daytime inspection, after-dark light leak inspection, roof review, dock review, and utility entry verification. Inspectors should evaluate door sweeps, door closure speed, dock leveler gaps, bird access at canopies, air curtain performance, screen condition, and drainage. Exterior grounds matter too. Standing water, dense vegetation, unmanaged pallets, scrap storage, and overflowing compactors can defeat even a strong interior program. Facilities near Gulf Coast humidity, Midwest grain lanes, or major port traffic often need stronger dock discipline because frequent trailer movement increases exposure. The same is true around rail-fed ingredient sites and cross-dock distribution centers. If a receiving bay remains open for operational convenience, monitoring may detect the issue, but exclusion solves it. This table shows that exclusion failures are rarely mysterious. They are physical, observable, and correctable. The challenge is ownership. The most effective plants assign each gap to maintenance or facilities with due dates and verification photos, then review closure during food safety meetings. For companies planning expansions, line additions, or utility upgrades, building integrity should be considered before equipment arrives. Firms that combine engineering with field execution can help reduce future risk by designing cleaner utility routing, stronger hygienic zoning, better drain layout, and easier-to-clean support structures. That type of up-front thinking is often more valuable than repeated downstream pest treatments. Monitoring is the data backbone of pest management. Device placement should follow pest biology, traffic flow, product sensitivity, and structural risk. Too many facilities still use a static map that has not been updated after line changes, warehouse re-racking, or expansion work. When packaging storage moved, did traps move? When a syrup room was added, were fly monitoring devices reassessed? When a utility trench was opened, did rodent risk change? Interior and exterior devices should not be placed simply by equal spacing. They should be positioned around doors, perimeters, utility corridors, ingredient receiving, waste routes, vulnerable corners, and historically active zones. Glue boards, mechanical traps, pheromone devices, insect light traps, and exterior rodent stations each have specific roles. In exposed product spaces, insect light traps should be chosen and oriented carefully to avoid drawing insects toward production. U.S. processors that ship nationally often face seasonal variation. The Southeast may see longer fly pressure windows, while northern states can see autumn rodent migration into warm buildings. Good monitoring maps reflect these shifts. The same is true for urban sites near dense food corridors versus rural sites near fields or livestock activity. The explanation here is straightforward: each device answers a different question. Monitoring only works when plants define what they want to learn from the device and what action is triggered by the result. A trap that creates no decision is only paperwork. Technology adoption is accelerating. Remote sensors, digital map platforms, photo-logged service reports, and dashboard alerts are becoming more common in 2026 planning cycles. For large networks of facilities, especially those spread across multiple states, digital standardization can make trend review faster and more consistent. Bait stations are one of the most misunderstood parts of a food plant program. Exterior baiting may be appropriate where risk justifies it, but it should never substitute for exclusion and interior sanitation. Every station should have a unique identifier, a current map location, secure anchoring where required, a service history, and clear notation of consumption, damage, or tampering. Missing or undocumented stations create audit exposure and can obscure real rodent pressure. Documentation should show not only that a station was checked, but what changed. Was there fresh feeding? Was a station relocated because of construction? Did landscaping increase harborage nearby? Were non-target conditions observed? Good records allow a plant to connect bait pressure with receiving patterns, weather, nearby construction, and housekeeping performance. In sensitive operations, especially those with USDA oversight, bait choices, station placement, and service language should align tightly with site policy. Interior toxic bait use may be highly restricted or prohibited in many food contact environments, so programs often rely more on mechanical devices indoors and baiting strategies outdoors. The message from this table is that documentation is not busywork. It is how a plant proves control, identifies change, and supports timely intervention. In many customer audits, weak records can damage confidence even when actual pest pressure is low. Sanitation and pest management are inseparable. Pests need food, water, and shelter. Most recurring issues survive because one or more of those conditions remain available after each service visit. In food and beverage plants, hidden residues under conveyors, syrup drips near tank farms, powder buildup under mezzanines, condensate near utility lines, and neglected employee areas are common enablers. Harborage elimination means more than general cleaning. It includes removing unused parts, limiting cardboard storage, managing idle equipment, cleaning beneath low-clearance assets, correcting leaks, and keeping wall perimeters inspectable. In older plants, dead spaces behind added panels, abandoned conduit openings, and inaccessible hollow frames can become chronic trouble spots. Sanitation integration works best when pest findings translate into specific cleaning tasks. If fly activity rises in a filler room, teams should inspect drains, gaskets, rinse cabinets, and nearby waste routes. If stored product insects appear in a spice warehouse, inspect aged inventory, torn bags, and structural ledges above storage racks. The corrective action should be location-specific and evidence-based. Buying advice for sanitation-linked pest control is simple: choose contractors and internal protocols that can diagnose root causes, not just count captures. Facilities with high-moisture processing, washdown systems, or sweet product handling should prioritize drain care, leak control, and residue mapping. Dry plants should prioritize dust, spillage, stock rotation, and inaccessible ledges. Harbor elimination also overlaps with capital project execution. Better equipment spacing, hygienic framework, drainage design, and utility coordination can reduce future residue traps. This is where engineering-minded project partners can bring value beyond a conventional contractor approach. By aligning process layout, utilities, and maintainability, facilities can lower chronic sanitation burden and therefore lower pest pressure. A pest control contractor should be managed as a technical service provider, not just a vendor that swaps traps. Food manufacturers need clear scopes, escalation paths, documentation expectations, service intervals, emergency response rules, and trend reporting standards. Plants should know who approves pesticide use, who signs off on corrective actions, and how unresolved structural issues are escalated. Service records should include inspection notes, devices checked, captures, species identified, sanitation observations, structural deficiencies, chemicals or non-chemical interventions used, and recommended actions with deadlines. The strongest plants review these records in cross-functional meetings that include QA, sanitation, operations, and maintenance. For multi-site operations in the United States, standardization matters. A plant in North Carolina should not use materially different documentation logic than a sister facility in Texas or California unless risk truly requires it. Consistent service records make enterprise review easier and support customer confidence. When facilities are expanding or adding process systems, contractor oversight should also connect to construction management. During shutdowns, line relocations, or wall penetrations, temporary pest exposure increases. Coordinating contractors with engineering teams reduces the chance that project work introduces long-term vulnerabilities. This is one reason many processors prefer partners that understand both plant operations and field execution. More on integrated project support can be found through food and beverage engineering services that bridge design, build, and operational oversight. Data without action does not improve food safety. Trend analysis should occur at least monthly and include device captures, species shifts, station consumption, high-risk zones, recurring sanitation observations, unresolved structural findings, and seasonality. A single spike may reflect a weather event or a receiving issue. A three-month upward pattern usually signals a process or building problem that remains open. Plants should chart findings by area and pest type, then match each trend to corrective action. If rodent exterior bait pressure rises at the west dock, review door timing, dock seals, waste handling, and adjacent vegetation. If fly captures increase near packaging, review drains, condensate, floor cleaning, and door practices. If stored product insects appear near a specific ingredient, inspect supplier history, lot age, and rack cleanliness. The table makes trend review practical by linking data to ownership and timeframes. This is what auditors, customers, and internal leadership want to see: not just findings, but a controlled management response. Looking toward 2026, three trends are shaping U.S. programs. First, digital monitoring and remote reporting will expand, especially in larger networks. Second, policy and customer requirements will continue pushing toward lower-risk, targeted interventions with stronger documentation. Third, sustainability goals will encourage facilities to emphasize exclusion, sanitation, material management, and precision treatment rather than broad chemical dependence. For food and beverage manufacturers that want pest prevention supported by stronger plant design and execution discipline, Disruptive Process Solutions brings a broader operational perspective than a typical specialty contractor alone. The company works across the United States and Canada, supporting processors with project-based engineering, installation, and integration that can materially affect long-term sanitation performance, equipment access, and building integrity. On the technological side, DPS supports structural, mechanical, plumbing, electrical, process, and controls engineering, including automation, PLC programming, and SCADA integration. Those capabilities matter in pest-risk reduction because utility routing, drainage, condensate control, process zoning, and line logic all influence housekeeping and exposure. Manufacturers evaluating expansions, utility upgrades, or sanitation-sensitive process changes can review service capabilities for engineered project support when planning preventive improvements rather than waiting for repeated operational symptoms. On the manufacturing side, DPS also develops and supplies selected process equipment such as tanks, CIP systems, marination tumblers, and cooking vessels. For processors seeking easier cleaning access and better operational flow, equipment selection and custom fabrication can support cleaner layouts and fewer harborage points. Additional information on process equipment solutions is useful for facilities modernizing high-moisture, protein, beverage, or aseptic systems. On the service side, DPS operates through a design-build-manage model that combines planning, construction coordination, project management, owner representation, and installation oversight. This is especially relevant when a plant is relocating lines, adding utilities, redesigning receiving zones, or scaling a co-packing operation where pest risk can change quickly during construction. Manufacturers can explore company background through the team and operating approach, or review project case examples to see how disciplined execution supports operational outcomes. In practical terms, DPS is not a pest control contractor. Its value in this conversation is helping food and beverage plants build cleaner, more maintainable, more operationally sound environments where integrated pest management becomes easier to execute and sustain. What is the most important part of integrated pest management in a food facility?Accurate identification and root-cause correction are the foundation. Without species-level understanding and area-specific response, facilities often spend money on repeated treatment without solving the entry or harborage issue. How often should a food plant review pest trends?At minimum, monthly. High-risk plants or sites under active pressure may need weekly review of key metrics such as rodent captures, fly trends, drain findings, and open structural actions. Are bait stations enough to control rodents?No. Bait stations can help manage exterior pressure, but exclusion, sanitation, waste control, and dock discipline are what prevent recurring problems. Interior control in sensitive spaces usually relies more on monitoring and mechanical devices. What pests are most common in U.S. food and beverage plants?House mice, roof rats, flies, ants, cockroaches, and stored product insects are common, but the mix changes by product type, geography, age of facility, and season. How should facilities near ports or major logistics hubs adjust their program?Sites near Savannah, Long Beach, Newark, Houston, or major inland freight corridors should give extra attention to receiving inspection, dock management, trailer gaps, pallet condition, and raw material quarantine procedures because traffic volume raises exposure. What records should always be available during an audit?Current maps, device logs, service reports, species identification records, pesticide usage records where applicable, corrective action logs, trend summaries, and verification that structural and sanitation issues were closed. How do capital projects affect pest risk?Construction can open walls, create dust, move traffic patterns, and expose utility gaps. Any expansion, line move, or shutdown should include temporary pest controls, post-project inspection, and map updates. What is changing in 2026?Expect greater use of digital monitoring, stronger documentation expectations, more sustainability focus, and tighter alignment between pest prevention, sanitary design, and cross-functional plant management. A mature integrated pest management program is not just a compliance necessity. It is a business system that protects product, uptime, customer trust, and long-term plant performance. For U.S. food manufacturers, the best results come when pest prevention is treated as part of facility design, operational discipline, and continuous improvement. -
Food Plant Foreign Material Control: 7 Prevention Strategies
Foreign material control in food manufacturing is a plantwide discipline that combines equipment design, inspection technology, supplier management, maintenance control, and employee behavior. In the United States, processors are expected to prevent, detect, and respond to risks such as metal, glass, stones, hard plastic, rubber, wood, and packaging fragments before product reaches consumers. The strongest programs do not rely on a single checkpoint. They build multiple barriers across receiving, processing, packaging, warehousing, and sanitation. For operators in major U.S. production corridors such as Chicago, Dallas, Fresno, the Carolinas, Central California, and the Gulf Coast, foreign material prevention is also tied to uptime, recall exposure, insurance pressure, customer scorecards, and retailer expectations. Plants shipping through Los Angeles/Long Beach, Savannah, Houston, or Port Newark often handle complex supply chains where ingredient variability raises contamination risk. That is why prevention strategies must fit the product, line speed, packaging format, and hazard profile of each facility. The fastest answer is this: food plants reduce foreign material incidents by using seven layered strategies. First, install and validate X-ray systems where density-based contaminants can be detected. Second, use metal detectors with routine challenge testing and disciplined calibration. Third, strengthen visual inspection with clear human error controls. Fourth, tighten supplier approval and incoming material verification. Fifth, manage glass and brittle plastic through a documented register and breakage response plan. Sixth, control tools, parts, and maintenance activity so equipment work does not create contamination. Seventh, train employees to report near misses immediately without fear. In the United States market, best results come when these controls are linked to HACCP, preventive controls, sanitation standard operating procedures, and food safety culture metrics. Facilities producing ready-to-eat proteins, dairy, beverages, sauces, frozen meals, bakery items, aseptic products, and contract-packed consumer goods usually need different combinations of detection and prevention points. A high-speed bottled beverage line in California may prioritize closure integrity and glass control, while a Midwest protein processor may focus more heavily on metal wear, knife management, and maintenance part accountability. Below is a practical summary of the most common foreign material sources seen across U.S. plants. This table shows why no single device can solve the issue. Foreign material prevention works when plants treat it as an integrated operational system rather than a standalone inspection step. X-ray inspection is one of the most valuable tools for identifying dense foreign material in finished product and, in some applications, in-process product. It is commonly used to detect metal, glass, mineral stone, calcified bone, and certain dense plastics, depending on product thickness, orientation, and package composition. X-ray also offers side benefits such as fill level checks, mass verification, and missing component detection. In the United States, high-risk categories such as ready meals, cheese blocks, nut products, confectionery, tray-packed meats, and bottled foods increasingly use X-ray as a critical verification step. Still, X-ray should never be oversold. It does not detect everything equally well. Low-density films, soft rubber, wood, paper, or very thin plastic may escape detection. Detection sensitivity also changes with product effect, package depth, temperature, and line speed. A frozen entrée in a black CPET tray presents different challenges than a pouch sauce, a glass jar, or a bulk protein chub. Plants should validate systems using realistic test pieces and worst-case product conditions rather than generic vendor assumptions. From a technology standpoint, the most effective systems are integrated into the line layout instead of being added as an afterthought. This is where a strong engineering partner matters. Disruptive Process Solutions supports processors with process engineering, controls integration, and capital planning that help align inspection technology with actual throughput, utilities, and operating constraints. For manufacturers expanding lines in states such as North Carolina, Texas, Wisconsin, or California, proper placement of X-ray units can reduce false rejects, improve access for sanitation, and protect downstream packaging efficiency. Plants should also distinguish between foreign body identification and simple rejection. If a line experiences repeat contaminants, the system should feed root-cause investigation. Image logging, reject confirmation, event coding, and trend analysis can reveal whether the source is upstream ingredient contamination, wear in a depositor, a damaged screen, or packaging line breakage. That information is what turns a detector from a reactive device into a preventive management tool. This comparison matters because equipment selection should match product physics. A plant that buys an X-ray machine without considering aperture, software, reject design, sanitation access, and package geometry often ends up with poor sensitivity or excessive false rejects. Metal detection remains a foundational control because it is versatile, widely understood, and often less costly than X-ray. It is especially useful for detecting ferrous, non-ferrous, and stainless steel contaminants in dry goods, bakery, snacks, meats, dairy, and packaged foods. However, good performance depends on aperture size, product effect, environmental conditions, and disciplined testing. The strongest U.S. plants challenge their systems at start-up, at regular intervals during production, at changeover, and at shift end using certified test pieces in realistic product carriers. Calibration is not just a technical formality. It is a management discipline that proves the detector is working under actual operating conditions. Wet products, salty products, hot products, and metallized packaging all complicate sensitivity. A detector that performs well on one SKU may fail on another. That is why leading plants maintain product-specific settings, documented challenge protocols, reject verification checks, and escalation rules whenever a test fails. The engineering side also matters. Poor conveyor stability, vibration, electrical noise, bad grounding, or cramped line layout can degrade detector performance. Processors planning new installations or line retrofits often benefit from working with firms that understand both process and controls. DPS provides structural, mechanical, electrical, process, and automation support, including PLC and SCADA integration, which helps inspection equipment communicate clearly with upstream and downstream devices. For plants adding metal detection to high-speed conveyance or washdown environments, this type of systems thinking helps prevent nuisance rejects and control downtime. In categories like seasonings, flour, snack inclusions, frozen vegetables, and ground meat, metal detection may be used in several places: after grinding, after screening, before packaging, or on final packaged product. Multi-point detection improves control but only if plants understand what each point is expected to catch. This table shows why a detector is only as strong as the program surrounding it. Calibration, challenge standards, reject confirmation, and documentation are what make the control defensible during audits and effective during real production. Visual inspection still plays a major role in foreign material control, especially for hazards that are difficult for machines to detect, such as low-density plastic, paper, wood, color changes, container defects, and setup errors. Human observation is important at receiving, pre-op, changeovers, packaging material staging, and rework handling. Yet visual programs fail when expectations are vague or when people are overloaded. Plants should define what operators are looking for, where they should look, and what they should do when they find something. A workstation where employees inspect open product for fragments should have lighting standards, line speed limits, contrast backgrounds, reject containers, and documented hold procedures. In U.S. labor markets with high turnover, relying on tribal knowledge is risky. Standard work instructions, image boards, and bilingual training often improve consistency more than adding another sign-off sheet. Human error controls also include practical design choices. Clear bins prevent accidental mixing. Shadow boards reduce missing tools. One-piece pens, detectable utensils, and controlled blade programs lower contamination risk. Packaging line checks should confirm that no loose labels, cut film tails, broken guides, or fragmented cap parts are entering product zones. For plants near logistics hubs like Memphis, Indianapolis, and Atlanta, where high-volume e-commerce and retail replenishment put pressure on speed, these simple controls can be the difference between a near miss and a market withdrawal. A good visual inspection system is measurable. Plants can track findings per shift, repeat causes, reaction time, and effectiveness by area. If one line repeatedly finds blue plastic, that should trigger deeper investigation into scraper wear, scoop condition, or packaging material handling rather than repetitive operator reminders. Many foreign material events start before ingredients ever reach the plant. Spices may contain stones, produce may carry field debris, meat trim may include bone, and dry ingredients may arrive with bag fragments, pallet splinters, or transport contamination. That is why incoming material controls are one of the most effective prevention strategies in the United States market. A plant with strong supplier management can reduce downstream inspection burden and lower customer complaint risk. Supplier controls should include approval criteria, hazard history review, specification alignment, audit or questionnaire review, and verification testing where justified. For imported ingredients entering through ports such as Los Angeles/Long Beach, Savannah, or Newark, extra attention may be needed around transit damage, repacking, and lot traceability. For domestic suppliers in produce-heavy states like California, Arizona, Washington, and Florida, seasonal shifts may change the risk profile of stems, pits, stones, or other field-related contamination. Incoming inspections should be intelligent rather than merely routine. High-risk ingredients may need sieves, magnets, destoners, or X-ray verification before use. Packaging materials should be checked for brittle plastic damage, loose staples, splintered pallets, and liner integrity. Plants should also define action thresholds: when to reject, when to hold for quality review, and when to increase monitoring frequency. Companies planning line expansions or new ingredient systems often need more than a purchasing checklist. They need material handling systems designed for cleaner transfer, screening, and storage. Through its process and manufacturing capabilities, DPS designs and integrates receiving, batching, mixing, pumping, filtration, and utility systems for food and beverage facilities across North America. This matters because well-designed ingredient handling reduces opportunities for contamination during unloading, dumping, conveyance, and rework. This table is useful because it ties each material type to a practical receiving strategy. Plants should focus resources where the contamination history and business impact are highest. Glass and brittle plastic management is one of the clearest foreign material disciplines because the rules can be documented and verified. Every plant should maintain a register of glass and brittle plastic items, identify where they are located, evaluate their proximity to exposed product, and inspect them on a defined schedule. Common examples include light covers, sight glasses, gauge faces, touch screens, windows, and instrument housings. High-performing sites use engineering controls first. They replace unnecessary glass, shield exposed fixtures, and redesign traffic or forklift patterns where breakage is likely. If the plant handles hot-fill, carbonated beverages, dairy, or acids, material selection matters because some plastics become brittle more quickly in harsh washdown or thermal environments. Facilities running older assets should pay close attention to yellowed guards, cracked indicator covers, and legacy instrument housings that can fracture under routine use. A documented breakage procedure is essential. It should define immediate stop actions, product hold zones, cleanup tools, inspection and release authority, sanitation verification, and disposal of exposed product. The goal is not only to clean up visible fragments, but to prevent questionable product from moving downstream because of production pressure. For processors undertaking plant upgrades, material choices can dramatically reduce future risk. DPS supports capital projects that include sanitary design, utility integration, equipment selection, and facility modifications; those decisions often influence whether inspection points remain accessible and whether brittle components are kept out of critical zones. Manufacturers looking at new vessels, custom CIP systems, or other process hardware can review equipment capabilities here to better align design decisions with food safety and maintainability. Maintenance activity is a frequent but underappreciated source of foreign material. Loose fasteners, weld slag, insulation fragments, gasket pieces, broken drill bits, temporary repairs, and forgotten tools can all enter product streams during line work. The risk rises during emergency repairs, contractor projects, and overnight maintenance windows where speed is prioritized over line clearance discipline. The best maintenance procedures separate food-safe execution from general mechanical work. That means pre-job review, parts accountability, protected product zones, controlled lubrication, tool shadowing, magnet sweeps where appropriate, and line clearance sign-off before restart. Temporary fixes such as tape, wire, cardboard shims, or loose wraps should be prohibited in product-contact and product-exposure zones. If a screen breaks, a blade chips, or a fastener goes missing, product disposition rules must be immediate and clear. Tool control deserves special emphasis. Shadow boards and serialized kits reduce the chance of lost tools. Breakaway knife policies, controlled blade issuance, and count reconciliation at shift end prevent a very common contamination pathway. Contractors should be held to the same standards as plant employees. This is especially important in U.S. plants executing expansions, utility upgrades, or equipment relocations while production continues in adjacent areas. DPS often supports processors in complex project environments where installation, integration, and production readiness must coexist. Its design-build-manage approach helps coordinate engineering, construction, local trades, and startup oversight so line changes do not create avoidable food safety exposure. For manufacturers planning equipment moves, utility reroutes, or capacity upgrades, disciplined project execution can be just as important as the hardware itself. This table helps plants convert general maintenance expectations into point-of-use controls. The practical detail is what prevents “we thought someone checked it” failures. Even the best detection technology will not compensate for a weak reporting culture. Employees are often the first to notice a cracked scraper, a missing bolt, a broken pallet board, unusual detector rejects, or a supplier issue. If they hesitate to report because they fear blame or production delay, the foreign material program is fragile. Training should explain not only the rules but the reasons behind them. Employees need to know what counts as foreign material, which items are especially dangerous, how to hold suspect product, when to stop the line, and who must be notified. Short, repeated training tied to real plant examples tends to work better than annual classroom sessions alone. Visual aids, multilingual instruction, and area-specific drills are especially useful in large U.S. facilities with diverse workforces. Reporting culture also depends on leadership behavior. When supervisors thank employees for raising concerns and act quickly on near misses, reporting increases. When the response is dismissive or punitive, issues stay hidden. Many successful plants track near misses, not just confirmed contamination. That gives them more data for prevention and helps shift the culture from “avoid blame” to “protect the brand and the customer.” By 2026, this area will likely become even more data-driven. Plants are adopting digital maintenance logs, smart inspections, image capture at CCPs, and mobile incident workflows that speed escalation and trend analysis. Sustainability goals are also influencing the conversation: preventing contamination reduces waste, rework, packaging loss, and recall-related disposal. Regulatory and customer scrutiny around preventive controls, traceability, and documented verification is expected to tighten, especially for high-risk and ready-to-eat categories. Disruptive Process Solutions serves food and beverage manufacturers across the United States and Canada with a practical, profit-focused engineering model. Rather than operating as a conventional contractor, the company works at the intersection of capital planning, process design, installation, integration, and execution management. That matters for foreign material control because prevention is rarely solved by one machine purchase. It often requires better line layout, more sanitary utility routing, stronger automation logic, improved receiving design, or a cleaner equipment changeover strategy. On the technology side, DPS brings process, controls, electrical, mechanical, plumbing, and structural engineering together with PLC programming and SCADA integration. That makes it well suited for projects where inspection systems must communicate with conveyors, fillers, reject devices, batching controls, or plantwide monitoring. On the manufacturing side, the company supports processing environments ranging from beverage systems and aseptic applications to protein, dairy, prepared foods, and ingredient operations, while also offering proprietary equipment such as tanks, CIP systems, tumblers, and cooking vessels. On the service side, DPS supports capital planning, feasibility work, owner’s representation, project and program management, general contracting where licensed, equipment supply, and turnkey installation and integration. For manufacturers evaluating line upgrades, new builds, or contamination-risk reduction projects, that breadth is useful because food safety controls work best when the process, equipment, building systems, and business case are aligned from the start. You can learn more about the company’s background and operating approach, explore its broader service capabilities, and review selected project examples and case stories relevant to complex manufacturing environments. A practical buying lesson for U.S. plants is this: choose partners who can challenge assumptions. If a facility needs to reduce foreign material risk, the right answer may be a detector, but it may also be an upstream screen, a redesigned transfer point, a better maintenance access platform, or revised automation sequencing. The most valuable partner is one that protects long-term operating performance, not just project spend. What foreign materials are most common in U.S. food plants?Metal, hard plastic, glass, stones, wood, rubber, bone, and packaging fragments are among the most common. The mix depends on the product category and the age and design of the facility. Is X-ray better than metal detection?Neither is universally better. X-ray detects a broader range of dense contaminants, while metal detection is highly effective for metal and often more cost-efficient. Many plants use both at different control points. How often should metal detectors be checked?Frequency should be risk-based, but many U.S. plants test at startup, during the run at defined intervals, at product changeover, and at the end of production. The key is consistent challenge testing with documented response to failures. Can visual inspection replace automated detection?No. Visual inspection is valuable, but it should support, not replace, validated machine detection where the hazard profile justifies technology. Human inspection is strongest when tasks are limited, clear, and measurable. What is the first step in improving supplier control?Start by ranking ingredients and packaging by contamination risk, complaint history, and business impact. Then tighten specifications, receiving checks, and verification for the highest-risk materials first. Why are glass and brittle plastic registers important?They create visibility. Without a register, plants often miss hidden risk points such as gauge covers, sight glasses, and indicator housings. A register supports routine inspections and a more effective breakage response. How do maintenance teams reduce contamination risk?Use controlled parts trays, shadow boards, line-clearance checks, approved materials, and documented restart inspections. Emergency repairs should follow the same discipline as scheduled work. What industries need the strictest foreign material controls?Ready-to-eat foods, dairy, beverages, infant-related products, aseptic foods, protein processing, and contract manufacturing usually require especially strong controls because of consumer exposure and customer expectations. What U.S. market trends should plants watch through 2026?Expect more investment in data-linked inspection systems, stronger traceability expectations, wider use of automation and image capture, more emphasis on sustainability through waste reduction, and tighter customer requirements around preventive control verification. When should a plant bring in an engineering partner?Bring one in when contamination risk is linked to layout, line speed, utility routing, sanitation access, equipment wear, or expansion planning. A technical partner can often solve the root cause upstream instead of adding reactive inspection only at the end. -
2026 Guide to Food Facility Zone Segregation and Color Coding
Food manufacturers in the United States are under constant pressure to prevent cross-contamination, protect product integrity, and satisfy FDA, USDA, SQF, and BRC expectations. A strong zone segregation and color-coded equipment program helps facilities separate risk, assign sanitation responsibility, control personnel movement, and reduce environmental pathogens before they reach finished product. In 2026, the most effective programs combine clear hygienic zoning, practical tool separation, disciplined traffic design, environmental monitoring, and engineering choices that make cleaning easier every day. The fastest way to improve hygienic control in a U.S. food plant is to divide the facility into four risk zones, assign cleaning tools by color to each zone, restrict employee and forklift movement between zones, and verify the system with environmental monitoring. Zone 1 covers direct food contact surfaces and requires the strictest controls. Zone 2 includes nearby non-contact surfaces that can still transfer contamination. Zone 3 covers remote production support areas, and Zone 4 addresses exterior and perimeter risks. When these zones are mapped correctly, supported by written SOPs, and tied to sanitation validation, manufacturers in places like Chicago, Dallas, Fresno, Charlotte, and the New Jersey logistics corridor can reduce both microbial risk and downtime. For buyers, the best program is not just a set of brushes and floor signs. It is an operational system that includes layout planning, drain strategy, utility routing, washdown design, personnel flow, traffic barriers, storage racks, ATP or microbiological verification, and training. This is why many processors now align hygienic zoning decisions with capital planning and plant engineering rather than treating sanitation segregation as a stand-alone purchase. This table shows why zone control is multidisciplinary. A sanitation team may own tools, but engineering, QA, operations, and facilities all influence whether the program works in practice. Zone 1 includes any surface that directly touches food, beverage, ingredients, or product-contact packaging. Examples include conveyors, slicers, fillers, depositors, kettles, blend tanks, tote contact points, nozzles, chutes, augers, and utensils. In ready-to-eat protein, dairy, aseptic beverage, and prepared foods plants, Zone 1 is the highest-risk environment and deserves the most conservative control strategy. In the United States, buyers often focus on sanitizer chemistry first, but that is only one part of Zone 1 control. The bigger picture is hygienic design. Product contact surfaces should be smooth, accessible, drainable, corrosion-resistant, and free from niches. Welds, seals, dead legs, hollow framework, poorly pitched piping, and hard-to-open machine guards create cleaning obstacles that can undermine even the best chemical program. For that reason, many processors now evaluate capital upgrades through a hygienic design lens before new lines are installed. During equipment planning, it helps to work with firms that understand both process performance and cleanability. DPS applies this approach through integrated process engineering and system design for food and beverage plants across North America, with experience spanning high-care food lines, beverage processing, aseptic systems, utilities, controls, and compliance-driven projects. Companies considering broader process upgrades can review engineering and project services that align sanitation performance with production needs. Zone 1 also requires the most disciplined verification. Facilities should define acceptable ATP thresholds, microbiological pass criteria, pre-operational inspection standards, and escalation rules when results fail. In a USDA-inspected protein plant in the Midwest, for example, a failed Zone 1 swab on a slicer leg may trigger expanded sampling, recleaning, root cause review, and intensified checks on adjacent conveyor transfer points. The practical buying advice for Zone 1 is simple: do not purchase equipment solely on throughput or price. Ask how long it takes to open, inspect, clean, validate, and restart. The true cost of ownership in Los Angeles, Atlanta, Minneapolis, or Houston depends as much on sanitation labor and contamination exposure as on nameplate speed. Zone 2 includes non-food-contact surfaces that sit close enough to product or Zone 1 equipment to create a realistic transfer risk. Common examples include machine frames, control panels, guards, conveyor undersides, drip shields, filler housings, catwalk rails, and support structures near open product. Zone 2 is where many contamination problems begin because the surfaces appear less critical, yet they are close enough to spread splash, condensation, dust, or harborage contamination into Zone 1. Environmental monitoring programs in U.S. ready-to-eat facilities often emphasize Zone 2 as an early warning layer. If an organism appears repeatedly on a framework cross-member beneath a conveyor or on a panel handle beside a filler, the plant has a chance to intervene before product contact surfaces become involved. That is why sanitation schedules should not treat Zone 2 as an afterthought. It needs documented access methods, cleaning chemistry compatibility, dry-vs-wet cleaning rules, and post-clean inspection standards. Zone 2 control is especially important in product categories such as sliced proteins, cultured dairy, aseptic support rooms, salad toppings, sauces, and low-acid beverages after a kill step. These products often move through open handling environments where nearby contamination can migrate through overspray, employee touchpoints, or difficult-to-clean components. Facilities expanding or retrofitting legacy plants in older industrial corridors such as Philadelphia, St. Louis, Milwaukee, or the Inland Empire should assess whether machine spacing, utility drops, and structural members make proper Zone 2 cleaning difficult. Smart engineering can reduce hidden ledges and congestion points. This table highlights the operational difference between Zone 1 and Zone 2. Zone 1 failure can be immediate product risk, while Zone 2 often acts as the leading indicator. Strong plants use Zone 2 data to prevent future events rather than waiting for a crisis. Zone 3 covers areas within the processing environment but farther from direct product exposure. Examples include floors, drains, forklifts, pallet staging zones, walls, maintenance carts, room perimeters, wheels, hose stations, wash sinks, refrigeration units, and utility corridors. These are not product-contact surfaces, but they can seed contamination into higher-risk spaces if left unmanaged. For environmental monitoring, Zone 3 often provides the richest trend data. Floors and drains, especially in wet protein or dairy operations, can serve as reservoirs for organisms that later travel through aerosols, footwear, wheels, hoses, and poor cleaning practices. In beverage processing, syrup rooms, blending spaces, and utility interfaces may show yeast, mold, or spoilage pressure long before packaged product quality is affected. A robust monitoring protocol should define sample sites by risk, season, moisture profile, and traffic pattern. Gulf Coast plants may face different moisture and pest pressures than facilities in Arizona or Colorado. Plants near major agricultural and logistics hubs like Fresno, Salinas, Omaha, Savannah, and Kansas City may also experience unique raw material and inbound vehicle contamination patterns. Trend review matters as much as single-point testing. One isolated floor drain finding may be manageable. Repeated positives across related drains, hose reels, and forklift wheels suggest a route of spread that calls for CAPA, not just recleaning. Many sophisticated processors now pair Zone 3 data with maintenance work orders, drain maps, and traffic logs to identify root causes faster. As a buying strategy, plants should choose monitoring programs that connect sanitation, maintenance, and operations data. If software is too complex for supervisors to use, results will sit in spreadsheets instead of driving action. Zone 4 covers the outer boundary of the food plant and surrounding property. This includes loading docks, roof interfaces, waste handling areas, exterior walls, employee entrances, trailer yards, utility pads, compressed air intakes, parking lots, and landscape edges. Zone 4 is where outside contamination enters the site through vehicles, weather, pests, dust, and standing water. In the United States, perimeter control varies by geography. Plants near ports such as Long Beach, Savannah, Newark, or Houston may face heavier trailer turnover and imported material exposure. Facilities in humid Southeast climates may need stronger standing-water and insect control. Dry inland plants may struggle more with wind-blown dust around dock doors and air intakes. Zone 4 is also where many facilities underinvest because contamination is not immediately visible on product. Yet exterior pressure often drives interior problems. Poor dock seals, cracked pavement, open waste handling, clogged roof drains, and unmanaged vegetation can all increase pest activity or moisture intrusion. This table explains why exterior programs belong in hygienic zoning discussions. A perimeter weakness eventually becomes an interior issue, especially when high trailer turnover, wet weather, or warm temperatures increase vector activity. A color-coded tool program is the visible backbone of zone segregation. Brushes, squeegees, shovels, buckets, hoses, scrapers, floor pads, aprons, gloves, and mobile carts should be assigned to risk zones so that tools never move casually from raw to ready-to-eat or from drains to food-contact areas. The most effective color systems are simple, durable, and tied to physical storage locations. Many U.S. plants use a four-color model that aligns to zones, but the best system is the one that your workforce can understand instantly across shifts and languages. If a site in North Carolina uses red for raw and blue for ready-to-eat, that rule should appear on tool boards, SOPs, training cards, and sanitation records. Plants with allergen segregation may add another color layer for ingredient classes or line dedication. When sourcing tools, buyers should evaluate chemical resistance, bristle retention, hygienic design, ease of inspection, heat tolerance, and replacement cost. Low-cost tools that crack, shed, or trap residue create hidden risk. Storage matters too. Tools should hang dry, off the floor, in the correct room, and near the point of use. Centralized storage can work in smaller facilities, but large plants generally perform better with distributed, zone-specific racks. For processors also planning equipment upgrades, there is value in aligning sanitation tools with process equipment selection. DPS supports this kind of systems-level planning through process integration and its own equipment capabilities, including custom tanks, CIP systems, marination tumblers, and cooking vessels designed to fit broader plant execution goals. Manufacturers evaluating line changes can also explore available process equipment solutions as part of larger hygienic improvement projects. By 2026, the trend is moving beyond simple color matching. The leading plants pair color-coded tools with QR-tagged inventories, wash verification, replacement logs, and sanitation ownership by room. Sustainability is also shaping purchases, with stronger demand for longer-life materials and reduced disposable waste. Even the best color-coded system fails when people, pallets, and maintenance activity move freely across hygienic boundaries. Traffic patterns and personnel flow controls are therefore essential. The goal is to design the plant so clean-to-dirty and post-lethality-to-raw crossover is minimized by default, not merely discouraged by policy. Practical controls include separate entry points, gowning transitions, footwear changes, foam or sanitizer barriers, handwashing stations, wheel wash points, one-way corridors, dedicated forklifts, visual floor markings, and scheduling rules for maintenance and waste removal. In high-care environments, facilities may use controlled air pressure cascades, interlocked doors, and badge-limited access. Traffic control decisions should be made during plant design and renovation, not after equipment is already squeezed into place. This is where service capability matters. DPS works as an engineering and execution partner that bridges planning, buildout, and implementation, helping processors think through process flow, utility coordination, capital feasibility, installation, controls, and project management as one system. Companies exploring project support can learn more about the team and operating approach behind that model. Industries with the strongest need for strict flow control include ready-to-eat meat, dairy, fermented beverages, aseptic filling, fresh prepared foods, and co-packing facilities with multiple SKUs and rapid changeovers. Applications range from raw receiving and thaw rooms to post-cook slicing, blending, canning, filling, and secondary packaging. Buying advice: before approving a traffic-control investment, observe the facility during sanitation, startup, changeover, and shift turnover. These are the moments when policy is most likely to break down. A beautiful flow map that ignores real forklift congestion near docks or maintenance response patterns will not hold up in production. Vectors are the routes by which contamination travels. In food plants, the most common vectors are employees, gloves, tools, hoses, wheels, drains, condensate, overspray, pallets, maintenance equipment, incoming packaging, and pests. Cross-contamination prevention depends on identifying which vectors are realistic for each zone and interrupting them with physical and procedural controls. Vector mapping is especially useful after repeated environmental positives or unexplained spoilage trends. For example, a dairy plant may discover that mobile ladders move between wet utility rooms and open filling areas. A beverage site may find that hose nozzles touch floors during sanitation and then contact external machine surfaces near open containers. A protein processor may see recurring spread from pallet jack wheels crossing raw and cooked support corridors. Strong vector control programs combine engineering, sanitation, and discipline. Condensation management, drain placement, pallet policy, tool assignment, traffic barriers, and preventive maintenance all reduce transfer pathways. Pest control also belongs here; birds near receiving can lead to dock contamination, and rodent pressure around waste handling can increase transfer risk through wheels and personnel shoes. For local supplier evaluation, U.S. buyers should compare providers on more than product catalog size. Ask whether they support site assessments, hygienic design input, validation guidance, replacement planning, and staff training. Regional support matters in high-volume manufacturing areas such as the Carolinas, California Central Valley, Texas, Wisconsin, Arkansas, and the Midwest protein belt. In 2026, future trends include smarter sensors for environmental conditions, digital route tracking for sanitation tools, more pressure from audit schemes on documented zoning logic, and stronger sustainability requirements tied to water, chemical, and material use. Policy expectations are also increasing around preventive controls, validation, and documented risk assessment, especially for high-risk products. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a practical, profit-focused engineering mindset. Rather than approaching sanitation zoning as an isolated compliance project, the company helps clients connect hygienic design, production goals, utility systems, automation, and capital efficiency. From a technological standpoint, DPS brings multidisciplinary engineering across process, mechanical, structural, plumbing, electrical, and controls. That includes PLC programming, SCADA, batch logic, utility integration, and line coordination for beverage, dairy, protein, prepared foods, aseptic processing, and other regulated applications. This matters when a zoning improvement also affects CIP strategy, equipment access, drain routing, air handling, or automation sequencing. From a manufacturing standpoint, DPS designs and supplies selected process equipment such as tanks, CIP skids, marination tumblers, and cooking vessels that can be integrated into broader facility upgrades. That helps processors align equipment procurement with sanitation, cleanability, and installation realities rather than sourcing each item in isolation. From a service standpoint, DPS provides planning, feasibility support, owner representation, project management, general contracting coordination, installation, and system integration. For processors evaluating expansion, relocation, or modernization, that full-scope model can reduce the gaps that often appear between engineering intent and plant-floor execution. Additional examples of project outcomes are available in these food and beverage case studies. The company is headquartered in Cary, North Carolina, with a West Coast office in Lake Forest, California, and supports clients across all 50 states. That national footprint is useful for manufacturers operating multiple plants or planning standardized hygienic zoning programs across geographically different facilities. 1. What is the difference between Zone 1 and Zone 2?Zone 1 touches food directly. Zone 2 does not touch food but sits close enough to spread contamination into Zone 1 through splash, touch, condensation, or debris. 2. How many colors should a food plant use?Use only as many colors as employees can apply consistently. Four is common, but some plants add colors for allergen control or dedicated production lines. 3. Do all U.S. food plants need formal zoning maps?Not every site needs the same complexity, but most modern facilities benefit from a documented zone map tied to cleaning, monitoring, and traffic rules. 4. What products need the strictest segregation?Ready-to-eat meats, dairy, aseptic beverages, fresh prepared foods, sauces after lethality, and any open product exposed after a kill step usually require the strongest controls. 5. How often should environmental monitoring be reviewed?High-risk sites often review results weekly, with monthly trend analysis and immediate escalation for repeat findings in the same route or vector path. 6. Can old plants still build strong zone control?Yes. Legacy facilities can improve with better traffic separation, color-coded tools, drain strategy, equipment access upgrades, and focused monitoring, even before full renovation. 7. What should buyers ask sanitation tool suppliers?Ask about material durability, cleanability, chemical compatibility, replacement cycles, storage systems, training support, and whether they understand hygienic zoning by product risk. 8. How does zoning affect ROI?Good zoning reduces contamination events, downtime, product loss, audit findings, and emergency cleaning. It also supports longer-term equipment reliability and faster troubleshooting. 9. What is the biggest 2026 trend?The biggest shift is from basic visual segregation to integrated programs that combine hygienic design, digital verification, monitoring data, personnel control, and sustainability planning. 10. When should a company bring in an engineering partner?Bring one in during early planning for expansions, equipment changes, high-risk product introductions, repeated environmental issues, or when plant layout is limiting sanitation performance. Across the United States, food facility zone segregation and color coding are no longer optional best practices for sophisticated manufacturers. They are operating disciplines that protect product, customers, brand reputation, and capital performance. The strongest programs treat zoning as part of plant design, not just sanitation training. When Zone 1 through Zone 4 are clearly defined, tools are controlled, traffic is managed, vectors are interrupted, and monitoring confirms results, facilities are better positioned for safer growth in 2026 and beyond. -
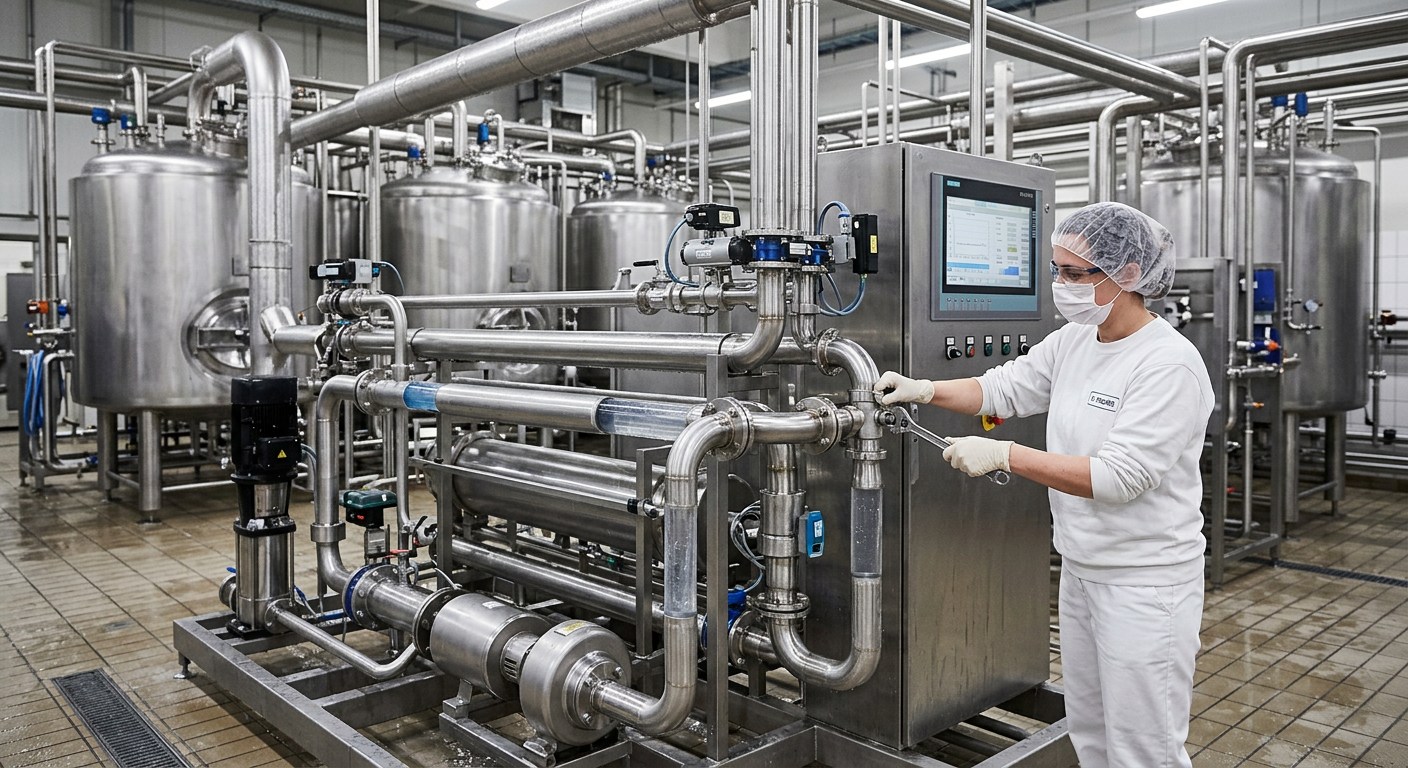
Food Plant Personnel Hygiene Programs: Complete 2026 Checklist
Personnel hygiene is one of the most important control points in any food or beverage facility in the United States. Whether a plant handles ready-to-eat meals in Chicago, poultry in Arkansas, dairy in Wisconsin, sauces in New Jersey, or aseptic beverages near Los Angeles and Houston, employee hygiene programs directly affect food safety, audit performance, labor efficiency, and brand protection. In 2026, food manufacturers are expected to tighten hygiene controls not only to meet FDA, USDA, SQF, and BRC expectations, but also to reduce operational variability, support workforce turnover, and document compliance more effectively. This guide explains how to build and maintain a practical personnel hygiene program for U.S. food plants. It covers exclusion policies, hand washing station design, protective clothing, glove protocols, training, visitor management, and documentation. It also looks at industry demand, product categories, buying advice, applications, local supplier considerations, and upcoming technology and policy trends shaping the American market. A strong food plant personnel hygiene program in the United States should do five things well: prevent sick or contaminated personnel from entering production areas, make correct hand washing easy, standardize protective clothing by risk zone, define glove changeover rules, and verify compliance through training and records. Plants that do this consistently are better positioned for FDA inspections, USDA oversight, customer audits, and GFSI-benchmarked certification reviews. For most facilities, the most effective hygiene program is not the one with the longest policy manual. It is the one that operators can actually follow on first shift, second shift, weekends, and during peak season staffing. That means clear visual controls, good entry design, practical gowning layouts, line-of-sight supervision, digital documentation when possible, and reinforcement during onboarding. In the U.S. market, hygiene programs are increasingly tied to automation and facility design. Modern plants in manufacturing corridors such as North Carolina’s Research Triangle, Texas food logistics hubs, California beverage clusters, and Midwest protein processing regions are investing in better hand wash infrastructure, access control, sanitation zoning, and audit-ready data capture. The 2026 trend is clear: hygiene is moving from a policy topic to an engineered system. For buyers planning a plant expansion or retrofit, personnel hygiene should be addressed at the same time as process flow, utilities, CIP routing, HVAC pressure relationships, and material movement. Retrofitting hand washing points after construction is often more expensive than integrating them during layout development. The chart above reflects a realistic growth pattern in U.S. spending on hygiene-related plant systems, including hand wash access equipment, gowning controls, digital monitoring, training tools, and software. Growth is being driven by labor turnover, retailer expectations, audit readiness, and the need to reduce contamination events in higher-risk categories. Health screening and exclusion policies are the first line of defense in a personnel hygiene program. U.S. food plants should maintain written rules that explain when employees, contractors, and temporary workers must report symptoms, when they are restricted from handling food or food-contact surfaces, and when they are excluded from production areas entirely. At a minimum, screening should address vomiting, diarrhea, fever with sore throat, jaundice, infected wounds on exposed body parts, and diagnosed communicable illnesses relevant to food handling. Policies should also account for respiratory illness procedures where facilities choose to adopt enhanced controls, especially in ready-to-eat environments. These policies matter across product categories, but especially in high-risk applications such as deli salads, dairy processing, post-lethality protein slicing, aseptic packaging, cultured beverages, and prepared foods. A bakery with a fully wrapped product may manage some exposures differently than a ready-to-eat meat operation under USDA scrutiny, but both still need clear decision trees. The table shows the practical difference between restriction and exclusion. Restriction usually means the person may perform non-food-contact duties. Exclusion means they should not enter production, packaging, or ingredient handling areas at all. Plants should define this clearly because confusion at the supervisory level is a common audit finding. For multi-site operators with plants near Savannah, Kansas City, Fresno, or Philadelphia, consistency matters. A centralized policy should be adapted for site risk but not rewritten so heavily that one facility tolerates what another excludes. Temporary labor providers should be contractually required to support the same reporting expectations. Hand washing only works when stations are correctly located, properly supplied, and engineered for flow. In many U.S. plants, compliance problems are caused less by employee resistance and more by poor layout. If staff must detour around forklift traffic, wait in a bottleneck near a gowning room, or reach a sink that is not visible from entry control, hand washing quality drops. Best practice is to place stations at every production entry point, near high-risk transitions, restrooms, rework areas, allergen handling zones, and maintenance access points where employees can re-enter processing spaces. In a large beverage or food campus, hygiene access should be matched to traffic patterns from locker rooms, breakrooms, warehouse interfaces, and maintenance corridors. In retrofit projects, station design should be coordinated with plumbing, floor drainage, splash control, chemical dispensing, sensor activation, and sometimes turnstile release systems. This is one reason many processors involve engineering partners early in a capital plan rather than treating hand wash points as minor fixtures. This table highlights a key point: compliance is strongly influenced by design. When managers ask why hand washing scores are inconsistent, the answer is often found in utility access, ergonomics, and traffic flow rather than in discipline alone. Facilities handling seafood near Gulf Coast ports, meat processing in Omaha, or beverage filling near the Port of Long Beach may each have different layouts, but all benefit from the same principle: the hand wash station must be the natural path of entry, not an optional stop. Protective clothing requirements should be matched to product risk, area classification, and employee task. A low-care dry storage room does not need the same controls as an exposed ready-to-eat slicing room. The goal is not to overburden every employee, but to assign the right garments to the right zone and make changeover easy enough to sustain. Typical garments include smocks, frocks, aprons, beard covers, hairnets, sleeve covers, frosted safety glasses where needed, cut-resistant gloves under outer gloves, dedicated footwear, and color-coded uniforms for departments such as raw, cooked, allergen, sanitation, maintenance, and quality assurance. In high-risk environments, plants may also require segregated boot wash and gowning transitions. Color coding becomes especially useful in larger plants where contractors, sanitation crews, forklift operators, and line personnel move through overlapping spaces. It reduces visual confusion and helps supervisors identify out-of-zone movement quickly. The table shows why a one-uniform-fits-all policy usually fails. Zone-specific clothing improves contamination control and can also simplify training. Employees understand expectations faster when garments visually reinforce area boundaries. For buyers selecting uniforms or gowning systems, look for durability, ease of laundering, replacement lead time, compatibility with metal detection or X-ray requirements where relevant, and support for local service routes. Plants in remote regions may need backup garment inventory if their laundry provider is not nearby. Gloves are useful, but they are not a substitute for hand washing. In many audits, overreliance on gloves actually hides poor hygiene practice. U.S. food plants should treat gloves as a controlled barrier that must be donned correctly, changed at defined events, and matched to product risk and task. Single-use gloves are common in ready-to-eat and packaging tasks, while heavier reusable gloves may be used for sanitation, deboning, thermal operations, or chemical handling. Some operations also use cut-resistant inner gloves beneath disposable outer gloves. Each combination needs a written cleaning and replacement rule. The explanation here is straightforward: gloves need event-based and time-based controls. Event-based changes cover obvious contamination points. Time-based changes are valuable on repetitive tasks where wear, perspiration, and unnoticed contamination can accumulate. Glove buying advice should include material compatibility, dexterity, puncture resistance, food-contact suitability, allergen concerns such as latex avoidance, and procurement resilience. Plants around major freight routes such as Memphis, Dallas-Fort Worth, and the New York-New Jersey distribution corridor increasingly prefer approved secondary suppliers to avoid disruptions. This bar chart reflects how hygiene program intensity varies by sector. Ready-to-eat foods and protein processing tend to show the highest demand because employee contact, product exposure, and contamination consequences are more severe. Beverage plants range from moderate to high depending on whether they run aseptic, dairy-based, fermented, or hot-fill applications. Training is where many hygiene programs either become real or remain theoretical. Every employee should receive hygiene training at onboarding, but effective plants go further by validating understanding, repeating key points by department, and using observations to confirm behavior on the floor. Core training topics should include illness reporting, hand washing sequence, glove use, uniform rules, jewelry and personal item restrictions, traffic flow between zones, allergen movement, breakroom re-entry, reporting damaged PPE, and response to contamination events. Supervisors should receive extra instruction on when to restrict, reassign, or escalate a hygiene issue. Competency checks are especially important for temporary workers, multilingual teams, seasonal hires, and roles with high turnover. In practical terms, that means short quizzes, observed demonstrations, sign-off records, and coaching tied to real tasks. Plants that rely only on slide decks without floor verification often struggle during customer audits. In 2026, training is shifting toward blended models: classroom basics, multilingual video prompts at access points, QR-linked refresher content, and digital observation forms. This is particularly useful in large facilities in Atlanta, Phoenix, Indianapolis, and Charlotte where labor pools are diverse and staffing ramps can happen quickly. The area chart shows a realistic shift in the U.S. market from paper-based hygiene monitoring to digital verification. The change is not only about convenience. Digital systems improve trend review, training follow-up, corrective action closure, and audit retrieval speed. Competency assessment should be retained as part of the training record. A signed attendance sheet alone is weak evidence. A stronger record shows the topic covered, the employee’s department, the trainer, the date, the evaluation method, and any remedial coaching performed after observation. Visitors, vendors, auditors, executives, maintenance contractors, and temporary workers all create unique hygiene risks because they may not be familiar with plant-specific movement rules. A good policy separates low-risk office visits from production access and applies the same hygiene expectations to everyone entering controlled areas. Visitors should complete a sign-in process, basic health declaration, PPE issue, and escorted route. In high-care spaces, facilities may limit access only to essential visits. Photography, loose personal items, and jewelry should also be controlled where they pose contamination or confidentiality concerns. Temporary workers need more than a badge and a quick orientation. They should receive the same hygiene instruction as regular employees, adapted to literacy level and language. Staffing agencies should be aligned on illness reporting, attendance expectations, and disciplinary escalation. This is especially relevant in large seasonal markets such as California produce, Midwest frozen foods, Gulf Coast seafood, and holiday-related bakery or confectionery plants. During labor surges, the weakest point in hygiene control is often compressed onboarding. Useful controls include colored visitor helmets or frocks, restricted zone maps, escort logs, pre-entry checklists, contractor tool sanitation protocols, and a defined process for collecting PPE at exit. Temporary workers should be traceable by line assignment and shift in case an incident review is needed later. Monitoring converts policy into evidence. U.S. plants need enough documentation to show that hygiene expectations are defined, communicated, observed, corrected, and reviewed. At the same time, records should not be so burdensome that supervisors spend more time checking boxes than managing behavior. The best monitoring systems focus on a few high-value checks: pre-op readiness of hygiene stations, PPE availability, entry compliance, hand wash and glove observations, illness reporting documentation, visitor entry records, and corrective actions for repeated misses. Plants can then trend recurring issues by department, shift, or access point. This table illustrates how each record answers a different audit question. Together, they show the plant did not merely write a policy; it implemented and maintained it. If a facility is still heavily paper-based, start by digitizing the records that are hardest to retrieve under pressure, such as visitor logs, training sign-offs, and corrective actions. Plants in highly regulated or customer-audited sectors often combine QA review, operations ownership, and HR support. That cross-functional structure works well because hygiene is not solely a quality issue. It also affects labor management, maintenance access, and production continuity. The comparison chart shows why many larger manufacturers are moving toward integrated hygiene systems rather than isolated products. A basic program may satisfy minimum needs, but an engineered approach usually delivers better audit readiness and smoother labor flow over time. The U.S. market for personnel hygiene products and systems is broad. Buyers may source sinks, turnstiles, boot washers, locker room equipment, disposable PPE, reusable garments, glove dispensers, digital training software, access control hardware, and sanitation-zone signage from separate vendors or through integrated partners. The right approach depends on plant size, category risk, and project complexity. Different industries prioritize different products: Local supply conditions also matter. Plants near major ports such as Long Beach, Savannah, Houston, and Newark may have broader import access for disposable PPE, while inland facilities may prioritize domestic stock reliability. During procurement, ask suppliers about lead times, alternate SKUs, emergency replacements, and regional service support. When comparing local suppliers, buyers should evaluate more than unit cost. Useful criteria include installation support, sanitation-friendly design, spare parts availability, documentation, compatibility with USDA or FDA expectations, and whether the vendor understands food traffic flow rather than only selling generic industrial fixtures. The lesson from this table is that product selection should follow process risk and labor flow. A cheap solution that slows entry or creates confusion often costs more over time through labor loss, workarounds, or nonconformance findings. Several trends are shaping hygiene program decisions in the U.S. food and beverage sector for 2026 and beyond. First, facilities are adopting more digital verification. This includes sensor-linked dispensers, access systems that prompt hand wash sequences, mobile observation tools, and dashboards that show repeat deviations by area. These tools are not replacing supervisors, but they are giving managers better visibility. Second, policy expectations are becoming more risk-based and more documented. Manufacturers increasingly align personnel hygiene with broader preventive controls, environmental monitoring, allergen management, and food defense plans. In practical terms, hygiene no longer sits as a separate SOP binder; it is tied into site-wide compliance systems. Third, sustainability is becoming part of hygiene decisions. Plants are asking whether towel use, garment laundering, water consumption, and disposable PPE can be optimized without compromising food safety. Sensor faucets, efficient wash cycles, durable reusable garments where appropriate, and smarter replenishment systems are becoming more common. Fourth, workforce realities are pushing for simpler, more visual systems. Labor shortages, high turnover, and multilingual staffing are all encouraging better icon-based signage, clearer gowning sequences, and more intuitive plant entry design. Finally, capital project teams are treating personnel hygiene as a built environment issue. That means integrating hygiene controls into early-stage planning with process equipment, drains, utility routing, HVAC, and automation, rather than trying to add them after a layout is fixed. For manufacturers planning new construction, expansion, relocation, or complex retrofit work, hygiene performance often depends on whether facility design and execution are aligned from the start. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a practical, project-driven approach focused on long-term profitability rather than short-term patchwork. From a technological capability standpoint, DPS works across structural, mechanical, plumbing, electrical, process, and controls engineering. That matters for personnel hygiene because hand washing systems, boot sanitation, gowning transitions, utilities, drains, access points, and automation cannot be solved in isolation. In plants producing carbonated beverages, dairy-based drinks, sauces, proteins, aseptic products, or prepared foods, coordinated engineering helps ensure hygiene controls fit the production reality rather than disrupt it. From a manufacturing capability standpoint, DPS also supports equipment-related execution for complete processing environments and offers its own process equipment line, including tanks, CIP systems, tumblers, and cooking vessels. In practice, that gives clients a partner who understands how personnel movement, sanitation access, processing equipment placement, and utility integration affect food safety and labor efficiency at the same time. Companies exploring new system layouts can review relevant processing equipment capabilities when considering how hygienic design and production throughput intersect. From a service capability standpoint, DPS provides process engineering, capital planning, owner’s representation, project and program management, general contracting functions where applicable, installation, and integration through its design-build-manage model. For food plants trying to improve hygiene access during an expansion or major retrofit, this kind of end-to-end support can reduce the disconnect between concept design and field execution. Manufacturers considering broader plant improvements can explore available engineering and project services or review selected project case examples to understand how integrated execution supports compliance and operations together. In short, the company’s value in this context is not limited to supplying a single hygiene product. It lies in helping manufacturers build production systems where personnel hygiene, utilities, process flow, and business goals work together. The most common weakness is inconsistency between written policy and floor execution. Plants may have strong SOPs, but poor sink placement, weak onboarding, unclear glove change rules, or inconsistent supervision undermines compliance. No. Gloves should be used where risk assessment and product exposure justify them. They are not a replacement for hand washing, and unnecessary glove use can create waste and false confidence. At minimum, during onboarding and at defined refresher intervals. Additional retraining should happen after deviations, role changes, policy updates, or repeated observation failures. High-turnover operations often benefit from short monthly refreshers. Yes. Temporary labor should follow the same health reporting, PPE, hand washing, and traffic control rules as direct employees. Their onboarding may be simplified, but expectations should not be lower. Training and competency records, visitor logs, health reporting documentation, hygiene station checks, and corrective action records are usually the most valuable because they show active implementation rather than passive policy ownership. Start with the highest-risk gaps: production entry control, hand washing access, clothing zoning, glove rules, and training verification. After that, digitize the records or observations that consume the most time and are hardest to retrieve. It depends on the product and process. A shelf-stable hot-fill line differs from an aseptic dairy beverage or kombucha facility. Product exposure, post-process handling, and regulatory expectations determine the needed rigor. Expect wider use of digital verification, more risk-based documentation, stronger integration between hygiene and plant design, and more attention to sustainability in water use, garment programs, and disposable consumables. A well-run personnel hygiene program protects product, supports audits, improves labor discipline, and reduces avoidable risk. In the U.S. food and beverage market, the most effective programs in 2026 will be the ones that combine policy, training, facility design, and practical execution into one system. -
Beverage Plant Expansion Services
Expanding a beverage plant is rarely just a matter of adding another filler or buying a larger tank. In the United States, successful beverage capacity growth depends on utility depth, product-specific processing needs, line balancing, regulatory planning, and the ability to execute construction without interrupting revenue-critical production. Whether a manufacturer is increasing output for carbonated soft drinks, ready-to-drink beverages, beer, kombucha, spirits, juice, dairy-based drinks, or aseptic products, the expansion strategy must connect processing, packaging, utilities, warehousing, cold chain, and sanitation into one business case. For many operators in markets such as Dallas-Fort Worth, Chicago, Atlanta, Charlotte, Los Angeles, and New Jersey logistics corridors, the biggest mistake is focusing too narrowly on the visible equipment. The real constraints usually sit upstream or downstream: pure water generation, syrup room throughput, carbonation stability, CIP recovery, compressed air, glycol, warehouse dwell time, dock turn rate, or pallet flow at peak season. A profitable expansion plan starts by identifying the true bottleneck and then sequencing capital so that each phase supports the next. This page explains how beverage manufacturers in the United States can evaluate expansion projects with a practical lens: what to upgrade first, how to design around seasonal swings, how to compare suppliers, how to estimate payback, and how to manage compliance from concept through startup. If you need a fast answer, the best beverage plant expansion projects in the United States follow five rules. First, confirm the actual bottleneck before buying equipment. Second, size utilities such as water treatment, CIP, compressed air, cooling, and electrical infrastructure for the next phase, not just today’s need. Third, separate processing expansion from packaging integration in a phased sequence so production can continue. Fourth, design with FDA, HACCP, and when applicable CFIA export requirements in mind from the beginning. Fifth, calculate return on investment using throughput, labor, scrap, changeover time, energy, and warehousing effects rather than only equipment cost. That is the approach used by Disruptive Process Solutions, a North American food and beverage engineering firm that works as a business-focused project partner rather than a conventional installer. Its team supports owners that need engineering, construction coordination, utility integration, equipment supply, and execution management aligned to profitability. The table above works as an executive filter. If a project team cannot answer these six questions clearly, the expansion plan is usually not mature enough for procurement. Beverage manufacturing is not one market. A brewery, a juice processor, an RTD co-packer, a kombucha producer, and a carbonated soft drink bottler all use different sanitation cycles, hold times, ingredient handling methods, and thermal or non-thermal processing requirements. That is why plant expansion services for beverages must start with the product mix. For still beverages, pure water consistency, blending accuracy, ingredient dosing, and microbiological control are usually the first design priorities. For carbonated drinks, carbonation efficiency, CO2 supply stability, low-temperature process control, and bright tank or buffer capacity move up the list. For dairy beverages and high-protein functional drinks, hygienic design, allergen separation, and more demanding cleaning validation become central. For aseptic operations, expansion decisions must protect environmental separation and validated sterilization pathways. For beer, wine, spirits, and fermented drinks, fermentation capacity, cellar logistics, filtration, and packaging synchronization are often more important than nameplate filler speed alone. Manufacturers near major distribution hubs such as the Port of Savannah, the Port of Houston, the Inland Empire, or the I-95 corridor often experience a second layer of complexity: they need flexible infrastructure that can handle both local retail demand and multi-state shipment patterns. This means utility redundancy, more robust staging space, and stronger dock planning than a small single-region operator may need. The main lesson is that expansion should be beverage-specific, not copied from another facility. A plant that handles acidic juices will not have the same hygienic risks, storage constraints, or utility loading pattern as a dairy beverage plant. A carbonated line may appear simple on paper but become unstable if water temperature, deaeration, or CO2 pressure swings during production. In practice, this is where technical breadth matters. DPS supports processing and utility design across brewing, spirits, wine, kombucha, RTD, carbonated and non-carbonated soft drinks, juice, dairy beverages, and aseptic applications. That range is important because expansion teams often need cross-category knowledge when a facility is adding new product platforms rather than only increasing existing volume. The line chart shows why expansion planning remains active heading into 2026. Investment is being driven by SKU proliferation, premiumization, contract manufacturing, automation, and regionalization of supply chains in the United States. Water is the foundation of most beverage facilities, yet it is one of the most underestimated parts of expansion planning. Moving from 100 gallons per minute to 350 gallons per minute and beyond is not just a larger skid purchase. It usually requires a fresh review of incoming municipal capacity, pretreatment, reverse osmosis staging, storage, sanitization, pump redundancy, distribution loop design, reject handling, and instrumentation. In cities with variable source water conditions such as Phoenix, Houston, or parts of California, seasonal changes in incoming conductivity, hardness, and chlorine levels can affect the sizing and operating strategy of an upgraded pure water system. If the plant also supplies humidification, ingredient hydration, boiler makeup, and multiple beverage lines from the same treatment train, peak diversity loading becomes critical. A typical jump from 100 GPM to 350 GPM often requires: The table makes one point very clear: water system scaling is a plant infrastructure project, not simply an equipment purchase. It affects beverage quality, sanitation, energy, wastewater, and uptime. Companies that treat water expansion as a strategic utility upgrade usually avoid expensive rework later. DPS brings process, mechanical, electrical, plumbing, and controls engineering together for this type of project. That integrated capability matters because water systems connect directly to RO skids, disinfection, storage tanks, CIP, automation, and packaging demand. Beverage clients can review engineering and project delivery services when evaluating how to coordinate utility growth with processing and filling. Many beverage plants do not have the luxury of shutting down for three months to build. Carbonated soft drinks can surge ahead of summer. RTD beverages and flavored waters may peak with promotional calendars. Beer can see major spring and summer lift. Dairy beverages and specialty holiday drinks have different cycles. Expansion planning must fit around these revenue windows. In the United States, a practical schedule often revolves around shoulder seasons, regional weather patterns, and customer buying calendars. Facilities serving the Southeast may experience earlier warm-weather spikes than plants supplying the Upper Midwest. West Coast operations tied to grocery and convenience channels may have different promotional timing than co-packers serving club stores nationwide. This table helps operations teams align capital work with sales realities. The exact windows change by category, but the discipline remains the same: build the schedule around the market, not around the contractor’s convenience. A common tactic is to complete civil, structural, utility, and off-line fabrication first; then perform short-duration cutovers in carefully planned shutdowns. Another is to install new process capacity in parallel while the existing packaging line runs, then connect packaging later. Plants with critical summer volume in Texas, Florida, Georgia, and Southern California often benefit from especially conservative summer cutover plans. The bar chart reflects where expansion demand is trending in the United States. Functional beverages, RTD products, and established carbonated categories are sustaining strong capital planning, especially where co-packing networks are expanding. Cold chain is often the last budget line to be fully appreciated and the first place where plants feel pain after a successful line expansion. If production increases but coolers, freezers, or docks do not, throughput simply moves from the filler to the warehouse bottleneck. For dairy beverages, cultured drinks, chilled juices, and some high-value functional products, cold chain determines both shelf life and customer service reliability. Even for products that are shelf stable, climate-controlled staging can be important in humid or high-heat regions where packaging materials, ingredients, and finished goods are sensitive. Manufacturers operating in Gulf Coast climates or in dense Northeast logistics zones may need better dock seals, traffic flow, and temperature management to prevent quality drift and labor inefficiency. Expansion can include larger coolers, blast chilling, freezer room additions, insulated panels, low-temperature air distribution, underfloor heating in freezer applications, dock shelters, traffic management systems, and separate inbound/outbound temperature zones. The decision should be based on dwell time, pallet velocity, SKU count, and truck turn performance, not only on square footage. The explanation is straightforward: warehouse and dock capacity must expand in step with processing and packaging, or the project will not deliver its intended throughput. This is especially true for beverage operators near major freight gateways such as Long Beach, Savannah, Newark, and Memphis distribution channels. One of the safest ways to expand a beverage plant is to separate the project into logical phases. In many cases, processing should be upgraded before final packaging integration. That allows owners to build utility depth, create ingredient and batching capacity, validate sanitation, and install controls while the current packaging line continues to run. A phased approach might look like this: This sequence lowers risk because it addresses the hidden capacity drivers first. It also improves startup quality. Beverage lines that try to tie in utilities, processing, and packaging at the same time often encounter compounded delays. When everything is critical path, nothing is predictable. From a technology standpoint, DPS supports this model through process design, structural and utility engineering, controls integration, PLC programming, SCADA, and on-site execution management. That matters when a plant needs clean handoff between legacy systems and new equipment. It also helps when a manufacturer is adding proprietary or custom-built assets. Companies exploring integrated skids, tanks, or custom process equipment can review process equipment capabilities as part of expansion planning. The area chart reflects a clear 2026 trend: more beverage expansion budgets are shifting toward automation, controls visibility, resource efficiency, and utility resilience, rather than only toward visible packaging speed. Compliance should not be treated as a final checklist item. In beverage projects, it should influence layout, materials, drainage, zoning, cleanability, allergen handling, water system validation, and documentation strategy from the very beginning. In the United States, FDA expectations apply broadly, while HACCP-based preventive thinking underpins hazard control. If the plant ships into Canada, CFIA requirements and customer documentation standards can add another layer. For many beverage manufacturers, the expansion review should include hygienic design, environmental controls, traffic segregation, ingredient traceability, validated cleaning procedures, calibration programs, and records integration. Plants serving large retailers or national restaurant chains may also need to satisfy customer audit frameworks such as SQF or BRC-aligned expectations even if the base legal requirement is different. The explanation behind this table is simple: the physical expansion and the compliance system must be built together. If they are handled separately, plants often end up paying twice through redesign, extra validation, or delayed startup. DPS has experience supporting regulated food and beverage environments across FDA, USDA, SQF, and BRC-aligned projects, with service reach across the United States and Canada. For owners comparing execution partners, that combination of engineering and compliance fluency can reduce handoff friction between design, construction, and commissioning. A beverage expansion should be approved as a profit project, not as an equipment project. The strongest return models capture more than simple additional volume. They include contribution margin per case, labor reduction, scrap reduction, lower changeover losses, reduced outsourced storage, lower freight touches, energy savings, and avoided downtime. A practical payback formula is: Payback Period = Total Installed Cost / Annual Net Benefit Annual net benefit can include: Suppose total installed cost is $4.8 million and annual net benefit is $3.72 million. The payback period is about 1.29 years. That is the kind of model that gets executive attention because it ties capacity expansion to cash generation. One reason DPS has gained traction with larger beverage and food manufacturers is its focus on identifying the real economic bottleneck. In some cases, a controls or PLC issue can unlock more capacity than major steel in the floor. In others, a well-planned utility expansion creates the foundation for multiple future phases. For examples of how projects are approached in the field, manufacturers can review project case studies. Tight schedules are normal in beverage manufacturing. Lead times on tanks, chillers, RO skids, fillers, labelers, compressors, electrical gear, and refrigeration components can vary widely. Mechanical contractors may have labor constraints in fast-growth markets such as Texas, the Carolinas, Tennessee, Arizona, and parts of California. Successful owners manage this by aligning engineering release, procurement, fabrication, permitting, and site readiness in one integrated schedule. Supplier management should include not just price and delivery, but also utility loads, service access, startup support, spare parts, controls compatibility, factory acceptance testing, and documentation quality. A cheaper machine that cannot integrate cleanly with the plant SCADA or CIP architecture can become far more expensive in the field. The table shows how owners can compare bidders on more than headline cost. The best expansion projects are won in planning meetings, not during emergency troubleshooting on startup weekend. The comparison chart highlights a common reality in the United States market: packaging lines and refrigeration systems often carry the longest lead times, so they should be planned early even when installation occurs in a later phase. From a manufacturing capability standpoint, DPS can also supply selected proprietary process equipment such as tanks and CIP systems, which can simplify coordination when owners need custom dimensions, faster alignment with process requirements, or fewer vendor handoffs. From a service capability standpoint, the company’s Design Build Manage approach gives owners a single partner for design, field coordination, local trade management, and execution oversight, especially useful when timelines are compressed. The first step is a bottleneck and feasibility assessment. Measure where the plant actually loses capacity: water, batching, carbonation, pasteurization, filler speed, packaging labor, cooler space, or docks. Do not buy equipment before validating the true constraint. Small utility or process modifications may take a few months. Major line additions or warehouse and refrigeration expansions can take nine to eighteen months depending on permitting, procurement, and shutdown windows. Long-lead equipment often determines the schedule. In many beverage facilities, processing and utilities should be expanded first. That creates stable upstream capacity and reduces risk before the packaging integration phase. The exact answer depends on where the current bottleneck sits. It is critical. Water treatment affects taste, microbiological control, equipment life, sanitation, and uptime. A line cannot reliably produce at higher rates if the water system cannot support volume and quality targets. Late review of hygienic zoning, CIP validation, drainage, traffic flow, traceability integration, and customer audit requirements causes many delays. These should be reviewed during design, not after installation. Use real throughput data and include gross margin, labor savings, waste reduction, utility changes, outside storage, freight touches, and downtime avoidance. Avoid relying only on the supplier’s nameplate capacity. Often yes, but only with phased sequencing. Off-line fabrication, utility prework, weekend tie-ins, and shoulder-season cutovers are common methods. Total avoidance of downtime is rare, but disruption can be minimized sharply. Co-packers, regional bottlers, breweries, RTD brands, juice and functional beverage processors, dairy beverage plants, and aseptic facilities all benefit when volume growth, SKU complexity, or service expectations begin to outpace the plant’s infrastructure. DPS supports clients across engineering, capital planning, owner representation, project management, equipment supply, utility integration, installation, and startup. Its team works across all 50 U.S. states and Canada, with beverage-specific expertise spanning water systems, fermentation, carbonation, pasteurization, aseptic systems, utilities, and automation. Key 2026 trends include stronger investment in automation and SCADA visibility, water reuse and sustainability planning, energy optimization, flexible multi-SKU lines, regionalized supply chains, tighter documentation expectations, and more resilient cold chain and dock operations. For beverage manufacturers in the United States, expansion is no longer just a construction event. It is a capital strategy that must connect product mix, utilities, compliance, labor, distribution, and profit. Plants that plan in phases, size infrastructure correctly, and work with partners who understand both engineering and operations are the ones most likely to grow without sacrificing service or margin. -
Food Factory Expansion Planning
Expanding a food factory in the United States is rarely just a construction decision. It is an operational, regulatory, financial, and commercial decision that must protect production while creating new capacity. Whether a processor is adding a new ready meal line in Chicago, increasing dairy throughput in Wisconsin, building cold storage near Atlanta, or relocating utilities for a beverage site near Los Angeles/Long Beach, the winning plan starts with demand realism, process flow logic, and strict hygiene separation. A successful expansion must answer five questions early: Is the market demand durable, what bottleneck is truly limiting output, which lines cannot stop, how will certification be preserved, and how will the facility return to production safely after construction? In the U.S. market, food plant expansion planning is especially sensitive because supply chains vary by region. Protein processors around Kansas City and Omaha may prioritize livestock proximity and wastewater capacity. Beverage operations in North Carolina, Texas, and California often focus on utility redundancy, packaging line speed, and route-to-market timing. Imported ingredient users near the ports of Savannah, Newark, Houston, and Long Beach may design around dock flow, quarantine areas, and warehouse turns. The best projects connect commercial demand, product mix, sanitation zoning, and construction execution from the very beginning. The short answer is this: a food factory expansion should begin with a feasibility and bottleneck study, not with demolition, equipment ordering, or contractor bidding. In most U.S. facilities, the lowest-risk path is to map process flow, identify the lines that cannot stop, align the design with BRC, SALSA, or SQF Level 3 expectations, then build in phases that follow the movement of raw materials, people, waste, and finished goods. This design-first approach usually reduces rework, shortens downtime windows, and can save 15% to 25% of total project cost compared with a rushed build-first model. For operators buying capacity, the right advice is to invest capital where margin, throughput, and operational resilience intersect. That might mean a new cook/chill room, a CIP upgrade, a packaging hall extension, utility expansion, or a better automation strategy rather than a larger building footprint. A strong owner will test multiple scenarios: more shifts, debottlenecking controls, partial line duplication, off-site warehousing, and complete expansion. The best decision is not always the biggest one. The table above shows why expansion decisions should be sorted by business driver. A plant that mistakes a packaging bottleneck for a building shortage can overspend dramatically. Likewise, a site with audit pressure may need segregation, airflow, drainage, and personnel flow improvements before it needs more square footage. The growth trend reflects the reality that U.S. processors continue to invest in automation, resiliency, and regional manufacturing. The 2026 outlook is shaped by reshoring pressures, retailer service-level expectations, labor constraints, and sustainability upgrades such as heat recovery, water reuse, and energy monitoring. Pre-planning is where a profitable project is separated from an expensive mistake. A feasibility study should test market demand, production capacity, utility constraints, labor availability, site logistics, and total cost of ownership. In the United States, this means reviewing not only customer forecasts but also freight patterns, regional labor markets, energy prices, wastewater limits, and state-level permitting timelines. Market demand assessment should be product-specific. Frozen prepared foods in the Midwest have different volume curves and storage profiles than aseptic beverages in California or protein marinated products serving the Southeast. Demand quality matters as much as demand size. Long-term private label awards, multi-state retail distribution, and strategic foodservice contracts provide better expansion support than speculative pipeline estimates. If a plant ships through the Port of Savannah or Port of Houston, imported packaging and ingredients can also influence the shape of inventory and warehouse expansion needs. For product types, feasibility should separate shelf-stable, chilled, frozen, aseptic, fermented, raw, and allergen-sensitive products. Each has a distinct sanitation burden, utility profile, and line balance requirement. A yogurt expansion may depend on fermentation and cold chain capacity. A sauce line may depend on kettle throughput, CIP efficiency, and hot-fill timing. A co-packer may need more flexible batching, more changeover control, and stronger scheduling logic than a single-SKU manufacturer. During this phase, many owners benefit from outside engineering support that understands both process and project economics. Food and beverage engineering services that combine feasibility, process design, owner representation, and capital planning are often more valuable than early contractor pricing because they help define the right project before money is committed. This table matters because many expansions fail in planning, not in construction. A site may have plenty of floor space yet lack sanitary drainage, electrical capacity, or wastewater headroom. Another may have demand but not the workforce to support a second shift, making automation or relocation the smarter path. At this stage, companies should also define what success means. Is the goal more cases per hour, lower labor cost per unit, reduced changeover time, additional cold storage, or multi-product capability? A sound feasibility study converts general ambition into measurable outputs. Every operating facility has sacred lines. These are the lines that cannot stop without triggering customer shortages, spoilage losses, labor disruption, or major revenue hits. Operational constraints analysis identifies those lines, the utility systems they depend on, and the upstream or downstream functions that must remain live throughout construction. In practical terms, this means mapping production by criticality. For example, a cooked protein line in Arkansas may feed a retailer with strict fill-rate penalties. A beverage blending and filling operation near Dallas-Fort Worth may support a summer seasonal build where downtime is commercially unacceptable. An East Coast bakery may be able to stop packaging on weekends but cannot interrupt proofing or freezer systems. Expansion planning should categorize assets into no-stop, short-window stop, and relocatable operations. The analysis must include process, utilities, people, sanitation, and warehouse flow. A line may appear stoppable until the team realizes it shares compressed air, wastewater trenches, ammonia, or CIP circuits with two other production zones. Construction phasing must therefore be built around live dependencies, not just around equipment footprints. The explanation is straightforward: a plant should never judge line shutdown risk only by production hours. Cleanup validation, restart checks, thermal stabilization, and quality hold times often make a four-hour shutdown behave like a full-day event. Industry demand remains strongest where throughput, shelf-life control, and labor efficiency create immediate returns. Protein, beverage, and prepared foods are especially active because regional distribution, private label growth, and automation pressure continue to drive capex in those segments. Any expansion inside an operating food plant must be designed around the certification environment. BRC, SALSA, and SQF Level 3 all place serious emphasis on site standards, zoning, contamination control, traceability, maintenance discipline, and validation. The specific wording differs by scheme, but the practical expectation is the same: construction must not compromise food safety or audit readiness. BRC-oriented sites often focus deeply on environmental control, fabric condition, segregation, and documented risk assessment. SALSA may be more common in smaller or growing operations, but it still requires disciplined controls around hygiene, materials, and site management. SQF Level 3 adds a strong quality management dimension on top of food safety, making process consistency and controlled change management especially important during expansions. The right alignment process begins with a certification gap review of the future state, not just the current state. An owner should ask: after the new room, line, utility route, and people flow are installed, will the facility still support hygienic zoning, allergen separation, air balance, drainage design, cleanable surfaces, handwashing access, and traffic control? A temporary construction arrangement that creates audit risk for six months can still damage the business, especially if a major retailer or branded customer audits between phases. Plants in the United States serving national chains often need to satisfy customer-specific add-ons beyond formal certification. That is why design and execution partners with experience in FDA, USDA, SQF, and BRC environments are valuable. Firms that understand sanitary detailing, hygienic utility integration, and audit-sensitive shutdown planning reduce the risk of expensive redesigns later. The table shows that certification alignment is not paperwork alone. It changes wall systems, drainage, workflow, startup validation, and even how temporary doors and access routes are controlled during the project. The most reliable sequencing strategy is to follow process flow. Start by understanding how ingredients arrive, where they are stored, how they move into preparation, processing, packaging, palletizing, and shipping, and where waste, people, tools, and maintenance traffic intersect. Then phase the construction in a way that preserves this logic while moving risk away from live production. In many U.S. projects, the best sequence is not the fastest-looking one on paper. For example, expanding a packaging hall before upstream utilities are ready may create stranded equipment. Building a new warehouse before modifying docks may actually ease congestion and allow internal space to be repurposed with less disruption. In a beverage facility, a new syrup room, boiler yard, or compressor pad may need to come first because utilities govern the rest of the schedule. Following process flow also supports food safety. Dirty-to-clean migration should not worsen during construction. Raw receiving traffic should not cross finished goods routes. Contractors should have dedicated pathways that avoid high-care zones. If the facility is cold-chain intensive, sequencing must also consider thermal envelope integrity so temporary works do not degrade storage conditions or create condensation risk. A strong phased plan usually includes enabling works, temporary utility support, shell or civil modifications, utility tie-ins, process installation, controls integration, dry commissioning, wet commissioning, and hygiene validation. This is often where integrated project delivery matters. Teams that can design, build, and manage together typically resolve field issues faster because engineering intent, contractor coordination, and startup priorities remain aligned. Companies looking at end-to-end capital project execution can review DPS and its Design Build Manage approach to understand how integrated oversight supports live-plant expansions. The trend is clear: U.S. food manufacturers increasingly prefer phased expansion over full shutdown construction. Labor shortages, tighter retailer service expectations, and food safety exposure make business continuity a strategic requirement, not just a convenience. A design-first approach saves money because it exposes hidden scope before procurement and construction begin. In food plants, hidden scope usually includes utilities, drains, hygienic finishes, controls modifications, temporary partitions, environmental controls, and startup support. These items are expensive when discovered late. Owners often think early contractor pricing gives budget certainty. In reality, if the process basis, sanitary requirements, and shutdown plan are not defined, the number is only a placeholder. Design-first budgeting develops equipment lists, utility loads, room conditions, sequencing logic, and tie-in strategies early enough to reduce change orders and avoid purchasing the wrong capacity. For U.S. projects, the savings can be substantial because permit review, trade availability, and material lead times can vary by market. Stainless fabrication, insulated panels, hygienic drainage, switchgear, refrigeration components, and control panels may all face long lead times. A well-developed design allows smarter buyout timing and better substitute evaluation without compromising food safety or performance. Budget planning should include direct and indirect costs: temporary operations, lost production windows, quality validation, operator training, spare parts, software changes, utility commissioning, and contingency. It should also include lifecycle thinking. A lower-cost floor system that traps water or degrades under sanitation chemicals can become the most expensive decision in the project. This table explains why 15% to 25% savings are realistic. The savings rarely come from cheaper materials alone. They come from avoiding wrong work, duplicated work, missed tie-ins, and extended downtime. By this point in a project, owners should also compare internal capabilities with external support. Some teams have excellent operations knowledge but limited bandwidth for engineering coordination, equipment integration, or contractor management. That is where structured project leadership becomes important. In food manufacturing, the lowest bid can be the highest-cost outcome. Food plants are not generic industrial buildings. They involve hygienic details, cleanable construction, utility reliability, shutdown precision, and compliance-sensitive execution. A contractor without food industry experience may price aggressively and still miss the true complexity of drains, washdown protection, airflow control, insulated envelopes, sanitary supports, or staged tie-ins. What matters most is relevant experience in live food and beverage environments. Has the contractor worked around USDA inspection? Do they understand allergen containment? Can they coordinate with sanitation and quality teams? Have they executed utility cutovers without contaminating production? Do they know how to protect a high-care area from dust, traffic, and vibration? These questions are more important than a line-item discount. Local supplier networks also matter. In the United States, successful projects often rely on a national management team combined with vetted regional trades. A processor in North Carolina may need different concrete, mechanical, refrigeration, or panel specialists than a plant in the Pacific Northwest or Southern California. Regional knowledge shortens response time and improves permit and inspection coordination. When comparing partners, owners should review service capabilities, not just installation capacity. Strong providers can support feasibility studies, process engineering, owner representation, project management, equipment procurement, construction oversight, controls integration, and commissioning. That broad service model reduces gaps between design intent and field execution. For companies needing both engineering depth and field execution, a partner that can handle process design, capital planning, general contracting functions, installation, and project management under one umbrella often reduces risk. Selected project examples can help owners evaluate whether a firm has solved similar expansion challenges in real operating environments. The comparison chart illustrates a common truth in capital projects: general contractors may look cheaper on bid day, while food-specialist teams usually outperform where contamination control, utility tie-ins, and startup reliability decide the real cost. The hygiene interface is the most sensitive part of an operating expansion. It is where contractor traffic, dust, tools, waste, noise, and temporary openings meet active production, open product, packaging materials, and sanitation routines. If this interface is weak, a project can trigger audit findings, product risk, and unstable operations even when the construction quality is otherwise good. The control strategy should begin with zoning. Construction areas need physical separation, marked access routes, dedicated PPE rules, waste handling plans, and cleaning accountability. Air movement must be controlled so dust does not migrate into production. Temporary walls, negative pressure in work zones, sticky mats, door management, and contractor hygiene protocols are all useful tools. In high-care or allergen-sensitive environments, those controls become non-negotiable. Daily coordination between operations, quality, sanitation, maintenance, and the construction manager is essential. This is not a weekly meeting issue. It requires routine permit-to-work management, pre-task reviews, and escalation procedures for any event affecting water, air, drains, electrical systems, doors, or traffic patterns. Construction waste must have a defined route that never compromises ingredient or finished goods movement. This is also the right place to note technology capabilities that matter during food expansions. Advanced providers can support structural, mechanical, plumbing, electrical, process, and controls engineering; PLC programming; automation; and SCADA integration. Those capabilities become valuable when a plant needs temporary utility logic, phased controls cutovers, or production data visibility during a live transition. Manufacturing capabilities also shape hygiene success. Teams that understand tanks, CIP systems, vessels, mixing, cooking, pasteurization, retort, fermentation, filtration, carbonation, aseptic systems, dairy process equipment, protein lines, and utility skids are better able to plan construction around real product contact risks and cleaning requirements. Companies evaluating equipment options can explore food processing equipment solutions as part of a broader expansion strategy rather than as isolated purchases. The table demonstrates that hygiene management is operational discipline, not just a wall between two spaces. Daily verification and documented controls are what preserve production integrity during months of work. Commissioning is where capital spending finally becomes productive capacity. In food factories, this stage must prove more than mechanical completion. It must verify safety, sanitation, controls, utility performance, operator readiness, and product protection before the first saleable run begins. Post-expansion commissioning typically progresses from construction completion to punch resolution, dry checks, utility startup, controls checkout, water runs, CIP validation, thermal or flow testing, line integration, and then product trials. Each step should have defined acceptance criteria. Compressing this sequence often creates false speed and expensive instability later. Pre-production hygiene validation should include environmental cleaning verification, ATP where appropriate, microbiological checks based on product risk, allergen cleaning validation when relevant, utility quality confirmation, compressed air review, water quality checks, and pre-op inspections of all food contact and adjacent surfaces. If the project modified HVAC, drainage, or room pressurization, those systems should also be revalidated as part of startup. Training is equally important. Operators, maintenance staff, sanitation crews, and quality teams need updated SOPs, lockout methods, cleaning steps, startup sequences, alarm responses, and traffic rules. In many failed startups, the equipment works but the organization is not ready. The most mature projects treat commissioning as a business readiness process, not just an engineering milestone. Looking toward 2026, future trends in U.S. food plant expansion include greater use of automation, energy monitoring, digital maintenance tools, recipe and batch control improvements, water reuse strategies, low-emission utility design, and more robust data collection for food safety and ESG reporting. Policy pressure around wastewater, energy intensity, refrigerant management, and labor availability will continue to influence project design. Sustainability will matter not only for corporate reporting but also for utility cost control and customer expectations. Companies with broad process and utility expertise are better positioned here. A capable expansion partner should understand boilers and steam, refrigeration and glycol, compressed air, wastewater, process water, HVAC, CIP, automation, and startup integration across food and beverage categories. That blend of technology, manufacturing know-how, and service execution is what helps a project move from installed equipment to profitable production. How long does a food factory expansion usually take in the United States?A moderate live-plant expansion commonly takes 6 to 18 months from feasibility to startup, depending on permitting, utility complexity, equipment lead times, and how much production must remain live. What is the biggest mistake owners make?Starting with construction pricing before completing feasibility, process design, and utility analysis. That usually produces incomplete budgets and avoidable change orders. Can a plant stay certified during construction?Yes, but only if risks are formally managed. Temporary barriers, contractor GMP rules, documented zoning controls, and validation planning are essential for maintaining audit readiness. Should we expand the building or debottleneck first?Debottlenecking should be tested first. In many plants, the actual limit is controls logic, CIP capacity, packaging speed, or utility reliability rather than floor area. What industries benefit most from phased expansion?Protein, dairy, beverages, sauces, prepared foods, aseptic processing, and co-packing operations benefit strongly because downtime is costly and hygiene risks are high. How important is contractor food industry experience?Very important. Food-specialist experience affects sanitary detailing, shutdown planning, contamination prevention, and startup reliability, which usually matter more than the lowest initial bid. What should be included in pre-production validation?Mechanical completion checks, controls verification, utility testing, cleaning validation, environmental checks, operator training, SOP updates, and documented release criteria. How should we evaluate a project partner?Look for proven food and beverage engineering, process knowledge, installation capability, project management discipline, and experience with certifications and live operating sites. For firms that want a national partner with agile execution across North America, DPS is known for combining strategic planning with hands-on delivery in food and beverage capital projects. A well-planned food factory expansion in the United States should protect the present while building the future. The strongest projects begin with market-backed feasibility, identify true bottlenecks, respect line criticality, align with certification, and phase construction around process flow. They also treat hygiene management and commissioning as central workstreams, not finishing tasks. When those elements are integrated, manufacturers gain more than capacity. They gain reliability, audit resilience, and a facility platform ready for 2026 growth, sustainability expectations, and smarter manufacturing. -
Food Plant CAPA Systems: 2026 Best Practices Guide
Food plant CAPA systems are no longer just a quality department formality in the United States. In 2026, they are a core operating discipline that protects food safety, supports FDA, USDA, SQF, and BRC expectations, and reduces expensive repeat failures across production, utilities, sanitation, automation, and packaging. For manufacturers running high-throughput operations in markets such as Chicago, Dallas, Fresno, Charlotte, Houston, Atlanta, and the port corridors of Los Angeles/Long Beach and Savannah, a strong corrective and preventive action process is essential for keeping products moving, customers satisfied, and capital investments profitable. A practical CAPA system must do more than record deviations. It should identify issues quickly, assign risk, determine the real root cause, implement corrections at the plant floor and system level, verify effectiveness, retain clear records, and convert plant history into management insight. This matters across protein, dairy, aseptic beverages, sauces, prepared foods, shelf-stable foods, co-packing, fermentation, and cold-chain operations. Plants that treat CAPA as an integrated business tool usually see fewer shutdowns, lower rework, stronger audit performance, and more predictable throughput. The quick answer is simple: a best-practice CAPA system for a U.S. food plant should connect quality, maintenance, production, engineering, sanitation, warehouse, procurement, and leadership in one disciplined workflow. It begins when a nonconformance, complaint, audit finding, environmental result, utility failure, startup issue, or process drift is detected. It then moves through containment, investigation, root cause analysis, action planning, implementation, verification, closure, and trend review. In 2026, leading facilities are shifting away from isolated spreadsheets and after-the-fact paperwork. They are building digital CAPA workflows tied to SCADA alarms, batch data, downtime logs, preventive maintenance systems, sanitation records, metal detector checks, allergen controls, and supplier quality events. The strongest programs also distinguish between a correction and a corrective action. A correction solves the immediate symptom, such as holding a lot or replacing a failed gasket. A corrective action addresses the cause so the same issue does not recur. Preventive action goes one step further by updating the system before similar risk appears elsewhere. For buyers evaluating CAPA software, consulting support, or plant modernization partners, the best advice is to choose a solution that fits actual plant complexity. A small regional processor may need a simple digital workflow with strong accountability and retention controls. A multi-line beverage, dairy, or protein network may require automated evidence capture, audit trails, configurable risk scoring, and integration with maintenance, ERP, and controls. CAPA should be designed around plant reality, not just compliance language. The table above shows why CAPA is best managed as a timed, evidence-based operating process rather than an open-ended investigation file. Plants that define ownership and expected timing reduce backlog and avoid the common problem of “closed on paper, still recurring in production.” Every strong CAPA program starts with disciplined issue identification. In U.S. food plants, reportable issues can arise from customer complaints, internal audits, third-party audits, regulatory inspections, sanitation failures, environmental monitoring positives, process deviations, foreign material incidents, packaging leaks, coding errors, startup losses, utility interruptions, automation faults, or supplier defects. Many plants still under-report problems because operators think CAPA is only for serious events. In reality, repeated small deviations often become the most valuable signals. Plants should define clear trigger thresholds. For example, one isolated label skew may be a line correction; repeated label skew across a week may require CAPA. One temperature excursion during startup may be a deviation; recurring excursions on a kettle, retort, or HTST loop likely require deeper investigation. Complaint trends by SKU, shift, or line should also trigger escalation. Sites near high-volume distribution lanes such as Memphis, Indianapolis, New Jersey, and the I-85 corridor often benefit from tying CAPA triggers to complaint velocity because market exposure grows quickly once product leaves the plant. Good documentation must answer six questions: what happened, when it happened, where it happened, who detected it, what product or system was affected, and what immediate controls were applied. Photos, historian trends, batch records, CIP reports, maintenance work orders, allergen cleanout records, calibration results, and warehouse disposition records should be attached at the start, not collected weeks later. The explanation behind this table is straightforward: every source of plant risk creates a different evidence trail. When plants use a single generic form without source-specific prompts, investigations become slower and less accurate. A modern CAPA intake should guide the user to collect the right records based on event type. Documentation quality also improves when the plant floor is designed for visibility. Engineering choices matter here. Better line layouts, utility labeling, access to instrument trends, and sanitary equipment design all make issues easier to detect and document. Companies seeking plant-wide improvements often turn to specialists that can align quality needs with process design and installation. A firm such as DPS engineering and project services can be relevant when issue frequency is tied to process architecture rather than operator behavior alone. Root cause analysis is where many CAPA systems fail. Teams often stop at the first plausible explanation: operator error, training gap, or maintenance oversight. These may be contributing factors, but they are rarely the full cause. In food and beverage manufacturing, true root causes often combine method, machine, material, manpower, environment, and measurement failures. A filler misfire may trace back to compressed air quality. A recurring sanitation miss may actually be a poor equipment drainage point. A complaint spike may come from line speed changes that were never validated against package integrity. The most useful methodologies include 5 Whys, fishbone diagrams, fault tree analysis, Pareto review, cause-and-effect matrices, and failure mode thinking. Plants do not need every tool for every event. They need the right level of rigor for the risk involved. A mislabeled rework tote might need a fast 5 Whys. A recurring pathogen niche in a ready-to-eat area may need a deeper multidisciplinary review involving hygienic zoning, airflow, traffic patterns, and redesign. This table shows that methodology selection should match complexity. The best-performing U.S. plants teach supervisors and engineers when to use a fast problem-solving tool and when to elevate the event into a systems review. Technology can significantly improve root cause accuracy. Integrated controls, PLC diagnostics, batch sequencing, historian data, and SCADA trend capture help teams move from assumptions to evidence. That is especially valuable in beverage, dairy, aseptic, retort, and protein plants where process timing and utilities heavily influence outcomes. Manufacturers looking at process modernization can benefit from partners with controls, automation, and process engineering depth, especially when CAPA findings point to instrumentation blind spots or weak interlocks. Review of process equipment capabilities is also useful when repeat failures are linked to vessel design, CIP coverage, mixing performance, or thermal equipment limitations. The line chart reflects a realistic market direction: food manufacturers across the United States are steadily moving toward digital CAPA systems because customer requirements, recall readiness, and labor constraints all favor faster evidence collection and better follow-through. Corrective action is the point where analysis becomes operational change. Actions should be specific, assigned, funded when necessary, and tied to a completion date based on risk. “Retrain operators” by itself is not a strong corrective action. A stronger plan might include revising the setup standard, adding a keyed part to eliminate incorrect assembly, updating the HMI prompt, changing startup checks, and validating new settings over three production runs. Implementation should separate immediate correction from durable systemic action. In a food plant, corrections may include holding product, re-inspecting inventory, cleaning equipment, repairing a seal, adjusting parameters, or reworking packaging. Corrective actions may include redesigning a conveyor transfer, changing a supplier specification, relocating an allergen staging point, automating a verification, or rebuilding a utility loop that creates inconsistent temperatures. Capital planning matters here. Some CAPA findings can be fixed procedurally; others require engineering intervention. Many recurring failures are created by aging layouts, under-sized utilities, weak sanitary design, poor line integration, or controls that do not match production goals. This is where implementation partners matter. Through a design-build-manage model, DPS supports process engineering, installation coordination, and execution oversight in ways that help plants convert CAPA findings into profitable infrastructure upgrades rather than piecemeal patchwork. Manufacturers wanting broader context can explore project case examples to see how operational bottlenecks are often solved at the system level. The explanation here is that corrective action must be matched to the failure mechanism. The more technical the cause, the less likely it is that retraining alone will work. Plants that repeatedly use training as the default corrective action often see recurrence. Preventive action is where CAPA becomes strategic. Once a root cause is proven on one line or product family, management should ask where else the same weakness exists. If a filler valve design causes sanitation risk on one beverage line in California, does a similar risk exist on sister lines in Texas or North Carolina? If a supplier COA verification process failed for one ingredient in a Midwest sauce facility, does the same vulnerability affect spices, oils, or dry blends from other vendors? Best-practice preventive measures include SOP harmonization, PM plan updates, control system alarms, line clearance improvements, sanitation redesign, hygienic zoning upgrades, stronger incoming inspection, operator certification, utility monitoring, spare parts standardization, and supplier development. For 2026, plants should also focus on sustainability-linked prevention. Water reuse systems, energy recovery, compressed air optimization, and CIP chemical control can all create new failure modes if not integrated with food safety and CAPA logic. Sustainable systems must still be verifiable systems. This is also where technological capabilities have major value. DPS works across process, mechanical, plumbing, electrical, structural, and controls disciplines, including PLC programming, automation, SCADA, utilities, CIP systems, thermal processing, and full system integration. That matters because preventive measures often fail when a plant tries to solve a process problem in isolation. A temperature deviation might not be a kettle issue at all; it could originate from steam pressure instability, valve response, control logic, or condensate management. Cross-discipline engineering gives preventive action a better chance of sticking. The area chart highlights an important trend shift for 2026 and beyond: preventive control programs are increasingly linked to digital plant systems. This shift is being pushed by labor efficiency, audit expectations, cybersecurity-conscious version control, and the need for faster trend review across multi-site networks. A CAPA is not complete when the action item is marked done. It is complete when the plant proves the action eliminated or materially reduced the problem. Verification confirms the required steps were carried out. Validation or effectiveness review confirms they worked in real operating conditions. For low-risk issues, effectiveness may be demonstrated by a limited run review, observation audit, or documentation check. For high-risk issues, the plant may need multiple production cycles, environmental monitoring rounds, thermal validations, package integrity tests, allergen swab results, or complaint trend reductions over 30 to 90 days. In highly regulated sectors such as aseptic beverages, dairy, meat, or ready-to-eat foods, closure without measurable evidence is weak and often challenged during audits. Useful metrics include repeat rate, days to closure, overdue CAPA count, recurrence by line, complaint reduction by SKU, sanitation verification pass rate, startup scrap reduction, and downtime impact. Plants with robust verification methods usually set effectiveness criteria at the time the action is approved, not after the due date arrives. The explanation is that each CAPA should have a defined proof method tied to the nature of the problem. Plants close fewer weak CAPAs when they specify the effectiveness test before implementation begins. Documentation and retention are often overlooked until an FDA inspection, customer audit, legal inquiry, or recall simulation exposes gaps. A strong CAPA record should include the event description, risk assessment, containment actions, disposition decision, investigation notes, root cause method, evidence reviewed, action plan, approver names, due dates, implementation proof, effectiveness review, and final closure authorization. Retention periods vary based on product category, customer requirements, certification schemes, and company policy. In practice, many U.S. food manufacturers keep CAPA records for at least the product shelf life plus one year, and often longer where regulatory, legal, or customer expectations justify it. Multi-site businesses commonly standardize retention windows so that records can be compared across states and product groups. Digital retention should include audit trails, secure access, backup protocols, and revision control. If control logic or HMI sequences were changed as part of the corrective action, those software versions should also be retained with proper change management. Plants that rely on uncontrolled local files create avoidable risk. This table matters because record retention is not just a document issue; it is a plant memory issue. Without organized historical evidence, teams repeat the same investigations, lose engineering context, and struggle to defend decisions made under pressure. Trend review is where CAPA data becomes management intelligence. Site leaders should not only review open and closed actions, but also recurrence, aging, source patterns, line concentration, shift concentration, and the share of CAPAs tied to utilities, sanitation, supplier quality, packaging, controls, or startup execution. In many plants, the best insights come from combining CAPA with OEE loss data, downtime logs, complaint analytics, and maintenance histories. A practical monthly management review should answer these questions: Are we seeing more events from one product family? Are overdue CAPAs clustered in one function? Which issues are repeat events from prior quarters? Are temporary fixes replacing long-term solutions? Is capital spending needed to eliminate chronic risk? This level of visibility is especially important for multi-site networks serving major retail and foodservice channels from hubs such as Chicago, Kansas City, Southern California, and the Southeast. The bar chart shows where demand for CAPA improvement is strongest. Aseptic, beverage, and protein operations often face the highest need because process complexity, distribution scale, and compliance stakes are especially high. Management reporting should also support buying decisions. If trends show most CAPAs originate from line integration, utility instability, and startup losses, the answer may not be more forms. The answer may be a broader plant upgrade or redesign. If trends show supplier defects as the dominant source, stronger specifications, incoming inspection, and vendor scorecards may provide the best return. CAPA data should guide where management spends money. The comparison chart illustrates a key point for plant leaders: software can improve workflow, but chronic CAPA problems often require engineering-led changes to equipment, controls, utilities, and installation execution. The strongest outcomes usually come from combining system tools with plant-level technical action. Disruptive Process Solutions serves food and beverage manufacturers across the United States and Canada with a practical focus on profitable capital execution. Rather than acting like a generic contractor, DPS is built to help processors make better decisions about system design, installation, integration, and project delivery. From a service capability standpoint, DPS supports capital planning, feasibility studies, owner’s representative work, project and program management, general contracting functions where licensed, and turnkey installation coordination. This matters for CAPA-driven upgrades because many manufacturers need more than recommendations; they need someone to carry the solution from concept through execution. You can learn more about the company’s background at the DPS company overview. From a manufacturing capability standpoint, DPS works across both beverage and food. Beverage experience includes brewing, spirits, wine, kombucha, RTD, soft drinks, juice, functional beverages, dairy beverages, and aseptic systems. Food experience spans protein processing, prepared foods, sauces, marinades, dairy, retort, shelf-stable applications, and co-packing operations. That breadth is valuable when a CAPA issue crosses categories, such as thermal performance, CIP coverage, mixing consistency, sanitary design, or packaging line behavior. From a technology capability standpoint, DPS brings engineering depth across process, mechanical, plumbing, electrical, structural, controls, PLC programming, SCADA, and utilities. The company also designs and supplies selected process equipment such as tanks, CIP systems, tumblers, and cooking vessels. For clients, this creates a practical advantage: CAPA findings can be translated into engineered plant changes rather than disconnected recommendations. The best fit for DPS is typically a manufacturer that values long-term thinking, wants clear operational honesty, and sees plant investment as a driver of profitability rather than just expense control. In the context of CAPA, that means using corrective and preventive action not only to pass audits, but to strengthen throughput, reliability, labor efficiency, and first-year return on capital. The table above can guide buying decisions for manufacturers comparing local suppliers, software vendors, engineering firms, and turnkey project partners. CAPA improvement is most effective when the selected partner can address both compliance workflow and physical system performance. What is the main purpose of a CAPA system in a U.S. food plant?Its main purpose is to identify nonconformances, contain risk, determine root cause, implement durable corrective and preventive actions, and prove those actions work. What events should trigger CAPA?Common triggers include customer complaints, audit findings, environmental positives, process deviations, recurring downtime, supplier defects, labeling errors, food safety incidents, and repeated startup losses. How fast should a CAPA be opened?High-risk food safety or compliance events should be opened immediately, often within the same shift. Lower-risk events can follow a defined escalation matrix, but delay should never compromise containment or evidence quality. What is the difference between correction and corrective action?A correction addresses the immediate problem, such as isolating product or replacing a broken part. Corrective action removes the root cause so the issue does not recur. Which industries benefit most from strong CAPA systems?All food and beverage sectors benefit, but the need is especially high in protein, dairy, beverage, aseptic, prepared foods, retort, and co-packing due to complexity and compliance pressure. Should CAPA be digital in 2026?For most U.S. manufacturers, yes. Digital systems improve traceability, approval control, trend review, closure discipline, and integration with production and maintenance data. How many people should be involved in root cause analysis?That depends on the event. Simple issues may need two to four people. More complex issues often require QA, production, maintenance, engineering, sanitation, procurement, and management input. How long should CAPA records be retained?Retention should align with product shelf life, regulatory expectations, customer requirements, and corporate policy. Many companies keep records for shelf life plus at least one year, and often longer. What are the biggest CAPA trends for 2026 in the United States?The biggest trends are digital workflow adoption, stronger links between CAPA and automation data, more preventive design work, higher audit scrutiny on effectiveness evidence, and greater attention to sustainability-related process risks. When should a plant involve an engineering partner?An engineering partner should be involved when recurring CAPAs point to line design, utility capacity, hygienic design, controls logic, thermal processing, or integration problems that procedural changes alone cannot solve. -
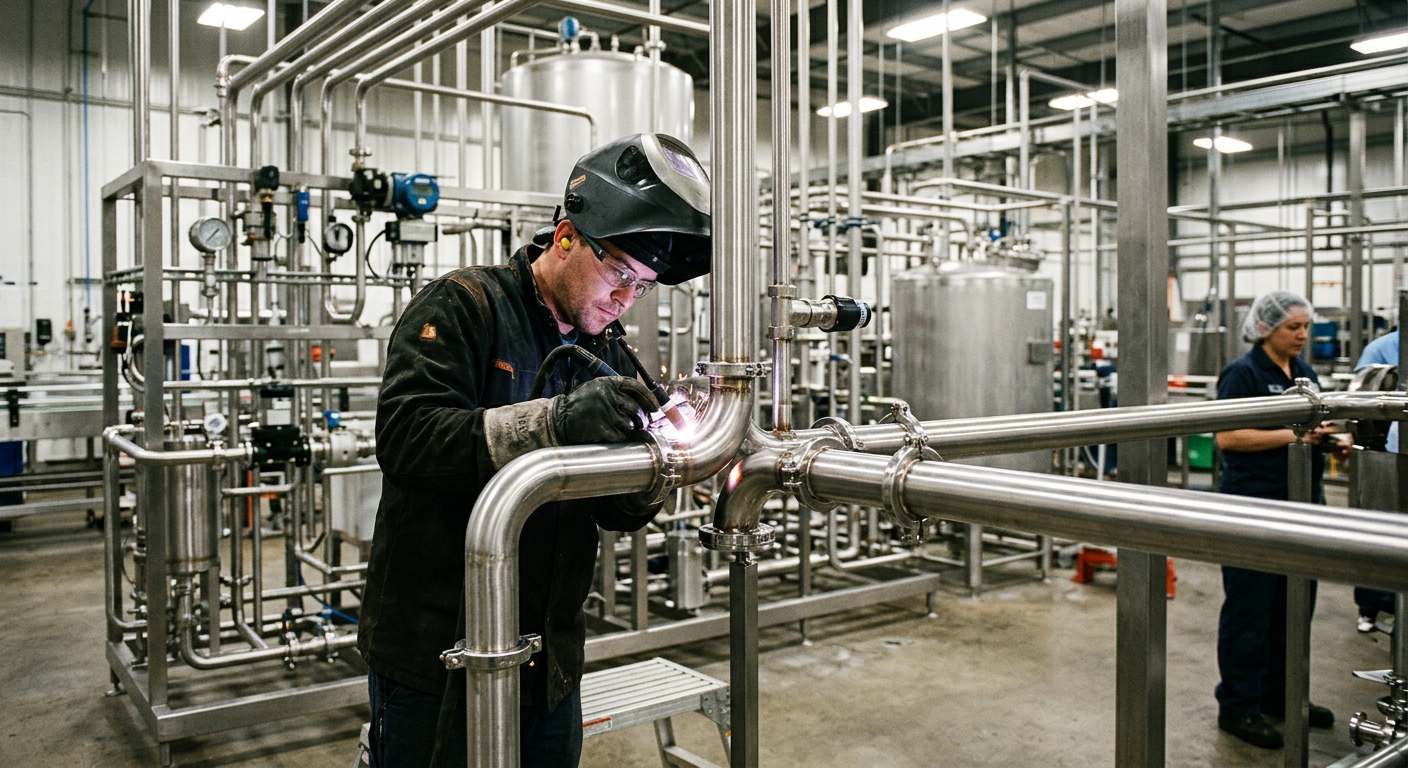
6 Sanitary Design Principles Every Food Plant Must Follow
In the United States, sanitary design is not just a best practice for food plants; it is a risk-control framework that directly affects food safety, operating uptime, audit readiness, labor efficiency, and long-term capital performance. Whether a processor runs a dairy line in Wisconsin, a protein facility in Arkansas, a beverage plant near Atlanta, or a co-packing operation in Southern California, equipment and utility systems must be designed so they can be cleaned effectively, inspected easily, drained fully, and maintained without creating harborage points. The most reliable sanitary systems follow six core principles: cleanability, proper surface finish, corrosion-resistant materials, self-draining geometry, high-quality fabrication, and recognized hygienic compliance. When these principles are backed by structured inspection and maintenance programs, processors reduce contamination risk, shorten changeovers, and support stronger performance under FDA, USDA, SQF, and BRC expectations. Across major U.S. manufacturing corridors such as Chicago, Dallas-Fort Worth, Charlotte, Fresno, Minneapolis, and the I-95 distribution belt, food and beverage producers are upgrading lines to meet tighter customer requirements, labor constraints, and sustainability targets. Sanitary design decisions now influence more than hygiene alone; they shape water use, CIP cycle times, allergen control, product recovery, automation strategy, and even expansion flexibility. For capital projects, the right sanitary standard should be embedded at the earliest concept stage, not added after procurement. That means evaluating vessels, piping, pumps, fillers, heat exchangers, drains, access platforms, controls, and utility routing as a complete processing ecosystem. The six sanitary design principles every U.S. food plant should follow are straightforward: make equipment easy to clean and inspect, specify the correct surface finish, choose materials that resist corrosion and product interaction, eliminate dead legs and standing water through self-draining geometry, hold welds and fabrication to hygienic standards, and verify conformance with recognized sanitary frameworks such as 3-A and EHEDG where appropriate. These design choices should be reinforced by preventive inspection and maintenance protocols. Plants that apply these standards consistently usually see lower contamination risk, better audit outcomes, faster sanitation, and fewer costly interruptions. In practical terms, this applies to a wide range of product types and applications: dairy, cultured products, protein processing, sauces, aseptic beverages, RTD coffee, carbonated soft drinks, kombucha, prepared foods, plant-based proteins, and shelf-stable retort lines. It matters equally in raw receiving, batching, thermal processing, filling, CIP, packaging, and utility support systems. For buyers and plant leaders, the safest purchasing approach is to evaluate sanitary design at the system level instead of comparing equipment only by upfront cost. The table above shows why sanitary design should be treated as an operating strategy rather than a narrow engineering detail. Each principle protects a different failure point, and together they support both food safety and financial performance. The line chart reflects a realistic market pattern seen across the United States: more processors are funding hygienic upgrades because labor savings, customer standards, and risk reduction increasingly justify capital spending. Gulf Coast ports, Midwest dairy hubs, and Southeastern beverage corridors are especially active due to network expansion and co-manufacturing demand. Cleanability is the first and most visible principle of hygienic equipment design. If operators cannot reach, inspect, rinse, or verify a surface, they cannot confidently control contamination. In U.S. plants, cleanability must be considered in both manual cleaning and clean-in-place environments. Product-contact surfaces should be fully exposed to either human access or validated cleaning flow. Guards, covers, housings, supports, and utility drops should not block sanitation crews from seeing and reaching the critical areas where residue accumulates. Accessibility is just as important as cleanability. A perfectly polished tank interior still becomes a sanitation risk if spray devices cannot be inspected, gaskets require extensive disassembly, or platforms make valve clusters difficult to reach. This is why buyers should review access points, door geometry, shadowing, removable components, and safe maintenance clearances during the design phase. In high-throughput U.S. facilities where sanitation windows are tight, inaccessible equipment often drives overtime, rushed procedures, and inconsistent outcomes. Plants in protein-heavy regions such as Nebraska, Iowa, and Georgia often need more aggressive access standards because soils are heavier and the consequences of trapped residue are greater. Beverage operations in California, Texas, and North Carolina may rely more heavily on CIP, but they still need visual inspection access for fillers, blending skids, syrup rooms, and hygienic utilities. The best designs balance enclosed hygienic processing with practical access for validation. This table highlights a useful buying lesson: a sanitary machine should be judged not only when it is new and idle, but also when it is wet, in production, under time pressure, and being cleaned by a real shift crew. That is where hidden access problems become expensive. For capital projects, this is also where integrated engineering matters. Process design, structural supports, piping routes, electrical drops, and controls enclosures must be coordinated so one discipline does not compromise another. Processors seeking a more complete project strategy can review food and beverage engineering services that align sanitary design with layout, utilities, installation, and execution oversight. The bar chart shows strong demand across multiple sectors, with beverage and dairy often leading because of frequent sanitation cycles, SKU complexity, and high customer scrutiny. Co-packers also rank high due to changeovers and contract compliance expectations. Surface finish is a technical topic with direct plant-floor consequences. Rough, pitted, or inconsistent product-contact surfaces can retain soils and encourage biofilm formation. In stainless systems, buyers should specify appropriate roughness values, fabrication methods, passivation practices, and finishing documentation. The right target depends on the product, process, and regulatory environment, but the principle is universal: smoother, well-finished surfaces are easier to clean and less likely to trap residue. In the United States, sanitary surface specifications are especially important in dairy, aseptic, high-acid beverage, and ready-to-eat applications. A processor in Idaho producing cultured dairy and a juice co-packer near Newark may run very different products, yet both need interior surfaces that support repeatable clean-out and withstand chemical exposure. Surface finish must also be consistent across weld zones, fittings, valve seats, and transitions. A highly polished tank shell does little good if the nozzle weld or instrument connection creates a rough, hidden defect. Buyers should review not only the numeric finish requirement but also how it will be measured, verified, and maintained after fabrication. Mechanical polishing, electropolishing, proper weld finishing, and passivation all play a role. The specification should clearly identify which surfaces are product-contact, splash-zone, or non-product-contact because each may need a different treatment. This is a common source of confusion during procurement and one reason why system-level engineering review is valuable. The explanation here is simple: surface finish affects how much force sanitation must apply to remove soil. Better surfaces generally mean more predictable cleaning, lower chemical use, and less rework. As plants push toward 2026, surface science will become even more important. U.S. processors are increasingly interested in digital roughness records, improved passivation verification, and lower-water cleaning strategies. Sustainability goals are now tied to hygienic design because easier-to-clean surfaces reduce rinse time, thermal load, and chemical consumption. Material selection is not merely a stainless-versus-non-stainless question. U.S. food plants must choose metals, elastomers, plastics, coatings, and seal materials that can withstand product chemistry, cleaning chemicals, temperature cycles, abrasion, and mechanical wear without degrading sanitary performance. Corrosion is both a hygiene and reliability problem. Once a surface pits, flakes, cracks, or reacts with cleaning chemicals, sanitation becomes harder and the risk of contamination rises. For many food and beverage applications, properly specified stainless steel remains the default choice, but the correct grade depends on the environment. High-salt sauces, acidic beverages, chloride-heavy sanitation, and coastal locations near ports such as Houston, Savannah, Long Beach, or Newark can create more aggressive corrosion exposure than inland dry-product facilities. Likewise, gasket compounds that work in one dairy process may fail quickly in hot-fill juice or spirit processing. Plants should evaluate material selection based on the full process life cycle: product contact, cleaning regime, thermal expansion, wear points, utility chemistry, and maintenance practices. Mixed metals, incompatible elastomers, and unprotected structural details often become recurring failure points. Good sanitary design therefore includes material traceability, chemical compatibility review, and specification control across both purchased equipment and field-installed components. This table shows why material selection belongs in early buying decisions. The lowest-cost component often becomes the highest-cost lifecycle choice if it degrades under real sanitation conditions. In addition to the equipment itself, utility systems matter. Poor water quality, steam contamination, and incompatible cleaning chemical storage can undermine otherwise well-designed lines. That is why leading processors often partner with firms that understand process systems, utilities, controls, and installation as one integrated hygienic platform rather than separate trades. Self-draining design is one of the most important and most frequently overlooked sanitary principles. Any area where liquid, condensate, or product can stand becomes a potential microbial growth site and can also dilute or contaminate the next batch. In hygienic systems, piping should slope correctly, vessel bottoms should drain fully, branches should be minimized, and dead legs should stay within acceptable limits for the application and cleaning method. Dead zones occur when flow bypasses a branch, fitting, cavity, or recess and leaves trapped material behind. This may happen in instrument tees, oversized headers, poorly located valves, pump casings, or low points created by field installation. A design that looks acceptable on paper can still fail in the field if support spacing changes slope, utility routing introduces sags, or skid placement forces awkward tie-ins. That is why drainage must be validated during installation and commissioning. In U.S. plants with complex product portfolios, self-draining geometry is especially important for allergen changeovers, aseptic processing, and high-value product recovery. A plant in Minnesota producing cultured dairy and one in Southern California blending functional beverages both benefit when lines empty predictably and CIP circuits do not retain caustic or rinse water. Self-draining geometry protects food safety while also reducing waste. The area chart reflects a strong design trend: U.S. processors are moving from minimum-compliance layouts toward fully drainable systems that also support product recovery, water efficiency, and faster startup after cleaning. This table explains why self-draining design should be verified after installation, not assumed from fabrication drawings alone. Many dead zones are created during field execution rather than original equipment manufacturing. For plant expansions, the buying advice is clear: ask equipment and engineering partners to demonstrate drainage philosophy before procurement. Require slope details, valve orientation logic, drain maps, and field acceptance checks. This is particularly important for processors near major trade hubs where rapid production growth often forces phased installations and future tie-ins. Even the best sanitary concept can be undermined by poor weld execution. Hygienic welds should be smooth, fully fused, and free of pits, cracks, crevices, excessive oxidation, and abrupt internal transitions. Fabrication quality matters on tanks, tube welds, custom manifolds, CIP skids, and structural components exposed to washdown. Inferior welds are common sources of repeat contamination, failed inspections, and early asset degradation. For U.S. processors, fabricated sanitary systems often include a mix of shop-built and field-installed elements. This is where standards, documentation, and contractor oversight become critical. Tube preparation, purge control, filler selection, polishing, passivation, and inspection should all be governed by written procedures. Buyers should also verify whether field welders and fabricators have direct experience with sanitary food and beverage systems rather than general industrial piping only. Fabrication quality affects much more than sanitation. Clean internal welds improve flow, protect pump performance, reduce fouling, and support more consistent heat transfer. Exterior fabrication also matters because poor bracket design, open tube ends, flat ledges, and unfinished supports can trap water and create environmental contamination points around process areas. The lesson from this table is that fabrication standards need to be contractual, measurable, and enforced. Hygienic quality cannot be left to assumption. Case experience across the U.S. market shows that plants gain the best results when engineering, fabrication, installation, and startup are coordinated. On fast-track projects, rushed field modifications often create the very sanitary defects a processor was trying to avoid. Reviewing prior food and beverage project case studies can help buyers evaluate whether a partner has successfully executed hygienic systems under real production pressure. Recognized sanitary standards provide an external framework for design and evaluation. In the United States, 3-A Sanitary Standards are widely used in dairy and other hygienic processing applications, while EHEDG guidance is often referenced for broader hygienic engineering principles, especially by multinational processors or facilities influenced by global validation expectations. These frameworks do not replace sound engineering judgment, but they provide a valuable benchmark for equipment design, cleanability, and component selection. Processors should not treat compliance logos as a shortcut. A line can contain certified components and still perform poorly if installed with dead legs, inaccessible valves, or incompatible utility connections. The right approach is to use 3-A, EHEDG, and plant-specific standards as part of a layered sanitary design review. That includes equipment selection, piping geometry, fabrication quality, CIP strategy, and maintenance access. U.S. manufacturers with export ambitions or multinational ownership often benefit from designing to a broader hygienic standard than local minimums. This is common in dairy, infant nutrition, functional beverages, aseptic products, and premium prepared foods. In 2026 and beyond, processors should expect greater digital documentation, more traceable hygienic validation, and stronger sustainability links between sanitary design and resource efficiency. The comparison chart shows how U.S. buyers increasingly rank drainability, fabrication quality, and documentation above simple purchase price. That reflects a more mature market where long-term operating results drive procurement decisions. When comparing suppliers, local support also matters. Manufacturers around Milwaukee, St. Louis, Kansas City, Charlotte, and Sacramento often prioritize regional service access for startup support and replacement parts. Still, national project execution matters just as much for multi-site companies operating across all 50 states. Sanitary design is only successful if it remains sanitary over time. Inspection and maintenance programs are what preserve the original design intent. Gaskets wear, valve seats erode, supports settle, spray devices clog, instrumentation is replaced, and field fixes can create unintended dead zones. A plant that invests in excellent hygienic design but neglects preventive verification eventually loses its advantage. Effective protocols should include routine visual inspections, borescope checks where appropriate, gasket and seal replacement intervals, weld condition reviews, passivation tracking, drainage verification, and CIP performance trending. Maintenance teams should document not only failures but also sanitary observations that could affect cleanability. For example, a replacement sensor installed with a longer branch connection may look acceptable mechanically while creating a new hygienic dead leg. Plants should also connect maintenance with sanitation data. Rising rinse conductivity time, increased chemical usage, recurring ATP failures, slower heat transfer, or frequent re-clean events often indicate a design or maintenance issue rather than a sanitation labor problem. This integrated view becomes increasingly important as U.S. plants adopt more automation, digital work orders, SCADA trend review, and predictive maintenance tools. The explanation is direct: maintenance preserves hygienic performance, and data helps identify when a system is drifting from its design assumptions. Plants that combine engineering review with sanitation metrics are usually faster at correcting risk before it becomes a product issue. Future trends for 2026 include broader use of digital twins for hygienic layouts, AI-assisted maintenance planning, smarter inline sensors, and sustainability-oriented CIP optimization. Policy pressure around water use, wastewater loading, and energy efficiency is also pushing U.S. processors toward sanitary systems that clean better with fewer resources. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a business-first engineering approach that connects sanitary design to production economics. Rather than treating hygienic compliance as a checklist, the company works to align plant layout, process capability, installation strategy, and long-term operating performance so clients can invest capital more intelligently. From a technological capability standpoint, DPS brings process, mechanical, structural, electrical, plumbing, and controls expertise into one project framework. Its team supports automation, PLC programming, SCADA integration, utility coordination, process line design, and commissioning for product categories ranging from brewing, spirits, RTD beverages, and dairy drinks to proteins, sauces, prepared foods, aseptic systems, and retort operations. That multi-discipline capability is important because sanitary performance often depends on how controls, utilities, equipment, and field installation work together. From a manufacturing capability standpoint, DPS also supports proprietary process equipment solutions, including sanitary tanks, CIP systems, marination tumblers, and cooking vessels. That practical equipment perspective helps the company evaluate how fabrication details, accessibility, drainability, and maintenance realities affect total project success. Companies reviewing integrated sanitary equipment options can explore process equipment capabilities for a better sense of how engineered components fit into complete plant systems. From a service capability standpoint, DPS operates through a design-build-manage model that helps clients move from planning to execution with stronger control over scope, schedule, and sanitary outcomes. Services include process engineering, capital planning, owner’s representation, project management, system integration, and general contractor coordination where applicable. For manufacturers that want a partner able to assess current-state sanitary risk, support expansions, or build new process capacity, learn more about the company and how it approaches profitable, execution-focused projects. This model is particularly valuable in U.S. markets where speed matters but sanitary compromise is unacceptable, such as co-packing corridors in the Southeast, dairy belts in the Upper Midwest, and beverage growth zones in Texas and California. A well-run sanitary capital project protects more than compliance; it protects margin, uptime, and customer confidence. What is the most important sanitary design principle for a food plant?Cleanability is usually the starting point because every other sanitary decision supports the ability to remove soil and verify that removal. However, true hygienic performance depends on all six principles working together. Do all U.S. food plants need 3-A or EHEDG compliance?Not every plant needs formal adherence to both frameworks, but many benefit from using them as design references. Dairy and high-hygiene applications often rely more heavily on 3-A, while global or advanced hygienic programs may also reference EHEDG concepts. How can buyers compare sanitary equipment suppliers?Look beyond price. Compare cleanability, drainability, weld documentation, material traceability, spare part support, maintenance access, FAT and SAT standards, and the supplier’s experience in your product category. Also confirm whether the supplier can coordinate with site utilities and controls. Why do dead legs matter so much?Dead legs trap product, rinse water, or chemicals in stagnant zones where cleaning flow is limited. They increase contamination risk and can create product quality variation, especially during changeovers or startup. What industries in the United States benefit most from strong sanitary design?All food and beverage sectors benefit, but the impact is especially high in dairy, meat and poultry, prepared foods, sauces, aseptic processing, brewing, spirits, functional beverages, and co-packing operations with frequent SKU changes. How often should sanitary equipment be inspected?Frequency depends on the process, soil load, and production hours. Critical items such as gaskets, spray devices, valve internals, and drainage conditions should be checked on a recurring preventive schedule and reviewed whenever sanitation performance trends shift. Is sanitary design only about product-contact surfaces?No. Non-product-contact areas such as frames, platforms, supports, enclosures, and drainage zones also matter because they can harbor moisture, debris, and environmental contamination that affects the process area. What should U.S. plants prioritize in 2026?Plants should prioritize hygienic layouts that reduce water and chemical use, improve digital traceability, support predictive maintenance, and stay flexible for future product changes. Sanitary design is becoming a sustainability and profitability issue as much as a compliance issue. -
Flexible Food Manufacturing Plant Design: Engineering Multi-Product Facilities for the Future
Flexible food manufacturing plant design in the United States is no longer a niche strategy. It is becoming the preferred approach for processors that need to switch between SKUs, package formats, batch sizes, and even product categories without rebuilding the facility every few years. A well-designed multi-product plant supports faster commercialization, stronger margin protection, better use of capital, and lower exposure to market volatility. For U.S. manufacturers serving retailers, foodservice chains, private label programs, and contract customers, flexibility is now directly tied to profitability. From Chicago and Dallas to Charlotte, Fresno, Atlanta, and the Inland Empire, food producers are facing the same pressure: more product variety, shorter runs, tighter labor markets, higher utility costs, and stricter food safety requirements. The best answer is not just buying more equipment. It is designing the plant around changeovers, utility adaptability, sanitation logic, floor loading, automation, and future expansion from day one. For companies evaluating a new build, expansion, retrofit, or co-packing model, a partner with process, utility, controls, and project delivery expertise matters. Disruptive Process Solutions works across North America as a food and beverage engineering partner focused on profitable capital projects, helping manufacturers align plant design with commercial goals rather than treating the building as a stand-alone construction exercise. A flexible food plant is engineered to run multiple products, recipes, and formats with minimal downtime, controlled contamination risk, and scalable utilities. In the U.S. market, the most effective flexible facilities share six characteristics: These plants are especially valuable for sauces, dressings, seasonings, dairy, plant-based foods, proteins, beverages, aseptic products, prepared foods, and contract manufacturing environments. In most cases, the business case is strongest where SKU churn is high, customer requirements change frequently, or growth depends on adding adjacent categories rather than scaling one legacy product forever. The table above shows why flexible design is more than an architectural preference. Each feature supports a financial outcome, whether through faster launches, safer operations, or lower retrofit costs. In the United States, food demand is stable in aggregate but volatile by category, pack size, channel, and region. Consumer shifts toward better-for-you snacks, protein-rich meals, premium sauces, functional beverages, and convenience foods can move quickly. At the same time, private label expansion, retailer consolidation, and foodservice menu cycles make forecasting more difficult. A rigid plant optimized for one product family often struggles when volume migrates elsewhere. Flexible plants solve that problem by giving operators portfolio options. Instead of being locked into one line architecture, manufacturers can move capacity toward the products with the strongest margins or most resilient demand. That matters in freight-sensitive geographies such as Southern California, New Jersey, Houston, and the Midwest distribution belt, where market access can shift due to retailer strategy, labor conditions, or port activity. For example, a processor originally designed around refrigerated dressings may later add shelf-stable sauces, marinades, or dairy-adjacent emulsions. A plant-based protein facility may evolve into prepared meals. A beverage co-packer may add aseptic, hot fill, or carbonation capabilities over time. Facilities with utility headroom, adaptable rooms, and controls flexibility can monetize these shifts faster. That is why many investors and operating teams now evaluate food plants less like fixed-purpose factories and more like strategic manufacturing platforms. A building that can support multiple product families becomes a commercial hedge. The chart illustrates a realistic upward trend in U.S. investment interest for flexible food plants as processors pursue resilience, capacity optionality, and faster product turnover. When buying or designing a plant, executives should ask one core question: will this facility still fit our portfolio in five to ten years if our top products change? If the answer is uncertain, flexibility deserves a premium. Many food companies want one site to support both wet and dry production, but this is only practical when zoning, air handling, sanitation methods, and material flow are designed correctly. Hybrid production is common in seasonings plus sauces, bakery ingredients plus fillings, dairy powders plus cultured products, and meat processing plus dry rub or coating operations. The challenge is that wet rooms and dry rooms behave differently. Wet processing usually demands washdown construction, drainage, hygienic utility drops, and moisture-tolerant finishes. Dry mixing areas prioritize dust control, humidity management, explosion considerations where applicable, and protection against moisture migration. If these environments are casually combined, operators often create sanitation conflicts, condensation issues, and cross-contact risks. The best hybrid plants use controlled transitions: separate corridors, gowning logic, pressure cascades, dedicated handwash and sanitation stations, and carefully planned ingredient staging. Often, the receiving and warehouse logic must also support distinct ingredient classes, from powders and spices to oils, dairy inputs, and frozen components. In practical terms, a U.S. plant near Kansas City or Memphis might receive dry ingredients by super sack and also manage chilled liquid ingredients for blended prepared foods. A hybrid layout allows both while keeping wet cleaning patterns from compromising dry material handling areas. The table highlights why hybrid plants require room-by-room engineering rather than generic “open floor” concepts. A facility can support both wet and dry operations, but only when each environment is deliberately protected from the other. Utilities are often the true bottleneck in flexible manufacturing. Product lines can be changed or replaced, but if the steam system is undersized, the chilled water loop has no spare capacity, or the HVAC design cannot maintain room conditions after a process shift, expansion becomes expensive and disruptive. In multi-product food plants, utilities should be designed as scalable platforms. That means evaluating not only current loads but future peak diversity across heating, cooling, compressed air, process water, wastewater, CIP, and electrical distribution. It also means designing distribution paths that can be extended without tearing through production. Steam remains central for kettles, blanching, sterilization, cooking, clean-in-place heating, and hot water generation. Refrigeration or glycol systems are equally critical for dairy, beverage, protein, and prepared food operations. HVAC plays a major role in condensation control, room pressurization, temperature consistency, odor management, dust control, and shelf-life protection. DPS is especially relevant here because its technical capabilities span structural, mechanical, plumbing, electrical, process, controls, PLC programming, and SCADA integration. That matters when a facility needs utility planning tied directly to process behavior rather than designed in isolated silos. Learn more about these integrated offerings through its engineering and project services. For buying advice, U.S. owners should ask for utility master planning, not just equipment hook-up design. In cities with high energy costs like Los Angeles, Boston, and parts of the Northeast, utility efficiency can materially affect operating margin. In regions with faster industrial growth like Texas, Tennessee, and the Carolinas, expansion-ready infrastructure can shorten time to revenue. One of the most practical ways to build flexibility is to reduce dependence on permanent line geometry. Mobile tanks, modular skids, quick-connect process piping, roll-in depositor systems, movable conveyors, and flexible packaging cells give operators the ability to reshape production around demand. This approach works particularly well in high-mix environments producing sauces, soups, fillings, marinades, cultured dairy, beverage concentrates, and specialty batches. It is also effective in R&D-to-commercial transition models where products scale before a dedicated line is justified. Reconfigurable cells should not be confused with temporary setups. Good design still requires hygienic utility interfaces, drain planning, hose management, line clearance procedures, validation protocols, and digital recipe controls. The goal is controlled adaptability, not improvised manufacturing. DPS also brings manufacturing capabilities to these projects through its own branded process equipment line, including tanks, CIP systems, marination tumblers, and cooking vessels. For manufacturers seeking equipment that integrates with broader plant design, that combination of equipment knowledge and facility integration can reduce coordination gaps. More on available systems can be found at process equipment solutions. The bar chart shows where flexible layouts are especially valuable. Prepared foods, beverages, and sauces often lead because their product development cycles and customer demands change quickly. Future-proofing starts with the building shell. Too many food plants are forced into expensive workarounds because structural decisions were made for the first process only, not the next three generations of process. Column placement, slab loading, roof support, utility racks, and clear height all determine whether the plant can absorb larger vessels, mezzanines, overhead piping, robotic palletizing, or automated storage systems later. Column-free or long-span spaces are particularly valuable in blending, filling, packaging, warehousing, and co-packing zones. They allow production cells to be moved, enlarged, or replaced with less disruption. Floor loading matters wherever brine tanks, silos, kettles, retorts, water treatment systems, mezzanines, or dense automated packaging equipment may be added. Ceiling height becomes critical when process lines require top-entry access, elevated ingredient systems, can conveyors, ductwork, or future warehouse automation. For example, a plant near Savannah or Newark serving import-driven ingredients and East Coast retail distribution may initially run standard packaged sauces. Three years later, it may need mezzanine-mounted dry ingredient handling, tote dumpers, automated palletizing, and larger vessel farms. If structure and height were underspecified, the plant loses speed and incurs major retrofit cost. The key buying advice here is simple: spend more effort on irreversible building decisions. Equipment can be replaced. Poor structure is much harder to fix. Flexible plants often gain commercial reach by producing a broader set of products, but that can increase allergen complexity. In the U.S., allergen control has direct implications for labeling, sanitation validation, customer audits, scheduling, and recall exposure. The core design decision is whether to use dedicated equipment, shared equipment with validated cleaning, or a hybrid model. Dedicated systems usually make sense where allergens are highly potent, customer expectations are strict, or cleaning validation is costly and slow. Shared systems are viable when sanitary design is strong, CIP or COP procedures are validated, and production sequencing is disciplined. Many successful plants use dedicated minor ingredient handling for allergens while sharing core batching or packaging assets. Physical layout matters just as much as equipment strategy. Warehousing, weighing rooms, traffic routes, hose storage, tool control, drain design, and air movement can all influence allergen risk. Dry allergen powders deserve particular attention because airborne migration can compromise adjacent production. DPS frequently supports regulated food and beverage environments with compliance awareness spanning FDA, USDA, SQF, and BRC project needs, which is especially important when designing flexible operations where audit readiness and practical throughput must coexist. The area trend suggests that more U.S. plants are moving toward validated shared systems where commercially sensible, though dedicated allergen infrastructure remains critical in many categories. For many U.S. processors, the right answer is not “all dedicated” or “all shared.” It is a risk-based segmentation model aligned to product portfolio, customer requirements, sanitation capability, and growth plans. Automation in flexible food plants is less about maximum speed and more about repeatable change. High-mix, low-volume environments benefit from control systems that can manage recipes, ingredient verification, batch sequencing, CIP routines, line clearance, downtime tracking, and operator prompts. Robotics then adds value where repetitive packaging, palletizing, loading, sorting, or case handling would otherwise consume labor and create bottlenecks. The strongest automation programs connect process data to business outcomes. That includes yield monitoring, utility consumption by batch, sanitation cycle verification, genealogy, and OEE visibility. Plants running many SKUs need to know exactly where time is being lost during changeovers and which product families are most profitable. Because DPS combines controls engineering, PLC programming, automation, and SCADA with process and utility design, it can support facilities where software and infrastructure must be planned together. This is especially important in plants where production gains may come from logic improvements rather than major capital spend. By 2026, three trends are likely to accelerate in the U.S. market: broader use of recipe-driven manufacturing execution layers, more robotic end-of-line cells sized for mid-volume operations, and stronger sustainability reporting tied to utility and waste data at the batch or SKU level. Policy pressure around energy use, water management, refrigerant practices, and traceability will also push plants toward better digital visibility. Co-packing is one of the clearest business cases for a flexible plant. A contract manufacturer must absorb shifting customer mixes, varied batch sizes, diverse packaging needs, and uneven launch timelines. A facility designed for only one product architecture will struggle to win or keep business. In the U.S., co-packing demand is especially strong around major logistics corridors, consumer population centers, and ingredient hubs. Areas such as Dallas-Fort Worth, Indianapolis, Central California, the Carolinas, and parts of Pennsylvania remain attractive because they combine access to labor, trucking, suppliers, and downstream markets. Successful flexible co-packing plants generally share several features: adaptable batching and filling, broad utility capability, smart warehouse and staging flow, robust quality systems, and clear commercial rules for sanitation, allergen changeover, and scheduling. Margin performance often depends on how fast the facility can onboard new products without disrupting existing customers. A good real-world model is a growth-oriented beverage or food co-packing facility designed with staged capacity. DPS has experience on large-scale manufacturing projects of this type, including facilities built around first-year profitability and long-term expansion logic. For examples of how engineering decisions translate into business results, visit the project case studies page. The comparison chart reflects what many U.S. manufacturers now prioritize when selecting design-build and integration partners for flexible food plants: not just construction ability, but combined strength in process, utilities, controls, and growth planning. Local supplier strategy also matters. Near ports such as Long Beach, Savannah, Houston, and Newark, global ingredient and packaging access can support broader product portfolios. In agricultural and protein regions such as Iowa, Nebraska, Arkansas, and the Central Valley, raw material proximity can shape the product mix a flexible plant should target. Buying decisions should consider not only customer demand but inbound supply resilience. When choosing a partner, many owners prefer firms that can bridge service capabilities across feasibility, capital planning, owner’s representation, project management, general contracting support, installation, and commissioning. That full-lifecycle approach lowers handoff risk and helps align schedule, cost, and operational readiness. DPS positions itself in that lane through its design-build-manage model, combining engineering, execution oversight, and hands-on integration with a strong focus on project profitability. Industries that benefit most from flexible plants include beverage, dairy, protein processing, prepared foods, sauces and dressings, aseptic and retort products, plant-based foods, and specialty ingredients. Common applications include pilot-to-commercial scaling, multi-SKU private label production, co-packing growth, regional manufacturing hubs, and facility consolidation after acquisition. Ultimately, the U.S. market rewards plants that can do more than produce. They must adapt, protect quality, manage utilities intelligently, and support business evolution. Flexible design is how manufacturers future-proof both operations and capital. What is a flexible food manufacturing plant?It is a facility designed to run multiple products, recipes, package formats, or production models with less downtime and lower retrofit cost than a dedicated single-purpose plant. When does flexibility justify higher upfront capital?Usually when a company has high SKU turnover, uncertain future demand, co-packing ambitions, private label exposure, acquisition-driven portfolio changes, or plans to enter adjacent product categories. Can one plant safely handle both wet and dry food production?Yes, but only with correct zoning, air management, sanitation design, drainage, material flow control, and allergen risk management. Hybrid production requires deliberate engineering. Which utilities should be oversized or future-ready?Common priorities include steam, refrigeration or glycol, HVAC, compressed air, electrical distribution, CIP, and wastewater handling. These systems are often the hardest and costliest to expand later. Are mobile process skids a good idea for food plants?Yes, especially for high-mix environments, pilot-to-commercial growth, and co-packing. They work best when supported by hygienic quick-connect utilities, validated procedures, and recipe-based controls. How should allergens be handled in a flexible facility?Use a risk-based strategy combining dedicated and shared systems where appropriate. Consider product type, cleaning validation, airborne risk, customer standards, and scheduling complexity. What automation is most useful in high-mix, low-volume production?Recipe management, batch control, traceability, CIP automation, downtime tracking, robotic palletizing, and digital changeover support often create the strongest returns. Why are column-free space and floor loading so important?They preserve future options. As products change, plants may need larger tanks, mezzanines, packaging cells, robotics, or additional utility infrastructure. Structural constraints can block that growth. What should U.S. companies look for in an engineering partner?Look for integrated expertise in process, utilities, controls, food safety, construction execution, and expansion planning. A partner should understand the business model, not just the equipment list. How does DPS fit into flexible plant projects?DPS supports food and beverage manufacturers across the United States and Canada with engineering, capital planning, integration, equipment, project execution, and compliance-aware design. Its strength is aligning manufacturing design with profitability, scalability, and real operational outcomes.


