-
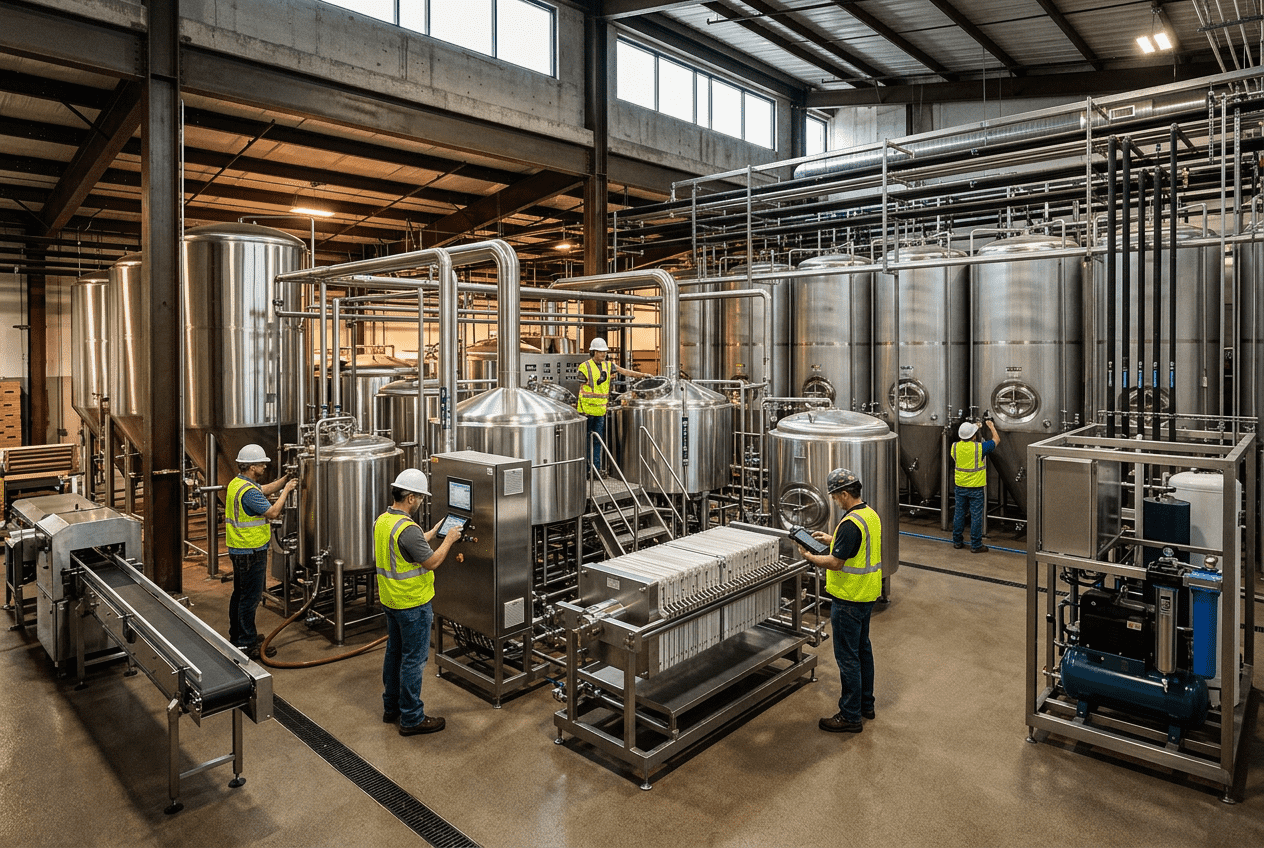
Ready-to-Drink Beverage Manufacturing Solutions
Ready-to-drink beverage manufacturing in the United States requires more than a filler and a formula. Successful RTD programs depend on water treatment, ingredient handling, thermal processing, packaging selection, microbiological control, cost discipline, and a facility layout designed for profitable scale. Whether a brand is launching canned cold brew in Austin, shelf-stable protein shakes in Chicago, juice blends near the Port of Los Angeles, or functional beverages distributed through New Jersey and Atlanta, the best results come from aligning product design with processing technology, distribution realities, and capital planning from day one. RTD beverage manufacturing solutions combine process engineering, batching, thermal treatment, filling, packaging, utilities, automation, quality assurance, and distribution planning into one integrated production model. In the United States, the right solution depends on product acidity, ingredients, desired shelf life, sales channel, expected run rate, and whether the brand will use a contract manufacturer or build in-house capacity. For most brands, the fastest path to market is to validate the formulation, processing method, and packaging format before making major capital commitments. For growing operators and co-packers, the highest-value investment is usually not a single machine but a well-designed system: syrup rooms, CIP, pasteurization or aseptic capability, tankage, utilities, controls, and plant flow that support both current volumes and future expansion. Manufacturers evaluating new capacity often benefit from working with a partner that understands both engineering and commercial performance. Disruptive Process Solutions approaches these projects from a profitability-first perspective, helping food and beverage operators structure smart capital programs rather than simply buying equipment in isolation. The RTD manufacturing process begins with water, because water quality affects flavor, microbiological risk, process consistency, and equipment life. In the United States, many facilities treat municipal or well water with carbon filtration, softening, reverse osmosis, UV disinfection, and ozone or other sanitizing methods depending on the beverage profile. A sports drink line in Phoenix may prioritize mineral consistency and taste neutrality, while a tea bottler in North Carolina may balance flavor retention with local source characteristics. After water treatment, ingredients move into a controlled batch preparation environment. This can include dry ingredient handling, liquid ingredient receiving, syrup blending, hydration, heating, high-shear mixing, inline metering, homogenization, deaeration, and carbonation where needed. Product is then routed to the relevant processing step such as HTST pasteurization, tunnel pasteurization, retort, or aseptic sterilization and fill. Once filled into cans, PET, glass, cartons, or pouches, the beverage is coded, inspected, packed, palletized, and released based on QA protocols. Each step has to support not only food safety but also throughput and line efficiency. In high-volume U.S. markets like Southern California, Dallas-Fort Worth, and central Pennsylvania, the biggest hidden losses often come from poor material flow, undersized utilities, changeover delays, and weak integration between process and packaging systems. The table above shows why RTD production should be engineered as a continuous system rather than a collection of disconnected machines. A line may have enough filler speed on paper but still underperform if upstream batching, CIP recovery, or cooling capacity is weak. One of the most important choices for an RTD brand is whether to work with a co-packer or build internal manufacturing. Contract manufacturing can lower initial capital exposure, accelerate launch timing, and provide access to specialized process capabilities such as aseptic packaging or retort. This approach is often ideal for emerging brands selling through regional grocery, convenience, or direct-to-consumer channels. In-house production makes sense when volume is stable, margins justify capital investment, proprietary process control matters, or the product portfolio is too complex for shared-line scheduling. Companies distributing through major U.S. chains from Miami to Seattle often move to owned production when freight costs, service requirements, and speed-to-market outweigh co-packing flexibility. The right decision depends on product complexity, minimum run sizes, warehousing strategy, geographic reach, quality requirements, and tolerance for operational risk. Brands with dairy-based, low-acid, or particulate-containing drinks may find that suitable contract capacity is limited. In those cases, a structured engineering review and phased capital plan can create a better long-term outcome. For companies considering plant expansion, utility upgrades, or a new production line, process engineering and capital planning services can clarify the true bottlenecks before money is committed. Sometimes the most profitable answer is new capacity; other times it is controls optimization, better CIP sequencing, or a redesigned tank farm. This comparison is most useful when matched to actual distribution lanes and channel economics. For example, a brand shipping from a Midwest co-packer to West Coast natural retailers may discover freight is eroding margin faster than expected. In-house production near inland hubs like Kansas City or Memphis can improve reach, while coastal sites near Long Beach, Savannah, or Newark may better support import-heavy ingredient programs. Processing technology determines shelf life, product quality, packaging options, and plant complexity. Acidified beverages, teas, juices, dairy beverages, plant-based drinks, and functional RTDs all have different microbial and stability demands. The four most common approaches are pasteurization, UHT, aseptic processing, and retort. HTST and flash pasteurization are common for products that will be hot-filled or rapidly filled after heat treatment. Tunnel pasteurization is widely used in packaged beverages, especially in glass and cans. UHT extends shelf life by heating product at very high temperature for a short time, but it is most effective when paired with aseptic handling and filling. Retort is valuable for highly shelf-stable packaged products, especially where particulates, dense formulas, or certain food-service applications are involved. The right technology is not simply the most advanced one. It is the one that fits the beverage, the package, the sales channel, and the economics. A low-acid protein shake sold nationally through ambient distribution may justify UHT and aseptic fill. A refrigerated kombucha line in Portland may be better served by different process controls. A nutraceutical beverage in glass for specialty retail may fit tunnel pasteurization better than aseptic conversion. The chart below illustrates how U.S. demand for processing methods differs by category. Shelf-stable nutrition and functional products continue to shift demand toward aseptic and UHT, while premium refrigerated categories keep HPP and chilled pasteurized systems relevant. On the technology side, DPS supports beverage systems that include pasteurization, UHT, retort, aseptic integration, filtration, carbonation, inline Brix control, water treatment, automation, and SCADA. This breadth matters because beverage projects fail when thermal systems, utilities, controls, and packaging are designed separately instead of as one operating platform. Ingredient handling is where many RTD lines gain or lose efficiency. Functional beverages, energy drinks, coffee-based RTDs, dairy alternatives, and enhanced waters often use a mix of powders, sweeteners, acids, flavors, concentrates, vitamins, emulsions, and stabilizers. These materials require appropriate receiving, storage, metering, hydration, and allergen or sanitation controls. Dry handling systems should reduce dust, improve operator safety, and support accurate dosing. Liquid ingredient systems should account for viscosity, temperature sensitivity, tote or drum changeovers, and transfer sanitation. For emulsified or protein-rich products, high-shear mixing and homogenization become essential. For sugar-reduced beverages, sweetener sequencing and flavor masking can affect both batch consistency and sensory quality. Batch preparation also has to support repeatability across shifts and plants. Load cells, recipe automation, inline Brix monitoring, conductivity tracking in CIP, and historian data allow managers to reduce giveaway and tighten specifications. In busy co-packing regions such as the Midwest and Southeast, these controls often separate profitable plants from plants that appear busy but suffer from chronic yield loss. When manufacturers need purpose-built tanks, CIP skids, or integrated process components, custom process equipment solutions can be a practical way to align equipment with the actual formulation and sanitation demands of the line. This table highlights a recurring issue in RTD operations: the formulation may be excellent in the lab but unstable in production if ingredient handling was not engineered for real run conditions. Scale-up should always include mixing energy, residence time, heat history, and cleanability. Quality assurance is not a final inspection task; it is a design discipline. RTD beverage QA in the United States must align formulation, processing, packaging, sanitation, environmental monitoring, release criteria, and regulatory expectations. Microbial testing should fit the product type and hazard profile. Shelf-life studies should evaluate not only microbiological stability but flavor drift, separation, color change, nutrient retention, carbonation, and package interaction over time. Brix control is especially important in sweetened, juice-based, and concentrate-driven products because even small deviations affect taste, nutrition panels, and cost of goods. Inline Brix instruments, calibrated lab checks, and robust recipe control can reduce variability. In functional beverages, pH and active-content verification often matter just as much. For shelf-stable products, validation should include challenge studies where appropriate, process authority review, thermal mapping, closure integrity, and warehouse simulation. This is especially important for brands shipping across varied climates from Florida humidity to Arizona heat to upper Midwest winter conditions. DPS has experience supporting FDA, USDA, SQF, and BRC-driven environments, which matters for operators building systems that need to pass audits, maintain sanitation integrity, and scale cleanly across product lines. The explanation behind these controls is straightforward: every QA variable is tied directly to margin. A rejected batch, a short shelf life, or excessive product giveaway can erase the value of a seemingly efficient line. Packaging selection shapes not only consumer appeal but also processing method, freight profile, retailer acceptance, and sustainability performance. Cans remain strong for sparkling waters, cocktails, coffee, tea, and energy beverages because they stack efficiently, chill quickly, and fit convenience and club channels. PET is still common for juices, teas, and still beverages, although recycling expectations continue to influence resin selection and lightweighting. Aseptic cartons are attractive for ambient nutrition and plant-based drinks, especially in grocery and food-service channels. Glass can support premium positioning but adds freight cost and breakage risk. Flexible pouches may fit certain kids, sports, or value formats but require careful compatibility assessment. Distribution channel matters. A single-serve bottle for c-store in Houston may not be the right format for e-commerce fulfillment in California or club multipacks in the Midwest. Warehouse temperature, pallet pattern stability, retailer shelf dimensions, and returns handling all affect the final choice. Below is a comparison chart showing relative market attractiveness by packaging type for broad U.S. RTD distribution use cases. Manufacturing capability must match packaging ambition. DPS supports complete system integration from process utilities and controls to physical installation, which is particularly valuable when a beverage producer is adding a new package format without disrupting existing operations. Three trends are reshaping the U.S. RTD landscape: shelf-stable, sustainable, and single-serve. Shelf-stable products continue gaining traction because they simplify distribution, reduce cold-chain cost, and open national retail reach. This is driving interest in UHT, aseptic, retort, and improved ambient packaging formats. Sustainability is influencing both engineering and procurement. Manufacturers are under pressure to reduce water consumption, chemical use, packaging weight, utility intensity, and waste. In 2026, the strongest plants will combine efficient CIP recovery, heat recovery, smart compressed air management, recyclable or reduced-material packaging, and better production scheduling to cut changeover waste. Single-serve remains powerful because U.S. consumers value portability, portion control, and convenience. This trend is particularly strong in convenience stores, airports, stadiums, campus retail, and grab-and-go grocery environments. Cities like New York, Chicago, and Los Angeles continue to reward fast-moving single-serve formats, especially in functional hydration, energy, coffee, and protein categories. Policy and market trends are also shaping the future. Extended producer responsibility discussions, stricter sustainability reporting, retailer packaging standards, and growing scrutiny of ingredient claims will push beverage producers to invest in traceability, automation, efficient utilities, and better package design. The area chart shows why future-ready RTD manufacturing in the United States is less about one trend and more about convergence. The plants that win will be flexible enough to produce shelf-stable products, efficient enough to meet sustainability goals, and agile enough to serve high-velocity single-serve channels. RTD profitability depends on more than unit conversion cost. The full cost structure includes ingredients, packaging, labor, utilities, quality testing, sanitation chemicals, downtime, changeover loss, freight, warehousing, spoilage, depreciation, and working capital. In many U.S. beverage operations, packaging is the largest single cost element after ingredients, followed by labor and utilities depending on the process type. Aseptic and UHT systems can improve distribution economics by eliminating refrigeration and extending shelf life, but they require higher capital and technical discipline. Retort adds flexibility in some applications but can influence package cost and throughput. Hot fill and conventional pasteurized systems may be more economical for certain acid products at regional scale. Plant design has a direct effect on margin. Poor equipment placement increases labor. Inadequate tankage creates filler starvation. Weak automation increases giveaway. Underbuilt utilities reduce uptime. A properly engineered project often produces profit gains that far exceed the savings from choosing the cheapest equipment vendor. This is where DPS is differentiated operationally. Its approach combines design, build, and execution management with a business-minded view of capital efficiency. The firm works across North America on beverage, food, aseptic, and process utility projects, helping manufacturers plan facilities that can reach first-year profitability instead of becoming expensive bottlenecks. This table is a reminder that the cheapest manufacturing option is not always the most profitable one. Freight from one side of the country to the other, especially for heavier glass or low-cube formats, can quickly erase savings from lower copacking rates. Manufacturers seeking evidence of how integrated project execution performs in the field can review selected process and facility case studies that reflect practical challenges such as utility infrastructure, layout optimization, and scalable beverage operations. The best method depends on pH, formulation, particulates, shelf-life target, package type, and distribution model. Acid beverages may fit pasteurization or hot fill, while low-acid dairy or plant-based products often need UHT with aseptic handling. Usually when annual volume is high enough to support equipment utilization, margins are compressed by co-packing and freight, or the brand needs tighter quality and scheduling control. A phased economic model should be built before committing capital. It is foundational. Water chemistry affects taste, stability, thermal performance, and equipment maintenance. Regional source variation across the United States makes site-specific treatment design essential. There is no universal answer, but cans, PET, and aseptic cartons are the most common choices for national reach because they balance channel acceptance, freight efficiency, and consumer convenience. At minimum, manufacturers typically monitor Brix, pH, sensory profile, fill volume, package integrity, coding, and relevant microbiological indicators based on the hazard profile. Common hidden costs include downtime, product giveaway, sanitation overruns, poor line balancing, freight inefficiency, changeover waste, and underbuilt utilities that choke production capacity. Expect more shelf-stable product launches, stronger sustainability requirements, wider use of automation and recipe control, tighter packaging scrutiny, and continued growth of single-serve convenience formats. A strong partner should understand process engineering, utilities, installation, compliance, automation, project execution, and commercial reality. The best teams help clients avoid misallocated capital, not just purchase machinery. Across the United States, from beverage corridors in California and Texas to manufacturing centers in the Carolinas, Ohio, and the upper Midwest, RTD success comes from disciplined integration. The product, process, package, utility system, and business model must all support each other. Companies that plan this early can enter the market faster, protect shelf life, control cost, and scale with confidence. -
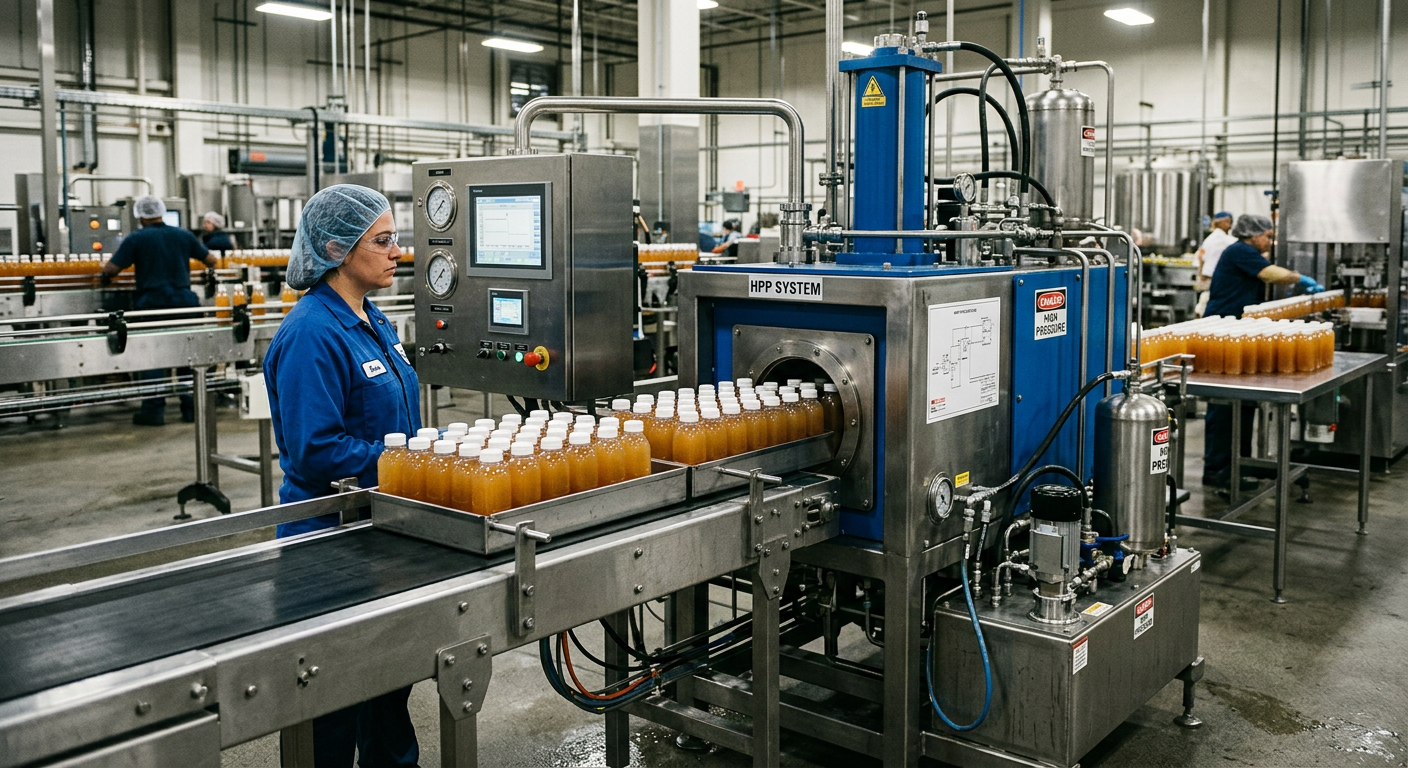
Aseptic Beverage Filling Systems
Aseptic filling systems are designed to keep a commercially sterile product separate from environmental contamination from the moment the product leaves the sterilizer until the package is sealed. For beverage producers in the United States, that means sterilizing the product, sterilizing the package, maintaining a controlled filling zone, validating the process, and minimizing downtime that can compromise both throughput and sterility. These systems are widely used for shelf-stable dairy, plant-based beverages, nutraceutical drinks, teas, juices, low-acid formulations, and premium functional products that need long shelf life without refrigerated distribution. Across the U.S. market, aseptic packaging continues to expand because brands want lower logistics costs, wider retail reach, and better flavor retention than some hot-fill alternatives. Producers shipping through Los Angeles, Long Beach, Savannah, Houston, Chicago, and the Northeast corridor increasingly evaluate aseptic lines not only on fill accuracy and sterility, but also on changeover time, utility efficiency, sustainability, operator ergonomics, and compatibility with upstream UHT and downstream secondary packaging. For companies planning new capacity or retrofits, the decision is rarely about the filler alone. It also includes product formulation, clean utility design, CIP and SIP strategy, package sterilization technology, air handling, automation, validation, and project execution. That is why many manufacturers work with multidisciplinary partners that combine engineering, installation, equipment integration, and field project management. As a North American food and beverage engineering firm, Disruptive Process Solutions approaches aseptic projects with a design-build-manage model focused on profitability, risk reduction, and startup performance rather than simply placing equipment. Aseptic filling systems work by sterilizing the beverage, sterilizing the bottle or closure, and filling in a microbiologically controlled environment so the final sealed package remains commercially sterile. In the United States, the best system depends on product acidity, target output, package format, shelf-life goals, sanitation philosophy, and the amount of downtime a plant can tolerate during SKU changeovers. In practical terms, a successful aseptic line usually combines five essentials: For U.S. beverage manufacturers, the strongest return on investment often comes from matching the filler configuration to the business model. A high-volume co-packer near Dallas or Atlanta may prioritize integrated combiblock speed and low labor. A specialty nutrition producer in New Jersey or California may place greater value on flexible linear filling with easier package changes and smaller campaign sizes. The table above shows why aseptic line selection is both a technical and business decision. Many failed projects are not caused by bad equipment, but by poor alignment between demand profile, sanitation strategy, and facility infrastructure. This line chart illustrates the steady growth trajectory expected for aseptic beverage equipment demand in the U.S. through 2029, supported by functional drinks, premium dairy alternatives, and wider shelf-stable distribution. The basic principle is simple: sterilize the product, sterilize the packaging material, keep both separate from contamination, then seal immediately. The operational reality is more complex. Aseptic filling requires a complete chain of control from ingredient receiving to pallet discharge. On the product side, beverages are commonly sterilized using UHT or ultra-clean thermal treatment. Product moves through heat exchangers, holding tubes, and sterile surge systems under carefully controlled time-temperature conditions. The treatment must be sufficient for commercial sterility while preserving flavor, color, nutrients, and viscosity. Once sterilized, the product moves through sterile piping and valves into the filler bowl or product path. On the package side, bottles, caps, or preforms are decontaminated before entering the fill zone. The filler enclosure maintains positive pressure with HEPA-filtered air or equivalent sterile air management. Surfaces that contact sterile product must remain within validated aseptic boundaries. Any intervention, unplanned stop, or utility upset can trigger re-sterilization procedures depending on system design. For U.S. plants, aseptic performance also depends on utility quality. Sterile air, clean steam, hot water, chemical dosing, condensate handling, HVAC, and control logic all matter. This is where engineering depth becomes critical. Through its process and project services, DPS supports clients with process engineering, controls integration, utility planning, and execution oversight so the sterile boundary is protected not just on paper, but in daily operations. This workflow table shows that aseptic filling is not a single machine function. It is a controlled sequence where each step must support the one after it. A weak cap sterilization step, for example, can erase the benefit of a perfectly controlled UHT system. Rotary, linear, and combiblock aseptic fillers each serve different production strategies. The right fit depends on speed, footprint, flexibility, operator skill, and whether the plant prefers integrated or modular architecture. Rotary aseptic fillers are typically chosen for higher throughput. Their continuous motion design supports efficient handling of large bottle volumes and consistent filling at scale. They are common in large beverage plants serving national retailers or multi-region distribution from hubs such as the Midwest, Texas, or the Southeast. Linear aseptic fillers are often favored when flexibility matters more than maximum speed. They can be attractive for specialty dairy beverages, functional formulations, and fast-growing brands with multiple bottle sizes or short production campaigns. Combiblock systems integrate blow molding, sterilization, filling, and capping into a tighter production unit. For high-output PET applications, this can reduce material handling, contamination opportunities, and floor space. These systems are especially relevant when a producer is building a new greenfield plant and wants a streamlined operating model. The table above highlights the tradeoffs. A plant in Chicago serving club retail may justify rotary or combiblock speed. A co-manufacturer near Charlotte or Phoenix with frequent changeovers may benefit from a linear setup that protects uptime across many customer formulas. This comparison chart makes the decision easier to visualize. Rotary and combiblock units lead in throughput, while linear fillers typically score better in flexibility and changeover responsiveness. Package sterilization is central to aseptic success. In PET and HDPE operations, three technologies frequently enter the conversation: hydrogen peroxide vapor, peracetic acid, and electron beam. Each offers specific advantages depending on package geometry, line speed, residual tolerance, validation strategy, and sustainability objectives. Hydrogen peroxide vapor is widely used in aseptic filling because it provides proven microbial reduction and integrates well into many bottle and cap treatment systems. It requires close control of concentration, temperature, contact time, and residual removal. Peracetic acid can be effective for bottle rinsing or surface decontamination strategies. It is often evaluated where wet sterilization approaches align with container design and sanitation preference. Plants must manage chemical handling, rinse validation, and wastewater considerations. E-beam uses ionizing energy rather than wet chemistry. It can reduce chemical usage and support attractive sustainability messaging, but the suitability depends on package type, investment level, line architecture, and regulatory execution. This comparison helps buyers frame the choice beyond simple sterilization effectiveness. In many U.S. projects, the deciding factor becomes total operating philosophy: chemical handling, utility load, validation comfort, line speed, and long-term environmental goals. By 2026, more producers are expected to evaluate low-water and low-chemical sterilization options as sustainability reporting grows and corporate ESG goals tighten. In states such as California and Arizona, water stress can make package sterilization chemistry and rinsing requirements an even more important line-design variable. For many American beverage plants, the true profit leak is not sterile failure but changeover loss. Aseptic lines increasingly run many bottle sizes, formulas, closures, and label programs. Every minute spent on format parts, recipe adjustments, rinse verification, and line clearance directly affects OEE. The best changeover strategy begins in design. Standardized bottle families, rationalized cap platforms, servo-driven adjustments, guided setup, recipe management, and quick-release components all reduce downtime. So does a sensible zoning plan around fillers, depalletizers, cap feeders, buffer systems, and downstream packers. Controls matter as much as mechanics. Modern HMI guidance, electronic work instructions, interlocked verification steps, and automated data capture shorten the transition between SKUs while reducing operator error. This is an area where DPS brings strong technological capability. Its teams support controls engineering, PLC programming, SCADA integration, and project execution that connect aseptic processing with utilities, blending, packaging, and line-wide performance goals. That matters when a client needs capacity gains without automatically buying a larger line. Plants serving club, grocery, and e-commerce channels from Tennessee, Ohio, or New Jersey often run tighter customer windows than before. Changeover efficiency is therefore a strategic issue, not just a maintenance one. When evaluating suppliers, ask for documented mean changeover times by bottle family and by product class, not just idealized demonstrations. Advanced aseptic productivity increasingly depends on smart sterilization control. Two concepts frequently discussed are F0-based process strategies and CSIP, or clean/steam-in-place approaches that help preserve sterile integrity while reducing manual intervention. F0 solutions use equivalent lethality concepts to quantify thermal impact in sterilization processes. In practical line design, this helps engineers align safety, product quality, and process efficiency. It can support more disciplined control of hold times, thermal treatment windows, and startup validation logic. CSIP expands the idea of repeatable, automated hygienic recovery. Well-designed CIP and SIP sequences reduce human variability, shorten sanitation cycles, and improve documented compliance. This is especially valuable in high-value beverages where downtime can mean missed retail deliveries or expensive ingredient waste. The 2026 trend is toward deeper digitalization: automated recipe management, electronic batch records, predictive maintenance alerts, remote troubleshooting, and utility optimization dashboards. Many large U.S. facilities are also incorporating energy tracking to compare steam, compressed air, water, and chemical consumption by SKU. These tools are most effective when they are integrated from the start rather than added as isolated software later. The area chart shows the projected rise in advanced automation adoption. It reflects the market shift toward data-backed sanitation, sterility assurance, and productivity management across U.S. aseptic operations. Integration is often where major gains are won. When blow molding, preform sterilization, filling, capping, and secondary packaging are engineered as one system, contamination risk and handling losses can drop substantially. Integrated PET aseptic systems also help reduce floor space and simplify material flow. Preform sterilization is especially relevant in compact, high-output lines. Instead of sterilizing full bottles after blow molding, some systems sterilize the preform before it is blown into shape inside a controlled process chain. This can improve process efficiency and support more streamlined equipment layouts. For greenfield projects, integration should also extend to utilities, syrup rooms, blending, water treatment, compressed air, boilers, cooling systems, and plant controls. DPS brings notable manufacturing and technology capabilities here, including custom equipment supply, tanks, CIP systems, utility integration, structural-mechanical-electrical coordination, and controls architecture. For clients building or expanding co-packing capacity, this cross-functional capability helps prevent the common problem of a fast filler sitting idle because upstream or utility systems were undersized. At the facility level, U.S. location matters. Plants near high-volume logistics corridors like I-85, I-35, the Inland Empire, Chicagoland, and the Port of Savannah may favor integrated aseptic PET systems that support large outbound flow. Plants serving regional specialty channels may value modularity more than absolute compactness. Aseptic systems are only as good as their validation program. Media fill testing, environmental monitoring, sterile boundary checks, package integrity verification, and sanitation validation all work together to demonstrate process control. Media fill testing simulates production using a microbiological growth medium in place of actual product. The goal is to challenge the aseptic process under defined conditions and confirm that contamination does not occur. These trials should represent real operating risks, including line stops, interventions, and startup conditions where appropriate. Sterility validation extends beyond a single trial. It includes thermal process validation, package decontamination studies, cap sterilization verification, residual testing, filter integrity testing, airflow confirmation, and documented SOP compliance. Strong programs are data-rich and repeatable. This table shows why sterility assurance must be procedural as well as mechanical. An aseptic filler can be well designed, but weak operator qualification or inconsistent environmental monitoring can still create unacceptable risk. The bar chart shows how demand varies by industry segment. Nutraceutical and dairy-related applications remain particularly active because they combine high product value with strong shelf-life and distribution requirements. Maintenance on aseptic lines is not just about reliability; it is part of sterility assurance. Worn seals, drifting sensors, damaged gaskets, poor lubrication practice, and delayed valve rebuilds can become contamination pathways or cause unnecessary shutdowns. Best practices start with a preventive and predictive maintenance plan aligned to actual failure modes. Critical spares should include sterile valves, seals, filters, dosing components, cap handling wear parts, and instrumentation that can affect validation status. Utilities deserve equal attention. In many facilities, compressed air quality, steam quality, condensate behavior, and HVAC performance determine whether the filler can operate in control. Service capability matters here. DPS supports clients not only with design, but also with installation management, owner representation, capital planning, integration, and project execution across the United States and Canada. Its lean structure can be useful for manufacturers that need fast decisions, practical field coordination, and a partner able to connect engineering intent with startup reality. Companies evaluating long-term aseptic investments should also review available process equipment capabilities and project examples from completed work in food and beverage environments. The explanation is straightforward: aseptic maintenance should be risk-based. Components tied directly to sterility, validated process control, or closure integrity deserve priority over generic mechanical routines. Looking toward 2026 and beyond, predictive analytics and remote diagnostics will play a bigger role in aseptic maintenance. Plants that connect maintenance data with SCADA, sanitation records, and production events will be better positioned to reduce emergency downtime and extend component life without over-maintaining expensive parts. For buyers comparing project partners in the U.S., it is worth asking whether the supplier understands the entire manufacturing environment or only the filler. The strongest outcomes usually come from teams that can connect process, utilities, automation, installation, and plant operations. A useful starting point is to review a provider’s case experience to see whether they have delivered integrated systems rather than isolated equipment placements. Aseptic filling is commonly used for shelf-stable dairy drinks, plant-based beverages, juices, teas, nutrition products, broths, liquid foods, and premium functional formulations. It is especially attractive when cold-chain avoidance and long shelf life are important. Hot fill relies on elevated product temperature in the package to control microorganisms, while aseptic filling sterilizes product and package separately before filling in a controlled sterile environment. Aseptic systems can better preserve sensory quality for many formulations and are often used for more heat-sensitive products. It depends on volume and SKU complexity. A high-volume co-packer with stable bottle families may prefer rotary or combiblock systems. A co-packer with many short runs and multiple customer formats may benefit from a linear filler with stronger changeover flexibility. Not universally. E-beam is gaining attention because it can reduce chemical use and water demand, but hydrogen peroxide vapor and peracetic acid remain well-established and widely used. The right choice depends on package format, cost, validation comfort, and sustainability goals. Integration. Many projects focus on the filler but underestimate utilities, upstream blending, sterile air, controls logic, cap handling, and downstream packaging balance. Poor integration creates hidden bottlenecks and longer startup timelines. It is critical. Media fills are one of the most important ways to demonstrate that the aseptic process can operate without contamination under defined challenge conditions. They should be part of a broader validation program, not treated as a one-time event. Use common packaging platforms, recipe-driven setup, better HMI guidance, quick-release parts, stronger line clearance procedures, and balanced downstream systems. Standardization often delivers the fastest payback. Ask about validated speed at your product viscosity, package sterilization method, mean changeover time, utility demand, media fill support, spare parts strategy, intervention recovery, cap sterilization method, controls integration, and service coverage in your region. Expect more emphasis on low-water sterilization, energy-efficient UHT systems, chemical reduction, lightweight packaging, digital utility tracking, and designs that support ESG reporting. These trends are becoming more important in procurement decisions, especially for national brands and large co-manufacturers. Ideally, a partner that understands process engineering, utilities, automation, installation, and project execution together. For many U.S. manufacturers, that means selecting an engineering-led firm that can design, build, and manage the project with clear accountability from concept to startup. In summary, aseptic filling systems succeed when sterility, productivity, and integration are treated as one operating strategy. For beverage companies in the United States, the best investment is not always the fastest machine. It is the system that best matches product risk, package format, labor capability, maintenance discipline, validation burden, and long-term growth plans. -
Protein Processing Tumblers
Protein tumblers are a core processing step for U.S. meat, poultry, seafood, and alternative protein operations that need better marinade uptake, improved bind, tighter purge control, and more consistent texture. In practical terms, a tumbler uses controlled mechanical action, often under vacuum and low temperature, to activate salt-soluble proteins, distribute brine evenly, and build the surface tack needed for formation, slicing, cooking, and packaging. For processors in major production corridors such as Arkansas poultry plants, Midwest pork facilities, Texas beef operations, and West Coast prepared-food manufacturers, the right tumbler setup directly affects yield, throughput, product quality, and labor efficiency. In the United States, buying decisions are rarely about the drum alone. Plants also evaluate refrigeration capacity, sanitation design, CIP strategy, automation, downstream forming or smoking, and project execution risk. That is why many processors work with integrated engineering partners such as Disruptive Process Solutions, which supports capital projects with a business-first approach focused on profitability, not just equipment placement. For facilities shipping through logistics hubs like Chicago, Kansas City, Atlanta, Houston, the Port of Savannah, or the ports of Los Angeles and Long Beach, dependable protein tumbling performance can help stabilize finished quality across demanding production schedules. A protein processing tumbler is used to improve marinade distribution, protein extraction, binding strength, finished texture, and yield in whole muscle meats, poultry items, ground systems, and many alternative proteins. The tumbler works by rotating product in a drum, usually under vacuum, so pieces lift and gently impact one another while salt, phosphate, functional ingredients, and moisture penetrate the tissue. This action extracts myofibrillar proteins that create a sticky surface matrix, which helps products hold water, bind together, slice cleanly, and perform better in thermal processing. For U.S. processors, the best tumbler is not simply the largest or fastest model. The best choice is the system calibrated to product type, target pickup, cycle time, sanitation standard, available floor space, and integration with upstream and downstream equipment. A boneless ham line in Iowa, a marinated chicken breast operation in Georgia, and a plant-based formed product line in California all require different vacuum profiles, drum speeds, temperature control approaches, and loading strategies. When evaluating equipment, buyers should focus on five practical questions: The table above shows why one-size-fits-all sizing is risky. A processor should match the machine to a specific business objective, whether that is higher line yield, lower package purge, a stronger bind in formed products, or a cleaner deli slice after thermal processing. The market trend is upward because U.S. processors continue to demand more automation, more precise yield management, and stronger food safety controls. By 2026, projects are expected to emphasize recipe control, sustainability reporting, and lower-energy chilled processing, especially in multi-line prepared-food operations. Protein tumblers serve a broad application range. In whole-muscle processing, they are used for hams, turkey breasts, roast beef, pork loins, chicken fillets, and seasoned steaks. The objective may be marinade pickup, tenderness enhancement, uniform flavor distribution, or extraction of enough functional protein to support a formed or tied shape before cooking. In poultry, tumbling is widely used after injection or pre-dust seasoning to improve moisture retention and eating quality. Plants in poultry-heavy states such as Arkansas, Georgia, Alabama, and North Carolina often tune tumbling cycles carefully because the product is delicate and throughput is high. Excessive mechanical action can lead to soft texture or visual damage, while insufficient action may leave flavor uneven and pickup below target. Ground meat applications differ. The need is often rapid functional distribution, controlled bind, and a repeatable handoff to forming equipment. Taco meat components, protein crumbles, sausage bases, and hybrid meat-plant systems can all benefit from a tumbler or tumbler-mixer configuration. Alternative proteins also fit here, especially when hydration and seasoning must be achieved without overworking the structure. For buyers comparing product types, the business case should include not only product quality but also changeover frequency, sanitation labor, and SKU complexity. A co-manufacturer near Los Angeles serving multiple retail and foodservice accounts may need more recipe flexibility than a single-SKU ham processor in Nebraska. That is why application review should happen at the plant-system level, not just at the equipment specification level. The bar chart reflects current project demand patterns in the United States, where poultry continues to lead due to volume and widespread marination needs, while alternative proteins are becoming a larger investment category because of innovation in texture, hydration, and label-driven formulation changes. The science of tumbling centers on myofibrillar protein extraction. When salt and functional ingredients are present, and the product is mechanically worked under controlled conditions, proteins such as myosin become more available on the surface. These proteins form a tacky layer that improves adhesion between pieces and strengthens water retention inside the product matrix. In whole-muscle applications, that tack helps pieces bind into a consistent shape for netting, stuffing, molding, or slicing. In ground and restructured products, it supports particle adhesion and bite. In plant-protein systems, the mechanism differs somewhat from animal muscle, but tumbler action still helps distribute moisture, binders, oils, and flavors while improving the final texture profile. Extraction is not a “more is always better” variable. Too little extraction can lead to weak bind, poor slicing, and free purge in the package. Too much extraction can create an overly dense bite, a rubbery texture, or excessive exudate during thermal processing. This balance is why processors often use recipe-specific tumble and rest cycles. The explanation behind the table is straightforward: successful protein activation comes from a controlled relationship between chemistry, mechanics, and temperature. Plants that document these variables tightly usually see lower rework, more consistent cook yields, and fewer packaging complaints. This is also where technological capabilities matter. DPS supports processor projects that involve process engineering, controls, PLC programming, recipe management, and utility coordination, which is critical when tumbling must interact with injection, chilling, smoking, and packaging systems. More detail on integrated project capabilities is available through its engineering and service offerings. Vacuum and drum speed are two of the most influential settings in tumbler performance. Vacuum reduces entrapped air, opens tissue structure, improves marinade movement, and changes how product lifts and falls in the drum. Drum speed controls the intensity of mechanical action. The correct combination depends on density, particle size, surface fragility, pickup target, and desired texture. For chicken breast fillets, a moderate speed and high vacuum often deliver strong uptake without surface tearing. For dense pork muscles, processors may use slightly longer cycles with enough speed to generate meaningful movement and extraction. For ground systems, speed is usually managed conservatively to avoid smear and excessive mechanical heat. Plant proteins may need unique profiles because hydration kinetics can differ from animal proteins. In operations near freight-intensive hubs such as Dallas-Fort Worth or the Chicago metro, processors often standardize recipes across multiple shifts and facilities. That makes repeatable control logic extremely valuable. A tumbler with programmable recipes, vacuum ramping, direction changes, and timed rests can reduce operator variation significantly. These ranges are starting points, not absolute rules. Pilot trials are still essential, especially when ingredient systems include phosphates, starches, fibers, clean-label binders, yeast extracts, or specialty proteins. A buying team should always request application testing tied to measurable outcomes such as pickup percentage, cook yield, bind strength, and package purge after distribution. Temperature control is central to both food safety and protein functionality. As product is mechanically worked, friction and handling can raise product temperature. If the system is not cooled adequately, proteins may lose functionality, fat may smear, purge may increase, and food safety margins may tighten. That is why serious U.S. processors usually evaluate tumbling alongside chilled rooms, glycol or refrigerant support, and time-at-temperature controls. For USDA-regulated environments, cold-chain discipline matters throughout the process, especially in high-throughput facilities running multiple shifts. In summer conditions in regions such as the Southeast or Gulf Coast, ambient heat load can influence how quickly product warms during loading and discharge. Facilities in Houston, Jacksonville, or inland distribution-heavy areas like Memphis often need especially robust supporting utilities. Modern protein processing projects frequently connect tumblers to broader utility systems, including refrigeration, chilled water, compressed air, and automation alarms. DPS is active in this kind of technological integration, supporting process, mechanical, electrical, and controls coordination so processors do not treat the tumbler as a standalone asset. Companies evaluating equipment can review broader processing equipment capabilities when planning a full line or utility upgrade. The area chart highlights a major 2026 trend: more projects are combining tumbling with advanced cooling, data capture, and recipe governance. This shift is being driven by retailer quality requirements, labor consistency concerns, traceability expectations, and sustainability goals tied to waste reduction and utility efficiency. Batch size is often underestimated. Even a well-designed tumbler can perform poorly if the load factor is too low or too high. Underfilling can reduce effective product-to-product contact and lead to poor lift patterns. Overfilling can compress the batch, limit movement, and create uneven marinade distribution. The ideal fill level depends on drum geometry, baffle design, protein density, and product fragility. For processors scaling from pilot to commercial volume, this is an especially important purchasing consideration. A machine that performs well at one batch level may not scale linearly. Plants in growth markets such as Nashville, Phoenix, or Central Valley California frequently face this issue when moving from regional production to national retail programs. Load factor optimization should also consider upstream logistics. Injection systems, combo bin handling, tote weights, and labor rhythms affect how consistently the tumbler is fed. Downstream constraints matter too. If the cooking, smoking, or packaging department cannot absorb discharge at the same pace, the resulting delay can cancel out the gains from a well-tuned tumbling cycle. The table shows why production teams should validate not only maximum drum capacity but also the realistic operating range that delivers repeatable quality. In many plants, the most profitable batch size is not the highest possible weight. It is the weight that keeps quality, labor, and line balance in the best zone. Sanitation design is not optional in protein processing. USDA and customer standards increasingly require equipment that is easier to clean, easier to inspect, and less likely to harbor residue. For tumblers, that generally means smooth welds, accessible surfaces, proper drainability, robust seals, fewer exposed niches, and suitable material selection for corrosive cleaning environments. 316L stainless steel is often specified for high-hygiene applications because it offers excellent corrosion resistance, especially where chlorides, aggressive sanitation chemicals, and repeated washdown are involved. While the exact material strategy depends on product and cleaning regimen, processors seeking long service life and strong sanitary performance often favor 316L in critical contact areas. This subject also connects directly to manufacturing capability. DPS designs and supplies process equipment, including tumblers and vessels, and supports installations where sanitary design, utility routing, and plant access must work together. For a processor building a greenfield line or upgrading an older room with limited floor space, fabrication quality and cleanability are every bit as important as nominal capacity. When evaluating sanitary design, ask for details on weld finishing, frame openness, seal replacement access, clean-in-place options, panel placement, and washdown durability. Also evaluate whether the equipment can be safely cleaned within the plant’s sanitation window without creating production bottlenecks. For most U.S. processors, the financial value of a tumbler is tied to yield. That includes water-holding capacity, reduced package purge, lower cook loss, stronger bind, cleaner slices, and fewer customer complaints. Even a small improvement in retained moisture can create significant margin gains when production volumes are measured in millions of pounds per year. Water-holding capacity improves when the protein matrix is properly activated and moisture is distributed effectively. Purge control improves when that moisture is actually retained through chilling, storage, and distribution. Sliceability improves when the product structure is uniform and sufficiently bound after cooking. These outcomes depend on more than the tumbler alone, but tumbling is often the key step where success begins. Case experience across the U.S. shows that yield improvement projects are strongest when processors measure the full chain: raw weight, injected weight, post-tumble weight, post-cook yield, chill loss, and in-package purge after a defined hold period. This is one reason integrated project teams outperform isolated equipment purchases. A coordinated engineering approach can link tumbling to recipe management, smokehouse scheduling, chilling capacity, and packaging specs. Processors interested in system-level examples can review project case studies and execution examples to see how integrated process planning supports long-term profitability rather than one-off capital spending. The comparison chart illustrates a common buying reality in the United States: the processor often gains more value from an integrated supplier-partner model than from purchasing equipment in isolation. Better coordination typically means better yield control, stronger sanitation outcomes, and lower project risk. A tumbler should fit into the full production architecture. Upstream, it may connect with thawing, trimming, grinding, brine preparation, injection, and tote handling. Downstream, it may discharge to forming, netting, stuffing, smokehouses, ovens, chillers, slicers, MAP packaging, or case packing. If these interfaces are poorly planned, the line loses productivity even if the tumbler itself performs well. This is where service capability becomes critical. DPS supports front-end planning, feasibility, owner representation, design-build-manage execution, project management, installation, and integration for food manufacturers across the United States and Canada. That means processors can align equipment layout, utilities, controls, local trades, compliance goals, and startup planning under one execution framework instead of trying to coordinate everything separately. For facilities expanding near major distribution routes such as Interstate 35, the Midwest rail corridor, or Southeastern cold-chain networks, line integration affects truck turn times and customer service just as much as product quality. A tumbler that discharges erratically into a constrained smokehouse schedule or a packaging room with limited buffer capacity will create hidden costs. Buying advice for U.S. plants should therefore include: By 2026, future-forward lines are expected to include tighter recipe governance, more sensor feedback, more water and chemical optimization in sanitation, and stronger alignment with retailer sustainability reporting. Policy pressure around traceability, labor reliability, and resource use is likely to continue pushing processors toward smarter integrated systems rather than stand-alone machines. Local sourcing strategy also matters. Processors in the Midwest may prioritize rapid parts access and field support in regions around St. Louis, Indianapolis, and Minneapolis. Gulf and coastal operators may care more about corrosion resistance and port-adjacent logistics resilience. West Coast co-packers may emphasize SKU flexibility and plant-protein compatibility. The right supplier is the one that understands those practical realities in your geography and category. What products benefit most from protein tumbling? Whole muscle pork and poultry, deli meats, roast items, restructured meats, seafood portions, and many plant-based protein systems benefit from tumbling when yield, bind, texture, or marinade distribution matter. Is vacuum always necessary? Not always, but vacuum is highly beneficial for many applications because it improves uptake, reduces air pockets, and supports more effective protein extraction. Ground systems and some specialty products may use lower vacuum levels or modified cycles. How much can tumbling improve yield? Results vary by formulation and process, but even small gains in retained moisture and reduced purge can create meaningful value. The right way to evaluate improvement is through controlled plant trials measuring pickup, cook yield, chill loss, and package performance. What is the ideal material of construction? For high-hygiene protein environments, 316L stainless steel is commonly preferred in critical contact areas because of corrosion resistance and cleanability, especially under aggressive washdown conditions. How do I size a tumbler for my facility? Start with product type, target batch weight, cycle time, line throughput, and realistic fill range. Then evaluate utility support, room layout, loading method, sanitation window, and downstream capacity. Do not size only by nameplate volume. Can tumblers be used for alternative proteins? Yes. They are increasingly used for hydration, seasoning distribution, oil incorporation, and texture development in plant-based chunks, strips, and hybrid protein systems. What should I ask a supplier before buying? Ask for application data, sanitary details, controls capability, cooling strategy, expected maintenance points, installation requirements, integration experience, and support after startup. Why work with an integrated engineering partner instead of buying only equipment? Because real performance depends on line integration, utilities, controls, compliance, startup, and profitability. A capable partner helps align equipment selection with production reality and long-term return on capital. For protein processors in the United States, the tumbler is not just a marination tool. It is a profit lever that influences yield, quality, labor, sanitation, and downstream efficiency. Whether the application is poultry in the Southeast, pork in the Midwest, beef in Texas, seafood on the coasts, or alternative proteins in innovation-heavy markets like California, the best results come from matching application science with disciplined engineering and practical plant execution. -
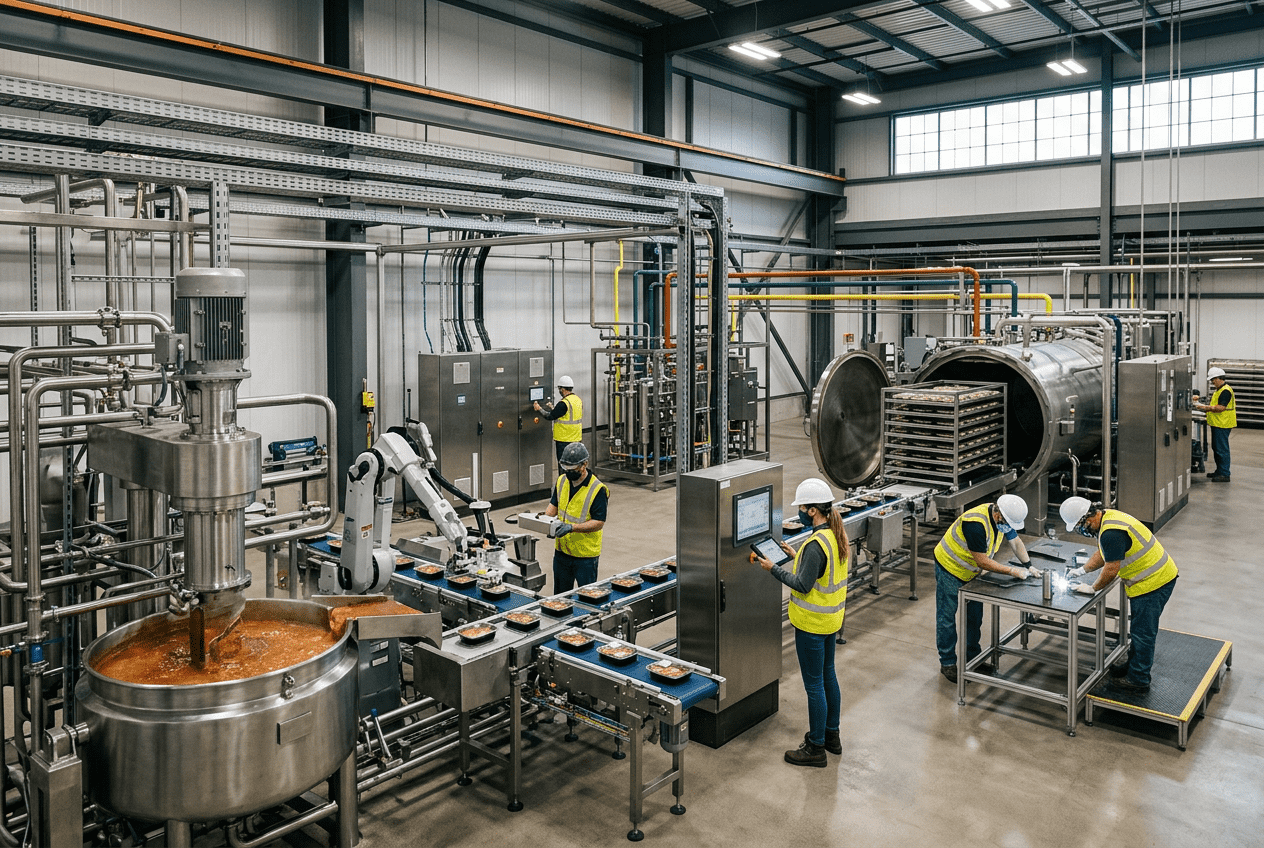
Custom Process Equipment for Food & Beverage
Food and beverage manufacturers in the United States often reach a point where standard equipment no longer fits their throughput, sanitation, footprint, product quality, or automation goals. In those cases, custom process equipment becomes the practical path forward. A well-engineered custom system can improve yield, reduce labor, support FDA and 3-A sanitary objectives, integrate with existing utilities and controls, and align capital spending with long-term profitability rather than short-term convenience. For companies expanding in markets such as Texas protein processing, California beverages, Midwest dairy, or East Coast co-packing, the decision is rarely about buying a tank alone. It is about how vessels, CIP, pumps, heat exchangers, automation, utilities, structural supports, and installation work together inside one production strategy. That is where a design-build-manage partner can make the difference between a line that merely runs and a line that produces margin. Custom process equipment makes the most sense when off-the-shelf systems cannot meet a plant’s required capacity, product characteristics, sanitation standards, space limitations, utility conditions, or automation architecture. In the United States, food and beverage manufacturers typically choose custom equipment for high-value applications such as blending, thermal processing, aseptic service, CIP, fermentation, distillation, marination, dairy, proteins, sauces, and specialty ingredient handling. A successful custom project usually includes front-end engineering, 3D layout review, material selection, code and sanitary compliance review, fabrication, factory testing, shipment planning, field installation, controls integration, startup, and operator handoff. Companies that treat custom equipment as part of a broader production and profitability model tend to see the strongest results. The table above shows the central buying truth: standard equipment can be appropriate for simple needs, but custom process equipment usually wins when the operating environment is complex, regulated, or margin-sensitive. Custom equipment is not automatically the better option. It is the better option when the economics of operation, compliance, uptime, or expansion justify the added engineering. For example, a co-packer in Chicago may need a syrup room skid sized for future line additions, while a poultry processor in Arkansas may need washdown-ready product handling equipment designed around USDA expectations, labor flow, and existing utility corridors. Off-the-shelf systems work well for standardized processes with predictable duty conditions. A stock transfer tank, utility cart, or basic pump set may be enough when product variability is low and layout flexibility is high. But once the project involves difficult heat transfer, corrosive ingredients, high viscosity, foam control, allergen segregation, hygienic weld details, or SCADA-driven batch management, the limitations of catalog equipment appear quickly. Manufacturers often move toward custom process equipment in five situations: This is especially common in logistics corridors such as Houston, Charlotte, Atlanta, Los Angeles, and Milwaukee, where plants frequently combine legacy infrastructure with new capacity targets. In those environments, the right solution is rarely a simple equipment purchase. It is a systems integration exercise. As a buying rule, if poor fit will cost more than custom engineering over three to seven years, custom usually makes sense. The chart indicates a realistic upward trend in U.S. demand as manufacturers modernize plants, reshore production, and push for more flexible line design heading into 2026. The best custom equipment projects start before drawings. They start with process goals, product characteristics, operational constraints, and expected business outcomes. That means understanding not only what the equipment should do, but why the plant needs it and how it affects yield, labor, utility demand, sanitation time, and packaging throughput. A disciplined process typically follows these stages: In practice, this work is often coordinated by an engineering partner that can connect process, mechanical, electrical, controls, structural, and installation scopes. That matters because many projects fail not on vessel design, but on poor coordination between trades. A well-run project prevents conflicts around access, cleanability, drainage, pipe routing, steam service, glycol distribution, electrical loads, and control panel placement. Disruptive Process Solutions approaches these projects with a design-build-manage model that aligns engineering decisions with installation execution and business performance. Instead of isolating design from field realities, the model helps owners connect concept development, procurement strategy, general contracting, integration, and commissioning into one capital plan. More about the company’s operating approach can be found on its about page. The table shows why the design phase is not just paperwork. It is where cost control, startup speed, and sanitation performance are largely determined. Material selection directly affects corrosion resistance, cleanability, fabrication cost, weld behavior, and total lifecycle value. In U.S. food and beverage processing, 304 stainless steel remains common for general applications, but 316L is often preferred when chloride exposure, aggressive clean-in-place chemistry, acidic products, or longer service life are important. For especially demanding environments, AL-6XN and other specialty alloys may be justified. Choosing the right metal is not about selecting the most expensive alloy. It is about aligning chemistry, temperature, pressure, cleaning regime, and expected duty cycle with the real operating environment. For example, a brewery in Portland may use 304 for some non-critical support applications but specify 316L for product-contact surfaces exposed to harsher chemicals. A sauce or brine application near the Gulf Coast may justify more robust alloy decisions because of corrosive conditions and washdown demands. This comparison helps buyers avoid overspecifying every surface while still protecting critical product-contact zones. Good engineering often uses different materials intentionally within one project. Special finishes, weld passivation, electropolishing, and surface roughness targets may also matter, especially in dairy, aseptic, or high-care systems. Material selection should be tied to cleaning validation, not just corrosion charts. Integration is where many projects either create long-term value or create years of frustration. Installing a custom tank, skid, tumbler, kettle, or thermal system into an active plant means dealing with real-world constraints: low ceilings, existing trench drains, overloaded utility headers, old PLC architecture, sanitation pathways, forklift traffic, allergen zones, and line balancing. Successful integration begins with accurate site data and realistic shutdown planning. For brownfield facilities in places like New Jersey, Ohio, and North Carolina, even a well-built piece of equipment can become a costly problem if tie-in points, access clearances, and operator movement were not evaluated early. Key integration questions include: DPS is particularly strong in this area because its technical capabilities extend beyond process design into structural, mechanical, plumbing, electrical, and controls engineering, including PLC programming, automation, and SCADA. That cross-discipline capability matters when integrating a new processing asset into a live facility. Owners can review broader engineering and integration services when evaluating project support. The bar chart highlights where custom food process equipment is in strongest demand. Beverage, protein, and dairy continue to lead due to sanitation complexity, recipe variation, and utility intensity. Custom equipment does not mean informal equipment. In regulated food and beverage operations, one-of-a-kind systems still need disciplined design documentation, material traceability where required, sanitary detailing, and code alignment. Depending on application, equipment may need to satisfy ASME pressure design requirements, 3-A sanitary principles, and FDA-focused hygienic considerations for product-contact surfaces. For some plants, compliance also intersects with USDA, SQF, BRC, customer audit expectations, and internal corporate engineering standards. That is why compliance should be built into the project from the start rather than checked near shipment. Important compliance elements often include: For processors serving retail, foodservice, export, or pharmaceutical-adjacent applications, compliance also affects customer confidence and insurance posture. A tank or skid that looks sanitary is not enough. It must be engineered and documented in a way that supports validation, operations, and audit readiness. The value of this matrix is simple: compliance is not one item; it is a stack of overlapping requirements that can influence fabrication, installation, startup, and future audits. Custom equipment schedules are shaped by engineering depth, material lead times, shop capacity, controls complexity, shipping method, and plant shutdown windows. For U.S. projects, realistic timeline planning also needs to account for local permits, freight constraints, contractor availability, and seasonal production peaks. A beverage plant in California may need installation before summer volume ramps, while a protein plant in Kansas may require holiday blackout planning. A disciplined project schedule should include formal milestones rather than broad promises. Owners need visibility into design approval, long-lead procurement, shop completion, FAT readiness, field installation, utility tie-ins, dry commissioning, wet commissioning, and performance confirmation. The explanation is important here: delays usually do not come from fabrication alone. They often come from late owner decisions, weak site information, poor coordination between trades, or underestimating controls integration. DPS serves manufacturers across all 50 U.S. states and Canada, which is useful for multi-site operators that need repeatable project management rather than one-off local coordination. The company’s service capabilities include capital planning, owner’s representation, project and program management, general contracting where licensed, and turnkey installation and integration. Not every project begins with a full-size system. In many product development or process improvement cases, manufacturers first need pilot-scale equipment to validate heat transfer, residence time, ingredient incorporation, sanitation behavior, or operator workflow. That is especially true in functional beverages, plant-based proteins, fermented products, specialty sauces, and aseptic concepts. Fabrication flexibility matters because the right approach may be a prototype vessel today, a pilot skid next quarter, and a full production train next year. A capable equipment partner should be able to support that progression without forcing owners to start over each time. DPS has been growing its proprietary equipment manufacturing around practical food and beverage applications, including storage and processing tanks up to 12,000 gallons, custom CIP systems, marination tumblers, and cooking vessels. That manufacturing capability becomes more valuable when combined with engineering and field integration support, because the equipment is designed with the site and project outcome in mind rather than treated as an isolated product. You can review the company’s process equipment offerings for examples of manufactured systems. For many U.S. manufacturers, modular fabrication is becoming the preferred strategy because it reduces field labor, shortens installation windows, and simplifies future capacity additions. The area trend reflects how buyers are moving toward flexible, modular, and automation-ready equipment strategies, especially as labor pressures and SKU complexity continue into 2026. Many buyers make the mistake of comparing only purchase price. The better comparison is total delivered value over the asset’s operating life. That includes engineering, fabrication, freight, structural support, installation, controls, startup, operator training, maintenance burden, sanitation time, utility usage, spare parts, uptime, and future expansion potential. Custom equipment can carry a higher initial price than catalog equipment, but the lifecycle economics are often stronger when the system reduces downtime, prevents product loss, shortens cleaning, or eliminates labor-intensive workarounds. In high-volume facilities, even a small gain in OEE or yield can outweigh the initial engineering premium quickly. Consider a simple example: if a custom batching system reduces ingredient giveaway by 1.5%, cuts sanitation time by 30 minutes per shift, and improves line utilization by 4%, the annual financial impact can be substantial. This is why sophisticated operators increasingly evaluate capital through throughput, margin, and payback, not unit price alone. This comparison chart shows a common commercial reality: standard equipment may appear attractive on initial price, but custom equipment often performs better across operational value drivers. When evaluating suppliers, buyers should ask for a cost model that includes: For plants making large capital decisions, case-based review is often useful. DPS shares project examples and outcomes through its project case studies, which can help owners compare approaches across beverage, food, and utility-intensive applications. What types of custom process equipment are most common in the United States food and beverage market?Common examples include process tanks, blending systems, CIP skids, cooking vessels, marination systems, fermentation equipment, distillation systems, thermal processing skids, utility modules, and integrated packaging support systems. How do I know whether 304 or 316L is the better choice?304 is often suitable for general service, while 316L is typically preferred where higher corrosion resistance, aggressive cleaning chemistry, or more demanding sanitary conditions are expected. The final decision should be based on product chemistry, cleaning protocol, and lifecycle goals. Can custom equipment be installed into an older facility?Yes, but the project needs careful field verification, utility review, layout modeling, and controls planning. Brownfield integration usually requires more engineering attention than greenfield installation. Does custom equipment always cost more?It usually costs more upfront, but not always more over the equipment’s life. If custom design improves uptime, yield, sanitation time, labor efficiency, or future expansion options, the total value can be better than a cheaper standard unit. What compliance standards matter most?That depends on application, but ASME, 3-A, FDA-related hygienic design principles, USDA expectations for certain food sectors, and private audit frameworks such as SQF or BRC are common factors in U.S. projects. How long does a custom project take?Simple projects may move in a few months, while larger integrated systems can take much longer. Timeline depends on design complexity, material lead times, controls integration, and the owner’s shutdown window. What industries benefit most from custom process equipment?Beverage, dairy, protein, prepared foods, sauces, ingredient processing, distilling, aseptic operations, and co-packing are among the strongest candidates because they often combine sanitation demands with changing throughput and product requirements. What trends are shaping 2026 buying decisions?The biggest 2026 trends include energy-aware system design, water and chemical reduction in CIP, increased automation and SCADA visibility, modular skid construction, stronger traceability expectations, and more capital planning tied to sustainability and labor resilience. U.S. manufacturers are also watching policy developments around domestic production, infrastructure reliability, food safety modernization, and environmental efficiency. Why do some owners choose a partner like DPS instead of separate designers, fabricators, and installers?Because combining engineering, manufacturing understanding, project management, and field execution can reduce coordination gaps. For many projects, especially complex food and beverage expansions, that integrated approach lowers schedule risk and aligns the equipment decision with broader plant profitability. In summary, custom process equipment is most valuable when it is treated as part of a complete operating system. For U.S. food and beverage manufacturers, the smartest projects are the ones that connect process performance, sanitary design, utility realities, compliance, integration, and long-term business value. Whether the need is a pilot-scale skid, a 12,000-gallon process vessel, a custom CIP system, or a fully integrated production upgrade, the right solution starts with honest engineering and ends with reliable startup. -
Aseptic Beverage Processing Systems
Aseptic beverage processing is a manufacturing method that sterilizes the product and the package separately, then combines them inside a sterile environment to produce shelf-stable drinks without refrigeration. In the United States, this method is widely used for dairy beverages, protein drinks, plant-based beverages, functional drinks, juices, coffee, teas, and sensitive low-acid formulations that demand long shelf life, flavor protection, and national distribution efficiency. For processors evaluating capital investment, the right aseptic system is not just a filler. It is a tightly integrated production platform that includes UHT treatment, sterile surge handling, packaging sterilization, aseptic filling, clean utilities, automation, and validated microbiological controls. For manufacturers in major production corridors such as Chicago, Dallas, Los Angeles, Atlanta, Charlotte, and the New Jersey distribution belt, aseptic processing often becomes a strategic tool for freight flexibility, SKU expansion, and warehousing efficiency. It also matters in port-connected supply chains through Long Beach, Savannah, Houston, and New York/New Jersey, where long dwell times and wide geographic distribution make ambient stability especially valuable. Aseptic beverage processing works by rapidly sterilizing liquid product, usually with UHT heat treatment, cooling it under sterile conditions, sterilizing the packaging material, and filling the beverage in a closed aseptic chamber. Compared with hot fill and retort, aseptic systems typically provide better sensory retention, support more package formats, reduce thermal load on the beverage, and enable high-speed output from about 12,000 to 72,000 bottles per hour depending on format, viscosity, and automation level. In practical U.S. terms, aseptic is usually the right choice when a brand needs one or more of the following: nationwide ambient distribution, low-acid beverage safety, dairy or plant-based protein stability, premium flavor retention, lightweight package formats, or high-volume production economics. Hot fill remains effective for many high-acid beverages. Retort is still essential for certain shelf-stable foods and highly robust packaged products. The best choice depends on product pH, particulate content, shelf-life target, package type, throughput goals, utility availability, and regulatory expectations. For companies that need engineering guidance from concept to commissioning, Disruptive Process Solutions supports U.S. manufacturers as a food and beverage engineering partner focused on profitable project execution rather than one-dimensional equipment sales. The aseptic journey begins with product formulation and microbiological risk classification. The product is blended, standardized, and often deaerated before entering thermal treatment. In most beverage applications, UHT sterilization heats the liquid to approximately 135 to 150 degrees Celsius for a very short holding time, often only a few seconds. That thermal exposure is enough to destroy vegetative cells and spores when paired with validated residence time, flow control, and temperature monitoring. After heating, the beverage is flash cooled or indirectly cooled in sterile heat exchange sections. It then moves into a sterile surge tank or balance vessel that maintains overpressure with sterile air or nitrogen. From there, the liquid is transferred through sterile piping to the filler. The packaging, whether PET bottle, HDPE bottle, carton, cup, or flexible structure, is sterilized separately using hydrogen peroxide, steam, UV, or a hybrid method. Finally, the product is filled and sealed inside an aseptic chamber maintained with filtered air, controlled pressure differentials, and validated environmental conditions. Three engineering issues determine whether a system performs in the field: thermal design, hygienic design, and automation logic. A poorly designed heat profile may overcook proteins or destabilize emulsions. A poorly designed hygienic circuit may create dead legs, gasket risks, or difficult-to-clean valves. Weak automation may undermine sterility through unverified setpoint drift, improper SIP sequencing, or incomplete changeover interlocks. That is why many U.S. processors prefer an integrated project model that combines process engineering, utilities, controls, and installation. DPS applies a design-build-manage approach that helps clients align UHT, blending, utilities, CIP, controls, and filling into one capital plan rather than fragmented vendor packages. The table above shows why aseptic success depends on the entire chain, not only the sterilizer. A weak receiving program or poorly validated filler can undermine even an excellent UHT process. Choosing the right processing method starts with product chemistry and commercial objectives. A high-acid juice for regional retail may fit hot fill perfectly. A low-acid protein shake with national e-commerce distribution will generally need aseptic processing. A shelf-stable product with particulates or a package intended to withstand post-fill sterilization may call for retort. Hot fill typically heats product and fills it while hot enough to sanitize the container interior. It is common for juices, teas, and acidified beverages. It is proven and often less capital intensive than aseptic. However, it places more heat stress on flavor, color, and nutrients, and it may limit package selection. Retort processes the sealed package after filling, usually inside a pressure vessel. It is robust and suitable for many shelf-stable foods and some specialty beverages, but thermal load is even higher and throughput is often slower, depending on package size and cycle time. Aseptic processing separates product sterilization from packaging sterilization. This preserves sensory quality better and supports very high line rates once the system is tuned. It also demands higher engineering rigor, sterility validation, and disciplined operating procedures. The table shows that no single technology is universally better. The right answer depends on your product family, growth plan, labor model, and distribution radius. A co-packer serving both East Coast and West Coast retailers may value aseptic shelf stability more than a local juice brand distributing only in the Southeast. An aseptic beverage line is a system of interdependent hygienic assets. The core typically includes raw ingredient handling, batching, high-shear mixing where needed, deaeration, homogenization, UHT treatment, aseptic holding, sterile transfer, package sterilization, aseptic filling, secondary packaging, and comprehensive CIP/SIP support. Utilities matter just as much as the main process path: clean steam, culinary water, compressed air, chilled water, glycol, boiler capacity, condensate management, and HVAC all influence sterility and uptime. From a technological capability standpoint, DPS supports complete process, mechanical, electrical, structural, plumbing, and controls engineering for aseptic facilities. That matters because filler performance alone does not solve plant bottlenecks. The surrounding infrastructure must be sized correctly for thermal load, utility redundancy, recipe complexity, and future line expansion. Manufacturing capability also matters. DPS designs and supplies selected process equipment such as tanks and custom CIP systems, which helps align fabrication details with the broader project intent. Service capability is equally critical: capital planning, feasibility analysis, owner’s representation, general contracting, installation management, and startup coordination all affect how quickly an aseptic line reaches commercial production. Many beverage investors underestimate the utility envelope around these components. For example, a line may be mechanically rated for 48,000 bottles per hour but effectively capped by steam generation, sterile air preparation, or CIP turnaround. That is why comprehensive process engineering and project services are often more valuable than buying hardware without full integration planning. Sterility Assurance Level, or SAL, is a way of expressing the probability that a viable microorganism survives the sterilization process. In beverage manufacturing, the exact interpretation depends on product type, packaging, process authority expectations, and applicable regulations, but the core concept is constant: sterility claims must be supported by validated science, not assumptions. Validation typically includes thermal mapping, residence time studies, challenge testing, packaging sterilization verification, aseptic boundary integrity checks, filter integrity testing, environmental monitoring, media runs where appropriate, and documented operating limits. Processors also need a robust hazard analysis that identifies biological risks across formulation, transfer, filling, storage, and maintenance activities. In the United States, manufacturers dealing with low-acid aseptic products must align with FDA expectations for commercial sterility, scheduled process establishment, and detailed process records. Validation must be specific enough to cover worst-case formulations, maximum viscosity, minimum flow conditions, startup transitions, and abnormal events such as power interruptions or pressure loss. The explanation above highlights a common U.S. mistake: companies validate the sterilizer but not the whole aseptic ecosystem. True validation extends from raw material assumptions through final package seal integrity. Packaging sterilization is one of the most important decisions in any aseptic project because it shapes package compatibility, operating costs, environmental controls, and validation complexity. The most common methods are hydrogen peroxide, steam, UV, or combinations of these technologies. Hydrogen peroxide, often written as H2O2, is widely used because it is effective and compatible with many high-speed systems. It may be applied as vapor, mist, or liquid depending on package format and line design. The process requires tightly controlled concentration, temperature, exposure time, and residual management. Steam sterilization provides strong microbial reduction and may suit some packaging components or closures, especially in lines already supported by clean steam infrastructure. However, moisture and heat effects must be managed carefully to avoid package deformation or condensation-related issues. UV methods can be useful in certain package and cap applications, particularly where dry processing advantages are attractive. Yet UV is line-of-sight dependent and often works best as part of a broader decontamination strategy rather than as a universal standalone answer. For U.S. processors facing sustainability targets in 2026 and beyond, dry or lower-water sterilization approaches are getting more attention, especially in regions where wastewater, heat recovery, and energy intensity affect total operating cost. Plants in California, Arizona, and Texas are especially sensitive to utility efficiency planning. U.S. aseptic beverage operations must be designed around compliance from day one, not retrofitted after installation. FDA requirements can apply to low-acid foods, acidified products, preventive controls, cGMPs, process records, and scheduled processes depending on the product category. Hygienic design standards from organizations such as EHEDG and 3-A concepts are also useful in minimizing cleanability risk and strengthening validation readiness. For processors supplying major retailers or co-manufacturing national brands, practical compliance goes beyond passing inspection. It means documented hygienic zoning, sanitary weld quality, drainability, accessible valve clusters, segregated utilities, CIP proof, alarm management, controlled interventions, and accurate lot traceability. DPS frequently supports clients that need not only design expertise but also regulatory fluency across FDA, USDA, SQF, and BRC-aligned projects. That service capability is important for mixed portfolios where a manufacturer may run beverages, dairy, prepared foods, or retort products at the same campus. In cities with aggressive expansion of co-packing infrastructure such as Dallas-Fort Worth, Nashville, Phoenix, and the Carolinas manufacturing corridor, compliance-centered engineering has become a competitive differentiator. Investors want systems that can scale without triggering redesign because a filler was installed before the sanitary utility map was fully planned. Cleaning-in-place and sterilization-in-place are the heartbeat of aseptic reliability. CIP removes product residues, films, proteins, sugars, and minerals. SIP then sterilizes the clean equipment path using steam or equivalent validated methods. If either protocol is weak, sterility assurance collapses. Effective CIP programs define chemical concentration, flow velocity, temperature, time, circuit segmentation, return conductivity targets, and final rinse acceptance. Effective SIP programs define steam quality, temperature hold, cold spot verification, condensate control, and sterile boundary confirmation. From a maintenance perspective, the best plants do not treat CIP/SIP as a sanitation checkbox. They use trend data to identify fouling rates, valve wear, gasket fatigue, heat exchanger performance decline, and campaign length optimization. This reduces both microbiological risk and unnecessary downtime. The table shows why CIP/SIP should be engineered with the same seriousness as production. Many underperforming lines in the United States are not limited by filler speed but by cleaning turnaround and unstable campaign scheduling. Capacity planning for aseptic beverage lines should begin with market strategy rather than nameplate speed. A startup protein beverage brand shipping through Atlanta and Chicago may only need 12,000 to 18,000 bottles per hour. A national co-packer serving club stores from Southern California, Texas, and Pennsylvania may require 48,000 to 72,000 bottles per hour or more. The correct line size depends on SKU count, changeover frequency, OEE target, warehousing logic, labor model, and utility redundancy. One of the biggest planning errors is selecting speed before understanding annualized demand and true run time. A line designed for 72,000 bottles per hour may still miss budget if there are too many short runs, excessive cap changes, unstable sterilization cycles, or insufficient downstream packaging capacity. Another key factor is footprint. Existing plants in urban industrial zones such as New Jersey, Los Angeles County, or inner-ring Chicago suburbs often have layout constraints that change filler choice, sterile tank sizing, mezzanine strategy, and CIP routing. Greenfield sites in North Carolina, Texas, or Tennessee may offer more flexibility and stronger long-term utility planning. When buyers compare suppliers, they should look beyond machine speed. Evaluate integration experience, controls architecture, hygienic design philosophy, utility consumption, FAT/SAT methodology, local service access, spare parts strategy, and startup support. A faster filler with weak commissioning support can cost more than a slower but stable line. For companies planning a new line or expansion, it is often wise to benchmark available process equipment options against projected SKU mix, required sterility validation effort, and downstream packaging demand before finalizing procurement. Looking toward 2026, four trends are shaping the U.S. market. First, more beverage brands are moving into functional, protein, and hybrid dairy-plant products that favor aseptic processing. Second, automation and SCADA-driven batch traceability are becoming standard rather than premium features. Third, water and energy efficiency are gaining board-level attention, encouraging heat recovery, smarter CIP reuse, and lower-chemical decontamination strategies. Fourth, policy and retailer pressure are increasing around documentation, food safety culture, and sustainability metrics. DPS is especially well positioned for these trends because its work spans process engineering, utilities, automation, installation, and project management. The company has supported beverage and food clients across North America, from breweries and distilleries to dairy, prepared foods, aseptic, and retort operations. In practical terms, that means a client can engage one team to evaluate feasibility, engineer the process, coordinate trades, manage execution, and support startup instead of trying to align disconnected vendors. For readers who want examples of project execution style and industry fit, the firm’s project case studies offer a useful view into how integrated capital work is planned and delivered. What beverages are best suited for aseptic processing?Low-acid dairy drinks, protein shakes, plant-based milks, coffee beverages, nutritional beverages, creamers, some juices, and many functional products are strong candidates. Products with national ambient distribution needs benefit the most. Is aseptic processing always better than hot fill?No. Hot fill can be the better business decision for high-acid products, lower capital budgets, and simpler packaging needs. Aseptic is usually stronger for sensitive low-acid beverages and broader shelf-stable distribution. How long can aseptically processed beverages last?Shelf life varies by product, package, oxygen control, and storage conditions. Many products target six to twelve months, while some achieve longer validated shelf life with proper formulation and packaging. What is the biggest hidden cost in an aseptic project?Utility and integration gaps. Steam, sterile air, CIP, controls, building modifications, HVAC, and validation often create more cost exposure than the main filler if not planned early. Can an existing hot-fill plant be converted to aseptic?Sometimes, but not always efficiently. Conversions require careful review of utilities, hygienic zoning, package strategy, floor layout, sterile boundary design, and compliance obligations. What line speed should a new U.S. co-packer target?It depends on annual volume, SKU count, and customer mix. Many new entrants begin around 12,000 to 24,000 bottles per hour, while larger co-packing hubs may plan 36,000 to 72,000 bottles per hour. How important is local support in the United States?Very important. Downtime costs can be severe, especially in high-volume ambient beverage plants. Buyers should assess spare parts availability, remote support capability, and technician coverage across regions such as the Midwest, Southeast, Texas, and the West Coast. What should buyers ask an engineering partner before investing?Ask about process authority coordination, validation scope, utility load assumptions, hygienic design standards, CIP/SIP philosophy, startup staffing, changeover modeling, and future expansion planning. The right partner should challenge assumptions, not simply confirm them. Aseptic beverage processing in the United States is ultimately a business system as much as a sterilization system. When properly designed, it gives brands longer reach, stronger quality retention, and a path to profitable scale. When poorly scoped, it becomes an expensive bottleneck. The best outcomes come from aligning product risk, package strategy, utilities, validation, and commercial growth into one engineering roadmap. -
2026 Food Facility Fire Suppression Design: Wet Chemical vs Dry Chemical Systems
Food and beverage facilities across the United States are under growing pressure to improve fire protection in kitchens, process areas, packaging lines, utility rooms, and special hazard zones. In 2026, the key design question is rarely whether a suppression system is needed. The real question is which suppression method fits each hazard, how it integrates with ventilation and controls, and how the system can be delivered without interrupting production or creating compliance gaps. For most commercial cooking lines, wet chemical systems remain the preferred solution because they are designed to suppress grease-laden fires and reduce reflash risk. For industrial hazard areas outside kitchen hoods, dry chemical systems still play an important role where flammable liquids, certain process hazards, or localized equipment exposures require rapid knockdown. In major manufacturing corridors such as Chicago, Charlotte, Dallas, Los Angeles, Atlanta, Houston, and the I-95 food distribution belt, plant owners are also asking broader capital-planning questions. They want systems that align with NFPA 96, local fire code review, insurer expectations, USDA or FDA operational realities, and long-term maintainability. They also want fewer trade conflicts between fire protection, HVAC, utility piping, controls, structural steel, and process equipment. That is why design-build delivery has become more attractive for food plants, beverage operations, co-packers, protein processors, dairy facilities, and high-throughput prepared-food sites. The short answer is this: wet chemical systems are generally the best choice for commercial kitchen lines, conveyorized fryers, griddles, ranges, broilers, and hood-protected foodservice cooking operations because they are specifically engineered for cooking oil and grease fires. Dry chemical systems are more commonly used in industrial hazard areas where the risk profile is not centered on grease vapors under kitchen ventilation. The correct choice depends on appliance type, fuel source, exhaust design, local code adoption, cleanup requirements, business continuity goals, and insurer criteria. For U.S. facilities, a compliant fire suppression design must do more than discharge agent. It must coordinate with hood exhaust, makeup air, duct protection, appliance coverage, manual pull stations, gas or electric shutoff interlocks, audible and visual alarms, and inspection access. In a mixed-use food plant, one building may require both system types in different zones. A prepared-food plant in New Jersey may use wet chemical protection over kettle batteries and fryers, while a nearby packaging mezzanine or solvent-related maintenance area may use a different special hazard approach. The answer is therefore not either-or for the whole building. It is hazard-by-hazard engineering. The table above shows why system selection should be tied to the hazard itself, not to habit or vendor preference. In practical terms, most food production clients in the United States need a zone map that distinguishes commercial cooking protection from adjacent industrial fire risks. The chart reflects a realistic market trend: retrofit and modernization demand is rising as older systems age, insurers tighten expectations, and food plants expand prepared-food production. Wet chemical systems are the standard solution for commercial kitchen lines because they are formulated for cooking media fires, especially where animal fats, vegetable oils, and grease residues are present. When discharged through listed nozzles, the agent cools the fire and reacts with hot grease to help create a foam-like blanket that limits oxygen contact and reduces re-ignition potential. In food plants, this matters most over fryers, open-flame broilers, charbroilers, woks, kettles, ranges, conveyor ovens, and hybrid cooking suites used in commissaries or prepared-food operations. In cities with dense foodservice and processing activity such as New York, Philadelphia, Miami, and Las Vegas, wet chemical systems are commonly seen not only in restaurants but also in centralized food production hubs, stadium commissaries, airport kitchens, hotel production kitchens, and fresh prepared-meal plants. In manufacturing, the same logic applies when commercial-style cooking equipment is installed inside a plant environment. The presence of a production floor does not change the hazard chemistry under a grease hood. Wet chemical systems also bring operational advantages. Cleanup is often more manageable than with broad dry powder discharge, especially where food safety and restart time matter. That does not mean cleanup is trivial, but contamination spread is typically easier to control in hood-protected cooking zones than in adjacent packaging or open-ingredient areas. For this reason, facilities producing ready meals, sauces, proteins, or snack foods often prefer wet chemical protection whenever the hazard falls under commercial cooking standards. This table highlights an important buying point: wet chemical systems should be selected with appliance-specific listings and hood geometry in mind. Food producers often make the mistake of treating the suppression package as generic. It is not. A fryer line in Memphis processing breaded chicken is not automatically covered by the same nozzle arrangement as a commissary wok line in Seattle or a university kitchen in Boston. By 2026, more facilities are also pairing wet chemical suppression upgrades with broader ventilation modernization. That includes improved hood capture, variable-frequency exhaust strategies, replacement fans, grease-rated duct modifications, and smarter control logic. In retrofit markets around Southern California and the Carolinas, this integrated approach often reduces rework and shortens AHJ review cycles because the fire protection design is coordinated from the start rather than forced into an existing mechanical layout. Dry chemical systems remain relevant in industrial hazard areas where the fire risk differs from grease-laden commercial cooking. These systems are often used for flammable liquid hazards, certain machinery exposures, fuel handling points, loading or transfer areas, maintenance hazards, and other localized industrial applications where rapid flame knockdown is the main objective. In food and beverage facilities, these may be found in support spaces rather than under kitchen hoods, though every application should be reviewed against the specific hazard and local code requirements. For example, a beverage facility near Houston may have process utility zones, maintenance areas, or flammable storage interfaces that justify dry chemical protection, while the same building uses wet chemical systems over a culinary R&D kitchen. A plant near the Port of Long Beach that handles specialty ingredients, packaging, and mixed industrial operations may need separate strategies for different rooms. One of the biggest mistakes in industrial fire protection is assuming the cleanest-looking room has the simplest hazard. Hidden ignition sources, heat release rates, and material compatibility must still be studied. Dry chemical systems can be highly effective, but they come with tradeoffs. Cleanup can be more disruptive, sensitive equipment may require extra protection, and production restart can be slower if powder disperses into process-adjacent areas. In facilities with open ingredients, exposed packaging materials, or strict sanitation turnover, these factors carry real economic weight. The lesson from the table is that dry chemical systems should be reserved for the right industrial conditions, not installed by default. Facilities in the United States are increasingly weighing production downtime, sanitation, and insurer expectations alongside raw suppression performance. This demand comparison shows where retrofit activity is strongest: cooking-heavy sectors and institutional foodservice environments lead the market, while beverage-only facilities are generally lower unless they include culinary development, tasting kitchens, or mixed industrial hazards. In U.S. food facilities, fire suppression design cannot be separated from ventilation design. NFPA 96 remains the core reference for ventilation control and fire protection of commercial cooking operations, and in practice that means the hood, grease duct, exhaust fan arrangement, makeup air system, access doors, clearances, and suppression package must function as a coordinated system. If one part is poorly designed, the whole fire protection strategy weakens. Integration starts with capture and containment. A hood that fails to capture grease-laden vapors increases deposition in the duct and creates long-term fire risk. Oversized or poorly balanced makeup air can spill contaminants out of the hood envelope. Fan selection affects plume behavior. Access for cleaning affects fire loading over time. By the time the suppression contractor arrives, many of these issues are already baked into the project unless the design team has coordinated mechanical and fire protection scopes upfront. This is especially important in retrofit-heavy markets such as New Jersey food corridors, California urban production kitchens, and Southeast poultry processing expansions. Facilities often inherit older hoods, patched ducts, changed appliance lineups, and incomplete as-builts. A compliant design in 2026 usually requires field verification, not just plan review. The practical takeaway is simple: ventilation and suppression should be engineered together. That is one reason many owners choose integrated project partners rather than managing separate mechanical, electrical, fire, and process trades in isolation. The area chart reflects a clear industry shift: more U.S. owners are procuring ventilation and fire protection as one coordinated package, especially where schedule certainty and operational continuity matter. System performance depends heavily on proper component selection and nozzle placement. The best agent in the world will underperform if the tank size, piping layout, detection method, fusible link location, appliance coverage, and nozzle angles do not match the actual hazard. Listed manufacturer requirements govern much of this work, and deviations can create real compliance and liability problems. In food manufacturing projects, nozzle placement is often complicated by custom stainless fabrication, utility drops, washdown shields, overhead conveyors, access hatches, and changing appliance elevations. A fryer line in Arkansas, for example, may include OEM guarding and removable covers that affect discharge patterns. A commissary in downtown Chicago may have limited ceiling height and tight duct transitions. A university kitchen in California may need seismic coordination and phased shutdowns during retrofit. All of these affect design quality. Owners should also think beyond first cost. Better component selection can reduce false trips, improve serviceability, and make annual or semiannual inspections more efficient. Smart control integration, clean piping routes, clearly labeled manual pull stations, and accessible test points save money over the life of the system. In complex facilities, a multidisciplinary engineering approach is valuable. Companies with strong process, structural, mechanical, plumbing, electrical, and controls capability can spot conflicts earlier. That matters in real food projects where fire protection has to coexist with clean utility lines, automation panels, SCADA visibility, CIP systems, steam, refrigeration, and sanitary routing. A suppression discharge event must trigger the right actions immediately. In most kitchen-protected applications, that includes shutting off fuel or electrical energy to protected cooking appliances, activating alarms, and coordinating any required fan or control responses. If these interlocks are missing or poorly tested, the suppression system may discharge while ignition sources continue feeding the fire. For gas-fired equipment, fuel shutoff reliability is critical. Solenoid valves, emergency stop sequences, and control relays must be compatible with the appliance arrangement and local code enforcement. For electric equipment, shunt-trip or other shutdown logic may be required depending on the configuration. Integration with the building fire alarm system should also be reviewed carefully, especially in larger food plants where an event under one hood may need local annunciation, central monitoring, or plant-wide response protocols. Facilities in major logistics hubs such as Dallas-Fort Worth, Columbus, and Savannah often run around the clock, so nuisance shutdown risk is a real business concern. That is why design quality and commissioning discipline matter. An interlock system should be fail-safe, documented, labeled, and tested with operations staff present. It should also be easy to restore correctly after an event. The explanation behind this table is straightforward: alarm and interlock design is not a side issue. It is central to fire suppression effectiveness and plant restart planning. Even a well-designed system will fail expectations if inspection and maintenance are neglected. U.S. operators should maintain a documented schedule covering routine visual checks, semiannual inspections where applicable, detector and pull station verification, cylinder condition, nozzle cap condition, pipe integrity, fuel shutoff functionality, alarm interface testing, fan logic verification, and post-service documentation. The exact schedule depends on system type, local authority requirements, and manufacturer listing instructions, but the compliance principle is the same: fire suppression must remain ready, accessible, and matched to the current hazard. Food facilities often struggle with maintenance discipline because production changes faster than life safety records. Appliances get moved, guards are added, ducts are modified, and utilities are rerouted. If the suppression layout is not updated, the site may believe it is protected when it is not. This is especially common in fast-growth sectors like meal kits, commissaries, co-packing kitchens, and hybrid foodservice-manufacturing operations. The maintenance schedule above works best when tied to a broader compliance program. Facilities with strong management systems often include fire suppression review in change control, preventive maintenance software, shutdown planning, and annual risk audits. Design-build delivery is becoming more attractive for food and beverage fire suppression projects because it reduces coordination gaps between engineering, procurement, installation, controls, permitting, and startup. Instead of an owner separately managing mechanical design, fire protection design, electrical controls, field trades, and process shutdown planning, a design-build team can align the sequence from the start. This is especially valuable in brownfield retrofits where every shutdown hour has a real cost. For plants in the United States, the strongest design-build outcomes usually come from teams that understand not only fire protection but also food production realities. That includes sanitation windows, temporary production routing, utility tie-in planning, process downtime minimization, and regulatory expectations. In a protein facility, replacing suppression over a cook line may require coordination with washdown and USDA scheduling. In a beverage innovation center, the challenge may be keeping pilot operations running while controls are upgraded. In a high-volume co-packer near Atlanta or Phoenix, speed-to-production can outweigh small equipment cost differences. This is also where broader technical capabilities matter. A partner with in-house or closely coordinated expertise across mechanical, electrical, plumbing, structural, controls, and process engineering can solve conflicts before they become field change orders. That same value extends to automation coordination, PLC modifications, SCADA visibility, utility routing, and commissioning. In food and beverage environments, fire protection is rarely an isolated package. Some firms also add value through equipment manufacturing and integration support. Custom stainless process equipment, skids, tanks, or utility packages may affect hood geometry, line spacing, or maintenance access, so a project partner that understands fabrication and layout can better align suppression design with production objectives. The comparison chart shows why many owners now prefer integrated delivery. The advantage is not just construction speed. It is reduced risk across design, controls, and operational restart. When evaluating U.S. suppliers, owners should compare more than system price. They should ask about hazard analysis depth, listing compliance, local permitting support, integration with exhaust and makeup air, controls capability, commissioning process, and after-service reach. In major regional markets such as North Carolina, Texas, California, Illinois, and Florida, local fire code interpretation can vary, so national consistency combined with local trade coordination is a significant advantage. Disruptive Process Solutions supports food and beverage manufacturers across North America with an approach built around engineering, construction coordination, and execution management rather than siloed contracting. In fire suppression-related projects, that matters because the system often sits at the intersection of process equipment, ventilation, controls, utilities, structural supports, and facility operations. You can learn more about the company background on the about our team page. From a technological capability standpoint, DPS works across structural, mechanical, plumbing, electrical, process, and controls disciplines. That broad engineering view is useful when suppression design must align with PLC logic, SCADA visibility, utility loads, equipment relocation, or line expansion plans. In a real food plant, the best fire protection solution is usually the one that fits the operating model, not just the drawing set. From a manufacturing capability standpoint, DPS also understands how equipment design affects plant layout and protection strategy. The company supports custom processing equipment and integrated systems, including tanks, CIP packages, tumblers, and cooking-related process solutions, which gives added perspective when nozzle placement, access clearances, washdown realities, or utility routing interact with fabricated equipment. More detail on broader capabilities is available through the equipment solutions section. From a service capability standpoint, DPS operates with a design-build-manage philosophy that helps owners move from concept to execution with tighter coordination. That includes planning, engineering, project management, installation oversight, and integration support for food, beverage, protein, dairy, aseptic, and prepared-food applications across the United States and Canada. For owners assessing complete project support, the engineering and project services page provides a broader picture, and selected project examples can be explored in the case study library. For clients evaluating fire suppression within a larger capital program, this integrated model is often valuable because hood protection is rarely the only issue. It may connect to line expansion, utility upgrades, process relocation, or facility modernization. In those situations, the ability to engineer, build, and manage under one coordinated strategy can reduce both timeline risk and operating disruption. What is the main difference between wet chemical and dry chemical systems?Wet chemical systems are mainly used for commercial cooking hazards involving grease and oils, while dry chemical systems are more often applied to industrial hazards outside typical kitchen grease applications. Is NFPA 96 relevant for food manufacturing plants?Yes, whenever the facility includes commercial cooking operations, hood systems, grease ducts, and related protection. It is highly relevant for prepared-food plants, commissaries, institutional kitchens, and mixed production sites. Can one facility use both wet and dry chemical systems?Yes. Many U.S. food facilities use wet chemical protection over cooking lines and a different special hazard approach in industrial support areas, depending on the risk. How often should a suppression system be inspected?The exact schedule depends on system type, manufacturer listing, and local authority requirements, but regular visual checks and formal service intervals are essential. Semiannual servicing is common for many hood systems. What happens if we change appliances under an existing hood?The suppression design should be reviewed immediately. New appliance geometry, heat release, or oil capacity can invalidate the original nozzle arrangement and coverage listing. Do alarm and fuel shutoff interlocks really matter that much?Yes. A suppression system without reliable interlocks may not fully remove the ignition source. Functional testing is one of the most important parts of commissioning and maintenance. What should owners ask potential suppliers before buying?Ask about hazard-specific design, code and AHJ coordination, appliance listings, ventilation integration, controls expertise, commissioning process, maintenance support, and experience in food and beverage environments. What are the biggest 2026 trends in the United States?The biggest trends are integrated design-build delivery, stronger insurer scrutiny, better controls integration, retrofit modernization of aging hood systems, sustainability-driven ventilation optimization, and greater focus on maintainability and documented compliance. How does sustainability affect suppression design?Sustainability is influencing hood and fan upgrades, smarter exhaust control, reduced rework, and better lifecycle planning. Owners increasingly want safer systems that also support energy-conscious ventilation strategies. Where is demand strongest in the U.S. market?Demand is strongest in prepared foods, institutional kitchens, protein processing, fast-growing commissaries, and facilities in high-density logistics and manufacturing regions such as Texas, California, the Southeast, and the Mid-Atlantic. In closing, the best 2026 fire suppression strategy for a food facility in the United States is the one built around real hazards, real operations, and real compliance pathways. Wet chemical systems remain the first choice for commercial kitchen lines. Dry chemical systems still have a role in industrial hazard areas. But neither should be selected in isolation. The most effective projects integrate ventilation, controls, utility shutdown, maintenance planning, and long-term plant performance from the beginning. -
Food Plant Dust Collection System Design for Combustible Dust Compliance
Food manufacturers in the United States face a difficult balancing act: control airborne dust, protect workers, preserve sanitation, and comply with combustible dust expectations without hurting throughput. In flour handling, sugar transfer, spice blending, cocoa processing, dairy powder packaging, seasoning systems, and plant protein operations, a poorly designed dust collection system can create housekeeping burdens, product loss, filter failure, fire risk, and major shutdown exposure. A well-designed system does the opposite. It stabilizes air movement, captures dust at the source, supports sanitation programs, and aligns the plant with recognized combustible dust safety practices. Across major food production hubs such as Chicago, Kansas City, Fresno, Dallas, Atlanta, Charlotte, Minneapolis, and California’s Central Valley, manufacturers are upgrading dust control for both brownfield retrofits and greenfield projects. Coastal trade and import corridors including the Ports of Los Angeles, Long Beach, Houston, Savannah, and New York/New Jersey also drive demand because ingredients often arrive, transfer, and repackage in facilities where dust hazard management is critical. In these settings, dust collection design should not be treated as a stand-alone equipment buy. It must be engineered as part of the broader process, utility, controls, sanitation, and building strategy. The quickest answer is this: a compliant food plant dust collection system in the United States should be designed from the pickup point backward. Start by identifying the dust type, Kst and Pmax data when available, moisture behavior, minimum explosible concentration concerns, and the process steps generating dust. Then calculate required airflow at each hood or enclosure, size the collector for total cfm plus diversity and pressure losses, maintain conveying velocity that prevents settling, select filters compatible with the product and cleaning method, and determine whether the dust hazard requires explosion venting, isolation, suppression, or a different prevention approach under the facility’s risk basis. For most food applications, the right design path includes: Buying advice for United States food manufacturers is straightforward: avoid purchasing a collector based only on cfm nameplate or unit price. The cheapest collector is often the most expensive system once duct losses, explosion protection, utility demand, maintenance labor, and product changeover downtime are included. Plants producing bakery mixes, nutritional powders, spices, powdered beverage bases, protein ingredients, sugar products, and cereal components should evaluate the full system life cycle, not just the fan package. The table above shows why system design must reflect process reality. The same collector model can perform well in one plant and fail in another because the operating objective changes by product, room layout, sanitation method, and dust explosibility. The growth trend reflects stronger investment in safety retrofits, labor-saving maintenance, and food-grade process modernization. By 2026, many facilities are expected to prioritize digital monitoring, lower energy fans, and better integration between dust systems and production controls. Dust collector sizing starts with required capture performance, not catalog capacity. In food plants, each pickup point should be assigned a target airflow based on one of three conditions: open hood capture, partial enclosure, or full enclosure/negative pressure containment. Open dump stations often require substantially more air than enclosed screw transfer points. A small leak path on a bag dump station can change the required airflow enough to make a previously “adequate” collector ineffective. Designers typically total branch airflows, apply a diversity factor if operations do not run simultaneously, and then add an engineering margin. Static pressure must include hood entry loss, branch duct loss, fittings, blast gates where applicable, main duct friction, collector pressure drop, filter loading allowance, safety devices, and discharge losses. This full-system method is what prevents the classic error of buying a collector with the right cfm but the wrong fan performance. For food facilities in humid Gulf Coast environments like Houston or New Orleans, moisture behavior can alter filter loading and dust adhesion. In dry inland climates like Denver or parts of California, static generation and particle transport can become more significant. In both cases, sizing should reflect local operating conditions rather than generic assumptions. The table highlights that sizing is a balancing exercise. High duct velocity helps transport dust, but excessive velocity can increase abrasion, fan energy, and usable product loss. Large filter area can improve filter life, but too much idle capacity may undermine pulse cleaning efficiency or increase total installed cost without solving the real process problem. Industry demand also differs by sector. Dry ingredient processing and powder packaging generally need more robust source capture than wet processing lines, while spices and flavorings often demand more specialized filter and odor control decisions. Plants comparing product types should also understand how bulk density, particle size, and hygroscopic behavior affect system design. Flour behaves differently from cocoa. Powdered sugar behaves differently from salt. Casein behaves differently from starch. These distinctions matter when selecting hoods, branch sizes, cleaning cycles, and discharge handling. In the United States, safe combustible dust design in food plants is strongly influenced by NFPA-based thinking, insurance expectations, local authority review, and internal corporate risk standards. A good design addresses hazard recognition, ignition source control, dust accumulation prevention, equipment grounding and bonding where required, access for cleaning, and event mitigation or isolation strategies where the dust hazard justifies them. For food plants, a safe design is more than adding an explosion vent to a collector. It includes reducing fugitive dust in the building, minimizing horizontal ledges, selecting appropriate housekeeping approaches, designing for inspection, and preventing flame or pressure propagation into connected equipment where necessary. The dust collector must be treated as one node in a larger process hazard picture. Key practical design questions include: This table matters because compliance is not a single document; it is a practical design condition. Facilities in states such as North Carolina, Texas, California, Illinois, and Pennsylvania often face different combinations of insurer scrutiny, municipal interpretation, and corporate engineering standards. The best approach is a documented design basis that ties process data, equipment decisions, and protection choices together. Choosing between explosion venting and prevention or suppression strategies depends on risk, layout, cost, occupancy, and collector location. Outdoor collectors with clear vent discharge paths may be suitable candidates for venting. Indoor collectors, collectors near walkways, or systems serving occupied production zones may require alternate strategies because a vented event still produces a violent discharge and must be directed safely. Prevention and protection options are not interchangeable in every case. Some sites benefit from venting plus isolation. Others require suppression due to indoor location or space limitations. In dense retrofit environments such as legacy plants in the Northeast or Midwest, equipment spacing, roofline constraints, and utility congestion often drive the decision more than equipment list price. When comparing options, buyers should review: The comparison above helps explain why no single solution is always “best.” The right decision is the one that fits the process, building, hazard data, and operating model. Food manufacturers planning expansions in Atlanta, Phoenix, Dallas-Fort Worth, or Inland Empire distribution corridors should examine outdoor collector placement early, before civil, traffic, or utility routing limits the safest options. Ductwork is where many food dust collection projects succeed or fail. Even a quality collector cannot overcome poor branch takeoffs, excessive elbows, oversized mains, or dead legs where dust settles. Layout should minimize pressure loss while maintaining transport velocity for the actual dust being conveyed. The design must also respect structural clearances, sanitation access, electrical routing, and future maintenance needs. In practical terms, optimized ductwork means short, direct runs where possible, smooth transitions, disciplined branch balancing, and careful routing around process equipment. It also means avoiding the temptation to oversize duct “for future capacity” unless fan control and branch operation truly support that future state. Oversized mains often lower velocity below safe transport levels during partial load operation. Food applications with multiple intermittent pickups should be modeled according to actual operating sequences. A dump room that runs two stations at a time behaves differently from a packaging hall with ten simultaneously active points. Velocity optimization should therefore reflect real operating logic, not best-case assumptions. By 2026, more projects are expected to use digital balancing support, variable frequency drive fan control, and pressure monitoring to maintain stable transport conditions as production shifts. That trend is especially relevant for multiproduct contract manufacturers and co-packers whose line usage changes week to week. The area chart shows a realistic technology shift: fixed, manually balanced systems are giving way to smarter systems that support changing production loads, energy management, and maintenance alerts. This is increasingly important in labor-constrained markets. Filter selection should reflect dust characteristics, cleaning method, sanitation approach, humidity, and available maintenance labor. Fine, dry flour dust may perform acceptably with one media choice, while sticky seasoning or oily cocoa dust may require different media, surface treatments, or pre-separation strategy. In food plants, maintenance scheduling is not just a reliability issue; it also affects product quality, housekeeping, and labor planning. A good maintenance program includes differential pressure trending, pulse cleaning review, hopper discharge checks, leak testing, gasket inspection, and documented replacement intervals. Plants that wait for a visible emission problem usually replace filters too late, after product contamination risk or fan overloading has already increased. This table shows why filter selection and maintenance should be planned together. It is not enough to choose a media type. The plant must also decide who monitors pressure, when changeouts occur, how spare parts are stocked, and how maintenance is coordinated with sanitation and production windows. ATEX is not the primary regulatory framework for most United States food plants, but it remains relevant for multinational operators, export-oriented facilities, and corporate engineering teams that standardize equipment practices across North America and Europe. If a U.S. manufacturer shares design standards with plants in Ireland, Germany, the Netherlands, or Spain, ATEX zone thinking may influence enclosure choices, instrumentation, grounding practices, and equipment procurement. For dust hazards, the useful takeaway is not to force European classifications into every U.S. project, but to understand how hazardous area categorization can support disciplined equipment selection. This is especially true for global food brands with engineering governance across multiple regions. The value of the table is practical: zone thinking helps define where releases are credible and where equipment needs more disciplined review. For U.S. facilities serving both domestic and international networks, this can improve design consistency even when NFPA-based methods remain the primary framework. Dust collection and HVAC should be designed together. If the dust collector removes a large amount of conditioned air from a room without proper makeup and pressure control, the plant can suffer from door-opening issues, unstable room temperatures, sanitation drift, and migration of dust into cleaner zones. This is particularly important in facilities with powder handling adjacent to packaging, allergen segregation rooms, or temperature-controlled ingredient spaces. Integration topics include room pressure cascades, tempered makeup air, dehumidification strategy, exhaust discharge location, odor control, and control system communication. In cold-weather markets such as Minnesota, Wisconsin, or upstate New York, heated makeup air can significantly affect operating cost. In humid southeastern markets like Georgia, the Carolinas, and Florida, latent load and condensation control may become more important than sensible cooling. Food manufacturers often underestimate this interaction. A dust collection retrofit that appears simple at the process line can become an HVAC project once room pressure, rooftop unit capacity, and makeup air pathways are evaluated. This is one reason integrated engineering usually delivers better outcomes than isolated equipment purchasing. In new facilities, dust collection and HVAC integration should also consider 2026 sustainability goals: fan efficiency, heat recovery feasibility, reduced compressed air consumption for pulse cleaning, lower rework from escaped dust, and controls that match airflow to actual production demand. Manufacturers seeking support for this level of planning should look for engineering partners able to bridge process, utilities, mechanical systems, and controls. That integrated capability matters more than a large product catalog. For project examples and broader facility delivery approaches, manufacturers can review food and beverage project case studies to understand how process utility decisions affect overall plant performance. Disruptive Process Solutions works with food and beverage manufacturers across the United States and Canada on capital projects where process performance, compliance, and commercial outcomes all matter. Rather than approaching a dust collection project as a stand-alone mechanical package, DPS evaluates how it fits into the broader production environment, from ingredient receiving and transfer through utilities, controls, commissioning, and long-term maintainability. On the technological side, DPS supports structural, mechanical, plumbing, electrical, process, and controls engineering with practical integration across plant systems. That matters in combustible dust projects because the collector, fan, duct routing, interlocks, alarms, PLC logic, utilities, and building airflow all need to work together. Clients looking for a partner that can coordinate process systems with automation, SCADA, and utility infrastructure can learn more about these integrated offerings through the company’s engineering and project services. On the manufacturing side, DPS also brings hands-on process equipment experience that is highly relevant to food plants handling powders, ingredients, and utility-intensive systems. The company supports complete processing environments across food and beverage sectors and manufactures selected proprietary equipment, giving project teams a stronger understanding of how equipment design, cleanability, and installation details influence real operating performance. More information on this capability is available in the company’s process equipment portfolio. On the service side, DPS operates with an end-to-end design, build, and manage model that helps manufacturers move from concept and capital planning through installation and execution oversight. For dust collection projects, that can include feasibility review, layout development, utility coordination, contractor management, startup planning, and alignment with food facility standards. Because many clients are balancing expansion, relocation, retrofit, and compliance work simultaneously, this broader project discipline often prevents costly late-stage changes. Companies wanting to understand the team’s operating approach and background can visit the DPS company overview. DPS serves both food and beverage operations, including bakery ingredients, proteins, prepared foods, dairy, aseptic environments, breweries, spirits, RTD beverages, and co-packing facilities. That cross-sector experience is useful because many dust projects sit at the intersection of ingredient handling, utility infrastructure, sanitation expectations, and production economics. In practice, clients benefit when engineers understand both the mechanical details of air handling and the business implications of downtime, yield loss, and future expansion. For buyers in the United States, the best supplier is rarely the one with the longest brochure. It is the one that can define the problem correctly, integrate the answer with the full plant, and protect long-term profitability. That is particularly true for combustible dust systems, where poor coordination can create hidden costs for years. What dusts in food plants are commonly considered combustible?Many dry organic food materials can present combustible dust concerns, including flour, sugar, starch, cocoa, spices, powdered dairy products, grain dust, and some plant protein ingredients. Actual risk should be based on tested data and process conditions, not assumption alone. Should the dust collector be located outdoors?Often yes, especially when explosion venting is being considered and a safe discharge path is needed. However, climate, maintenance access, duct length, sanitation logistics, and site constraints may affect that decision. How do I know if my current collector is undersized?Common signs include visible dust escape at pickup points, frequent housekeeping around transfer areas, abnormal filter pressure trends, plugged ducts, poor capture during peak production, and operators opening access doors to make the process work. Is a baghouse always better than a cartridge collector?Not always. The right choice depends on dust characteristics, loading rate, footprint, service access, filter media needs, and protection strategy. Food dust behavior varies widely, so collector type should be matched to the application. Can HVAC alone control food dust?No. General room ventilation can help room conditions, but it is not a substitute for source capture. Dust should be captured where it is generated, then coordinated with the room HVAC strategy. What is the biggest purchasing mistake plants make?Buying on cfm alone. A collector that looks large enough on paper may fail if the fan cannot overcome actual static pressure, if ducts are poorly designed, or if the filter media is wrong for the product. How often should filters be replaced?There is no single interval. Replacement should be based on differential pressure trends, emissions performance, media condition, process changes, and maintenance history. Plants with recipe variation should monitor by product family, not calendar alone. Why discuss ATEX in a U.S. article?Because many U.S. manufacturers operate globally or follow international corporate standards. ATEX concepts can still be useful for equipment review and hazardous area discipline, even when U.S. codes drive the main compliance framework. What trends are shaping 2026 dust collection projects?Expect stronger focus on energy-efficient fans, variable flow control, smart differential pressure monitoring, improved fire and explosion protection integration, sustainability reporting, and dust systems designed alongside HVAC and utility optimization rather than after the fact. When should engineering start?As early as possible. The best time is during feasibility or early layout planning, before process equipment, utility routes, roof penetrations, and egress paths are locked in. Early design usually lowers both risk and total installed cost. For United States food manufacturers, combustible dust compliance is not only a safety obligation. It is a design discipline that protects uptime, sanitation, labor efficiency, and capital returns. Whether the project involves a single dump station retrofit or a new multi-line powder handling facility near Chicago, Houston, Fresno, Atlanta, or the Port of Savannah, the right dust collection system is one that is sized correctly, integrated properly, and managed as part of the entire production environment. -
2026 Food Plant Emergency Shutdown System Design Guide for Process Safety
Emergency shutdown system design in a U.S. food plant is not just an electrical or controls task. It is a process safety strategy that must isolate hazards, protect personnel, prevent ignition, preserve sanitation boundaries where practical, and allow a facility to return to production quickly after an event. In food and beverage operations, the best ESD program combines clearly defined shutdown zones, fail-safe field devices, code-compliant power isolation, coordinated PLC and SCADA logic, documented testing routines, and a hazard analysis that matches the real process risks on site. For operators in major production regions such as Chicago, Dallas-Fort Worth, Fresno, Atlanta, Charlotte, Houston, Kansas City, Omaha, and the Inland Empire, that means designing systems that work equally well in greenfield plants, brownfield retrofits, cold storage expansions, aseptic rooms, bottling halls, and protein processing lines. The U.S. market is moving toward more integrated shutdown strategies because modern plants are more automated, more utility-dense, and more dependent on continuous throughput. A simple hardwired e-stop loop is rarely enough in a facility with ammonia refrigeration interfaces, clean-in-place skids, batching systems, retort lines, high-speed fillers, boiler rooms, compressed air, process wastewater handling, and high horsepower packaging assets. At the same time, over-design can create nuisance trips, sanitation delays, and excessive restart costs. The practical goal is selective, safe, code-aligned shutdown. For project owners evaluating a new system, the smartest buying advice is to start with hazard ranking and operational zoning before hardware selection. Many plants first ask which safety relay, PLC, or disconnect to buy, but the higher-value question is which scenarios must stop instantly, which assets must coast to a controlled stop, which utilities must remain live for life safety, and which operations need product containment to avoid contamination or spoilage. That is especially important in sectors such as dairy, prepared foods, brewing, beverage co-packing, aseptic processing, seafood, and ready-to-eat proteins, where process continuity and safety have to be balanced carefully. Across the United States, implementation trends for 2026 include deeper use of safety-rated PLCs, segmented network architectures, diagnostics-rich field devices, digital test logging, cybersecurity controls for shutdown logic, and sustainability-driven shutdown sequences that reduce water loss, product waste, and uncontrolled dumping. Policy pressure is also rising through insurer scrutiny, owner standards, and closer alignment between process safety expectations and electrical compliance practices. Food manufacturers near ports and trade corridors such as Los Angeles/Long Beach, Savannah, Newark, Tacoma, and Houston are also investing more in resilient shutdown design as supply-chain volatility makes unplanned downtime more expensive. An effective emergency shutdown system for a food plant in the United States should be based on six core decisions: define credible hazards, divide the plant into shutdown zones, assign fail-safe actions by equipment type, comply with NFPA 70 NEC and related electrical requirements, integrate shutdown logic with process automation without weakening independence, and maintain the system through scheduled testing and documentation. In practice, that means a refrigerated protein plant in Omaha will need different shutdown priorities than a beverage blending and packaging site in North Carolina or an aseptic dairy facility in California. Most food and beverage facilities benefit from a layered ESD approach: From a market perspective, U.S. food manufacturers are spending more on shutdown modernization in brownfield facilities than on purely new greenfield systems, because legacy plants often have mixed-voltage assets, undocumented wiring, older PLC generations, and disconnected maintenance records. Product types commonly included in an ESD scope are line e-stops, utility shutdown panels, gas valve trains, pump interlocks, conveyor isolation, boiler room interfaces, refrigeration tie-ins, retort safeties, mixer and grinder stops, and area annunciation. Buyers should prioritize system simplicity, device availability, environmental ratings, sanitation compatibility, and ease of annual proof testing. The table above shows why a single shutdown philosophy rarely fits every process area. Good design aligns the action to the hazard, not just to the equipment list. The market growth trend reflects a practical reality: as automation intensity rises and downtime costs climb, plants increasingly treat emergency shutdown architecture as a capital risk-management tool rather than a narrow compliance purchase. System architecture should start with a documented cause-and-effect matrix. That matrix connects initiating events to logic actions and final elements. For example, a high-high pressure event in a syrup blending skid may need to stop positive displacement pumps, close inlet valves, hold vessel venting logic, generate a horn/beacon alert, and block restart until operator verification is complete. A line e-stop in a packaging lane may only need to de-energize motion equipment in that lane while preserving refrigeration, compressed air, and adjacent fillers. In U.S. food facilities, the most common architecture types are hardwired relay systems, hybrid relay-plus-PLC systems, and safety PLC platforms. Hardwired systems are simple and transparent, but they can become difficult to scale in plants with many zones. Hybrid systems are common in mid-size facilities where certain safety functions remain independent while automation supervises status and recovery. Safety PLC systems support more diagnostics, sequence control, and selective shutdowns, but they demand stronger specification, validation, and cybersecurity discipline. Component selection should account for washdown exposure, corrosive chemicals, temperature extremes, and maintenance access. In a poultry plant in Arkansas or a seafood site in the Pacific Northwest, NEMA enclosure ratings and hygienic mounting details can be as important as the electrical rating itself. In beverage plants with frequent caustic and acid cleaning, pushbuttons, pull cords, and junction boxes should be chosen for chemical resistance and easy replacement. The component table matters because ESD performance depends on the last device in the chain as much as the controller. Plants often invest in advanced controls while leaving weak final elements in place. That creates a false sense of safety. From a technology capability standpoint, Disruptive Process Solutions supports integrated process, electrical, and controls engineering for food and beverage clients across North America. That multidisciplinary capability is important for ESD work because shutdown design touches PLC programming, SCADA visibility, utility coordination, equipment interfaces, and mechanical process behavior at the same time. A line can only shut down correctly if controls logic and process design were developed together. NEC compliance is fundamental because emergency shutdown systems operate inside the broader electrical infrastructure of the facility. While ESD design also intersects with machinery safety, fire protection, and insurer requirements, NFPA 70 sets the baseline for wiring methods, disconnecting means, overcurrent protection, equipment installation, hazardous area considerations where applicable, grounding, working clearances, labeling, and maintenance implications. In food plants, compliance mistakes often appear during expansions when new process skids are connected to existing MCCs, panelboards, utility feeds, or control networks without a coordinated review. Emergency shutdowns should not create unintended electrical hazards. For instance, tripping a feeder without considering downstream control power, loss of ventilation, or recovery state can make an event worse. Likewise, disconnecting sanitation systems or freezer door controls in the wrong sequence can introduce secondary operational risks. NEC-aligned design therefore needs one-line review, arc flash implications, selective coordination strategy where needed, enclosure suitability, and field labeling consistency. Facilities in industrial corridors like Houston, New Jersey, Memphis, and Southern California often operate under aggressive production schedules, so brownfield shutdown upgrades must be designed for phased installation. That makes lockable disconnect locations, temporary feeds, panel separation, and commissioning windows especially important. The compliance checklist above is useful because many ESD failures are not logic failures; they are installation failures. A perfect sequence in software cannot overcome inaccessible disconnects, degraded enclosures, or poor field labeling. For buyers, the practical advice is to request a shutdown scope that includes electrical field verification, panel schedules, one-line updates, and a commissioning checklist tied to code compliance. If that work is not included, owners often discover expensive rework late in the project. Integration is where shutdown systems become truly valuable. An isolated e-stop circuit can stop equipment, but an integrated ESD can also preserve data, guide operators, prevent conflicting commands, and support faster recovery. In food processing, integration usually involves PLCs, HMI screens, SCADA historians, VFD status, recipe systems, utility controls, and alarm management. The key rule is that visibility and coordination can be integrated, but the safety function itself should remain robust and fail-safe. For example, when a filler room zone trips in a high-speed RTD beverage plant, the control system may need to stop depalletizers, cap feeders, labelers, and packers in staged logic while logging the event, preserving fault context, and preventing upstream overflow. In a protein grinding room, shutdown integration may need to stop grinders and augers immediately while allowing extraction or sanitation support systems to continue under controlled conditions. In an aseptic process, the sequence may include diversion, hold, sterile boundary protection, and quality event capture. Industry demand for integrated ESD is strongest in sectors with dense automation and expensive restarts. The bar chart shows why automation-linked shutdown design is especially relevant in beverage, aseptic, and protein operations where throughput, quality, and hazard exposure are closely coupled. Technologically, DPS works in the space where process engineering and automation meet. Its teams handle controls engineering, PLC programming, SCADA integration, and broader system coordination as part of complete process projects. That capability is useful when shutdown actions must align with equipment behavior such as pasteurization, retort, distillation, fermentation, batching, water treatment, or CIP. Instead of treating ESD as an isolated cabinet package, an integrated team can connect the shutdown philosophy to the actual manufacturing process. Local supplier strategy matters as well. U.S. plants often source safety hardware through regional electrical distributors near hubs like Charlotte, Milwaukee, Cincinnati, and Sacramento, while relying on national integrators for programming and startup. Owners should evaluate not only brand preference but also replacement lead times, field technician availability, and whether local maintenance teams already know the platform. Zone-based design is the best way to prevent both underreaction and overreaction. Instead of tripping the entire plant for every event, a zone strategy defines which process areas, utilities, and material flows are linked to a given hazard. This approach is especially effective in large U.S. facilities with multiple packaging halls, utility yards, ingredient rooms, and segregated hygienic spaces. A shutdown zone can be geographic, functional, or hazard-based. Geographic zones may separate raw processing from ready-to-eat packaging. Functional zones may isolate boiler house, refrigeration engine room, syrup room, or CIP center. Hazard-based zones may group all equipment affected by a flammable cleaning solvent interface, high-pressure steam network, or confined machinery line. The right structure depends on process flow, sanitation barriers, utility dependencies, and restart economics. The zone matrix above illustrates how selective shutdown protects both people and production. It is especially useful in facilities where one line issue should not dump the whole utility backbone. Trend-wise, 2026 designs increasingly use digital zoning tied to visualization layers in SCADA. Operators can see which assets are in each shutdown boundary, which permissives are preventing restart, and which field devices must be reset. That reduces confusion during stressful events. The area trend indicates a clear move toward smarter, narrower shutdown boundaries. That shift is driven by cost control, sustainability, and operator usability. An ESD system that is not tested should be treated as an assumption, not a safeguard. Food manufacturers often install shutdown hardware during a project but fail to maintain proof-test discipline after startup. That is a serious weakness because washdown environments, vibration, sanitation chemicals, thermal cycling, and production changes can degrade system performance over time. Testing should include field initiation devices, logic behavior, final element action, HMI and alarm indication, sequence timing, event logging, and restart permissives. Plants should define who owns each test: maintenance, controls, operations, EHS, or an outside specialist. The best protocol combines monthly visual checks, quarterly functional tests for selected devices, annual full-sequence validation, and change-management review whenever equipment is modified. This maintenance schedule is effective because it separates routine inspection from full proof testing. Many facilities do one or the other, but reliable systems need both. From a service capability perspective, companies that can design, install, integrate, and commission the system are often better positioned to create testable documentation. DPS uses a design-build-manage approach, meaning engineering intent, field execution, and startup coordination stay aligned through the project lifecycle. That matters when maintenance teams need accurate cause-and-effect lists, panel documentation, and realistic turnover packages rather than a stack of disconnected drawings. More detail on the firm’s project model is available on the company overview page. Risk assessment should drive the shutdown philosophy, not merely validate it after the fact. In food and beverage facilities, hazard analysis must look beyond fire and shock to include pressure release, thermal injury, chemical exposure, rotating equipment, product contamination, sanitation interactions, utility dependency, and environmental release. A plant with ammonia refrigeration interfaces, high-pressure steam, or caustic CIP service needs a more rigorous methodology than a small dry-pack line with isolated conveyors. Several methods are commonly used in the United States: process hazard analysis workshops, HAZOP-style reviews, what-if analysis, failure mode and effects analysis, machine risk assessment, and layer of protection thinking for higher-consequence systems. The best method depends on the process. A beverage blending line may benefit from what-if plus control narrative review, while a retort or aseptic project may need a more structured node-based analysis. The reason this comparison matters is simple: if the analysis method is too shallow, the shutdown design will likely be too generic. Better hazard analysis usually leads to fewer unnecessary trips and stronger protection where it truly matters. Applications vary by industry. Dairy plants often focus on CIP chemical handling, homogenization, and thermal loops. Protein facilities prioritize mechanical injury, sanitation chemical exposure, and refrigeration interfaces. Beverage sites emphasize high-speed packaging, CO2 systems, syrup handling, and utility resilience. Prepared foods operations may need integrated responses across cook, chill, fill, and freezer zones. Implementation success depends on more than design documents. In working U.S. food plants, shutdown projects must be installed around sanitation windows, production demands, utility outages, seasonal demand peaks, and inspection schedules. That is why design-build delivery can be effective for ESD modernization: engineering, procurement, field coordination, and commissioning are managed as one execution path rather than isolated tasks. Best practices include early field walkdowns, existing condition verification, tagged photo surveys, sequence workshops with operators, spare parts standardization, phased panel cutovers, FAT/SAT planning, and restart training. Owners should require a shutdown narrative, I/O list, panel schedule updates, one-line revisions, cause-and-effect matrices, and operator reset procedures before construction starts. It is also wise to identify long-lead items and local substitute options in case preferred components are delayed. Case studies in the U.S. market repeatedly show that the greatest savings come from solving the real bottleneck rather than buying the largest hardware package. On capital projects, that may mean revising PLC logic and zone boundaries instead of replacing every panel. On a relocation or expansion, it may mean integrating existing skids more intelligently instead of rebuilding proven equipment from scratch. Project examples and execution approaches can be explored through DPS project case studies. On the manufacturing side, DPS not only integrates third-party systems but also supplies proprietary process equipment such as tanks, CIP systems, marination tumblers, and cooking vessels as part of broader plant solutions. That manufacturing capability can reduce interface risk on projects where shutdown logic must coordinate tightly with process skids, vessels, pumps, and utility tie-ins. The company’s available equipment solutions show how in-house and integrated assets can support a more cohesive plant design. The implementation table highlights a major truth of ESD projects: most expensive failures happen at interfaces, not inside the specification. Good design-build delivery reduces those interface gaps. The comparison chart shows why many owners use both local suppliers and specialized integrators. Local distributors win on parts access, while integrated design-build partners usually outperform on process understanding, system coordination, and lifecycle support. Disruptive Process Solutions serves food and beverage manufacturers throughout all 50 U.S. states and Canada with a model built around engineering, construction coordination, and execution management. For clients planning emergency shutdown work, that matters because ESD is rarely a stand-alone purchase. It usually touches process equipment, utilities, controls, electrical distribution, startup sequencing, sanitation, and long-term operational strategy. In technology, DPS brings process, mechanical, electrical, and controls expertise together, including PLC programming, automation, SCADA, utility integration, and system commissioning. In manufacturing, the company supplies selected proprietary process equipment that can be integrated into broader plant projects, helping reduce mismatch between equipment behavior and control intent. In service delivery, DPS operates through a design-build-manage structure that supports feasibility studies, capital planning, owner’s representation, engineering design, general contracting functions where applicable, installation oversight, and turnkey execution. That model is especially useful for U.S. food and beverage plants that need practical shutdown strategies rather than generic templates. Whether the project involves a brewing operation in Colorado, a co-packer near Atlanta, a dairy expansion in Wisconsin, a prepared foods line in Texas, or an aseptic system in California, the objective is the same: build a shutdown plan that protects people and assets while supporting long-term profitability and maintainability. What is the difference between an e-stop system and a full ESD system?An e-stop system usually focuses on immediate machine stopping at local operator access points. A full ESD system includes broader cause-and-effect logic, utility interfaces, zone actions, annunciation, and structured restart controls across process areas. Do all food plants need a safety PLC?No. Smaller or simpler systems may be better served by hardwired safety relays. Plants with multiple zones, utility interactions, advanced automation, or complicated restart states often benefit from safety PLC architecture. How often should food plant emergency shutdown systems be tested?Visual inspections should typically occur monthly, selected functional tests quarterly, and full sequence verification at least annually. Frequency may need to increase in harsh washdown or high-change environments. Can an emergency shutdown damage product or sanitation conditions?Yes, if the sequence is poorly designed. That is why zone-based and process-aware logic is important. The safest sequence should also consider product containment, pressure relief, and chemical isolation. How does NEC compliance affect shutdown design?It affects disconnecting means, wiring methods, enclosure suitability, overcurrent protection, grounding, labeling, and maintainability. ESD logic must be supported by code-compliant electrical infrastructure. What industries benefit most from upgraded shutdown systems?High-automation beverage plants, dairy processors, protein facilities, aseptic operations, prepared foods manufacturers, and utility-dense co-packing sites often see the biggest gains from modernized ESD design. What should owners ask a supplier before buying?Ask for shutdown narratives, cause-and-effect matrices, proof-testing strategy, spare parts plan, field verification scope, local support coverage, and brownfield cutover methodology. Also ask who owns startup and post-start optimization. How do future trends affect 2026 projects?Expect more diagnostics, cybersecurity review, segmented shutdown zones, digital test records, stronger insurer scrutiny, and sustainability-oriented sequencing that reduces water, product, and energy waste during trips. In summary, a strong U.S. food plant emergency shutdown program is selective, documented, code-compliant, automation-aware, and maintained for the long term. Plants that treat ESD as part of overall process design, rather than as a late electrical add-on, usually achieve safer operations, fewer nuisance trips, and more reliable production performance. -
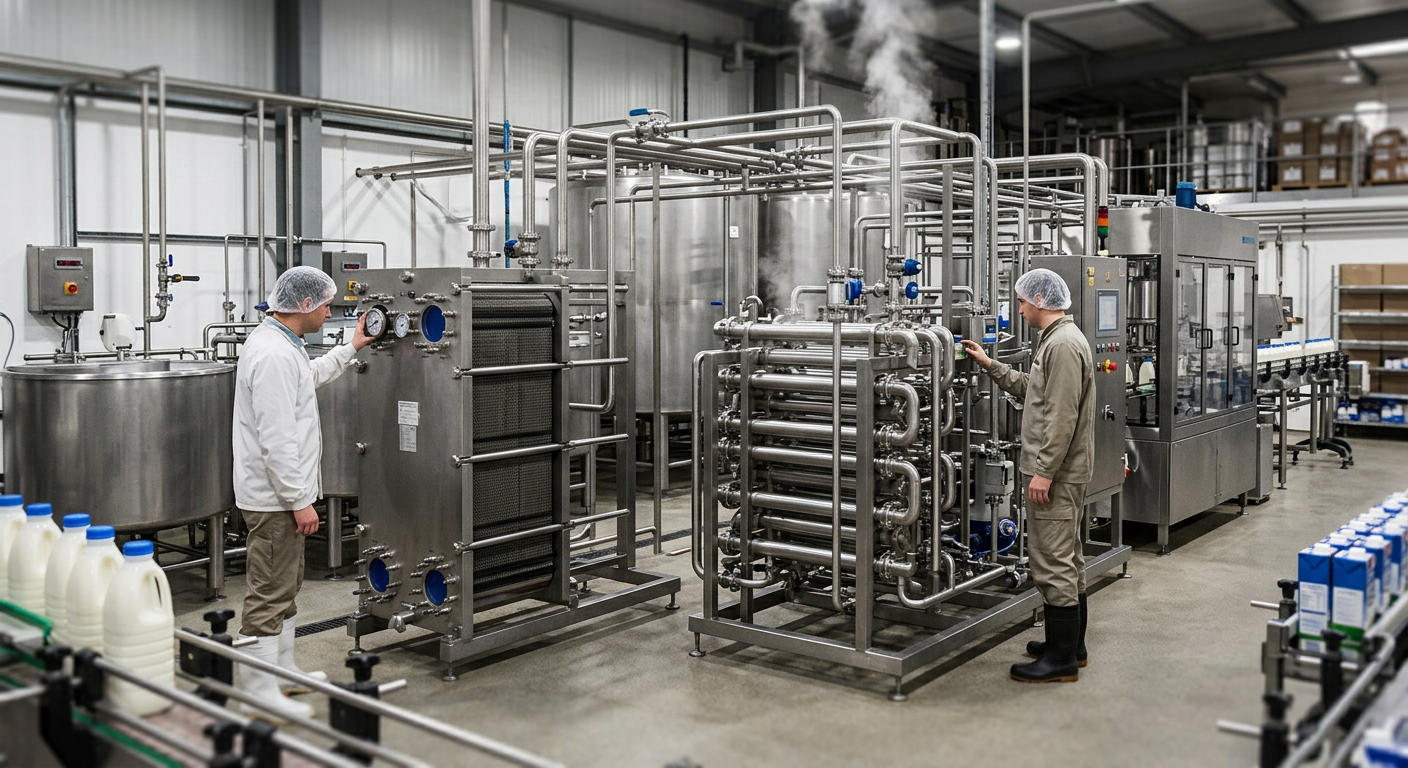
Food Facility Explosion Protection: 7 NFPA Standards You Must Know
Food and beverage plants in the United States increasingly handle combustible dusts, flammable vapors, sugar fines, starches, spices, grain solids, dairy powders, cocoa, protein ingredients, and alcohol-bearing process streams that can create serious explosion risk. Whether a plant is operating in the Midwest grain belt, along the Port of Houston, in California beverage production corridors, or in major logistics hubs such as Chicago, Atlanta, and Dallas-Fort Worth, owners must understand how core National Fire Protection Association requirements affect equipment design, building layout, utility systems, and operating procedures. For most facilities, the practical foundation includes NFPA 68 for deflagration venting, NFPA 69 for explosion prevention and isolation, Dust Hazard Analysis requirements, ignition-source control, and the transition to NFPA 660 as the consolidated combustible dust standard. This guide explains what U.S. manufacturers, engineering teams, and capital project leaders should know when planning new lines, retrofits, expansions, ingredient handling systems, milling rooms, spray drying operations, dust collection upgrades, and pneumatic conveying installations. It also covers how design-build delivery can reduce compliance gaps by aligning process engineering, construction, equipment integration, controls, and commissioning from the beginning. If you need the short version, here it is: U.S. food facilities that handle combustible dust or flammable atmospheres should evaluate their process against NFPA 68, NFPA 69, Dust Hazard Analysis expectations, ignition-source control practices, and the newer NFPA 660 framework. In real project terms, that means determining where dust can accumulate, identifying credible ignition sources, verifying whether equipment needs deflagration venting or suppression, deciding where explosion isolation is required between vessels and ducts, and ensuring that operating procedures match the engineered safeguards. For buyers and plant leaders, the biggest mistake is treating explosion protection as a late-stage add-on after equipment is purchased. The most successful projects in the United States integrate compliance into process design, structural support, duct routing, utility planning, controls logic, and construction sequencing from day one. This is especially important in high-throughput food sectors such as flour milling, cereal, bakery premix, sugar transfer, ingredient blending, seasoning systems, dry dairy, cocoa, and plant protein operations. The table above shows why explosion protection is both an engineering and operations issue. It affects layout, equipment selection, controls, employee training, maintenance planning, and insurance readiness. In many U.S. markets, a strong compliance program also improves insurer confidence and can support smoother Authority Having Jurisdiction review during expansions. NFPA 68 is the starting point when a vessel, bin, dust collector, dryer, bucket elevator, cyclone, or enclosure contains a combustible dust atmosphere that may experience a deflagration. The standard addresses how pressure can be relieved through venting so that the protected enclosure is less likely to rupture catastrophically. In food plants, this is commonly relevant to dust collectors serving sugar handling, flour transfer, powdered dairy ingredients, spice blending, starch systems, and plant protein powder operations. Deflagration vent design is not just about placing a panel on the side of equipment. Engineers must determine dust characteristics, enclosure volume, reduced explosion pressure, vent panel arrangement, vent duct effects, and discharge hazards outside the equipment. In an urban or tightly packed production environment such as New Jersey food manufacturing corridors, Los Angeles industrial zones, or redevelopment sites around Charlotte and Nashville, exterior vent discharge can be complicated by lot lines, roof geometry, pedestrian areas, and adjacent process skids. Vent ducts can significantly affect performance, so a collector inside a building often requires careful evaluation. Sometimes flameless venting or another protection strategy may be considered where traditional vent discharge is not practical. Structural supports, access platforms, cleaning access, weather exposure, and sanitation constraints also matter in food-grade environments. This table matters because many U.S. retrofit projects fail not in theory but in the field: panels become inaccessible, discharge zones conflict with truck lanes, or vent duct assumptions do not match the final installation. Good project planning reduces these late surprises. In practical buying terms, facility owners should ask equipment suppliers for pressure ratings, dust test assumptions, vent calculations, and the exact basis of design. If a supplier only sells the collector and leaves the vent discharge, support steel, access, and roof coordination to others, the owner can inherit a major integration risk. That is one reason many food manufacturers prefer a coordinated delivery team rather than separate, disconnected vendors. The line chart shows a realistic rise in U.S. capital investment for combustible dust and explosion protection measures. Growth is being driven by aging assets, insurer scrutiny, larger production throughputs, and the modernization of ingredient handling systems. NFPA 69 covers explosion prevention systems and can apply to a broad set of protective methods, including explosion isolation, suppression, oxidant concentration reduction, and spark detection arrangements depending on the process. In U.S. food plants, this often becomes critical when an explosion in one piece of equipment could propagate through interconnected ducts or conveyors into upstream or downstream equipment. A common example is a dust collector connected to process equipment by ductwork. If deflagration starts in the collector, the flame front and pressure wave can move back into indoor processing equipment unless suitable isolation is installed. This is why modern projects often include fast-acting valves, chemical isolation, rotary valve evaluations, abort gates, or other protective devices depending on the material and process configuration. NFPA 69 is especially relevant in complex production environments such as large snack plants in the Southeast, dry ingredient hubs in Kansas and Nebraska, and integrated protein or seasoning plants near Memphis, Indianapolis, and the Inland Empire. The more interconnected the system, the more important the isolation philosophy becomes. The table clarifies that “NFPA 69 compliance” is not one product purchase. It is a performance-based selection of methods that must match the process, material, duct arrangement, operating mode, and maintenance capability of the plant. A simple packaging line and a sophisticated spray-drying system do not need the same strategy. For operations teams, another key point is proof testing and lifecycle maintenance. An isolation valve that is never inspected or a suppression bottle that is past service interval weakens the entire protection scheme. Buyers should request not just the hardware price but also annual service assumptions, spare parts needs, and controls integration requirements. The Dust Hazard Analysis, or DHA, is one of the most important compliance tasks for U.S. food manufacturers. A DHA is a systematic review of where combustible dust hazards exist, how fires or explosions could occur, what safeguards are in place, and what additional actions may be needed. For food plants, the DHA often reveals that risk is not limited to one collector or one transfer point. Risk can extend across receiving, milling, blending, drying, packaging, rework, sanitation, and overhead building surfaces where fugitive dust accumulates. Food facilities should not assume a dust is harmless because it is edible. Flour, sugar, starch, cocoa, milk powder, coffee, grain, and many seasoning ingredients can present combustible dust hazards in the right conditions. DHA work typically evaluates process equipment, housekeeping, building surfaces, ducts, elevators, enclosed conveyors, electrical classification, hot work practices, and operator tasks. In aging brownfield plants around legacy manufacturing centers such as St. Louis, Milwaukee, Philadelphia, and Baltimore, DHA findings frequently lead to phased capital projects. These may include relocating collectors outdoors, improving aspiration systems, adding isolation devices, correcting housekeeping access limitations, or upgrading controls and interlocks. This table shows why a DHA is not just paperwork. It creates an action list that can affect capex, operating procedures, staffing, and insurer conversations. A strong DHA can also help prioritize projects so that owners spend money where risk reduction is most meaningful. For manufacturers evaluating expansion, the best timing is to perform or refresh DHA work before final equipment procurement. That way, protective features are designed into the project rather than retrofitted later at a premium. This is particularly valuable for new dry ingredient rooms, bulk bag unloading, central dust collection, and high-capacity conveying installations. Isolation and suppression are often the difference between a localized event and a plant-wide incident. Suppression works by detecting an event and rapidly discharging suppressant into the protected equipment. Isolation prevents flame and pressure from traveling between connected pieces of equipment. The right mix depends on process geometry, dust severity, production rates, sanitation needs, and available space. In food and beverage manufacturing, typical applications include dust collectors connected to mixers, sifters, packaging machines, grinders, hammermills, bucket elevators, spray dryers, and pneumatic transport lines. Suppression is often selected when venting outdoors is difficult or when building constraints make a vent duct impractical. Isolation is commonly mandatory where interconnections could spread the event into occupied process space. For buyers in dense industrial markets such as Boston-area food production, Seattle specialty ingredient plants, or mixed-use redevelopment zones around Denver, suppression and flameless or interior-friendly options may gain attention because exterior vent discharge space is limited. Still, these systems require a disciplined service culture. The bar chart highlights where demand is especially strong. Flour and grain remain leading segments, but plant protein and dry ingredient systems are also becoming major areas of compliance activity as formulation complexity increases. When comparing products, buyers should ask whether the supplier is merely a component vendor or can support process hazard interpretation, controls integration, startup testing, and long-term service. For many facilities, the cheapest hardware quote becomes the most expensive path if system interfaces are poorly coordinated. NFPA 660 matters because it consolidates combustible dust requirements into a more unified framework. For U.S. food manufacturers with multiple sites, this is significant. Instead of relying on fragmented interpretations spread across older standards and internal legacy documents, companies can use NFPA 660 as part of a more consistent corporate approach to hazard review, equipment protection, and management systems. This does not mean older hazards disappear or that all facilities need total redesign. It means engineering, EHS, maintenance, and operations leaders should update their internal standards, training language, and audit checklists to reflect the current structure of combustible dust compliance. For multi-site organizations with plants in Texas, the Carolinas, California, Ohio, and Ontario support operations, harmonization is especially valuable. NFPA 660 is also important for future capital planning. New lines, line relocations, and plant acquisitions should be evaluated against the consolidated framework so owners do not inherit inconsistent safeguards from prior projects. This is particularly relevant during mergers, co-manufacturing deals, and brownfield expansions. The table explains why NFPA 660 is not only a code topic but also a management topic. It helps companies standardize expectations across multiple facilities and future projects. The area chart reflects a clear U.S. trend: companies are moving away from isolated equipment fixes and toward integrated sitewide combustible dust programs. This shift is likely to continue through 2026 as policy expectations and insurer attention increase. Many events begin not because a facility lacked a vent panel, but because an ignition source was allowed to exist in the first place. In food plants, common ignition concerns include static electricity, overheated bearings, mechanical friction, tramp metal, electrical faults, hot work, smoldering material, and poorly controlled maintenance activity. Static control is especially important in pneumatic conveying, bag filling, flexible hose transfers, dust collection, and ingredient handling systems that move dry, low-moisture powders. Plants processing sugar, flour, starch, cocoa, milk powder, coffee, dry flavors, and nutritional powders should review grounding and bonding of metal components, hose construction, filter media compatibility, and preventive maintenance around rotating equipment. Thermal monitoring, speed monitoring, spark detection, and metal separation may also be appropriate depending on the process. Housekeeping remains a cornerstone. Even where primary equipment is protected, secondary explosions become possible when overhead beams, cable trays, light fixtures, and hidden horizontal surfaces accumulate dust over time. This issue is common in older buildings and in fast-growing plants where process additions outpace infrastructure upgrades. From a buying standpoint, do not evaluate ignition-source control as “soft cost.” Grounding, monitoring, PM discipline, and operator training are often among the highest-return risk reduction measures available. They can also reduce nuisance shutdowns, product loss, and unplanned maintenance. Design-build integration is one of the most practical ways to improve explosion protection outcomes in the United States. Instead of splitting responsibility among separate process designers, equipment vendors, contractors, electricians, controls firms, and commissioning teams, an integrated model allows hazard requirements to shape the project early. This is especially useful in food expansions where utility upgrades, sanitation requirements, production uptime, and schedule pressure all interact. For example, relocating a dust collector outdoors may affect foundations, support steel, roof penetrations, process duct lengths, weather protection, freeze protection, electrical classification, and cleanability. Adding suppression and isolation affects controls architecture, panel design, alarm management, testing procedures, and operator training. A fragmented project team can miss these interfaces. Integrated execution is particularly valuable in active plants around major U.S. logistics centers such as Houston, Savannah, Kansas City, and Columbus where shutdown windows are short and material flow must resume quickly. Good planning reduces change orders, startup delays, and compliance ambiguity. Manufacturers looking for a project partner should ask for experience not only with explosion protection hardware but with process engineering, utility coordination, installation sequencing, and food-grade commissioning. A team that understands production reality can often find a safer and more profitable project path. Disruptive Process Solutions, or DPS, supports food and beverage manufacturers across the United States and Canada with a design-build-manage approach that aligns engineering, construction oversight, and execution. Rather than acting as a simple equipment reseller, the company works as a capital project and manufacturing partner focused on practical, profit-driven outcomes. On the technological side, DPS brings multi-discipline engineering capabilities that matter when explosion protection must fit inside a larger processing environment. That includes process, mechanical, structural, plumbing, electrical, and controls engineering as well as PLC programming, automation, and SCADA integration. In a combustible dust or flammable atmosphere project, these skills help connect hazard controls with real production needs such as conveying logic, interlocks, utility loads, alarm handling, and startup sequencing. Manufacturers can learn more about its broader project approach through the engineering and project services page. On the manufacturing side, DPS also designs and supplies selected process equipment, including tanks, custom CIP systems, marination tumblers, and cooking vessels. That capability matters because food plants often need explosion protection decisions to align with vessel geometry, sanitation design, product changeover requirements, and utility integration. A partner that understands fabrication and equipment interfaces can often reduce field conflicts during installation. Additional details are available on the process equipment section. On the service side, DPS supports capital planning, owner representation, process design, project management, general contracting functions where applicable, installation coordination, and system integration for manufacturers in all 50 states. The company is particularly well suited for clients who want honest technical guidance, strong execution, and a partner that can connect safety requirements with throughput, cost, and long-term operability. For background on the team and project philosophy, visit the company overview. Examples of execution can be seen in recent project case studies. For food plants evaluating explosion protection upgrades, this kind of integrated capability is useful because compliance decisions rarely stand alone. They affect line layout, utility systems, controls, scheduling, and future scale-up. The strongest outcomes usually come when safety, production, and capital efficiency are engineered together. The comparison chart illustrates what buyers often value most in a project partner: not only equipment knowledge, but coordination across engineering, controls, construction, and food manufacturing operations. 1. Which food products most often trigger combustible dust concerns?Flour, sugar, starch, cocoa, dry dairy powders, grain dust, seasonings, coffee, and many plant protein ingredients are common examples. Even edible materials can be highly combustible when dispersed as fine particles. 2. Does every dust collector in a U.S. food plant need NFPA 68 venting?Not automatically. The answer depends on the material, housing, location, and selected protection strategy. Some systems use venting, others may use suppression, flameless approaches, or alternative methods where justified. 3. What is the biggest mistake owners make?Waiting until after equipment is purchased to address explosion protection. By then, vent discharge, isolation, electrical changes, and controls integration may become expensive retrofit items. 4. Is a Dust Hazard Analysis just a one-time exercise?No. It should be reviewed and updated when processes, materials, equipment arrangements, or operating conditions change. Major expansions, new products, and line relocations often justify reassessment. 5. How does NFPA 69 differ from NFPA 68?NFPA 68 focuses on deflagration venting, while NFPA 69 addresses explosion prevention and protective methods such as isolation, suppression, and inerting. Many facilities need both concepts in different parts of the process. 6. Why is NFPA 660 important now?Because it brings combustible dust requirements into a more consolidated framework. That helps U.S. food companies standardize compliance language, project criteria, and audit programs across multiple sites. 7. What should buyers ask suppliers before ordering equipment?Ask for dust test assumptions, pressure ratings, venting basis, isolation requirements, maintenance needs, controls interfaces, startup testing requirements, and any site-specific limitations. Do not accept vague “code compliant” language without details. 8. What are the main 2026 trends for U.S. food plant explosion protection?Expect tighter integration of DHA findings into capex planning, wider adoption of digital monitoring for bearings and spark events, stronger insurer review of dust management programs, increased alignment with NFPA 660, and more emphasis on sustainable retrofits that improve both safety and energy efficiency. Plants will also continue to pair explosion protection work with broader modernization projects such as dust collection optimization, utility upgrades, and automation improvements. 9. Are local conditions important when designing protection systems?Yes. Coastal corrosion near ports such as Houston or Savannah, cold-weather design in Minneapolis or Buffalo, seismic considerations in California, and dense urban lot constraints in the Northeast can all affect vent discharge, equipment placement, and maintenance access. 10. When should a food plant bring in an integrated engineering partner?Ideally before procurement and layout freeze. Early involvement improves hazard assessment, budget accuracy, schedule planning, and coordination across process, utilities, structures, controls, and installation. In the United States, food facility explosion protection is no longer a niche topic reserved for a few high-risk sectors. It is a mainstream engineering, compliance, and capital planning issue that affects product quality, uptime, insurability, and employee safety. Companies that act early, perform strong DHA work, align with NFPA 68, NFPA 69, and NFPA 660, and integrate protection into project delivery are typically better positioned for safe growth through 2026 and beyond. -
Jacketed Kettle Manufacturer
For food and beverage manufacturers in the United States, a jacketed kettle is one of the most versatile pieces of thermal processing equipment available. It is used to heat, cook, hold, reduce, blend, and sometimes cool products such as sauces, soups, fillings, jams, dairy bases, brines, confections, and ready-to-eat meal components. The right kettle configuration depends on heating utility, batch size, product viscosity, cleanability, metallurgy, agitation, pressure code requirements, and how the kettle fits into the full production line. In U.S. plants from North Carolina to California, and from dairy hubs in Wisconsin to sauce processors near Chicago and New Jersey, the best jacketed kettle installations are not selected in isolation. They are engineered as part of a profitable process system. That system-level mindset is especially important when the kettle must connect with upstream ingredient handling and downstream fillers, heat exchangers, transfer pumps, CIP skids, retorts, or packaging lines. Companies looking beyond a single vessel often benefit from working with an experienced process partner. Disruptive Process Solutions supports food and beverage manufacturers across North America with engineering-led project execution, helping clients align equipment choices with throughput, sanitation, controls, utilities, and long-term return on capital. A jacketed kettle is a processing vessel with an outer shell, or jacket, that circulates steam, hot water, thermal oil, or another heating medium around the product zone. This indirect heating method delivers more even temperature distribution than direct flame or localized electric contact, which helps reduce scorching and improves batch consistency. In the U.S. market, steam jacketed kettles remain the most common for medium and large food plants, while electric and gas units are widely used in pilot rooms, commissaries, and facilities with limited boiler access. Thermal oil designs are selected when high temperatures, precise control, or special utility conditions make them more practical. Buyers should focus on eight core questions: What product are you cooking? How viscous is it? How large is the batch? Is the product acidic or salty? Do you need agitation? Does the kettle need to tilt? Is the jacket pressure-coded? And how will it integrate into the rest of the line? Those answers determine the ideal heating method, vessel alloy, agitator style, discharge design, and controls package. For most U.S. sauce, soup, and prepared foods applications, a common specification starts with a 304 or 316L stainless steel vessel, ASME-rated steam jacket, variable-speed agitation, sanitary outlet valve, temperature instrumentation, and either a fixed-mounted or tilting body depending on batch size and discharge method. Pilot kettles may start around 50 liters, while industrial production units can exceed 5,000 liters and tie into automated ingredient batching, recirculation, cooling, and packaging systems. In the United States, jacketed kettles are typically categorized by their heat source. Each option has advantages based on plant utilities, batch economics, and operating flexibility. Steam is preferred in many established food plants because boilers already support retorts, CIP, blanchers, and other process loads. Electric units are attractive for clean installation, accurate control, and smaller capacities. Gas-fired kettles are common where direct combustion offers utility savings or where a simple self-contained setup is desirable. Thermal oil systems serve niche but important applications that require elevated temperatures with stable indirect heat. The table above shows why there is no single “best” heating method. A co-packer in Texas with strong boiler capacity may favor steam. A high-value specialty producer in Oregon may choose electric for recipe precision. A processor near the Port of Newark handling acidic marinades may prioritize corrosion resistance and hygienic cleanability over utility simplicity. Regional energy costs, environmental goals, and expansion plans all affect the choice. U.S. market demand for jacketed kettles continues to rise as processors invest in labor efficiency, recipe control, and line automation. Jacketed heating works by transferring heat through the vessel wall rather than applying direct flame or localized heat directly to the product. The jacket surrounds the kettle bowl or sidewall, allowing heat to spread over a larger surface area. In a well-designed kettle, this reduces thermal hotspots and creates a more stable heating profile, especially when paired with gentle agitation. This indirect transfer matters because many food products are heat sensitive. Tomato sauces, cheese sauces, cream soups, starch-thickened fillings, barbecue sauces, fruit preps, and sweetened condensed products can scorch when exposed to uneven surface temperatures. Burn-on creates flavor defects, dark specks, lower yield, longer cleaning cycles, and potential food safety risk if carbonized residue remains in place. Steam is effective because condensation releases a large amount of latent heat quickly and evenly. Thermal oil is useful when higher setpoints are needed without the same pressure profile as steam. Electric jacket systems can be excellent for controlled ramping. Whatever the utility, the real performance depends on jacket geometry, wall thickness, insulation, agitation pattern, control loop tuning, and product rheology. For U.S. processors seeking repeatability across multiple shifts and plants, jacketed kettles should be treated as thermal systems, not just containers with heat. That means recipe parameters, utility conditions, and automation logic must all work together. This is one reason engineering support matters when scaling from bench-top formulation to commercial production. Stainless steel selection is not a cosmetic choice. It affects equipment life, product compatibility, cleanability, and total ownership cost. In most food and beverage applications, 304 stainless steel is widely used and performs well. However, 316L stainless steel offers improved resistance to chlorides, salts, and acidic conditions because of its molybdenum content and lower carbon profile. Processors making pickle brines, salsa, hot sauce, tomato products, vinegar-based dressings, citrus reductions, and certain protein marinades often evaluate 316L for product-contact areas. The same is true for facilities running aggressive sanitation chemistry or frequent CIP cycles. In coastal regions such as Southern California, the Gulf Coast, and ports near Savannah or Houston, environmental exposure may also influence external finish and material decisions, especially for equipment installed in humid utility spaces. In practice, many buyers use a mixed approach: 316L for product-contact zones and 304 for structural or non-contact components where appropriate. The decision should be based on recipe chemistry, temperature, exposure time, cleaning chemicals, and expected service life. A low-cost vessel built from the wrong alloy can become expensive very quickly through pitting, premature repairs, contamination risk, or downtime. Agitation is often the feature that separates a basic jacketed kettle from a high-performing process vessel. The right agitator improves heat transfer, suspends particulates, prevents settling, reduces wall fouling, and supports texture development. The wrong agitator can damage particulates, trap product, aerate excessively, or fail to move high-viscosity masses. Anchor agitators sweep close to the vessel wall and are common for viscous sauces and fillings. Paddle mixers work well for lower-viscosity products requiring broad circulation. Scraper agitators continuously clean the heated wall, making them valuable for delicate or sticky products. Planetary systems are chosen for very thick formulations where conventional rotational flow is not enough. Speed control, torque rating, seal type, and shaft support are all important, especially as batch size increases. Demand differs by industry segment. Sauces and prepared foods lead usage, but dairy, confectionery, and protein applications are also significant. When scaling up, agitator choice should be validated with the actual product, not just the stated viscosity on paper. Chunk size, sugar level, starch loading, protein content, fat phase behavior, and target final texture all matter. This is where pilot testing and process engineering support can prevent expensive rework later. Tilting and fixed kettles solve different operational problems. Tilting designs are popular in smaller capacities because they simplify discharge into bins, hoppers, depositors, or mobile transfer vessels. They are intuitive for operators and useful in culinary-style batch environments. Fixed kettles are more common in larger industrial capacities where product is discharged through a bottom outlet, often with pump assistance, load cells, automated valves, or downstream piping connections. Cleaning is another major consideration. A tilting kettle can be easier to visually inspect and manually clean in low-throughput settings. A fixed kettle is often better suited to repeatable CIP integration, sanitary hard piping, and automation. For U.S. processors facing labor shortages, food safety audits, and rising throughput targets, the best choice depends on whether the plant prioritizes manual flexibility or integrated batch transfer. In high-volume regions such as the Midwest prepared foods corridor, the Carolinas, and California’s contract manufacturing clusters, fixed CIP-capable systems are increasingly preferred because they support repeatability, labor reduction, and food safety documentation. Capacity should never be chosen only from target batch size. Headspace, foam behavior, agitation efficiency, ingredient addition sequence, heating time, and downstream takt time all influence the proper vessel volume. A 500-liter target batch may require a larger kettle if particulates, boil-up, or aggressive agitation demand extra working space. Conversely, oversizing a kettle can reduce thermal efficiency and batch control for smaller runs. Small pilot kettles in the 50- to 150-liter range are common for new product development, customer sampling, and scale-up work. Mid-range units from 300 to 1,000 liters are popular with regional processors and specialty food brands. Large production kettles from 1,500 to 5,000 liters often serve national brands, co-manufacturers, and integrated meal-component lines. For many U.S. manufacturers, capacity planning also ties to warehouse flow, utility loading, and future expansion. A plant in Atlanta shipping across the Southeast may design for one current shift plus a second-shift growth path. A West Coast processor near Los Angeles or Oakland may invest in fewer but larger vessels to offset labor and floor-space constraints. The right capacity is therefore both a process and business decision. As the chart suggests, the trend through 2026 favors larger, more automated kettle systems tied to integrated batching and cooling. However, pilot and flexible small-batch equipment remain important because U.S. brands continue to launch new flavors, seasonal SKUs, premium sauces, and functional formulations. For steam-heated kettles, code compliance is not optional. U.S. buyers should verify vessel and jacket pressure ratings, safety relief devices, nameplate data, and documentation. In most industrial food applications, ASME code compliance is expected for steam jackets, particularly when the equipment will be installed in facilities with formal boiler programs, insurance inspections, or state pressure vessel oversight. Pressure rating affects allowable steam conditions, heat-up performance, and operating margin. Safety relief protects the jacket from overpressure. Additional instrumentation may include pressure gauges, condensate traps, temperature transmitters, low-water protections for related utility systems, and interlocks that prevent unsafe heating conditions. Plants in states with strict inspection practices, and companies operating under large corporate engineering standards, typically require full documentation packages during procurement. That package may include ASME stamps where applicable, material certifications, weld procedures, test reports, and operation manuals. Buyers should also confirm whether local utility hookups, insulation, controls, and support frames are in scope. U.S. manufacturers increasingly evaluate kettle suppliers not just on vessel price, but on total project readiness: code compliance, installability, serviceability, controls compatibility, and long-term documentation discipline. The most valuable jacketed kettle is the one that fits the rest of the process. In modern food plants, kettles often connect to ingredient systems, tote dump stations, powder induction, liquid metering, vacuum transfer, inline shear mixing, plate or scraped-surface cooling, surge tanks, fillers, pouch systems, canning lines, or retort operations. That integration can transform the kettle from a standalone cooker into the thermal heart of a profitable line. For example, a cook-cool line may start with dry and liquid ingredient batching, move into a jacketed kettle with anchor-scraper agitation, then discharge through a lobe pump to a scraped surface heat exchanger before filling. A protein marinade line may use a 316L kettle for heated brine preparation before transfer to insulated hold tanks. A dairy dessert system may need precise temperature control, sanitary automation, and complete CIP verification across all connected assets. This is where process engineering capabilities become critical. DPS supports clients with process, mechanical, electrical, plumbing, structural, and controls expertise, allowing kettle systems to be integrated with utilities, PLC logic, SCADA visibility, and plant-wide execution plans. More information on these capabilities is available through the company’s engineering and project services. Their model is especially useful for clients who need more than equipment supply and want design, build, and management alignment across a larger capital project. On the manufacturing side, DPS also develops proprietary process equipment including tanks, CIP systems, marination tumblers, and cooking vessels, which helps streamline compatibility between the kettle and adjacent process assets. Buyers exploring broader system packages can review the company’s process equipment portfolio to understand how vessel design, utility planning, and integration can be coordinated. Service capability matters as much as engineering and fabrication. Installation sequencing, trade coordination, field quality control, commissioning, and start-up support often determine whether a kettle project meets schedule and budget. A kettle may be well-built but still fail commercially if condensate return is undersized, controls are not tuned, CIP coverage is incomplete, or discharge does not match filler demand. The comparison above reflects a common procurement reality in the U.S. market: suppliers that combine equipment knowledge with integration capability often create better outcomes than those selling only a standalone vessel. The U.S. market for jacketed kettle systems is broad and fragmented. Demand comes from sauce and condiment manufacturers, soup processors, dairy plants, meat and poultry value-add operations, confectionery producers, beverage ingredient blenders, pet food manufacturers, and co-packers. Geographic clusters matter. Chicago and the upper Midwest remain strong for prepared foods and sauces. California supports specialty foods, plant-based products, and beverage innovation. Texas and the Southeast continue to expand with greenfield and brownfield projects. Ports such as Los Angeles, Houston, Savannah, and Newark support imported ingredients and export-oriented production, influencing utility costs, floor planning, and equipment lead time strategy. When buying a jacketed kettle in the United States, start with process data, not brochure language. Define product family, batch size, solids content, target heat-up time, hold profile, cleanability, future SKUs, utility availability, and operator model. Then request a thermal and mechanical recommendation. Review metallurgy, agitator torque, outlet diameter, control philosophy, pressure code documentation, insulation, and support package. If the kettle will eventually feed a filler, retort, holding tank, or cooling system, specify those interfaces early. Otherwise, change orders arrive later. Different industries also prioritize different features. Dairy processors often emphasize hygienic finish and temperature precision. Protein operations care about brine compatibility, sanitation durability, and high-throughput batching. Confectionery processors may need scraper agitation and elevated temperature control. Plant-based food companies frequently require flexible formulations and allergen cleanout discipline. Applications include kettle cooking of soups, reductions, fruit preparations, syrups, fillings, meal sauces, cheese products, custards, marinades, glazes, and starch systems. In many plants, kettles are also used for preheating ingredients before homogenization, retort filling, or aseptic processing. The vessel may be the primary cooker or an upstream thermal preparation step. Case-based evaluation is useful. Processors often learn more from a completed integration than from a generic specification sheet. DPS has supported food and beverage clients with end-to-end execution ranging from capital planning and owner’s representation to full installation and system integration. Examples of project thinking and execution approach can be explored through selected client case studies and project examples. This is particularly relevant for buyers who want to understand how a kettle decision fits a larger operational and profitability plan. As for local suppliers, the U.S. market includes regional fabricators, national sanitary equipment builders, rep networks, and full-system integrators. Local sourcing can help with site visits, service response, and freight, but the best supplier is not always the closest supplier. Buyers should compare local and national options on engineering depth, sanitary fabrication quality, controls experience, code knowledge, lead time reliability, and field support. A regional fabricator may offer attractive pricing, while a national integration partner may reduce total project risk. Looking toward 2026, three trends stand out. First, controls sophistication will increase, with recipe management, data capture, and remote diagnostics becoming more common. Second, sustainability pressure will push greater interest in energy recovery, better insulation, condensate return optimization, lower-emission utilities, and water-efficient CIP. Third, policy and customer expectations around food safety, documentation, and traceability will keep favoring engineered systems over ad hoc batch setups. Kettles that can support automation, efficient thermal use, and validated sanitation will hold their value better in this environment. For companies seeking a partner rather than a simple vendor, DPS brings three practical strengths. In technology, the company supports process and controls integration across food and beverage systems, including utilities, automation, SCADA, and complete line architecture. In manufacturing, DPS offers proprietary process equipment such as storage and processing tanks, CIP systems, tumblers, and cooking vessels designed to fit broader plant needs. In service, the company provides planning, design, installation, project management, and on-site execution support across the United States and Canada. That combination is helpful for processors who want smart capital deployment and equipment that works in the real production environment, not just on paper. What is the most common jacketed kettle type in U.S. food plants?Steam jacketed kettles are the most common in medium and large facilities because they provide fast, even heating and often fit existing boiler infrastructure. When should I choose 316L instead of 304?Choose 316L when processing acidic, salty, or chloride-rich products such as brines, marinades, tomato sauces, hot sauces, or vinegar-based formulations, or when aggressive CIP chemicals are used regularly. Is a tilting kettle better than a fixed kettle?Not always. Tilting kettles are excellent for smaller, operator-driven batches. Fixed kettles are usually better for larger, automated, CIP-integrated systems with hard-piped discharge. Do I need an agitator?If your product is viscous, heat sensitive, particulate-containing, or prone to settling or scorching, yes. Agitation usually improves thermal consistency and product quality. Are steam jackets required to be ASME compliant?In many U.S. industrial applications, ASME compliance is strongly expected or required. Always confirm local code expectations, insurer requirements, and plant engineering standards. What capacity should I buy?Base capacity on actual working volume, headspace needs, heat-up time, future growth, and downstream line speed. Do not size only by nominal batch target. Can a jacketed kettle cool product too?Some systems can be configured for cook-cool duty or integrated with downstream cooling equipment such as scraped-surface or plate heat exchangers. Cooling strategy should be designed early. How long should a kettle last?A well-built stainless kettle with correct metallurgy, proper maintenance, and suitable process conditions can provide many years of service. Life span depends heavily on product chemistry, cleaning practice, and mechanical load. What should I ask suppliers before ordering?Ask about metallurgy, pressure rating, code documentation, agitator torque, discharge design, controls, cleaning method, lead time, installation scope, and support after start-up. Who should help if I need a full process line, not just a vessel?An engineering-led integrator is usually the better fit when the kettle must connect with utilities, automation, CIP, cooling, filling, or broader plant expansion plans.


