-
Food Plant Cold Storage Design: 7 Steps to Refrigerated Warehouse Planning
Cold storage design in the United States is no longer just about holding product below a target temperature. For food manufacturers, processors, and co-packers, a refrigerated warehouse must protect food safety, preserve shelf life, support throughput, reduce utility costs, and align with FDA, USDA, SQF, and BRC expectations. In practical terms, the best food plant cold storage design starts with product and process requirements, then moves through envelope design, refrigeration sizing, airflow, dock control, floor protection, and commissioning. Whether a project is supporting poultry in Arkansas, dairy in Wisconsin, frozen prepared foods in Illinois, seafood moving through Seattle and Los Angeles, or beverage ingredients staged near Savannah and Houston, the design approach has to match the local climate, utility profile, labor conditions, and distribution pattern. A cold room serving a Midwest meat processor will be engineered differently from a blast-ready freezer expansion in Southern California or a mixed-temperature e-commerce fulfillment space near New Jersey ports. This guide explains seven practical steps for refrigerated warehouse planning in the U.S. market and highlights common buying mistakes, product categories, applications, and future trends shaping 2026 decisions. The fastest way to plan a successful food plant cold storage facility is to define product temperatures first, separate incompatible zones second, and then size the envelope, refrigeration, airflow, dock interface, and floor system around actual operating loads instead of generic square-foot rules. That means understanding what enters the room, how warm it arrives, how fast it must be pulled down, how often doors open, how forklifts move, and how inventory turns. In the United States, most food plant cold storage projects fall into six operating bands: ambient support spaces, cool processing support rooms, refrigerated storage, deep-chill staging, frozen storage, and blast or pull-down applications. Each one carries different insulation thicknesses, defrost strategies, humidity needs, door packages, and evaporator air throw requirements. A room at 35°F for fresh sauces or dairy ingredients is not designed the same way as a -10°F freezer for boxed proteins. Buying advice is simple: do not buy refrigeration tonnage before confirming product load, infiltration load, and future throughput. Many facilities overbuild compressors and underbuild doors, docks, and controls. That creates high capital cost with poor real-world performance. In many cases, the most profitable design decision is better zoning and tighter envelope control, not more horsepower. The U.S. market continues to grow as processors add regional distribution nodes near Atlanta, Dallas, Chicago, Phoenix, and the Inland Empire. Demand is especially strong in protein, prepared meals, dairy, frozen bakery, beverage ingredients, and contract manufacturing. Food producers want faster installation, lower energy intensity, and designs that can scale with automation and changing SKUs. The table below shows how typical food categories map to storage requirements and design priorities. For U.S. operators, the strongest business case usually comes from matching the room to the product, not forcing every SKU into one oversized cold box. Multi-zone layouts improve shelf life, labor flow, and utility performance while giving plants more flexibility for growth. The growth trend above reflects continued investment in food-grade cold capacity, especially in regions with strong interstate freight access and large consumer bases. Temperature zoning is the foundation of refrigerated warehouse planning. Before wall panels, evaporators, or compressors are selected, the design team should map every product stream by entry temperature, target storage temperature, residence time, packaging type, pallet density, and sanitation risk. A single mixed room is often the most expensive long-term solution because it forces one condition onto many incompatible products. For example, ready-to-eat deli proteins may need stricter environmental stability than raw ingredient pallets. Frozen bakery may tolerate different airflow velocities than boxed seafood. Beverage ingredients used in short-interval batching can often operate in a cooler support room instead of a full frozen environment. Zoning also affects traffic. A room with constant forklift activity has a very different infiltration profile from a reserve freezer with limited access. In U.S. food plants, common zones include receiving buffer coolers, quarantine rooms, raw and finished goods coolers, frozen storage, ingredient tempering areas, and dispatch staging areas. In higher-complexity sites, there may also be separate allergen, export hold, rework, or high-value product zones. Plants serving major retail or club channels often add more SKU-specific flexibility because promotions and seasonality create uneven volume patterns. The next table can be used during early programming meetings to define zoning by product behavior. As a buying recommendation, processors should ask equipment vendors and design partners to provide a load matrix showing product load by zone, not just a combined refrigeration total. This prevents underestimating the impact of production timing, truck arrivals, and peak receiving windows. It also helps finance teams compare modular expansion options. Industries benefiting most from disciplined zoning include protein processing, frozen meals, dairy, specialty sauces, brewery ingredients, and contract packaging operations. Applications range from on-site finished goods storage to cross-dock support, export staging, and integrated cold process rooms adjacent to packaging lines. This demand profile shows why temperature zoning matters so much in the United States: industries with the highest volume often have the greatest product diversity and the highest cost of mistakes. The building envelope determines whether the refrigeration system works efficiently or fights a losing battle every hour of the year. For U.S. food plants, envelope design should address climate zone, indoor setpoint, vapor migration, washdown exposure, panel joints, roof transitions, penetrations, and long-term maintainability. A great compressor package cannot overcome a weak panel seam or poorly detailed threshold. Processors in humid regions such as Florida, Louisiana, and coastal Texas face aggressive vapor drive. Facilities in Minneapolis, Denver, or upstate New York may experience freeze-thaw conditions that challenge joints and slab edges differently. A building near the Port of Savannah may need stronger corrosion planning than an inland distribution support cooler in Kansas City. Most food-grade cold storage rooms rely on insulated metal panels, but selecting thickness is only one piece of the design. Joint sealing, vapor barrier continuity, thermal break detailing, suspended ceiling interfaces, and door frame installation matter just as much. Roof and wall intersections should be designed to minimize thermal bridging and prevent hidden condensation. Penetrations for pipe racks, sprinkler lines, supports, and electrical conduit must be sealed and documented during construction, not patched later. The table below summarizes common envelope choices and when they are appropriate. Buying advice here is to request lifecycle analysis, not just panel pricing. A lower first-cost package can become expensive if it raises compressor runtime, creates condensation remediation work, or shortens the service life of doors and hardware. Ask for details on sealants, vapor barrier continuity, and thermal bridge treatment, especially where cold rooms meet processing spaces. Processors evaluating expansions should also consider future openings. It is easier and cheaper to pre-plan knockout panel locations, utility corridors, and support steel for later phases than to rebuild a functioning freezer envelope two years after startup. Refrigeration selection should follow loads, operating mode, and business priorities. The correct solution for a central frozen warehouse in Indiana may be very different from a packaged glycol-supported cooler in North Carolina or a distributed low-charge system in California where environmental and utility considerations influence decisions. System choice is not only about tonnage; it is about resilience, maintainability, refrigerant strategy, controls, and total cost of ownership. The major load components include product pull-down, transmission through walls and roof, infiltration at doors and docks, people, lights, motors, fans, forklifts, defrost, and process-related heat gain. Designers should model peak summer conditions and realistic traffic loads. In many food facilities, infiltration and operational activity are underestimated, while actual product load varies sharply by shift and season. Common U.S. system choices include ammonia for large industrial loads, low-charge ammonia packages, CO2-based systems for selected applications, and halocarbon or HFO-based systems for smaller or compartmentalized spaces. The right answer depends on room size, staffing, operator familiarity, safety strategy, local regulations, and utility costs. The area chart below illustrates how U.S. project preferences are shifting. That shift reflects demand for easier phasing, improved safety narratives, and stronger sustainability positioning. It also aligns with facilities that need quicker startup and more localized service coverage. When comparing suppliers, ask for part-load performance, control logic, defrost energy impact, spare parts strategy, and service response expectations. A system that looks efficient at nameplate conditions may underperform in a real plant with variable shift schedules and frequent door events. Cold room performance depends on what happens around the product, not just what happens at the compressor rack. Poor airflow creates dead zones, stratification, slow recovery after door openings, localized freezing, and inconsistent product temperature. In food plants, this can translate directly into shelf-life loss, QA holds, and customer complaints. Airflow design starts with pallet dimensions, rack layout, ceiling height, evaporator placement, aisle width, product packaging permeability, and stacking pattern. A room with high-density double-deep racks needs a different air strategy from a low-bay cooler supporting frequent hand picks. Evaporator throw must be selected carefully to avoid short-circuiting air across open areas while starving corners or lower pallet lanes. Product should never be stored tight against evaporators, walls, or ceilings unless the design specifically accounts for it. Forklift drivers often become the hidden variable in airflow performance because emergency overflow locations gradually turn intended air paths into blocked corridors. Good design therefore combines engineering, line marking, signage, and operational rules. The following table summarizes common airflow issues and remedies. Comparison among common room concepts can also be visualized by supplier or layout package. The chart below compares relative performance factors often used in procurement scoring. For facilities investing in ASRS, shuttle systems, or semi-automated pallet handling, airflow coordination becomes even more important because tighter clearances can change return-air behavior. Early CFD-style review or detailed airflow planning often pays back quickly in reduced troubleshooting after startup. Many cold storage projects fail at the dock before they fail in the machine room. Docks are where outside air, truck cycles, labor pressure, and real production variability collide. Every unnecessary second of open-door time increases infiltration, frosting risk, compressor load, and unstable room conditions. In busy food plants, docks should be treated as thermal control assets, not just shipping openings. U.S. plants near high-volume corridors such as I-35, I-80, I-95, or major logistics hubs around Memphis, Chicago, and Dallas often face intense truck scheduling pressure. Facilities serving port traffic from Long Beach, Newark, Savannah, or Houston also see irregular arrival patterns that can create simultaneous opening events. This makes dock zoning and sequencing critical. Design options include enclosed refrigerated docks, vestibules, rapid-roll doors, dock seals, dock shelters, interlocked controls, trailer restraints, strip curtains in selected cases, and traffic-light systems that coordinate opening and closing. For frozen rooms, vestibules and door heating packages may be essential. In some applications, a short transition chamber can dramatically reduce frost and moisture migration. Buying advice: if a vendor is presenting refrigeration capacity without a detailed door-and-dock strategy, the proposal is incomplete. In many retrofits, infiltration reduction is the cheapest available tonnage. Better dock discipline may delay or eliminate the need for a compressor upgrade. For case studies and practical examples of integrated project execution, manufacturers can review food and beverage project examples that show how process flow, utilities, and building systems must work together rather than as isolated packages. Freezer floor design is often underestimated until a slab starts moving. Frost heave happens when subgrade moisture freezes and expands under low-temperature spaces, lifting and damaging the floor. Once it appears, repair costs are disruptive and expensive. Prevention must be built into the original design through insulation, heating strategy, drainage, vapor control, and edge detailing. Not every refrigerated room needs the same floor approach. A 38°F cooler may have very different subfloor needs than a -10°F freezer. Soil conditions, water table, climate, loading pattern, and slab thickness all matter. High-rack forklift traffic, washdown areas, and heavy pallet concentration increase structural demands and can influence insulation protection details. Common U.S. solutions include sub-slab insulation, underfloor heating pipes or electric systems for freezers, perimeter insulation at slab edges, vapor barriers, and carefully managed drainage. The design must also coordinate with door thresholds, rack anchoring, and nearby ambient slabs to avoid thermal weak points. The table below highlights key floor planning considerations. For expansion projects, always assess whether the existing slab can support the intended freezer conversion. Many processors try to convert ambient or cool space into frozen storage without addressing subfloor risk. That can create a serious long-term liability even if the conversion looks economical at first. Cold storage design is not complete at startup. Commissioning and validation prove whether the room actually performs under real operating conditions. This includes mechanical startup, controls verification, alarm testing, airflow balancing, door sequencing checks, defrost confirmation, floor heat checks, and temperature mapping under both idle and loaded conditions. In food plants, validation should reflect production reality. A room that holds setpoint overnight while empty may fail during morning receiving surges or after multiple outbound truck cycles. Sensors should be placed at representative heights and room locations, including corners, door-adjacent areas, rack interiors where feasible, and return-air paths. Product simulators or packaged thermal masses can improve data quality. Documentation matters because quality teams, auditors, and corporate engineering groups increasingly expect evidence that the room meets design intent. In regulated or certification-driven environments, commissioning records support risk management and CAPA response. Looking toward 2026, U.S. facilities are increasing use of wireless sensors, cloud dashboards, automated alarm analytics, and energy monitoring tied to SCADA or plant historian systems. Temperature validation is becoming more predictive, not just reactive. Facilities also face stronger sustainability expectations, making commissioning a chance to establish energy baselines and identify optimization opportunities. Manufacturers that want broader capital planning support often benefit from reviewing integrated engineering and project delivery services before committing to standalone equipment purchases, because commissioning success is usually determined upstream during design coordination. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a practical, profit-focused approach to capital projects. Rather than treating a cold storage project as a standalone box with refrigeration attached, the team aligns building systems, process flow, utilities, controls, and long-term operating economics. From a technological capability standpoint, DPS brings multi-discipline engineering across structural, mechanical, plumbing, electrical, process, and controls. That matters in refrigerated warehouse planning because cold storage rarely stands alone. It connects to production scheduling, utility loads, PLC logic, SCADA visibility, washdown requirements, ingredient handling, and sanitation compliance. Facilities adding a cold room to a protein line, dairy process area, beverage syrup room, or aseptic support space need those disciplines integrated from the beginning. From a manufacturing capability standpoint, DPS also supports projects through proprietary equipment offerings and process-system integration experience. That includes tanks, CIP systems, and other production assets that often sit upstream or downstream of cold storage. For manufacturers trying to balance storage, batching, process uptime, and sanitation, that wider perspective helps avoid the classic problem of building refrigerated space that does not match the actual manufacturing rhythm. More information about available process equipment solutions can help processors understand how storage and production infrastructure should work together. From a service capability standpoint, DPS operates through a design-build-manage model that covers planning, feasibility, owner’s representation, project management, general contracting where licensed, installation, integration, and commissioning. That end-to-end structure is especially useful for cold storage expansions where multiple local trades, refrigeration vendors, utilities, and food safety stakeholders must stay aligned. Companies considering a strategic partner can learn more about the DPS team and approach. For food and beverage manufacturers in markets such as North Carolina, Texas, California, Illinois, Georgia, and beyond, the value of this approach is speed with discipline: fast decisions, practical engineering, transparent guidance, and a constant focus on profitable project outcomes rather than oversized scope. What temperature should a food plant cold storage room be designed for?It depends on the product, packaging, dwell time, and regulatory requirements. Fresh proteins, dairy, frozen foods, beverage ingredients, and prepared meals all have different needs. Start with product specifications, then build the room around them. How large should a refrigerated warehouse be?Size should be based on pallet count, SKU growth, aisle strategy, inbound and outbound peaks, and future expansion plans. Avoid sizing by square footage alone. Throughput matters as much as storage volume. What is the most common design mistake?A common mistake is focusing on refrigeration tonnage while ignoring door traffic, zoning, and infiltration. Many underperforming rooms have enough cooling on paper but poor real-world control at docks and openings. Is one large room better than several smaller temperature zones?Usually not. Multiple zones often improve energy use, food safety, and flexibility. They also allow different products to be held under more suitable conditions and simplify future expansion. How do U.S. climate conditions affect design?Hot and humid regions increase vapor drive and infiltration risk, while colder northern climates create different freeze-related envelope and slab concerns. Local weather should always influence insulation, vapor barrier, dock, and floor decisions. What should be included in commissioning?Startup checks, controls verification, alarm tests, airflow review, door cycle performance, defrost testing, underfloor heat confirmation where applicable, and temperature mapping under realistic operating conditions. Are sustainability and policy changes affecting 2026 projects?Yes. Owners are increasingly evaluating refrigerant strategy, energy intensity, automation readiness, and utility monitoring. State-level environmental policy and corporate ESG goals are pushing more efficient and lower-impact designs. When should a manufacturer bring in an engineering partner?As early as possible. Early involvement improves product zoning, capital budgeting, utility planning, constructability, and expansion logic, which usually produces a better return than waiting until equipment has already been selected. In short, strong refrigerated warehouse planning for U.S. food plants combines technical rigor with operational realism. If the room is designed around product behavior, traffic, local climate, utility cost, and future growth, it will protect quality and support profitability for years. -
Aseptic Beverage Processing Systems
Aseptic beverage processing is a manufacturing method that sterilizes the product and the package separately, then combines them inside a sterile environment to produce shelf-stable drinks without refrigeration. In the United States, this method is widely used for dairy beverages, protein drinks, plant-based beverages, functional drinks, juices, coffee, teas, and sensitive low-acid formulations that demand long shelf life, flavor protection, and national distribution efficiency. For processors evaluating capital investment, the right aseptic system is not just a filler. It is a tightly integrated production platform that includes UHT treatment, sterile surge handling, packaging sterilization, aseptic filling, clean utilities, automation, and validated microbiological controls. For manufacturers in major production corridors such as Chicago, Dallas, Los Angeles, Atlanta, Charlotte, and the New Jersey distribution belt, aseptic processing often becomes a strategic tool for freight flexibility, SKU expansion, and warehousing efficiency. It also matters in port-connected supply chains through Long Beach, Savannah, Houston, and New York/New Jersey, where long dwell times and wide geographic distribution make ambient stability especially valuable. Aseptic beverage processing works by rapidly sterilizing liquid product, usually with UHT heat treatment, cooling it under sterile conditions, sterilizing the packaging material, and filling the beverage in a closed aseptic chamber. Compared with hot fill and retort, aseptic systems typically provide better sensory retention, support more package formats, reduce thermal load on the beverage, and enable high-speed output from about 12,000 to 72,000 bottles per hour depending on format, viscosity, and automation level. In practical U.S. terms, aseptic is usually the right choice when a brand needs one or more of the following: nationwide ambient distribution, low-acid beverage safety, dairy or plant-based protein stability, premium flavor retention, lightweight package formats, or high-volume production economics. Hot fill remains effective for many high-acid beverages. Retort is still essential for certain shelf-stable foods and highly robust packaged products. The best choice depends on product pH, particulate content, shelf-life target, package type, throughput goals, utility availability, and regulatory expectations. For companies that need engineering guidance from concept to commissioning, Disruptive Process Solutions supports U.S. manufacturers as a food and beverage engineering partner focused on profitable project execution rather than one-dimensional equipment sales. The aseptic journey begins with product formulation and microbiological risk classification. The product is blended, standardized, and often deaerated before entering thermal treatment. In most beverage applications, UHT sterilization heats the liquid to approximately 135 to 150 degrees Celsius for a very short holding time, often only a few seconds. That thermal exposure is enough to destroy vegetative cells and spores when paired with validated residence time, flow control, and temperature monitoring. After heating, the beverage is flash cooled or indirectly cooled in sterile heat exchange sections. It then moves into a sterile surge tank or balance vessel that maintains overpressure with sterile air or nitrogen. From there, the liquid is transferred through sterile piping to the filler. The packaging, whether PET bottle, HDPE bottle, carton, cup, or flexible structure, is sterilized separately using hydrogen peroxide, steam, UV, or a hybrid method. Finally, the product is filled and sealed inside an aseptic chamber maintained with filtered air, controlled pressure differentials, and validated environmental conditions. Three engineering issues determine whether a system performs in the field: thermal design, hygienic design, and automation logic. A poorly designed heat profile may overcook proteins or destabilize emulsions. A poorly designed hygienic circuit may create dead legs, gasket risks, or difficult-to-clean valves. Weak automation may undermine sterility through unverified setpoint drift, improper SIP sequencing, or incomplete changeover interlocks. That is why many U.S. processors prefer an integrated project model that combines process engineering, utilities, controls, and installation. DPS applies a design-build-manage approach that helps clients align UHT, blending, utilities, CIP, controls, and filling into one capital plan rather than fragmented vendor packages. The table above shows why aseptic success depends on the entire chain, not only the sterilizer. A weak receiving program or poorly validated filler can undermine even an excellent UHT process. Choosing the right processing method starts with product chemistry and commercial objectives. A high-acid juice for regional retail may fit hot fill perfectly. A low-acid protein shake with national e-commerce distribution will generally need aseptic processing. A shelf-stable product with particulates or a package intended to withstand post-fill sterilization may call for retort. Hot fill typically heats product and fills it while hot enough to sanitize the container interior. It is common for juices, teas, and acidified beverages. It is proven and often less capital intensive than aseptic. However, it places more heat stress on flavor, color, and nutrients, and it may limit package selection. Retort processes the sealed package after filling, usually inside a pressure vessel. It is robust and suitable for many shelf-stable foods and some specialty beverages, but thermal load is even higher and throughput is often slower, depending on package size and cycle time. Aseptic processing separates product sterilization from packaging sterilization. This preserves sensory quality better and supports very high line rates once the system is tuned. It also demands higher engineering rigor, sterility validation, and disciplined operating procedures. The table shows that no single technology is universally better. The right answer depends on your product family, growth plan, labor model, and distribution radius. A co-packer serving both East Coast and West Coast retailers may value aseptic shelf stability more than a local juice brand distributing only in the Southeast. An aseptic beverage line is a system of interdependent hygienic assets. The core typically includes raw ingredient handling, batching, high-shear mixing where needed, deaeration, homogenization, UHT treatment, aseptic holding, sterile transfer, package sterilization, aseptic filling, secondary packaging, and comprehensive CIP/SIP support. Utilities matter just as much as the main process path: clean steam, culinary water, compressed air, chilled water, glycol, boiler capacity, condensate management, and HVAC all influence sterility and uptime. From a technological capability standpoint, DPS supports complete process, mechanical, electrical, structural, plumbing, and controls engineering for aseptic facilities. That matters because filler performance alone does not solve plant bottlenecks. The surrounding infrastructure must be sized correctly for thermal load, utility redundancy, recipe complexity, and future line expansion. Manufacturing capability also matters. DPS designs and supplies selected process equipment such as tanks and custom CIP systems, which helps align fabrication details with the broader project intent. Service capability is equally critical: capital planning, feasibility analysis, owner’s representation, general contracting, installation management, and startup coordination all affect how quickly an aseptic line reaches commercial production. Many beverage investors underestimate the utility envelope around these components. For example, a line may be mechanically rated for 48,000 bottles per hour but effectively capped by steam generation, sterile air preparation, or CIP turnaround. That is why comprehensive process engineering and project services are often more valuable than buying hardware without full integration planning. Sterility Assurance Level, or SAL, is a way of expressing the probability that a viable microorganism survives the sterilization process. In beverage manufacturing, the exact interpretation depends on product type, packaging, process authority expectations, and applicable regulations, but the core concept is constant: sterility claims must be supported by validated science, not assumptions. Validation typically includes thermal mapping, residence time studies, challenge testing, packaging sterilization verification, aseptic boundary integrity checks, filter integrity testing, environmental monitoring, media runs where appropriate, and documented operating limits. Processors also need a robust hazard analysis that identifies biological risks across formulation, transfer, filling, storage, and maintenance activities. In the United States, manufacturers dealing with low-acid aseptic products must align with FDA expectations for commercial sterility, scheduled process establishment, and detailed process records. Validation must be specific enough to cover worst-case formulations, maximum viscosity, minimum flow conditions, startup transitions, and abnormal events such as power interruptions or pressure loss. The explanation above highlights a common U.S. mistake: companies validate the sterilizer but not the whole aseptic ecosystem. True validation extends from raw material assumptions through final package seal integrity. Packaging sterilization is one of the most important decisions in any aseptic project because it shapes package compatibility, operating costs, environmental controls, and validation complexity. The most common methods are hydrogen peroxide, steam, UV, or combinations of these technologies. Hydrogen peroxide, often written as H2O2, is widely used because it is effective and compatible with many high-speed systems. It may be applied as vapor, mist, or liquid depending on package format and line design. The process requires tightly controlled concentration, temperature, exposure time, and residual management. Steam sterilization provides strong microbial reduction and may suit some packaging components or closures, especially in lines already supported by clean steam infrastructure. However, moisture and heat effects must be managed carefully to avoid package deformation or condensation-related issues. UV methods can be useful in certain package and cap applications, particularly where dry processing advantages are attractive. Yet UV is line-of-sight dependent and often works best as part of a broader decontamination strategy rather than as a universal standalone answer. For U.S. processors facing sustainability targets in 2026 and beyond, dry or lower-water sterilization approaches are getting more attention, especially in regions where wastewater, heat recovery, and energy intensity affect total operating cost. Plants in California, Arizona, and Texas are especially sensitive to utility efficiency planning. U.S. aseptic beverage operations must be designed around compliance from day one, not retrofitted after installation. FDA requirements can apply to low-acid foods, acidified products, preventive controls, cGMPs, process records, and scheduled processes depending on the product category. Hygienic design standards from organizations such as EHEDG and 3-A concepts are also useful in minimizing cleanability risk and strengthening validation readiness. For processors supplying major retailers or co-manufacturing national brands, practical compliance goes beyond passing inspection. It means documented hygienic zoning, sanitary weld quality, drainability, accessible valve clusters, segregated utilities, CIP proof, alarm management, controlled interventions, and accurate lot traceability. DPS frequently supports clients that need not only design expertise but also regulatory fluency across FDA, USDA, SQF, and BRC-aligned projects. That service capability is important for mixed portfolios where a manufacturer may run beverages, dairy, prepared foods, or retort products at the same campus. In cities with aggressive expansion of co-packing infrastructure such as Dallas-Fort Worth, Nashville, Phoenix, and the Carolinas manufacturing corridor, compliance-centered engineering has become a competitive differentiator. Investors want systems that can scale without triggering redesign because a filler was installed before the sanitary utility map was fully planned. Cleaning-in-place and sterilization-in-place are the heartbeat of aseptic reliability. CIP removes product residues, films, proteins, sugars, and minerals. SIP then sterilizes the clean equipment path using steam or equivalent validated methods. If either protocol is weak, sterility assurance collapses. Effective CIP programs define chemical concentration, flow velocity, temperature, time, circuit segmentation, return conductivity targets, and final rinse acceptance. Effective SIP programs define steam quality, temperature hold, cold spot verification, condensate control, and sterile boundary confirmation. From a maintenance perspective, the best plants do not treat CIP/SIP as a sanitation checkbox. They use trend data to identify fouling rates, valve wear, gasket fatigue, heat exchanger performance decline, and campaign length optimization. This reduces both microbiological risk and unnecessary downtime. The table shows why CIP/SIP should be engineered with the same seriousness as production. Many underperforming lines in the United States are not limited by filler speed but by cleaning turnaround and unstable campaign scheduling. Capacity planning for aseptic beverage lines should begin with market strategy rather than nameplate speed. A startup protein beverage brand shipping through Atlanta and Chicago may only need 12,000 to 18,000 bottles per hour. A national co-packer serving club stores from Southern California, Texas, and Pennsylvania may require 48,000 to 72,000 bottles per hour or more. The correct line size depends on SKU count, changeover frequency, OEE target, warehousing logic, labor model, and utility redundancy. One of the biggest planning errors is selecting speed before understanding annualized demand and true run time. A line designed for 72,000 bottles per hour may still miss budget if there are too many short runs, excessive cap changes, unstable sterilization cycles, or insufficient downstream packaging capacity. Another key factor is footprint. Existing plants in urban industrial zones such as New Jersey, Los Angeles County, or inner-ring Chicago suburbs often have layout constraints that change filler choice, sterile tank sizing, mezzanine strategy, and CIP routing. Greenfield sites in North Carolina, Texas, or Tennessee may offer more flexibility and stronger long-term utility planning. When buyers compare suppliers, they should look beyond machine speed. Evaluate integration experience, controls architecture, hygienic design philosophy, utility consumption, FAT/SAT methodology, local service access, spare parts strategy, and startup support. A faster filler with weak commissioning support can cost more than a slower but stable line. For companies planning a new line or expansion, it is often wise to benchmark available process equipment options against projected SKU mix, required sterility validation effort, and downstream packaging demand before finalizing procurement. Looking toward 2026, four trends are shaping the U.S. market. First, more beverage brands are moving into functional, protein, and hybrid dairy-plant products that favor aseptic processing. Second, automation and SCADA-driven batch traceability are becoming standard rather than premium features. Third, water and energy efficiency are gaining board-level attention, encouraging heat recovery, smarter CIP reuse, and lower-chemical decontamination strategies. Fourth, policy and retailer pressure are increasing around documentation, food safety culture, and sustainability metrics. DPS is especially well positioned for these trends because its work spans process engineering, utilities, automation, installation, and project management. The company has supported beverage and food clients across North America, from breweries and distilleries to dairy, prepared foods, aseptic, and retort operations. In practical terms, that means a client can engage one team to evaluate feasibility, engineer the process, coordinate trades, manage execution, and support startup instead of trying to align disconnected vendors. For readers who want examples of project execution style and industry fit, the firm’s project case studies offer a useful view into how integrated capital work is planned and delivered. What beverages are best suited for aseptic processing?Low-acid dairy drinks, protein shakes, plant-based milks, coffee beverages, nutritional beverages, creamers, some juices, and many functional products are strong candidates. Products with national ambient distribution needs benefit the most. Is aseptic processing always better than hot fill?No. Hot fill can be the better business decision for high-acid products, lower capital budgets, and simpler packaging needs. Aseptic is usually stronger for sensitive low-acid beverages and broader shelf-stable distribution. How long can aseptically processed beverages last?Shelf life varies by product, package, oxygen control, and storage conditions. Many products target six to twelve months, while some achieve longer validated shelf life with proper formulation and packaging. What is the biggest hidden cost in an aseptic project?Utility and integration gaps. Steam, sterile air, CIP, controls, building modifications, HVAC, and validation often create more cost exposure than the main filler if not planned early. Can an existing hot-fill plant be converted to aseptic?Sometimes, but not always efficiently. Conversions require careful review of utilities, hygienic zoning, package strategy, floor layout, sterile boundary design, and compliance obligations. What line speed should a new U.S. co-packer target?It depends on annual volume, SKU count, and customer mix. Many new entrants begin around 12,000 to 24,000 bottles per hour, while larger co-packing hubs may plan 36,000 to 72,000 bottles per hour. How important is local support in the United States?Very important. Downtime costs can be severe, especially in high-volume ambient beverage plants. Buyers should assess spare parts availability, remote support capability, and technician coverage across regions such as the Midwest, Southeast, Texas, and the West Coast. What should buyers ask an engineering partner before investing?Ask about process authority coordination, validation scope, utility load assumptions, hygienic design standards, CIP/SIP philosophy, startup staffing, changeover modeling, and future expansion planning. The right partner should challenge assumptions, not simply confirm them. Aseptic beverage processing in the United States is ultimately a business system as much as a sterilization system. When properly designed, it gives brands longer reach, stronger quality retention, and a path to profitable scale. When poorly scoped, it becomes an expensive bottleneck. The best outcomes come from aligning product risk, package strategy, utilities, validation, and commercial growth into one engineering roadmap. -
2026 Food Facility Floor Coating Selection: 3 Epoxy vs Urethane Cement Systems
Choosing the right floor system in a food plant is not a cosmetic decision. It affects sanitation, worker safety, regulatory readiness, maintenance cost, uptime, and the usable life of the slab beneath the finish. In the United States, the most common comparison is between epoxy floor coating systems and urethane cement flooring systems. In practical terms, epoxy is often the better fit for dry processing, packaging, and warehouse zones, while urethane cement is usually the stronger choice for wet production, hot washdown, and thermal shock exposure. The best answer, however, depends on traffic, cleaning chemicals, floor slope, substrate moisture, temperature swings, and the production profile of the facility. Food manufacturers from California’s Central Valley to meat and poultry operations in Arkansas, dairy plants in Wisconsin, beverage lines near Chicago, and export-driven facilities serving the ports of Savannah, Houston, and Long Beach all face the same core question: which floor system will protect operations without becoming a recurring failure point? This guide explains the selection process with direct buying advice, performance comparisons, installation timelines, maintenance protocols, and 2026 market trends for U.S. food and beverage plants. If you need a quick answer, start here: For most U.S. processors, the real mistake is not picking epoxy or urethane cement. The mistake is applying the same system everywhere. Facilities often need a zoned floor strategy, with different materials in raw receiving, wet production, packaging, cooler thresholds, maintenance shops, and warehouse aisles. The table above is useful because it turns the selection question into an operational question. Instead of asking which coating is “best,” ask what the floor must survive every day. Epoxy remains a strong option in U.S. food facilities when the area is primarily dry, temperature stable, and not exposed to repeated hot washdowns. It is widely used in secondary packaging, dry blending support spaces, palletizing zones, hallways, maintenance corridors, and warehousing. For plants in Phoenix, Dallas, Charlotte, Indianapolis, and other inland distribution centers where large dry production footprints matter, epoxy can provide attractive lifecycle economics when properly specified. Epoxy systems are available as thin film coatings, high-build systems, mortar systems, and self-leveling resinous floors. Their biggest strengths are aesthetics, chemical resistance in moderate conditions, ease of line-striping, and cost efficiency over broad square footage. They also provide seamless surfaces that are easier to clean than bare concrete or failing tile systems. That said, epoxy has known limitations. Repeated thermal cycling, steam exposure, and hot grease washdown can cause debonding or cracking, particularly if moisture vapor transmission from the slab is high or if the system is too thin. In food facilities, epoxy should not automatically be placed in every “clean” room just because it looks sanitary. Performance must come first. In packaging and dry processing areas, epoxy is commonly chosen for these reasons: Manufacturers should still validate coating choice against sanitation SOPs. Even a mostly dry room can become a wet room if cleaning practices change, if hose-down frequency increases, or if a line modification adds steam or warm-water use. This happens often in growing plants near major U.S. food corridors such as Omaha, Kansas City, Atlanta, and the Carolinas. The explanation behind this table is simple: epoxy excels when the environment is controlled. As soon as the floor is asked to absorb constant impact from moisture, heat, and aggressive cleaning chemistry, the selection should be reconsidered. The market growth trend shown above reflects steady expansion in resinous flooring demand in the United States, driven by food safety investment, cold-chain expansion, e-commerce distribution, and new beverage capacity. More facilities are also replacing aging quarry tile and patchwork concrete with zoned resin systems. Urethane cement is the workhorse system for the harshest food production environments. It is widely selected in poultry, beef, pork, seafood, dairy, brewing, distilling, prepared foods, sauces, frozen foods, and aseptic support areas where floors are exposed to hot water, steam, cold water shock, constant moisture, and aggressive sanitation. In major U.S. processing hubs such as Fresno, Modesto, Green Bay, Sioux Falls, Springdale, and along the Gulf Coast, urethane cement often delivers the best long-term value even when first cost is higher. This system is built for service conditions that break many epoxy floors. It tolerates thermal movement better, can be installed in thicker sections, performs well over concrete, and is commonly used with integral cove bases, ramps, trench edges, and slope corrections. In many plants, urethane cement is not just a coating; it is a protective operational surface. Urethane cement is usually preferred when the floor sees: Its superior performance in wet and thermal shock zones is why processors often specify it in raw rooms, kill floors, marinade areas, kettle and cooker zones, brewery wet process rooms, and dairy production. It is also common around trench drains and equipment legs, where moisture and movement combine to create high failure risk. One of the main buying lessons for 2026 is that floor selection should follow process mapping. If a room contains kettle discharge, CIP return splash, ice melt, or frequent sanitation downtime-to-restart pressure, the floor needs to be treated as critical process infrastructure. This comparison matters because many floor failures in food plants are not material defects. They are specification errors. A dry-room coating is placed into a washdown room, or a thin decorative system is expected to carry industrial thermal abuse. Slip resistance is a balancing act between worker safety and sanitation practicality. Floors that are too smooth can become hazardous with fats, sugars, oils, and water. Floors that are too aggressive can trap residue and make cleanup harder. The right texture profile depends on footwear, contaminants, slope, drainage, cleaning method, and regulatory expectations. In U.S. food plants, texture decisions are especially important in seafood operations in coastal regions, poultry plants in the Southeast, beverage facilities handling syrup or fruit solids, and dairy rooms where milk fats can create invisible slip hazards. Safety teams, sanitation leaders, and operations managers should all participate in the choice. Common texture options include: The key is to match the coefficient of friction target with cleanability. A packaging room in a dry bakery does not need the same profile as a raw poultry washdown corridor. The table shows why there is no universal “non-slip” answer. More grip is not always better. In many cases, the best specification is a mixed texture strategy across a single facility. The industry demand chart highlights where high-traction systems matter most. Protein, dairy, and beverage plants typically carry the highest slip-risk burden due to frequent wet cleaning and product residue. Food plant floors in the United States are exposed to much more than water. Sanitation programs may include sodium hydroxide, acid foams, quaternary sanitizers, chlorine compounds, peracetic acid, citric acid, phosphoric blends, and specialty detergents. Product spills add sugar, salt, fats, animal proteins, lactic acid, and fermentation byproducts. A floor must survive the actual chemistry profile, not just a generic “food safe” claim. Facilities near ports and export markets often face especially rigorous cleaning regimens because downtime and contamination risk carry higher commercial penalties. Plants in New Jersey, Baltimore, Savannah, and Southern California shipping product nationally or globally should review coating chemistry against documented SOPs and concentrations. Epoxy can resist many chemicals well, but resistance varies significantly by formulation and exposure pattern. Urethane cement often performs better under combined chemical and thermal stress, which is why it is common in wet sanitation zones. Still, no system is universal. Chemical concentration, contact time, and cleaning temperature all matter. The value of this table is in forcing real chemical review. Flooring should be selected only after the sanitation and quality teams provide the exact cleaners, concentrations, and temperatures used in each room. Thickness is one of the most misunderstood parts of food facility flooring. A resin system that is too thin may look acceptable after installation but fail early under impact, temperature, and cleaning stress. A system that is too thick or too smooth may be expensive without solving the actual operational problem. The correct build depends on slab condition, service conditions, drainage, and expected wear. In the U.S. market, common food plant ranges include thin film epoxy under 20 mils for low-duty support areas, high-build epoxy from 40 to 125 mils for dry industrial spaces, self-leveling epoxy around 1/8 inch for flatter decorative or clean support rooms, and urethane cement from 3/16 inch to 3/8 inch or more in punishing wet-service environments. Self-leveling systems are useful where flatness, cleanability, and aesthetics matter, but they should not be confused with heavy-duty thermal shock solutions. In some projects, self-leveling epoxy is excellent in dry packaging, while a trowel-applied urethane cement with integral cove and texture is installed ten feet away in the washdown side of the line. This thickness table shows that system selection is closely tied to duty class. A dry room does not benefit from a premium heavy-duty system unless conditions truly justify it. Likewise, a wet thermal area should not be downgraded to save short-term capital. The area chart illustrates an important 2026 trend: more U.S. processors are shifting budget toward heavier-duty wet-zone systems because sanitation intensity, labor shortages, and uptime pressure make early floor failure more expensive than the original material upgrade. Installation strategy can be just as important as material selection. Floor systems fail when substrate prep is weak, moisture conditions are ignored, drains are poorly integrated, or cure times are compressed to satisfy unrealistic startup schedules. In operating food plants, phasing, contamination control, and restart timing must be engineered carefully. Typical planning items include concrete moisture testing, pull-off adhesion testing, shot blasting or scarification, crack and joint treatment, slope correction, cove base integration, drain detailing, humidity control, and final cure verification. Facilities in humid regions such as Florida, Louisiana, and the Mid-Atlantic often need especially careful substrate review. Epoxy cure windows vary by product and ambient conditions, but many systems need longer return-to-service periods than decision-makers expect, especially for full chemical resistance. Urethane cement can sometimes offer faster functional turnaround in industrial conditions, but that depends on system design and site temperature. Fast-cure products can help during shutdowns, yet they should not be used as a substitute for good prep. For plants scheduling flooring work during holidays, weekend outages, or line relocations, the smartest approach is to align flooring with broader capital execution. This is where integrated project teams add value. Companies that understand process utilities, equipment settings, and production commissioning can better sequence flooring around real plant constraints. At DPS service capabilities, project planning is approached as part of the larger production system rather than as an isolated trade package. That matters when a floor replacement overlaps with line moves, utility reroutes, sanitation verification, and startup windows. The reason this schedule table matters is that flooring projects are often sold as simple shutdown work. In reality, they are mini-capital projects that affect safety, sanitation, and startup reliability. Long-term maintenance is where good flooring investments either prove their value or get wasted. Even the best resinous floor will deteriorate faster if drains are poorly maintained, joints are left open, impacts go unrepaired, or cleaning tools are too aggressive. Food processors should have a written floor maintenance protocol with inspection intervals, repair criteria, and responsibility assignments. Recommended practices include: In high-output plants, repairs should be treated as planned asset management, not emergency patching. A small edge failure around a trench drain in a seafood or protein plant can become a major sanitation and slab issue if ignored. On the other hand, many epoxy floors in dry distribution spaces can be economically refreshed with targeted recoats instead of full replacement. 2026 maintenance best practice in the United States is increasingly digital. More operators are adding floor condition tracking to their CMMS platforms, linking observations from sanitation, maintenance, and EHS. This is especially useful in multi-site networks across Texas, the Midwest, and the Southeast. This comparison chart helps clarify the decision. Epoxy usually wins on appearance and installed economy in dry zones, while urethane cement leads in wet durability, thermal shock, and harsher sanitation service. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a practical, operations-focused approach to capital execution. Rather than treating facility upgrades as disconnected scopes, the company works through a design-build-manage model that aligns engineering, construction oversight, equipment integration, and startup execution with the client’s production and profitability goals. From a technological capability perspective, DPS brings multidisciplinary engineering and integration experience across process, mechanical, plumbing, electrical, controls, and automation. That matters when flooring decisions interface with trench drains, CIP systems, process water, steam, refrigeration, tank farms, utility routing, and line controls. In a modern food plant, floor selection is often tied to process design, thermal loads, hygienic zoning, and future capacity plans. More information is available on the company’s about page. From a manufacturing capability standpoint, DPS also supports proprietary equipment and process system solutions for food and beverage operations, including tanks, CIP skids, and custom processing equipment. That broader plant knowledge is valuable because floor systems around vessels, skids, utility drops, and washdown interfaces should be coordinated with equipment placement and maintainability. You can review examples of equipment capabilities in active production environments. From a service capability standpoint, DPS supports capital planning, owner’s representation, project management, process design, construction coordination, installation, and commissioning. For flooring-related projects, that means the conversation can include utility shutdowns, line relocation, slab modifications, drainage upgrades, and startup sequencing instead of only the coating itself. Project examples and execution context can be seen in selected case studies. This integrated perspective is especially useful for processors building or expanding facilities in fast-growth markets such as North Carolina, Tennessee, Texas, Georgia, and Southern California, where speed to market matters but flooring mistakes still carry long operational penalties. 1. Which is better for a U.S. food plant: epoxy or urethane cement?Neither is universally better. Epoxy is typically better for dry processing and warehouse areas. Urethane cement is typically better for wet, hot, and heavily sanitized zones. 2. Can epoxy be used in washdown rooms?It can in some moderate conditions, but repeated thermal shock and aggressive sanitation often make urethane cement the safer long-term choice. 3. What thickness should I specify?Light-duty coatings may be under 20 mils, while industrial epoxy systems often run 40 to 125 mils. Urethane cement in wet food production is commonly 3/16 inch to 1/4 inch or thicker in extreme service. 4. Are self-leveling floors a good option?Yes, especially in dry areas where smoothness and cleanability matter. They are not automatically the right answer for hot washdown or severe wet zones. 5. How long before the area can return to service?It depends on the product, temperature, and whether you mean foot traffic, forklift traffic, washdown, or full chemical exposure. Always verify the manufacturer’s cure schedule and plan startup conservatively. 6. What cleaners should be reviewed before selecting a floor?Review all caustics, acids, sanitizers, degreasers, foaming agents, and specialty chemistry, along with concentrations, temperatures, and dwell times. 7. What are the most common failure points?Drain edges, movement joints, cooler thresholds, cracks in the slab, poor surface preparation, trapped moisture, and using the wrong system for thermal or wet exposure. 8. Is slip resistance always improved by adding more texture?Not always. More texture can reduce cleanability. The best result is a texture profile matched to the contamination risk and cleaning method of each zone. 9. How are 2026 trends affecting floor selection in the United States?Three trends stand out: more heavy-duty flooring in wet zones, more sustainability pressure for longer-life systems with lower replacement frequency, and more scrutiny around worker safety and sanitation-ready design. Facilities are also planning coatings alongside automation and utility upgrades rather than treating flooring as an afterthought. 10. Should flooring be part of a larger capital planning discussion?Yes. Floor systems interact with drainage, utilities, line changes, sanitation, and expansion planning. The best decisions are usually made within a full facility strategy. In summary, the smartest U.S. food facility flooring strategy is usually a zoned one: epoxy where the environment is dry and controlled, urethane cement where the environment is wet, chemically aggressive, or exposed to thermal shock. By tying product choice to actual process conditions, traffic, cleaning chemistry, and return-to-service needs, manufacturers can improve safety, compliance, and asset life while avoiding the hidden cost of premature floor failure. -
Vacuum Tumbler Manufacturer
For food manufacturers in the United States, a vacuum tumbler is one of the most practical tools for improving marinade uptake, protein extraction, product consistency, and line efficiency. Whether the application is chicken breast in Arkansas, pork in Iowa, seafood near Seattle, or value-added beef in Texas, the right vacuum tumbler can reduce marination time, improve cooked yield, and support more repeatable downstream forming, slicing, and packaging. Buyers usually evaluate drum size, vacuum stability, stainless grade, cooling method, automation level, sanitation design, and how well the tumbler fits into existing injection, mixing, or forming lines. In the U.S. market, vacuum tumbler demand is strongest in poultry, red meat, seafood, deli meat, and plant-based protein processing. Plants operating near major logistics corridors such as Chicago, Atlanta, Dallas-Fort Worth, Los Angeles, Savannah, Houston, and Newark often prioritize throughput and labor reduction, while regional processors may focus on recipe flexibility and sanitation. The best purchasing decision is rarely just about equipment price; it depends on total installed cost, utility integration, product mix, and return on capital. A vacuum tumbler uses reduced pressure and controlled drum rotation to open protein structure, improve marinade absorption, and create a gentle mechanical massage that increases extraction of functional proteins. In practical terms, it helps processors in the United States achieve better binding, more even seasoning distribution, higher yield, and shorter marination times than static soaking alone. For most U.S. processors, the right machine selection follows a simple rule set: Manufacturers evaluating a new system should also consider the provider’s engineering depth, not just the machine frame. A partner like Disruptive Process Solutions is relevant because it approaches processing projects from the perspective of plant profitability, utility readiness, automation compatibility, and long-term operability across North America rather than only selling a standalone unit. Vacuum tumbling combines two effects. First, vacuum lowers the pressure around the product, helping meat structure expand and improving the movement of marinade into surface and near-surface tissue. Second, drum rotation lifts and drops the product, generating a controlled massage effect. This action distributes brine, extracts salt-soluble proteins, and improves tackiness for products that must bind well during cooking or forming. On chicken, the process can improve pick-up uniformity and reduce dry edges. On pork and beef, it can support a firmer slice, better bind, and more consistent texture in cooked products. On seafood, careful settings help preserve structure while still promoting flavor penetration. For plant-based proteins, vacuum tumbling may be used to improve coating, seasoning distribution, and water management, especially in prepared foods. Typical operating logic includes loading product and marinade, pulling vacuum, rotating at a set speed, and applying either continuous or intermittent tumbling cycles. Some plants run a rest-and-tumble profile to limit mechanical damage while maximizing uptake. More advanced systems include recipe storage, automatic vacuum control, load cells, and data logging for quality assurance. This table shows why vacuum tumbling is more than simply spinning product in a drum. Each stage affects yield, texture, and food safety. U.S. plants with SQF, BRC, USDA, or customer audit requirements often want tight control and electronic traceability at every point. The choice between continuous and non-continuous vacuum tumblers depends on throughput, SKU complexity, labor strategy, and line architecture. Non-continuous units are batch-based and common in flexible operations producing multiple marinades or value-added SKUs per shift. Continuous units are designed for steady, high-volume flow and are often selected by larger protein processors that need predictable output with minimal interruption. Batch systems are usually easier to sanitize between allergens or flavor changes, making them attractive for co-packers and multi-product facilities. Continuous systems often deliver better labor efficiency for standardized production, but they require stronger upstream and downstream synchronization. If the injector, transfer conveyor, and portioning equipment are not balanced, the line can bottleneck. For processors shipping through hubs like Kansas City, Omaha, Memphis, and Charlotte, line uptime matters as much as machine performance. A batch tumbler may outperform a continuous model financially if product mix is diverse, staffing is variable, or weekly production plans change frequently. When buyers review options, it helps to work with a supplier that can evaluate the full process flow rather than only the drum. On the services side, DPS is known for project planning, installation oversight, integration support, and owner-focused decision making. That matters because a tumbler only performs as expected when utilities, controls, material handling, sanitation access, and downstream flow are properly engineered. Material selection has direct consequences for sanitation life, corrosion resistance, and maintenance cost. In many U.S. plants, 304 stainless is adequate for general food contact surfaces. However, 316L stainless steel is often preferred when the tumbler handles high-salt brines, phosphate systems, vinegar-based marinades, citrus blends, spicy acidic sauces, and aggressive cleaning regimes. The added molybdenum content improves corrosion resistance, while the low-carbon grade helps minimize issues in welded zones. Processors handling poultry marinades with sodium chloride and phosphate blends, seafood with saline exposure, or prepared proteins with citrus and smoke flavor systems often see long-term value in 316L. The upfront cost is higher, but lifecycle economics frequently justify it in demanding environments. The explanation behind this table is straightforward: if the tumbler will live in a corrosive environment, the cost of premature pitting, weld repair, downtime, and sanitation failures can quickly exceed the initial premium for 316L construction. This is especially relevant for processors near coastal markets such as Long Beach, Norfolk, Tampa, or Savannah where humidity and salt exposure can compound corrosion concerns. From a technology standpoint, DPS supports projects where equipment metallurgy must match the recipe chemistry and plant sanitation regime. The company’s engineering capabilities extend across process, mechanical, electrical, controls, and utility design, including PLC programming and SCADA integration when the tumbler must communicate with batching, injection, chilling, or packaging systems. Capacity selection should be based on usable load, not headline drum volume alone. Small 50L to 250L tabletop or pilot units are useful for R&D kitchens, seasoning trials, and restaurant supply innovation labs. Mid-size machines from 500L to 2,000L fit regional processors producing marinated chicken, pork cuts, deli items, or seafood. At the top end, industrial systems handling up to 4,500 kg per batch are designed for high-output plants serving national retail and foodservice channels. Processors in the United States often underestimate how capacity ties into handling labor. A machine may have enough theoretical volume, but if loading bins, elevators, or discharge conveyors are undersized, real output falls below target. That is why plant-level design matters. This capacity comparison is useful because many buyers select too small a machine to save on capital, then lose money on labor, overtime, and missed throughput. Others overbuy capacity without sufficient upstream supply or downstream chilling. Matching actual shift goals to net batch volume is more important than choosing the largest drum available. On the manufacturing side, DPS has been expanding its own branded equipment portfolio, including process tanks, CIP systems, marination tumblers, and cooking vessels. That manufacturing capability matters for buyers who need customization instead of a rigid catalog model. You can review broader equipment capabilities here when considering integrated solutions rather than isolated machine purchases. Temperature rise during tumbling can damage texture, shorten shelf life, and complicate compliance. Mechanical action generates heat, and long cycles can push protein temperatures upward if cooling is not built into the process. In the United States, where food safety expectations are strict and logistics may involve long transport distances from plant to distribution center, temperature control is not optional for many applications. Refrigerated jackets use chilled glycol or other cooling media around the drum to hold product temperature during processing. CO2 injection systems provide direct cooling and can be effective where rapid heat removal is required. The right choice depends on recipe sensitivity, cycle duration, plant utilities, and cost structure. This table shows why temperature control decisions should be tied to the full plant system. A tumbler with excellent mechanics can still underperform if the plant lacks chilled brine management, glycol support, or stable CO2 delivery. Facilities near hot-weather logistics centers such as Phoenix, Dallas, or Miami often pay closer attention to thermal margins. The line chart above illustrates a realistic growth pattern for vacuum tumbler demand in the United States, driven by value-added protein products, automation, labor pressure, and the expansion of ready-to-cook and ready-to-heat categories. Cycle optimization is where many processors unlock the most value. Two plants can run the same tumbler and get very different results depending on vacuum level, rpm, fill percentage, cycle length, rest intervals, marinade ratio, and product temperature. Over-aggressive settings can damage texture, while mild settings may leave yield and flavor on the table. Best practice is to validate parameters by product family and end-use. A thin chicken fillet for foodservice may need a different profile than diced pork for skewers or a formed roast program. Test work should consider post-cook yield, slice quality, purge, flavor distribution, and consumer bite. The explanation here is important: there is no single “best” tumbler recipe. Processors should tune cycles to the raw material, injector pattern, cut geometry, finished specification, and cooking method. Automation that stores and protects validated recipes can prevent expensive operator variation across shifts. This demand chart reflects the reality of the U.S. market: poultry remains the leading segment for vacuum tumbling, followed by pork and beef, while prepared foods and plant-based categories continue to grow. A tumbler should be evaluated as part of a system, not as a standalone cylinder. In many high-performing U.S. facilities, the process chain includes raw receiving, trimming, injection, transfer, tumbling, equilibration, forming or netting, thermal processing, chilling, slicing, and packaging. When these stages are disconnected, labor rises and consistency drops. Well-integrated lines can use infeed conveyors, bin lifts, automatic loading, recipe-driven vacuum control, discharge conveyors, and data transfer to upstream injectors or downstream formers. This is especially valuable in markets serving major retailers and foodservice chains that require repeatability across plants and distribution regions. This table highlights why engineering support matters. A vacuum tumbler can be excellent on paper but disappointing in the plant if conveyors, utilities, controls, or floor layout are not aligned. For companies expanding in regions such as the Carolinas, the Midwest, or Southern California, a system-minded approach usually produces the strongest ROI. DPS is particularly relevant in this type of project because its technological capabilities go beyond equipment supply. The company works across structural, mechanical, plumbing, electrical, process, and automation scopes, including PLC and SCADA solutions that help tumblers communicate with broader line operations. That is useful when a processor wants recipe control, alarms, trend data, and integration with utility systems such as compressed air, refrigeration, or CIP. The area chart shows the trend shift from isolated batch processing toward more connected marination, tumbling, and forming lines. Rising labor cost and stronger traceability expectations are pushing U.S. manufacturers toward integration. Return on investment is usually driven by three factors: yield improvement, cycle time reduction, and labor savings. Yield gains of even 1% to 3% can be financially significant for large poultry, pork, or deli plants. Faster marination may allow a processor to avoid adding a second shift. Labor reductions from automated loading, recipe control, and discharge handling can further improve the case. ROI should be modeled using realistic plant data: annual pounds processed, raw material cost, current yield, target yield, labor cost per shift, sanitation time, rework rate, and utility usage. Freight and installation also matter, especially for plants receiving equipment through ports like Long Beach, Houston, Savannah, or Newark and then transporting to inland sites. This table helps frame the financial discussion. In large U.S. protein plants, raw material yield often dwarfs all other savings. In specialty or mixed-SKU operations, labor and changeover flexibility may be the bigger economic driver. The comparison chart reflects a common U.S. buying reality. The cheapest option may not deliver the best lifecycle value if integration, service, or customization are weak. Buyers focused on long-term economics often favor engineering-backed suppliers over simple catalog resellers. On service capabilities, DPS uses a design-build-manage model that aligns well with capital projects where schedule, utility tie-ins, construction coordination, and operating readiness all matter. Founded in Cary, North Carolina, with a West Coast presence in Lake Forest, California, the company supports manufacturers across the United States and Canada with engineering, project execution, installation, compliance-aware system integration, and owner-representative style support. That model is especially valuable when the tumbler is part of a larger line modernization rather than a single machine replacement. What industries use vacuum tumblers most in the United States?Poultry, pork, beef, deli meats, seafood, prepared meals, and selected plant-based protein manufacturers are the largest users. Poultry remains the strongest segment because marination consistency and yield are major profit drivers. Is a vacuum tumbler better than static marination?In most commercial production environments, yes. Vacuum tumbling usually improves uptake consistency, reduces process time, and supports stronger protein extraction than static soaking alone. When is 316L stainless steel worth the extra cost?It is often worth the premium when the plant runs salty brines, acidic marinades, citrus or vinegar recipes, frequent chemical sanitation, or high-humidity operating conditions. How do I size a tumbler correctly?Start with actual pounds per shift, target batch time, fill rate, changeover requirements, and upstream/downstream flow. Do not size only by gross drum volume. Consider loading, unloading, staging, and cooling capacity as well. What is the difference between a continuous and batch tumbler?A continuous unit is designed for steady high-volume flow with fewer interruptions. A batch, or non-continuous, tumbler is better for recipe flexibility, lot separation, and plants with frequent SKU changeovers. Can a tumbler be integrated with injectors and formers?Yes. Many U.S. plants integrate injectors, conveyors, lifts, tumblers, surge handling, and formers through shared control logic and production scheduling. Do I need cooling on the tumbler?If cycle times are long, product temperature is tightly controlled, or the plant is handling sensitive proteins, active cooling is strongly recommended. Jacketed drums and CO2 systems are the most common options. What should I ask a supplier before buying?Ask about usable capacity, stainless grade, weld finish, vacuum performance, sanitation access, recipe control, service support, spare parts, installation scope, and expected ROI based on your products. Are local suppliers always better than imported machines?Not always, but domestic or North America-based engineering support can significantly improve installation, commissioning, spare parts response, and customization. That becomes more important in complex plants or time-sensitive expansion projects. What trends will shape vacuum tumblers in 2026?The key trends are smarter automation, digital recipe traceability, energy-conscious cooling design, more sanitary open-frame construction, higher use of 316L in aggressive environments, and stronger sustainability pressure around water, labor, and yield efficiency. Policy and audit pressure will continue pushing processors toward documented controls, validated sanitation, and integrated data systems. The U.S. market for vacuum tumbler systems is moving toward integrated, data-aware, sanitation-friendly equipment. Growth is linked to higher demand for value-added proteins, convenience foods, and premium seasoned products sold through grocery, club, meal-kit, and foodservice channels. Plants located near major trade routes and logistics centers are especially interested in reducing labor dependency and improving recipe repeatability because transportation cost and labor availability can directly affect profitability. Buyers in the United States should evaluate vendors on five levels: mechanical design, sanitary design, metallurgy, controls capability, and project support. Mechanical design includes drum geometry, paddle style, load factor, vacuum stability, and discharge efficiency. Sanitary design includes surface finish, drainability, access for washdown, gasket quality, and dead-leg avoidance. Metallurgy should match recipe chemistry. Controls should support recipe security, alarm history, and line communication. Project support should cover layout, utilities, installation, commissioning, and operator training. Applications are broad. In poultry, vacuum tumblers are used for breast fillets, tenders, wings, strips, and deli programs. In pork, they support loin, ham, rib meat, and seasoned retail cuts. In beef, they help with fajita strips, roast programs, and deli applications. In seafood, shrimp and fish portions benefit from seasoning distribution and moisture management. In prepared foods, the tumbler supports flavored protein components that later move to kettles, cookers, or packaging lines. Local supply matters, but “local” should be defined carefully. A nearby sales office is less valuable than strong engineering and execution. For example, processors on the East Coast may prioritize responsive support from Cary, Charlotte, or Atlanta, while West Coast operators may prefer access through Southern California. Midwestern plants in Missouri, Iowa, Nebraska, or Illinois often care most about installation coordination, startup readiness, and spare parts access during peak production periods. A capable partner should support all of these concerns, not just quote a machine. As for future direction, 2026 will likely bring more recipe automation, better sensor feedback, improved thermal control, and stronger sustainability scrutiny. Yield improvement will remain the most powerful financial argument, but water use, sanitation chemistry consumption, and maintenance planning will become more visible in capital decisions. Equipment that can connect to plant-wide SCADA, MES, or digital quality systems will hold an advantage, especially in multi-site operations and high-audit environments. For processors that want proof of execution, reviewing real project outcomes is useful. DPS’s approach to capital projects emphasizes profitability, system fit, and practical implementation. That perspective can be seen in its broader project experience and case studies and project examples, which are helpful when evaluating whether a tumbler investment should remain a standalone purchase or become part of a wider processing upgrade. In short, the best vacuum tumbler manufacturer or integration partner for the United States market is not the one with the lowest quoted price. It is the one that can align product quality, corrosion resistance, thermal control, automation, sanitation, throughput, and project execution with the processor’s actual business model. When those elements are aligned, vacuum tumbling becomes a profit tool rather than just another machine on the floor. -
2026 Guide to Food Facility Hygienic Cladding for FDA and USDA Compliance
Food and beverage plants in the United States are under constant pressure to improve sanitation, reduce downtime, support audit readiness, and protect product quality. In that environment, hygienic wall cladding is not just a finish material. It is part of the food safety system. Whether a facility is handling poultry in Arkansas, dairy in Wisconsin, sauces in New Jersey, aseptic beverages in California, or seafood near the Port of Savannah, wall surfaces must stand up to washdown chemicals, daily abuse, temperature swings, and detailed inspections. This guide explains how to evaluate hygienic wall panels for U.S. food plants, with a focus on PVC vs FRP panel selection, FDA and USDA expectations, installation details, joint treatment, cleanability, fire performance, and retrofit strategy. It is written for plant owners, engineering managers, quality leaders, sanitation teams, and capital project stakeholders looking for a practical answer rather than a generic product pitch. If you need the short version, choose hygienic wall cladding based on sanitation intensity, chemical exposure, traffic, fire code requirements, and installation conditions. In most U.S. food facilities, smooth PVC hygienic panels are often preferred in high-cleanability spaces because they can deliver a bright, low-porosity surface with welded or sealed joints. FRP remains common where impact resistance, lower first cost, and broad contractor familiarity matter. Neither material is automatically compliant by itself. The installation method, sealant system, substrate condition, joint detailing, cleanability, and code compliance all determine whether the finished wall is suitable for a regulated food environment. For facilities under FDA oversight, surfaces should be smooth, durable, cleanable, and maintained in sanitary condition. In USDA-inspected environments, especially meat and poultry rooms, expectations are often stricter in practice, particularly around moisture resistance, joint integrity, and the elimination of harborage points. High-risk processing zones usually benefit from systems with minimal seams, coved transitions, and details designed for repeated wet cleaning. For most plant teams, the best buying sequence is simple: define the room risk level, map the cleaning chemistry, verify fire requirements, inspect the substrate, then select a cladding system and installer together. That process prevents the common mistake of buying panels first and discovering later that the adhesive, trims, or substrate conditions undermine performance. The U.S. market is growing because older factories in Chicago, Philadelphia, Dallas-Fort Worth, Atlanta, and the Inland Empire are being modernized to meet higher audit standards, while greenfield plants near logistics hubs such as Houston, Charlotte, and Columbus are being built for more aggressive sanitation programs. The growth trend above reflects a realistic increase in retrofit and expansion work across American food manufacturing, especially where labor shortages and retailer audit pressure are pushing companies to standardize easier-to-clean interiors. PVC and FRP are the two most frequently compared options in U.S. hygienic wall upgrades. They are not interchangeable in every room. PVC wall panels are usually selected for smoothness, chemical resistance, moisture resistance, and a cleaner appearance in areas with frequent washdown. FRP wall panels are often selected for impact resistance, broad availability, and lower installed cost in dry or moderately wet support spaces. However, the wrong material in the wrong room can increase repair frequency, sanitation effort, and long-term ownership cost. Plant teams should also remember that panel chemistry varies by manufacturer. A generic FRP sheet and a purpose-built food plant FRP system are not the same product. Likewise, PVC panels differ in thickness, hardness, installation system, and seam treatment options. Procurement based on panel price alone can create expensive rework later. The table shows why material selection should be room-specific. For example, a protein plant in Omaha may use PVC in post-lethality packaging rooms and FRP in adjacent maintenance corridors. A beverage facility near Los Angeles/Long Beach may choose PVC around syrup rooms and blending areas but retain FRP in warehouse walls where forklift impact is the bigger issue. Buying advice for U.S. operators: ask for panel thickness, seam method, substrate requirements, chemical compatibility data, cleaning temperature limits, fire test data, impact rating information, and warranty exclusions. Also ask how the material behaves at floor-to-wall transitions and around penetrations. Many failures happen at the details, not on the flat field of the wall. In the United States, FDA and USDA frameworks do not simply prescribe one panel material for all plants. Instead, they focus on performance. Wall surfaces should be durable, cleanable, non-absorbent where needed, and maintained so they do not contribute to contamination. In practice, inspectors and auditors want to see intact finishes, sealed joints, no flaking coatings, no standing moisture behind panels, no delamination, and no inaccessible niches around utilities and supports. FDA-regulated facilities such as beverage, dairy, ingredient, and prepared food plants should align wall systems with current good manufacturing expectations and preventive controls. USDA-inspected meat and poultry plants often operate under more intensive daily washdown conditions, which makes moisture management, seam integrity, and damage repair especially important. In high-volume facilities near Kansas City, Fresno, Grand Rapids, or Charlotte, wall systems are often selected in conjunction with floor coating, drains, ceiling construction, and air handling because those systems interact. A wall that looks acceptable in isolation may fail operationally if it traps moisture at the slab edge or breaks down under thermal shock from nearby sanitation procedures. The important point is that compliance is demonstrated by the completed environment. A premium panel installed over a damp, failing substrate with poor sealing is still a poor sanitary wall system. This is why capital teams often benefit from integrating wall selection into broader facility planning, especially when line changes affect washdown, drainage, traffic, or temperature. Companies looking for broader project support can review food and beverage engineering services that connect sanitary construction decisions with the rest of the production environment. Installation quality determines whether hygienic cladding performs for ten years or starts failing in one. In U.S. retrofit work, the most common substrates are painted CMU, gypsum board in support areas, old FRP, ceramic tile, and occasionally insulated wall assemblies. Each requires different prep. Surface flatness, adhesion, moisture content, and thermal movement must be addressed before the first panel goes up. Seamless or near-seamless performance is especially important in high-risk environments. Depending on the panel system, contractors may use heat-welded joints, chemically welded joints, interlocking profiles, hygienic H-trims, or sealant-filled seams. The right method depends on room risk and cleaning intensity. A dry ingredient room has very different needs than a ready-to-eat poultry packaging room. Good seam practice includes consistent gap control, manufacturer-approved sealants, temperature-aware installation, and field inspection before the room is released. It also includes coved inside corners, sanitary base transitions, and well-detailed terminations at doors, drains, and ceilings. Plants that install excellent panels but ignore utility penetrations or floor transitions often see mold risk, odor retention, or recurring sanitation findings. For complex projects, installation should be coordinated with process piping, electrical drops, wall-mounted equipment, and controls panels. That is one area where firms with broader engineering depth can add value. Disruptive Process Solutions, for example, brings structural, mechanical, plumbing, electrical, process, and controls coordination to food and beverage projects, which helps avoid wall penetrations and access conflicts being solved in the field after cladding is complete. Panel brochures often promise washdown durability, but food plants should verify performance against their actual sanitation regime. A cheese plant using acid cleaners in Idaho, a protein plant using chlorinated alkaline foam in Georgia, and an RTD beverage site using quaternary sanitizers in Nevada will stress surfaces differently. Cleanability is not only about whether the wall survives chemical exposure. It is also about whether soils release quickly, whether the finish stains, and whether joints stay intact over time. Testing should review concentration, contact time, cleaning temperature, rinse procedures, and frequency. A panel that performs well under weekly cleaning may struggle under two wet sanitation cycles per shift. In areas with aggressive foaming and hot water, adhesive selection matters as much as face-sheet chemistry. Best practice is to build a sanitation compatibility matrix before material approval. That matrix should include chemical names, supplier concentrations, room temperature, wash pressure, expected splash zones, and daily frequency. Then compare those inputs with manufacturer data and, if needed, field mockups. This is especially valuable in plants subject to repeated changeovers or allergen cleanouts. By 2026, one of the most important trends in the United States is the move toward lower-water and lower-chemical cleaning strategies driven by sustainability goals and wastewater cost. That shift can favor smoother, more easily cleaned wall systems because operators want faster soil release with less aggressive chemistry. The area trend reflects a real market change: more U.S. manufacturers are evaluating lifetime sanitation efficiency instead of selecting wall finishes on material cost alone. Food safety is critical, but wall systems must also satisfy building and fire code review. In the United States, ASTM E84 is commonly referenced to evaluate surface burning characteristics, including flame spread and smoke developed. Plant owners should not assume all hygienic wall systems carry the same tested results. Performance can vary by panel, thickness, backing, adhesive, and installation assembly. Code review may differ by occupancy, room type, local jurisdiction, and whether the panel is used throughout a space or only in limited areas. Plants in states with heavy food manufacturing activity such as North Carolina, Texas, California, Iowa, and Pennsylvania often face varied interpretations by local authorities having jurisdiction. Early coordination with the architect, contractor, and code consultant avoids surprises after procurement. When reviewing ASTM E84 data, ask whether the test reflects the exact assembly intended for your project. A panel tested one way over one substrate does not automatically mean identical performance over another substrate or with another adhesive. This matters in retrofits where the existing wall construction may not match standard test setups. A sound specification should identify required documentation, listing current test values, installation conditions, and any application limits. If the project involves cold rooms, utility chases, or process areas with elevated temperatures, additional code considerations may apply. In all cases, code compliance should be reviewed alongside hygiene, not after the sanitary design decision is already made. Not every room deserves the same cladding system. High-risk zones require more rigorous materials and detailing than dry warehouses or non-production corridors. For practical decision-making, divide the plant into risk bands: low-risk dry support, medium-risk processing, high-moisture washdown, and high-risk post-lethality or ready-to-eat zones. That risk map should drive material choice, seam strategy, and maintenance planning. In protein, dairy, and aseptic operations, the highest-risk rooms usually include exposed product areas, post-cook packaging, clean fill spaces, and hygiene transition corridors. These rooms need smooth surfaces, minimal joints, and disciplined integration with air handling, drains, and utility penetrations. In beverage plants, syrup rooms, blending rooms, high-care packaging areas, and aseptic support spaces often need a higher wall standard than bulk dry storage. The highest-performing facilities treat wall systems as part of hygienic zoning. They do not over-specify every room, but they do avoid under-specifying the critical rooms. This balance helps control capital cost while protecting sanitation outcomes. The bar chart reflects how protein, dairy, and beverage categories continue to lead demand because they combine heavy sanitation needs with high audit visibility and frequent facility upgrades. Retrofit work is the dominant use case in many U.S. plants because older facilities cannot afford long shutdowns. Installations over existing painted block, tile, or worn FRP can be successful, but only if the substrate is stable, dry, and properly prepared. Covering a failing wall does not fix the underlying problem. It hides it until the damage becomes larger and more expensive. Retrofits in older industrial cities such as Milwaukee, St. Louis, Newark, and Memphis often reveal hidden moisture, uneven walls, past patching, and undocumented penetrations. Plants near humid coastal trade hubs like New Orleans and Savannah may also have more vapor-management concerns. Before committing to an overlay system, conduct a substrate assessment, moisture survey, adhesion review, and traffic analysis. The retrofit strategy should also consider sequencing. In many cases, wall work is best coordinated with floor resurfacing, drain replacement, utility rerouting, or equipment relocation. That integrated approach often reduces total downtime even if the initial planning takes longer. This is one of the reasons many owners prefer a design-build-manage model rather than separate disconnected vendors. Coordinated planning can align civil, MEP, process, and sanitary finish decisions into one execution path, reducing rework and preserving startup dates. Project examples and execution approaches can be explored through food and beverage project case studies. Disruptive Process Solutions serves food and beverage manufacturers across all 50 U.S. states and Canada, supporting both greenfield and retrofit capital projects. The firm is headquartered in Cary, North Carolina, with a West Coast presence in Lake Forest, California, and works with manufacturers from the Carolinas to the Central Valley, from the Midwest protein corridor to Gulf Coast beverage operations. Rather than approaching hygienic cladding as an isolated finish decision, DPS evaluates it as part of the broader manufacturing system. On the technology side, DPS supports structural, mechanical, plumbing, electrical, process, and controls engineering, including automation, PLC programming, and SCADA integration. That technical depth matters because wall systems in food plants are affected by pipe routing, utility penetration count, sanitation methods, room pressurization, temperature, and line layout. When a facility is redesigning a syrup room, retort area, dairy process room, or aseptic support space, cladding decisions benefit from that cross-disciplinary coordination. On the manufacturing side, DPS also develops and supplies its own branded process equipment, including storage and process tanks, CIP systems, marination tumblers, and cooking vessels. That manufacturing capability gives the team practical visibility into how real equipment interacts with hygienic room construction. A wall panel does not perform in isolation; it performs beside hose reels, control stations, supports, curbs, drains, and washdown routines. On the service side, DPS delivers capital planning, feasibility work, owner’s representation, project management, general contracting in licensed jurisdictions, equipment supply, installation, and system integration. Its Design Build Manage model is intended to help manufacturers connect smart capital spending with long-term operational profitability. For plants planning sanitary upgrades, production expansions, or full facility modernization, you can learn more about the company, review broader engineering and project services, or explore available process equipment solutions. That combination of technological capabilities, manufacturing capabilities, and service capabilities is especially relevant when hygienic cladding is only one part of a wider plant initiative such as a line relocation, utility expansion, high-care room buildout, or sanitation-driven retrofit. The comparison chart highlights a common market reality: no single wall system wins every category. The right choice depends on the room, the cleaning regime, and the operating profile. Which is better for food plants in the United States, PVC or FRP?Neither is universally better. PVC is often favored in higher-risk wet or clean-critical spaces because of its smooth finish and seam options. FRP is often practical in lower-risk or impact-heavy areas. The best choice depends on room risk, washdown intensity, and code requirements. Do FDA or USDA require a specific wall panel material?Usually no. They focus on sanitary performance: cleanable, durable, moisture-resistant surfaces maintained in good condition. Material selection must support that outcome. Can hygienic panels be installed over old tile?Yes, in many cases. But the tile must be stable, the wall must be dry, and flatness issues must be corrected. Hidden moisture is the biggest risk in tile overlays. Are seamless walls really possible?Fully monolithic results depend on the system, but near-seamless hygienic performance is achievable with welded or well-sealed joints, coved details, and careful penetration management. Why does ASTM E84 matter for food facility walls?It helps demonstrate fire performance for interior finish review. Local code authorities may require documentation before approving the wall assembly. What is the biggest installation mistake?Skipping substrate assessment. Many failures come from moisture, poor adhesion, unstable old coatings, or rushed detailing rather than from the panel itself. How should plants budget for cladding?Budget by room risk, not by gross square footage alone. Include substrate repair, utility modifications, trims, sealants, protection rails, and downtime costs. What are the biggest 2026 trends?More retrofits in aging U.S. plants, stronger demand for easier-to-clean surfaces, closer attention to water and chemical reduction, and more integrated design between process systems and sanitary construction. For U.S. manufacturers, the best hygienic cladding program is the one that matches real operating conditions. A wall system should help the sanitation team work faster, help quality teams pass audits with confidence, help maintenance reduce emergency repairs, and help leadership protect long-term plant profitability. When those goals are aligned, the cladding decision becomes part of a smarter manufacturing strategy rather than a simple finish selection. -
Industrial Food Cookers
Food processing cooker systems are the thermal backbone of many U.S. food plants. The right industrial cooking solution depends on product viscosity, target lethality or pasteurization level, throughput, package format, sanitation demands, utility costs, and downstream cooling or freezing requirements. For processors in the United States, the best choice is rarely just “buy a cooker”; it is to engineer a complete cooking process that protects food safety, texture, yield, labor efficiency, and long-term profitability. Across major food manufacturing hubs such as Chicago, Kansas City, Fresno, Dallas, Atlanta, Charlotte, Houston, and the ports of Los Angeles/Long Beach and Savannah, processors are investing in more precise, energy-aware, data-driven thermal systems. Demand is strongest in prepared foods, protein processing, sauces, dairy, aseptic products, and shelf-stable packaged foods. Whether a facility needs a jacketed kettle for sauces, a retort for shelf-stable meals, a smokehouse or oven for proteins, or a continuous cooker for high-volume line production, the purchasing decision should connect process design, utilities, automation, sanitation, and regulatory validation from the beginning. Industrial food cookers include kettles, retorts, ovens, fryers, blanchers, scraped-surface systems, and continuous thermal lines. In the United States, processors typically choose among these based on product type, hourly capacity, package format, heating medium, and compliance obligations. High-viscosity sauces often favor steam-jacketed kettles; shelf-stable canned or pouched foods usually require retorts; proteins and prepared meals commonly rely on ovens or smokehouses; and high-output vegetables, grains, pasta, and ready meals often benefit from continuous cookers. From a capital planning standpoint, buyers should evaluate five issues first: required throughput, critical temperature profile, product sensitivity, utility availability, and integration with chilling or packaging. A cooker that reaches target temperature quickly but causes burn-on, moisture loss, or inconsistent lethality is not an optimized asset. Strong projects align thermal performance with production economics. For companies seeking broader process planning, equipment integration, and utility design, food and beverage engineering specialists can help define the most commercially sound path before equipment is specified. That is especially important when multiple steps—mixing, cooking, holding, cooling, filling, and CIP—must work as one system rather than isolated machines. The table above summarizes why cooker selection must start with process realities, not only nameplate capacity. U.S. manufacturers dealing with SKU proliferation, retailer audits, labor pressure, and energy volatility benefit from a more engineered approach. The main classes of industrial food cookers serve different food categories and thermal objectives. Kettles are versatile for soups, sauces, fillings, jams, gravies, dairy bases, and other pumpable or semi-viscous foods. They may be steam-jacketed, direct-injection, or electrically heated and often include agitation, vacuum options, ingredient dosing, and automated recipe control. Retorts are used for packaged foods that require thermal sterilization or high-level pasteurization after filling and sealing. They are common in canning, pet food, pouch meals, ready entrees, seafood, vegetables, and institutional products. Batch retorts remain widely used, but rotary, static, water spray, water immersion, and steam-air systems all serve different package and heat transfer conditions. Ovens and smokehouses dominate in meat, poultry, plant protein, bakery, and prepared meal operations. They can roast, bake, steam-cook, brown, smoke, or finish products before chilling, slicing, or packaging. Airflow, humidity, zone control, and belt loading strongly affect yield and color. In protein-heavy regions such as Arkansas, Georgia, Iowa, Nebraska, and North Carolina, these systems are critical production assets. Continuous cookers are favored where throughput and consistency outweigh batch flexibility. They include spiral ovens, belt blanchers, screw cookers, hydrostatic systems, continuous steam tunnels, and scraped-surface heat exchangers. They are common in vegetables, grains, pasta, sauces, liquid dairy, confections, and ready meal components. In the U.S. market, equipment choice often reflects local product clusters. Tomato processors in California may prefer continuous systems for high-volume sauces. Midwest prepared-food plants often pair kettles with cooling and filling skids. Gulf Coast seafood processors may rely heavily on retort technology for stable packaged products. Matching the cooker to the regional supply chain and labor environment can materially affect project payback. This growth trend reflects rising investment in prepared meals, protein processing upgrades, automation, and thermal validation tools across the United States. Direct heating transfers energy straight into the product, usually through steam injection, infusion, open flame, or direct contact systems. It provides rapid heat-up and can be highly efficient where fast thermal response matters. Direct methods are common in certain liquid foods, blanching systems, and some kettle operations. However, they may change product moisture content or demand tighter condensate and flavor management. Indirect heating uses a barrier—such as a vessel jacket, coil, plate, scraped surface, or heat exchanger wall—between the heating medium and the food. This approach is preferred where flavor protection, burn-on control, contamination avoidance, or exact thermal control matters more than the fastest possible heating rate. It is widely used for sauces, dairy, confectionery, and many high-value formulated foods. There is no universal winner. Direct heat often benefits high-volume, lower-viscosity products that can tolerate dilution or are designed around steam addition. Indirect heat is usually better for viscous, premium, particulate, allergen-sensitive, or highly formulated products where repeatability is more important than speed alone. As a buying rule, choose direct heating when speed and thermal efficiency dominate, and choose indirect heating when product integrity and exact control dominate. Many U.S. processors ultimately use both in different areas of the same plant. Batch cookers remain a strong option for manufacturers managing frequent recipe changeovers, seasonal demand, co-packing schedules, or premium low-volume products. They are easier to pilot, easier to validate during product development, and often cheaper to install at modest capacities. Batch kettles, retorts, smokehouses, and vacuum cookers fit plants that value flexibility and shorter product campaigns. Continuous cookers are best where output, labor efficiency, and consistency drive the business case. Once dialed in, they reduce operator intervention, support automation, and integrate more smoothly with upstream dosing and downstream cooling or packaging. For large-scale processors around major logistics corridors such as Dallas-Fort Worth, Chicago, central California, and New Jersey distribution zones, continuous lines often unlock better margin at scale. The hidden variable is total system architecture. A continuous cooker can still underperform if ingredient handling, buffer tanks, chill capacity, or packaging speed are undersized. Likewise, batch systems can outperform expectations when sequencing, CIP planning, and labor deployment are well designed. An anonymized example from the prepared-food segment illustrates the point. A regional manufacturer initially planned a major capacity expansion for cooked sauce and meal bases. Instead of adding large new thermal assets immediately, the process review identified sequencing and controls constraints as the true bottleneck. By redesigning control logic, buffer timing, and operator workflow, the plant improved throughput significantly before larger capital was deployed. That philosophy—solve the process, not just buy a bigger machine—is increasingly important in U.S. manufacturing. The bar chart shows why supplier selection and system design increasingly focus on prepared foods, proteins, and sauce applications in the United States. Temperature uniformity is one of the most important performance measures in industrial food cooking. A system that hits target average temperature but leaves cold spots can create safety risk; one that overheats edge zones or thin areas can destroy texture, color, or yield. Uniformity matters in retorts, ovens, kettles, and continuous systems alike. Key variables include agitation method, airflow balance, steam distribution, vessel geometry, product depth, fill weight, particulate size, belt loading, and sensor placement. Plants should not assume a machine is uniform because the setpoint looks stable on the HMI. Verification through mapping, challenge testing, and process data trending is essential. For USDA- and FDA-regulated foods, thermal performance must be tied to validated process expectations. In practice, that means tight instrumentation, calibrated sensors, reliable recording, documented hold times, alarm management, and repeatable recipes. It also means thinking beyond the cooker itself. Uneven feed temperature entering a continuous line or inconsistent package stacking in a retort can undo otherwise strong thermal design. Processors evaluating upgrades often need not just equipment, but controls architecture. That is where broad process and automation capabilities matter. Teams that can combine process engineering with PLC programming, SCADA visibility, recipe management, and utility balancing can materially improve thermal repeatability. Companies offering integrated process engineering and project delivery services are often better positioned to solve the entire cooking step rather than only the machine purchase. In 2026 and beyond, thermal mapping, digital historian data, predictive alarms, and tighter model-based control are expected to become standard in larger U.S. facilities. Retailer scrutiny and internal OEE programs are pushing plants to document not just that a product was cooked, but that it was cooked uniformly and efficiently. Material selection affects corrosion resistance, cleanability, longevity, and regulatory confidence. In most food applications, 304 stainless steel is the default for structural and product-contact surfaces because it balances cost and performance well. However, 316L becomes important where products are high in salt, acid, chlorides, aggressive cleaning chemistry, or where higher corrosion resistance helps preserve service life. For example, marinades, brines, seafood, tomato-based products, and some dairy or acidic formulations may justify 316L in product contact zones. Coastal environments near ports such as Houston, Norfolk, Newark, or Long Beach can also influence material strategy due to ambient corrosion conditions, especially in utility or washdown areas. Surface finish, weld quality, drainability, and hygienic design are just as important as the base alloy. Material upgrades should not be specified blindly. The smarter approach is to compare chemistry, sanitation practice, run hours, and expected service life. That avoids overspending on unnecessary alloy while preventing expensive corrosion-related downtime later. Cooking does not end when heat is applied. In many U.S. food plants, the real success of a cooking system depends on what happens immediately afterward: cooling, chilling, freezing, holding, dewatering, or packaging. A fast, stable thermal process can still fail commercially if post-cook cooling is too slow, causes purge loss, or creates product traffic jams. Cook-chill lines for soups and sauces may require scraped-surface cooling, plate heat exchange, glycol integration, or chilled water loops. Protein operations often need blast chilling, spiral chilling, or cold-room equalization before slicing or packaging. Frozen meal lines may route cooked components to IQF or spiral freezers. Retort operations may need controlled post-process cooling to protect package integrity and prevent overcooking. From an engineering standpoint, utility balance matters. Steam demand on the front end must be coordinated with refrigeration, glycol, chilled water, condensate recovery, compressed air, and CIP capacity on the back end. Providers with capabilities in cooking vessels, utility systems, and controls can create smoother thermal-to-cold transitions. Companies offering integrated process equipment solutions often add value by designing vessels, CIP systems, and custom process skids that match the broader line rather than forcing the plant to adapt around disconnected assets. In 2026, sustainability pressure is increasing interest in heat recovery from cook and cool loops, smarter refrigeration staging, and utility dashboards that show energy per pound produced. Plants in power-constrained or water-stressed regions, including parts of California, Arizona, and Texas, are especially focused on this integration. Energy source selection can change both operating cost and cooking performance. Steam remains the dominant heating utility in many U.S. food plants because it provides high heat transfer rates, supports multiple process users, and fits sanitary vessel design well. Gas-fired systems often offer favorable utility economics where natural gas supply is strong, especially for ovens and certain direct-heated assets. Electric systems deliver excellent controllability and are increasingly attractive where decarbonization or local emissions constraints matter. Thermal fluid systems can be useful where precise high-temperature indirect heating is needed without steam condensate issues. The right answer depends on local utility rates, decarbonization goals, boiler room condition, maintenance capability, and production profile. A Midwest plant with an existing robust boiler system may logically stay steam-based. A greenfield site in the Southeast with utility incentives may consider electric or hybrid solutions. Plants facing air-permitting complexity may prioritize lower-emission options even if first cost is higher. The area chart reflects a realistic trend: steam remains dominant, but electric and hybrid interest is rising as sustainability goals and grid modernization reshape plant utility decisions. In the United States, compliance requirements for industrial food cookers depend on product category, hazard profile, package format, and regulatory jurisdiction. USDA-regulated meat and poultry products face specific expectations for lethality, stabilization, recordkeeping, and sanitation. FDA-regulated foods must align with preventive controls, process validation, sanitation controls, and applicable low-acid canned food or acidified food requirements where relevant. Pasteurization or sterilization is not just a machine setting; it is a documented and validated process. Retort systems require especially rigorous process establishment, instrumentation, venting, distribution understanding, and record retention. Ovens and smokehouses in protein plants must support validated time-temperature-humidity relationships. Kettle-cooked sauces or dairy bases may need CCP or preventive control monitoring tied to final cooling and filling conditions. Across all cases, data integrity matters. Processors often underestimate the documentation side of a cooker purchase. Thermal validation, SOPs, calibration, alarm handling, operator training, and commissioning records are all part of a defensible compliance position. Organizations with experience across FDA, USDA, SQF, and BRC environments can reduce project risk by connecting engineering decisions to audit realities. Complex projects also benefit from firms that can act as owner-side advocates, manage contractors, and coordinate local trades while protecting schedule and compliance goals; practical examples can be seen through selected food and beverage project case studies. Future policy direction into 2026 points toward stronger digital traceability, more formal verification of preventive controls, energy reporting in some jurisdictions, and continued emphasis on sanitary design and data-backed validation. This comparison chart highlights a common U.S. procurement reality: the “best” cooker is the one whose strengths align with plant economics, product mix, and validation burden. What is the best industrial cooker for sauces?For most sauces, gravies, and fillings, a steam-jacketed kettle or scraped-surface system is the best starting point. The final choice depends on viscosity, particulates, batch size, and whether the line is batch or continuous. When do I need a retort instead of a kettle?You need a retort when the food is already sealed in a container and requires post-package pasteurization or sterilization, especially for shelf-stable cans, trays, and pouches. A kettle cooks bulk product before filling; a retort thermally processes packaged product. Is steam always the lowest-cost option?Not always. Steam is often cost-effective in large U.S. plants with an existing boiler system, but gas, electric, or hybrid options may be better depending on local rates, emissions strategy, and utility infrastructure. Should I choose batch or continuous cooking?Choose batch for flexibility, smaller SKU runs, and frequent changeovers. Choose continuous for high-volume output, lower labor per pound, and tighter production consistency. Many facilities use both. How important is 316L stainless steel?It is important when products are salty, acidic, chloride-rich, or cleaned with aggressive chemistry. For many standard food applications, 304 is sufficient and more economical. Can I integrate cooking with chilling and freezing in one project?Yes, and that is often the smartest approach. Cooking, cooling, glycol, refrigeration, CIP, and controls should be designed as one process system to avoid bottlenecks and quality loss. What should U.S. buyers ask suppliers before purchasing?Ask for thermal performance data, validation support, utility loads, sanitation design details, controls scope, spare parts strategy, installation requirements, and references in your specific product category. How long does a cooker project usually take?Smaller vessel upgrades may take a few months. Integrated line projects involving utilities, controls, structural work, and commissioning can take much longer, especially if permits, refrigeration, or major building modifications are involved. What trends will matter most in 2026?Expect stronger demand for automation, recipe control, digital validation records, energy recovery, hybrid utility systems, hygienic design, and sustainability-driven capital planning. Who should manage a complex cooking system upgrade?The best outcomes usually come from a partner that can combine technological, manufacturing, and service capabilities. In practical terms, that means process engineering, utility design, automation, equipment fabrication, installation management, and commissioning under one coordinated strategy. For U.S. manufacturers scaling production or modernizing legacy plants, Disruptive Process Solutions supports this type of end-to-end execution across North America through process design, capital planning, equipment integration, installation oversight, and project management. For manufacturers in the United States, industrial food cooker selection should be treated as a profit-impacting process decision, not merely an equipment purchase. The most effective projects connect cooker type, heating method, throughput, thermal control, material choice, energy source, cooling integration, and compliance strategy into one business case. That is especially true in today’s market, where labor efficiency, energy performance, food safety documentation, and speed to scale all influence return on capital. A disciplined engineering approach can turn a cooking step from a bottleneck into a competitive advantage. -
Sandwich Production Facility Design: Assembly, Packaging, and Cold Chain
Designing a ready-to-eat sandwich production facility in the United States requires more than placing prep tables beside a packaging line. Successful plants combine ingredient preparation, portion-controlled assembly, hygienic zoning, packaging technology, refrigeration, food safety, labor efficiency, and dispatch planning into one coordinated system. For chilled sandwiches sold through retail, foodservice, convenience stores, airports, hospitals, universities, and vending channels, the facility must protect product quality from raw ingredient receipt through refrigerated distribution. In practice, that means carefully engineered flows for bread, proteins, produce, sauces, allergens, operators, waste, totes, packaging materials, and finished goods. The U.S. market continues to reward manufacturers that can produce consistent, attractive, high-throughput sandwiches with reliable shelf life. Growth is particularly strong in metro corridors such as New York–New Jersey, Chicago, Dallas–Fort Worth, Atlanta, Los Angeles, Seattle, and South Florida, where convenience retail, corporate foodservice, airport catering, and institutional feeding drive daily demand. Ports and cold chain hubs like Savannah, Los Angeles/Long Beach, Newark, and Houston also matter because proteins, packaging materials, and specialty ingredients often move through these logistics nodes before entering production networks. This guide explains how to plan a sandwich production plant for the U.S. market, including line layout, automation, modified atmosphere packaging, cold storage, sanitation, visual inspection, and unidirectional traffic. It also covers buying considerations, major end-use sectors, practical equipment decisions, and how an engineering partner can reduce capital risk while improving long-term profitability. A well-designed ready-to-eat sandwich facility in the United States should separate raw and high-care areas, use a unidirectional flow from ingredient receiving to refrigerated dispatch, support precise ingredient portioning, integrate packaging with cold chain control, and be built for aggressive sanitation and environmental monitoring to minimize Listeria risk. The most effective plants balance throughput, shelf life, labor flexibility, and regulatory compliance under FDA, USDA, SQF, or BRC expectations depending on product mix and customer requirements. For most projects, the best design approach includes: In the U.S. market, facilities producing club sandwiches, wedges, paninis, wraps, subs, breakfast sandwiches, open-faced products, and premium deli-style offerings should be designed for menu variation without compromising food safety. That is especially important for operators supplying national convenience chains, contract foodservice providers, airline caterers, hospitals, and regional grocery private label programs. The table above summarizes the foundational requirements. These are not optional enhancements; they are the core design criteria that determine whether a plant can operate safely and profitably at scale. Ingredient preparation is where sandwich plants either gain efficiency or inherit chronic bottlenecks. Bread may seem simple, but proteins, sliced cheeses, leafy greens, tomato, sauces, pickles, bacon, eggs, and specialty spreads all behave differently in a chilled environment. Layout must consider receiving frequency, shelf life, cut size consistency, and the handling sensitivity of each component. In a typical U.S. ready-to-eat facility, incoming materials are staged by category: ambient dry goods, refrigerated proteins, refrigerated dairy, produce, and packaging materials. From there, components move into prep rooms based on process need. Produce washing and slicing should remain isolated from high-care finished assembly wherever practical. Post-lethality proteins and ready-to-use ingredients should enter the cleanest controlled zones possible, especially for sandwiches distributed to retailers with strict food safety audit standards. Assembly line design depends on SKU count and daily output. A low-SKU regional operator may use straight-line conveyors with manual placement stations. A higher-volume national supplier may use multiple parallel lanes with dedicated component feeding and synchronized portioning. U-shaped layouts can improve labor access in compact footprints, while linear layouts often simplify sanitation and expansion planning. Common product types that influence layout in the United States include: Good layout also anticipates labor reality. Plants in markets such as Southern California, North Carolina, Texas, and Illinois often need flexible stations that can switch between manual and assisted assembly depending on labor availability, wage pressure, and order mix. This layout table shows how every room supports the next. The aim is simple: ingredient prep should feed assembly without backtracking, queue build-up, or temperature drift. Automation in sandwich manufacturing is not all-or-nothing. The best U.S. facilities often combine manual craftsmanship at sensitive placement points with automated systems for repetitive, high-variance, or high-cost steps. Portion control is the first place most producers see a strong return, especially for meats, cheese, egg patties, sauces, and sliced vegetables. Automated and semi-automated options include slice counters, checkweigh-guided protein loading, servo depositors for condiments, robotic pick-and-place for packaged components, and vision-guided reject systems. For plants producing thousands of units per hour, even a 2-gram average overfill on protein or sauce can create major annual cost leakage. Portion control systems therefore improve both food safety documentation and gross margin. Automation strategy should reflect product architecture. Soft breads, delicate croissants, or premium visible-fill sandwiches may require gentle handling and lower conveyor speeds. Wrap lines may benefit from specialized rolling and folding equipment. Breakfast products may integrate heating, cooling, and rapid assembly into more complex sequences. In facilities serving both private label retail and foodservice channels, changeover speed matters as much as nameplate throughput. By 2026, U.S. manufacturers are expected to adopt more vision-assisted assembly verification, digital recipe management, and data capture tied to labor, yield, and downtime. Plants that can connect PLC controls, checkweighers, and traceability software will be better positioned for retailer scorecards and continuous improvement. The chart above reflects a realistic investment trend: rising demand for convenient chilled foods is driving steady capital spending on sandwich assembly and packaging capacity in the United States. The table highlights a practical buying principle: invest first where labor variability and giveaway are highest. For many U.S. producers, that means portioning and inspection before full robotic assembly. Modified atmosphere packaging, or MAP, can extend shelf life and preserve fresh appearance when it is aligned with recipe, moisture migration, bread performance, and refrigeration discipline. It is not a substitute for sanitation or temperature control, but it is a valuable packaging strategy for chilled sandwiches distributed across wider U.S. regions. Retail sandwich programs shipping from the Midwest into the Northeast, or from Texas into surrounding states, often need code life that supports production scheduling, retailer receiving windows, and store-level selling days. MAP helps by replacing package oxygen with a controlled gas mix, commonly using carbon dioxide and nitrogen depending on product characteristics. The correct mix must be validated against bread texture, produce respiration, sauce behavior, and protein quality. Package format also matters. Wedge packs, flow-wrap, thermoformed trays, and lidded packs each create different sealing and merchandising conditions. Seal quality must be stable across production speeds and environmental humidity. In U.S. retail, shelf appeal is not secondary; consumers expect visible ingredients, clean labels, and intact pack geometry. Sustainability is shaping packaging decisions as well. By 2026, more buyers are expected to request recyclable or downgauged materials, while still demanding shelf life and leak resistance. This tension means packaging selection should be treated as a plant-design decision, not a late procurement task. This area chart shows the likely trend shift toward higher-performance packaging in the U.S. chilled sandwich segment, driven by longer distribution lanes, retail quality expectations, and waste reduction goals. The packaging choice should be matched to route-to-market. A local same-day commissary can package differently from a multi-state retail program serving Chicago, Philadelphia, Charlotte, and Tampa from one hub. Cold chain design begins long before finished pallets enter a cooler. The assembly room itself, ingredient staging points, in-process dwell times, and dock operations all determine how well a sandwich facility protects shelf life. In the United States, where products may move from production sites to cross-docks, distribution centers, retail backrooms, and store chillers, the plant must assume some downstream stress and build resilience into the product and process. Critical design features include pre-chilled ingredients, refrigerated staging carts, temperature-controlled assembly rooms, short transfer distance to packaging, blast-assisted pull-down where justified, finished goods cold rooms, and dock vestibules or refrigerated staging for dispatch. Facilities in hot, humid regions such as Florida, Texas, and the Southeast should pay particular attention to dock exposure and condensation management. Refrigeration systems may use centralized ammonia, packaged systems, glycol loops, or distributed refrigerant strategies depending on plant size, capital goals, utility philosophy, and local service support. Controls should integrate room temperature, product dwell time, alarm notification, and trend logging. Energy efficiency is increasingly important, but it should not compromise food safety performance. For manufacturers serving urban areas like Boston, Washington, D.C., San Francisco, and Seattle, route density may allow frequent deliveries and shorter storage windows. For nationwide programs or co-packers shipping longer distances, cold chain buffering becomes more important. The bar chart above illustrates where demand is strongest. Convenience and grocery channels continue to be major drivers, shaping the need for robust chilled distribution and dependable code life. This cold chain table shows that refrigeration is not only a utilities topic. It is a production design issue tied directly to yield, shelf life, and customer acceptance. Because sandwiches are assembled after ingredients are cooked or otherwise prepared, post-process contamination is one of the biggest hazards in the category. That is why hygienic design and Listeria prevention must be built into the facility from the start. In the U.S., customers often expect environmental monitoring programs, sanitation zoning, and documented controls that go beyond minimum code compliance. Floors should drain well, wall penetrations should be minimized and sealed, overhead structures should resist condensation, and equipment should avoid hollow members, dead legs, and inaccessible harborage points. Conveyor supports, slicer frames, guard mounts, and table undersides deserve particular attention. If a sanitation team cannot easily reach it, the design should be questioned. Personnel flow is equally important. Gowning transitions, handwashing points, boot sanitation, tool control, and forklift segregation all reduce cross-traffic risk. Waste and dirty utensil return should never move against the clean product path. Water use must also be disciplined; excessive moisture in high-care rooms can increase environmental risk instead of reducing it. By 2026, more sandwich manufacturers are expected to expand use of hygienic design audits, ATP verification linked to digital records, and environmental mapping software. Buyers in grocery and institutional channels are increasingly asking for evidence that sanitation is engineered into the plant, not merely handled by SOPs. When planning these systems, manufacturers often benefit from working with specialists who understand processing, utilities, controls, and compliance together. Firms such as Disruptive Process Solutions support integrated project planning so sanitary design decisions align with capital budgets, scheduling, and production goals. The practical takeaway is that Listeria control is a facility design challenge as much as a sanitation challenge. Plants that treat it that way are more resilient. Quality control in pre-packaged sandwich operations must cover food safety, package integrity, and visual appeal. Unlike many processed foods, sandwiches are judged instantly by appearance. Uneven fillings, displaced bread, smeared sauce, collapsed structure, poor cut alignment, and label wrinkles all affect saleability. Inspection systems should be layered. Incoming checks verify ingredient condition, lot traceability, and temperature. In-process checks confirm portion weights, component presence, and assembly order. Post-packaging checks focus on seal quality, label accuracy, use-by coding, and finished weight. Retail-facing products often benefit from machine vision that detects missing bacon strips, absent cheese slices, or poor presentation in clear packs. Quality targets should be built around channel needs. Airport and travel plaza programs emphasize appearance and secure packaging under heavy handling. Hospital and university contracts may focus more on allergen accuracy, date code control, and nutritional consistency. Convenience chains often expect high-speed production with very low visual defect rates. For producers evaluating equipment suppliers, it helps to compare the overall system rather than one machine at a time. The right line balances assembly, package seal performance, inspection, and reject handling. This comparison chart presents the type of criteria U.S. manufacturers often use when selecting sandwich line partners. Service support and sanitary design are frequently as important as raw throughput. The best quality programs convert these checks into actionable data. Trend analysis can reveal whether defects originate in ingredient prep, assembly timing, packaging setup, or operator training. Unidirectional flow is one of the clearest indicators of a well-planned ready-to-eat facility. The concept is straightforward: materials, people, and waste should move forward through the process without crossing back into cleaner or later-stage zones. In sandwich manufacturing, this principle helps reduce contamination risk while simplifying operations. A strong U.S. facility layout usually progresses through receiving, chilled storage, ingredient prep, controlled assembly, packaging, finished goods refrigeration, and dispatch. Support functions such as maintenance shops, chemical storage, employee welfare areas, and waste rooms should be positioned to avoid disrupting the clean process path. Forklift traffic should be isolated from high-care foot traffic wherever possible. This matters especially for plants retrofitting older buildings in dense industrial markets such as New Jersey, greater Chicago, or Los Angeles County, where footprint constraints can tempt teams into compromised traffic patterns. Sometimes the most cost-effective decision is not to force a complex RTE sandwich operation into a poorly suited shell. A careful feasibility study can save major downstream operating costs. Manufacturers planning expansion should also reserve room for additional lines, cooler growth, packaging changes, and future automation. A plant that works at launch but cannot scale by year three may become a costly bottleneck. Project teams seeking this kind of long-range planning often engage specialists with process, utilities, and construction management experience. Through its design-build-manage approach, DPS engineering and project services helps manufacturers evaluate layouts, phase capital correctly, and align plant design with production economics. This table explains why flow planning is so powerful: it makes food safety simpler while improving labor efficiency and line uptime. For companies comparing local suppliers or project partners in the United States, useful buying criteria include high-care design experience, refrigeration integration knowledge, packaging line compatibility, controls expertise, and the ability to manage permitting and construction across jurisdictions. Manufacturers near Raleigh, Charlotte, Dallas, Fresno, Milwaukee, or Philadelphia may find different contractor ecosystems, so national coordination can be valuable on multi-state programs. When reviewing candidates, ask for examples of chilled food facilities, utility coordination, and startup support. Also verify whether the partner can assist with custom equipment integration through resources such as process equipment solutions and whether they can provide references or examples from prior project work through project case studies. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a practical focus on profitable capital execution. Rather than operating only as a traditional contractor, the company approaches projects as an engineering-led partner that aligns facility decisions with operational and financial outcomes. On the technology side, DPS brings multidisciplinary engineering capabilities across process, mechanical, plumbing, electrical, structural, and controls. That includes automation, PLC programming, SCADA integration, utility coordination, and system design for refrigeration, CIP, water, compressed air, steam, and clean processing environments. For sandwich and other ready-to-eat food operations, that kind of cross-functional capability is especially valuable because assembly, sanitation, packaging, HVAC, and cold chain performance must work as one system. On the manufacturing side, DPS has broad experience with food processing systems including mixing, cooking, slicing, portioning, protein handling, dairy, aseptic, and prepared foods applications. The company also manufactures selected branded process equipment, giving clients another option when custom tanks, CIP systems, tumblers, or processing vessels need to fit a larger integrated project. That background helps when sandwich facilities must connect ingredient prep, utility infrastructure, and packaging equipment into one scalable platform. On the service side, DPS provides capital planning, feasibility studies, owner’s representation, project and program management, general contracting functions where licensed, installation oversight, and turnkey integration. Its design-build-manage model is intended to reduce fragmentation between engineering, procurement, construction, and startup. Manufacturers that want a partner for long-range facility planning can learn more about the company and how it supports food and beverage expansion programs throughout North America. For sandwich producers, that means help not only with drawings and equipment lists, but with the bigger questions: how to size a line, where to phase investment, how to prevent utility bottlenecks, how to preserve hygiene, and how to build a plant that remains profitable as product mix changes in 2026 and beyond. What is the most important design principle for a ready-to-eat sandwich plant?The most important principle is controlled unidirectional flow with clear separation between raw, support, and high-care ready-to-eat zones. This reduces contamination risk and improves production discipline. Should a sandwich facility in the United States use full automation?Not always. Many successful plants use a hybrid model with manual placement for delicate ingredients and automated systems for portioning, conveying, weighing, and inspection. The right choice depends on SKU complexity, labor conditions, and throughput targets. How much does packaging influence shelf life?Packaging has a major effect, especially when combined with disciplined refrigeration and hygienic production. Seal quality, barrier properties, gas mix, and pack geometry all influence performance, but none can compensate for poor sanitation or temperature abuse. Is modified atmosphere packaging necessary for every sandwich line?No. Local commissaries with short distribution windows may not need MAP. It becomes more attractive when products travel across larger U.S. regions, when retailer shelf-life expectations are longer, or when waste reduction is a strategic priority. What industries buy pre-packaged sandwiches in the United States?Key sectors include retail grocery, convenience stores, airport concessions, travel centers, hospitals, universities, corporate dining, vending, military feeding, and contract foodservice. Demand patterns vary by region, with strong convenience growth in major commuting corridors and airport-heavy metros. How should a company choose a facility design partner?Look for experience in chilled ready-to-eat foods, hygienic design, refrigeration integration, packaging line coordination, automation, compliance, and project execution. A partner should understand both process performance and capital efficiency, not just construction scope. What future trends should be considered for 2026?Expect increased use of machine vision, digital traceability, energy-aware refrigeration controls, sustainable packaging formats, stricter retailer verification standards, and more emphasis on environmental monitoring in high-care food plants. Policy and customer pressure around waste reduction and packaging recyclability will also influence design choices. Can an older building be converted into a sandwich plant?Yes, but only if the building supports high-care zoning, adequate drainage, airflow control, refrigeration, employee hygiene transitions, and clean traffic separation. In some U.S. industrial markets, retrofit can work well; in others, new build or major shell modification is the smarter long-term choice. In summary, the strongest sandwich production facilities in the United States are designed as integrated ready-to-eat systems. Ingredient prep, assembly, packaging, sanitation, quality checks, refrigeration, and dispatch must be planned together. When those elements are aligned, manufacturers gain better shelf life, stronger food safety performance, lower labor waste, and a more scalable business for the years ahead. -
Stainless Steel Process Tanks
Across the United States, stainless steel process tanks are used for blending, holding, heating, cooling, fermenting, reacting, batching, and CIP circulation in food, beverage, dairy, protein, and specialty sanitary manufacturing. The best tank is not simply the one with the lowest purchase price. It is the vessel that matches product chemistry, required cleanability, pressure or vacuum conditions, heat transfer needs, plant utilities, structural loads, automation requirements, and long-term throughput goals. For many sanitary applications, 304 stainless is acceptable, 316L is preferred where chlorides, acids, brines, or aggressive cleaning chemicals are present, and 2205 duplex can be justified when corrosion resistance and strength must both increase. In the United States market, buyers also need to evaluate whether the tank is atmospheric or pressure-rated, whether it falls under ASME requirements, and how field delivery and rigging will affect startup timing. At a market level, demand for process tanks remains strong in major manufacturing corridors such as the Carolinas, Texas, California, Wisconsin, Illinois, Pennsylvania, and the Pacific Northwest. Growth is being supported by expansion in dairy beverages, ready-to-drink products, sauces, protein processing, fermentation, and co-packing. Port access through Long Beach, Houston, Savannah, Newark, and Seattle also influences lead times, especially when projects combine domestic fabrication with specialty components sourced globally. Companies planning a new line, brownfield upgrade, or utility optimization project should align tank selection with plant expansion strategy rather than viewing the vessel as a standalone item. That is where a systems-focused engineering partner matters. Disruptive Process Solutions supports manufacturers across North America with a practical design-build-manage approach that ties equipment decisions to production economics, sanitation, controls, utilities, and installation sequencing. Instead of stopping at vessel supply, the team evaluates how the tank integrates into the larger process, from pump sizing and CIP return velocities to automation logic, structural support, and startup performance. If you need a quick recommendation, start here: For U.S. plants, the buying decision usually comes down to six questions: what is in the tank, how clean must it be, what pressure and temperature will it see, how will it be heated or cooled, how will it be installed in the building, and how will it fit your expansion plan over the next three to five years. The table above shows why tank procurement should be tied to process design and facility planning. A vessel bought in isolation often creates downstream cost in utilities, controls, sanitation, or structural work. Material selection is one of the most important decisions in process tank design. In U.S. food and beverage facilities, 304 and 316L dominate because they balance sanitary performance, weldability, availability, and cost. However, not all products behave the same. Tomato-based sauces, saline marinades, cultured dairy, cleaning acids, chlorinated washdown environments, and high-temperature CIP can quickly expose the limits of an underspecified alloy. 304 stainless is widely used for potable water tanks, ingredient tanks, blending tanks, syrup tanks with mild chemistry, dry ingredient hoppers, and utility-related process vessels. It is economical and readily available. But in chloride-rich or low-pH applications, it may show pitting or crevice corrosion over time, especially at welds, dead legs, or under deposits. 316L adds molybdenum, improving pitting resistance. It is often the default sanitary choice for dairies, beverage plants, flavor systems, brines, and many CIP-exposed vessels. The low-carbon “L” designation also supports better weld corrosion performance after fabrication. 2205 duplex is less common in routine food plant vessels but can be valuable where both higher strength and greater corrosion resistance are needed. In some coastal facilities near the Gulf Coast or Southern California, or in aggressive protein and brine processing environments, duplex can reduce long-term risk. It may also allow thinner wall sections in some engineered cases, though fabrication complexity and cost must be considered. This comparison helps buyers avoid the mistake of treating every stainless vessel as interchangeable. Alloy selection should always be reviewed against product chemistry, cleaning chemicals, temperature, weld detail, and expected equipment life. For plants with mixed product portfolios, one useful strategy is to standardize 316L on critical sanitary process vessels and reserve 304 for non-critical utility or storage functions. That can simplify spare parts, reduce corrosion risk, and improve resale value. A qualified engineering review through integrated process and project services can identify where premium alloy spend adds value and where it does not. Many buyers use the phrase “process tank” broadly, but from an engineering and compliance standpoint, the distinction between atmospheric and pressure-rated service is critical. An atmospheric tank is typically vented and designed for minimal internal pressure, often only enough for filling, draining, and safe operation under open or lightly vented conditions. A pressure-rated tank, by contrast, is engineered for defined internal or external pressure and may require ASME Section VIII compliance depending on design pressure, application, customer specification, and local inspection requirements. Common examples of atmospheric tanks include ingredient blend tanks, raw product holding tanks, open-top mix vessels, and CIP supply tanks. Pressure-rated examples include carbonation tanks, vacuum receivers, heated reactors with controlled pressure, and certain aseptic or sterile process vessels. In the United States, the code path can also affect insurance, owner standards, and resale. A tank that technically could have been built as atmospheric may still be specified to ASME if the owner wants a higher standard of documentation, nameplate traceability, material records, and fabrication control. The main lesson from the table is that “pressure-rated” is not a minor upgrade. It changes shell design, nozzle reinforcement, fabrication records, testing, and often project cost and lead time. For brownfield projects in older plants around Chicago, Milwaukee, Fresno, or Atlanta, code review is especially important because legacy vessels may not align with current operating expectations. A process may have changed over time, creating pressure or vacuum events the original tank was never designed to withstand. That is why tank replacement should be paired with a broader process hazard and operating review. A tank shell alone rarely defines process performance. Internals determine whether the vessel actually mixes, suspends, heats, drains, vents, and controls product the way production expects. Agitator type should be selected based on viscosity, shear sensitivity, solids loading, batch time, and target turnover. High-shear applications may need rotor-stator systems, while low-viscosity beverage blending often works with pitched-blade turbines or axial-flow impellers. Baffles prevent vortexing and improve mixing efficiency in cylindrical vertical tanks. Dip tubes can support bottom-entry fill, CO2 purge, flavor dosing, or CIP return strategy. Level instrumentation may include sight glasses, load cells, hydrostatic transmitters, guided wave radar, or sanitary point-level probes depending on accuracy requirements and foam behavior. Plants that process sauces, dairy bases, cultured products, and marinades often underestimate the impact of internal geometry on cleanability. A poorly placed agitator seal, oversized dip tube, or unnecessary dead leg can extend CIP time and leave residual product behind. This table shows that internals are not accessories; they are process-critical components. The wrong mixer or level device can undermine throughput, quality, or sanitation even when the vessel itself is well built. DPS brings strong technological capabilities to these decisions. Its engineering scope spans process, structural, mechanical, plumbing, electrical, and controls disciplines, including PLC programming and SCADA integration. That matters because level instrumentation, agitator control, recipe sequencing, and CIP verification all benefit from integrated controls logic rather than separate vendor assumptions. On complex projects, this systems view often prevents the kind of bottleneck that only becomes visible once production starts. Heating and cooling performance drives batch time, energy use, and product quality. U.S. manufacturers generally choose among dimple jackets, limpet coils, half-pipe style external circuits, or internal coils depending on pressure, utility medium, heat transfer rate, cleanability, and fabrication budget. Dimple jackets are popular for sanitary process tanks because they provide efficient heat transfer over a broad surface area and are relatively compact. They work well with glycol, chilled water, or hot water systems in beverage and dairy plants. Limpet or half-pipe coils are often selected where higher pressure or more robust external heating circuits are needed. Internal heating coils can provide direct thermal transfer but may complicate cleaning and reduce usable volume. In breweries, kombucha operations, dairy beverage plants, and sauce kitchens, the thermal utility selected upstream often determines the most practical jacket style. A plant using central glycol from a packaged system in Charlotte or Denver may optimize one way; a protein operation with plant steam in Omaha or Kansas City may optimize another. The thermal option should be chosen only after reviewing utility availability, cleaning requirements, and batch timing. A low-cost jacket that cannot meet cooling targets can become the most expensive choice in operation. The market growth trend above reflects continued U.S. investment in sanitary process equipment, particularly in food, beverage, dairy, and value-added protein applications heading into 2026. Surface finish affects more than appearance. It influences cleanability, microbial risk, residue release, corrosion behavior, and how customers or auditors perceive the installation. Mill finish may be acceptable on non-product-contact exteriors or utility vessels. Brushed finishes improve appearance and are common for visible exterior surfaces. Electropolishing is often selected for high-purity, aseptic, biotech-adjacent, or difficult-to-clean sanitary applications where smoother passive surfaces provide performance benefits. Inside food and beverage plants, the required finish should be tied to product behavior. Sugar syrups, dairy proteins, sticky sauces, and botanical extracts can all behave differently during cleaning. A surface that is acceptable for potable water may be inadequate for a high-value, allergen-sensitive formulation process. The finish decision should balance hygiene, cost, and process risk. In many U.S. plants, the optimal specification is not the highest polish everywhere, but the right finish in the right zone, supported by good weld execution and passivation. Tank sizing is one of the most common areas where manufacturers either overspend or create operational constraints. Nominal tank volume is not the same as working volume. A 5,000-gallon tank may only support a much smaller effective batch if foam, agitation, gas breakout, thermal expansion, CIP spray patterns, or product surge require extra headspace. For low-viscosity products, many designers target working fill ratios around 70 to 85 percent depending on agitation intensity and foam behavior. Fermentation, carbonation, and high-foaming products may require even more headspace. Viscous products may demand larger outlet geometry and lower aspect ratios to ensure complete drainability and heat transfer performance. When planning a tank farm in the United States, layout and logistics matter too. Ceiling height, mezzanine access, forklift travel, truck delivery limits, and future line tie-ins all influence practical vessel size. A larger tank may reduce batch frequency, but if it requires major building modification in Phoenix, Nashville, or Newark, the total installed cost can climb quickly. The sizing guide above should be treated as a planning tool, not a final engineering rule. Actual fill ratios depend on product, process controls, agitation, and sanitation strategy. DPS also brings manufacturing capabilities that matter in this range. The company designs and supplies its own process equipment line, including storage and process tanks up to 12,000 gallons, along with CIP systems and other custom vessels. That in-house manufacturing perspective helps bridge the gap between what looks efficient on paper and what can be fabricated, delivered, and integrated effectively in the field. More equipment details are available through the company’s process equipment portfolio. The bar chart highlights where current demand is strongest. RTD beverages, protein, and dairy continue to lead tank investment as manufacturers expand throughput and product diversity. Structural design is often underappreciated until installation day. Tank supports must carry static product weight, dynamic loads from mixing, thermal expansion, nozzle piping loads, and, in some regions, wind and seismic forces. Leg-supported tanks are common for smaller sanitary vessels, while skirt-supported or saddle-supported designs may be preferred for other geometries and capacities. Lifting lugs are not decorative details. They must be engineered for actual rigging loads, center of gravity, and lift orientation. Improperly planned lifting arrangements can delay installation or damage a new vessel before it ever runs product. Seismic design is especially relevant in California, Washington, Oregon, Utah, and parts of the Intermountain West. Even outside those zones, local building codes and owner standards may require anchorage calculations. Large tanks in active production plants also need protection against vibration interaction, accidental forklift impact, and piping stress introduced after startup. For sanitary systems, support design should not create cleanability issues or inaccessible floor zones. This table illustrates why structural review is inseparable from vessel specification. A tank that is perfectly suited for the process can still be the wrong choice if the support design does not fit the site. Tank projects often succeed or fail in the final ten percent of work. Delivery, unloading, setting, utility tie-in, automation checkout, and startup sequencing all affect schedule and cost. Before fabrication is complete, the project team should verify truck route, bridge clearances, permit needs, building access, roof openings if applicable, crane radius, floor capacity, and final set elevation. For large vessels moving into dense industrial corridors such as Los Angeles, Houston, Philadelphia, or the New York-New Jersey region, delivery windows and onsite traffic restrictions can change the rigging plan. For rural protein plants in the Midwest or dairy plants in upstate New York, weather, yard conditions, and winter access may be the main variables. Best practice is to create a full installation package that includes rigging drawings, center-of-gravity information, anchor layout, nozzle orientation, utility connection points, controls IO list, FAT/SAT expectations, and startup cleaning protocol. That reduces field improvisation and shortens commissioning. DPS is strongest when acting not just as an equipment source but as a service partner. Its service capabilities cover process engineering, capital planning, owner’s representation, project and program management, general contracting where licensed, equipment integration, installation oversight, and commissioning support. That full-scope model is particularly valuable when a process tank is part of a wider expansion involving utilities, controls, CIP, and line balance. Examples of project execution and field coordination can be seen in selected project case studies. The area chart reflects a major 2026 trend: process tanks are increasingly specified as intelligent assets, with integrated level sensing, batch control, historian connectivity, and utility performance monitoring. What industries use stainless steel process tanks in the United States?Food and beverage manufacturing leads demand, including dairy, sauces, dressings, brewing, spirits, wine, kombucha, RTD products, carbonated beverages, juices, protein processing, and aseptic systems. Pharmaceutical-adjacent and specialty ingredient plants also use similar sanitary vessels. Is 316L always better than 304?Not always. 316L offers better corrosion resistance and is often worth the premium in sanitary process applications, but 304 can still be the right value choice for mild products and non-aggressive cleaning environments. When is ASME code required?Usually when the tank is pressure-rated, vacuum-sensitive beyond simple vented service, or otherwise specified by the owner, insurer, or authority having jurisdiction. The exact requirement should be reviewed during design. How much headspace should I leave?A common planning range is 15 to 30 percent, but actual headspace depends on foaming, agitation, thermal expansion, gas release, and process control strategy. What finish should I specify for sanitary product contact?That depends on your product and cleaning standard. Many sanitary vessels use mechanically polished interiors with controlled Ra values, while electropolish is reserved for higher-purity or more demanding applications. What are the most common internal components?Agitators, baffles, spray devices, dip tubes, sample valves, level instrumentation, temperature probes, manways, and vent/filter assemblies are the most common. How should I compare suppliers?Look beyond price. Compare alloy traceability, weld quality, code knowledge, thermal design, finish specification, delivery capability, controls integration, FAT/SAT support, and installation planning. The comparison chart shows why buyers increasingly favor integrated project partners over commodity-only vessel sourcing, especially when schedule, utilities, automation, and sanitation are interconnected. Who are the right local suppliers?In the United States, buyers typically evaluate regional fabricators, national OEMs, and integrated engineering-installation partners. The best choice depends on whether your need is a simple replacement tank, a custom sanitary process vessel, or a full line expansion tied to utilities, controls, and startup. What trends will shape process tank buying in 2026?Three trends stand out. First, higher sustainability expectations will push buyers toward better insulation, smarter utility use, and faster CIP cycles that reduce water and chemical consumption. Second, policy and compliance pressure around food safety, traceability, and energy efficiency will drive more documented design decisions and digital monitoring. Third, automation will continue moving from optional to expected, with tanks increasingly connected to SCADA, batch systems, predictive maintenance tools, and plantwide energy dashboards. For manufacturers planning 2026 capital projects, the smartest path is to define the tank as part of a broader production asset strategy. That means aligning metallurgy, thermal performance, controls, structural support, and serviceability with your long-term commercial model. In practice, companies that take this approach tend to reduce rework, shorten startup time, and generate better return on capital than those purchasing vessels on quoted price alone. Whether you are building a new beverage facility in Texas, upgrading a dairy line in Wisconsin, expanding sauce capacity in North Carolina, or modernizing a protein plant in the Midwest, a well-engineered stainless steel process tank can become a durable production asset rather than a recurring bottleneck. The key is matching the vessel to the full process ecosystem: product, utilities, controls, structure, compliance, and growth. -
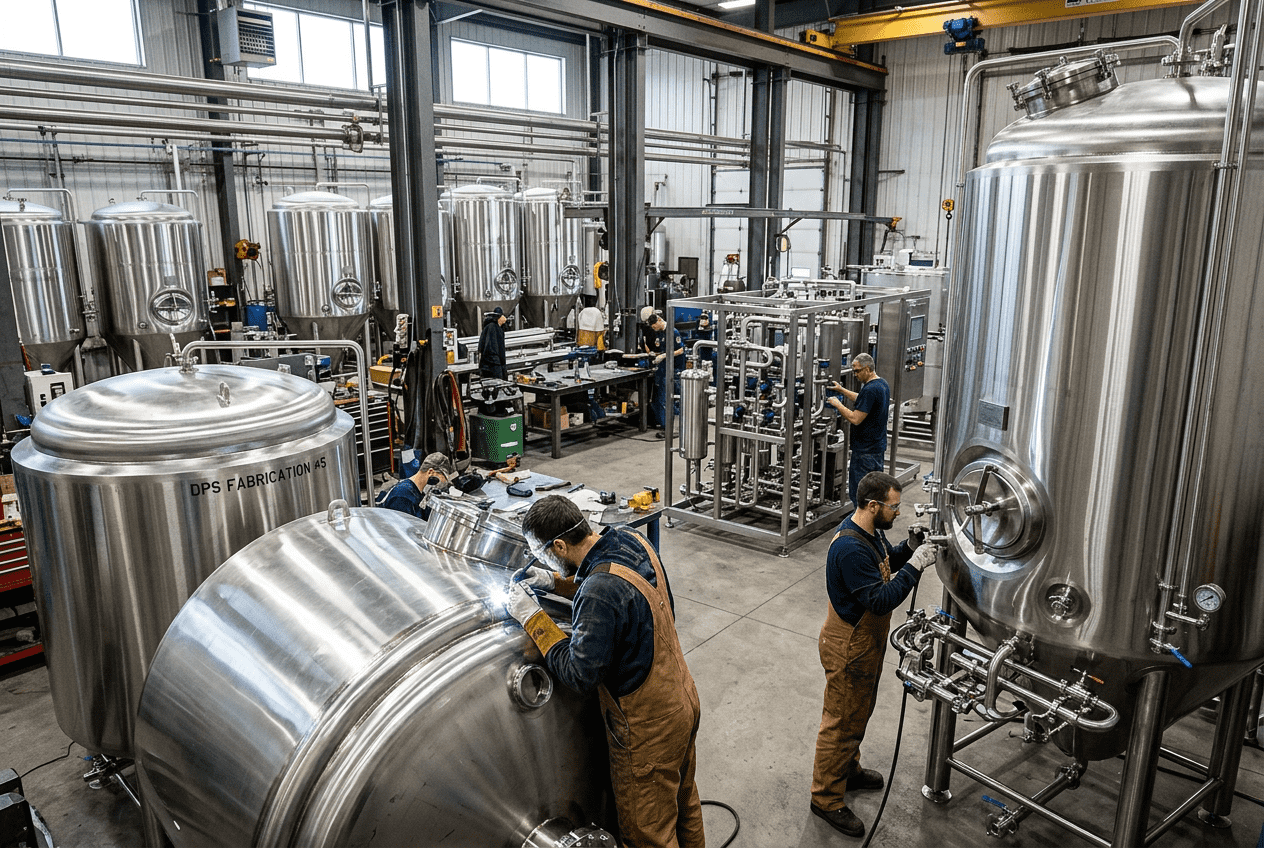
Produce Wash Line Design in 2026: Advanced Sanitation Systems
Designing a produce wash line in 2026 is no longer just about rinsing soil off vegetables. In the United States, processors are being pushed by retailer standards, FSMA expectations, labor constraints, water costs, and customer demand for cleaner, longer-lasting fresh products. A modern line must combine the right wash technology, validated sanitation chemistry, controlled water reuse, gentle handling, reliable dewatering, and integration with grading, cutting, and packaging. The best systems are built around the actual product mix: root vegetables, leafy greens, herbs, cut vegetables, and mixed produce all behave differently on the line. The quickest answer is this: for most U.S. produce processors in 2026, the best wash line design uses air bubble washing for delicate leafy products, brush roller washing for root vegetables, integrated ozone or peracetic acid sanitation for microbial control, two-stage dewatering with a vibratory screen and air knife, sanitary conveyors with variable speed control, and a recirculated water loop supported by filtration and monitored chemistry. The line should also connect cleanly to sizing, cutting, weighing, and packaging while supporting HACCP verification, daily sanitation, and documented preventive controls. For a processor shipping into major markets such as Chicago, Los Angeles, Dallas, Atlanta, Philadelphia, Seattle, and New York, the line must do more than “work.” It must protect shelf life, reduce bruising, keep water usage under control, and maintain throughput during seasonal volume spikes. Processors receiving product through California’s Central Valley, Yuma, Salinas, South Texas, Florida, or warehouse hubs near the Port of Savannah and Port of Long Beach often need flexible wash systems that can handle changing field conditions throughout the year. In practical terms, buying advice for 2026 comes down to five decisions: The U.S. market is moving toward integrated lines that are more automated, easier to clean, and better instrumented. Buyers increasingly ask for conductivity monitoring, ORP tracking, flow balancing, recipe-driven conveyor speeds, and remote diagnostics. That trend is strongest among fresh-cut processors, foodservice suppliers, and multi-site manufacturers serving national retail and club channels. The chart above reflects a realistic market direction: processors are steadily increasing spending on line upgrades, especially when projects support water savings, labor reduction, and food safety verification. This selection table shows why product-first design matters. A line built for potatoes will often damage spring mix, while a delicate greens washer may not remove enough soil from carrots or beets. Wash technology selection should start with product biology, field load, target throughput, and acceptable mechanical force. Air bubble systems are ideal when processors need flotation, gentle agitation, and broad contact between water and product. They are commonly chosen for romaine, spring mix, spinach, kale, herbs, and cut vegetables that bruise easily. Brush roller systems are better when the product arrives with attached soil, rough skin, or surface debris that needs physical scrubbing. Potatoes, carrots, radishes, beets, and some onions fit this category. For U.S. operations supplying supermarkets in Boston, Miami, Houston, Denver, and Minneapolis, line versatility is attractive, but over-flexibility can create compromise. A dual-path line often works better than a single universal washer. One path may use a bubble tank with turbulence control and soft transfer points for greens. A second path may use brush rollers with top sprays, debris removal, and adjustable dwell time for root crops. Key design variables include tank residence time, bubble density, product depth, brush stiffness, spray pressure, make-up water rate, and discharge transfer geometry. In 2026, more processors are requesting servo-adjusted speeds, recipe memory by SKU, and CIP-friendly wash modules to reduce changeover time. A useful buying rule is simple: if your biggest complaint is field grit, choose more physical cleaning; if your biggest complaint is bruising or short shelf life, choose gentler product movement. Where processors handle both categories, a front-end receiving and destoning system can reduce the cleaning burden before product enters the wash section. Application-specific design matters in industries such as fresh-cut salads, retail meal kits, frozen vegetable preparation, institutional foodservice packs, and value-added root vegetable processing. In those sectors, performance is measured not only by visible cleanliness but by cut quality downstream, package seal integrity, and days of shelf life in refrigerated distribution. Pathogen control in produce wash systems is a water-management problem as much as a chemistry problem. In U.S. operations, peracetic acid, often shortened to PAA, remains a leading choice because it is effective across a broad pH range, works in cold water, and aligns well with many produce applications when validated correctly. Ozone also attracts attention because it decomposes without persistent residue and can support lower chemical carryover, but it requires precise engineering, off-gas management, and careful control around worker safety and contact conditions. For most fresh-cut produce facilities, the right question is not “ozone or PAA?” but “where should each technology be used?” PAA is commonly favored in the main wash loop or final antimicrobial stage due to practical dosing and proven processor familiarity. Ozone can be useful in supplemental water treatment, recirculation support, or targeted sanitation zones where the system is designed to maintain effectiveness without creating instability. In 2026, regulators and customers are paying closer attention to validation data, not assumptions. Processors need documented concentration targets, contact time logic, sensor calibration, and corrective action plans. This is especially important for shipments entering large distribution corridors through New Jersey, Southern California, the Midwest, and Southeastern cold-chain hubs. The table highlights that chemistry choice is inseparable from system design. A processor can buy excellent sanitizer and still underperform if the wash tank short-circuits, organic load is too high, or dosing is not linked to changing throughput. The strongest projects define sanitation by zone: incoming dirty wash, intermediate wash, final antimicrobial intervention, and clean water finishing. Future trends for 2026 include tighter automation of dosing skids, better digital logging for HACCP and preventive controls, and stronger sustainability pressure to reuse water safely rather than discharge excessive volumes. Buyers should also consider local wastewater permit conditions and the effect of sanitation chemistry on downstream treatment. This industry demand view shows why sanitation system integration is a top buying priority: leafy greens and fresh-cut segments have the highest sensitivity to wash water control, while meal kits and foodservice packs are also driving investment because of shelf-life and consistency requirements. Dewatering is one of the most underrated parts of produce line performance. Too much residual moisture can dilute seasoning, reduce package seal quality, cause clumping in weighers, create fogging inside bags, and shorten refrigerated shelf life. In 2026, a two-stage dewatering design using a vibratory screen followed by an air knife section is often the best balance between water removal and gentle handling. The first stage, a vibratory screen or shaker conveyor, removes free water efficiently while spreading product into a more consistent bed depth. The second stage, an air knife or controlled blower tunnel, strips surface water before product enters grading, cutting, checkweighing, or packaging. For cut lettuce, baby spinach, shredded vegetables, herbs, and washed root crops, this combination improves downstream stability without excessive dwell time. Design details matter. Air velocity must be strong enough to remove moisture but not so aggressive that it flips leaves, dries edges, or causes weight giveaway. Vibration frequency must support drainage without compacting soft product. The transfer between stages should avoid drop heights and pinch points. Processors often see the biggest hidden return from dewatering in packaging. Multihead weighers run more consistently, baggers seal better, and operators spend less time cleaning up standing water around the pack area. For plants supplying chains in Phoenix, St. Louis, Charlotte, and the Pacific Northwest, where distribution distances differ significantly, moisture control can directly affect delivered shelf life. Material handling is where many produce projects either protect value or quietly destroy it. Conveyors must be designed around product fragility, sanitation, and traffic flow. Root vegetables usually tolerate cleated belts, roller inspections, and more assertive elevation changes. Leafy greens require broad belts, shallow troughing, low drop transfers, cleanable supports, and precise speed matching between equipment. In mixed-product facilities, one of the best approaches is segmented handling architecture: dirty receiving, prewash transfer, wash discharge, dewatering, inspection, clean conveyance, and packaging feed. Each zone should have a defined hygiene level and maintenance strategy. Crossovers should be minimized, and where possible, operator access should not force people to lean across open product. Applications vary by industry. A foodservice root vegetable plant near Idaho or Wisconsin may prioritize ruggedness and mud tolerance. A leafy greens operation near Salinas, Yuma, or New Jersey may prioritize hygiene, low bruising, and rapid sanitation. Meal kit suppliers near urban fulfillment centers often need flexible conveyor routing because SKU variation changes daily. The trend is clear: processors are moving from basic conveyor layouts toward hygienic, automated handling with easier washdown, less manual sorting, and better line balancing. When reviewing conveyors, buyers should ask: Water is now a strategic utility in produce processing. In many U.S. regions, water cost, wastewater discharge, and sustainability reporting are making recirculation and filtration central design topics. Plants in California, Arizona, Texas, and parts of the Southeast often feel this pressure most strongly, but even facilities in water-rich areas are facing customer expectations around environmental stewardship. A sustainable wash line does not mean maximum recirculation at all costs. It means using water where it adds the most hygienic value and reusing water only where risk is controlled. Typically, the dirtiest stages receive the least clean reusable water, while the cleanest stages receive higher-quality treated or fresh water. Filtration may include rotary drum screens, static screens, settling, hydrocyclones, bag filters, or more advanced polishing steps depending on solids load and reuse goals. Instrumentation is increasingly important. Turbidity, flow, oxidation-reduction potential, temperature, and tank level data help operators keep the system in control. Automated dump-and-refresh logic can prevent degraded water quality before it affects product. In 2026, U.S. buyers are also more interested in reporting dashboards that connect water usage to pounds processed. This table shows how sustainable operation is achieved by layering technologies rather than relying on one “magic” filter. For many processors, the best path is a staged recirculation strategy that lowers water use substantially while preserving the cleanest final contact conditions. Policy trends also matter. In 2026, more corporate buyers are requiring ESG-style reporting, and more plants are preparing for tighter local utility expectations. Projects that reduce water consumption per pound of produce while protecting food safety will remain strong candidates for capital approval. A wash line should not be designed as an island. The real value appears when washing connects smoothly to grading, sizing, cutting, optical inspection, weighing, and packaging. If line integration is poor, the wash system may perform well on its own but still create backups, inconsistent feed rates, and excess labor downstream. For root vegetables, grade sizing may include roller graders, diverging lane sortation, or camera-based systems depending on pack style. For leafy products, the critical integration points are usually feed metering, cut quality protection, and moisture consistency before weighers and baggers. In mixed application plants, packaging may include pillow bags, vertical form-fill-seal systems, clamshells, trays, foodservice bulk bags, or case-ready retail formats. U.S. processors near logistics hubs like Atlanta, Inland Empire, Kansas City, and Harrisburg often benefit from flexible packaging line integration because they ship to multiple channels with different case counts, pallet patterns, and labeling needs. As a result, 2026 line design increasingly includes recipe-based controls, modular discharge options, and data links between wash line speed and packaging equipment performance. One of the smartest buying questions is whether the supplier can engineer the interfaces, not just the machines. Integration determines whether the entire process behaves like one system or a collection of separate assets. The comparison illustrates why engineered integration usually outperforms piecemeal purchasing, especially when processors expect growth, tighter retailer requirements, or future automation. Compliance is not a separate layer added after installation. HACCP thinking, preventive controls, sanitary design, and daily cleaning requirements should shape the wash line from the beginning. A produce line should be laid out to support hazard analysis, defined intervention points, accessible cleaning, drainability, and documented verification. Daily sanitation protocols in U.S. facilities typically include dry debris removal where applicable, pre-rinse, foam or detergent application, manual detail cleaning, rinse verification, sanitizer application, reassembly checks, pre-op inspection, and startup verification. Equipment frames should avoid hollow-body contamination risks, standing water traps, and inaccessible bearings over open product zones. Operators and quality teams should clearly understand control points such as antimicrobial dosing, final rinse condition, metal detection if applicable downstream, package seal performance, and temperature management through the process. Records must be practical enough that teams actually use them during busy production days. This table shows how compliance is improved through design. Good engineering lowers the burden on operators and makes the right behavior easier to sustain every day. For plants selling to national retailers or operating under SQF or BRC expectations, documented sanitation and start-up verification are increasingly important. The same is true for co-packers handling multiple customer standards in one facility. Disruptive Process Solutions, or DPS, works with food and beverage manufacturers across the United States and Canada on engineered capital projects that must perform in the real world, not just on a proposal sheet. In produce applications, that matters because wash lines sit at the intersection of process design, sanitation, utilities, controls, installation, and startup. A processor needs more than a machine vendor; it needs a partner that can engineer, build, and manage the entire project. From a technological capability standpoint, DPS supports process engineering, mechanical and utility integration, controls architecture, PLC programming, automation, and SCADA-informed system visibility. That means a produce wash line can be designed with coordinated conveyor speeds, monitored sanitation dosing, recirculation control, pump logic, utility tie-ins, and startup support that aligns with production goals rather than isolated equipment operation. You can learn more about the company background on the About Us page. From a manufacturing capability standpoint, DPS also brings proprietary equipment experience into broader processing projects. That approach is useful when a customer needs custom tanks, CIP support equipment, specialty process skids, or integrated fabrication that standard catalogs cannot solve cleanly. Produce processors often benefit when utility skids, tanks, and process modules are designed to fit the line as-built rather than forced into the layout later. Additional capabilities are outlined in the equipment solutions section. From a service capability standpoint, DPS operates through an end-to-end model covering planning, design, capital project support, owner representation, installation management, and execution oversight. That is especially valuable for U.S. processors expanding in active facilities, relocating lines, or balancing production continuity with modernization. Whether the need is feasibility, detailed engineering, integration, or full delivery, the firm’s broader offering is described on its service capabilities page. For examples of project work and execution style, readers can review selected case studies and project examples. What differentiates this approach is business-minded engineering. The project is not only about buying hardware; it is about improving profitability through the right scope, utility planning, controls strategy, labor model, and startup sequence. In the produce segment, that often means avoiding overbuilt systems in low-risk areas while investing heavily where food safety, shelf life, and throughput actually depend on the design. What is the best produce wash line for leafy greens in the United States?For most leafy greens, an air bubble wash system with controlled agitation, antimicrobial dosing, sanitary transfer conveyors, and strong dewatering is the preferred configuration. Final design depends on leaf fragility, throughput, and pack format. Is PAA better than ozone for produce sanitation?Neither is universally better. PAA is often easier to validate and operate in the main wash system. Ozone can be effective in well-engineered water treatment applications. Many plants use a combination strategy by zone. Why is dewatering so important after washing?Residual moisture affects shelf life, package seals, weighing consistency, and visual quality. A two-stage dewatering system helps stabilize downstream operations and reduce package-related rejects. Can one wash line handle both root vegetables and leafy greens?Sometimes, but not always well. If the product mix is broad, separate wash paths or modular zones usually deliver better cleaning, less damage, and easier sanitation than a one-size-fits-all machine. How much water can be recirculated safely?That depends on product risk, solids loading, filtration performance, chemistry control, and validation. Safe recirculation is a system-engineering question, not a fixed percentage. What U.S. regulations most affect produce wash line design in 2026?FSMA preventive controls, customer food safety standards, wastewater requirements, worker safety expectations, and retailer shelf-life demands all influence line design and documentation. What industries use advanced produce wash lines?Fresh-cut produce, retail salad packing, foodservice vegetables, meal kits, frozen vegetable preparation, value-added root vegetable processing, and specialty herb packing all rely on these systems. How should buyers compare suppliers?Look beyond equipment price. Compare process fit, sanitation design, automation depth, utility requirements, installation capability, startup support, parts access, and the supplier’s ability to integrate the full line. What future trends matter most in 2026?More sensor-driven sanitation control, stronger water reuse expectations, better hygienic automation, digital recordkeeping for compliance, and project decisions tied to total cost of ownership rather than only purchase price. What is the smartest first step for a processor planning an upgrade?Start with a process review that maps product types, throughput, sanitation risks, water balance, labor model, and downstream packaging needs. The best wash line comes from whole-system planning, not isolated equipment shopping. -
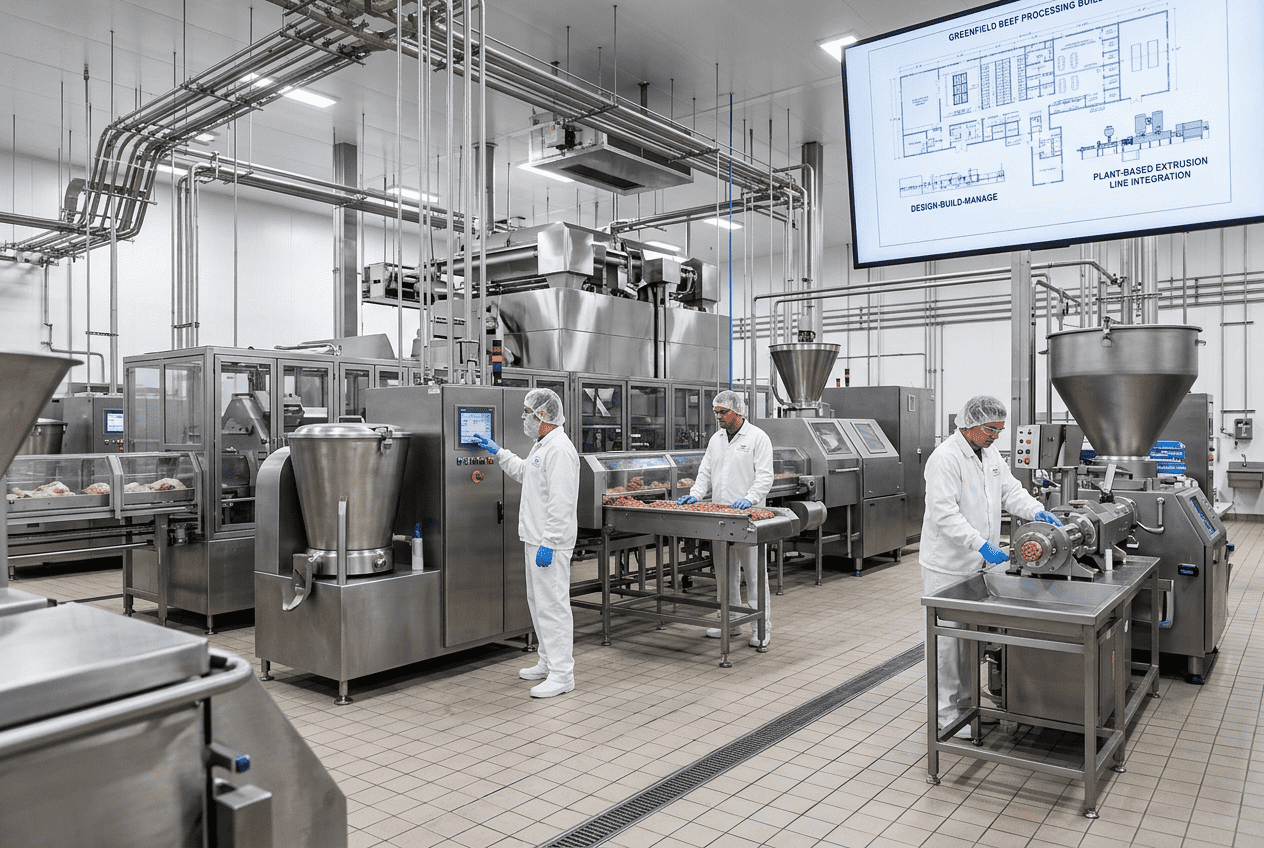
Tortilla Production Line Design in 2026: From Masa to Packaging
Tortilla manufacturing in the United States is moving toward higher throughput, tighter labor control, better food safety, and more flexible product changeovers. A successful 2026 tortilla line design starts with matching dough preparation, forming, baking, cooling, and packaging equipment to the exact product mix, utility profile, plant footprint, and commercial goals of the facility. For most U.S. manufacturers, the best tortilla production line is not simply the fastest line. It is the line that delivers repeatable diameter, target moisture, clean release, strong stack integrity, and packaging uptime while keeping labor, energy, and sanitation costs under control. Whether the facility is producing corn tortillas for foodservice in Texas, wheat tortillas for retail in California, or mixed SKU private-label products in the Midwest, the design should begin with five decisions: product type, hourly throughput, flexibility requirements, utility capacity, and distribution format. In practical terms, corn tortilla lines and wheat tortilla lines share many downstream elements, but the front-end process differs significantly. Corn systems are centered on masa preparation or prepared masa handling, while wheat systems require more precise hydration, gluten development, resting, dividing, rounding, pressing or sheeting, and final proof-like relaxation depending on formulation. After forming, both product families depend on tightly controlled tunnel oven zones, stable cooling profiles, gentle transfer, accurate counting or stacking, and packaging systems that protect freshness and shelf life. Across the United States, high-volume tortilla plants near Los Angeles, Dallas-Fort Worth, Chicago, Phoenix, Atlanta, and New Jersey are investing in automation because labor volatility, retailer expectations, and freight economics increasingly reward consistency. Plants located near major logistics corridors such as the Port of Los Angeles, the Port of Houston, Savannah, and intermodal hubs in Kansas City or Memphis also benefit from line designs that reduce rework and improve case-ready packaging performance. When evaluating capital projects, buyers should look beyond the press or oven alone. The real business case comes from whole-line integration: mixer sizing, dough residence time, conveyor synchronization, recipe control, sanitation access, and final packaging efficiency. In many projects, the limiting factor is not a single machine but the coordination between machines. That is why system-level engineering matters. The table above shows why early front-end planning is essential. A tortilla line should be engineered around the business model, not purchased as a collection of disconnected machines. The dough room defines the performance of the entire tortilla line. For corn tortillas, processors may handle dry corn flour with water and minor ingredients, or integrate upstream nixtamalization and masa preparation when producing from whole corn. For wheat tortillas, the system must control flour type, water absorption, shortening or oil incorporation, minor ingredient dispersion, dough temperature, and rest time. A well-designed mixer and dough preparation system reduces variability before the dough ever reaches the divider or press. In the United States, corn tortilla lines serving quick-service restaurants often prioritize high rate, uniform diameter, and robust hot-hold performance. Retail wheat tortilla lines, by contrast, often require softer bite, foldability, longer shelf life, and a broader product range including fajita, burrito, taco, and better-for-you formulas. That means the dough system needs recipe flexibility, lot traceability, and automation strong enough to maintain consistency from shift to shift. Common equipment options include horizontal mixers, high-capacity batch mixers, continuous dosing systems, ingredient pre-blending skids, water tempering modules, and intermediate dough hoppers. For wheat tortillas, a dough rest conveyor or trough arrangement is frequently critical because relaxation affects final press quality, snapback, and edge symmetry. For corn products, moisture management and feed consistency into the sheeter or press are equally critical to avoid edge cracking and weight drift. Well-integrated plants also connect the dough room to controls architecture. Recipe management, batch records, temperature trending, and ingredient verification can be handled through PLC and SCADA systems so operators can identify deviations before they create scrap. This is especially useful for high-volume operations near Dallas, Fresno, and Chicago where production schedules are tight and downtime carries immediate freight and customer penalties. From a technology standpoint, a partner with process engineering and controls expertise can significantly improve this area. Disruptive Process Solutions supports food manufacturers with process design, automation, PLC programming, SCADA integration, utility design, and complete system coordination, which is especially valuable when mixer performance, ingredient delivery, and line rate need to function as one system rather than as isolated assets. This comparison highlights why dough system selection should always follow product definition. A plant that tries to run diverse formulas on an underspecified dough room often fights the same defects every day downstream. Once the dough is prepared correctly, the next step is to create uniform pieces and shape them consistently. Divider, rounder, and hot press selection affects product weight, diameter, thickness, edge appearance, stackability, and oven loading efficiency. For wheat tortillas, a divider-rounder combination must handle the intended dough softness without smearing or excessive flour use. For corn tortillas, the forming system must keep product geometry stable while minimizing sticking and deformation. Hot press selection should consider platen size, thermal control, dwell time, press force, release materials, and sanitation access. If a line is intended to run multiple diameters, the design should also evaluate tooling changes, setup time, and servo-driven adjustment capability. High-throughput U.S. plants commonly prioritize repeatable piece weight and low giveaway because even small variance becomes expensive at national scale. Some manufacturers prefer very high speed dedicated lines for a narrow SKU range. Others, especially private-label and regional producers serving the Southeast and Northeast, benefit more from flexible equipment that can change between 6-inch taco tortillas, 8-inch wraps, and 12-inch burrito formats. The correct choice depends on sales mix, order volatility, and labor availability. Buyers should also examine upstream-downstream matching. A divider that can outrun the press or a press that floods the oven infeed will not create real capacity. The target is balanced throughput with enough surge handling to absorb short interruptions. If the packaging line stops briefly, the rest of the system should not immediately dump product. Manufacturing capability matters here as well. DPS designs and integrates custom process equipment and supports complete system buildouts, including fabricated tanks, CIP modules, and food-grade process components. That broader manufacturing perspective is useful when the tortilla line needs custom hoppers, transfer frames, guarding, platforms, or utility skids tailored to the building rather than off-the-shelf compromises. The explanation is straightforward: the best forming package is the one that protects product quality while matching the facility’s true sales profile. Overbuying speed without enough flexibility can be just as costly as underbuying capacity. The oven is the thermal heart of a tortilla line. Multi-tier or multi-deck tunnel oven design allows processors to optimize floor space while delivering the rapid, controlled heating needed for puffing, color development, moisture removal, and final texture. A successful oven design is not based only on total length. It depends on thermal profile, air management, burner arrangement, belt selection, zone independence, exhaust balance, and access for cleaning and maintenance. For tortilla plants in the United States, natural gas remains the most common fuel source, but electric and hybrid heating discussions are growing as utilities, state incentives, and carbon reporting requirements evolve. California and some Northeast markets are especially active in evaluating future energy strategy, while Texas and the Midwest continue to favor gas-fired designs where infrastructure is strong. Temperature zone control is critical because tortillas do not need the same thermal conditions across the entire bake. Early zones often focus on set and steam release, middle zones on structure and color, and later zones on moisture balance and finish. Independent controls by zone improve product uniformity and make it easier to switch between corn and wheat formulations or between thicker wraps and thinner taco styles. Engineers should also review how the oven interacts with upstream and downstream conditions. Press temperature, belt loading pattern, ambient room conditions, and final cooling capacity all influence the effective bake. Excessive oven variability often shows up later as stack sticking, poor package appearance, or shelf-life inconsistency. This is one area where strong mechanical, process, electrical, and controls coordination delivers outsized value. A full-scope engineering partner can address combustion integration, ventilation, utility routing, controls architecture, and code compliance together. Manufacturers looking for broader project support can review integrated engineering and project services when planning complex thermal systems. The table shows why zone-level control is a strategic investment rather than a luxury. It gives operators a practical way to manage product quality and energy performance at the same time. Cooling is often underestimated in tortilla manufacturing, yet it directly affects stack quality, condensation risk, packaging speed, and shelf life. After the oven, tortillas must lose heat in a controlled way while preserving shape and moisture balance. Cooling conveyor design should consider residence time, airflow, belt material, sanitation access, and plant room conditions. In humid climates such as Houston, Miami, or New Orleans, ambient conditions can make cooling design especially important. Counter-stackers and indexing systems must then gather tortillas accurately without crushing edges or miscounting. A line designed for retail packs may require extremely precise stack counts with smooth handoff to baggers, while foodservice bulk packs may prioritize robust throughput and larger stack heights. Synchronization between the cooling section and the counter-stacker is essential because loose timing creates jams, tilted stacks, and operator intervention. Some facilities also benefit from vision or sensor-based counting verification, especially where customer complaints about count accuracy carry chargeback risk. Others may need side guides, vacuum assists, or transfer flights depending on tortilla size and pliability. The correct integration depends on product geometry and the variability tolerated by the market channel. For plants expanding into new distribution regions, cooling and stacking can become the hidden bottleneck. A product that looks good at the oven discharge may still fail in retail if it packs too warm, sweats in the bag, or arrives in stores as a compressed or irregular stack. That is why complete line design should include post-bake handling from the start, not as an afterthought. In short, the cooling section protects the value created by the oven. If the product is not conditioned correctly before stacking and bagging, the plant gives back quality and efficiency downstream. Packaging is where a tortilla line either converts efficiently or loses margin. Vacuum transfer systems can gently move tortillas or stacks into the final packaging sequence with reduced manual handling, helping preserve product shape and improve line speed. Modern packaging automation may include stack orientation, bag feeding, date coding, seal inspection, checkweighing, metal detection, case packing, palletizing, and production data capture. For U.S. retail distribution, packaging automation must also support label compliance, traceability, and retailer-specific pack counts. Foodservice operations may require bulk sleeves, higher weight packs, or club-store configurations with stronger case structures. Plants serving national accounts often need the ability to switch between channels without lengthy mechanical changeovers. One of the most important purchasing questions is whether the packaging line can run at the realistic sustained speed of the upstream process, not just the advertised mechanical maximum. In many facilities, packaging micro-stops create the most frustrating form of lost capacity. The solution is usually better integration: synchronized controls, buffer logic, reject handling, and clear operator interfaces. Service capability becomes especially valuable at this point. DPS supports end-to-end project management, owner’s representation, installation oversight, general contracting where licensed, and complete integration of process, utilities, and controls. For manufacturers that want a single partner to engineer, build, and manage execution, that model reduces coordination gaps between process equipment and packaging infrastructure. More information on available equipment solutions can help frame project scope. Applications are broad. Tortilla lines may serve retail chains in New York and Boston, foodservice distributors in Atlanta and Charlotte, or regional restaurant networks across Arizona and Nevada. Packaging automation should be tailored to the actual route-to-market, because pack style and handling requirements influence every downstream decision. The explanation here is simple: packaging is not the end of the line from an engineering perspective. It is the point where capital efficiency becomes visible in labor, yield, customer complaints, and delivered cost. Cleanability is now a capital design issue, not just a sanitation issue. In tortilla production, flour dust, seasoning residues, oils, and allergens can accumulate across mixers, dividers, conveyors, ovens, coolers, and packaging frames. If sanitation is difficult, plants lose production time, increase labor, and raise food safety risk. Equipment should therefore be evaluated for open-frame design, weld quality, drainage, access panels, removable components, hygienic fasteners, and minimized harborage points. Allergen control is especially important when plants run both standard and specialty products. Wheat is itself a major allergen concern for some operations, and lines that alternate between wheat, gluten-free, dairy-containing flavored wraps, or protein-enhanced formulas need disciplined segregation and validated cleaning methods. Plants serving contract manufacturing or private-label customers may face even tighter verification expectations. U.S. buyers should also design around real compliance conditions. SQF and BRC audits, FDA expectations, customer environmental monitoring programs, and documentation requirements all favor equipment that can be cleaned and inspected efficiently. In older buildings common in the Northeast and upper Midwest, sanitation upgrades often require better utility access, improved airflow, and redesign of difficult transfer points. Engineering support should extend beyond equipment purchase into plant layout, COP/CIP strategy, utility routing, and hygienic zoning. This is another reason to work with a team that understands food processing, compliance, and plant execution together instead of treating sanitation as a later retrofit. The key takeaway is that hygienic design protects uptime as much as it protects food safety. Cleaner equipment is easier to run, easier to inspect, and less likely to create avoidable quality losses. Energy efficiency is becoming one of the most important buying criteria for tortilla manufacturers in 2026. Gas cost volatility, labor cost pressure, sustainability commitments, and state-level environmental expectations are all pushing plants to reduce energy intensity per thousand tortillas. The biggest opportunity usually sits in thermal design: burner efficiency, insulation, exhaust control, recirculation strategy, and heat recovery. Heat recovery can take several forms. Some plants capture waste heat from oven exhaust to preheat combustion air or process water. Others combine oven improvements with broader utility projects such as boiler optimization, compressed air reduction, and HVAC coordination. In markets such as California, Washington, and parts of the Northeast, utility incentives may improve the project payback for well-documented energy upgrades. Future trends also matter. By 2026, more food manufacturers are expected to evaluate digital energy monitoring, carbon reporting support, and electrification readiness. Even if a plant does not switch fuels immediately, designing controls and space allocation with future utility flexibility can reduce long-term retrofit cost. Policy pressure around emissions disclosure and corporate sustainability reporting is making that foresight more valuable. In many cases, the best result comes from combining process engineering with utility engineering. DPS works across structural, mechanical, plumbing, electrical, process, and automation disciplines, and also supports utility systems such as boilers, steam, compressed air, cooling, refrigeration, process water, and energy management. That cross-functional capability is particularly relevant when tortilla oven performance is tied to the rest of the plant’s infrastructure rather than standing alone. From a buying perspective, the lowest purchase price rarely delivers the lowest lifetime cost. U.S. manufacturers should ask for modeled energy performance, not just nameplate features. Disruptive Process Solutions serves manufacturers across the United States and Canada as a food and beverage engineering partner focused on profitable capital execution. Rather than approaching a tortilla project as a simple equipment sale, the company works through an end-to-end design, build, and manage approach that aligns process performance, utilities, installation, controls, and commercial objectives. For tortilla manufacturers, that means support can begin with feasibility, throughput analysis, and concept layout, then move into process engineering, utility planning, equipment integration, construction coordination, and startup oversight. The team’s work spans both food and beverage sectors, but on the food side it includes mixing, forming, thermal processing, sanitary systems, automation, and full plant infrastructure that are directly relevant to tortilla operations. Technologically, the company brings process and controls depth, including PLC programming, SCADA, recipe and batch logic, utility integration, and broader plant engineering. From a manufacturing perspective, DPS also provides proprietary process equipment such as tanks and CIP systems while coordinating custom fabrication needed for complete projects. From a service perspective, the company supports capital planning, owner’s representation, project and program management, installation, system integration, and general contracting functions where applicable. Manufacturers seeking background can visit our company overview, explore broader engineering services, or review selected project case examples. This integrated model is especially useful for tortilla plants because the line often touches nearly every plant function at once: process, thermal, packaging, utilities, building modifications, sanitation, and controls. A coordinated partner can help reduce change orders, speed decisions, and keep the project focused on long-term operating margin. What is the first step in designing a tortilla production line?Start with the commercial plan: product mix, hourly output, package format, shelf-life target, and labor strategy. Equipment should follow those requirements, not the other way around. How different are corn and wheat tortilla lines?They share downstream handling, cooling, and packaging concepts, but the front-end dough system and forming methods are often very different. Wheat lines usually require more dough development and rest control. What throughput range is common in the United States?There is no single standard, but many commercial lines range from mid-volume regional systems to very high-speed national-account lines. The right capacity depends on SKU complexity and distribution footprint. Should I choose a dedicated line or a flexible line?If demand is concentrated in one or two SKUs, a dedicated line can deliver efficiency. If the business serves private label, multiple diameters, or mixed channels, flexibility often creates better total return. Why is oven zoning so important?Independent temperature zones improve bake consistency, moisture control, color development, and changeover response. They also support energy optimization. What causes packaging problems in tortilla plants?Common causes include insufficient cooling, unstable stacking, poor transfer timing, packaging equipment micro-stops, and lack of buffer logic between upstream and downstream systems. How should buyers compare suppliers?Compare complete system capability, not only individual machine price. Review process knowledge, sanitation design, controls integration, utility understanding, installation support, and service responsiveness in the United States. What future trends should shape a 2026 project?Expect more automation, energy monitoring, heat recovery, digital recipe control, stronger traceability, sustainability reporting, and designs that support faster sanitation and broader SKU flexibility. Are local supplier relationships still important?Yes. Even with national engineering support, local trades, service technicians, utility coordination, and regional code knowledge matter, especially in major manufacturing hubs like Southern California, Texas, Illinois, and the Southeast. Can an existing tortilla line be upgraded instead of replaced?Often yes. Bottlenecks may sit in controls, post-bake handling, utilities, or packaging rather than the entire line. A disciplined assessment can reveal where modernization delivers the best return.


