-
Food Facility Equipment Reliability Engineering
Food facility equipment reliability engineering is the discipline of making processing, packaging, utility, and sanitation systems run safely, consistently, and profitably with fewer failures. In the United States, where food and beverage plants operate under strict production schedules, retailer service expectations, and FDA or USDA compliance pressures, reliability is not just a maintenance topic. It is a production, quality, safety, labor, and capital planning strategy. A dependable plant protects throughput, reduces waste, supports food safety, stabilizes labor scheduling, and improves return on investment for every line, utility skid, tank farm, filler, retort, cooker, pasteurizer, compressor, boiler, conveyor, pump, and CIP circuit. For manufacturers operating in major hubs such as Chicago, Dallas, Atlanta, Los Angeles, Fresno, Milwaukee, Charlotte, Houston, and the New Jersey corridor near Port Newark and Philadelphia distribution lanes, equipment downtime can quickly create missed shipments, spoiled product, overtime, and customer penalties. Reliability engineering helps leadership decide what equipment matters most, what failure modes create the largest business risk, and what maintenance tactics actually produce higher uptime. This article explains how U.S. food and beverage manufacturers can apply reliability-centered maintenance principles, equipment criticality assessment, failure mode and effects analysis, mean time between failures optimization, redundancy planning, condition monitoring technologies, and practical reliability KPIs. The quickest answer is this: food facility equipment reliability engineering improves plant uptime by identifying critical assets, understanding how they fail, selecting the right preventive and predictive maintenance tasks, and designing backup capacity where shutdown risk is unacceptable. In the United States market, the most effective reliability programs usually combine five actions: For food and beverage facilities, the biggest reliability gains often come from utilities and controls rather than the most visible process equipment. A single PLC issue, compressed air failure, valve cluster malfunction, glycol outage, or CIP gap can stop production across multiple lines. That is why reliability engineering must connect maintenance, operations, sanitation, quality, engineering, and finance. Plants that treat reliability as a site-wide operating system usually outperform plants that view it only as a wrench-turning function. When leadership is evaluating upgrades, expansions, line relocations, or new greenfield builds, reliability planning should begin before equipment is purchased. This includes design review for maintainability, access, sanitation compatibility, instrumentation strategy, utility resilience, controls architecture, and spare part standardization. That front-end work typically lowers lifecycle cost far more effectively than reactive maintenance after startup. The table above shows why reliability engineering should not be reduced to a maintenance checklist. Each area ties directly to cost, output, and customer service. Plants in high-volume categories such as dairy, protein, RTD beverages, sauces, frozen meals, and aseptic products often see the fastest payback from structured reliability work because downtime cascades through sanitation windows, changeovers, and cold-chain constraints. Reliability-centered maintenance, or RCM, asks a simple but powerful question: what maintenance strategy is appropriate for each asset based on how it fails and what happens when it fails? In U.S. food plants, that matters because not every machine deserves the same inspection frequency, not every component should be replaced on a calendar basis, and not every failure can or should be prevented. Some failures are age-related, some are random, some are operational, and some are caused by cleaning practices, product chemistry, startup routines, or utility instability. A strong RCM program in food manufacturing usually starts with these principles: For example, a homogenizer in a dairy plant, a retort in a shelf-stable foods facility, or a filler in a beverage plant has different reliability consequences than a low-risk warehouse fan. The first group may require detailed inspection intervals, oil analysis, seal monitoring, thermal checks, and critical spares. The second may be suitable for simpler preventive maintenance or controlled run-to-failure. This distinction protects maintenance budgets from being spread too thin. RCM also supports buying advice. When selecting new process systems, manufacturers should compare not just capacity and purchase price, but also hygienic design, cleanability, access for maintenance, instrumentation quality, OEM support, controls transparency, standard motor and gearbox availability, and ease of integration with CMMS and SCADA. Plants that overemphasize low initial cost often inherit expensive downtime later. In many U.S. facilities, one of the most common RCM mistakes is over-maintenance. Bearings get replaced too early, instruments are calibrated too often without risk basis, and PM routes consume labor without reducing failures. Another common mistake is under-maintaining utilities because they are less visible than process lines. Yet boilers, chilled water, refrigeration, glycol, compressed air, RO, wastewater, and CIP are often the true backbone of reliability. The line chart reflects a realistic directional trend: U.S. spending on reliability programs is rising as plants automate more heavily, labor remains constrained, and customers expect better service levels. By 2026, more companies are expected to combine maintenance planning with digital condition monitoring, energy management, and production intelligence. Equipment criticality assessment helps a plant determine where to focus engineering time, maintenance hours, capital reserves, and spare parts. In food and beverage environments, criticality should be based on consequence, not emotion. The loudest machine on the floor is not always the most important asset. A modest utility skid may have a far larger impact than a large visible process vessel. A practical criticality model for U.S. plants scores assets across six dimensions: safety, food safety, regulatory impact, production throughput, quality risk, and repair recovery time. Many facilities also include part lead time and detectability. A valve island with a 16-week lead time may deserve a higher criticality score than expected if one failure can stop a filler or CIP sequence. This type of matrix allows management to separate must-protect assets from convenience assets. It also guides the right level of spare parts. A plant near major logistics centers like Memphis, Kansas City, or the Inland Empire may have better access to regional distributors, but relying on same-day supply is still risky for custom controls, sanitary pumps, specialty valves, and imported drives. Criticality analysis should therefore influence local supplier strategy and stocking policy. Buying advice also changes by sector. In protein processing, sanitation-driven wear, washdown exposure, and cold-room conditions elevate reliability needs for motors, drives, scales, slicers, and conveyors. In beverage plants, carbonation systems, fillers, labelers, bright tanks, blending systems, and utility balance are often key constraints. In aseptic and retort operations, instrumentation, validation integrity, and sterile barriers raise the consequence of small failures. For companies planning expansions in Georgia, Texas, North Carolina, California, or the Midwest manufacturing belt, criticality assessment should be completed during concept design so that electrical distribution, bypasses, utility loops, isolation points, and maintenance access are built into the project from the beginning. Failure mode and effects analysis, or FMEA, is one of the most useful tools in reliability engineering because it forces the team to move from vague concern to specific risk logic. Instead of saying “the line keeps going down,” FMEA asks exactly how it fails, why it fails, how often it fails, what happens when it fails, and whether the failure can be detected before it becomes a shutdown or quality event. In food facilities, FMEA works best when cross-functional teams participate. Maintenance may know the mechanical weak points. Operators know startup behaviors and nuisance stops. Sanitation knows which components degrade after chemical exposure. Quality knows which failures create product holds. Controls engineers know where alarms lack diagnostic value. Purchasing knows which parts are hard to source. The value of FMEA is not the document itself. The value is the action plan it produces. Good outputs include redesigned guards for easier inspection, upgraded instrumentation, revised sanitation SOPs, controls changes, PM interval changes, improved training, and better spare part kits. On high-speed packaging lines, FMEA often identifies low-cost sensor mounting or cable routing issues that create outsized downtime. In wet environments, it frequently uncovers enclosure integrity and connector failures. In thermal processing, it often reveals calibration and valve response weaknesses. Case studies across the U.S. repeatedly show that hidden control logic can limit capacity as much as hardware can. When an engineering partner reviews logic, sequencing, and alarm handling early, plants can sometimes recover significant throughput without large capital spending. Readers interested in examples of project-led problem solving can explore food and beverage project case studies that illustrate how operational bottlenecks are often solved through integrated engineering rather than equipment replacement alone. Mean time between failures, or MTBF, is a useful reliability metric when used correctly. It measures the average operating time between failure events for repairable assets. In food and beverage plants, MTBF optimization is not about making a number look better in a dashboard. It is about increasing stable run time between business-disrupting events while avoiding excess maintenance cost. The first rule is to define failure consistently. A five-minute sensor reset should not always count the same way as a gearbox replacement or a product hold event. Many U.S. manufacturers classify failures by severity so that engineering can distinguish nuisance stops from critical outages. The second rule is to pair MTBF with MTTR, mean time to repair. A plant with moderate MTBF but excellent repair readiness may outperform a plant with slightly higher MTBF but chaotic recovery execution. To improve MTBF, plants usually need a mix of actions: eliminate design flaws, improve operating discipline, tighten planned maintenance, improve lubrication control, add predictive monitoring, and standardize failure coding in the CMMS. Plants near busy labor markets such as Southern California or central Texas also benefit from better documentation because workforce turnover can otherwise erase tribal knowledge. For executives, MTBF should be translated into dollars. If increasing filler MTBF by 70 percent prevents two lost shifts per month, reduces cleanup scrap, and stabilizes retailer shipments, the business case becomes clearer than a maintenance graph alone. Redundancy is one of the most misunderstood topics in food facility reliability engineering. Redundancy does not mean duplicating everything. It means selectively designing backup capacity where the business consequence of a single-point failure is too high. In U.S. food and beverage operations, the most common redundancy candidates are utilities, controls infrastructure, sanitation systems, and product-holding functions. Examples include duplex sanitary pumps, lead-lag air compressors, N+1 chilled water or glycol circulation, backup RO trains, dual boilers where justified, network path redundancy, spare VFD strategy, emergency power for critical controls, and parallel CIP functionality in plants with tight sanitation windows. In some sectors, inventory buffering can be a practical alternative to full mechanical redundancy. In others, such as aseptic, dairy, or high-speed beverage, downtime cost may justify stronger backup design. Geography matters. Plants on the Gulf Coast may weigh hurricane resilience, utility interruption risk, and port-related supply chain variability. Facilities in the Upper Midwest may prioritize winterization and freeze protection. Plants serving major retail networks out of Pennsylvania, Ohio, Indiana, or Tennessee may emphasize uninterrupted distribution commitments. Reliability engineering must adapt to local operating realities. The bar chart shows realistic differences in how much redundancy demand tends to exist by category. Aseptic and RTD beverage plants often place a very high premium on uninterrupted controls, utilities, and sterile support systems. Frozen foods may still need reliability upgrades, but the redundancy profile may differ based on process design and production flexibility. When evaluating local suppliers, U.S. manufacturers should ask about response times, regional service coverage, sanitary parts availability, control panel support, and commissioning competence. The best supplier is not always the lowest bidder. It is often the one that can keep the line recoverable. Strategic sourcing should include nearby parts support in regions such as the Carolinas, Midwest dairy corridor, Central Valley, Pacific Northwest, and Texas manufacturing triangle. Condition monitoring technologies are increasingly important because food plants need earlier warning of asset deterioration without excessive manual inspection. The most practical technologies for U.S. food and beverage sites include vibration monitoring, infrared thermography, oil analysis, ultrasonic inspection, motor current analysis, pressure and flow trend analytics, valve position feedback, compressed air leak detection, and advanced PLC/SCADA alarm diagnostics. Not every plant needs every technology. The correct deployment depends on criticality, failure history, environment, and available skill. High-speed lines may benefit from smart sensing and alarm analytics. Wet-process plants may benefit more from pump, motor, valve, and heat exchanger monitoring. Utility-intensive sites can gain significant value from compressor, boiler, chiller, and water treatment analytics. For 2026, the most important trend is convergence. Plants will increasingly connect condition monitoring with sustainability, food safety, and labor efficiency. For example, compressor leak detection cuts both downtime risk and energy cost. Better heat exchanger monitoring can reduce product loss and utility waste. Smart CIP analytics can improve cleaning reliability while lowering water and chemical consumption. As environmental reporting and energy scrutiny increase, reliability and sustainability will continue to overlap. The area chart illustrates the ongoing U.S. shift from reactive maintenance toward predictive approaches. The change is being driven by automation growth, tighter labor conditions, stricter uptime expectations, and the falling cost of monitoring technologies. Reliability metrics are only valuable if they drive better decisions. In food manufacturing, the most useful KPI set usually includes MTBF, MTTR, planned maintenance completion, schedule compliance, percent reactive work, spare parts fill rate, OEE impact from downtime, repeat failure rate, sanitation-related failures, and utility uptime. Plants should also track production consequence, such as pounds lost, cases not shipped, overtime hours, and product hold incidents linked to equipment events. The goal is balance. A plant can hit PM completion targets while still suffering chronic failures if the wrong PM tasks are being done. It can also show strong OEE on one line while missing the broader issue of unstable utilities. KPI reviews should therefore connect maintenance metrics with operations and quality outcomes. Supplier and product comparison can also support KPI decisions, particularly when standardizing new equipment or evaluating service partners. The comparison chart reflects a common reality in U.S. manufacturing: the lowest installed cost supplier may underperform in support, controls transparency, and spare parts access. For plants with aggressive throughput commitments, support quality often matters more than modest upfront savings. As a buying rule, manufacturers should require reliability deliverables during capital projects: critical spares list, recommended PM library, controls backups, sensor maps, utility demand profile, FAT and SAT documentation, and operator-maintainer training. Companies exploring broader project support can review integrated engineering and project services that combine design, installation, and execution oversight with plant performance objectives. Disruptive Process Solutions, or DPS, approaches food and beverage reliability through a business-first engineering lens. Rather than treating uptime as an isolated maintenance problem, the company aligns plant design, project execution, controls strategy, utility resilience, and operational profitability. That approach is especially relevant for U.S. manufacturers balancing growth, labor pressure, compliance demands, and capital discipline. From a technological capabilities perspective, DPS works across structural, mechanical, plumbing, electrical, process, and automation disciplines. Its team supports PLC programming, SCADA integration, utility systems, process controls, batching, recipe management, and energy-related infrastructure. In practice, that means reliability issues can be solved at the system level instead of being pushed between departments. A throughput problem may be mechanical, controls-related, utility-related, or sequencing-related, and integrated engineering is often required to identify the true root cause. More detail on the company’s background and operating philosophy is available on the about page for DPS. From a manufacturing capabilities perspective, DPS supports equipment and system solutions used across beverage, dairy, protein, prepared foods, aseptic processing, fermentation, distillation, pasteurization, retort, blending, and water treatment applications. The company also manufactures selected process equipment such as tanks, CIP systems, tumblers, and cooking vessels, which helps it align design intent with field execution. For reliability-driven buyers, this matters because equipment selection, maintainability, cleanability, and integration all affect long-term uptime. Manufacturers comparing equipment options can explore process equipment solutions relevant to food and beverage operations. From a service capabilities perspective, DPS uses an end-to-end design-build-manage model that covers process engineering, feasibility, owner’s representation, project and program management, general contracting where licensed, system installation, and commissioning. This is important for reliability because project handoffs are where many plants lose performance. When planning, design, construction, and startup are coordinated, the final system is more likely to support maintenance access, spare part standardization, utility resilience, and stable commissioning. For manufacturers in the United States expanding capacity, relocating assets, or launching new lines, that integrated project structure can reduce startup risk and help achieve profitable output faster. DPS serves manufacturers across all 50 U.S. states and Canada, with strong relevance for facilities handling beverages, proteins, dairy, sauces, aseptic products, and co-packing operations. The company’s value proposition is not simply technical breadth; it is the willingness to challenge poor capital assumptions and prioritize client profitability over unnecessary spending. In reliability engineering, that often means fixing the actual bottleneck instead of just adding more steel and stainless. What equipment is usually most critical in a food plant?Usually the most critical assets are those that can stop the entire process or create food safety exposure: boilers, compressed air, refrigeration or glycol, primary fillers, retorts, aseptic barriers, CIP systems, and control networks. How often should a plant perform a criticality review?At minimum once a year, and again after major line changes, new product introductions, utility expansions, or facility acquisitions. Is preventive maintenance enough?Not by itself. Food plants usually need a mix of preventive, predictive, operator care, redesign, and planned run-to-failure depending on the asset and consequence of failure. What is a good first step for a reactive plant?Start with a Pareto review of downtime, identify top ten failure contributors, perform criticality scoring, and complete FMEA on the top three bottlenecks. This creates a realistic roadmap without overwhelming the site. How does reliability affect food safety?Reliable equipment supports consistent time, temperature, flow, cleaning, and sealing performance. Poor reliability can lead to incomplete CIP, process deviations, contamination risk, and product holds. Which industries gain the most from reliability engineering?High-throughput and compliance-sensitive sectors benefit most, including dairy, beverage, protein processing, aseptic manufacturing, prepared foods, sauces, frozen foods, and co-packing. Should every plant invest in condition monitoring?Most should, but the scope should match asset criticality and team capability. A small plant may begin with infrared and compressor leak surveys, while a larger plant may deploy vibration sensors, SCADA analytics, and utility dashboards. What are the most important 2026 trends?Expect deeper use of predictive analytics, tighter integration between reliability and sustainability, stronger energy monitoring, more cyber-aware controls architecture, and increased focus on resilient utility design due to climate and supply chain risks. How should local supplier strategy be handled in the United States?Build a hybrid model: national standards for key equipment, regional service support near your plant, and on-site critical spares for components with long lead times. Facilities near ports, inland freight corridors, or remote production areas should account for logistics disruption risk. When should a company bring in an external engineering partner?Typically during expansions, chronic downtime on bottleneck systems, line relocations, utility failures, controls limitations, or when internal teams are too busy firefighting to redesign the system properly. In summary, food facility equipment reliability engineering in the United States is most successful when it is treated as a profit protection system, not merely a maintenance program. The strongest plants define criticality clearly, analyze failure modes rigorously, monitor asset condition intelligently, design selective redundancy, and hold themselves accountable with business-linked KPIs. Whether the plant is shipping beverages through California, processing protein in Texas, filling dairy in Wisconsin, or supporting co-packing in the Carolinas, reliability remains one of the clearest paths to safer operations, stronger margins, and more dependable growth. -
Food Plant Pump Selection Guide 2026
Choosing the right pump for a food plant is not a simple equipment purchase. In the United States, pump selection affects food safety, line efficiency, labor costs, cleanability, yield, utility consumption, and audit readiness. A pump that works well for water-like juice may fail in yogurt, tomato paste, marinades with particulates, or hot CIP return. For processors in hubs such as Chicago, Los Angeles, Fresno, Houston, Atlanta, Charlotte, Seattle, and the New Jersey port corridor, the best pump is the one that matches product behavior, sanitary standards, cleaning strategy, and the wider process system around it. This guide explains how to evaluate pump types for food applications, what sanitary design details matter most, how viscosity and flow influence performance, how to choose seals and elastomers, and how to avoid common installation mistakes. It also reflects 2026 trends in automation, sustainability, traceability, and regulatory expectations across FDA, USDA, SQF, and BRC-aligned facilities. If you need a fast recommendation, start with the product itself. Use centrifugal pumps for low-viscosity liquids such as water, beer, milk, brine, and many CIP services. Use positive displacement pumps, such as rotary lobe, twin-screw, circumferential piston, or progressive cavity designs, for thicker or shear-sensitive products like yogurt, sauces, dressings, nut butters, fruit preps, and protein slurries. Then confirm five critical fit factors: sanitary construction, flow and pressure requirements, clean-in-place compatibility, seal material compatibility, and piping integration. For most U.S. food plants, the ideal food-grade pump should offer 316L stainless steel wetted surfaces, hygienic connections, documented elastomer compatibility, a drainable design, and reliable performance across production and cleaning cycles. Plants shipping through major distribution lanes from Savannah, Long Beach, Newark, and Dallas-Fort Worth often prioritize uptime because delivery windows are tight and missed production can quickly become a customer service problem. The table above gives a practical first-pass screening method. Before comparing brands or price quotes, define product properties, cleaning conditions, and line integration requirements. This avoids a common mistake in the U.S. market: buying on pump model familiarity instead of application fit. The line chart reflects a realistic growth pattern for hygienic pumping demand in the United States, driven by expansion in ready-to-drink beverages, protein processing, plant-based foods, dairy innovation, and automation-led retrofits. Food plants use several pump designs, but most decisions come down to whether the application is better served by centrifugal or positive displacement technology. Centrifugal pumps are usually preferred for thin fluids, high flow, and simpler transfer duties. Positive displacement pumps are favored for viscous, delicate, or particulate-containing products and where more consistent flow under pressure is required. In dairy plants in Wisconsin, sauce facilities in California’s Central Valley, meat and poultry operations in Arkansas and Georgia, and beverage packaging sites around North Carolina and Texas, the chosen pump often reflects both product complexity and plant utility design. A beverage mixer feeding a syrup room may need very different pump performance than a retort sauce transfer system. This comparison table helps narrow the field. In many modern food plants, twin-screw pumps are gaining attention because they can transfer product and also support CIP with the same unit, reducing equipment count. That is especially attractive in high-value urban and suburban plant footprints where space is limited. Application examples include: When processors are scaling capacity in places like Phoenix, Nashville, or the Inland Empire, pump standardization across multiple lines can simplify spare parts, training, and maintenance. Still, over-standardizing can hurt performance if distinct products require different pumping behavior. Sanitary design is often the deciding factor in long-term pump value. In food plants, pump performance alone is not enough. The pump must also minimize microbial risk, support complete cleaning, avoid product retention, and comply with customer and regulatory expectations. A pump that meets flow targets but creates dead zones or recurring seal contamination can become a hidden cost center. For most U.S. food and beverage applications, 316L stainless steel is the standard choice for wetted parts due to corrosion resistance and compatibility with common cleaning chemistries. Surface finish matters as well. Smooth, polished product-contact surfaces reduce the chance of residue buildup and improve cleanability. Hygienic clamp connections, orbital weld quality, proper slope, and drainability all influence the full sanitary outcome. The table shows that sanitary performance depends on system design, not just the pump body. A perfectly hygienic pump can still underperform in a poorly routed skid with horizontal runs that trap product or branch legs that are difficult to clean. By 2026, more plants in the United States are expected to request stronger material traceability, digital maintenance records, and validation-ready documentation packages. This is especially relevant for aseptic and high-care operations supplying national retailers and co-manufacturing partners. Viscosity is one of the most misunderstood variables in pump selection. Many products change viscosity with temperature, shear, solids loading, or fat content. A dressing at 70°F may behave very differently at 40°F. Chocolate syrup, cultured dairy, gravy, or plant protein slurry can appear pumpable in a cup test but become difficult in long pipe runs with elbows, elevation changes, and restrictive valves. Flow rate should always be defined at actual operating conditions. That means not only target gallons per minute, but also inlet pressure, discharge pressure, product temperature, line length, fitting count, and production mode. If a plant in Minneapolis needs to transfer chilled dairy concentrate in winter conditions, or a Houston sauce line must move hot product to a filler, pump sizing will differ significantly even at the same nominal flow rate. This table is useful because it links product behavior to pump family rather than product name alone. Two sauces can have the same label category yet require different pump types because one is shear-sensitive and the other contains particulates. The bar chart highlights where pump demand is strong across U.S. food categories. Beverage and dairy remain large users, but sauces, protein, and prepared foods continue to grow as processors pursue line flexibility and value-added products. Another practical factor is net positive suction head. If the product is warm, volatile, or supplied from a poorly designed suction line, cavitation risk rises. That can reduce capacity, damage internal surfaces, and create noisy, unstable operation. In brownfield retrofits, especially in older Midwest plants, suction-side design problems are often more important than the pump model itself. Clean-in-place performance is now central to pump purchasing. A pump that requires frequent disassembly, long manual washdowns, or inconsistent sanitation verification can erase any savings from a lower purchase price. U.S. plants facing labor constraints and tighter sanitation documentation increasingly prefer pumps that integrate cleanly into automated CIP programs. When evaluating CIP compatibility, ask whether the pump can handle cleaning chemistry, flow velocity, temperature swings, and return conditions. Also confirm whether the pump is fully drainable, whether seals tolerate caustic and acid exposure, and whether the pump can be cleaned at the same velocities as the rest of the line. This table matters because CIP success is both a hygienic and operational issue. In facilities running multiple allergens or quick product changeovers, a pump that cleans predictably can increase available production time. By 2026, more processors are expected to adopt data-driven CIP optimization. That includes conductivity tracking, temperature verification, valve sequencing logic, and recipe-controlled cleaning through SCADA systems. This reduces water, chemical, and energy consumption while improving repeatability. Those gains are especially valuable in water-stressed regions such as California and Arizona, where sustainability targets are increasingly tied to capital decisions. The area chart illustrates the shift toward pumps selected not only for transfer duty but also for their role in automated cleanability, utility reduction, and sanitation data capture. Seals and elastomers are small components with outsized consequences. Many pump issues blamed on design are really caused by incorrect material selection. If the seal faces are not suited to product abrasiveness, or if elastomers are not compatible with oils, acids, caustic, temperature, or steam exposure, failure rates increase quickly. Common elastomer choices include EPDM, FKM, HNBR, and PTFE-based options. EPDM often performs well in hot water and many CIP environments. FKM can be preferred for certain oils and temperatures. HNBR may suit some wear-focused applications. PTFE can offer broad chemical resistance but may not always be the best choice for every dynamic seal arrangement. Actual selection should always match the product and cleaning profile. Double mechanical seals may be needed in applications with higher pressure, challenging product conditions, or where extra leak protection is desired. Flush plans and barrier fluids should be considered as part of the system, not as an afterthought. The key lesson from this table is that there is no universal best elastomer. The right selection depends on product chemistry, CIP routine, operating temperature, pressure cycling, and maintenance discipline. In high-acid beverages, cultured dairy, and flavored oil systems, material review should happen early in the design phase. This is one area where involving process, sanitation, and maintenance teams together can prevent months of recurring downtime. Even the best food-grade pump can perform poorly if it is installed incorrectly. Pump reliability is heavily influenced by suction conditions, line routing, support, valve placement, instrumentation, and control philosophy. Many chronic issues in U.S. plants come from piping integration mistakes rather than defective equipment. Good installation starts with a clear understanding of the process sequence. Is the pump feeding a filler, a heat exchanger, a homogenizer, a filter, a cooker, or a tank farm? Is the line batch-based or continuous? Are there frequent startups and shutdowns? Does the product foam, settle, separate, or crystallize? Each answer changes how the pump should be integrated. For example, a centrifugal pump in a beverage plant near Tampa handling deaerated product may need careful control to avoid entrained air issues. A protein slurry line in Omaha may need wider bends, robust supports, and attention to solids settling. A syrup transfer skid in New Jersey may need instrumentation for both viscosity-sensitive transfer and documented CIP performance. This table shows why pump installation should be treated as a process engineering task, not just a mechanical hookup. In capital projects, upstream and downstream integration often determine whether the pump adds flexibility or becomes a bottleneck. For companies expanding across multiple sites in the United States, standard details for hygienic skid layout, valve matrices, VFD programming, and CIP interfaces can significantly improve startup speed and maintenance consistency. The comparison chart offers a simplified view of relative fit across major pump categories. It is not a substitute for engineering review, but it helps explain why twin-screw and rotary lobe pumps are increasingly considered for flexible food plants. Food pump maintenance should combine preventive practices, operator awareness, and root-cause troubleshooting. Too often, plants replace seals or impellers repeatedly without solving the real issue, which may be cavitation, dry running, improper cleaning chemistry, misalignment, or uncontrolled speed changes. Strong maintenance programs in U.S. food plants usually include spare parts rationalization, operator startup checks, vibration and temperature monitoring where justified, and documented sanitation inspection. Facilities with high SKU counts and frequent changeovers particularly benefit from standard operating procedures that link production, sanitation, and maintenance tasks. The table above is useful for daily troubleshooting because it links visible symptoms to likely process causes. This reduces the risk of replacing parts without fixing the underlying condition. Maintenance best practices include keeping verified seal kits in stock, documenting elastomer changes by product family, training sanitation teams on visual inspection points, and reviewing pump performance after process changes. If a plant adds a new thick sauce, allergen, or fruit inclusion, the pump should be reassessed rather than assumed to remain suitable. Plants modernizing for 2026 are also moving toward condition-based maintenance. With better controls and SCADA visibility, pump run hours, pressure trends, cleaning cycle data, and alarm history can be tracked to predict failures before they affect production. Choosing a pump is often part of a much larger processing decision. That is where Disruptive Process Solutions can add value. Rather than approaching pumps as stand-alone purchases, DPS evaluates how the equipment fits into the profitability, sanitation, capacity, and long-term operating model of the plant. On the technological side, DPS supports food and beverage manufacturers across the United States and Canada with process engineering, utilities integration, controls, PLC programming, automation, and SCADA. That broader capability matters because pump performance is shaped by the full system around it, including recipe control, CIP sequencing, tank logic, heat treatment, filtration, batching, and downstream packaging. Companies looking for an integrated project partner can learn more about these capabilities on the food and beverage engineering services page. On the manufacturing side, DPS also develops and supplies its own process equipment, including tanks, custom CIP systems, marination tumblers, and cooking vessels. That practical manufacturing experience helps when pump decisions must align with vessel geometry, agitation strategy, utility loads, sanitary access, and skid layout. More information on available systems and equipment can be found on the process equipment solutions page. On the service side, DPS operates through a design-build-manage model that covers planning, engineering, installation, integration, and project oversight. For food processors expanding a dairy line in the Midwest, building an RTD beverage site in the Southeast, upgrading protein capacity in Texas, or improving sanitation systems on the West Coast, that full-scope approach reduces handoff risk. DPS works across processing environments that include dairy, beverages, sauces, proteins, aseptic systems, and prepared foods. You can review the team’s background on the about our company page and see examples of execution on the project case studies page. What separates DPS in practice is a business-first mindset. The company is known for evaluating whether the proposed capital spend actually solves the problem. In some cases, the right answer is a pump upgrade. In others, it may be controls optimization, line balancing, utility redesign, or a different sanitary strategy. For U.S. manufacturers under margin pressure, that kind of honest evaluation is often more valuable than simply buying more equipment. What is the best pump for food processing?There is no single best pump. For thin liquids, centrifugal pumps are often the first choice. For viscous, delicate, or particulate products, rotary lobe, twin-screw, circumferential piston, or progressive cavity pumps may be more suitable. What material should a food-grade pump use?Most sanitary food applications in the United States use 316L stainless steel for wetted parts, along with compliant elastomers and hygienic fittings. Final material selection should match product chemistry and cleaning requirements. When should I choose a positive displacement pump?Choose a positive displacement pump when the product is thick, shear-sensitive, contains particles, or requires more stable flow under varying pressure conditions. Can one pump handle both product transfer and CIP?In some cases, yes. Twin-screw pumps are increasingly selected for dual-duty service, but the application must be engineered carefully to ensure performance in both modes. How important is CIP compatibility?It is critical. CIP compatibility affects sanitation results, labor, downtime, chemical usage, and audit confidence. It should be evaluated at the same level as flow and pressure. What causes repeated seal failures in food pumps?Common causes include wrong elastomer selection, dry running, cavitation, piping strain, poor alignment, abrasive product, and exposure to incompatible cleaning chemicals. Do I need a VFD on a hygienic pump?Often yes, especially where flow flexibility, product protection, energy savings, or controlled startup is important. VFDs are common in modern U.S. food and beverage facilities. How do 2026 trends affect pump selection?Future-ready pump selection increasingly includes sanitation data, automation integration, lower water and chemical use, energy efficiency, stronger traceability, and flexibility for new products and cleaning regimes. What local factors matter in the United States?Utilities, labor, sanitation standards, wastewater limits, plant age, and logistics all matter. A facility near the Port of Los Angeles may prioritize rapid throughput and expansion, while a Midwest dairy may focus on CIP repeatability and cold-product handling. Should pump selection be done by purchasing alone?No. The best outcomes come from collaboration among process engineering, maintenance, sanitation, operations, and quality teams. Pump choice affects all of them. In summary, food plant pump selection should never be reduced to horsepower and pipe size alone. The right decision balances sanitary design, product behavior, cleanability, seal compatibility, installation quality, and future operational flexibility. For manufacturers in the United States, especially those planning 2026 upgrades in dairy, beverage, protein, prepared food, or aseptic processing, the most successful projects treat the pump as part of a complete process system. -
Food Plant Automation Services
Food plant automation in the United States now goes far beyond wiring controls to a single line. Modern projects connect field devices, PLCs, SCADA, recipe and batch systems, maintenance software, quality records, production planning tools, and ERP platforms so plant leaders can run safer, faster, and more profitable operations. For processors in Chicago, Fresno, Dallas, Charlotte, Omaha, Atlanta, Los Angeles, and near logistics hubs such as the Port of Savannah, Port of Long Beach, and Port of Houston, automation has become a strategic capital decision rather than a narrow controls upgrade. Whether the facility produces proteins, sauces, dairy, ready-to-drink beverages, plant-based foods, shelf-stable meals, or aseptic products, the best automation programs align operations, food safety, maintenance, and finance. In practice, that means better visibility into downtime, digital HACCP records, faster changeovers, tighter utility control, and cleaner data flowing from the plant floor into business systems. For U.S. processors dealing with labor constraints, retailer scorecards, USDA or FDA scrutiny, and margin pressure, automation is increasingly tied to survival as much as growth. At a project level, buyers should think about automation as part of the entire production system: equipment, utilities, sanitation, controls, commissioning, training, and long-term support. That is where an integrated engineering partner adds value. Disruptive Process Solutions supports food and beverage manufacturers across North America with a design-build-manage approach that links process engineering, installation, controls, and project execution into one accountable delivery model. Food plant automation services typically cover instrumentation, control panels, PLC programming, operator interfaces, SCADA visualization, batch and recipe control, historian data capture, alarm management, traceability, maintenance integration, quality documentation, utility monitoring, and ERP connectivity. In U.S. food manufacturing, the highest-value automation projects usually target three outcomes first: reduced downtime, stronger food safety compliance, and better production planning. For most plants, the quick buying answer is this: start with the bottleneck line, connect critical assets and quality points, digitize the records that create the most labor or compliance risk, and then scale plantwide after proving ROI. A successful project should fit the sanitation environment, support HACCP plans, integrate with existing equipment, and give both operators and management usable information rather than more screens with no action path. The table above shows why automation projects should be defined by business outcome, not just by hardware scope. Plants that begin with a clear operational target generally see faster payback and fewer integration surprises. Automation in a food or beverage plant begins at the device level. This includes temperature transmitters, pressure sensors, conductivity probes for CIP, flowmeters, level sensors, load cells, valve position feedback, vision systems, safety devices, and motor controls. In hygienic production, these devices must survive washdown, temperature swings, and chemical exposure while still delivering reliable data. From there, signals move into local control hardware, usually PLCs and remote I/O. The control layer manages pumps, valves, conveyors, mixers, cookers, kettles, retorts, pasteurizers, packaging machines, batching skids, and utility systems. Above that, HMI and SCADA platforms allow operators and supervisors to see line status, alarms, trends, sanitation sequences, and production counts. The next level covers manufacturing execution and business integration. That may include batch genealogy, electronic work instructions, material usage tracking, shift dashboards, OEE reporting, lot traceability, maintenance triggers, and production scheduling. ERP integration then connects actual plant activity with purchasing, inventory, costing, and order fulfillment. This matters especially for manufacturers serving national distribution through Memphis, Kansas City, Inland Empire distribution corridors, and major refrigerated networks across the Southeast and Midwest. In practical terms, food plant automation covers these product and process types: This structure helps buyers evaluate vendors. If a supplier only handles controls panels but cannot address traceability, sanitation logic, or ERP connectivity, the plant may still need multiple contractors and extra coordination risk. The most useful way to explain plant automation to executives is the three-layer model. Layer one is machine control. Layer two is plant visibility. Layer three is production and business execution. This model works well for single-site processors and national manufacturers alike. Layer one: PLCs and machine control. This is where real-time actions happen. A PLC starts pumps, stops conveyors, opens mix valves, confirms thermal setpoints, controls retort sequences, and manages sanitation interlocks. In food processing, the logic has to protect both product quality and food safety. That means handling permissives, clean/dirty states, recipe parameters, and emergency stop behavior correctly. Layer two: HMI and SCADA. Here operators interact with the system. HMIs on the line support start, stop, recipe selection, and fault acknowledgment. SCADA typically gives supervisors a wider view of tanks, utilities, packaging lines, environmental alarms, and sanitation progress. Good SCADA design reduces alarm flooding and makes root cause analysis easier. Plants in labor-tight markets such as North Carolina, Texas, and California especially benefit because fewer experienced operators can still manage more complexity with better visibility. Layer three: MES and ERP. MES converts production activity into business-ready information. It tracks what was made, when, by whom, from which ingredients, on which equipment, and with what performance result. ERP then uses that information for inventory transactions, scheduling, costing, procurement, and order management. The biggest gains come when actual runtime, waste, and output are trusted enough to drive planning decisions. DPS brings strong technological capabilities to this layer model, including controls engineering, PLC programming, SCADA development, utility integration, and complete system commissioning. That matters because food plants rarely need isolated software. They need controls that match the physical process, the sanitation design, and the commercial objective. The explanation behind this table is simple: each layer serves a different purpose, and problems occur when companies ask one layer to do the job of another. For example, a PLC should not become the plant historian, and ERP should not substitute for real-time production logic. Industry 4.0 in food manufacturing is not about adding trendy dashboards. It is about creating a connected operating environment where maintenance, production, quality, and finance all work from the same source of truth. When CMMS, MES, ERP, and SCADA are integrated correctly, the plant gains a measurable advantage. SCADA provides live status. MES translates live signals into production events. CMMS uses runtime, cycles, or fault patterns to trigger work orders and preventive maintenance. ERP receives actual material usage and output, improving planning and cost visibility. The result is fewer surprises, better traceability, and stronger capital allocation. For example, a beverage plant near Charlotte serving East Coast retail may use SCADA to monitor syrup room temperatures and filler states, MES to log lot genealogy and line performance, CMMS to schedule maintenance on pumps and heat exchangers based on actual use, and ERP to close work orders and reconcile ingredient inventories. A protein processor in Kansas may use similar logic for smokehouses, grinders, slicers, and packaging assets. From a manufacturing capability standpoint, DPS supports complete processing systems that include tanks, CIP skids, cooking vessels, process utilities, blending and batching systems, thermal systems, and automation-ready equipment integration. Because processing hardware and automation are tightly linked, this full-scope capability is especially useful when retrofitting existing plants or scaling a greenfield site. For buyers, the key question is not whether to connect systems, but in what sequence. Plants with limited internal IT/OT resources should begin with reliable data collection and event definitions before attempting advanced AI or enterprise reporting. Good Industry 4.0 begins with disciplined tagging, naming, role-based dashboards, and cybersecurity governance. Three automation areas consistently produce fast value in the U.S. market. 1. Digital monitoring. This includes line states, asset utilization, utility usage, critical temperatures, pressure trends, CIP verification, and downtime codes. Digital monitoring replaces whiteboards and manual log sheets with time-stamped records. It also allows management to compare shifts, products, or facilities without waiting for month-end reports. 2. HACCP compliance. Food safety records remain one of the biggest drivers for automation in regulated environments. Digital CCP and preventive control records reduce paper handling, strengthen audit readiness, and speed investigations. For FDA-regulated and USDA-inspected plants, automated exception alerts can reduce the risk of missed checks or undocumented deviations. 3. Production planning. Once output, downtime, and changeover data are captured accurately, schedulers can create more realistic plans. Plants often discover that nominal line rates do not match actual sustained rates. With better data, planners can reduce overtime, prioritize profitable SKUs, and coordinate labor and sanitation windows more effectively. The reason these areas work so well is that they combine operational need with manageable scope. Plants do not need a full digital transformation on day one to get measurable value. Automation investments are approved when the financial case is clear. In many food and beverage facilities, realistic ROI comes from five sources: reduced downtime, improved OEE, lower giveaway, less manual record labor, and fewer quality or compliance deviations. A common mid-range result after targeted implementation is a 23% drop in downtime and an 18% improvement in OEE on the constrained asset or line, especially when root-cause coding and response workflows are included. Consider a prepared foods line in the Midwest running two shifts. If it loses 11 hours per week to minor stops, waiting, and untracked changeover delays, even modest automation can recover sellable capacity. If the line supports retailer distribution into Chicago, St. Louis, and Minneapolis, recovered output may prevent outsourced production or delayed shipments. In beverage, syrup room automation and filler performance visibility can reduce flavor changeover losses and improve first-pass quality. The biggest mistake in ROI models is using only labor savings. Most food processors gain more from capacity recovery, reduced scrap, better scheduling, and avoided capital spending than from headcount reduction alone. The table demonstrates that automation should be tied to baseline data before approval. A plant that cannot define its current losses will struggle to validate the return after deployment. In food plants, automation hardware must fit the sanitation environment. Hygienic design is not optional. Enclosures, sensors, cable glands, touchscreens, pushbuttons, and junction boxes should be selected based on washdown intensity, chemicals, temperature, and installation location. In U.S. facilities, IP69K or washdown-rated components may be needed in high-moisture protein, dairy, and beverage environments, while drier packaging zones may allow different specifications. Beyond the IP rating itself, buyers should review sloped surfaces, cleanable mounting methods, stainless construction, sealed cable management, and the avoidance of harborage points. Poor controls cabinet placement can create sanitation headaches and shorten equipment life. Hygienic design should also align with plant airflow, drainage, and personnel movement. DPS supports these projects with service capabilities that extend beyond controls alone: process engineering, capital planning, owner’s representation, project management, installation oversight, commissioning, and integration across utilities, equipment, and automation. That broader execution model is important because hygienic compliance often depends on mechanical, electrical, and process decisions being coordinated from the start. This table matters because the wrong enclosure or sensor choice can undermine the entire project. Hardware selection should follow sanitary zoning, not simply catalog price. The most successful automation programs in U.S. food manufacturing follow a staged roadmap. For U.S. buyers, pilot projects are often best scheduled around seasonal demand windows. A sauce plant in New Jersey or a beverage site in Southern California may have limited outage opportunities, while dairy and protein plants may need phased work around sanitation and inspection routines. Companies exploring full-scope project partners can review engineering and integration services to understand how process, controls, and execution can be aligned from concept to commissioning. Integration challenges are common, especially in brownfield plants. Legacy PLCs, undocumented code, mixed OEM equipment, unstructured tag naming, poor network segmentation, and inconsistent operator practices can slow the project. Many facilities also underestimate change management. A technically sound system will still underperform if supervisors, maintenance, QA, and operators do not use it consistently. Key challenges and responses include: One reason full-scope partners are increasingly preferred is that automation rarely stands alone. It touches utility loads, process sequencing, panel locations, equipment layout, startup planning, and sanitation procedures. Buyers looking at integrated equipment and plant systems can also review process equipment capabilities when evaluating how automation fits a broader capital project. A practical U.S. case pattern is worth noting. Some processors assume they need a multimillion-dollar expansion to increase output, when the actual bottleneck is controls logic, sequencing, or line balance. In one example similar to many brownfield plants, throughput increased materially after PLC reprogramming and controls optimization, avoiding unnecessary capital expansion. Additional real-world project examples can be explored through industry case studies. Looking toward 2026, future trends in U.S. food plant automation will include stronger energy analytics, wider use of AI-assisted maintenance prioritization, tighter digital traceability expectations from retailers, greater water and utility monitoring for sustainability reporting, and deeper integration between environmental compliance and production systems. Policy and customer pressure will likely push more plants to document emissions intensity, water usage per unit, and sanitation resource consumption alongside traditional output metrics. Plants that build a clean, connected automation architecture now will be better prepared for those requirements. What types of U.S. food companies benefit most from automation?Mid-sized and enterprise manufacturers typically see the fastest returns, especially in protein, dairy, beverages, prepared foods, sauces, aseptic, and co-packing operations. However, smaller high-growth plants can also benefit when labor, traceability, or scheduling complexity is rising. Should a plant start with SCADA, MES, or ERP integration?Usually start by stabilizing the control and visibility layers first. Reliable PLC and SCADA data should come before complex MES or ERP integrations. Without trusted floor data, enterprise reporting becomes misleading. How long does a pilot automation project take?A focused pilot may take 8 to 20 weeks depending on hardware lead times, outage windows, software complexity, and validation needs. Brownfield upgrades often take longer because of discovery and compatibility issues. What is the best first application for food safety digitization?Critical control point monitoring, thermal process records, CIP verification, and electronic sanitation or quality checks are common starting points because they reduce paper burden and strengthen audit readiness. Do all plants need MES?No. Some plants can gain major value from SCADA, historian, OEE dashboards, and limited transaction links first. MES becomes more important when recipe control, lot traceability, multi-line scheduling, and work-in-process visibility become operational priorities. How do I compare suppliers?Compare them on food industry knowledge, hygienic design experience, PLC and SCADA depth, utility and process understanding, commissioning support, documentation quality, cybersecurity awareness, and ability to coordinate mechanical, electrical, and process scope. Why does full-scope integration matter?Because line performance depends on more than code. Utilities, CIP, equipment layout, piping, electrical distribution, operator workflows, and startup discipline all affect automation results. A partner that understands the full process can reduce costly handoff gaps. Can automation help avoid unnecessary capital expansion?Yes. In some plants, poor controls, sequencing, or scheduling create hidden bottlenecks. Fixing those issues may recover enough capacity to delay or reduce new equipment spending. What should buyers in the United States ask during vendor selection?Ask for food-specific case history, validation and startup approach, sanitation hardware standards, brownfield integration experience, support model, project governance, and the expected path from pilot to scale. Who is a strong fit for a partner like DPS?Manufacturers that want a practical, business-focused partner for profitable capital execution, especially when the project spans process engineering, equipment integration, utilities, automation, and rollout management across U.S. facilities. -
Food Facility Spare Parts Management System
Food and beverage manufacturers in the United States cannot treat spare parts as an afterthought. A modern food facility spare parts management system is a profit protection tool that reduces downtime, protects food safety, shortens recovery time after failures, and improves capital planning. For plants running fillers, pasteurizers, pumps, mixers, conveyors, refrigeration systems, boilers, CIP skids, PLC-based controls, and packaging lines, the best approach is to identify critical assets, classify parts by risk and lead time, stock what would stop production, and build supplier and emergency procurement pathways before a breakdown occurs. Across U.S. manufacturing hubs such as Chicago, Atlanta, Dallas, Charlotte, Fresno, Milwaukee, Houston, and the Inland Empire, plant leaders are under pressure to do more with less labor, tighter sanitation standards, and volatile lead times. Imported components that once moved predictably through the Ports of Los Angeles, Long Beach, Savannah, Houston, New York and New Jersey, and Seattle can now face swings in transit time, customs clearance, and domestic freight availability. That is why spare parts planning has become an operating discipline, not just a storeroom function. The fastest way to improve spare parts performance in a U.S. food plant is to build a structured program around five actions: rank equipment criticality, define minimum and maximum stock levels, standardize part numbers and descriptions, qualify primary and backup suppliers, and connect replacement schedules to preventive maintenance and actual run hours. This helps processors avoid the two most expensive mistakes in spare parts management: carrying too much low-value inventory and carrying too little of the parts that can shut down a line. For example, a poultry processor in Arkansas, a dairy plant in Wisconsin, and a beverage co-packer in North Carolina may all use very different process technologies, but they share the same spare parts logic. Bearings, motors, seals, VFDs, photoeyes, valve seats, gaskets, sensors, pump components, gearbox kits, control cards, and sanitary fittings should not be purchased reactively. They should be mapped to the asset, criticality, sanitation requirements, shelf life, storage conditions, and procurement risk. In the United States market, spare parts planning also needs to reflect regional realities. Gulf Coast hurricane exposure affects inventory risk in Houston and New Orleans. West Coast port congestion can affect imported OEM components used in California and Nevada facilities. Midwest cold chain facilities may face winter transport delays. East Coast plants drawing parts from European suppliers often route through Savannah or Newark, increasing sensitivity to marine freight schedules. A good program translates these market realities into stocking policy. The table above shows why not all parts deserve the same stocking policy. The key is to align inventory depth with business impact, replacement complexity, and lead-time risk. The line chart reflects a realistic market direction: U.S. plants are steadily increasing investment in digital inventory planning, asset visibility, and maintenance-linked procurement. This is expected to accelerate in 2026 as automation labor shortages and resilience planning become stronger board-level priorities. Critical spare parts inventory planning starts with asset criticality, not with the storeroom shelf. Every facility should create a ranked asset register covering process equipment, utilities, packaging systems, and controls infrastructure. In food and beverage plants, the most overlooked assets are often utility systems that support the line indirectly: boilers, air compressors, glycol systems, refrigeration skids, water treatment units, CIP skids, and electrical distribution gear. If one of these fails, multiple production lines may go down at once. A practical planning model uses four factors: downtime cost per hour, replacement lead time, failure frequency, and food safety exposure. If a homogenizer seal kit has a short lead time and low outage impact, it may require only a small buffer. If a custom aseptic filler component comes from Europe with a 16-week lead time, it may justify on-site stocking even if it fails rarely. Plants should also split inventory by product type. Common spare categories in U.S. food facilities include: Buying advice for U.S. operators is straightforward: do not assume OEM-only stocking is always best. For standardized items such as bearings, common motors, sanitary fittings, and electrical consumables, approved alternates from domestic distributors can reduce cost and shorten lead times. For highly specialized control boards, software-bound components, proprietary filling parts, and validated aseptic hardware, stay close to the OEM and document revision compatibility carefully. This table shows that stock decisions should follow business risk, not just unit price. A low-cost sensor can stop a high-value line; a high-cost component may not need stocking if it is easy to source locally. For processors looking to align spare parts planning with expansion or line redesign, it helps to involve engineering during capital project development. Firms such as Disruptive Process Solutions support manufacturers by integrating maintainability, utility reliability, and equipment access into project planning so plants are not left solving spare parts issues after startup. Classification and coding are the backbone of a scalable spare parts management system. Many U.S. food plants have duplicate inventory because the same item is stored under different names: “2 in sanitary gasket,” “2-inch gasket,” and “tri-clamp seal 2in” may all refer to the same part. Without disciplined coding, plants overbuy, lose visibility, and fail to locate parts during emergencies. The best coding model includes six data elements: part family, equipment tag, manufacturer, OEM part number, approved alternate, and storage requirements. For sanitary and product-contact components, include material grade and compliance notes. For electrical and automation parts, include firmware or revision level where relevant. A strong classification structure for the United States market should also identify domestic versus imported sourcing, because this affects lead-time exposure. Parts moving through Memphis or Louisville air cargo networks may be recoverable in 24 to 48 hours, while containerized imports routed through Long Beach or Savannah may carry much longer variability. The table above is useful because it ties the item code to practical retrieval and quality requirements. A part number should not just identify what the part is; it should help someone find, verify, and install it correctly during a time-sensitive repair. Classification should also serve different industries and applications. Beverage plants often need faster turnover on fillers, depalletizers, labelers, and carbonation systems. Protein processors may need deeper spares around grinders, slicers, conveyors, metal detection, and refrigeration. Dairy plants face more sanitary valve and pump wear. Aseptic and retort operations require higher control over validated components and documented change management. The bar chart shows how spare parts demand intensity varies by industry. Protein and beverage operations often carry heavier spare requirements because uptime sensitivity, sanitation cycles, and line speed are especially demanding. Supplier management is where many spare parts programs succeed or fail. Plants need more than a vendor list; they need a supplier strategy based on criticality, geography, response speed, and technical support. A strong supplier portfolio generally includes the OEM, at least one qualified distributor, one fabrication or machine shop resource for custom parts, and an emergency logistics path for same-day or next-flight-out needs. Local supplier networks matter. Facilities in California may source quickly from Orange County, Los Angeles, and the Central Valley. Midwest plants often benefit from strong industrial distribution in Chicago, Milwaukee, Indianapolis, and Minneapolis. Southeast processors can tap Atlanta, Charlotte, Greenville, and Jacksonville. Gulf Coast plants may rely on Houston’s broad MRO market and port-linked import channels. Lead time management should be data-driven. Every stocked part should carry an average lead time, a worst-case lead time, and a last-confirmed date from the supplier. If a supplier quoted six weeks in 2023, that number may no longer be valid in 2025 or 2026. Trade policy shifts, reshoring activity, semiconductor constraints, and sustainability reporting requirements are all influencing supplier performance. This table is important because it matches supplier type to the role it should play. Plants that rely on a single vendor for every part usually discover the weakness of that model only during a crisis. One practical buying recommendation is to ask suppliers for branch inventory visibility. A part that is unavailable in St. Louis may be in stock in Phoenix or Newark. Another is to maintain quote-ready documentation for fabricated parts, including dimensions, material specifications, finish requirements, and photos. That shortens emergency sourcing dramatically. For larger manufacturers expanding lines or relocating equipment, a project partner with both engineering and execution experience can strengthen the supplier plan. Through its design-build-manage approach, DPS project case experience reflects how early vendor coordination, utility planning, and equipment integration can reduce future spare parts exposure after startup. Good inventory control is not just software. It combines transaction discipline, physical organization, and storage conditions that preserve part quality. In food facilities, poor storage can ruin gaskets, electronics, lubricants, sensors, and calibration-sensitive instruments long before they are installed. A strong storeroom setup typically uses location coding by aisle, rack, shelf, and bin; barcode or QR scanning; cycle counts; and separate control for food-contact components. Critical automation parts should be stored in clean, dry, climate-controlled cabinets. Elastomers should be protected from heat, UV exposure, and compression damage. Stainless components should be isolated from carbon steel contamination when necessary. Plants should also decide whether to centralize inventory or place point-of-use spares near lines. A hybrid model works best in many U.S. plants: keep high-value critical items centrally secured, but place commonly used wear items near major production zones. This reduces wrench time and speeds restoration without losing accountability. The table demonstrates that one storage method will not fit every part family. The best systems combine security, speed, and preservation. Technology also matters. Facilities increasingly connect CMMS, ERP, and procurement tools so parts usage updates reorder points automatically. In 2026, expect stronger adoption of AI-assisted forecasting, digital twins for failure prediction, and image-based inventory verification. Policy trends around traceability and supply chain transparency may also push processors to keep cleaner records for critical food-contact components. The area chart highlights a healthy trend shift: as planning maturity improves, the share of spend tied to planned purchasing rises while emergency buying falls. This is one of the clearest indicators that a spare parts system is working. Replacement scheduling should connect preventive maintenance, predictive indicators, and actual operating conditions. Time-based replacement alone is often too blunt. A filler star wheel may wear according to throughput and container type. A pump seal may fail based on cleaning chemistry, temperature swings, and operator handling. A VFD cooling fan may fail according to ambient conditions rather than calendar age. Best practice is to segment parts into three replacement models: scheduled replacement, condition-based replacement, and run-to-failure. Product-contact seals, valve kits, and certain calibration-sensitive instruments usually fit scheduled replacement. Bearings, motors, and drives often benefit from vibration, temperature, or performance-based monitoring. Low-cost noncritical items may be allowed to run to failure if they do not threaten food safety or line uptime. Scheduling should also support shutdown planning. Many U.S. plants only get limited maintenance windows around weekends, holidays, or seasonal demand dips. Building a shut list 60 to 90 days ahead allows buyers to confirm stock, engineering to review scope, and suppliers to reserve material. This is especially important for summer beverage peaks, holiday protein surges, and dairy seasonality. Application matters by industry. Breweries need attention on packaging line wear parts, glycol system reliability, and control components. Meat and poultry plants need durable plans for blades, conveyors, refrigeration, and sanitary washdown-sensitive parts. Prepared foods operations need mixing, cooking, heat transfer, and packaging spares aligned to recipe changeovers and allergen cleanouts. On the technology side, processors gain value when equipment, controls, and utilities are considered together. DPS supports manufacturers with process, mechanical, electrical, structural, plumbing, and controls expertise, including PLC programming and SCADA integration, which is important because replacement scheduling is strongest when it reflects how assets actually operate as a system rather than as isolated machines. Even the best system will face emergencies. The goal is not to eliminate emergency procurement; it is to control it. Every plant should have a written emergency procurement protocol with named decision makers, spending thresholds, supplier contacts, freight contacts, approval paths, and installation readiness steps. A strong protocol answers practical questions in advance. Who can authorize a premium freight move at 2:00 a.m.? Who verifies part compatibility before purchase? Which supplier branches can open after hours? Is the receiving team prepared for weekend intake? Does maintenance have lifting gear, permits, and lockout resources ready when the part arrives? Plants should also define what counts as an emergency. If a part is urgently needed because the min-max policy failed, that is a planning issue, not a true emergency. A true emergency usually involves unpredictable failure, safety exposure, or a commercial event that justifies extraordinary cost. For facilities operating multi-state networks, regional spare sharing can be powerful. A company with sites in Texas, Ohio, and California may hold one critical OEM drive at each location and allow emergency transfer within the network. That approach often beats overstocking every site independently. Local supplier knowledge makes a difference here. Same-day courier access in Chicago or Atlanta can be a major advantage. Air freight out of Louisville, Memphis, or Dallas-Fort Worth can shorten response times. Plants near major ports may have more inbound flexibility for imports, but they should still assume risk around customs and drayage timing. Cost optimization does not mean minimizing inventory value at all costs. It means deploying inventory where it protects margin, while reducing hidden waste such as obsolete stock, duplicate SKUs, premium freight, emergency overtime, and line downtime. The true cost of a spare part is not its purchase price; it is the total cost of not having it when needed and the total cost of holding it unnecessarily. Start budget planning with an annual spare parts review by line, utility system, and asset family. Separate budget categories into preventive stock, shutdown stock, project stock, and emergency reserve. This gives leadership a clearer view of where money supports reliability and where it merely reacts to instability. One useful method is ABC-criticality analysis. A-items are high-value or high-risk parts requiring closer control. B-items are moderate-value recurring items. C-items are low-value frequent-use consumables. But in food manufacturing, also apply an “R” overlay for regulatory or sanitation significance. A low-cost gasket can still be an A-R item if it protects product integrity. This table matters because it connects inventory decisions to actual financial outcomes. Senior leaders often support spare parts initiatives more quickly when they can see how storeroom discipline affects throughput, labor, freight, and working capital. The comparison chart shows a realistic tradeoff: OEM sources often score highest on fit and support but lower on cost efficiency, while plant-to-plant transfer and local fabrication can be highly effective when properly governed. By 2026, cost planning will also be shaped by sustainability and policy expectations. More processors are evaluating energy use, material life, repairability, and domestic sourcing resilience when approving parts strategies. In some cases, a longer-life component with higher upfront price will be the better budget choice because it reduces changeouts, waste, and sanitation disruptions. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a practical, business-first approach to processing and utility projects. Rather than viewing spare parts only as maintenance inventory, DPS sees them as part of a broader reliability and profitability strategy that should be considered during design, installation, and startup. From a technological capability standpoint, DPS works across process, mechanical, electrical, plumbing, structural, and controls disciplines. That includes PLC programming, automation, SCADA integration, utility coordination, and processing system design for everything from fermentation and blending to pasteurization, aseptic applications, retort systems, refrigeration support, and CIP infrastructure. This matters for spare parts planning because a complete asset view improves criticality ranking, startup spare identification, and future replacement scheduling. From a manufacturing capability standpoint, DPS also brings equipment knowledge through its branded process equipment offerings, including tanks, CIP systems, marination tumblers, and cooking vessels. For processors evaluating in-house fabrication potential, OEM dependence, or maintainability standards, that equipment perspective helps create better spare packages, documentation sets, and commissioning handoffs. You can learn more about its equipment focus at process equipment solutions. From a service capability standpoint, DPS provides engineering, capital planning, owner’s representation, project and program management, system integration, installation oversight, and general contracting support where licensed. Its design-build-manage delivery model is especially useful for companies that want reliability planning incorporated into expansions, relocations, line upgrades, or new greenfield developments. More background on the company’s approach is available at the DPS company overview. For food and beverage plants, the value is straightforward: spare parts performance improves when project teams think ahead about access, standardization, controls architecture, utility redundancy, and operator reality. That is where disciplined engineering and disciplined maintenance planning meet. What is the most important first step in building a spare parts management system?Start with asset criticality ranking. If you do not know which failures hurt throughput, food safety, and recovery time the most, you cannot stock intelligently. How often should minimum and maximum levels be reviewed?Critical items should be reviewed monthly. Broader inventory policies are usually reviewed quarterly, with a full annual review tied to shutdowns, budget planning, and equipment changes. Should every food plant use OEM parts only?No. Use OEM parts for proprietary, validated, or revision-sensitive items. For standardized MRO components, approved alternates can reduce cost and improve availability without increasing risk. How do we reduce obsolete inventory?Tie storeroom records to your asset register and capital projects. Every line upgrade, controls migration, or equipment relocation should trigger a spare parts review so old items do not remain in stock unnoticed. What parts are most commonly understocked in U.S. plants?Controls hardware, specialty sensors, sanitary valve kits, heat exchanger gasket sets, and utility system components are frequently understocked because they are not always visible in day-to-day operator attention. What role does CMMS or ERP software play?Software is essential for transaction visibility, reorder logic, and linkage to maintenance work orders, but it only works well when part descriptions, locations, lead times, and equipment tags are clean and current. How should multi-site companies handle critical spares?Use a network strategy. Keep some parts at each site, but identify regional shared spares and transfer rules. This often lowers total inventory while improving coverage. What are the top 2026 trends to watch?AI-assisted forecasting, condition-based replenishment, stronger domestic sourcing strategies, sustainability-driven material choices, and policy pressure for more transparent and resilient supply chains. A food facility spare parts management system is no longer just about shelves, bins, and emergency purchase orders. In the United States, it is a strategic operating framework that connects market realities, product categories, supplier access, maintenance planning, and capital efficiency. Plants that build this capability systematically are better positioned to protect uptime, comply with sanitation expectations, and scale profitably even when supply conditions tighten. -
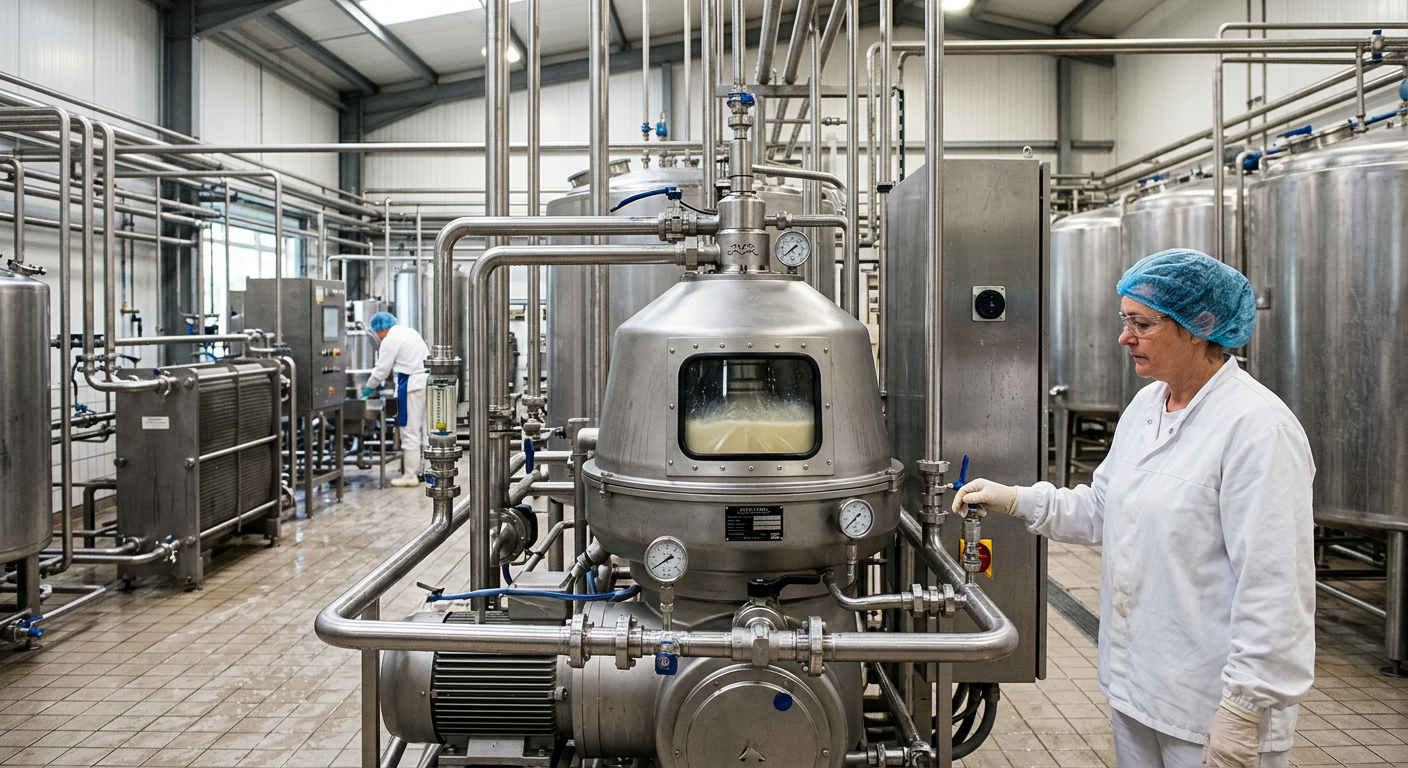
5-Phase Food Plant Equipment Lifecycle Management
Managing food plant equipment over its full useful life is no longer a maintenance-only task in the United States. It is a capital strategy, an operating discipline, and a profitability lever. For processors in hubs such as Chicago, Dallas, Fresno, Charlotte, Omaha, Atlanta, Los Angeles, and the Port of Houston corridor, the best lifecycle programs start before a machine is purchased and continue through commissioning, production optimization, repair decisions, and eventual replacement. When manufacturers connect engineering standards, operator training, sanitation requirements, spare parts planning, and CMMS data into one framework, they reduce downtime, improve food safety, and make smarter reinvestment decisions. In food and beverage plants, lifecycle management applies across mixers, tanks, pumps, pasteurizers, retorts, fillers, conveyors, refrigeration systems, boilers, CIP skids, packaging lines, controls networks, and utility infrastructure. The stakes are high because a poorly specified asset can create years of hidden labor, changeover, sanitation, and energy costs. A well-managed asset, by contrast, supports throughput, compliance, and long-term margin. Food plant equipment lifecycle management is the structured process of planning, buying, installing, operating, maintaining, and replacing production assets to maximize uptime, food safety, and return on capital in the United States. The strongest programs use five practical phases inside a broader business framework: equipment acquisition and specification, installation and commissioning, operational performance monitoring, maintenance and repair optimization, and end-of-life replacement planning. These phases are tied together by total cost of ownership analysis and lifecycle data captured in a CMMS or enterprise asset management system. For U.S. processors, the direct answer is simple: buy only what your process truly needs, commission it correctly, monitor real performance instead of nameplate promises, maintain it with data rather than habit, and replace it based on economics instead of age alone. This approach matters whether you run a poultry facility in Arkansas, a dairy plant in Wisconsin, a beverage co-packer in North Carolina, or a protein line near the rail and cold-chain networks of Kansas City. In practice, lifecycle success depends on several market realities in the United States: The chart above reflects a realistic growth pattern driven by modernization, labor scarcity, retrofit automation, and stronger asset governance. By 2026, many U.S. manufacturers are expected to expand lifecycle management beyond maintenance into engineering, finance, and plant leadership decision-making. The lifecycle of food processing equipment is won or lost at the specification stage. Too many plants still buy around initial price, available floor space, or a favorite vendor relationship. In the United States, that approach often leads to chronic issues: undersized utilities, poor washdown design, limited maintenance access, control system incompatibility, and excessive changeover time. Better acquisition planning begins with business needs. Is the plant chasing capacity, labor reduction, yield, sanitation improvement, SKU flexibility, or geographic expansion? A ready-to-drink line serving Southeast distribution through Atlanta and Savannah has different design priorities than a frozen protein operation feeding the Midwest through Omaha and Minneapolis. The specification must reflect product type, line speed, packaging format, regulatory environment, utility profile, and future expansion needs. Common equipment categories that benefit from lifecycle-based specification include: Buying advice for U.S. processors: evaluate cleanability, spare parts access, controls openness, local service coverage, domestic code alignment, utility consumption, and operator ergonomics before comparing quotes. Also account for freight routing and installation logistics if your plant sits near congested corridors such as Southern California, New Jersey, or the Chicago intermodal region. This table shows why equipment specification must be cross-functional. Engineering, operations, quality, sanitation, finance, and maintenance should all sign off before procurement. That alignment reduces expensive surprises during startup and the first year of operation. Manufacturers looking for a structured front-end approach often benefit from external engineering support that connects process goals to capital scope. A partner with feasibility, utility design, and integration experience can prevent overspending on the wrong asset. For a broader view of project planning and execution support, manufacturers can review food and beverage engineering services that cover design, project management, and capital planning. Installation is where paper assumptions meet field reality. In many U.S. projects, problems arise not because the equipment is poor, but because alignment, piping slope, controls handoff, utility balancing, or operator training were incomplete. A successful commissioning phase is more than “turning it on.” It is the formal proving of mechanical integrity, control logic, safety interlocks, sanitation performance, and process capability. Plants in expanding manufacturing regions such as Texas, Tennessee, and the Carolinas often face compressed schedules and multiple trades working simultaneously. That makes structured commissioning even more important. Every tank, skid, conveyor, valve cluster, and packaging machine should be tested against documented criteria before final acceptance. The table highlights a key point: commissioning is a multi-discipline process, not a single event. It should include operators, maintenance technicians, quality managers, sanitation leads, and automation specialists. If any of these groups are missing, hidden failure points often surface weeks later. For example, a filler installed in a beverage plant near Charlotte may pass a no-load run but fail during sticky, high-sugar production because CIP spray coverage or drain-back behavior was never validated. A retort line in California’s Central Valley may meet throughput targets but create thermal process inconsistencies if steam quality fluctuates under full utility demand. These are lifecycle issues, not isolated startup issues, because weak commissioning creates years of operating penalties. Once an asset is live, the next phase is monitoring what it actually does, not what the brochure said it would do. U.S. processors increasingly use OEE, downtime codes, energy intensity, sanitation cycle time, product giveaway, and maintenance response data to evaluate equipment health and value. The most useful metrics vary by equipment type and application: The chart suggests where lifecycle investment pressure is strongest across U.S. food and beverage sectors. Beverage, protein, and dairy operations often move first because they combine strict quality risk with expensive downtime. This KPI table is valuable because it links numbers to action. Monitoring without defined response thresholds only creates reports. Plants should set review cadences by asset criticality, typically daily for bottleneck lines, weekly for utilities, and monthly for broader capital planning. By 2026, future-ready plants in the United States are expected to deepen performance monitoring with predictive analytics, vibration data, thermal imaging, and historian-driven process alarms. Sustainability policy and customer pressure will also make water use, energy intensity, and wastewater load more visible in asset reviews. Maintenance optimization means choosing the right mix of preventive, predictive, condition-based, and corrective work. In food plants, this balance is complicated by sanitation windows, production variability, allergen segregation, and labor shortages. A robust program does not simply add more PMs. It applies maintenance effort where failure consequences are greatest. Critical assets usually include thermal processing systems, refrigeration, compressed air, CIP, water treatment, primary packaging, control panels, and production bottlenecks. A line may have dozens of minor components, but only a handful truly threaten safety, compliance, or volume if they fail. For buying and operating advice, U.S. plants should ask these questions: This table shows that maintenance optimization is a portfolio decision. Plants should not apply one method to every asset. A centrifugal pump in a noncritical washwater loop may justify a different strategy than a homogenizer feeding a dairy HTST line in Wisconsin or a retort control valve in a shelf-stable operation near Memphis. 2026 trend: more plants will blend predictive maintenance tools with remote support, especially for multi-site manufacturers. However, technology alone will not solve reliability issues if the plant lacks clean downtime data, parts discipline, and standard work for lubrication, inspection, and operator care. End-of-life planning is one of the most misunderstood parts of equipment lifecycle management. Equipment is not “end of life” simply because it is old. In many U.S. plants, a 20-year-old system can still outperform a newer one if it has been well maintained, upgraded intelligently, and matched to the current product mix. Replacement should be based on economics, risk, compliance exposure, and strategic fit. Typical replacement triggers include: The table clarifies that replacement planning should link plant-floor symptoms to business impact. This is especially important in sectors with thin margins and fast growth, such as co-packing, RTD beverages, prepared meals, and protein processing. Case patterns in the U.S. show that many replacement decisions are delayed too long because teams look only at repair invoices, not lost capacity, utility waste, sanitation labor, or customer service risk. A better model is to forecast the next three years of operating burden and compare that with retrofit or replacement options. Total cost of ownership, or TCO, is the financial language that connects engineering decisions to executive approval. In food processing, purchase price usually accounts for only a portion of asset cost. Installation, utilities, water, chemicals, labor, maintenance, downtime, spare parts, validation, and compliance all influence the true cost of an equipment decision. For example, a lower-priced tank system might require more manual cleaning, more operator intervention, and more product loss during changeovers. A more expensive pasteurizer may reduce energy use, improve controls integration, and shorten startup variation. Over five to ten years, the second option may be financially superior. The area chart reflects an important market shift: U.S. food plants are moving away from reactive repair culture and toward data-guided asset ownership. This trend is likely to accelerate in 2026 as ESG reporting, utility cost management, and labor scarcity increase the value of predictable operations. This TCO table explains why procurement decisions should never be made on quote value alone. Strong U.S. manufacturers compare multiple scenarios: new purchase, retrofit, rebuild, used equipment with modifications, and phased modernization. That approach is especially relevant when interest rates, lead times, or utility costs are uncertain. Lifecycle management becomes scalable only when asset data is organized. A CMMS should hold more than work orders. It should connect asset hierarchy, manuals, critical spare parts, PM frequencies, failure codes, lubrication standards, calibration history, sanitation procedures, and cost records. For processors running multiple facilities across the United States, standardizing this structure is a major advantage. It allows a beverage plant in North Carolina, a protein facility in Texas, and a prepared foods site in Illinois to compare similar assets on a common basis. It also supports better capital prioritization at the portfolio level. Best-practice CMMS integration elements include: This comparison chart illustrates a common U.S. buying lesson: the lowest quoted equipment cost may score well on initial price but poorly on support, integration, and long-term value. Lifecycle-focused sourcing often produces stronger business outcomes, especially for systems that touch food safety, automation, or plant bottlenecks. As policy and sustainability reporting evolve in 2026, more plants are expected to track carbon intensity, water consumption, and refrigerant performance at the asset level. CMMS and connected data platforms will become increasingly important for documenting these outcomes and supporting capital requests. Disruptive Process Solutions supports manufacturers across the United States and Canada with a business-first view of engineering and capital execution. Rather than treating equipment as isolated hardware, the company approaches projects as integrated operating systems meant to improve profitability, scalability, and long-term plant performance. From a technological capabilities perspective, DPS works across structural, mechanical, plumbing, electrical, process, and controls engineering. That includes PLC programming, SCADA, batch and recipe control, utility systems, water treatment, thermal processing, aseptic applications, and complete process integration. This breadth matters because lifecycle performance depends on how equipment, controls, and utilities behave together, not separately. From a manufacturing capabilities perspective, DPS supplies and manufactures selected branded process equipment such as tanks, custom CIP systems, marination tumblers, and cooking vessels. That practical equipment knowledge supports stronger specification, cleaner integration, and more realistic commissioning outcomes. Manufacturers exploring available process systems can review food processing equipment solutions to see how asset selection aligns with plant performance goals. From a service capabilities perspective, DPS provides capital planning, feasibility, owner’s representation, project and program management, general contracting support where licensed, and turnkey installation and integration. That model is especially valuable for food and beverage plants that need one team to align engineering intent, field execution, and startup accountability. Companies wanting background on this approach can visit the DPS company overview. In real project environments, this integrated model helps clients avoid costly misalignment between concept, procurement, construction, and production ramp-up. It is well suited to beverage, dairy, protein, aseptic, prepared foods, and co-packing applications, particularly where utilities and automation are as important as the process line itself. What is the biggest mistake in food plant equipment lifecycle management?Focusing only on purchase price. In the United States, downtime, sanitation labor, utility consumption, and controls obsolescence often cost more over time than the original machine quote. How often should equipment be reviewed for replacement?Critical assets should receive an annual repair-versus-replace review, with quarterly monitoring of downtime, repair spend, and capacity constraints. Which industries benefit most from lifecycle management?All food and beverage sectors benefit, but the impact is especially strong in dairy, protein, beverages, prepared foods, aseptic systems, and co-packing operations where uptime and sanitation are tightly linked to margin. Is a CMMS necessary for smaller plants?Yes. Even a smaller plant in regions such as the Midwest, Southeast, or Pacific Coast gains from standardized work orders, spare parts control, and failure history. The system can be simple at first, then expanded. Should plants rebuild old equipment or buy new?It depends on controls support, sanitary design, energy use, and production fit. A rebuild can be the best option when the base asset is mechanically sound and the process requirements remain stable. How do local supplier networks affect lifecycle planning?They matter significantly. Plants near major manufacturing and logistics hubs like Chicago, Dallas-Fort Worth, Los Angeles, Houston, and Charlotte may have faster access to stainless fabricators, electricians, controls support, and emergency parts. Remote plants should account for travel and inventory risk in TCO models. What should be included in a handover package after commissioning?As-built drawings, controls backups, PM schedules, spare parts lists, manuals, sanitation procedures, training records, alarm rationalization, and acceptance test results. How can case studies help with lifecycle decisions?They show how specification, automation upgrades, utility integration, and startup discipline affect long-term value in real plants. For practical examples of integrated project execution, manufacturers can explore project case studies in food and beverage facilities. What are the top 2026 trends in U.S. equipment lifecycle strategy?Predictive maintenance expansion, stronger energy and water tracking, cybersecurity-driven controls modernization, more modular skids, broader use of digital twins for commissioning, and tighter sustainability reporting tied to asset performance. What is the best first step for a plant that wants to improve?Start with an asset criticality ranking, collect twelve months of downtime and repair history, identify the top bottleneck systems, and then build a lifecycle roadmap that combines engineering, maintenance, operations, and finance. Across the United States, from West Coast beverage facilities to Gulf Coast processing hubs and Midwestern protein plants, food equipment lifecycle management is becoming a core business capability. Plants that specify wisely, commission rigorously, monitor honestly, maintain strategically, and replace based on economics will outperform those that simply react. The result is more reliable production, stronger compliance, better capital efficiency, and a plant platform built for 2026 and beyond. -
Food Factory Expansion Feasibility Study
Food manufacturers in the United States often reach a point where demand rises faster than plant capability. At that moment, leadership must decide whether to expand an existing facility, reconfigure production, add utilities, or pursue a new greenfield site. A sound food factory expansion feasibility study reduces capital risk, protects uptime, and ties engineering decisions to actual profit. For operators producing protein, dairy, sauces, ready-to-drink beverages, aseptic products, or contract-packed goods, the right path depends on production targets, site limits, utility headroom, labor access, compliance obligations, and return on invested capital. Across major U.S. manufacturing corridors such as the Midwest, Texas, the Southeast, California, and the Carolinas, expansion projects are being driven by reshoring, retailer service-level pressure, co-manufacturing growth, and stricter sustainability expectations. Facilities near Chicago, Dallas-Fort Worth, Charlotte, Fresno, Atlanta, and ports such as Savannah, Houston, Long Beach, and Newark often gain logistics advantages, but they also face higher complexity around permitting, utilities, and phased construction. A detailed feasibility process turns those variables into a practical expansion roadmap. For many manufacturers, the best answer is not automatically “build bigger.” In some cases, debottlenecking controls, utilities, sanitation flow, batching logic, or packaging line balance can unlock double-digit capacity gains before heavy construction begins. That business-first mindset is central to how capital projects should be evaluated in the U.S. food and beverage market. If your food factory has strong market demand, a structurally sound building, utility reserve, and room for process flow improvement, expanding the current plant is often faster and more capital-efficient than constructing a new facility. If your site is landlocked, utility-constrained, labor-challenged, or operationally incompatible with future product mix, a new build may deliver better long-term economics. The fastest way to determine the right path is to compare five factors: current capacity utilization, forecasted throughput, site expansion envelope, utility loading, and financial payback. A feasibility study should also test whether lower-cost changes such as automation updates, line balancing, scheduling redesign, or targeted equipment replacement can close the capacity gap first. In the United States, this step is critical because construction costs, power interconnection lead times, and wastewater permit requirements vary widely by state and municipality. The table above shows why expansion decisions should be framed as a business case, not just a construction question. In many U.S. projects, a hybrid approach works best: debottleneck immediately, add modular utilities next, and reserve greenfield planning for a later phase. The expansion-versus-new-build decision usually starts with timing, but it should end with lifecycle value. Expanding an existing plant can preserve tax advantages, labor continuity, supplier routes, and established certifications. It also avoids the learning curve of starting up at a new location. For plants near distribution hubs like Memphis, Kansas City, Indianapolis, or Allentown, maintaining the current freight network may be a major advantage. However, not every plant is expandable in a practical sense. Older facilities may suffer from low clear heights, poor raw-to-ready separation, undersized drainage, outdated ammonia or glycol systems, or limited truck queuing. A new build becomes attractive when the legacy site forces inefficient flow or recurring compliance risk. This is especially common for processors shifting from regional production to national scale or adding aseptic, retort, USDA-inspected protein, or allergen-segregated operations. Disruptive Process Solutions approaches this question from a profitability perspective rather than a generic construction lens. The company’s teams support food and beverage manufacturers across the United States and Canada with planning, engineering, installation, integration, and execution oversight. That practical range matters because the right answer may involve process redesign, equipment relocation, owner’s representation, or a phased design-build-manage strategy instead of a single large capital event. You can learn more about the company’s planning approach on its company overview page. The comparison above is useful when management needs a board-level recommendation. In practice, the decision should be backed by modeled throughput, utility load calculations, construction phasing plans, and a realistic commissioning schedule. This growth trend reflects the broader U.S. push toward automation, domestic production resilience, and higher-throughput processing systems. By 2026, capital spending is expected to remain focused on facilities that improve labor productivity, energy efficiency, and service reliability. A capacity gap analysis measures the difference between what your plant can consistently produce today and what the business must produce in the future. This includes not only nameplate equipment ratings, but also changeover losses, sanitation windows, labor availability, yield loss, maintenance reliability, and utility support. Many plants overestimate capacity because they use theoretical hourly rates rather than true OEE-based output. A strong analysis separates bottlenecks by process area: receiving, batching, thermal processing, filling, packaging, warehousing, and shipping. For example, a beverage site may have enough blending volume but insufficient bright tank turnover or filler speed. A prepared foods plant may have enough cook capacity but limited chilling, slicing, or case packing. Protein facilities often hit constraints in wastewater, refrigeration, or USDA inspection flow before core equipment appears full. DPS frequently helps clients look beyond equipment count and into system balance. Its technological capabilities span process, structural, mechanical, plumbing, electrical, and controls engineering, including PLC programming, automation, SCADA, batch control, and utility integration. That matters because hidden capacity is often buried in control logic, CIP sequencing, recipe timing, or poor synchronization between upstream and downstream assets. More on these integrated offerings can be found on the services page. This table illustrates why a plant can miss demand even when some equipment still appears underutilized. The gap may sit in labor, support systems, or sanitation frequency rather than in the main processing asset. The sector demand chart shows why capacity planning should be product-specific. Ready-to-drink beverages, protein processing, and aseptic lines are among the most active categories in U.S. capital expansion discussions due to retail velocity, shelf-life demands, and co-packing growth. Site feasibility answers whether the plant can physically grow without creating flow conflicts or code issues. This includes building envelope, ceiling height, column spacing, floor loading, access roads, employee circulation, raw and finished segregation, maintenance access, and room for future utility yards. In U.S. food manufacturing, site feasibility is often constrained by truck flow, stormwater rules, neighboring parcels, or municipal setback requirements. Manufacturers near dense metros such as Los Angeles, Northern New Jersey, or greater Boston often find land expansion difficult, while sites in Texas, the Carolinas, Tennessee, or parts of the Midwest may have better expansion envelopes. Yet more land does not automatically mean easier expansion if electrical service, water supply, or sewer discharge permits are limited. For food and beverage operators, space must be judged by hygienic zoning as much as square footage. A plant may have open floor area but still lack room for proper ingredient staging, allergen control, forklift segregation, or maintenance access. That is why process flow modeling and adjacency planning should be part of the site review. The explanation here is straightforward: most “space problems” are really flow problems. A site with disciplined master planning can often outperform a larger but poorly organized facility. Production line integration is where good feasibility work protects revenue. Expansions fail when new systems are treated as standalone purchases rather than connected process networks. Tie-ins affect utilities, controls, sanitation, scheduling, operator training, and startup stability. The key goal is to sequence work so the plant stays commercially functional while upgrades occur. Best practice is to identify shutdown-critical activities early: process piping cutovers, electrical switchgear upgrades, controls migration, roof penetrations over active production, steam tie-ins, wastewater reroutes, and refrigeration shutdown windows. For many U.S. processors, holiday demand cycles, retailer promotions, or harvest seasons determine the only acceptable installation window. DPS is especially relevant in this area because it combines design, installation, integration, and project management under one execution model. Its manufacturing capabilities include custom tanks, CIP systems, cooking vessels, and specialty process equipment that can be engineered to fit retrofit conditions. Its teams also manage turnkey installation and system integration, reducing handoff risk between design intent and field execution. Equipment-related capabilities are outlined on the equipment solutions page. When line expansion is phased correctly, plants can install utility backbone first, stage new skids off-line, test controls in parallel, and execute final tie-ins during short planned outages. That approach reduces startup surprises and shortens the path to stable production. The area trend reflects a growing U.S. preference for phased retrofits over full plant shutdowns. As labor costs rise and customer service penalties tighten, producers increasingly favor staged integration strategies that preserve production continuity. Utility capacity is often the hidden governor of food factory growth. A plant may have room for more production equipment yet lack the electrical service, steam generation, chilled water, refrigeration tonnage, process water treatment, compressed air, or wastewater discharge capacity to support it. In many U.S. municipalities, utility upgrades have lead times longer than process equipment procurement. Power capacity should include transformer loading, switchgear condition, spare breaker space, motor starting impact, standby generation needs, and utility-provider interconnection schedules. Water reviews should cover peak flow, pressure stability, pretreatment needs, seasonal restrictions, and product-contact quality where applicable. Wastewater feasibility must analyze flow, BOD, TSS, fats, oils, grease, pH, and local surcharge structures. For protein, dairy, beverage, and prepared food plants, wastewater can become the decisive project constraint. DPS’s technological capabilities extend deeply into utility infrastructure, including CIP, boilers and steam, compressed air, cooling towers, glycol and refrigeration support, water treatment, wastewater planning, HVAC, controls, and energy management. That breadth matters because utility systems should be sized for process reality, not just generic rule-of-thumb assumptions. This table shows why utility feasibility should be completed early. Late-stage discovery of a sewer limit or switchgear replacement can radically change project economics and timing. A food factory expansion should be judged by incremental EBITDA, not just by installed cost. Financial feasibility requires a complete view of direct CAPEX, soft costs, utility upgrades, permitting, contingencies, startup losses, working capital, maintenance burden, and labor impact. The right model should also compare multiple scenarios: debottleneck only, phased expansion, major retrofit, and new build. In the United States, financing assumptions matter more than many teams expect. Interest rates, depreciation treatment, local incentives, utility rebates, and tax abatement can materially alter project payback. States competing for food manufacturing investment, such as North Carolina, Texas, Tennessee, Georgia, Indiana, and parts of the Midwest, may offer grants or infrastructure support that improve returns. Expansion economics should also reflect avoided costs: reduced co-manufacturing spend, lower freight, lower scrap, lower labor per unit, and fewer service failures. For some plants, the best ROI comes from digital controls upgrades, utility optimization, or packaging automation rather than from adding entirely new process trains. The table above highlights why ROI is only credible when both cost and operational realism are included. A low-budget project with weak commissioning planning can produce a worse return than a higher-CAPEX project with stronger execution certainty. This comparison suggests a common U.S. pattern: debottlenecking and targeted line expansion frequently generate the fastest payback, while full retrofits and new builds are better justified when strategic growth or compliance needs outweigh near-term return speed. Regulatory feasibility is a major part of expansion planning in the United States. Depending on the product category, facilities may need to address FDA, USDA, state environmental agencies, local building departments, fire marshals, wastewater authorities, and third-party certification bodies such as SQF or BRC. Expansion plans should be reviewed for food safety zoning, air handling, personnel flow, allergen management, sanitary design, labeling impact, thermal process validation, and utility compliance. Protein and dairy expansions may face especially rigorous oversight around drainage, refrigeration, sanitation, and wastewater. Beverage and aseptic projects require close attention to process controls, fill environment, CIP validation, and water quality. Plants adding retort or shelf-stable systems must also consider process authority review and documentation discipline. DPS has experience supporting projects that align with FDA, USDA, SQF, and BRC expectations, which is valuable because compliance must be built into equipment layout, utility design, and operating procedures from the beginning. Manufacturers assessing options can review relevant execution examples in the company’s project case studies. Beyond current compliance, 2026 trends point toward tougher expectations around energy intensity, water stewardship, wastewater pretreatment, refrigerant strategy, digital traceability, and worker safety. Expansion feasibility should therefore include future-proofing for automation, data visibility, sanitation verification, and sustainability reporting. A phased expansion strategy reduces both operational and financial risk. Instead of trying to solve every capacity issue in one large project, the manufacturer sequences improvements based on business urgency, cash flow, and site logic. Typical phases include immediate debottlenecking, utility backbone upgrades, process line additions, warehouse or cold storage expansion, and long-range site redevelopment. This approach is especially useful for co-packers, multi-SKU food plants, and beverage manufacturers with seasonal demand volatility. It allows leadership to validate market growth, preserve optionality, and incorporate lessons from early phases into later investments. It also supports better contractor scheduling and less disruptive tie-in planning. DPS’s service capabilities are well suited to this model because the company acts across capital planning, feasibility analysis, owner’s representation, project and program management, general contracting where licensed, equipment supply, installation, and integration. Its design-build-manage framework helps align engineering, field execution, and stakeholder decision-making, which is often the difference between a controlled phased rollout and a fragmented expansion effort. The value of this phased table is that it turns growth into a managed sequence rather than a single all-or-nothing bet. It also fits the realities of U.S. permitting lead times, labor availability, and financing windows. As a practical buying guideline, manufacturers should select engineering and integration partners that understand both food process realities and capital discipline. Look for a team that can challenge assumptions, quantify utility impacts, model downtime, coordinate local trades, and tie every major scope item to profit, compliance, and scalability. That is particularly important for enterprises expanding in multiple states or standardizing facility platforms across a network. For product categories such as sauces, dressings, RTD beverages, dairy, plant-based proteins, meat, poultry, seafood, and aseptic foods, feasibility should never be generic. Each category has distinct thermal, sanitary, storage, and utility implications. The strongest expansion plans are product-specific, location-aware, and phased to match real commercial demand. Local supplier strategy also matters. U.S. food plants benefit when regional fabricators, electrical contractors, mechanical installers, and automation specialists are coordinated through a clear project governance structure. Whether the project is in North Carolina, California, Illinois, Texas, or Ontario-border logistics territory, local trade execution needs to be aligned with process-critical design intent. How long does a food factory expansion feasibility study usually take in the United States?Most studies take from 4 to 12 weeks depending on scope, data quality, and whether utility providers, environmental agencies, or multiple production scenarios must be evaluated. When is expansion better than a new build?Expansion is usually better when the current site has utility headroom, good labor access, workable hygienic flow, and enough space to add process or support infrastructure without major operating disruption. What is the biggest hidden risk in plant expansion?Utility limitations are among the most common hidden risks, especially electrical service, wastewater discharge, refrigeration, and sanitation support capacity. Can controls upgrades really increase capacity without major CAPEX?Yes. In some plants, PLC logic, recipe timing, CIP sequencing, line balancing, and packaging synchronization create larger bottlenecks than core equipment size. Which industries most often need detailed expansion studies?Protein, dairy, ready-to-drink beverages, sauces, prepared foods, aseptic processing, and co-packing operations frequently require detailed studies because of high throughput pressure and strict compliance requirements. How should a manufacturer compare suppliers or project partners?Compare them on food-industry experience, utility expertise, retrofit integration capability, project management discipline, compliance familiarity, and willingness to challenge weak assumptions. What trends will shape expansion planning in 2026?Expect stronger focus on automation, energy efficiency, water reuse, wastewater reduction, digital traceability, modular utility systems, and phased projects that protect production continuity. What role can DPS play in this process?DPS can support feasibility studies, capital planning, process and utility engineering, owner’s representation, equipment integration, installation, and managed execution for food and beverage manufacturers across North America. -
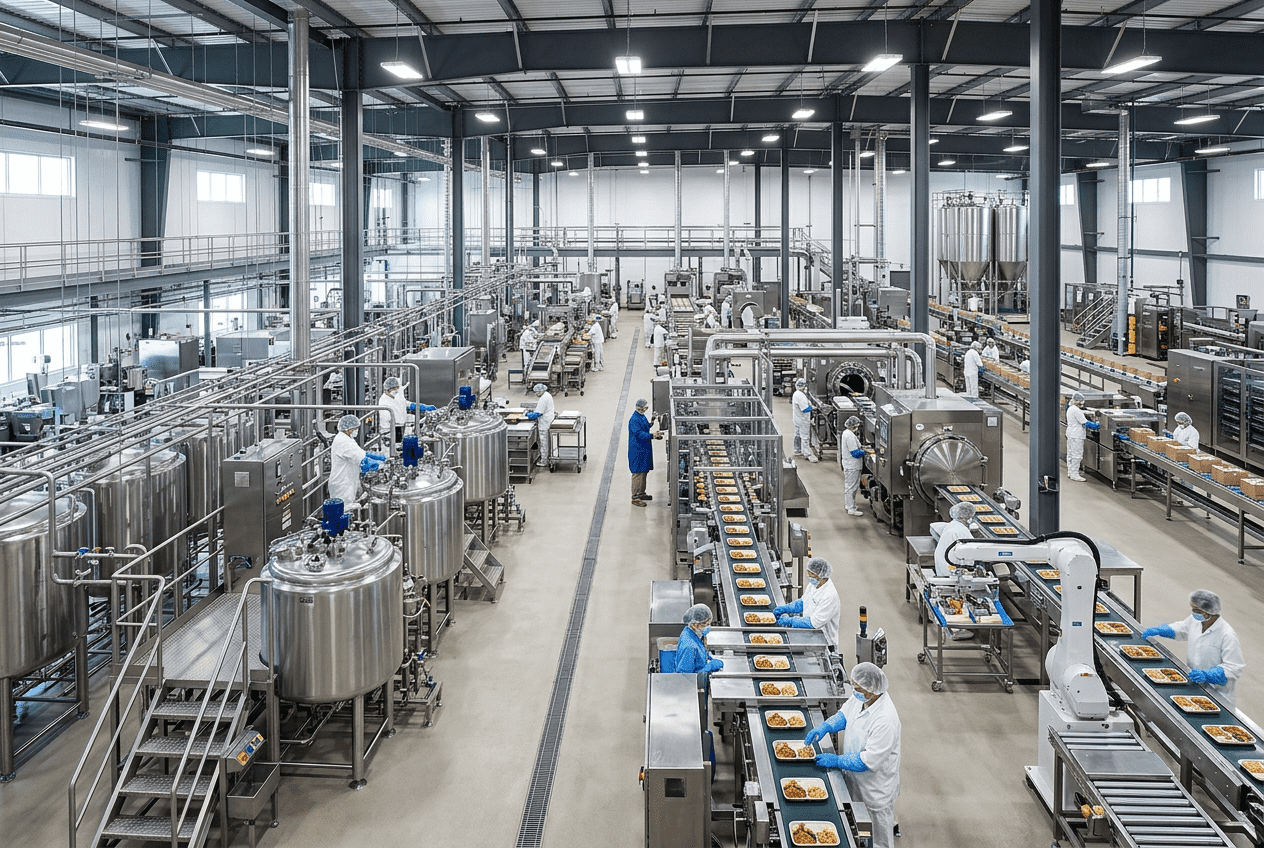
Beverage Factory Expansion Feasibility
Expanding a beverage plant in the United States can create major profit upside, but only when capacity, utilities, layout, labor, automation, and financial returns are evaluated together. Many manufacturers assume they need a new line, a larger syrup room, or additional packaging equipment, when the real limit is often hidden inside controls logic, CIP scheduling, wastewater treatment, compressed air, or warehouse flow. A disciplined expansion review helps beverage producers avoid overbuilding and directs capital toward the true constraint. For U.S. manufacturers producing soft drinks, ready-to-drink beverages, spirits, juices, kombucha, dairy beverages, brewing products, and aseptic formats, expansion decisions are increasingly tied to regional distribution strategy, retailer service levels, freight economics, and utility resilience. Plants near major trade corridors such as Chicago, Dallas-Fort Worth, Atlanta, Los Angeles/Long Beach, Savannah, Houston, and New Jersey often see strong scale opportunities, but they also face tight labor markets, more demanding municipal utility rules, and increasingly complex compliance expectations. This guide explains how to assess whether a beverage facility is truly ready for expansion, what technical and financial criteria matter most, and how to build a smarter project plan that protects long-term profitability. Yes, a beverage factory is ready for expansion only when five core conditions are met: current bottlenecks are clearly identified, the building and site can physically support additional process and packaging assets, water and wastewater systems have sufficient reserve capacity, the expansion delivers acceptable payback under realistic demand scenarios, and the project can be executed without destabilizing seasonal production commitments. In practice, that means a U.S. beverage producer should validate: If one or more of these areas is weak, expansion can still happen, but the project scope must be adjusted. Often, a targeted debottlenecking effort produces better returns than a full line addition. The table above shows why beverage plant expansion cannot be judged by sales growth alone. Even when customer demand is strong, utility or process limitations can turn a seemingly simple growth project into an expensive underperformer. The first step is separating market demand from operational readiness. A factory may have enough orders to justify more output, but if uptime, changeover discipline, sanitation windows, or tank utilization are weak, adding equipment may only magnify inefficiency. In the United States, where labor, construction, and utility costs vary sharply by region, expansion readiness must be measured with operating data, not assumptions. Producers serving retailers, foodservice channels, club stores, and contract manufacturing customers should review at least 12 to 24 months of operating history. This should include hourly performance by SKU family, downtime causes, shift staffing, utility peaks, warehouse turnover, and customer service penalties. Plants in high-growth beverage categories such as energy drinks, functional beverages, alcohol alternatives, premium mixers, and aseptic RTD coffee should also stress-test demand against packaging supply lead times and regional freight patterns. Useful readiness criteria include: U.S. beverage plants near major logistics hubs often have an advantage. For example, distribution from Indianapolis, Memphis, Kansas City, and Columbus can reduce outbound freight to broad regions of the country. However, those savings can be erased if the plant lacks wastewater permit flexibility or cooling capacity during summer production surges. At this stage, many manufacturers benefit from an outside engineering perspective. A firm like Disruptive Process Solutions approaches readiness from a business-first standpoint, focusing on whether capital will improve profitability rather than simply increase installed equipment. That mindset matters because the best answer is not always “build bigger”; sometimes it is “fix the process first.” This readiness matrix helps teams decide whether expansion capital should go into new production assets, utility reinforcement, software integration, or operational discipline first. The market growth trend above reflects a realistic view of continued U.S. beverage investment. Growth is not uniform across all categories, but the broader direction supports careful capacity planning, especially in high-value packaged beverage segments. The most important expansion question is simple: what is actually limiting throughput today? In beverage operations, the bottleneck is often dynamic. On one SKU run it may be blending, on another it may be filler speed, tunnel pasteurization, label application, secondary packaging, or palletizing. In some facilities, the true bottleneck is not hardware at all. It may be CIP turnaround time, PLC logic, changeover sequencing, or operator staffing. A good bottleneck study maps the full production path from ingredient receiving through batching, blending, treatment, filling, packaging, palletizing, warehousing, and loadout. It should look at both peak rate and sustained rate. Advertised equipment speed is rarely the number that matters; sellable output over an entire shift is what drives economics. For example, a carbonated soft drink plant in Texas may have a filler rated at 600 bottles per minute, yet only average 68% of theoretical output because syrup changeovers, CO2 management, capper stoppages, and downstream accumulation issues reduce run efficiency. In that case, buying a faster filler would not solve the problem. A better answer may be controls reconfiguration, accumulation redesign, or improved line balancing. This is where practical engineering experience matters. DPS has built a reputation by identifying hidden constraints before clients commit unnecessary capital. The company’s technology depth includes process engineering, controls engineering, PLC programming, automation, SCADA, and integration across utilities and production systems. In one representative situation, the real bottleneck was controls-related, and resolving the PLC limitation created a significant capacity gain without forcing a multimillion-dollar expansion. That kind of analysis protects capital and often improves payback more than a new asset purchase. This table shows that not every bottleneck requires major construction. Some can be solved through sequencing, controls, and process optimization, which usually produce faster returns. The bar chart highlights where expansion demand is strongest across beverage segments. High-growth categories typically justify faster investment decisions, but they also require more disciplined risk screening because product mix can shift rapidly. Even when demand and utilities support growth, the building may not. Space and layout feasibility is more than finding enough floor area for a new filler or canning line. U.S. plants must also consider access for installation, code-required clearances, sanitation zoning, traffic separation, mezzanine loading, forklift flow, ingredient staging, spare parts access, and future maintenance. Layout failures are expensive because they create lasting inefficiency. A line inserted into an already crowded building can generate chronic congestion between depalletizing, packaging material feed, QA hold zones, and finished goods staging. It can also compromise food safety design by crossing raw and finished traffic paths or by creating hard-to-clean dead spaces. For beverage categories such as kombucha, dairy beverages, and aseptic products, hygienic zoning becomes even more important. Additional tanks, valves, transfer piping, and CIP return routing must be evaluated as a system, not as isolated pieces of equipment. DPS supports this kind of planning through integrated engineering disciplines that include structural, mechanical, plumbing, electrical, process, and controls design. That matters during line addition studies because the “space” question often becomes a roof loading question, a utility corridor question, or an access and constructability question. For manufacturers reviewing possible reconfiguration or equipment relocation, the broader engineering and project delivery services available from an experienced design-build-manage partner can reduce coordination gaps and change-order risk. Layout reviews often reveal that minor relocation of existing assets can unlock better value than a building addition. In dense urban or suburban U.S. sites where land costs are high, reflowing operations may be more economical than expanding the footprint. Water and wastewater are among the most underestimated factors in beverage expansion planning. Beverage plants consume water for product, CIP, sanitation, boiler feed, cooling tower makeup, and general operations. The plant may be able to fit a new line physically, yet still fail expansion feasibility because municipal water pressure, pretreatment, or discharge permits cannot support added volume. This issue is particularly important in regions facing infrastructure or sustainability pressure, including parts of California, Arizona, Colorado, and fast-growing areas of the Southeast. Plants near major metros like Phoenix, San Diego, Charlotte, and Austin may encounter stricter water management expectations, rising rates, or longer permitting timelines. Wastewater is just as critical. Increased sugar loads, pH swings, suspended solids, alcohol content, dairy loads, or cleaning chemical discharge can overwhelm existing pretreatment systems. Municipal surcharges can quickly erode the economics of expansion if not modeled in advance. Strong beverage expansion planning therefore includes incoming water quality analysis, treatment capability review, peak-day and peak-hour demand modeling, sewer discharge characterization, and resilience planning. DPS brings relevant capabilities here through complete utility system integration, including process water systems, reverse osmosis, disinfection, CIP, boilers and steam, glycol systems, compressed air, refrigeration, cooling towers, and wastewater coordination. This is especially valuable for beverage manufacturers adding more complex products or high-sanitation processes. The main lesson is that beverage growth frequently depends on utility resilience as much as production equipment. A plant with strong water and wastewater planning is better positioned to support expansion, compliance, and sustainability goals at the same time. The area chart illustrates a clear shift toward water efficiency, reuse, and sustainability-driven utility planning through 2026. This is becoming a strategic advantage, not just a compliance checkbox. Once bottlenecks and utilities are understood, the next question is which equipment and technology investments will create scalable gains. In many U.S. beverage plants, a successful expansion requires more than just adding primary process equipment. It may involve packaging automation, inline quality monitoring, recipe control, data collection, energy management, or upgraded CIP architecture. Technology requirements vary by product type: Manufacturing capability should be reviewed holistically. DPS supports beverage manufacturers with system design and integration across fermentation systems, pasteurization and sterilization technologies, carbonation, blending and batching, filtration, aseptic processing, filling support, and broad utility infrastructure. In addition, the company manufactures selected process equipment such as tanks and custom CIP systems, giving clients a practical path when standard off-the-shelf solutions do not match project requirements. More on those equipment options can be found through the company’s process equipment capabilities. For 2026 and beyond, upgrade decisions are being shaped by three trends: higher automation adoption, tighter sustainability expectations, and stronger demand for operating data. Producers increasingly want systems that can scale without proportional labor growth. That means more attention to SCADA visibility, remote diagnostics, batch reporting, predictive maintenance, and energy tracking. These upgrade categories matter because expansion decisions should strengthen future competitiveness, not only solve today’s capacity gap. Every beverage plant expansion should be tested against realistic economics, not optimistic top-line assumptions. The financial model should compare at least three paths: debottleneck only, partial expansion, and full expansion. It should also model a downside case where demand grows more slowly than forecast, input costs rise, or startup takes longer than expected. In the United States, the cost of expansion is affected by location, labor rates, local permitting complexity, utility connection fees, sanitary design requirements, and whether the project includes a building expansion. A line installed in North Carolina or Tennessee may have a different cost profile than a similar line in Southern California or the Northeast corridor. Key financial categories include: Service capabilities are especially important here. DPS supports capital planning, feasibility studies, owner’s representation, project and program management, general contracting where licensed, and turnkey installation and integration. That end-to-end model helps manufacturers connect financial assumptions to actual execution realities, which is critical when estimating startup risk and payback timing. This example shows why payback can vary dramatically based on project type. Many of the strongest returns come from solving constraints before adding full-scale assets. The comparison chart reflects a common market reality: integrated project delivery tends to produce stronger outcomes because engineering, construction, controls, and startup decisions are aligned earlier. Timing can make or break an expansion. Beverage demand in the United States is often seasonal, with strong summer peaks for soft drinks, flavored waters, energy beverages, beer, and many RTD formats. Holiday demand can also drive spikes for spirits, mixers, and promotional packs. If a plant schedules installation during peak selling periods, revenue loss and customer service failures can outweigh the long-term benefit of the project. The best timing strategy starts with customer commitments, promotional calendars, weather-sensitive demand, packaging material lead times, and utility availability. A plant serving southeastern states through Atlanta or Florida lanes may face very different summer risks than one serving the Pacific Northwest from Portland or Seattle. Likewise, a brewery supplying Midwestern stadium and event channels may need winter shutdown windows, while a juice or dairy beverage plant may align around harvest cycles or school-year demand patterns. Expansion timing should also consider contractor access, equipment lead times, municipal permitting schedules, and startup labor readiness. U.S. utility interconnection or wastewater approval can take longer than the mechanical installation itself. A strong strategy usually includes phased implementation: By 2026, producers are also expected to factor in resilience planning. Heat stress, water restrictions, power instability in some regions, and stricter sustainability reporting can affect the ideal expansion window. Plants that sequence projects around these risks will be better prepared for long-term operating stability. A practical example helps illustrate how expansion feasibility should work. Consider a U.S. beverage manufacturer operating a multi-SKU facility near a major distribution corridor in the South. Sales growth from private label and co-packing customers suggested the need for a multimillion-dollar capacity expansion. Initial thinking focused on adding major new process equipment and increasing packaging speed. However, the feasibility review showed that the plant’s actual limits were more nuanced. The primary issues included inefficient controls logic, poorly sequenced CIP activity, and utility coordination gaps during product changeovers. Packaging assets were not fully synchronized, and realized throughput lagged theoretical capacity by a meaningful margin. Rather than immediately installing the largest possible expansion package, the team first corrected the real bottlenecks. Controls and sequencing improvements increased output, stabilized line performance, and improved labor effectiveness. Only after the plant captured those gains did it move into the next phase: targeted equipment and utility upgrades sized to realistic future demand. This phased approach is consistent with how DPS typically supports manufacturers: engineer the solution, manage execution, and keep profitability at the center of the decision. The company’s project model is built around aligning capital with operational reality, whether the need is a feasibility study, utility upgrade, equipment integration, relocation, or a complete growth plan. Additional project examples and outcomes can be explored through the firm’s case study portfolio. The core lessons from this case are clear: For U.S. beverage producers, this is often the difference between a profitable expansion and a costly underperforming project. What is the first sign that a beverage plant should consider expansion?The first sign is sustained sold demand that consistently pushes the plant near practical capacity, not just occasional sales spikes. That signal should be confirmed with OEE data, downtime records, and utility usage. How much reserve utility capacity should a plant have before adding a line?There is no single number for every site, but many plants aim for meaningful headroom in water, wastewater, compressed air, cooling, steam, and electrical systems. If current loads are already close to peak, utility upgrades should be part of the project. Can debottlenecking replace a full expansion?Often, yes. Controls improvements, CIP redesign, line balancing, tank utilization changes, and packaging upgrades can deliver significant gains at lower cost and with faster payback than a complete line addition. Which U.S. regions are attractive for beverage manufacturing expansion?That depends on market access, labor, freight, utilities, and permitting. Regions around Dallas-Fort Worth, the Carolinas, Tennessee, the Midwest logistics belt, and parts of the Southeast are frequently attractive, but each project must be evaluated site by site. How long does a beverage expansion feasibility study usually take?A focused study may take several weeks, while a more complex review involving utility modeling, multiple product types, building constraints, and capital staging may take longer. The right duration depends on risk and project size. What product categories most often require advanced hygienic design?Aseptic beverages, dairy beverages, kombucha, functional products with sensitive ingredients, and certain shelf-stable RTD products usually require more rigorous hygienic design and process control. Should expansion planning include future sustainability requirements?Yes. By 2026, water efficiency, energy performance, wastewater reduction, and broader reporting expectations will increasingly shape project approvals and operating costs in the United States. What kind of project partner is best for beverage expansion?The strongest partner is one that can evaluate process, utilities, controls, installation, and financial implications together. That integrated view reduces the risk of solving one problem while creating another. In summary, beverage factory expansion feasibility in the United States depends on rigorous assessment, not enthusiasm alone. The best projects begin with a direct answer to the real operating constraint, then move through layout, utilities, technology, capital modeling, and timing in a disciplined way. Manufacturers that take this approach are far more likely to add profitable capacity, protect service levels, and create a plant platform ready for the next phase of growth. -
Food Facility Equipment Procurement Best Practices
Procuring food facility equipment in the United States is not just a purchasing task. It is a capital decision that affects throughput, food safety, labor efficiency, utility consumption, compliance exposure, and long-term profitability. The best results come from aligning engineering, operations, quality, maintenance, finance, and procurement before issuing bids. Whether the project involves a new dairy line in Wisconsin, a beverage expansion near Atlanta, a protein upgrade in Kansas, or an aseptic packaging installation in California, buyers that define scope clearly, compare suppliers objectively, and manage installation and startup with discipline consistently outperform buyers that focus only on the lowest initial price. The most effective approach to food facility equipment procurement in the United States is to treat the process as a structured project lifecycle rather than a series of purchase orders. Start with a realistic business case, define process and utility requirements, prepare a detailed specification, run a disciplined request for quotation process, compare suppliers on technical fit and execution capability, negotiate commercial and performance protections, coordinate delivery and installation around plant readiness, and close the project with documented commissioning and handover. This reduces cost overruns, change orders, startup delays, and compliance risk. In practical terms, the procurement team should answer six questions before contacting vendors: What production outcome is required? What product and regulatory standards apply? What utilities and building constraints exist? What labor model will support the line? What is the total installed budget, not just the equipment price? What is the expected return on investment? In food and beverage manufacturing, those questions matter because a mixer, filler, retort, pasteurizer, still, fermenter, or CIP system never operates in isolation. It must fit the process, the building, the sanitation plan, and the commercial model. Across U.S. manufacturing hubs such as Chicago, Charlotte, Houston, Fresno, Minneapolis, and Philadelphia, capital buyers increasingly prioritize procurement methods that integrate process engineering with construction and startup planning. That shift is especially important at facilities near major logistics gateways such as the Port of Los Angeles, Port of Long Beach, Port of Savannah, Port of Houston, and Port of New York and New Jersey, where inbound lead times and freight complexity can materially affect project schedules. The table above shows why the strongest procurement programs connect commercial decisions to execution milestones. Each stage has a different owner, but success depends on a single integrated plan. Procurement planning and budgeting should begin with product demand, not equipment brochures. A facility producing sauces in New Jersey needs a very different design basis than a beverage co-packer in Texas or a poultry processor in Arkansas. The project team should forecast volumes, define SKU mix, identify sanitation requirements, evaluate labor availability, and estimate utilities such as steam, glycol, chilled water, compressed air, process water, wastewater, and power capacity. For U.S. buyers, budgeting errors often come from leaving out indirect costs. The quoted purchase price may represent only 35 to 60 percent of the total installed cost, depending on the system. Foundations, mezzanines, rigging, freight, tariffs, controls integration, validation, startup support, spare parts, operator training, and local permitting can materially increase the final investment. This is especially true for high-complexity systems such as UHT skids, aseptic fillers, retorts, distillation systems, full CIP networks, and automated batching lines. Another best practice is to classify the project by investment purpose: replacement, capacity expansion, quality upgrade, compliance correction, energy reduction, or product innovation. That classification helps executives compare projects more accurately. A replacement project may protect uptime, while an automation project may lower labor costs and improve batch consistency. Both can be worthwhile, but they should not be evaluated with the same assumptions. The explanation behind this budgeting structure is simple: capital decisions fail most often because teams underestimate everything around the equipment. In the U.S. market, a disciplined budget is a scope document with numbers attached, not a rough quote multiplied by a guess factor. Market conditions also matter. Stainless steel pricing, controls lead times, labor shortages, and regional contractor availability can shift budgets materially. For example, projects in high-demand manufacturing corridors around Raleigh-Durham, Dallas-Fort Worth, and Southern California may face tighter scheduling pressure than projects in smaller secondary markets. Buyers should also plan for 2026 trends including stronger energy reporting expectations, rising demand for water reuse, more cybersecurity scrutiny for industrial controls, and wider adoption of modular skid fabrication to reduce field labor. The line chart illustrates a realistic upward trend in U.S. food equipment capital spending, reflecting expansion in automation, sanitation upgrades, and resilience investments. Vendor selection and evaluation should be based on evidence, not brand familiarity alone. A well-known OEM may still be the wrong fit if its design assumptions, support model, or spare parts availability do not match your plant. Likewise, a smaller supplier can be the better choice if it demonstrates stronger process knowledge, cleaner documentation, faster decision-making, and a better startup team. In food and beverage plants, vendor evaluation should cover at least six categories: technical compliance, sanitary design, execution capability, service support, financial/commercial strength, and cultural fit. Technical compliance includes throughput, product viscosity range, heating or cooling profile, cleanability, automation compatibility, and changeover performance. Sanitary design includes weld quality, drainability, dead-leg control, seal selection, allergen management, and compliance with FDA, USDA, SQF, or BRC expectations where relevant. Execution capability often separates successful projects from disappointing ones. A supplier may build excellent hardware but lack field coordination, FAT discipline, or documentation quality. In the United States, buyers should request U.S.-based references, ask about technician coverage by region, and confirm how the vendor supports plants in different time zones. Support expectations for a facility in North Carolina are not identical to those for a site in Washington state or Alberta. This evaluation framework works because it converts supplier selection from subjective preference into a transparent decision model. It also helps procurement defend recommendations internally when competing vendors are close on price. Local supplier strategy is another important factor. For standard utility items, fabricated piping supports, simple tanks, and field services, U.S. regional suppliers may offer faster response and lower freight. For specialized aseptic systems, tunnel pasteurizers, advanced fillers, or custom retort systems, national or international suppliers may still be necessary. The right approach is usually hybrid: source specialized process technology from proven OEMs and pair it with local execution resources where appropriate. The bar chart shows relative equipment demand by sector, with beverage and protein continuing to drive strong capital activity in the U.S. market. The request for quotation process is where procurement quality is either created or lost. If the RFQ package is vague, every supplier will make different assumptions, and the buyer will receive prices that cannot be compared fairly. A strong RFQ creates an apples-to-apples comparison by defining scope, performance requirements, interfaces, standards, schedule expectations, commercial terms, and documentation needs. A proper RFQ package for food facility equipment should include process descriptions, product characteristics, target throughput, utility data, site drawings, required materials of construction, automation standards, sanitary requirements, FAT expectations, delivery windows, installation responsibilities, startup obligations, warranty requirements, and training expectations. If the project involves U.S. regulatory exposure, the package should also note any requirements tied to FDA, USDA inspection environments, allergen zoning, or customer audit standards. Buyers should issue a bid tab template with the RFQ. That forces vendors to disclose inclusions and exclusions consistently. Without this step, one quotation may include valves, instrumentation, and startup support while another excludes them, making the lower price misleading. A clarification log is equally important. All bidders should receive the same answers so the process remains fair and auditable. The explanation for this table is straightforward: every missing RFQ element becomes a future clarification, a future change order, or a future schedule risk. Good RFQs reduce all three. For imported equipment arriving through ports such as Long Beach, Houston, Savannah, or Newark, the RFQ should define Incoterms, customs responsibilities, site delivery conditions, storage requirements, and crane or rigging assumptions. Plants in urban areas such as Boston or Seattle should also address access limitations, staging areas, and restricted delivery hours. These details have real cost consequences. Contract negotiation strategies should protect performance and execution, not only purchase price. Many buyers focus heavily on headline discounts while overlooking delivery guarantees, installation support, software access, spare parts availability, and acceptance criteria. In food equipment projects, those overlooked terms often matter more than a small reduction in unit price. The first negotiation principle is to align payment milestones with evidence of progress. A typical structure might include deposit, approved drawings, fabrication completion, factory acceptance test, shipment, mechanical completion support, and final acceptance. Buyers should avoid front-loaded terms that transfer too much cash before performance is proven. The second principle is to define acceptance clearly. Factory acceptance testing should confirm core functions before shipment. Site acceptance testing should confirm integrated performance under real plant conditions. If acceptance language is vague, disputes become more likely. The contract should also define punch list closure, response times for defects, and software or controls obligations. The third principle is to negotiate support, not just hardware. That includes operator training, maintenance training, spare parts recommendations, remote diagnostics, emergency service response, and post-startup optimization days. For plants with demanding production schedules, like beverage facilities in the Southeast or protein plants in the Midwest, those support commitments can protect revenue far more than a modest upfront discount. The value of this approach is that it converts negotiation into risk allocation. The best contract is not the one with the fewest words; it is the one that makes project responsibilities unmistakable. By 2026, contract language in the U.S. is also likely to evolve around sustainability reporting, equipment energy performance, refrigerant management, cybersecurity for connected controls, and data access for predictive maintenance. Buyers planning multi-site portfolios should begin incorporating these requirements now. Delivery and installation coordination is where procurement becomes reality. Many projects that look successful on paper lose value during field execution because equipment arrives before the site is ready, the utilities are incomplete, the controls contractor is not aligned, or the rigging plan is inadequate. This phase requires strong project management, especially in active plants that cannot stop production for long. Best practice is to build a site readiness checklist before the first shipment leaves the vendor. That checklist should confirm foundations, drains, overhead clearances, utility stubs, floor conditions, sanitation zoning, electrical disconnects, access routes, permits, and safety plans. It should also define who owns unloading, storage, preservation, and damage inspection. For coastal or humid environments such as Florida, the Gulf Coast, or Pacific Northwest sites, preservation planning is especially important for stainless systems, motors, and controls panels. Installation coordination should also consider sequence. In many food projects, utility backbone work, drains, structural steel, and controls rough-in must happen before process skids can be set. If the sequence is wrong, crews interfere with each other and productivity drops. This is one reason many owners prefer an integrated partner that can connect engineering, construction oversight, and process installation. An additional U.S. consideration is local trade availability. Mechanical and electrical labor conditions differ widely between Phoenix, Milwaukee, Nashville, and the Inland Empire. Lead project teams should align contractor strategy with local market realities instead of assuming labor is interchangeable nationwide. The area chart reflects a growing shift toward modular and preassembled systems, a trend driven by schedule compression, field labor constraints, and quality control needs. Commissioning and handover should begin long before startup week. The most successful projects define commissioning strategy during procurement so vendors know what tests, documents, and training outputs will be required. In food facilities, this process typically includes mechanical completion checks, loop checks, dry testing, wet testing, CIP verification, performance trials, alarm testing, safety verification, operator training, maintenance training, and final document turnover. For regulated or highly audited environments, handover should include calibration records, material certificates where required, as-built drawings, IO lists, software backups, recommended spare parts, preventive maintenance tasks, SOP support, and equipment manuals. Plants that skip structured handover often struggle months later when troubleshooting or preparing for audits. Commissioning should verify more than whether the machine turns on. It should test whether the integrated system produces the product at the expected rate and quality. For example, a mixing system may meet speed criteria but still fail yield or viscosity consistency targets. A filler may run but underperform on changeover time. A retort may heat correctly but create packaging issues under real loads. The handover process should capture these realities before final acceptance. Case studies across U.S. manufacturing show that startup outcomes improve when the owner appoints a single accountable leader to coordinate OEMs, utilities, controls, operators, and sanitation. That structure keeps decision-making fast during the most dynamic phase of the project. Total cost of ownership analysis is one of the most important and least used best practices in equipment procurement. Two systems with similar purchase prices can produce dramatically different long-term costs. The more complete analysis includes not only acquisition cost but also utilities, labor, cleaning chemistry, water use, maintenance parts, service support, downtime exposure, yield loss, training needs, and expected useful life. In many food and beverage applications, the higher-priced option can be more profitable if it reduces cleaning time, improves first-pass yield, lowers changeover losses, or simplifies maintenance. This is particularly true in high-volume categories such as ready-to-drink beverages, dairy processing, protein forming, and sauce batching where small percentage improvements compound into major annual savings. The explanation here is critical: total cost of ownership analysis reframes procurement from “What does it cost to buy?” to “What does it cost to own and operate?” That perspective is essential for executives managing plant profitability. The comparison chart shows how a supplier with a slightly lower technical score may still be the better procurement choice if service coverage, documentation, and startup support are materially stronger. When evaluating applications by product type, buyers should adapt TCO models accordingly. Fermentation systems should emphasize temperature control stability and cleanability. Distillation systems should emphasize safety, throughput, and utility efficiency. Dairy systems should emphasize product recovery and hygienic design. Protein lines should emphasize uptime, washdown durability, and labor efficiency. Aseptic systems should emphasize sterility assurance, validation, and specialized support. For manufacturers seeking a partner rather than a transactional seller, Disruptive Process Solutions supports food and beverage capital projects across the United States and Canada with a business-first mindset. The company is built around helping clients make smarter capital decisions, execute cleanly, and protect long-term profitability rather than simply pushing scope. From a technological capabilities perspective, DPS works across structural, mechanical, plumbing, electrical, process, and controls engineering, including PLC programming, automation, and SCADA integration. That matters because equipment procurement decisions must fit real process conditions, utility systems, and control architectures. Whether a project involves fermentation, blending, carbonation, pasteurization, retort, aseptic processing, water treatment, or advanced batching, DPS helps connect process design to execution so equipment selections work in practice, not only in quotations. From a manufacturing capabilities perspective, DPS also provides proprietary equipment for selected applications, including tanks, CIP systems, marination tumblers, and cooking vessels. That manufacturing perspective helps the team evaluate fabrication quality, sanitary design details, and field integration requirements more rigorously. Buyers looking at custom systems can review relevant process equipment capabilities while still keeping the focus on fit-for-purpose design. From a service capabilities perspective, DPS delivers process engineering and design, capital planning, feasibility studies, owner’s representative support, project and program management, general contracting functions where applicable, installation oversight, and system integration. The company’s Design Build Manage model is especially useful for clients that want one accountable team connecting procurement, field execution, and startup. Organizations evaluating project delivery options can explore available engineering and project services or review selected project examples and outcomes for context. That integrated structure is particularly valuable in U.S. projects where schedule pressure, contractor coordination, and utility integration drive major risk. Instead of treating procurement as separate from design and commissioning, DPS helps align the commercial decision with the full lifecycle of the plant asset. What is the biggest mistake in food equipment procurement?The most common mistake is buying based on the lowest quoted price without fully defining scope, utilities, controls integration, startup support, and total cost of ownership. How many suppliers should be invited to quote?For most projects, three to five qualified suppliers is enough. Fewer may limit competition; more can create unnecessary administrative work without improving decisions. Should buyers prefer local U.S. suppliers?Not always. Local suppliers may offer faster response and lower freight, but specialized equipment may require national or international OEMs. The best choice depends on technical fit, support model, and lifecycle value. What should be included in a food equipment RFQ?Include process data, product characteristics, throughput targets, utility information, sanitary requirements, controls standards, documentation expectations, FAT and SAT criteria, schedule milestones, and commercial terms. How long does a typical procurement cycle take?For moderate complexity equipment, 8 to 16 weeks is common from specification to order. Larger integrated systems can take several months longer, especially if imported or highly customized. How should commissioning be managed?Use a formal plan with mechanical completion, dry and wet testing, utility verification, operator training, maintenance training, and documented acceptance criteria. Assign one owner-side leader to coordinate the process. What are the key 2026 trends in the United States?Expect more automation, stronger energy and water efficiency expectations, expanded use of modular skid systems, greater cybersecurity attention for controls, and tighter focus on sustainability and lifecycle reporting. Which industries benefit most from structured procurement?Beverage, dairy, protein, sauces, prepared foods, aseptic processing, and co-packing operations all benefit because they depend on uptime, sanitary performance, and rapid startup. When should an owner’s representative or engineering partner be involved?As early as possible, ideally before the RFQ is issued. Early involvement improves scope definition, budget accuracy, vendor comparison, and installation planning. How can a buyer compare product types fairly?Use a weighted matrix that scores technical fit, sanitary design, controls compatibility, lead time, service support, warranty, and total cost of ownership for each equipment type and supplier. In summary, food facility equipment procurement best practices in the United States depend on disciplined planning, clear technical definition, balanced vendor evaluation, strong contracts, coordinated execution, and a lifecycle view of asset value. When these elements are managed together, manufacturers gain more reliable startups, stronger compliance outcomes, and better returns on capital. -
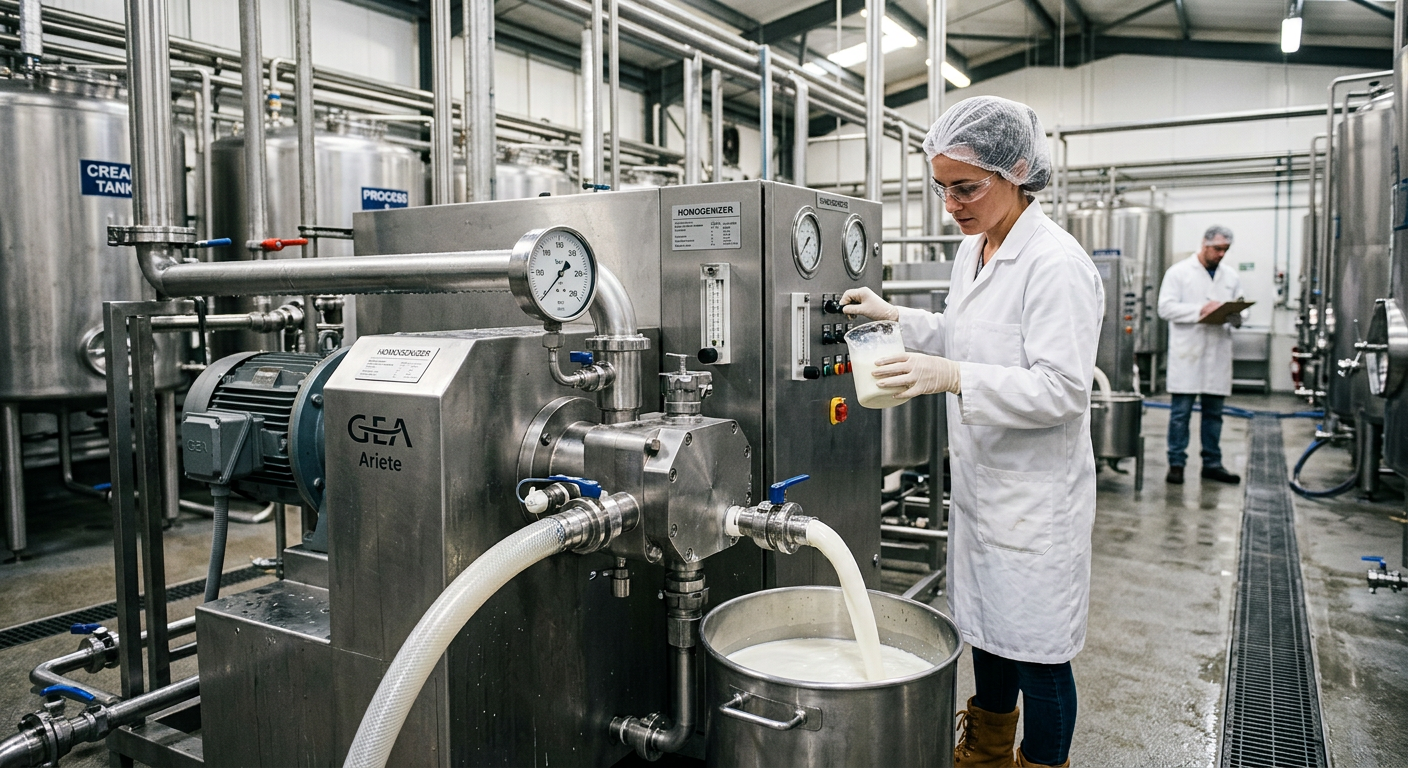
Food Facility Constructability Review: Design-to-Build Feasibility
Food and beverage manufacturers in the United States are under constant pressure to expand capacity, improve food safety, shorten startup time, and spend capital more carefully. A constructability review is one of the most practical ways to protect those goals before money is committed to demolition, utilities, equipment procurement, or field labor. In simple terms, a constructability review tests whether a proposed design can actually be built safely, efficiently, and profitably within the realities of the site, the production environment, local codes, and the operating schedule. For a processor planning a greenfield beverage site near Dallas, a protein expansion in Kansas City, a dairy retrofit in Wisconsin, or a co-packing line addition in Southern California, the same question comes up: will this design work in the field without expensive surprises? That is where disciplined review of site conditions, equipment access, utility congestion, maintenance clearances, temporary works, and sequencing becomes essential. A paper design may look complete, yet still fail when trucks cannot unload near the building, mezzanine steel blocks vessel rigging, trench drains conflict with slab reinforcement, or the utility corridor has no room left for sanitary process piping and electrical raceways. Across major trade and logistics hubs such as Chicago, Houston, Atlanta, Los Angeles, Long Beach, Savannah, Newark, and Memphis, food plants face additional complexity from labor availability, transportation lead times, utility interconnection schedules, and municipal review procedures. In a market where missed production weeks can cost far more than design fees, constructability is not a box-checking exercise. It is a profitability decision. A food facility constructability review is a structured design-to-build feasibility check performed before procurement and field execution accelerate. It is used to identify site constraints, utility conflicts, access limitations, sanitation risks, and schedule bottlenecks early enough to fix them economically. In the United States, this review is especially important for facilities governed by FDA, USDA, SQF, and BRC expectations, where build quality affects both production and compliance. The most effective review answers several direct questions: For manufacturers evaluating budget approvals, the return is usually found in avoided rework, fewer RFIs, more reliable schedule commitments, better startup readiness, and cleaner handoff between engineering and operations. This is particularly valuable in beverage bottling, brewery expansion, aseptic processing, dairy, prepared foods, protein processing, retort systems, and ingredient plants where sanitary detailing and utility reliability are mission-critical. The United States market is also seeing broader use of constructability review earlier in capital planning, not just before construction. Owners now want design teams to validate crane paths, pad elevations, washdown zoning, compressed air routing, CIP recovery, boiler and refrigeration support areas, and packaging line serviceability before final equipment orders are released. The chart below illustrates a realistic view of rising demand for front-end constructability work in U.S. food and beverage capital programs. As the line trend suggests, more owners are moving constructability reviews upstream because financing, labor, and startup risk have become less forgiving. This shift is expected to continue into 2026, especially where automation, water reuse, electrification, and sustainability goals add engineering complexity. This table shows why constructability is not just a design issue. It sits at the intersection of market conditions, logistics, food safety, and execution strategy. The first major review area is the site itself. Existing conditions govern what can be built, how fast it can be built, and how much it will cost. In older food plants across the Midwest and Northeast, site constraints often include low roof elevations, undocumented drains, undersized electrical rooms, slab thickness uncertainty, and limited truck circulation. In newer campuses in Texas, the Carolinas, Arizona, and Tennessee, the challenge may be rapid expansion pressure, utility reservation, and future campus planning rather than aging infrastructure. A proper site condition assessment for a food facility should look beyond standard civil and architectural due diligence. It should review process flow, raw material receiving, waste handling, employee movement, hygienic zoning, cleanable surfaces, washdown exposure, floor slope suitability, roof support for utilities, and any restriction that could interfere with sanitary installation methods. It should also verify whether existing structures can support suspended piping bridges, platforms, skids, vessels, evaporators, or packaged utility systems. For example, a brewery near Denver may have enough floor area for more fermenters, but lack exterior glycol yard space and forklift turning radius for safe vessel placement. A protein facility near Omaha may have utility capacity but insufficient drainage and sanitation separation for new marinated product lines. A dairy plant near Fresno may fit a UHT skid inside the building, yet the route for delivery through doors, corridors, and roof openings may be impossible without temporary structural removal. In the United States, location matters. Facilities near the Port of Houston may benefit from freight access but need flood resilience planning. Facilities in New Jersey may face tighter utility and permit coordination. Sites around Memphis or Louisville may have strong logistics but must manage compressed schedules tied to distribution contracts. Plants in California may encounter stricter environmental and water-use scrutiny, making front-end review of wastewater, reuse, and permit pathways especially important. The value of this table is practical: each item turns a broad site walk into a construction decision. A design may satisfy process intent, but if truck movement, slab loading, or utility yard geometry are ignored, the build becomes harder and more expensive than expected. Even a sound design can fail if the construction sequence is wrong. Sequencing is especially important in food and beverage projects because many are retrofit or brownfield jobs inside operating facilities. Work may have to occur around active production, sanitation shifts, USDA inspection windows, peak seasonal demand, or narrow shutdown opportunities. The sequence must therefore align design release, procurement, demolition, utility outage planning, equipment setting, controls integration, startup, and validation. In real projects, the best sequence is rarely “build everything at once.” It is usually a staged approach based on risk and operational continuity. Utility backbone work may need to occur first. Structural steel or platforms may need to be installed before process skids arrive. Dust-generating demolition may need to be isolated from ready-to-eat areas. Packaging moves may need to be scheduled after upstream process tie-ins are commissioned. Cold storage work may need temporary environmental controls before door openings occur. Sequencing should also account for off-site fabrication. In many U.S. markets, modular pipe racks, skid-mounted CIP systems, packaged compressor rooms, prefabricated electrical assemblies, and pretested control panels can reduce field hours and improve schedule reliability. However, modularization only works if site dimensions, access paths, and crane planning are reviewed early. The bar chart below shows realistic relative demand for constructability review across major food and beverage segments in the United States. Aseptic, beverage, and protein projects tend to rank higher because they often combine demanding hygienic standards with dense utility needs, strong throughput expectations, and expensive startup risk. This sequence table helps owners understand where schedule compression often backfires. Pulling forward visible equipment while delaying structural, utility, or controls readiness can create expensive stop-start execution. Equipment access is one of the most common sources of field surprises in food plant construction. Tanks, kettles, retorts, fillers, palletizers, pasteurizers, boilers, air compressors, refrigeration skids, and CIP systems are often large enough that route planning becomes a project-critical activity. Constructability review should examine every step from supplier shipping configuration to final installed service envelope. The review should confirm loading dock suitability, trailer type assumptions, unloading method, crane access, interior path width, door and corridor dimensions, floor protection needs, temporary removals, hoisting points, and final clearances for operation and maintenance. It should also consider future replacement. A line may be installable today through a wall opening, but if that opening is later closed permanently, major replacement costs rise sharply. Food plants frequently underestimate service space around equipment. Sanitarians may need hose access. Mechanics may need motor pull space. Operators need line-of-sight and safe egress. Instrument technicians need access to panels and transmitters. In washdown areas, nearby electrical and controls equipment may need protective placement or special enclosures. Clearance is not just about fitting equipment in; it is about running the plant effectively for years. Product type also changes the clearance requirement. Fermentation systems need headspace and utility flexibility. Distillation systems may need strict safety review and vent routing. Aseptic systems require disciplined separation, service access, and validation logic. Protein processing lines often need careful coordination of conveyors, cleaning access, and overhead utility drops. Retort and canning systems need robust steam, condensate, and drainage planning around high-use operating zones. This table translates access review into asset-specific checks. It is especially useful when comparing vendor drawings that show minimum footprint but not true operational or maintenance envelopes. Utility conflict review is often where the biggest hidden risks are uncovered. Food and beverage facilities carry a dense mix of process piping, CIP, steam, condensate, compressed air, CO2, nitrogen, glycol, chilled water, hot water, domestic water, wastewater, electrical distribution, controls, data, and HVAC systems. Without disciplined coordination, these systems compete for the same overhead and equipment-side space. Older plants are especially vulnerable because legacy lines may be undocumented or routed in ways that no longer support sanitary or maintenance best practice. Newer buildings can also struggle when design packages are developed in separate silos. A process layout may assume one routing strategy while mechanical, electrical, and structural details assume another. The result is congestion discovered too late. Conflict review should check elevation bands, hygienic zoning, pipe slopes, trap access, cleanout points, panel location, washdown exposure, refrigeration safety interfaces, and utility redundancy. It should also confirm whether existing boilers, chillers, cooling towers, wastewater systems, and electrical service can handle new loads under actual operating diversity rather than nameplate assumptions. The following area chart illustrates how U.S. project priorities are shifting from pure capacity growth toward integrated reliability, sustainability, and digital visibility through 2026. The trend matters because utility conflicts become more complex when projects include heat recovery, water reuse, energy monitoring, automation upgrades, and digital controls integration in addition to throughput expansion. Owners looking for buying advice should ask suppliers to provide more than utility demand numbers. They should request connection locations, service clearance requirements, operating envelope, cleanout needs, controls interface details, and preferred routing constraints. That information makes constructability review more accurate and reduces vendor coordination gaps. For more detail on integrated engineering and project execution methods, manufacturers can review DPS service capabilities to understand how early coordination supports smoother buildout. Temporary works are often overlooked because they do not become permanent parts of the facility. Yet they can determine whether the project is safe, code-compliant, and buildable. In food plants, temporary works may include shoring, access platforms, temporary partitions, dust control, sanitary containment, weather protection, temporary power, bypass utilities, temporary drainage, rigging supports, roof openings, and short-term refrigeration or compressed air solutions during tie-ins. Brownfield projects frequently need temporary hygiene barriers to separate construction from production. If a ready-to-eat area remains active while adjacent work occurs, containment strategy must be treated as a design and sequencing issue, not a field improvisation. Similarly, temporary utility bypasses should be validated before shutdown windows. An unplanned outage to compressed air, process water, or refrigeration can affect product quality and plant revenue immediately. Temporary works planning is also where safety and profitability align. If crane pads, temporary floor protection, or elevated work platforms are not considered early, access methods become slower and riskier. Likewise, if temporary weatherproofing is omitted in Gulf Coast or Midwestern winter conditions, moisture intrusion and delayed finish work can follow. This table highlights a useful principle: temporary works are not overhead noise. They are often prerequisites for successful permanent work. Many projects are designed around startup day rather than the next fifteen years of operation. That is a mistake. Maintenance access verification ensures that pumps, valves, motors, instruments, heat exchangers, filters, conveyors, control cabinets, and utility assets can be inspected, cleaned, isolated, repaired, and replaced without excessive labor or sanitation disruption. In food and beverage plants, maintenance planning should account for both reliability and hygienic design. A valve cluster that is impossible to access will not be maintained properly. A panel mounted in a wet zone may create chronic reliability issues. A compressor yard with no removal path may turn routine service into a crane event. A process line with no clean break points may lengthen sanitation time and reduce throughput. This is where product applications matter. Aseptic systems require disciplined access for validation and sterile boundary management. Brewery and beverage systems need maintainable piping routes around tanks, pumps, and platforms. Dairy and prepared foods operations need cleanable arrangements that support frequent changeovers. Protein plants need robust washdown-compatible access and durable service paths. Co-packers often benefit from maintenance layouts that support rapid SKU changes and future line adaptation. Owners should insist that maintenance personnel, operators, and sanitation leaders participate in constructability review. They often see problems that design and construction teams miss. Their input can influence panel location, valve orientation, platform arrangement, access ladders, hose stations, floor drains, and lockout strategy before those details become expensive to change. Manufacturers comparing equipment vendors can also use maintainability as a buying criterion. Lower purchase price may not equal lower lifecycle cost if service points are crowded, proprietary parts are hard to source, or standard maintenance tasks require line disassembly. The financial purpose of constructability review is straightforward: reduce avoidable cost and improve schedule confidence. In the United States, the strongest business case usually comes from preventing rework, shortening outage windows, improving trade productivity, and reducing startup delays. Cost impacts are rarely limited to direct construction labor. They often include lost production, delayed revenue, premium freight, temporary operating inefficiency, and higher long-term maintenance cost. For that reason, cost and schedule impact analysis should compare alternative design and delivery strategies rather than viewing constructability as a pass-fail exercise. Can utility routing be simplified? Can skids be prefabricated? Can the sequence reduce shutdown hours? Can a larger roof opening reduce total rigging cost? Can future expansion stubs eliminate a second demolition event? Can controls integration be advanced earlier to avoid late commissioning chaos? The comparison chart below shows realistic scoring of common delivery and sourcing approaches for food plant buildability in the United States. While every project is unique, integrated delivery typically performs better where utility density, sanitary standards, startup coordination, and operating continuity all matter at once. This analysis table is important because it connects constructability decisions directly to owner economics. The conversation should not stop at installed cost; it should include startup timing, plant availability, and future operating burden. Looking toward 2026, several trends will shape cost and schedule analysis in U.S. food projects: Facilities seeking examples of how these decisions play out can review selected project case examples to see how front-end planning can influence execution and profitability. Disruptive Process Solutions serves food and beverage manufacturers across the United States and Canada with a business-first project approach centered on profitable execution. Rather than operating as a narrow specialty contractor, DPS supports projects from early feasibility through engineering, build coordination, installation, and startup oversight. More information about the firm’s background and project philosophy is available on the about DPS page. From a technological capability standpoint, DPS works across structural, mechanical, plumbing, electrical, process, and controls engineering. That matters in constructability review because food facilities rarely fail in only one discipline. A brewery expansion may involve fermentation vessels, glycol, carbon dioxide, automation, utility yard arrangement, and CIP integration at the same time. A dairy or aseptic project may require sanitary process design, utility modeling, automation logic, and compliance-aware layout decisions. DPS supports these cross-disciplinary interfaces so design assumptions can be tested against actual build conditions before they become field issues. From a manufacturing capability standpoint, DPS also brings practical familiarity with process equipment and system integration. The company supports applications across beverage, brewing, distillation, dairy, prepared foods, protein processing, aseptic systems, retort, utilities, and clean processing environments. It also manufactures selected process equipment, including tanks and CIP-related systems, which adds useful perspective during access, utility, and maintenance review. Manufacturers evaluating line additions or utility expansions can explore relevant process equipment capabilities as part of early planning. From a service capability standpoint, DPS uses an integrated Design Build Manage approach that aligns engineering, general-contractor-style execution management, and project oversight. For constructability work, that model is valuable because it closes the gap between design intent and field reality. Instead of handing off drawings and hoping contractors solve conflicts later, the process emphasizes early feasibility, build sequencing, equipment installation logic, utility coordination, and owner-focused decision support. This is especially relevant for processors that need honest feedback on whether a concept should be adjusted before major capital is committed. The best fit for this approach is often a manufacturer that values long-term operating results over short-term appearances. That includes multi-site food producers, growth-stage co-packers, breweries, dairy processors, protein operations, and beverage plants that need both technical rigor and practical execution planning in the United States market. What is the difference between a constructability review and a feasibility study?A feasibility study tests whether a project should be pursued from business, technical, and financial perspectives. A constructability review focuses more specifically on whether the chosen design can be built safely, efficiently, and reliably at the actual site. When should a food plant perform a constructability review?Ideally during concept or early design development, before equipment orders, final utility routing, and major permit commitments. Reviews performed only after IFC documents are issued usually find problems later and cost more to correct. Is constructability review only for large greenfield facilities?No. It is often even more valuable for brownfield expansions, line retrofits, utility upgrades, and phased modernization inside operating plants where shutdowns, sanitation, and access constraints are more severe. Which industries benefit most in the United States?Beverage, brewing, dairy, protein, prepared foods, aseptic processing, retort, and co-packing projects all benefit, especially where utilities are dense and startup timing affects contracts or seasonal demand. What should owners ask equipment suppliers during review?Ask for shipping dimensions, rigging loads, utility connection locations, maintenance clearances, operator access needs, controls requirements, spare parts assumptions, and replacement path considerations. How does constructability review support compliance?It helps identify poor hygienic zoning, inaccessible cleanable areas, unsuitable drain geometry, exposed electrical equipment in washdown zones, and other issues that can undermine FDA, USDA, SQF, or BRC expectations. Can a review reduce schedule risk even if the budget does not change?Yes. Better sequencing, prefabrication strategy, outage planning, and utility coordination can protect startup dates even if total capital remains similar. What are the biggest 2026 trends to watch?Expect stronger emphasis on automation integration, sustainability metrics, water reuse, energy efficiency, resilient utility design, modular construction, and earlier owner demand for proof that projects are truly buildable. How should a buyer compare local suppliers and contractors?Do not compare on price alone. Evaluate food-sector experience, sanitary installation quality, utility coordination ability, documentation standards, startup support, and willingness to challenge bad assumptions early. What is the main outcome of a strong constructability review?A project team gains a clearer path from design to startup: fewer surprises, cleaner execution, safer installation, stronger schedule confidence, and better long-term plant performance. -
Beverage Plant Capital Planning
Beverage manufacturers in the United States face a capital environment shaped by volatile input costs, labor constraints, packaging shifts, retailer service expectations, and aggressive growth timelines. A disciplined beverage plant capital planning process helps operators decide where to invest, when to invest, and how to structure projects so capacity, quality, utilities, compliance, and profitability improve together rather than in conflict. Beverage plant capital planning is the structured process of deciding how to invest in production lines, utilities, automation, storage, packaging, buildings, and supporting infrastructure to achieve growth, compliance, reliability, and margin goals. In practice, that means aligning demand forecasts with line capacity, identifying bottlenecks, sequencing projects by financial return and operational risk, and selecting the right capital structure for each investment. For U.S. manufacturers, the strongest plans usually share five characteristics: they start with throughput constraints instead of equipment wish lists; they account for total cost of ownership rather than sticker price alone; they phase investments around seasonal demand; they compare projects across the whole plant portfolio; and they use a delivery partner who can connect engineering, installation, utilities, controls, and execution. Companies that skip these steps often overspend on visible assets like fillers while underinvesting in compressed air, glycol, wastewater, CIP, or electrical distribution that actually determine uptime. In large beverage markets such as California, Texas, Florida, Illinois, Georgia, and North Carolina, capital planning also needs to consider freight lanes, labor availability, permitting timelines, utility interconnection, and access to co-packing or distribution hubs near ports such as Los Angeles, Long Beach, Savannah, Houston, Newark, and Seattle. Capital planning for a beverage manufacturing facility goes beyond annual budgeting. It is a decision framework used to evaluate whether a producer should expand a bottling hall, add blending capacity, modernize controls, upgrade a boiler room, increase warehouse space, improve sanitation design, or outsource selected production stages. It ties operations, finance, engineering, quality, and commercial strategy into one roadmap. In the U.S. market, beverage producers range from craft breweries and distilleries to national soft drink bottlers, RTD alcohol producers, dairy beverage manufacturers, juice processors, kombucha brands, and aseptic co-packers. Each segment has distinct CAPEX profiles. Carbonated soft drink operations may prioritize depalletizing, high-speed fillers, blow molders, and CO2 systems. Aseptic beverage plants may focus on sterile utilities, high-barrier packaging, cleanroom controls, and microbiological segregation. Distilleries often need fermentation, stills, proofing, barrel logistics, and wastewater management. Functional beverage producers may place more emphasis on batching accuracy, ingredient handling, and rapid SKU changeovers. A sound capital plan answers several core questions: When these questions are answered well, the plant avoids the common trap of buying capacity that cannot be supported by process flow or utilities. For example, a faster canning line may create little value if syrup prep, pasteurization, or refrigeration remain undersized. A practical framework for beverage facility capital planning should move from business strategy to asset-level decisions. The most effective sequence is commercial demand, plant diagnostics, concept alternatives, financial modeling, portfolio ranking, and staged execution. Step one is demand translation. Sales forecasts should be converted into cases, gallons, shifts, SKUs, package mix, seasonal peaks, and service-level commitments. A 20 million case forecast means little until it is translated into line rates, changeover frequency, concentrate storage, water demand, pallet positions, and labor models. Step two is current-state assessment. This should map every meaningful constraint across process, packaging, utilities, controls, quality, warehousing, sanitation, and material handling. Many U.S. plants discover the hidden bottleneck is not the filler but poor OEE driven by labeler stops, compressor instability, or inadequate CIP availability. Step three is alternatives development. Instead of assuming one answer, management should compare debottlenecking, brownfield expansion, greenfield construction, automation upgrades, utility modernization, outsourcing, or phased capacity additions. Step four is financial evaluation. This includes CAPEX, start-up losses, ramp time, labor impact, maintenance cost, energy intensity, service life, salvage, risk, and expected contribution margin. Step five is execution governance. A project only creates value if it is installed, commissioned, integrated, and handed over correctly. This is where an engineering-led partner matters. Integrated capital project services can reduce coordination gaps between process engineering, utilities, local trades, and controls integration. The table above shows why capital planning should be treated as a business system, not an equipment procurement exercise. Each stage protects the plant from a different form of value leakage. One of the most common mistakes in beverage plant investment is over-prioritizing visible production assets while neglecting utility and infrastructure systems. Bottling and canning lines create revenue, but they only perform if supported by stable power distribution, air compression, process water, glycol, steam, wastewater treatment, ventilation, and clean-in-place capacity. In a U.S. facility shipping to major retail and foodservice customers, line downtime can quickly trigger chargebacks, missed promotions, and lost shelf space. That means utility resilience often has a higher strategic value than managers initially assume. Typical CAPEX categories include: The right mix depends on product category. A hot-fill juice plant in Florida may prioritize pasteurization reliability and PET handling. A hard seltzer or RTD alcohol operation in Texas may focus on blending flexibility, seam integrity, and wastewater loads. A dairy beverage plant in Wisconsin or California may place greater emphasis on refrigeration, sanitary design, and clean utilities. This table matters because prioritization should not be based on which asset looks most urgent in isolation. It should be based on which project most improves site-wide throughput and margin under realistic operating conditions. Seasonality is a defining feature of U.S. beverage operations. Peak demand often accelerates in late spring and summer for soft drinks, bottled water, sports beverages, beer, canned cocktails, and convenience-store driven formats. Holiday demand can influence spirits, mixers, premium beverages, and specialty gift packaging. For dairy and certain nutritional beverages, school calendars and contract cycles may also matter. Capital timing should reflect this seasonality. Plants in Atlanta, Dallas, Phoenix, Tampa, and Southern California often face heavy seasonal service expectations as temperatures rise. Installing major assets too close to peak season can be risky if FAT, SAT, operator training, or debug periods run long. On the other hand, delaying investment until after a selling season can postpone revenue capture by an entire year. Smart timing principles include planning shutdown-heavy work in shoulder seasons, ordering long-lead equipment before procurement congestion peaks, and separating utility upgrades from line installation when the schedule demands it. A can line expansion may appear simple until switchgear lead times, concrete curing, drain work, and airflow balancing are considered. Port and freight dynamics also matter. Equipment arriving through Los Angeles/Long Beach, Houston, Savannah, or Newark may face congestion, customs variability, or inland trucking constraints. This should be built into the capital calendar rather than treated as an exception. The explanation here is simple: timing can be as important as scope. The right project, executed at the wrong moment, can damage service performance and erase expected gains. Total cost of ownership, or TCO, is one of the most important concepts in beverage CAPEX planning. Two fillers with similar rated output may produce very different economic outcomes depending on utility draw, maintenance profile, spare parts cost, sanitation time, changeover speed, labor requirement, and expected uptime. A full TCO model should include: In many U.S. projects, the cheapest quote does not produce the best ownership value. A lower-cost asset can require more labor, have slower changeovers, or depend on hard-to-source components. In high-volume operations around Chicago, Charlotte, Fresno, Denver, or Columbus, small efficiency differences can compound quickly into large annual cost gaps. It is also important to include utility and building enablement. A new process skid may require RO expansion, floor drains, steam capacity, and electrical upgrades that exceed the skid price itself. This table is especially useful for procurement teams because it shows why TCO is not a finance abstraction. It directly influences real cash flow, service reliability, and plant profitability. Most beverage companies have more good projects than available budget. That is why project selection should be portfolio-led rather than politically driven. A portfolio view compares candidate projects using common metrics such as NPV, IRR, payback, strategic fit, compliance urgency, capacity effect, and execution risk. For example, a new packaging line may have the highest raw revenue upside, but a wastewater project may carry lower return with a much higher urgency because it prevents permitting limits from constraining output. Likewise, an automation project may deliver a stronger risk-adjusted return than a warehouse expansion if it removes the true bottleneck. A practical scoring model often weighs these categories: In multi-site U.S. organizations, this approach allows a fair comparison between projects in different plants, whether in California, the Carolinas, the Midwest, or the Gulf Coast. It also helps avoid overfunding highly visible line investments while deferring lower-profile projects that support the entire network. The takeaway from this comparison is that “best” is not always the project with the biggest machine. The best project is the one that improves portfolio value after risk and dependencies are considered. Not every capacity need should be met with owned equipment. Beverage producers in the United States increasingly use hybrid strategies that combine ownership, leasing, and co-manufacturing. The right capital structure depends on demand certainty, balance sheet priorities, launch speed, technology risk, and internal operating capability. Buying is often preferred when utilization is high, process know-how is core, and long-term economics clearly favor ownership. Leasing may make sense for assets with rapid obsolescence, near-term cash constraints, or pilot-scale uncertainty. Outsourcing can be attractive when a brand needs immediate market entry, geographic reach, or specialized processing such as aseptic filling or high-acid hot-fill. However, outsourcing is not automatically “asset light” if freight, margin sharing, quality oversight, and scheduling constraints weaken profitability. Likewise, buying too early can trap a growing brand in inflexible infrastructure. The best decision is usually category-specific. RTD brands launching on the coasts may initially rely on co-packers near Los Angeles, Dallas-Fort Worth, Chicago, or New Jersey to reduce freight and speed entry. Established regional bottlers with stable demand may justify in-house expansion. Operators should also assess whether to own utility systems or use service agreements for compressed air, water treatment, or boiler support. Accurate budgeting requires more than a vendor quote plus contingency. Beverage plant CAPEX budgeting should reflect scope maturity, long-lead procurement, site conditions, utility integration, controls work, and startup realities. A strong process usually starts with order-of-magnitude screening, then budgetary design estimates, then final execution pricing as scope definition improves. Best practices include: For companies operating in multiple states, local labor availability and permitting can materially affect the budget. Wage pressure in California, New York, and major metro areas may differ sharply from rates in smaller inland markets. Electrical gear lead times, union requirements, and seismic or environmental code issues should also be recognized early. This is also where execution capability matters. Firms with integrated engineering and field coordination can often create more reliable budgets because process, structural, mechanical, plumbing, electrical, and controls assumptions are aligned from the start. Learn about the engineering-led approach behind DPS to see why early alignment often protects capital better than low-bid fragmentation. From a 2026 outlook perspective, budgeting should increasingly account for automation, energy efficiency, water stewardship, and traceability requirements. State-level utility incentives, carbon reporting expectations, wastewater scrutiny, and digital reporting demands are pushing more projects toward controls modernization, heat recovery, and resource monitoring. The capital planning model used by a beverage plant should match the process reality of the product. Carbonated drinks require careful balancing of syrup handling, deaeration, carbonation, and package integrity. Dairy-based beverages require sanitary design and cold-chain discipline. Functional beverages with particulates may need specialized mixing, homogenization, and fill technology. Distilled products involve proofing, tankage, explosion safety considerations, and often visitor-facing design constraints. Applications where capital planning is especially important include: For product categories such as kombucha, beer, wine-based cocktails, protein beverages, juices, flavored waters, and shelf-stable dairy drinks, the right asset sequence is often different. That is why capital planning should start from process chemistry, sanitation requirements, package format, and growth economics rather than from generic line templates. Real-world project experience consistently shows that the highest-value capital outcome often comes from identifying the true constraint before spending on major expansion. In one beverage setting, a client may believe a multimillion-dollar line expansion is required, only to learn that controls logic, changeover sequencing, or CIP timing is the actual limit. Solving the root cause can unlock more throughput at a fraction of the spend. That philosophy is central to how DPS approaches projects. The company works across beverage categories including brewing, spirits, RTD, soft drinks, juices, kombucha, dairy beverages, and aseptic applications, but it is known less for selling equipment than for aligning capital with profitability. Its technical capabilities span process, structural, mechanical, plumbing, electrical, and controls engineering, including PLC programming and SCADA integration. On the manufacturing side, it also supports custom process equipment such as tanks and CIP systems. From a service standpoint, the company covers planning, feasibility, owner representation, project management, general contracting where licensed, installation, and integration. That combination matters because many beverage projects fail at the handoff points between design, procurement, site work, utilities, and startup. A coordinated delivery model can reduce those gaps. A good example of project thinking can be found in selected beverage and food capital project case examples, where execution is tied to operational outcomes rather than isolated construction milestones. Another useful lesson is that greenfield and brownfield facilities need different planning disciplines. A greenfield site near a logistics corridor such as I-85 in the Carolinas, the Inland Empire in California, or the Dallas-Fort Worth metroplex may optimize future scale and freight access. A brownfield retrofit in an older industrial area near Chicago, Philadelphia, or Newark may offer customer proximity but require extra investment in drains, electrical rooms, airflow, or warehouse flow. Beverage companies do not just buy equipment; they buy execution risk. Selecting the right supplier and partner ecosystem is therefore a critical part of capital planning. Local suppliers may provide stronger field response and code familiarity, while national integrators can bring broader process knowledge and multi-site consistency. The right answer depends on project scope. When screening partners, operators should assess: DPS is a useful example of a U.S. partner built around this integrated model. Its beverage experience covers everything from fermentation and distillation systems to pasteurization, carbonation, water treatment, aseptic processing, and complete utility infrastructure. Its manufacturing capabilities include proprietary equipment such as tanks and CIP systems, while its service capabilities extend from capital planning and feasibility through installation and system integration. Companies evaluating partners can also review custom equipment and process system offerings when considering whether to standardize or tailor components. In practical terms, local market knowledge matters. Gulf Coast plants may prioritize storm resilience and wastewater coordination. West Coast sites may face tighter utility and environmental review. Southeastern growth corridors may offer favorable logistics but tighter contractor availability in peak build cycles. Your capital partner should understand those realities, not just equipment brochures. What is the main goal of beverage plant capital planning?The goal is to allocate capital to the projects that best improve capacity, reliability, compliance, and profitability over time. It turns business growth into a sequenced plant investment plan. How often should a beverage manufacturer update its capital plan?Most companies should review the plan at least quarterly and refresh assumptions annually. Fast-growth brands, co-packers, and multi-SKU operations may need more frequent updates. Which projects usually deliver the fastest returns?Debottlenecking, controls improvements, CIP optimization, changeover reduction, and targeted utility upgrades often deliver faster payback than major building expansions, especially when they remove hidden constraints. Why is total cost of ownership more important than purchase price?Because energy use, labor, maintenance, uptime, and startup performance usually determine long-term economics. A low initial price can still produce a poor investment if lifecycle cost is high. How should U.S. plants prepare for 2026 capital trends?They should expect more emphasis on automation, digital visibility, energy efficiency, water management, traceability, and sustainability reporting. Projects that combine capacity growth with resource efficiency will likely rank higher. When does outsourcing make more sense than owning equipment?Outsourcing can be smart for uncertain demand, rapid launch timelines, regional testing, or specialized formats. Ownership generally becomes stronger when demand is stable and asset utilization is high. What data is needed to rank capital projects by NPV and risk?At minimum: demand forecast, contribution margin, installed cost, operating cost, startup schedule, utility loads, maintenance assumptions, compliance impact, and execution risk factors. How do utilities affect beverage line investments?Utilities often determine whether a line can actually achieve expected throughput. Inadequate compressed air, chilled water, steam, electrical capacity, or wastewater handling can limit performance even when the packaging line is new. What should companies look for in a capital project partner?They should look for engineering depth, practical beverage experience, integrated project execution, honest feasibility analysis, startup support, and the ability to coordinate across process, utilities, controls, and site construction. What makes a capital plan successful?A successful plan connects market demand, process reality, financial discipline, and execution capability. It funds the right projects in the right order and measures value by plant performance, not by how quickly equipment is purchased. For beverage manufacturers across the United States, from port-connected facilities in California and New Jersey to growth corridors in Texas and the Carolinas, capital planning is no longer a back-office budgeting exercise. It is a strategic operating discipline. Plants that combine demand realism, lifecycle economics, portfolio prioritization, and integrated execution are far more likely to build profitable projects, protect service levels, and scale with confidence.


