-
Clean-in-Place Systems for Food Plants
In food manufacturing, cleaning is not a support activity. It is a production-critical function that affects uptime, food safety, labor efficiency, environmental performance, and audit outcomes. For U.S. processors handling dairy, sauces, ready-to-eat foods, bakery fillings, beverages, and protein products, a well-designed clean-in-place system can reduce changeover time, standardize sanitation, and provide the validation records needed for FSMA-driven preventive controls. This guide explains how CIP works, when it is a better fit than COP or manual washdown, what system types are available, which components matter most, and how to evaluate a system for a new line or retrofit project. It is written for operations leaders, plant engineers, sanitation managers, quality teams, and ownership groups planning capital investments in the United States. Clean-in-place, or CIP, is an automated or semi-automated method of cleaning the internal surfaces of process equipment without taking that equipment apart. In a typical U.S. food plant, a CIP skid circulates rinse water, detergent, and sanitizer through tanks, piping, pumps, heat exchangers, fillers, and related equipment at controlled flow, temperature, concentration, and time. The goal is repeatable sanitation with less labor, lower exposure to human error, and cleaner records for audits. CIP is most effective when a process line is closed, product-contact surfaces are smooth and drainable, spray devices and return paths are engineered correctly, and the sanitation recipe is matched to the soil load. It is commonly used in dairy plants in Wisconsin, sauce facilities in Illinois, beverage co-packers in Texas, aseptic processors in California, and prepared-food operations across hubs such as Chicago, Atlanta, Dallas-Fort Worth, Fresno, and the Carolinas. For many facilities, the strongest business case for CIP is not just sanitation. It is improved schedule reliability. A plant that can clean predictably can run more consistently, change products faster, and document compliance more easily. The table above shows why CIP is often selected for growth-oriented plants. The more complex the schedule, the more valuable repeatable cleaning becomes. CIP is a sanitary cleaning methodology in which fluids are circulated through process equipment to remove product residue, reduce microbial risk, and prepare the line for the next run. Instead of disassembling every valve body, pipeline, and tank connection, the plant uses a dedicated cleaning circuit that applies mechanical action, chemistry, temperature, and time in a controlled sequence. The science behind CIP is often described by the four key cleaning variables: mechanical force, chemical action, temperature, and exposure time. If one variable is reduced, the others may need to increase. For example, a viscous dressing line may require stronger circulation velocity or a hotter caustic step than a light beverage blend line. Likewise, a dairy system with fats and proteins may need different chemistry than a sugar-based syrup system. A standard CIP circuit usually includes supply tanks, a circulation pump, heat control, automated valves, instrumentation, return piping, and a control platform tied to PLC and HMI logic. During the cycle, the system may execute a pre-rinse, wash, intermediate rinse, acid step if required, final rinse, and sanitization. Conductivity, temperature, flow, and sometimes turbidity are measured to confirm the process is within validated limits. In U.S. facilities, modern CIP systems are increasingly tied into plant-wide controls for recipe management, alarm history, and batch reporting. That matters especially in regulated environments where teams need traceability and proof that sanitation steps were executed correctly. A processor moving products through the Port of Los Angeles, the Port of Savannah, or cross-border distribution into Canada may also need standardized records across multiple sites and jurisdictions. When a CIP system is engineered correctly, it does more than wash equipment. It becomes part of the plant’s production architecture. Not every line is naturally CIP-able. Dead legs, poor slope, oversized valves, air pockets, rough welds, uncleanable pump selections, and incompatible elastomers can all undermine sanitation. That is why many processors work with firms that understand not only sanitation but full-system process integration. Integrated engineering and project delivery services are especially valuable when CIP must be aligned with utilities, controls, tank farms, fillers, heat exchangers, and expansion plans. Food manufacturers often use a mix of CIP, COP, and manual cleaning. The right choice depends on equipment geometry, soil type, risk category, labor availability, and required turnaround speed. COP, or clean-out-of-place, requires components to be removed from the line and washed in dedicated tanks or parts washers. Manual cleaning uses operators with tools such as hoses, foamers, brushes, and hand-applied chemicals. Each method has a place. The issue is selecting the method that controls risk without overcomplicating the operation. The comparison above makes one point clear: CIP is usually the best fit when consistency matters more than initial simplicity. COP remains essential for removable parts such as gaskets, fittings, and specialty components. Manual cleaning is still necessary for non-product-contact areas, equipment exteriors, and some open-process applications. Plants in high-labor-cost markets like California and the Northeast often see especially strong CIP payback because automation offsets staffing pressure. In regions with older legacy facilities, such as parts of the Midwest, retrofit feasibility becomes the deciding factor. Not every plant needs a full central CIP room; some are better served by smaller skids dedicated to production cells. CIP systems are not one-size-fits-all. The correct configuration depends on line count, product family, cleaning frequency, utility costs, sustainability goals, and the plant’s growth plan. In practice, U.S. manufacturers usually evaluate three broad approaches: single-circuit systems, multi-circuit systems, and recovery-based systems. Single-circuit CIP is common in smaller operations or targeted line expansions. It is easier to validate, simpler to maintain, and often a good entry point for processors moving away from labor-heavy manual cleaning. Multi-circuit CIP is more appropriate for plants running multiple tanks, blending systems, HTST loops, filler paths, or sauce lines with overlapping production schedules. It takes stronger automation design and valve matrix planning, but it can support better asset utilization. Recovery CIP is increasingly attractive as water, sewer, and energy costs rise. In markets such as California’s Central Valley, Arizona, and parts of Texas, utility constraints can materially affect project economics. Recovery designs can reduce waste loads, but they must be validated carefully to avoid cross-contamination and preserve cleaning effectiveness. Buyers should also think beyond the skid. Tank sizing, heating source, return flow strategy, utility capacity, floor drainage, and control integration are just as important as the basic type selection. The performance of a CIP system depends on hardware selection as much as it depends on cycle logic. A strong sanitation recipe cannot overcome poor equipment choices. The most important elements include spray devices, supply and return pumps, hygienic valves, instrumentation, heat management, and the control layer. Spray devices matter especially in tanks, vessels, and kettles. Static spray balls can work well where complete wetting is achievable, but rotary jet heads may be preferred where higher impact cleaning is needed. Pump sizing must ensure turbulent flow throughout the circuit, not just high pressure at the skid. Valves are another frequent weak point. Poor seat leakage management or dead-leg-prone routing can compromise otherwise solid systems. Hygienic design standards, accessibility for inspection, and validation support are all critical. Sensors should not be treated as accessories; they are what convert CIP from a wash routine into a controlled sanitation process. Manufacturers planning capital projects often need more than a skid fabricator. They need expertise in process, controls, mechanical, electrical, plumbing, and utility integration. Firms such as Disruptive Process Solutions support food and beverage clients with cross-functional engineering, including PLC programming, automation, SCADA integration, and utility infrastructure needed to make sanitation systems perform in the real world. This broader technical scope matters when CIP must coordinate with boilers, chilled water, compressed air, batching systems, aseptic processes, or high-care environments. While cycle details vary by product and equipment, most CIP sequences follow a structured progression. The purpose of each step is different, and skipping or poorly tuning one step can reduce the effectiveness of all others. Product recovery is often overlooked, yet it can materially improve returns. In high-value lines such as dressings, dairy beverages, nutraceutical drinks, or flavor bases, product pushout can reduce waste before the wash even begins. Pre-rinse removes the bulk load, making the chemical wash more effective. Caustic breaks down organic soils; acid may be required where mineral deposition is a recurring issue. Sanitization may be chemical or thermal depending on the validated standard. Final release should never rely on assumptions. It should be tied to measurable criteria and documented procedures. For plants handling allergen changeovers, CIP timing and verification are especially important. The sanitation method must align with the facility’s preventive controls program and allergen management plan. That often means tighter endpoint validation and more disciplined swab review. The quality of fabricated equipment has a direct impact on CIP results. Smooth internal finishes, sanitary welds, drainability, correct nozzle placement, and reliable tank geometry all matter. Processors evaluating custom skids or vessels should consider suppliers with hands-on manufacturing capabilities, including sanitary tank fabrication and custom process equipment. Custom process equipment for food and beverage plants can be especially useful when standard OEM offerings do not match line layout, throughput, or utility constraints. In the United States, CIP design and operation should support a plant’s broader food safety management system. CIP itself is not a regulation, but it is frequently part of how a facility meets sanitation, preventive control, and verification expectations under FSMA, HACCP, and GMP frameworks. Under FSMA, plants must identify hazards and implement risk-based preventive controls. For many products, inadequate cleaning can create biological, chemical, or allergen hazards. A validated CIP program helps show that sanitation procedures are capable of controlling those risks. In HACCP environments, sanitation may support prerequisite programs or directly affect hazard control strategies, depending on the process. GMP requirements reinforce the need for cleanable equipment, hygienic operations, and documented procedures. The value of CIP in audits is straightforward: it reduces variability and improves records. If conductivity, time, flow, and temperature are captured by the control system, QA and operations can review actual execution rather than relying only on handwritten checklists. This becomes especially important in multi-site organizations or co-manufacturing networks. Standardized recipes help align plants in North Carolina, California, Texas, and the Midwest under a common sanitation logic. For enterprise clients, that consistency can simplify training, troubleshooting, and internal benchmarking. CIP brings value across many sectors, but the business case and design priorities differ by industry. Dairy: Dairy systems often involve proteins, fats, mineral films, and strict microbiological expectations. That makes CIP a natural fit for milk receiving, standardization, pasteurization loops, yogurt bases, cultured products, and dairy beverages. In regions such as Wisconsin, Idaho, and upstate New York, mature dairy operations often seek higher automation and water recovery. Bakery: Not every bakery process is CIP-friendly, but fillings, liquid ingredients, syrups, chocolate handling, and batter preparation systems can benefit significantly. The key challenge is matching cleaning chemistry to sticky or viscous residues. Sauces, marinades, and dressings: These lines often present high viscosity, oil phases, spices, particulates, and allergen concerns. CIP is valuable for changeover speed and allergen control, especially in co-packing operations serving multiple brands. Ready-to-eat foods: RTE facilities need strong sanitation discipline because post-lethality contamination risks can have severe consequences. Closed-system mixing, transfer, thermal processing support, and filler sanitation all benefit from validated CIP routines. Processed foods and ingredients: From soups to beverage bases to plant-protein slurries, any process involving closed transfer and repeated product families can often justify CIP when downtime costs are high enough. The chart above reflects the relative strength of CIP demand by segment. Demand is strongest where closed processing, high sanitation sensitivity, and frequent product changeovers overlap. The most visible benefit of CIP is reduced manual labor. But in well-run plants, the larger payoff often comes from consistency. A validated recipe that runs the same way every time reduces dependence on tribal knowledge and lowers the chance that a rushed crew will under-clean or over-clean a line. Labor savings can be meaningful in labor-constrained markets, but so can utility optimization. Modern systems can reduce water usage through recovery logic, shorten changeovers through better endpoint detection, and lower chemical loss with conductivity-guided transitions. These gains add up across hundreds of annual cycles. Audit readiness is another major benefit. Food safety and quality teams need records. CIP systems that capture cycle completion, alarm conditions, temperatures, concentrations, and operator interventions provide more defensible sanitation documentation than paper-only systems. When evaluating a CIP project, focus on total installed value rather than skid price alone. Ask whether the proposed design fits your current and future throughput. Review utility loads, control integration, line routing, sanitation validation, and operator usability. Clarify whether the provider can support engineering, installation, commissioning, and startup, not just fabrication. This is where service capability matters. Companies with a full project model can manage the work from concept to production release, coordinating local trades, controls, utility tie-ins, startup, and schedule risk. Project case examples in food and beverage facilities are useful for understanding whether a partner has delivered under real plant conditions, especially where uptime and profitability matter. A Midwest sauce facility may justify CIP based on allergen changeover speed and reduced sanitation labor. A Texas beverage co-packer may prioritize centralized utility integration and production scalability. A California dairy processor may focus on water recovery and wastewater load reduction. An RTE plant near Atlanta may put the greatest value on validation, traceability, and consistent execution across shifts. The right system is the one that reflects the operating model, not just a generic specification sheet. U.S. buyers often compare local stainless fabricators, OEM skids, and full-service integration firms. Local fabrication can be attractive for freight and access, particularly near manufacturing corridors such as Chicago, Charlotte, Raleigh-Durham, Los Angeles, and Houston. However, the best outcome usually comes from suppliers who can connect fabrication quality to process engineering, controls, and field execution. That is especially true when retrofitting active plants where tie-in windows are short and downtime is expensive. Disruptive Process Solutions serves food and beverage manufacturers across all 50 states and Canada, with a practical focus on profitable capital execution. For CIP projects, that means aligning sanitary design, utility planning, custom equipment, controls, and installation into one accountable delivery model rather than treating the skid as a standalone purchase. This approach is particularly valuable for multi-discipline projects involving tanks, process piping, automation, and startup support. Looking ahead to 2026, three trends are shaping CIP decisions in the United States. First is smarter automation: better analytics, recipe optimization, remote diagnostics, and stronger integration with MES and SCADA platforms. Second is policy and compliance pressure: sanitation documentation, allergen control, and environmental reporting are becoming more structured across enterprise operations. Third is sustainability: water reuse, chemical optimization, and energy recovery are gaining priority as utilities and wastewater costs rise. Plants planning major expansions today should consider whether their CIP platform can support future digital reporting, additional circuits, and more aggressive sustainability targets. The cheapest system today may become the most expensive to operate or retrofit in two years. CIP is commonly used on tanks, pipelines, heat exchangers, fillers, blenders, HTST systems, dosing systems, and some vessels with internal spray coverage. It works best on closed, hygienically designed equipment. For closed systems that run repeatedly and require consistent sanitation, yes. Manual cleaning still has an important role for exteriors, open equipment, and specialty tasks, but it is harder to standardize and document. Cycle time depends on product, soil load, equipment size, and validation requirements. Some light-duty systems may clean in under an hour, while more demanding allergen or dairy applications can take significantly longer. No. Acid is often used where mineral scale or inorganic deposits are a problem, such as in dairy or hard-water environments. The need should be determined by soil type, water chemistry, and validation results. Yes. Recovery designs, conductivity-based switching, better endpoint control, and optimized recipes can materially reduce water and chemical consumption, especially in high-cycle plants. Single-use systems discharge more of the cleaning media after each cycle. Recovery systems reclaim selected rinse or chemical streams for reuse where validated and appropriate. Recovery offers savings but requires stronger controls. Very important if the goal is repeatability, traceability, and lower operator dependency. Automation enables consistent flow, temperature, timing, and documentation, all of which support food safety and throughput. Ask about validation support, utility requirements, future expansion, sanitary design details, control architecture, spare parts strategy, field installation scope, startup assistance, and record-keeping capabilities. Often yes, but success depends on line geometry, drainability, valve arrangement, floor space, and utility capacity. Older facilities may need piping changes, control upgrades, or localized skids instead of a central system. Manufacturers that want engineering, custom equipment, installation, controls integration, and accountable project management under one delivery structure are generally the best fit. This is particularly helpful for growing food and beverage operations managing complex timelines or multi-line expansions. For U.S. food and beverage manufacturers, clean-in-place is no longer just a sanitation option. It is a strategic tool for safe growth, labor efficiency, and operational discipline. The right system should be designed around product realities, utility constraints, compliance needs, and future production goals. When those factors are aligned, CIP becomes a measurable driver of plant performance. -
2026 Compressed Air Efficiency Guide for Food Facilities
Compressed air remains one of the most expensive utilities in American food and beverage manufacturing, yet it is often treated as a background system until quality, downtime, or energy costs become painful. In 2026, the most successful facilities in the United States will not simply buy a bigger compressor. They will assess the full system, repair leaks, stabilize controls, lower pressure where possible, verify air quality at food contact points, recover waste heat, and maintain assets using data instead of guesswork. For plants in major manufacturing corridors such as Chicago, Atlanta, Dallas-Fort Worth, Los Angeles, Charlotte, and the Port of Savannah region, compressed air strategy now affects production margin, audit readiness, and expansion economics. Food processors, dairy plants, protein operations, beverage bottlers, breweries, RTD manufacturers, and aseptic facilities all use compressed air differently. A poultry processor in Arkansas may prioritize reliability for pneumatic controls and packaging equipment, while a beverage co-packer near Houston may focus on dry, oil-managed air for filling lines and utility stability across fast changeovers. A sauce manufacturer in New Jersey may struggle with pressure drops across legacy piping, and a dairy facility in Wisconsin may need better dew point control to protect sensitive valves and actuators. Because of those differences, system design and optimization should be tied to the process, sanitation plan, and long-term capital model, not just compressor horsepower. The fastest path to compressed air savings in United States food facilities is usually this six-step sequence: assess the system, fix leaks, optimize compressor sequencing, reduce unnecessary pressure, confirm air quality at food contact applications, and formalize predictive maintenance. Many plants can reduce compressed air energy use by 15% to 30% without sacrificing throughput. Facilities with poor controls, chronic leakage, oversized machines, or excessive pressure often see even larger gains. For buyers comparing equipment or engineering support, the best advice is to avoid evaluating compressors as standalone products. The real buying decision should include air demand profile, storage capacity, controls architecture, piping layout, filtration, drying, condensate management, heat recovery potential, utility redundancy, and food safety implications. In high-volume markets such as California, Texas, North Carolina, and the Midwest, utility costs, labor constraints, and aggressive production schedules make lifecycle value far more important than lowest bid. Typical compressed air product categories used in food and beverage plants include oil-flooded rotary screw compressors, oil-free screw compressors, reciprocating boosters, refrigerated dryers, desiccant dryers, filtration trains, wet and dry receivers, automatic drains, point-of-use regulators, flow meters, and master control systems. The right mix depends on whether the air serves packaging, valve actuation, product blow-off, clean-in-place automation, fermentation support utilities, or direct/indirect food contact applications. The table above shows why compressed air projects are often phased. Leak reduction and pressure optimization usually deliver the quickest payback, while air quality upgrades and heat recovery bring broader operational value. Plants serving export channels through ports such as Long Beach, Newark, Houston, or Savannah may also prioritize reliability and auditability because shipping schedules leave little room for utility failure. The market trend chart reflects a realistic increase in U.S. investment driven by rising electricity prices, ESG reporting pressure, utility rebate programs, and the need to expand production efficiently. In 2026, plants are expected to prioritize systems that can scale with growth rather than one-time fixes. A proper compressed air system assessment starts with the process, not the compressor room. Engineers should document where air is used, what pressure each use point actually needs, when demand spikes occur, which areas are quality sensitive, and where downtime risk is concentrated. This matters because food plants often operate mixed loads: packaging lines, process valves, ingredient handling, conveyors, palletizers, blow-off stations, and instrument air can all sit on the same system even though they have different requirements. In 2026, the most valuable assessments in the United States combine field measurements with operational context. Key data points include compressor power draw, loading profile, discharge pressure, system pressure at critical users, pressure differential across filters, dryer performance, dew point, flow rate by shift, and storage behavior during peak demand. Facilities in older industrial areas such as Cleveland, St. Louis, or parts of Philadelphia often discover that legacy piping layouts create artificial demand because long runs, undersized headers, and dead legs increase pressure drop. Assessment should also identify whether the plant needs one central utility standard or multiple air classes. For example, direct food contact or product-adjacent air may justify higher filtration and tighter verification protocols than general pneumatic utility air. Plants that fail to separate these service levels can overspend everywhere or underprotect the most critical applications. The table above shows how an assessment turns scattered symptoms into capital priorities. Instead of replacing equipment blindly, the plant can decide whether the problem is really leakage, controls logic, treatment equipment, or process demand mismatch. Case-driven decision making is especially important for expanding facilities. A co-packing site near Phoenix adding a second line may not need another compressor if storage, sequencing, and piping are corrected. A seafood processor in the Pacific Northwest may need improved drying and condensate control more than additional horsepower. A brewery in Colorado may benefit from separate utility zones for packaging and cellar operations. Assessment reveals the least-cost path to stable capacity. Leak management is still the highest-return compressed air initiative for many U.S. food facilities. Leaks commonly appear at quick-connects, flexible hoses, valve manifolds, FRL assemblies, solenoids, regulator stations, unused drops, drain traps, and packaging equipment interfaces. In washdown environments, repeated cleaning, vibration, and thermal cycling accelerate failure of seals and fittings. Effective leak programs are not one-time hunts. They are ongoing management systems with tagging, repair deadlines, verification, and accountability by area. Best practice includes ultrasonic inspection during production and non-production hours, leak severity scoring, repair prioritization by cost, and monthly validation of residual leak load. In plants with multiple buildings or utility zones, each zone should have a baseline so managers can see whether losses are returning. For food and beverage operations, leak repair has a second benefit beyond energy savings: it reduces pressure instability. That can improve filling consistency, actuator response, packaging uptime, and instrument reliability. In facilities running tight labor schedules, fewer nuisance utility problems can matter as much as the energy cost reduction itself. The table makes clear why a leak program should be built into maintenance planning. Some of the largest air losses come from small devices that are easy to overlook. In a large protein plant in the Southeast or a dairy campus in California’s Central Valley, dozens of moderate leaks can equal the output of an entire small compressor. By 2026, more facilities are linking leak management to digital work order systems and utility dashboards. Trend data helps supervisors justify repairs during planned downtime rather than waiting for a breakdown. Plants that already use broader engineering support for utility systems can integrate leak management into a larger reliability plan through partners such as food and beverage engineering services that connect compressed air actions with process uptime, sanitation requirements, and project sequencing. Compressor controls are a frequent source of hidden waste. Plants often add equipment over time without redesigning control logic, leaving multiple machines to load and unload inefficiently. The result can be excessive no-load power, wide pressure bands, poor trim behavior, and avoidable wear. This is especially common in facilities that have expanded in phases around Memphis, Indianapolis, Omaha, or the Inland Empire. Optimization starts with defining the true base load and trim load. A stable base compressor should handle the predictable demand range efficiently, while a trim compressor responds to variation. In larger systems, a master controller can sequence units according to efficiency curves, operating limits, maintenance status, and redundancy needs. Storage placement also matters. Properly sized receiver capacity can absorb transients so the compressors do not chase every short event. Variable speed compressors can be valuable, but only when correctly sized and integrated. They are not automatic solutions for every plant. A poorly applied VSD machine running outside its efficient zone can disappoint just as badly as an old load-unload setup. The key is system design, not brand marketing. The industry demand chart shows that beverage, aseptic, and protein operations are likely to lead compressed air optimization efforts in 2026 because their uptime and quality exposure are especially high. Prepared foods and dairy also remain strong markets, particularly where packaging automation and sanitary process control are extensive. Controls optimization is one of the areas where technical depth matters. A multidisciplinary engineering team that understands process loads, automation, electrical integration, and project execution can align utility design with production goals. That is where firms such as Disruptive Process Solutions add value through broad process, mechanical, electrical, controls, and SCADA capabilities, pairing compressed air decisions with the realities of line behavior, expansion planning, and plant-wide utility coordination. Many food facilities operate at higher pressure than they need because historical setpoints were never revisited. Every unnecessary increase in header pressure raises power consumption and often increases leakage rate. It can also mask poor piping design or neglected maintenance. Demand reduction should therefore start with measurement and root cause analysis, not arbitrary setpoint cuts. The practical method is to identify the highest legitimate pressure requirement in the plant, then work backward. If a packaging OEM needs 92 psig at the machine but the header is running 115 psig, the real issue may be pressure drop through undersized filters, regulators, or branch lines. Fixing those restrictions may allow the central system to operate significantly lower. Point-of-use boosters or isolated high-pressure zones can be more efficient than keeping the whole plant elevated. Demand reduction also includes eliminating inappropriate uses of compressed air. Open blow-offs for product movement, cooling, or cleaning should be reviewed carefully. In some cases, blowers, fans, or mechanical alternatives provide lower lifecycle cost. In sanitation-sensitive spaces, alternatives must still support hygienic design, but the review is worth doing. The buying takeaway from this table is simple: not every savings opportunity requires a new compressor. In many plants, pressure control, piping, and point-of-use design create more value than additional horsepower. This is especially relevant for sites facing capacity growth around trade hubs like Nashville, Kansas City, and Northern New Jersey, where speed-to-production matters and capital discipline is tight. The trend shift chart illustrates how buyer behavior is changing. More projects now prioritize system efficiency and right-sizing before equipment replacement, a sign of more mature capital planning across the United States food manufacturing base. Air quality is one of the most important and most misunderstood parts of compressed air strategy in food plants. Not all compressed air touches food directly, but when it does—or when it contacts product zones, packaging interiors, or sensitive equipment surfaces—the air must be treated and verified according to the application risk. The correct standard depends on the process, facility program, customer requirements, and audit framework. Critical variables include particulate control, oil aerosol management, vapor carryover, microbial risk, moisture level, and point-of-use filtration. Air class strategy should distinguish between instrument air, utility air, and higher-purity air used near product contact points. Validation protocols should define where testing occurs, what is tested, and how frequently. This is especially important in dairy, aseptic beverage, protein packaging, and ready-to-eat environments. Plants exporting through national retail channels or serving private-label programs often face tighter documentation expectations. In these environments, air treatment cannot be an afterthought. Filtration, dryer selection, drain reliability, piping materials, and sampling points should all be engineered with quality control in mind. The table highlights why “clean enough” is not a safe operating principle. Air quality must be designed for the actual application. Manufacturers that need support aligning compressed air with broader process compliance can benefit from an engineering partner with experience in FDA, USDA, SQF, and BRC environments, as well as beverage, dairy, protein, and aseptic systems. More detail on multidisciplinary execution can be found through the DPS team and approach, which emphasizes practical engineering tied to profitability and compliance. From a 2026 trend perspective, expect more U.S. plants to install permanent dew point monitoring, additional point-of-use filtration verification, and digital quality records for compressed air systems. Retailer scrutiny, customer audits, and internal ESG programs are pushing utilities toward better documentation and tighter risk management. Air compressors reject a large share of input energy as heat. In a food plant, that heat can often be recovered for useful purposes such as boiler makeup preheat, washdown water preheat, domestic hot water support, or seasonal space heating in warehousing and utility zones. Recovery opportunities are strongest where compressors run many hours per year and where there is nearby, consistent thermal demand. For example, a beverage plant in Texas may recover heat to support hot water loads, while a Midwestern prepared foods facility may use recovered heat during colder months for adjacent utility spaces. A dairy site with high cleaning demand may find water preheat especially attractive. The economics depend on compressor size, run profile, distance to the thermal load, control strategy, and whether the facility can use the heat year-round. Heat recovery should be reviewed alongside broader utility planning. When compressor room ventilation, boiler systems, water heating, and controls are designed together, the value can be much greater than a standalone retrofit. This is one reason integrated project execution often outperforms isolated equipment upgrades. Disruptive Process Solutions brings relevant manufacturing and integration depth here because the company not only engineers utility systems but also supports custom equipment, utility infrastructure, installation, and turnkey integration. That blend is useful when compressed air heat recovery must connect with process water systems, skids, controls, and plant construction sequencing without disrupting production. The comparison chart reflects a common buyer reality: supplier choice matters. A standalone vendor may be fine for a like-for-like replacement, but food plants often need broader system thinking. Integrated engineering partners usually score highest when the project touches process risk, compliance, multiple utilities, layout constraints, and line expansion. When evaluating local suppliers or project partners in the United States, buyers should ask about food-specific references, utility modeling, controls integration, commissioning support, startup sequencing, and understanding of sanitary operations. Plants near major manufacturing clusters like Raleigh-Durham, Minneapolis, Cincinnati, and Southern California often have many equipment sellers available, but fewer firms can tie the compressor room to production economics and food safety expectations. Compressed air systems drift toward inefficiency unless maintenance and monitoring are disciplined. Filters load, drains fail, couplings leak, dryers lose performance, controls get bypassed, and setpoints change. Plants with strong maintenance scheduling keep these issues from turning into chronic cost or quality problems. A modern maintenance program should include routine inspection, condition-based tasks, documented filter changes, dew point checks, drain verification, motor and vibration review, oil analysis where applicable, leak rounds, and periodic system audits. Monitoring should combine at least pressure, flow, and power, with alarms for critical deviations. In larger sites, trend dashboards can identify rising specific power, increasing off-shift flow, and declining dryer performance before the operators feel the consequences. For companies managing growth projects, maintenance planning should start in design. New compressors, dryers, receivers, and piping should be accessible, labeled, isolated properly, and connected to the plant’s CMMS and controls environment. That reduces lifecycle friction and makes optimization durable. This table shows that monitoring is not just about maintenance compliance; it is about preserving capacity and protecting product. A well-kept compressed air system can delay major capital spending, improve line reliability, and support sustainability reporting. In 2026, plants are increasingly integrating compressed air data into broader energy management and SCADA visibility, especially where multi-utility optimization is a strategic priority. Policy and sustainability trends also matter. More utilities across the United States are supporting audits, controls upgrades, VSD applications, heat recovery, and leak reduction through rebates. At the same time, corporate decarbonization goals are pushing manufacturers to measure compressed air performance more closely. Since compressed air is an electricity-intensive utility, efficiency gains contribute directly to scope-related energy reductions and cost resilience. Disruptive Process Solutions serves food and beverage manufacturers across the United States and Canada with a practical, project-based engineering model designed around profitability, speed, and accountability. Rather than acting as a generic contractor, DPS approaches capital work as a business-minded manufacturing partner that connects utility design, process performance, and execution risk. On the technology side, DPS supports structural, mechanical, plumbing, electrical, process, and controls engineering, including PLC programming, automation, and SCADA. That technical breadth is valuable for compressed air projects because the system rarely stands alone. Pressure stability, controls logic, packaging reliability, CIP functionality, energy monitoring, and utility interlocks all benefit when engineers understand how air interacts with the rest of the plant. This capability is especially useful for facilities planning new lines, expansions, relocations, or major retrofits. Companies evaluating integrated solutions can review engineering and project services to see how air systems fit into larger utility and process programs. On the manufacturing side, DPS designs and supplies process equipment and utility-related systems as part of broader turnkey delivery. Its experience spans beverage and food applications including fermentation systems, pasteurization, aseptic processing, blending, filtration, dairy systems, protein processing, prepared foods, and utility infrastructure such as CIP, boilers, cooling systems, refrigeration, water treatment, and compressed air. For clients that need coordinated equipment and utility execution, this combination reduces handoff risk. More on equipment capabilities is available through process equipment solutions. On the service side, DPS operates through a Design Build Manage approach that combines engineering, general contractor-style execution, local trade coordination, installation, integration, commissioning, owners representation, and capital planning support. That model can be especially valuable when compressed air improvements need to be implemented during active production, linked to multiple trades, or tied to broader expansion economics. The company works across all 50 states, including projects in fast-growing food and beverage markets where timing and operational continuity are critical. For examples of execution thinking and project outcomes, see selected case experiences. For U.S. buyers, the practical advantage is this: compressed air decisions become stronger when they are tied to long-term throughput, utility integration, compliance needs, and capital efficiency. That is the space where DPS is positioned to help—especially for manufacturers that want honest recommendations, disciplined planning, and a partner willing to challenge expensive assumptions when a smarter path exists. What is the best first step for a food plant with high compressed air costs?Start with a measured system assessment that captures flow, pressure, power, leakage, dryer performance, and end-use requirements. Most plants should not buy new compressor capacity until these basics are known. How much energy can a United States food facility save?Many facilities achieve 15% to 30% savings through leak repair, controls optimization, pressure reduction, and maintenance improvements. Some plants with severe inefficiencies do better than that. Do food plants always need oil-free compressors?No. The correct choice depends on the application, risk level, treatment train, and quality verification plan. Some direct or high-risk uses may justify oil-free approaches, while other plants can meet requirements with well-engineered treatment and monitoring. How often should compressed air leaks be surveyed?Monthly or quarterly is common, depending on plant size, washdown intensity, and production hours. Facilities with frequent changeovers or harsh cleaning environments often need more attention. Is heat recovery really worth it?Often yes, especially where compressors run many hours and the plant has steady hot water or space-heating demand. The economics improve when heat recovery is designed as part of a larger utility project. What industries benefit most from compressed air optimization?Beverage, dairy, protein, aseptic, prepared foods, bakery, and co-packing operations all benefit. The exact priorities differ by application, but nearly every food and beverage segment can reduce cost and improve reliability. What are the main 2026 trends?Expect more digital monitoring, stronger air quality verification, more utility rebate participation, greater emphasis on heat recovery, and wider use of integrated controls tied to plant SCADA and energy management platforms. How should a buyer compare local suppliers?Look beyond equipment price. Compare food-industry experience, controls capability, treatment design knowledge, commissioning support, project management strength, and the ability to work inside active production plants. Can compressed air upgrades support sustainability goals?Yes. Because compressed air consumes significant electricity, efficiency improvements lower operating cost and reduce the energy intensity of production. Heat recovery can further reduce fuel or water-heating demand. When should a plant bring in an integrated engineering partner?Bring one in when the project affects multiple utilities, food safety risk, process reliability, expansion planning, or phased installation during production. At that point, system integration matters more than simple equipment replacement. -
Beverage Plant Controls Integration
Beverage plant controls integration is the practical work of connecting field devices, PLCs, skids, packaging equipment, SCADA, historians, MES tools, and cloud analytics into one reliable operating environment. In the United States, the strongest projects are not the ones with the most software layers. They are the ones that improve throughput, reduce downtime, simplify sanitation, support food safety, and give operations teams one trustworthy source of production truth. For beverage manufacturers running breweries, RTD lines, juice systems, dairy beverage plants, carbonated soft drink lines, spirits operations, and aseptic processes, integration has become a business requirement rather than an optional automation upgrade. That requirement is growing across major production corridors such as Chicago and Milwaukee for brewing, California wine and functional beverage regions, the Carolinas for co-packing and food-grade utilities, Texas for fast-growing manufacturing relocation, and logistics-heavy markets near the ports of Los Angeles, Long Beach, Houston, Savannah, and Newark. Plants that once accepted isolated fillers, standalone pasteurizers, or packaging machines now need plantwide visibility, traceability, OEE reporting, recipe consistency, utility coordination, and better capital planning. This is where disciplined engineering and controls strategy matter. For teams evaluating an integration partner, it helps to work with a firm that understands both process and execution. Disruptive Process Solutions approaches beverage projects from a business and operations standpoint, aligning process engineering, controls, installation, and startup with profitability goals instead of treating integration as a software-only exercise. The fastest answer is this: beverage plant controls integration should create a standard, secure, and scalable data and control architecture from sensors on the floor to dashboards in the cloud. In most U.S. beverage facilities, that means connecting instruments, VFDs, valve manifolds, analyzers, and motor control to PLC platforms; standardizing alarms, tags, and naming; bringing line and utility data into SCADA or a modern visualization layer; and publishing contextualized production data to historians, MES tools, ERP connections, and cloud analytics. A good integration strategy also respects reality. Most beverage plants are not greenfield facilities with one automation vendor. They are patchworks of expansions, acquisitions, OEM packages, and legacy upgrades. A syrup room may be Allen-Bradley, a tunnel pasteurizer may be Siemens, a water treatment skid may be Schneider, and the packaging line may include multiple proprietary machine controllers. The right integration plan does not force everything into a single vendor at all costs. It creates interoperability, cybersecurity, maintainability, and clean data models that operations teams can actually use. For buyers, the main decision criteria are straightforward: can the architecture reduce downtime, improve changeovers, support food safety documentation, scale to additional lines or sites, and stay maintainable by internal staff after startup? If the answer is yes, the investment usually pays back through throughput, labor efficiency, lower waste, and smarter capital allocation. The beverage production stack begins at the process edge. This includes flow meters, pressure transmitters, temperature RTDs, conductivity probes, inline Brix instrumentation, dissolved oxygen analyzers, level sensors, barcode readers, checkweighers, and vision systems. These devices feed PLCs and local machine controllers. Above that sit HMI and SCADA layers, historians, OEE and MES applications, quality systems, ERP connections, and cloud data lakes or analytics platforms. In U.S. beverage operations, the challenge is not merely collecting data. It is contextualizing data. A filler speed number without SKU context, sanitation state, operator assignment, or upstream tank batch ID is only partial information. The architecture must define what the signal means, where it originated, when it changed, and how it maps to production events. This is especially important for regulated or audit-sensitive environments such as dairy beverages, low-acid products, or aseptic systems. This stack works best when the plant starts with a clear naming convention, agreed tag hierarchy, equipment states, time synchronization rules, and line segmentation strategy. Teams that skip this foundation often end up with attractive dashboards that no one trusts. From a technology perspective, DPS supports the controls and process side together, blending PLC programming, automation, SCADA, utilities coordination, and complete system integration with broader mechanical, process, electrical, and project engineering. That cross-disciplinary view matters because beverage integration failures often begin with process assumptions, not software bugs. Multi-vendor environments are normal in beverage manufacturing. A U.S. plant may have Rockwell Automation in brewhouse controls, Siemens in pasteurization or utilities, and Schneider Electric in power, water, or OEM skids. Integration success depends on choosing a practical interoperability method rather than trying to rewrite everything into one platform. In many cases, the best model is to preserve stable local control in the native PLC while exposing standardized line and equipment data to a plantwide layer. OPC UA, MQTT with Sparkplug, industrial gateways, and carefully designed API or database interfaces can all serve this model. The key is to keep machine safety and deterministic control local while sharing production states, counts, recipes where appropriate, and event data upward. For plant leadership, the buying advice is simple: require an interface document before procurement or FAT. It should define protocols, ownership of tags, recipe authority, downtime state mapping, cybersecurity zones, remote access rules, and exact deliverables for commissioning support. This prevents late-stage disputes between OEMs, integrators, and plant engineering. In the United States, this is especially relevant when expansions happen under aggressive schedules in Dallas-Fort Worth, Atlanta, or Phoenix, where line startup dates are often tied to retailer commitments or seasonal demand. A multi-vendor strategy built early reduces startup chaos. OEM equipment integration is where many beverage projects win or lose value. Fillers, depalletizers, rinser/fillers/cappers, tunnel pasteurizers, flash pasteurizers, carton erectors, tray packers, sleevers, labelers, palletizers, and CIP skids each come with their own controls philosophy. Some OEMs expose rich diagnostics and production counters. Others provide only the minimum interface required to run. The integration goal should be to capture the machine states that operations actually need: mode, run permissive, fault category, current product, actual speed, target speed, reject counts, starved and blocked conditions, sanitation mode, maintenance bypasses, and utility demand. It is equally important to map upstream and downstream dependencies. A filler slowdown means something different if it is caused by low product level, capper faults, conveyor accumulation, or label supply interruptions. Plants should also insist on a commissioning matrix showing who owns dry testing, wet testing, utility verification, recipe testing, line integration, and data validation. That avoids the all-too-common problem where every vendor says the issue is someone else’s responsibility. DPS also brings in a manufacturing perspective beyond controls. The company designs and supplies process equipment such as storage and process tanks, custom CIP systems, marination and cooking systems on the food side, and broader beverage infrastructure including blending, pasteurization support, and utility-connected process hardware. For plants trying to integrate mechanical scope and controls scope together, that can remove handoff gaps that typically slow startup. Real-time data architecture has shifted significantly in modern beverage facilities. Traditional point-to-point polling still exists, but more U.S. manufacturers are evaluating publish-subscribe models using MQTT and Sparkplug. The reason is flexibility. Instead of every application requesting data directly from every PLC, edge nodes publish structured data once, and approved consumers subscribe as needed. The Unified Namespace, or UNS, is a data architecture concept in which the business defines a common plant and enterprise data model. Rather than creating separate meanings for the same filler, SKU, batch, or line state in every software package, the UNS acts as a shared context layer. For beverage operations with multiple lines, seasonal SKU shifts, co-packing complexity, or multi-site reporting needs, this can be powerful. Still, the UNS is not a magic product. It requires disciplined governance, topic naming, payload standards, event definitions, and change control. Plants that rush into MQTT without a data ownership model can create a new kind of disorder. By 2026, more U.S. beverage producers are expected to combine edge computing, MQTT-based event flow, and cloud analytics with sustainability dashboards. That will make it easier to correlate throughput, water use, steam demand, compressed air consumption, and product loss at the line or SKU level. Policy pressure around energy use, ESG reporting, and traceability will continue to push architectures toward better plantwide data consistency. The chart above reflects a realistic growth pattern in U.S. demand for automation modernization, data visibility, and line integration. Growth is being driven by labor constraints, SKU complexity, retailer service expectations, and capital scrutiny. OEE monitoring is one of the most common reasons plants pursue integration, but it is also one of the most commonly mishandled. OEE only works when availability, performance, and quality are defined consistently across lines and shifts. A can line, PET line, glass line, and aseptic carton line cannot always be measured with identical event assumptions. The plant needs a standard framework with line-specific nuances. For example, a filler waiting on sanitized product may count differently from a line waiting on warehouse pallet supply. Planned sanitation, flavor changeover, and allergen changeover should not be mixed carelessly with unplanned downtime. If they are, the OEE number may look precise while telling management the wrong story. When multiple lines are involved, the plant should define one downtime reason tree and one governance process for adding or changing codes. OEE should also connect to maintenance planning and utility performance, not just production scoreboards. This demand profile aligns with current U.S. market dynamics. Functional beverages, RTD products, and aseptic lines tend to require stronger integration because of higher SKU churn, traceability demands, and tighter process control expectations. Technology alone does not deliver results. Beverage integration projects often underperform because operators, supervisors, maintenance teams, and sanitation leaders are brought in too late. A dashboard that nobody trusts, a downtime code tree that nobody uses correctly, or a CIP sequence that confuses night shift will weaken ROI quickly. Change management should begin at design. That means involving operators in HMI layout review, maintenance in alarm philosophy and remote access planning, quality teams in audit trail requirements, and operations leadership in KPI definitions. Workforce training should include not only button-level instruction but also why the new architecture exists, what decisions it supports, and what actions are expected from each role. By 2026, plants are likely to invest more in digital work instructions, role-based mobile alerts, remote subject matter support, and simulation-based startup training. This is especially helpful for high-growth co-packers and multi-shift plants where turnover or seasonal hiring can undermine consistency. For service capability, DPS is strongest when projects need more than isolated programming support. Its model spans capital planning, feasibility, owner’s representation, general contracting where licensed, end-to-end project and program management, installation coordination, commissioning, and controls integration. You can review the breadth of these capabilities through its engineering and project services, which are structured to keep execution aligned across disciplines. Scalability is one of the most important buying criteria for U.S. manufacturers. Many plants begin with one integration target such as a packaging line OEE project, but later want utility monitoring, batch traceability, warehouse connectivity, enterprise reporting, or replication to another site. If the first project is too custom or too vendor-locked, scaling becomes expensive. A scalable architecture usually includes standard naming, reusable code libraries, segmented industrial networks, edge data collection, a clear plant model, documented APIs or publish-subscribe topics, role-based access, and template-based dashboarding. It also includes capital realism. Not every single line needs a full MES stack. In many cases, a staged roadmap creates a better return. Single-site beverage operators in places like St. Louis, Grand Rapids, or Sacramento may only need line-level visibility first. Multi-site beverage groups with plants in the Southeast, Midwest, and West Coast will benefit more from a structured enterprise data model from the start. In both cases, the plant should design for the next step, even if it does not buy everything immediately. The trend above shows the gradual shift from tightly coupled plant integrations to more flexible event-driven architectures. Adoption will vary by plant size, IT maturity, and regulatory needs, but the direction is clear. Most integration failures are predictable. The most common mistake is starting with software screens instead of business goals. Plants often ask for dashboards before they define the decisions the dashboard should drive. Another frequent error is ignoring utility systems. A line may appear to have a filler problem when the root cause is compressed air instability, glycol temperature drift, or CIP timing conflicts. Another trap is poor documentation. Without a current network map, controls narrative, sequence of operations, tag list, alarm matrix, and FAT/SAT records, the plant becomes dependent on tribal knowledge. This increases risk during expansions, staffing changes, and audits. A practical way to reduce these risks is to choose a partner with both field execution and capital project discipline. On larger beverage projects, controls decisions are tied to utility routing, process safety, sanitation design, line layout, startup sequencing, and contractor management. That is why many manufacturers prefer integrated delivery rather than fragmented specialist handoffs. Below are common questions from U.S. beverage producers evaluating plant controls integration. For a single packaging line OEE and data visibility project, timelines may range from 8 to 16 weeks depending on OEM access and plant shutdown windows. For a full process-to-packaging integration with utilities, recipes, and reporting, timelines are commonly several months and should be aligned with equipment FAT, installation, SAT, and startup plans. Not always. Standardization helps maintenance and training, but forcing a full platform conversion can create unnecessary cost and risk. In many cases, keeping proven local controls in place and standardizing data exchange, visualization, and governance is the better business decision. Usually one of three: packaging line OEE, utility performance monitoring, or process visibility for a bottleneck area such as blending, pasteurization, or filling. The best first step is the one that produces a measurable operating decision quickly. Use a phased architecture. Legacy PLCs may require protocol converters, edge gateways, or read-only data extraction while newer machines can publish richer real-time data. Plan the migration path so old assets do not block future scalability. It is essential. Remote access for OEMs, cloud analytics, and plantwide networking create risk if poorly managed. Segmentation, user roles, secure remote access, patch governance, and documented ownership between IT and OT are mandatory. Yes. When production counts are correlated with water, steam, compressed air, glycol, and power use, the plant can identify utility intensity by SKU, shift, or line. This supports 2026 sustainability reporting and cost reduction initiatives. Look at beverage process knowledge, multi-vendor controls experience, startup support, documentation discipline, project management strength, and the ability to connect controls work to capital execution. A partner who understands fillers, pasteurizers, CIP, utilities, packaging, and compliance will usually outperform a software-only vendor. No. Many plants should first establish reliable local control, event models, historians, and OEE data. Cloud analytics are most useful when the plant already trusts its source data and wants multi-site comparison, advanced reporting, or enterprise optimization. For companies planning broader modernization, it is useful to review actual project examples and execution style. DPS shares selected project experience through its case study portfolio, which helps manufacturers see how process, utilities, installation, and automation can be aligned in real operating environments. Equipment strategy also matters. If the project includes custom process hardware, tanks, or CIP-related systems, integration is easier when mechanical and controls scopes are designed together. DPS supports this through its process equipment capabilities, helping reduce interface gaps between fabricated equipment, field installation, and startup programming. In the United States, the market is moving toward smarter, faster, and more accountable beverage manufacturing. Co-packers need rapid line changeovers and multi-customer reporting. Brewers need better packaging efficiency and utility control. RTD and functional beverage producers need recipe accuracy, traceability, and speed to market. Dairy and aseptic plants need tighter compliance and sanitation visibility. Across all of these segments, controls integration is now a foundation for profitability. The best next step is usually an assessment, not a software purchase. Document the current control platforms, OEM interfaces, data gaps, production bottlenecks, utility constraints, reporting needs, and expansion roadmap. Then define a phased architecture that fits your plant, your workforce, and your capital plan. This is especially important in regional manufacturing hubs where growth is fast and shutdown windows are short, from North Carolina and Georgia to Texas, California, and the Midwest. Manufacturers that take this approach tend to build systems that last. They get cleaner startup paths, better accountability between trades and vendors, stronger data trust, and more useful reporting for operations and leadership. In a market where margins are constantly pressured by labor, freight, packaging cost, and retailer expectations, that kind of integration is not just technical improvement. It is operating leverage. The comparison chart highlights a common purchasing reality in U.S. beverage projects: software expertise matters, but projects often create more value when controls are tied to process design, utilities, installation planning, contractor coordination, and startup management. -
Legacy PLC Upgrade for Food Plants
For food and beverage manufacturers in the United States, upgrading a legacy PLC is no longer a purely technical decision. It is an operational, compliance, cybersecurity, and profitability decision. Across production hubs such as Chicago, Dallas, Fresno, Charlotte, Los Angeles, Atlanta, and the Midwest protein corridor, plants are running aging automation hardware that was once dependable but is now increasingly difficult to support. When a controller fails on a packaging line, blending skid, retort, dairy pasteurizer, or CIP system, the cost of lost production can quickly exceed the price of the upgrade that was deferred. In food plants, every minute of downtime can affect raw material yields, labor utilization, sanitation windows, customer service levels, and retailer commitments. Legacy PLC systems also limit data visibility, make recipe management harder, and expose facilities to cyber and compliance risk. A structured PLC migration can reduce recovery time, improve maintainability, support plant expansion, and strengthen digital readiness for 2026 and beyond. Disruptive Process Solutions supports food and beverage manufacturers across the U.S. and Canada with process engineering, controls integration, capital planning, installation oversight, and turnkey execution. Companies evaluating automation modernization often need more than a programmer; they need a partner that can connect operations, utilities, safety, compliance, production scheduling, and project economics into one practical upgrade path. That is especially true in high-throughput facilities near major logistics corridors such as the Port of Los Angeles, Port of Savannah, Houston, and rail-linked manufacturing centers across the Midwest and Southeast. A legacy PLC upgrade for a U.S. food plant is critical when the installed controls platform is obsolete, spare parts are hard to source, cybersecurity protections are weak, or compliance expectations have outgrown the system. The best upgrade approach starts with a site survey, I/O inventory, code review, and risk assessment. From there, plants typically choose between a big bang cutover, a phased migration, or a parallel run strategy. Common target platforms include Allen-Bradley ControlLogix, Siemens S7-1500, and Schneider Electric M580. The strongest business case usually comes from avoiding downtime, improving recoverability, tightening access control, and gaining real-time production data. The table above shows why PLC modernization should be reviewed as a plant business case, not just a maintenance task. A controller replacement affects uptime, food safety support systems, operator workflows, and long-term digital infrastructure. Legacy PLCs often remain in service far beyond their intended support window. In many U.S. food plants, controllers installed 15 to 25 years ago still manage batching, pasteurization, conveying, canning, filling, refrigeration support, and wastewater utility functions. These systems may still run, but the support ecosystem around them has narrowed dramatically. Software licenses become harder to maintain, trained technicians retire, OEM knowledge fades, and replacement cards come from surplus channels with uncertain quality. Obsolescence is only one side of the problem. Older automation systems were not designed for today’s connected manufacturing environment. Remote access, historian integration, MES connectivity, cloud analytics, and multi-site visibility create business value, but they also expose weak points in legacy systems. Many older PLC architectures lack modern authentication, encrypted firmware validation, granular role-based access, and secure network segmentation features expected in contemporary industrial environments. Compliance pressure is also increasing. Food and beverage facilities must be able to support repeatable process control, change management, sanitation documentation, and traceability expectations. While a PLC alone does not create compliance, weak controls can undermine it. If a thermal process, recipe setpoint, or cleaning sequence is difficult to verify, difficult to lock down, or difficult to restore after failure, the plant assumes avoidable risk. This is where a broader engineering view matters. Integrated food plant services can align controls upgrades with process design, utility needs, operator interfaces, safety systems, and project execution. Instead of treating a migration as a box swap, the upgrade becomes a reliability and performance improvement initiative. The explanation behind this table is straightforward: legacy risk rarely appears as one dramatic event. It accumulates through smaller weaknesses until one outage exposes all of them at once. Many plants delay a controls upgrade because the current system is “still working.” That logic can hold until a processor fails on a Friday night, an obsolete communications card dies during a seasonal production surge, or a backup cannot be restored. The cost of inaction is usually hidden in four places: unplanned downtime, expensive emergency procurement, lost production flexibility, and rising labor burden on maintenance and engineering teams. Consider a prepared foods facility in the Southeast running a high-volume line into retail distribution. If the line loses eight hours due to an obsolete PLC failure, the impact may include wasted raw material, overtime, rescheduling sanitation, freight changes, missed customer windows, and reduced weekly throughput. In dairy, beverage, aseptic, or protein processing, restart complexity can push costs even higher. For plants shipping through national distribution routes from California’s Central Valley, Texas, the Carolinas, or the Great Lakes region, missed schedules ripple fast. Spare parts are another major issue. Many legacy systems now rely on broker markets or refurbished inventory. That introduces uncertain quality, counterfeit risk, and inconsistent lead times. A plant may think it is saving money by postponing modernization, yet it is really accepting a growing sourcing crisis. In some cases, one failed communication module can sideline an entire process area because the exact part is unavailable. The line chart illustrates a realistic market trend: U.S. food plant modernization activity is rising as aging infrastructure, cybersecurity expectations, and labor constraints converge. This table helps quantify why “do nothing” is not a neutral option. It is an active decision to accept higher downtime exposure and a shrinking maintenance support base. There is no one-size-fits-all migration method. The right strategy depends on production criticality, shutdown windows, code complexity, safety systems, utility interdependencies, and available testing time. Big bang cutover means replacing the old system in a single planned outage. This can be effective for smaller skids, isolated lines, or facilities with a defined shutdown period. It reduces the duration of mixed old-new architecture, but it raises the importance of detailed planning and off-site testing. Phased cutover replaces the legacy system in sections. This is often preferred in large plants where utilities, packaging, processing, and CIP areas can be migrated step by step. It reduces immediate risk but requires careful interface management between old and new systems. Parallel run uses a fully tested replacement system operating alongside the old system before final switchover. This approach can reduce startup risk in mission-critical environments such as aseptic processing, high-value beverage blending, or continuous thermal operations, but it usually demands more design effort and temporary installation planning. The table shows that migration strategy should match operational reality, not just engineering preference. A poultry plant in Arkansas, a dairy processor in Wisconsin, and a beverage co-packer in California may all need different cutover models. Platform selection should reflect plant standards, technician familiarity, OEM ecosystem, network architecture, and long-term support strategy. In the U.S. market, Allen-Bradley ControlLogix is frequently chosen due to installed base familiarity, integration across packaging and process lines, and maintenance team comfort. Siemens S7-1500 is often attractive where high performance, diagnostics, and global standardization matter. Schneider Electric M580 is a strong option for plants emphasizing Ethernet architecture, process applications, and modern distributed control needs. The right answer is not always the most popular brand. It is the platform that best supports uptime, maintainability, expansion, and cybersecurity in the context of the plant. If a facility has a large installed Rockwell base with PlantPAx direction, ControlLogix may reduce lifecycle friction. If corporate engineering uses Siemens globally, S7-1500 can improve standardization. If the site is rethinking network topology and process control architecture, M580 may deserve serious consideration. The comparison table is most useful when combined with a site-specific standards review. A technically excellent platform can still be a poor fit if local maintenance capability is weak. The most successful PLC upgrades are won before hardware arrives. Pre-upgrade planning should include a full site survey, I/O count verification, panel condition assessment, code backup validation, network mapping, instrument review, and operational interviews with maintenance, sanitation, production, and quality teams. A site survey identifies hidden risks such as panel heat loading, insufficient cabinet space, unlabeled field devices, unsupported remote I/O racks, and undocumented interlocks with boilers, refrigeration, compressed air, or wastewater systems. An accurate I/O inventory prevents scope gaps during design. Documentation review reveals whether as-builts match reality or whether years of field edits have drifted from drawings. Plants should also review process criticality. Not all I/O points are equal. A temperature loop on a pasteurizer, a retort safety chain, a CIP conductivity measurement, and a simple conveyor run signal have very different startup implications. Prioritization helps shape both test scripts and cutover sequencing. Manufacturers that need deep front-end planning often benefit from a broader engineering partner. About the DPS team explains how an agile food and beverage engineering group can connect process, utilities, controls, and capital planning under one execution model. This planning table matters because most upgrade surprises are discovered in the field, not in software. Better planning directly shortens outage duration. One of the most effective ways to reduce plant disruption is to perform as much work as possible off-site. That includes panel fabrication, FAT preparation, logic simulation, HMI screen development, network configuration, labeling, and documentation package assembly. A well-managed off-site build compresses cutover time and increases startup confidence. For U.S. food manufacturers, this approach is especially valuable when production schedules are tight. Plants in high-demand categories such as ready-to-drink beverages, dairy, proteins, sauces, and co-packing often cannot afford lengthy in-plant engineering windows. Building and testing systems off-site allows stakeholders to review logic and screens before installation. Technological capability is important here. DPS supports controls engineering, PLC programming, SCADA integration, process automation, and utility system coordination, which allows an upgrade to be aligned with broader plant systems rather than treated as an isolated electrical project. Manufacturing capability also matters. Through its process equipment and skid experience, DPS understands how tanks, CIP systems, marination systems, cooking vessels, and utility skids interact with controls architecture in real operating environments. Service capability completes the picture through project management, installation coordination, commissioning oversight, and owner-focused execution. For plants adding or modifying skid-based systems during modernization, custom process equipment solutions can be integrated into the automation plan to avoid fragmented execution. The area chart reflects a clear trend shift: more food plants are adopting off-site build and test methods to reduce cutover risk and shorten restart timelines. Cybersecurity modernization should be embedded in every PLC upgrade scope. Replacing the controller without improving cyber posture leaves too much value on the table. Modern systems can support better user management, firmware integrity controls, secure remote access methods, segmented industrial networks, and improved event visibility. At a practical level, food plants should focus on several essentials. First, restrict programming and administrative access to authorized roles. Second, separate business IT traffic from plant OT traffic through network segmentation. Third, document remote access pathways and eliminate informal or unmanaged methods. Fourth, establish tested backup and restore procedures. Fifth, use firmware and software management practices that support integrity and recoverability. These improvements matter because food plants are now highly connected environments. Historians, ERP links, quality databases, cloud dashboards, OEM service connections, and warehouse systems all increase the need for secure architecture. Plants in major U.S. manufacturing centers often share data across sites, making standard cyber design even more important. The table above shows that cybersecurity is not separate from uptime. In modern food manufacturing, secure architecture directly supports operational continuity. A strong ROI model for a legacy PLC upgrade should include both hard and soft savings. Hard savings usually include avoided downtime, lower emergency spare costs, reduced scrap, lower contractor premiums during failures, and reduced overtime. Soft savings often include faster troubleshooting, better alarm clarity, stronger data visibility, easier recipe management, and improved confidence in expansion planning. For example, if a packaging or processing line generates high hourly contribution margin, preventing even one major outage per year can justify a meaningful portion of the project. If the new platform also improves line diagnostics, batch visibility, and changeover consistency, the total return increases further. Plants that operate across multiple states may also use modernization to standardize spare parts, training, and support practices across sites. Data visibility is especially valuable heading into 2026. Manufacturers increasingly want better production analytics, utility monitoring, downtime categorization, and integration with SCADA or enterprise reporting tools. Modern PLC architecture supports that direction much more effectively than aging isolated systems. For companies evaluating business impact, project case examples can help frame how engineering, controls, and execution decisions translate into measurable plant outcomes. The explanation here is important: not every benefit shows up as a simple utility savings line item. Some of the strongest returns come from improved resilience and better management visibility. Looking ahead to 2026, three trends will shape PLC upgrade priorities in U.S. food and beverage manufacturing. First, cybersecurity expectations will continue to rise as insurers, customers, and corporate boards demand stronger OT resilience. Second, sustainability and energy visibility will matter more, pushing plants toward smarter controls architectures that can monitor utilities, CIP efficiency, refrigeration performance, and water usage. Third, policy and compliance pressure around traceability, electronic records, sanitation discipline, and digital accountability will favor modern platforms that integrate more cleanly with plant information systems. Local supplier and partner selection also matters. In markets such as North Carolina, Texas, California, Illinois, Georgia, and Wisconsin, manufacturers should look for integrators and engineering partners that understand food-specific realities: washdown environments, thermal processes, recipe management, hygienic design interfaces, utility dependence, and compressed shutdown schedules. The best supplier is rarely the cheapest bidder. It is the team that can reduce overall project risk and protect production economics. Buying advice for plant leaders is simple: start before the emergency. Build an asset list of legacy controllers. Rank systems by downtime cost, spare parts exposure, compliance criticality, and cyber risk. Validate backups. Standardize documentation. Identify preferred migration platforms. Then package projects according to shutdown windows and capital priorities. That turns modernization from a crisis response into a controlled investment program. How do I know if my food plant needs a PLC upgrade now?If parts are obsolete, backups are unreliable, maintenance depends on one specialist, or the system cannot support secure access and clean recovery, it is time to plan an upgrade. Which migration approach is safest?The safest approach depends on the process. Parallel run is often best for critical continuous processes, while phased migration works well in larger multi-area plants. Big bang can be effective when shutdown windows are clear and testing is strong. Is Allen-Bradley always the best choice in the U.S.?Not always. ControlLogix is often a strong fit due to installed base and support familiarity, but Siemens S7-1500 or Schneider M580 may be better depending on corporate standards, process needs, diagnostics, and long-term architecture goals. Can we reduce downtime during the upgrade?Yes. Off-site panel build, simulation, FAT, documented cutover sequencing, labeled wiring plans, and startup rehearsals can significantly reduce production disruption. What should be included in the project scope?Site survey, I/O verification, code archive, documentation review, panel design, HMI updates, network architecture, cybersecurity improvements, FAT, SAT, training, and backup/recovery procedures. How does this affect compliance?A modern controls platform can support better change management, more reliable process execution, clearer operator visibility, and stronger documentation practices that help with FDA, USDA, SQF, and BRC expectations. What food sectors benefit most from legacy PLC modernization?Nearly all do, but especially beverage, dairy, protein, aseptic, prepared foods, sauces, and co-packing operations where downtime, sanitation, and batch control are tightly linked to profitability. Why work with a full-scope engineering partner?Because PLC upgrades in food plants touch process equipment, utilities, safety, scheduling, sanitation, and capital planning. A partner with engineering, manufacturing understanding, and project execution capability can reduce risk across the full plant system. -
2026 Food Plant Refrigeration Efficiency Benchmarks
Food and beverage manufacturers across the United States are under growing pressure to cut energy use, reduce refrigerant risk, protect uptime, and meet stricter sustainability expectations. In 2026, refrigeration performance is no longer judged only by tons of cooling installed. Owners, plant engineers, and operations leaders are benchmarking systems by total kWh per pound of product, compressor lift, defrost strategy, leak rate, recoverable waste heat, automation quality, and lifecycle cost. This matters in high-throughput markets such as poultry in Arkansas and Georgia, beef in Nebraska and Texas, frozen foods in the Midwest, dairy in Wisconsin and California, and beverage production near major logistics hubs such as Chicago, Dallas-Fort Worth, Atlanta, and the Ports of Los Angeles and Long Beach. This guide explains what strong refrigeration performance looks like in 2026, how ammonia and CO2 systems compare, where compressor optimization delivers the fastest payback, when heat recovery creates real savings, and how aging systems can be modernized without disrupting production. It also provides practical buying advice for U.S. food plants balancing safety, compliance, capacity growth, and capital discipline. For most U.S. food plants in 2026, the best refrigeration system is the one that matches product temperature needs, site risk profile, utility cost structure, and future expansion plans. As a quick benchmark, high-performing facilities typically reduce refrigeration energy intensity by 10% to 25% versus poorly optimized legacy systems through compressor sequencing, floating head pressure, suction optimization, variable speed drives, leak reduction, and targeted heat recovery. Ammonia remains highly efficient for large central plants, especially in meat, cold storage, dairy, and prepared foods. CO2 is increasingly attractive for low-charge, lower-toxicity architectures, urban sites, and facilities that want a lower global warming potential path with strong compliance optics. Plants with the strongest returns usually do not start with a full replacement. They start with data: compressor runtime, condensing temperature, suction stability, evaporator performance, refrigerant losses, and thermal loads by process area. In many cases, the smartest investment is a phased upgrade that preserves useful assets while improving controls, motor efficiency, safety systems, and heat recovery. That approach is especially relevant for U.S. manufacturers facing tight labor, rising insurance scrutiny, and ongoing power cost volatility in markets from Southern California to the Carolinas. When evaluating options, buyers should focus on six questions: Manufacturers that answer those questions well usually outperform the market on both energy and uptime. In the United States, 2026 refrigeration benchmarks are being shaped by higher electricity rates, decarbonization programs, low-GWP refrigerant decisions, and increased use of automation. Plants are moving away from simple nameplate comparisons and toward outcome-based metrics tied to production. A poultry processor in Northwest Arkansas, a frozen pizza manufacturer near Chicago, and a beverage co-packer in North Carolina may all operate at different temperatures, but each can be measured by how efficiently refrigeration supports throughput and quality. The table below summarizes realistic benchmark ranges for common food and beverage applications. These are directional planning values rather than universal design limits, because ambient climate, process load profile, sanitation schedule, and distribution strategy can vary significantly between Phoenix, Seattle, Houston, and Boston. These benchmarks show why generic design rules often fail. A plant with stable load and strong controls may outperform a newer facility that is oversized, poorly staged, or constantly fighting product scheduling swings. In 2026, strong operators are also benchmarking by maintenance outcomes, not just energy. Mean time between leak events, response time to pressure abnormalities, oil carryover trends, and condenser fouling frequency all affect true cost of ownership. The U.S. market is also seeing more investment in digital trending and supervisory controls. Plants that use real-time analytics to detect suction drift, valve hunting, or condenser inefficiency can often avoid both energy loss and emergency downtime. The line chart reflects the rising pace of retrofit and optimization activity across the United States. Drivers include aging installed bases, lower-GWP refrigerant strategies, utility incentives, and the need to expand output without building entirely new central utility systems. Ammonia and CO2 are now the dominant comparison for many new industrial refrigeration decisions in the U.S. food sector. Both can perform well, but the right choice depends on plant scale, operating temperatures, staffing model, code environment, and owner risk tolerance. Ammonia still leads in thermodynamic efficiency for many large central systems and remains a proven choice in meat processing, dairy, prepared foods, and cold storage. It is familiar in industrial settings and can deliver excellent lifecycle economics. However, toxicity, PSM considerations, charge management, machinery room design, and emergency planning require disciplined engineering and operation. CO2 is gaining ground because it offers very low global warming potential and supports low-charge architectures, especially in cascade and pumped designs. It is often attractive where owners want reduced ammonia inventory, tighter urban siting flexibility, or a future-facing sustainability narrative. That said, CO2 brings high operating pressures, specific component requirements, and important design considerations for warm climates and transcritical behavior in some applications. For a greenfield cold storage development near Savannah, Newark, or Inland Empire distribution corridors, a low-charge or hybrid approach may help with insurer comfort and long-term refrigerant strategy. For a large protein processor in Omaha or Amarillo with experienced ammonia operators and heavy process loads, a modern ammonia system may still offer the strongest business case. In short, there is no universal winner. The correct answer is application-specific. The comparison chart illustrates how owners often weigh tradeoffs in 2026. Ammonia tends to score especially well on efficiency and service familiarity in traditional industrial markets. CO2 often scores highly on low-GWP positioning and simplified toxic exposure profiles, though actual outcomes depend heavily on the selected architecture and contractor expertise. Compressor optimization is usually the fastest path to measurable savings. Many food plants are paying excessive energy costs because compressors are fighting avoidable pressure lift, running in poor part-load combinations, or responding to unstable load signals. Even well-maintained systems can underperform if controls are outdated. The first priority is usually suction optimization. If suction pressure is set lower than necessary, every compressor in the system works harder than required. The second priority is condensing control. Plants that fail to float head pressure when outdoor conditions allow often waste major energy, especially in northern states and shoulder seasons. The third priority is compressor sequencing so that the most efficient machines carry the right load. These gains are not theoretical. In many older U.S. food plants, setpoints were built around worst-case production days and never re-optimized. A processor near Kansas City or Fresno may be carrying unnecessary lift year-round because one room needed extra margin five years ago. When operators trend evaporator approach temperatures, compressor loading, and room pull-down time by production shift, they often uncover major improvement opportunities. Industry demand for these optimization projects is growing fastest in energy-intensive categories with tight margins. The bar chart highlights strong demand in protein and frozen food segments, where refrigeration cost has a direct impact on yield, product quality, and delivered margin. Heat recovery is one of the most underused tools in industrial refrigeration. Refrigeration systems reject heat every hour they operate. In plants with steady sanitation, washdown, domestic hot water, or process preheat demand, that waste heat can become a valuable energy source. Dairy plants, beverage processors, protein facilities, and prepared food manufacturers often have strong heat recovery potential because they use large amounts of hot water for cleaning and product changeovers. Instead of rejecting all condenser heat to atmosphere, facilities can recover part of it through desuperheaters, condenser heat reclaim loops, or integrated heat pump strategies. Heat recovery must be engineered around actual load overlap. A plant with large refrigeration rejection but limited hot water demand may not justify an elaborate reclaim system. Conversely, a dairy or protein processor with heavy washdown loads may leave substantial money on the table without it. The best projects start with a thermal balance: when is heat available, when is it needed, and at what temperature? As natural gas volatility remains a concern in many U.S. regions, heat recovery is becoming more attractive. This is especially true in states offering energy efficiency incentives or carbon reduction support. Plants in California, New York, Massachusetts, and parts of the Pacific Northwest are increasingly evaluating heat reclaim as part of broader utility decarbonization planning. Leak detection and preventive maintenance are no longer just safety topics. In 2026, they are core efficiency and asset-management topics. A small persistent leak can drive refrigerant losses, trigger safety events, introduce moisture or contamination risks, destabilize oil management, and force emergency service at the worst possible time. Modern programs combine fixed gas detection, alarm integration, inspection rounds, vibration review, oil analysis, infrared screening, and trend-based maintenance. Plants with strong leak and PM programs typically have lower total cost than plants that only react to failures. This is especially true where product schedules are tight and downtime hits distribution commitments tied to national retail networks. For U.S. operators, the most important maintenance shift is moving from calendar-only work to condition-informed work. If compressor amps, pressure ratios, oil carryover, and valve response are continuously trended, technicians can fix emerging issues before they become downtime events. That matters whether the facility serves East Coast grocery distribution through New Jersey and Pennsylvania or cold chain export flows through Houston and Savannah. Plants should also update emergency response documentation and operator training as systems evolve. A site that has added automation, a new engine room package, or low-charge equipment may need revised SOPs, alarm routing, and maintenance task lists. Variable speed drives, or VSDs, are among the most practical tools for improving part-load efficiency in refrigeration systems. They are especially useful in food plants where loads shift by production campaign, sanitation window, season, or warehouse occupancy. Instead of using throttling or inefficient on-off cycling, VSDs allow motors to better match actual load. The strongest VSD applications in refrigeration are usually compressor motors, evaporator fans, condenser fans, and sometimes pumps in glycol or secondary loops. However, VSDs create value only when paired with sound control logic. Installing drives without revisiting setpoints and sequencing can limit savings. A beverage processor in the Carolinas running mixed package sizes may see major load swings across the day. A cold storage warehouse outside Columbus may need different fan strategies during off-peak occupancy. A seafood plant in the Pacific Northwest may see seasonal throughput changes. In each case, VSDs can improve turndown, cut demand spikes, and stabilize temperatures. The area chart shows a clear trend shift toward smarter controls and variable-speed operation. As electricity rates rise and utilities push for demand management, VSD adoption is expected to continue growing in 2026 and beyond. From a buying perspective, VSD projects should be evaluated by more than motor horsepower. Owners should confirm harmonic mitigation requirements, ambient protection, enclosure suitability, spare parts strategy, controls integration, cybersecurity considerations for connected devices, and operator training. Plants that treat VSDs as part of a system strategy, not an isolated electrical upgrade, usually get much better results. Many U.S. food and beverage facilities are operating refrigeration assets that are mechanically viable but operationally outdated. Full replacement is not always the best first move. A well-planned retrofit can improve safety, energy performance, capacity, and reliability while preserving the value of core assets. The right retrofit path depends on the plant’s bottleneck. Some facilities need control modernization. Others need refrigerant charge reduction, condenser replacement, evaporator upgrades, engine room reconfiguration, or better load distribution. The most successful retrofit programs are phased around production schedules so that business continuity is protected. Retrofit buying advice should include three steps. First, perform a measured assessment rather than a visual walk-through only. Second, rank projects by operational bottleneck and payback, not by which equipment looks oldest. Third, evaluate phasing and shutdown windows early. Many food plants lose value because they decide on hardware first and execution strategy second. Local supplier capability also matters. In high-density industrial markets such as Chicago, Dallas, Atlanta, Charlotte, Los Angeles, and the Central Valley, service networks may support sophisticated phased projects more easily than in remote regions. That does not mean rural projects should avoid advanced systems, but it does mean maintenance planning and spare strategy must be considered from the beginning. Owners comparing suppliers should assess technical depth, field execution quality, controls capability, safety record, and ability to align refrigeration decisions with the broader process. A freezer expansion, a utility house upgrade, and a sanitation water project should not be engineered in isolation if they affect one another. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with an engineering-led, business-minded approach to capital projects. Instead of treating refrigeration as a standalone mechanical package, the company evaluates how cooling demand interacts with process throughput, sanitation, automation, utilities, and long-term profitability. That matters when a client is deciding whether to optimize an existing central plant, add low-charge packaged equipment, or plan a future-ready utility backbone for a new facility. From a technological capabilities perspective, DPS brings multidisciplinary engineering across process, mechanical, electrical, plumbing, structural, and controls. That includes automation, PLC programming, SCADA integration, recipe and batch coordination, and energy-oriented utility design. In refrigeration-related projects, this means the cooling system can be integrated intelligently with product handling, CIP, glycol loops, boilers, compressed air, and facility controls rather than operating as a disconnected subsystem. More information about the company’s approach can be found on the About Us page. From a manufacturing capabilities perspective, DPS also designs and supplies proprietary process equipment, including tanks, CIP systems, vessels, and related utility-connected assets that frequently interact with refrigeration loads. That experience is useful when manufacturers need a coordinated solution instead of multiple vendors optimizing different parts of the plant in isolation. Details on available equipment capabilities are available through the equipment solutions section. From a service capabilities perspective, DPS operates through a design-build-manage model that helps manufacturers move from feasibility and capital planning through installation, integration, and execution oversight. Services include process engineering, owner’s representation, project and program management, general contracting support where applicable, utility integration, and turnkey installation. For plants evaluating refrigeration retrofits, that approach can reduce the gap between concept and real-world execution. Additional information on these capabilities is available on the services page. The company’s work spans both food and beverage sectors, including protein, dairy, prepared foods, aseptic systems, brewing, RTD beverages, and co-packing environments. That cross-sector experience is important because refrigeration is often tied to more than just room temperature control. It may influence fermentation, blending, chilling, retort support, process water, package stability, and product safety. Examples of project experience and execution context can be explored in the case studies section. For U.S. manufacturers, especially those balancing growth with capital discipline, the most valuable partner is often the one willing to challenge assumptions. Sometimes the answer is a new refrigeration plant. Sometimes the answer is smarter controls, better sequencing, or a utility redesign that unlocks capacity without unnecessary spending. That kind of honest evaluation is increasingly important in 2026. What is the most important refrigeration benchmark for a food plant in 2026?The most useful benchmark is energy and uptime performance tied to production output, not just installed tonnage. Plants should track kWh per pound or case produced, leak rate, head pressure control, suction stability, and unplanned downtime. Is ammonia still a good choice in the United States?Yes. Ammonia remains a strong option for large industrial applications where efficiency, experienced staffing, and central utility scale matter. Modern low-charge approaches can also reduce some traditional concerns. When is CO2 a better option?CO2 is often attractive where owners want a very low-GWP strategy, lower toxic refrigerant inventory, and a future-oriented compliance profile. It is especially relevant for hybrid systems, urban developments, and some low-charge applications. What retrofit usually pays back fastest?Controls modernization, compressor sequencing improvements, head pressure floating, suction optimization, and targeted VSD applications often provide the fastest returns, particularly when the existing mechanical assets are still sound. Can heat recovery really offset utility costs meaningfully?Yes, if the plant has consistent hot water or process preheat demand. Dairy, protein, and beverage plants often have strong opportunities to reclaim refrigeration heat for sanitation and CIP support. How often should leak detection systems be reviewed?Calibration and review frequency should align with code, insurance, site risk, and manufacturer recommendations, but quarterly checks and documented alarm testing are common parts of a strong preventive program. Are VSDs always worth installing?No. VSDs work best where loads vary and controls can use that flexibility. On constant-load equipment with poor control logic, expected savings may not materialize. Each application should be evaluated case by case. Should a plant replace an old system or retrofit it?It depends on safety exposure, refrigerant strategy, mechanical condition, efficiency gap, and expansion plans. Many plants benefit from a phased retrofit before considering full replacement. How do climate and location affect system choice?A plant in Minnesota, Georgia, Arizona, or coastal California will experience different ambient and utility conditions. Condenser strategy, refrigerant architecture, and heat recovery economics should always be localized. What trend will matter most after 2026?The biggest trends are likely to be low-GWP adoption, smarter automation, condition-based maintenance, tighter utility integration, and capital planning that connects refrigeration with full-plant profitability rather than treating it as a standalone utility. In summary, 2026 refrigeration decisions in the United States are being shaped by efficiency, resilience, compliance, and practical capital allocation. Plants that benchmark performance carefully, choose refrigerants by application instead of trend, and integrate refrigeration planning with the full production environment will be in the strongest position to control cost and support growth. -
Recipe Management for Food Manufacturing
In the United States, recipe management in food manufacturing is no longer just a way to store formulas. It is the operating backbone that connects R&D, quality, purchasing, production, maintenance, automation, and compliance. A modern recipe management system controls ingredients, process steps, critical parameters, version history, allergen rules, lot traceability, operator instructions, and plant-floor execution. For manufacturers producing sauces, proteins, dairy, beverages, prepared meals, nutraceutical products, or aseptic items, recipe control directly affects yield, safety, uptime, labor efficiency, and margin. As U.S. food and beverage plants face tighter labor markets, rising ingredient costs, stricter FDA and USDA scrutiny, and growing customer demands from retail, foodservice, and co-packing channels, the old model of paper binders and tribal knowledge is becoming too risky. Plants in Chicago, Fresno, Dallas, Atlanta, Charlotte, Houston, Minneapolis, and the Los Angeles-Long Beach corridor increasingly need digital recipe systems that scale across multiple lines and facilities while supporting ERP, MES, PLC, and SCADA integration. Recipe management in food manufacturing is the structured control of formulas, processing instructions, batch logic, quality checkpoints, allergen data, and revision history so a product can be made consistently, safely, and profitably at production scale. In U.S. plants, effective recipe management usually includes: For many U.S. manufacturers, the best results come when recipe management is treated as part of a broader plant systems strategy rather than a standalone software purchase. That is why engineering-led partners with process, controls, and installation experience can add real value during design and implementation. Companies looking to understand that broader approach can review how DPS approaches food and beverage project execution as part of end-to-end processing and automation programs. This table shows why recipe management should be viewed as an operating control system, not simply a digital cookbook. In a manufacturing environment, a recipe is the full production definition of a product. It includes not only what goes in, but how, when, where, and under what conditions it is processed. A barbecue sauce formula in Kansas City, a cultured dairy product in Wisconsin, or a retorted soup in New Jersey each requires more than a list of ingredients. The plant needs sequence control, quality checkpoints, permissible substitutions, lot consumption rules, sanitation conditions, and instructions for startup, hold, rework, and changeover. U.S. manufacturers often operate under mixed regulatory and customer requirements. A protein processor may need USDA alignment, a beverage plant may need FDA beverage controls, and a co-packer may also need SQF or BRC expectations imposed by retailers. That means recipe management must connect to quality management and production records in a way that supports real audits, not just internal convenience. At a practical level, recipe management spans five layers: Plants with multiple SKUs, seasonal formulations, retailer-specific variants, or regional ingredient sourcing need even stronger controls. A salad dressing plant shipping through Savannah, a beverage facility supplying the Northeast via Port Newark, or a frozen prepared foods site serving the Midwest all benefit when recipe data is standardized and centrally governed. Many recipe failures do not begin with the formula itself. They begin with missing process detail. A recipe may call for 1,200 pounds of tomato base, 250 pounds of sugar, and 40 pounds of spice blend, yet still fail if the system does not define when the spice is added, how long to shear, when to open steam, how quickly to cool, or how long to hold before filling. This is where critical process parameters, or CPPs, become essential. CPPs commonly include temperature ramp rates, cook or pasteurization time, vessel pressure, agitation speed, in-line Brix limits, homogenization pressure, dwell time, retort profile, and final fill temperature. For dairy and aseptic applications, even tighter control may be required. If a process depends on pH or viscosity windows, those values should not live in an operator’s memory. They should be embedded in recipe logic and tied to alarms, prompts, and exception handling. Scaling logic is equally important. A formula that works in a 50-gallon pilot kettle can behave differently in a 2,000-gallon batch tank or a continuous blending skid. Ingredient sequencing, hydration time, heat transfer, foam generation, and solids dispersion may all shift with scale. Strong recipe management accounts for: For plants adding automation, this is where engineering depth matters. A partner with controls, PLC, and process design experience can align recipe logic to actual vessel, utility, and line capabilities. DPS is active in that space through integrated processing, controls, and project execution support, including services for engineering, automation, and project delivery tailored to food and beverage operations. A recipe is never static. New suppliers are approved. Salt levels are adjusted. Sugar is reduced. Spice is rebalanced. Packaging changes trigger net weight changes. Thermal process validations are updated. Customer-specific variants are introduced. Without strict revision control, these routine changes can create major risk. Version control in food manufacturing should answer six questions immediately: This matters during internal investigations, customer complaints, line deviations, and regulatory audits. If a product shipped from a plant in Texas to a retailer distribution center in Atlanta is later questioned for flavor inconsistency or allergen labeling, the company must trace exactly which formula revision was active, which lots were consumed, and what instructions were executed. Rollback capability is equally valuable. If a new supplier changes hydration behavior or a reformulation reduces finished-product stability, the plant should be able to return to a previous approved recipe without confusion or delay. Paper systems rarely do this well. Spreadsheets only do it if the organization is unusually disciplined. Purpose-built digital systems do it by design. The chart above reflects the broader direction of the U.S. market: more manufacturers are moving toward formalized, software-driven recipe governance as labor, compliance, and traceability demands increase. Allergen control is one of the strongest business cases for modern recipe management. In U.S. manufacturing, mismanaged allergen information can trigger recalls, brand damage, customer chargebacks, and direct regulatory exposure. A robust system should identify allergens at the ingredient level, carry them through every formula and variant, and connect that information to scheduling, line clearance, sanitation validation, label approval, and rework rules. For example, if a plant in California runs both dairy-based beverages and non-dairy functional drinks, recipe logic should prevent inappropriate rework, flag allergen-sensitive changeovers, and support the sequencing of products to reduce wash time and contamination risk. In protein and prepared foods, soy, wheat, milk, egg, sesame, and tree nut impacts must be tightly governed. Recipe management also supports broader compliance integration by linking to: In regulated environments, the best systems do not isolate recipe data from the rest of operations. They integrate it with quality and production workflows so compliance becomes part of execution, not an afterthought. Recipe management is also a financial tool. Ingredient markets in the United States can move quickly due to freight shifts, weather, commodity volatility, labor disruptions, and port congestion. Dairy solids, proteins, oils, sweeteners, packaging materials, and spice blends can all change in cost within weeks. A recipe system that only stores target percentages, without current cost linkage, leaves margin management blind. Real-time or near-real-time costing allows a plant to model the effect of ingredient substitutions, packaging changes, batch-size adjustments, and yield losses before they hit the P&L. This is especially useful for co-packers and multi-plant networks where margin can erode through small, repeated variances. Yield analysis should extend beyond final weight. Mature plants analyze: Prepared foods, proteins, and sauce operations often show especially strong demand because they combine formulation complexity with high SKU counts and tight margin pressure. When these insights are linked to purchasing and execution data, management can identify where margin is leaking: not only in raw materials, but also in line performance and formulation discipline. Many U.S. plants still operate with a mix of paper batch sheets, ERP notes, spreadsheets, and operator knowledge. That may work for a small facility with a limited SKU count, but it becomes fragile as the business grows. Multi-line sites, co-packing facilities, plants with frequent changeovers, and operations shipping nationally cannot rely on disconnected documents for recipe execution. Digitization should not begin with software alone. It should begin with process mapping. Before migrating recipes into a platform, companies should standardize naming conventions, units of measure, revision policies, approval workflows, ingredient master data, line capabilities, and batch record expectations. A practical digitization roadmap usually follows these stages: For manufacturers expanding or building new capacity, it is often more efficient to design recipe digitization alongside the facility and process architecture rather than retrofitting it later. That is particularly true for plants adding new syrup rooms, batching areas, thermal systems, CIP skids, or automated transfer networks. Companies evaluating hardware for those environments can review process equipment capabilities from DPS in conjunction with automation planning. The explanation is straightforward: digitization succeeds when companies treat recipes as controlled operational data, not just documentation to be uploaded. The strongest recipe management programs in the United States are integrated, not isolated. ERP, MES, PLC, and SCADA systems each play a different role: Recipe management sits across these layers. It should receive approved data from upstream business systems, drive execution logic on the floor, and return actual usage and performance data back into reporting and costing systems. For a beverage blending and batching line, that may mean the ERP releases a production order, the MES calls the approved recipe version, the PLC meters ingredients into a blend tank, SCADA records Brix and transfer events, and actual consumption posts back for inventory and costing. In a protein marination or prepared foods environment, it may involve weigh-up verification, thermal processing steps, hold-and-release status, and packaging reconciliation. This integration is particularly valuable in facilities that depend on utilities and process coordination, such as plants with CIP systems, boilers, glycol, compressed air, process water treatment, and automated transfer skids. The technical challenge is not just software compatibility. It is making sure the process design, controls architecture, and recipe logic all reflect actual operating conditions. The trend is clear: hybrid systems remain common today, but fully integrated digital environments are gaining share as manufacturers invest in plant modernization. This is also where a full-scope engineering and integration partner can be more effective than a software vendor alone. DPS works across process engineering, controls, project management, and installation, which matters when the objective is not simply to buy a system but to make recipe execution work reliably inside a real production environment. Manufacturers exploring complete processing and controls outcomes can also see examples in project case studies from DPS. Even the best recipe software will fail if the plant does not manage adoption. Sustainable recipe control depends on disciplined people, documented governance, and recurring review. Best practices usually include the following: Training is especially important in plants with high turnover or multilingual workforces. Instructions should be clear, visual where possible, and tied to practical line behavior. If operators routinely bypass prompts because they slow production, the workflow likely needs redesign. Recipe discipline should help the floor, not fight it. Continuous improvement also means using recipe data to improve the process itself. A plant may discover that two approved versions create unnecessary complexity, that one ingredient is driving outsized variance, or that an equipment bottleneck is forcing manual interventions. In some cases, the best fix is not a capital project. In others, process redesign, controls changes, or equipment upgrades may produce outsized gains. This is one area where DPS’s model stands out in the U.S. market. Rather than approaching projects as isolated installs, the company combines technological capabilities such as controls engineering, PLC programming, SCADA, utility integration, and process automation with manufacturing capabilities across beverages, proteins, dairy, prepared foods, aseptic, retort, sauces, and plant-based processing. On the service side, DPS supports capital planning, engineering, owner’s representation, project management, general contracting, equipment supply, installation, and commissioning. That combination can be valuable when recipe control must align with both business objectives and plant-floor realities. For buying advice, U.S. manufacturers should resist choosing solely on license cost. The right decision depends on product complexity, line automation level, audit exposure, and growth plans. A sauce plant with two kettles has different needs than a national co-packer launching a greenfield beverage facility. The comparison chart reflects a common market reality: the more closely recipe control is tied to execution and integration, the more operational value it tends to deliver. What types of products benefit most from recipe management?Products with variable ingredients, complex processing, strict allergen exposure, or frequent SKU changes benefit the most. This includes sauces, dressings, protein marinades, dairy products, RTD beverages, aseptic products, prepared foods, soups, cultured products, and co-packed formulations. Is recipe management only useful for large enterprise plants?No. Mid-sized U.S. plants often see some of the fastest payback because they are large enough to feel the pain of inconsistency but small enough to implement improvements quickly. Sites with annual revenue above roughly $20 million often have a strong case for structured recipe control. How does recipe management help with audits?It creates a controlled record of approved formulas, revisions, execution steps, and batch history. That supports FDA, USDA, SQF, BRC, customer, and internal audit requirements. Can recipe management reduce labor dependency?Yes. It captures process knowledge in a repeatable system, reducing dependence on a few experienced operators and improving training speed for new staff. What is the difference between recipe management and batch control?Recipe management defines what should happen. Batch control executes it through people, systems, and automation. In advanced plants, the two are tightly linked. Should a company digitize recipes before or after plant expansion?Ideally during planning. If a company is adding new lines, utilities, or processing areas, recipe architecture should be designed alongside the physical and controls infrastructure. How do local supply chains affect recipe strategy in the United States?Regional sourcing can create variability in cost, ingredient functionality, and logistics. Plants near Houston, Savannah, Chicago, or Southern California may face different freight profiles and supplier lead times. A strong recipe system helps model substitutions and manage those changes without losing control. How should companies evaluate local suppliers and integrators?Look beyond software brochures. Evaluate whether the partner understands your product category, can support field integration, has controls experience, and can translate formulas into executable line behavior. Local responsiveness matters, but so does national delivery capability if you operate across several states. Looking toward 2026, recipe management will become more connected to sustainability, resilience, and portfolio planning. Manufacturers will increasingly use recipe systems to reduce water usage during changeovers, lower energy intensity in thermal processing, manage supplier variability, and support reformulation for nutrition or label claims. Plants that still rely on static documents will find it harder to compete on speed, compliance, and margin. For U.S. manufacturers, the central lesson is simple: recipe management is not an isolated IT project. It is a production, quality, compliance, and profitability discipline. When it is designed well, integrated correctly, and maintained through training and continuous improvement, it becomes one of the most valuable control systems in the plant. -
2026 Sustainable Design Principles for Food Facilities
Food and beverage manufacturers in the United States are under pressure to reduce utility costs, improve food safety, satisfy investor expectations, and build facilities that remain profitable as environmental rules tighten. In 2026, sustainable design is no longer a branding exercise. It is a capital planning discipline that affects throughput, labor efficiency, maintenance, audit readiness, and long-term operating margin. For processors building new plants or upgrading legacy sites, the best sustainable design strategies combine practical engineering with measurable returns: efficient water systems, lower-energy utilities, healthier indoor environments, durable materials, and commissioning practices that keep performance from drifting after startup. The quickest answer is this: the strongest 2026 sustainable design principles for food facilities in the United States are to choose a logistics-smart site, orient the building for heat and daylight control, reduce potable water demand, design natural and mechanical ventilation together, specify low-impact and cleanable materials, protect indoor environmental quality, and commission every major utility and process interface for long-term performance. A sustainable food plant must also support sanitation, regulatory compliance, labor retention, and future expansion. For U.S. processors, the most effective sequence is to start with site selection and utility risk, then integrate energy, water, process, and building design as one business case. A plant near Dallas-Fort Worth, Chicago, the Inland Empire, Savannah, Houston, or the Port of Los Angeles may have major freight advantages, but those savings can be erased by poor water reliability, weak wastewater capacity, storm exposure, or a building orientation that raises cooling loads. Sustainable design works best when it is tied to production economics, not when it is isolated as a separate checklist. In practical terms, owners should ask six questions before approving design: Will this layout reduce lifetime utility intensity? Can the envelope and orientation lower thermal stress? Are materials durable under washdown and chemical exposure? Can operators work safely and comfortably? Can systems be validated, commissioned, and re-tuned over time? And will these decisions improve profitability per pound, gallon, case, or batch? This table shows why sustainability should be framed as a performance platform. In most U.S. food and beverage projects, the strongest payback comes from decisions made before equipment is purchased: location, orientation, utility planning, and hygienic material choices. By 2026, sustainable food facility design in the United States is being shaped by three overlapping forces: state and local energy codes, water stress in key manufacturing regions, and supply chain pressure from retailers and investors who want resilient, lower-emission operations. California, Arizona, Texas, the Southeast, and major industrial hubs in the Midwest all face different utility and climate constraints, so sustainable design must be regionally specific. Market demand is also changing. Beverage co-packers, protein processors, dairy plants, and ready-to-eat food manufacturers are being asked to scale faster while using less labor and less water. That means modern sustainable design is not just about LED lighting or recycled content. It includes heat recovery, smart controls, advanced CIP optimization, utility metering by area, wastewater reduction strategies, and modular planning for future capacity. Plants around Atlanta, Columbus, Kansas City, and the New Jersey logistics corridor increasingly need designs that can expand without reworking the whole utility backbone. The strongest 2026 design approach combines the following principles: These principles apply across product types: craft brewing, spirits, wine, kombucha, RTD beverages, carbonated soft drinks, juice, dairy drinks, aseptic products, protein processing, prepared foods, sauces, dressings, shelf-stable foods, and plant-based products. Every category has a different utility profile, but all benefit from integrated design. The line chart reflects the rising capital interest in sustainable plant design. Across the United States, owners are directing more budget toward efficient utilities, advanced controls, and facilities that can satisfy both production growth and environmental reporting expectations. This segment table highlights a key buying lesson: there is no universal “green package” for food plants. Sustainable design must match the process technology, sanitation intensity, and production model of each operation. Site selection is where sustainability and profitability most clearly meet. In the United States, a food facility should be placed where inbound ingredients, outbound finished goods, labor, power, water, and wastewater treatment all align. A site near the Port of Savannah may support imported ingredients and East Coast distribution. A Houston-area site may favor chemical, packaging, and export connectivity. A Midwest location near Chicago, Indianapolis, or St. Louis may optimize national trucking reach for prepared foods or protein. A Southern California site may improve access to retail density and ports but can face higher land and water stress. Owners should analyze these site variables before locking in real estate: Orientation matters just as much. In hot climates such as Phoenix, Dallas, or central Florida, careful orientation can reduce solar gain on production and warehouse walls, support lower cooling loads, and improve employee comfort. North-facing daylight openings are often easier to manage than large west-facing glazing. Loading docks should be planned for prevailing winds, traffic circulation, and thermal control. Roof geometry should also anticipate future solar installation, daylighting devices, and rooftop mechanical service access. The matrix above is especially useful during early capital planning. If a site scores well on freight but poorly on water and expansion, it may look attractive on paper while locking the owner into long-term operating penalties. The bar chart shows where sustainable capital demand is strongest. Beverage, co-packing, and prepared food operations often move first because scale, SKU complexity, and retailer expectations make efficiency improvements easier to justify. Water strategy is one of the most important parts of sustainable design for food facilities in the United States. Water costs are rising, sewer charges are significant, and some regions face seasonal or structural stress. But food facilities cannot simply reduce water blindly. They must reduce non-value-added consumption while preserving sanitation and food safety. That means targeting domestic fixtures, hose stations, CIP routines, washdown practices, cooling systems, and reuse opportunities with engineering discipline. In office, lab, and employee welfare areas, low-flow faucets, high-efficiency toilets, and sensor-controlled fixtures are standard. In processing environments, the bigger gains often come from pressure management, nozzle selection, trigger-controlled hoses, timed washdown protocols, conductivity-based CIP endpoint control, and reclaim strategies where allowed. Facilities in California, Nevada, Colorado, and parts of Texas should be especially rigorous in evaluating water balance because rate escalation can affect long-term margin. This specification table demonstrates that the biggest savings often come from process-support systems rather than restroom fixtures alone. In most food plants, CIP and sanitation are where engineering attention creates meaningful water and wastewater reduction. Buying advice for water systems should be straightforward: ask vendors for lifecycle data, maintenance needs, spare parts availability, and documented performance in sanitary environments. A low-flow device that fails frequently or slows sanitation can become more expensive than a premium option. It is also smart to meter water by utility room, process line, and major sanitation zone so unusual use patterns are visible immediately. Natural lighting and ventilation must be handled carefully in food plants. Daylight can improve worker well-being, reduce electric lighting load, and support safer operations in packaging, warehouse, maintenance, and office areas. Yet uncontrolled daylight can create glare, heat gain, and surface temperature issues. Likewise, natural ventilation can reduce fan energy in selected spaces, but processing areas usually require tightly managed temperature, humidity, filtration, and pressure relationships. The best 2026 design strategy is mixed-mode planning. Use daylight aggressively where product protection allows it, such as offices, training rooms, break spaces, some warehouse aisles, maintenance shops, and circulation corridors. In production spaces, use controlled clerestory daylight, insulated translucent panels, or skylight systems with glare management only where condensation risk and sanitation requirements are addressed. In high-care, aseptic, or humidity-sensitive rooms, mechanical ventilation remains primary. Ventilation design should also respond to product type. A brewery or distillery has different moisture and CO2 management needs than a dry snack plant or protein portioning room. Prepared foods and sauce plants often need careful steam and heat removal near kettles and cook lines. Packaging halls may benefit from air destratification, filtered makeup air, and zoned exhaust. Across all categories, condensation control is a sustainability and food safety issue because uncontrolled moisture increases rework, microbial risk, and maintenance. The area chart illustrates a clear trend: more U.S. food projects are using integrated daylighting and ventilation strategies, especially in support areas and flexible packaging zones where energy savings and worker comfort can be achieved without compromising hygiene. Future-oriented plants are also using sensors to control ventilation by occupancy, humidity, temperature, and process condition. This is especially relevant in climate-diverse markets such as North Carolina, Tennessee, Wisconsin, and the Pacific Northwest, where ambient conditions vary dramatically by season. Sustainable material selection in food facilities is different from general commercial construction. A material is not sustainable simply because it has recycled content or low embodied carbon. In processing environments, it must also survive washdown, thermal cycling, aggressive cleaners, impact, and long operating hours without becoming a hygiene risk. The most sustainable material is often the one that lasts longest, cleans fastest, and resists corrosion under actual operating conditions. That is why owners should evaluate materials through four lenses at once: sanitation, durability, maintenance burden, and environmental impact. For example, stainless steel remains essential in many wet and sanitary areas because longevity and cleanability outweigh first-cost concerns. Flooring systems should be chosen based on drainage, slip resistance, thermal shock resistance, and chemical exposure. Insulated metal panels, sealants, vapor barriers, pipe insulation, doors, and ceiling finishes must all be selected with moisture management in mind. The material matrix makes a critical point for buyers: performance in a food environment should lead the decision. Material sustainability must be judged over the full service life, including cleaning labor, downtime, replacement frequency, and compliance exposure. For local supply strategy, owners should also evaluate regional fabrication and lead times. Plants near Charlotte, Raleigh, Milwaukee, Fresno, or the Gulf Coast may find different strengths in stainless fabrication, panel supply, or specialty flooring support. Local supplier capability matters because schedule delays can destroy the economics of an otherwise efficient project. The comparison chart shows why local and industry-specific suppliers often outperform generic commercial vendors in food manufacturing applications. Hygienic fit, service access, and lifecycle value usually matter more than lowest initial quote. Indoor environmental quality, or IEQ, is central to both sustainability and workforce stability. Food plants depend on people who can stay focused in physically demanding environments. Poor lighting, temperature swings, high humidity, stale air, noise, and odor all contribute to fatigue, turnover, and lower quality performance. In 2026, strong IEQ design is increasingly treated as a production reliability issue, not just an employee amenity. For food facilities, IEQ standards should address temperature control, humidity management, filtration, odor containment, acoustics, lighting quality, and contamination separation. The needs vary by zone. Raw receiving, thermal processing, packaging, warehouse storage, QA labs, and employee welfare spaces all require different environmental targets. Pressure relationships are especially important where product protection is critical. This IEQ table shows why one-size-fits-all ventilation design does not work in food manufacturing. A plant that aligns environmental conditions with each zone typically sees better sanitation outcomes, stronger retention, and fewer nuisance issues. Technology is increasingly part of the answer. Smart building controls, SCADA-linked utility monitoring, and environmental dashboards help teams see where humidity, airflow, or temperature drifts are affecting process or people. For companies planning upgrades, this is also where an experienced engineering partner adds value by connecting building systems to process realities rather than treating them separately. Even the best sustainable design can fail if the facility is not properly commissioned. In food and beverage plants, commissioning must go beyond startup checklists. It should validate how utilities, process systems, controls, building envelopes, HVAC, refrigeration, water treatment, and sanitation infrastructure work together under real operating conditions. In 2026, long-term commissioning should include prefunctional checks, functional testing, controls verification, sequence-of-operations review, operator training, baseline utility benchmarking, and post-occupancy tuning. It should also include a clear process for documenting deviations and assigning ownership for corrective action. Too many plants hit production and then stop paying attention, allowing compressed air leaks, control overrides, poor CIP execution, and unstable room conditions to erode performance over the next 12 to 24 months. The commissioning table makes one point very clear: long-term value comes from verification and follow-through. Owners who benchmark utilities and return for seasonal tuning preserve more of the original design intent. Case studies across the U.S. repeatedly show that the largest “sustainability losses” are often not design flaws but execution gaps. Controls are overridden, setpoints drift, piping is changed in the field, and operations teams never receive practical training. That is why commissioning should be budgeted from the beginning, not treated as an optional finish step. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with engineering-led capital project execution built around profitability, utility performance, and operational realism. Rather than approaching sustainability as a standalone design theme, DPS aligns it with production goals, labor realities, and compliance needs. From a technological capability standpoint, DPS works across structural, mechanical, plumbing, electrical, process, and controls engineering. That matters for sustainable food facility design because energy, water, automation, and process performance are interdependent. Projects often require integrated work across PLC programming, SCADA visibility, utility design, process control, water treatment, refrigeration, HVAC, and commissioning. This type of cross-functional engineering is especially important for operations involving fermentation systems, pasteurization, aseptic processing, blending, batching, retort, and advanced cleaning systems. From a manufacturing capability standpoint, DPS also brings direct process equipment expertise into project delivery. That includes tanks, CIP systems, cooking vessels, and other sanitary process assets that must fit tightly within the broader facility utility strategy. For owners, that means material selection, hygienic design, cleanability, and system integration can be considered together rather than in isolation. Companies exploring equipment options can learn more through the process equipment portfolio, especially when evaluating how custom systems affect water, energy, and footprint efficiency. From a service capability standpoint, DPS operates through a design-build-manage model that combines planning, engineering, installation coordination, project management, owner support, and startup oversight. For clients developing new plants, relocating lines, or expanding co-packing capacity, that model helps connect business case analysis with field execution. Additional information about the company’s project approach is available on the services page, while background on the team and operating philosophy can be found on the company overview. For buyers in the United States, one of the strongest advantages of this approach is that sustainability is filtered through real operating outcomes. A line that uses less water but creates downtime is not a win. A lower-energy building that limits future expansion is not a win. DPS focuses on solutions that make capital smarter over the full life of the asset. Examples of project execution and facility problem-solving can be reviewed through selected case studies and project examples. That perspective is particularly valuable in sectors such as brewing, RTD beverages, dairy, protein, prepared foods, and aseptic systems, where process utility demands are high and poor coordination between building and process design can become very expensive. Whether the project is located in North Carolina, Texas, California, the Midwest, or along major freight corridors, the goal is the same: engineer a facility that performs economically from day one and remains adaptable as regulations, products, and production targets evolve. What are the top sustainable design priorities for a new U.S. food facility in 2026?The top priorities are site utility reliability, building orientation, water reduction, hygienic durable materials, strong ventilation and humidity control, and full commissioning. These decisions usually produce larger long-term savings than cosmetic green upgrades. Do sustainable food facilities cost more to build?Sometimes initial costs are higher, but the better question is lifecycle cost. Efficient water systems, durable materials, improved controls, and optimized utilities often reduce operating expense, maintenance, and downtime enough to justify the investment. Which industries benefit most from sustainable facility design?Beverages, dairy, protein, prepared foods, and aseptic processing all benefit. High-water and high-energy sectors usually see the fastest returns, but nearly every food category gains from better layouts, environmental control, and commissioning. How important is local supply and contractor capability?Very important. Regional support affects schedule, service response, spare parts access, and installation quality. In major hubs like Chicago, Houston, Charlotte, Los Angeles, or Atlanta, local supplier strength can significantly influence total project risk. Can natural ventilation replace mechanical systems in a food plant?Usually not in critical production spaces. Natural ventilation can support warehouses, maintenance areas, and some non-critical zones, but most processing areas still require mechanical control for food safety, humidity, pressure, and temperature stability. What is the biggest water-saving opportunity in most food plants?It is often not restroom fixtures. The largest gains usually come from CIP optimization, sanitation hose management, cooling tower control, leak detection, and metering by area or line. How should owners compare materials for sustainability?Look at hygiene, durability, chemical resistance, replacement frequency, maintenance labor, and impact on cleaning time. The most sustainable option is often the one that lasts longest and performs best in washdown conditions. Why is commissioning so critical for long-term performance?Because design intent often degrades after startup. Commissioning verifies installation, testing, controls, training, and utility baselines so the plant continues to operate as designed instead of drifting into inefficient routines. What future trends will shape sustainable food facility design after 2026?Expect more submetering, AI-assisted utility analytics, stricter local water planning, electrification in some thermal systems, resilience planning for weather events, and stronger customer reporting requirements tied to emissions and resource use. What is the best first step for an owner planning a project?Start with an integrated feasibility and capital planning review. Before buying equipment or finalizing a site, quantify throughput goals, utility demand, sanitation needs, labor assumptions, and long-term expansion strategy. In summary, 2026 sustainable design principles for food facilities in the United States are most effective when they are tied directly to economics, sanitation, workforce performance, and operational resilience. The owners who lead in the next cycle will be the ones who treat sustainability as plant performance engineering rather than a marketing label. -
Food Plant Green Building Certification: LEED and Beyond
Food and beverage manufacturers in the United States are under pressure to cut utility costs, improve environmental performance, protect margins, and prove responsible capital investment. For new plants and major retrofits, green building certification has moved from a marketing idea to a board-level decision. In markets such as California, Texas, Illinois, Georgia, North Carolina, and New Jersey, owners are now evaluating certification not only for office buildings but also for processing rooms, utility plants, warehouses, and mixed-use manufacturing campuses. For food manufacturing, certification decisions must be grounded in operational reality. A poultry processor in Arkansas, a dairy plant in Wisconsin, a beverage co-packer near the Port of Savannah, and a frozen foods facility outside Chicago do not use energy, water, sanitation systems, and process controls in the same way. That is why LEED planning for a food plant has to be tied directly to throughput, hygienic design, refrigeration loads, wastewater treatment, compressed air demand, CIP cycles, and production scheduling. LEED is usually the most practical green building framework for food plants in the United States because it is widely recognized by lenders, investors, corporate sustainability teams, and local authorities. A food manufacturing facility can pursue Certified, Silver, Gold, or Platinum status by earning points across sustainable sites, energy, water, materials, indoor environmental quality, innovation, and regional priorities. In most food plants, the strongest opportunities come from energy performance credits, process water reduction, heat recovery, refrigeration optimization, HVAC controls, LED lighting, and integrated commissioning. If the project is in the United States and the owner wants broad market recognition, easier benchmarking, and alignment with common ESG reporting expectations, LEED is typically the first system to review. BREEAM can still be valuable, especially for international groups with European stakeholders, but LEED is more familiar to many U.S. design teams, utilities, incentive programs, and permitting stakeholders. For buyers making a capital decision, the key rule is simple: do not chase points that do not improve operations. The best certification strategies support lower utility spend, more resilient production, cleaner documentation, and easier expansion planning. In food manufacturing, the greenest project is not the one with the longest scorecard. It is the one that lowers total cost of ownership while preserving food safety, sanitation, and uptime. The table above shows the practical starting point for most U.S. food projects. A plant in Houston or Fresno may have very different utility profiles, but early modeling, disciplined scope control, and integrated execution are universal success factors. LEED certification levels are based on total points earned. While the exact system version and project category matter, the common framework includes Certified, Silver, Gold, and Platinum. For a food plant, those points must be earned while still protecting sanitation flows, maintenance access, process reliability, and regulatory compliance. Most food plants target Silver or Gold first. Certified may be appropriate for a modest retrofit or speculative industrial shell, while Platinum is generally reserved for projects with strong executive sponsorship, advanced utility design, high-performance envelopes, metering depth, and a disciplined documentation process. The real requirement is not just points. A successful LEED food plant usually needs six project behaviors in place from day one: In the United States, this matters even more in regions with strong utility incentives and higher energy prices. Plants in California, the Northeast corridor, and certain Midwest utility territories often have more financial upside from advanced controls, demand management, and metering than plants in lower-cost regions. Still, plants in Texas, Tennessee, and the Carolinas can achieve strong returns through operational optimization and better lifecycle planning. BREEAM and LEED both support sustainable building goals, but they are not equally practical for every food manufacturer. For U.S.-based owners, LEED usually has the advantage in familiarity, market signaling, and consultant availability. BREEAM may appeal to multinational processors with European parent companies, export-driven branding priorities, or global standards harmonization goals. In food manufacturing, the decision should be driven by customer expectations, investor communication, geography, and the internal reporting structure of the company. A plant supplying national retailers from Atlanta, Dallas, or Inland Empire distribution networks may benefit more from LEED because U.S. stakeholders readily understand it. A multinational dairy or beverage group operating in both the United Kingdom and the United States may choose BREEAM on selected assets for consistency. For buying advice, most U.S. food manufacturers should ask four questions before choosing a framework: Energy performance credits are often the backbone of LEED strategy in food and beverage plants because process-heavy facilities consume large amounts of electricity, steam, chilled water, glycol, refrigeration energy, and compressed air. Unlike office buildings, food plants may run multiple shifts, maintain cold storage, operate high sanitation loads, and rely on pasteurization, retort, evaporation, or cooking systems that materially change the load profile. In practical terms, the biggest energy opportunities in a U.S. food plant typically come from these categories: Plants handling protein, prepared foods, dairy, or aseptic beverages often gain more from process-linked energy measures than from simple envelope upgrades alone. For example, a beverage plant near Los Angeles may capture energy savings from compressor sequencing and heat recovery for hot water generation, while a dairy facility in upstate New York may benefit more from refrigeration optimization and heat exchange improvements tied to pasteurization. Industry demand also shapes where owners should focus. High-volume beverage co-packers, poultry processors, and frozen foods producers usually see stronger ROI from energy modeling because utilities directly affect margin and capacity planning. By 2026, the strongest trend is likely to be deeper integration of automation and energy intelligence. More plants will connect PLC and SCADA data to facility energy dashboards, making it easier to correlate production runs with utility consumption. That matters because future LEED and broader sustainability strategies will reward measurable performance, not just design intent. Water is a defining issue in food manufacturing. Plants use water for ingredients, sanitation, cooling, heating, CIP, product transfer support, and employee facilities. In drought-sensitive regions such as California and parts of the Southwest, water reduction strategy is now a resilience issue, not just a sustainability talking point. Even in water-rich regions, wastewater surcharges and pretreatment requirements can turn inefficient design into a long-term cost burden. For many food plants, water efficiency and innovation credits are where environmental value and operating value clearly overlap. The strongest projects map water by use case rather than looking only at total gallons. A processor in the Midwest may discover that final rinse optimization and recovered water loops drive the best savings, while a beverage facility in Arizona may prioritize cooling tower concentration cycles, low-flow fixtures, and reuse systems. Innovation credits can also come from unusually strong process integration, educational features, advanced metering, or exemplary performance above standard thresholds. In food manufacturing, innovation tends to be strongest when the team proves that sustainable design directly improves production control or sanitation outcomes. That could include smart CIP validation, utility dashboards for batch operations, or sophisticated energy and water balancing across process skids. The chart shows a broader market shift: as easy lighting and fixture improvements become standard, more projects are moving toward intelligent water design, digital monitoring, and process-level innovation. The documentation and application process is where many otherwise strong projects lose momentum. In food manufacturing, this risk is even greater because the project usually includes architectural systems, utility systems, process equipment, hygienic finishes, controls, and specialty vendor packages. If those packages are procured separately, documentation can become fragmented. A disciplined application process usually follows these stages: Good documentation is not only about compliance. It is also a management tool. Well-organized records support warranty claims, utility incentive applications, internal ESG reporting, and future expansions. That is why many owners now prefer project teams that can bridge process engineering and building systems rather than treating them as separate silos. When selecting a project partner, ask whether the firm can coordinate process equipment data, building utility design, controls integration, subcontractor management, and commissioning records in one workflow. That integrated approach is especially important for projects near fast-moving logistics and production centers such as Charlotte, Dallas-Fort Worth, the Inland Empire, Nashville, and the Chicago corridor. Cost-benefit analysis should be based on lifecycle value, not just registration fees or first-cost premiums. For food plants, the real financial picture includes reduced energy spend, reduced water use, lower maintenance burden, fewer operational surprises, improved incentive capture, stronger asset value, and reputation benefits with customers and investors. Some owners fear that certification always adds unnecessary complexity. That can happen if the team treats LEED as a paperwork exercise detached from manufacturing performance. But when certification is aligned with plant operations, the incremental cost is often offset by better utility infrastructure decisions and tighter project discipline. For a practical buying framework, owners should compare three scenarios: code-minimum design, high-performance design without certification, and high-performance design with certification. In many cases, the second and third scenarios share most of the same capital measures. The difference is that certification forces clearer documentation, accountability, and measurable outcomes. In 2026, cost-benefit analysis is likely to broaden further. More food manufacturers will include carbon reporting, climate resilience, grid volatility, water stress, and customer procurement standards in project justification. That means the value of certification may increasingly come from strategic risk reduction, not just utility payback. Consider a hypothetical but realistic U.S. case: a new ready-to-drink beverage and aseptic packaging facility in the Southeast, located within trucking reach of Atlanta, Charlotte, and the Port of Savannah. The owner wanted a flagship plant that could scale production quickly while keeping first-year operating margins intact. The project team set a Platinum target only after confirming that the certification strategy aligned with business goals. The plant included high-efficiency boilers, optimized compressed air, advanced refrigeration controls, LED lighting, a strong building envelope for mixed-temperature zones, process water metering, CIP optimization, reclaimed water opportunities for non-product applications, and a robust commissioning plan. Just as important, the team connected building systems and process systems. Utility design was matched to actual production ramp-up, not theoretical full-capacity assumptions. Controls were designed so operators could see energy and water performance by area. That allowed management to identify abnormal utility use during startup and correct it before waste became routine. The result was not simply a plaque. The plant achieved lower-than-expected utility intensity, smoother startup, and better data for expansion planning. That is the real lesson of a high-level certification project: Platinum works when operations and capital strategy are aligned. Manufacturers researching similar project paths can review broader project examples and industrial delivery approaches through the company’s food and beverage case studies. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a business-first approach to capital projects. Rather than treating engineering, construction, and execution as disconnected tasks, the company works through a Design Build Manage model intended to connect smart capital with smart manufacturing. For green building and process-intensive projects, technology integration matters. DPS provides engineering depth across structural, mechanical, plumbing, electrical, process, and controls systems. That includes PLC programming, automation, SCADA integration, utility coordination, and production-aware system design. In LEED-oriented projects, this technical range is especially valuable because it helps connect building performance goals with actual manufacturing behavior, from pasteurization and aseptic processing to refrigeration, compressed air, and clean utility management. DPS works across both food and beverage categories, including brewing, spirits, dairy beverages, RTD products, proteins, prepared foods, sauces, aseptic systems, and shelf-stable processing. The team also supports proprietary equipment manufacturing, including storage and process tanks, CIP systems, marination tumblers, and cooking vessels. Companies evaluating equipment-linked sustainability improvements can explore available process equipment solutions as part of a broader plant performance strategy. From capital planning and feasibility to owner’s representation, project management, general contracting support, installation, integration, and commissioning, DPS is structured for end-to-end project execution. That matters for certification-focused food projects because service coordination often determines whether sustainability goals survive procurement and startup. More detail on the firm’s integrated project delivery model is available on its engineering and project services page, while company background can be found on the about us page. The company is particularly well suited to manufacturers that want honest decision support, disciplined capital planning, and execution tied to profitability rather than simply maximum project spend. In a market where many owners are balancing rapid growth, utility uncertainty, and stricter sustainability expectations, that approach can make the difference between a certified building and a genuinely high-performing plant. Yes, if the facility has meaningful opportunities in energy, water, controls, metering, or operational upgrades. Existing plants often benefit when improvements are already planned and certification adds structure and accountability. Beverage, dairy, protein, frozen foods, prepared foods, and aseptic processing often see the strongest value because they are utility-intensive and can justify better metering, heat recovery, water optimization, and controls. Yes. The key is to design sustainability measures around hygienic requirements. Durable materials, efficient washdown strategies, controlled airflow, and smart CIP design can support both sanitation and certification. Most U.S. projects start with LEED because market recognition is stronger. BREEAM may still make sense for global owners who need consistency across international portfolios. At concept stage. Waiting until construction documents or procurement often limits point options and increases cost. Plants producing dairy, RTD beverages, beer, spirits, protein products, sauces, prepared meals, frozen foods, and aseptic goods usually have significant utility and water optimization opportunities. Absolutely. Water strategy is often critical in California and the Southwest. Energy and envelope decisions may carry more weight in the Midwest and Northeast. Logistics-heavy sites near ports such as Los Angeles, Savannah, Houston, and Newark may also prioritize transportation and site planning factors. Setting an unrealistic certification target, separating process design from building design, failing to collect documentation from vendors, and pursuing points that do not improve operating economics. Expect stronger integration of plant automation with energy management, tighter water reporting, more pressure from customer sustainability scorecards, broader resilience planning, and increased interest in electrification, heat recovery, and carbon-aware utility design. For U.S. food manufacturers, green building certification is no longer only about image. It is about building facilities that are efficient, resilient, easier to operate, and better aligned with long-term growth. LEED remains the leading option for most domestic projects, especially when it is treated as a manufacturing performance tool rather than a standalone compliance task. -
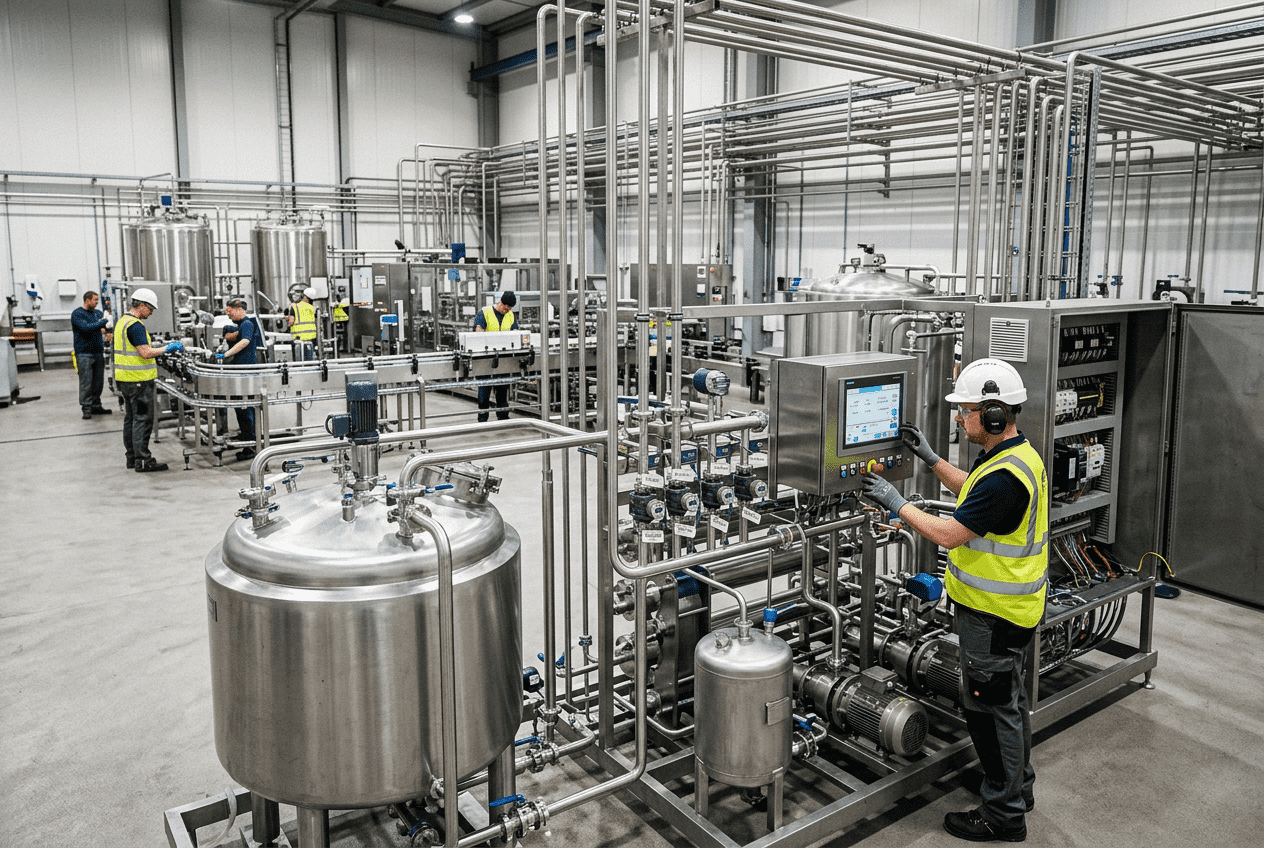
Food Plant Renewable Energy Integration: Options and ROI
Food manufacturers in the United States are under pressure to lower utility costs, improve resilience, meet retailer and investor sustainability requirements, and protect margins against volatile power and fuel prices. For processors running refrigeration, boilers, compressed air, wastewater treatment, clean-in-place systems, retorts, aseptic filling, or high-volume packaging lines, renewable energy is no longer a branding exercise. It is a capital planning decision tied directly to operating cost, uptime, and long-term competitiveness. Across major production corridors such as California’s Central Valley, the Midwest dairy and protein belt, the Carolinas, Texas, the Pacific Northwest, and logistics hubs connected to the ports of Los Angeles, Long Beach, Houston, Savannah, and Newark, plants are evaluating combinations of rooftop or ground-mount solar, anaerobic digestion, battery storage, grid participation, and third-party energy contracts. The right answer depends on load profile, thermal demand, wastewater strength, roof condition, interconnection rules, tax appetite, and how aggressively the plant wants to pursue decarbonization by 2026 and beyond. The fastest path to renewable energy integration for most U.S. food plants is a phased approach: first reduce demand through utility optimization, then add solar PV for predictable daytime electric savings, evaluate anaerobic digestion where wastewater or organic residuals are strong enough to support gas production, and use battery storage selectively where demand charges, outage risk, or time-of-use rates justify it. Plants with large balance sheets often prefer direct ownership to capture tax benefits and depreciation, while plants preserving capital may choose a power purchase agreement or energy-as-a-service structure. For many facilities, the highest-return sequence looks like this: This table shows why renewable energy for food plants should be treated as a plant-wide business case rather than a single equipment purchase. A facility processing poultry in Arkansas, yogurt in Wisconsin, sauces in New Jersey, or RTD beverages near Dallas-Fort Worth may all use renewables, but the winning mix will differ because their thermal loads, wastewater characteristics, and utility tariffs are different. The line chart reflects a realistic market direction: adoption is rising as corporate sustainability targets, state incentives, grid volatility, and decarbonization expectations converge. By 2026, adoption should broaden beyond marquee projects into mid-market food and beverage plants seeking margin protection. Food plants generally have five practical renewable or low-carbon energy pathways: solar PV, anaerobic digestion, renewable natural gas procurement, battery-backed grid optimization, and off-site contracted renewable supply. The selection should begin with process mapping. Refrigerated plants often have large electrical loads and gain the most from solar paired with controls and storage. Plants generating strong organic wastewater or byproducts may unlock biogas economics that purely dry facilities cannot match. The most common U.S. applications include meat and poultry operations in the Midwest and Southeast, dairy processing plants in Wisconsin, Idaho, and upstate New York, fruit and vegetable processors in California and the Pacific Northwest, beverage bottlers in the Carolinas and Texas, and aseptic or shelf-stable food manufacturers running high thermal loads near population centers like Chicago, Atlanta, and Phoenix. This comparison table highlights why there is no universal “best” renewable solution. A frozen food plant near Kansas City may gain more from battery-backed peak management than from biogas, while a cheese or protein processor with high-strength wastewater may find digestion far more attractive than pure solar. Buying advice for U.S. operators is straightforward: start with interval utility data, demand charges, steam demand, wastewater sampling, available roof or land area, and planned production growth. If the plant expects line additions, new refrigeration capacity, or utility corridor rework within two to three years, renewable energy design should be integrated with capital planning rather than bolted on later. That integration point matters. Companies that approach renewables as a standalone vendor purchase often miss opportunities to right-size switchgear, coordinate heat recovery, optimize CIP schedules, or align digesters with wastewater pretreatment and utility redundancy. That is especially true in complex facilities processing dairy, proteins, sauces, prepared meals, or fermentation-based beverages. The bar chart reflects where project activity is strongest today. Dairy and protein facilities often lead because they combine large utility consumption with wastewater, refrigeration, and thermal energy opportunities. Solar is usually the first renewable technology considered because it is well understood, modular, and relatively low maintenance. But for food plants, solar design is not just about panel count. It must account for washdown environments, sanitation routes, roof warranty conditions, electrical redundancy, utility curtailment rules, and production uptime. Key design considerations include roof age, structural load, shading from penthouses or HVAC units, inverter placement, electrical room capacity, and the relationship between daytime solar output and the plant’s actual load shape. A facility with steady daytime refrigeration and packaging demand tends to use solar power more efficiently than one whose biggest loads occur overnight. This table matters because solar underperforms financially when it is designed around available roof area instead of operational reality. In the United States, utility structures vary widely. A plant in California may focus on time-of-use value and resilience; a plant in ERCOT may focus on market exposure and backup strategy; a plant in the Midwest may prioritize self-consumption and distribution constraints. Solar product choices also matter. Rooftop systems may be ideal for high-value urban or infill sites such as facilities near Newark or Los Angeles where land is scarce. Ground-mount systems may work better in rural processing zones around Fresno, Modesto, Amarillo, or parts of Wisconsin where adjacent land is easier to secure. Carport systems can make sense for corporate campuses or high-traffic production sites where employee parking and EV charging are part of the long-term plan. By 2026, expect more food plants to pair PV with advanced controls, microgrid-ready switchgear, and production-aware energy management. Plants that already run SCADA, recipe systems, batch control, and automated utilities have an advantage because solar and storage data can be layered into operational decision-making instead of staying isolated in a vendor dashboard. Anaerobic digestion can be one of the strongest renewable energy options for food plants when the feedstock supports it. The process uses microorganisms to break down organic material in low-oxygen conditions, producing biogas that can be burned for heat, used in combined heat and power, or upgraded for renewable natural gas pathways where scale and local conditions support it. Biogas is especially relevant for facilities producing high-BOD or high-COD wastewater, fats, sugars, starches, proteins, or residual organics. Typical candidates include dairy processors, meat plants, breweries, distilleries, juice plants, sauce and prepared food operations, and some plant-based protein manufacturers. The explanation behind the table is simple: digestion economics depend less on the label of the plant and more on consistency, concentration, contamination control, and the ability to use the gas product. A digestion project without a stable feedstock plan often disappoints, while one integrated with wastewater treatment, solids handling, boiler demand, and utility controls can materially reduce both disposal cost and fossil fuel use. Food manufacturers should also evaluate whether the best project is full digestion, co-digestion, a phased pretreatment-to-digestion path, or no digestion at all. Not every site needs it. In some plants, the smarter move is to improve wastewater equalization, capture heat, and pursue solar first. In others, especially around major protein and dairy clusters, digestion can outperform every other on-site renewable option. From a manufacturing perspective, process integration matters. Renewable systems touch tanks, pumps, piping, valves, controls, utility skids, and cleanability standards. A partner with experience in custom vessels, sanitary utility design, process integration, and field installation can reduce handoff risk between civil, mechanical, electrical, and process scopes. That is particularly important when energy systems share interfaces with wastewater, CIP, heat exchangers, or production-side collection systems. Battery storage is not automatically a savings machine, but in the right tariff and reliability environment it can be highly effective. U.S. food plants often consider batteries for four reasons: shaving demand peaks, reducing exposure to time-of-use pricing, supporting backup power or ride-through for critical loads, and improving the value of on-site solar by storing midday excess for later use. Grid integration is where many projects become complex. The local utility, regional market rules, feeder capacity, protection settings, and export limitations all shape project economics. A plant in CAISO territory may see different opportunities from a plant in MISO, PJM, ERCOT, NYISO, or ISO-NE. Facilities near major logistics corridors like Inland Empire distribution hubs, Atlanta cold chain zones, or Chicago intermodal networks may also place higher value on resilience because downtime can ripple through retailer commitments. This table shows why battery systems should not be sold as a generic add-on. The financial case depends on rate design and operations, while the strategic case depends on product risk. A ready-to-drink beverage plant with continuous packaging may value outage avoidance differently from a dry ingredient plant that can tolerate short interruptions. The area chart shows a realistic trend shift: stand-alone solar remains important, but combined solar-plus-storage systems are gaining share as resilience and tariff optimization become more valuable in food manufacturing. Technological capability is critical here. Plants integrating storage need more than equipment supply. They need electrical engineering, controls architecture, PLC and SCADA integration, load sequencing, and utility coordination. Facilities with refrigeration, compressed air, steam, process water, and sanitation utilities can benefit when energy assets are tied into a broader operational control strategy rather than managed independently. A power purchase agreement, or PPA, allows a third party to finance, build, own, and operate an energy system while the food plant buys the output under a contract. For many U.S. manufacturers, PPAs are attractive because they reduce upfront capital needs and shift some performance and maintenance responsibility to the provider. There are several structures. An on-site PPA supports a system installed at the facility. A virtual or off-site PPA contracts for energy from a remote project and is more common for larger companies managing multi-state portfolios. The right structure depends on credit profile, tax appetite, roof or land availability, and internal capital priorities. PPAs can work well for food plants that want savings without owning energy assets, but the details matter. Contract length, escalators, buyout rights, production guarantees, curtailment terms, roof access, casualty language, and assignment provisions all affect value. This is especially relevant for leased facilities, private-equity-backed operators, and companies considering relocation or expansion. The value of this table is that it separates financing choice from technology choice. A plant may prefer solar and storage technically, but decide to implement through a PPA because capital is being allocated to a new line, warehouse automation, or expansion near ports like Savannah or Houston. Financing and incentives often determine whether a project moves this year or sits in a pipeline. In the United States, renewable energy for food plants can benefit from federal tax incentives, accelerated depreciation, selected state rebates, utility incentives, demand response programs, and in some cases grants or rural development support depending on the site and ownership structure. Plants should evaluate incentives early because they influence system size, ownership model, schedule, and procurement strategy. A project may qualify differently if it is owned directly by the operating company, by a real estate entity, or by a third-party developer under a PPA. Common U.S. funding levers include investment tax treatment for eligible solar and storage structures, depreciation benefits, state clean energy incentives, utility make-ready programs, and targeted support for resilience or grid modernization. Anaerobic digestion economics may also be improved by avoided disposal costs, wastewater savings, thermal fuel displacement, and renewable fuel attributes where available. Smart buyers should also account for non-cash returns: reduced outage exposure, improved customer scorecards, better ESG reporting, and support for retailer or foodservice procurement requirements. These benefits are often decisive for co-manufacturers and brand owners seeking preferred vendor status. Project timing varies sharply by technology. A relatively straightforward rooftop solar system may move from feasibility to operation in less than a year if roof condition, utility approval, and procurement are clean. A digester project can take longer because it involves process engineering, civil works, permitting, feedstock testing, gas handling, and integration with utilities or boilers. Performance should be measured with plant-specific KPIs, not generic sustainability claims. The best scorecards combine energy savings, demand reduction, gas displacement, wastewater improvements, uptime, maintenance burden, and ROI against the plant’s real production profile. The implementation table helps set expectations. Many project delays are not technology failures; they come from interconnection, procurement lead times, utility study queues, landlord approvals, environmental review, or incomplete front-end engineering. For performance, experienced food manufacturers should watch these indicators after startup: utility cost per unit produced, peak kW demand, boiler fuel displacement, energy intensity by line, digester uptime, wastewater surcharge reduction, avoided spoilage risk, and maintenance hours per month. In 2026, more owners will also track carbon intensity per pound, gallon, or case shipped as customer reporting expectations grow. The comparison chart illustrates a common U.S. buying reality: the more complex the process environment, the greater the value of a partner that understands both energy assets and plant operations. Food facilities are not generic warehouses; utility systems interact with sanitation, product quality, throughput, and compliance. That is why many manufacturers prefer an implementation partner that can move from feasibility to detailed engineering, construction management, and commissioning while coordinating process, utilities, controls, and local trades. This becomes even more important when renewable energy is packaged into a broader expansion, relocation, or capacity project. Disruptive Process Solutions supports food and beverage manufacturers across the United States and Canada with a practical, profitability-first approach to capital projects. Rather than treating energy, utilities, process equipment, and construction as separate silos, DPS works through an integrated design-build-manage model that helps clients make better investment decisions from concept through startup. From a service capability standpoint, DPS supports capital planning, feasibility evaluation, owner’s representation, project and program management, general contracting where licensed, equipment supply, installation, and full system integration. That makes the company especially valuable for processors that want one team coordinating schedule, budget, local trades, and operational startup instead of handing work across multiple disconnected vendors. You can learn more about the company’s approach on the about us page and review its broader engineering and project services. On the technology side, DPS brings cross-functional capability in structural, mechanical, plumbing, electrical, process, and controls engineering, including PLC programming, automation, SCADA, utility systems, and commissioning. For renewable projects in food plants, that technical depth matters because solar, biogas, storage, boilers, compressed air, refrigeration, water treatment, and process controls often affect one another. A renewable initiative performs better when it is designed around the whole plant. From a manufacturing capability perspective, DPS also designs and supplies branded process equipment such as tanks, CIP systems, tumblers, and cooking vessels, while integrating third-party systems across food and beverage applications. That manufacturing and integration experience is useful when renewable projects require utility skids, tanks, process tie-ins, cleanable piping, or coordinated equipment modifications. More detail is available through the company’s equipment capabilities and selected project case studies. DPS serves diverse sectors including brewing, spirits, wine, RTD, dairy, protein, sauces, aseptic processing, prepared foods, plant-based products, and co-manufacturing. For clients evaluating renewable energy options for food plants, the company’s value is not limited to equipment procurement. It lies in helping owners avoid poor capital allocation, align utility investments with production realities, and execute projects that strengthen long-term profitability. For many facilities, solar PV is the first step because it is modular, proven, and relatively easy to maintain. However, plants with strong organic wastewater or byproducts may gain more from anaerobic digestion, and plants with heavy demand charges may justify battery storage. Simple solar projects may move from study to commissioning in roughly 6 to 12 months. Storage may be similar. Digestion projects often take longer, commonly 12 to 24 months, due to process, permitting, and integration complexity. No. Storage is valuable when the plant has high demand charges, outage sensitivity, export limits, or time-of-use pricing. If the facility already uses most solar output during the day and resilience is not a major concern, solar alone may be sufficient. Usually not for most sites, but it can offset a meaningful share of boiler or thermal demand when feedstock volume and quality are strong. The outcome depends on wastewater strength, residual handling, digester uptime, and gas utilization strategy. Not always. Ownership often provides the highest total economic upside when the company can use tax benefits and fund the project. PPAs are attractive when preserving capital or outsourcing asset operation is more important than capturing every dollar of upside. Collect 12 to 24 months of electric and gas bills, interval meter data, production trends, demand charges, roof drawings, site plans, wastewater data, and future expansion plans. Strong front-end information improves proposal quality and reduces pricing surprises. Dairy, protein, beverage, prepared foods, and large co-manufacturing operations are among the most active. These sectors often have the scale, utility intensity, or wastewater profile that supports strong project economics. Expect continued growth in solar-plus-storage, smarter utility controls, tighter customer carbon reporting expectations, more policy support for resiliency and decarbonization, and greater use of integrated project delivery where energy systems are designed together with production expansion and utility modernization. In the United States, renewable energy integration is becoming less about checking a sustainability box and more about building stronger, more resilient food plants. The companies that win will be the ones that connect energy choices to throughput, uptime, utility strategy, and capital efficiency. -
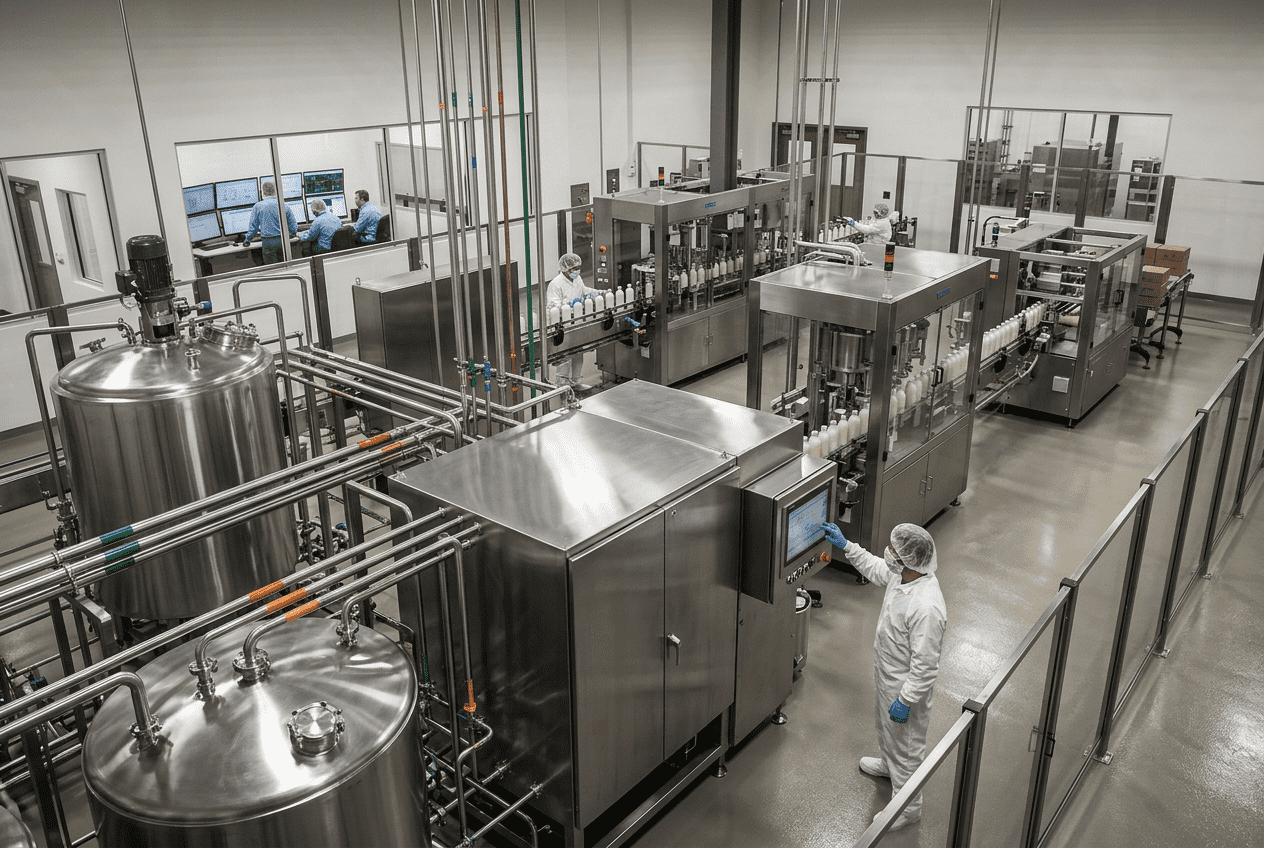
Food Batch Control System Design
In the United States, a modern food batch control system is the combination of automation software, procedural logic, recipe governance, equipment coordination, electronic records, and operator workflows used to produce repeatable batches safely and profitably. For food and beverage manufacturers, it is not just a PLC program that starts mixers and opens valves. It is the operating framework that ties together ingredients, tanks, transfer routes, CIP, weigh and dispense, quality checks, traceability, scheduling, and compliance. When designed correctly, batch control reduces giveaway, prevents operator error, improves first-pass quality, and makes scale-up from pilot to production much more predictable. For plants producing sauces, dairy products, beverages, prepared foods, cultured products, dressings, marinades, cheese, plant-based foods, and aseptic products, batch control design is now a strategic capital decision. U.S. manufacturers in markets such as Chicago, Dallas, Atlanta, Los Angeles, Fresno, Charlotte, and the I-95 distribution corridor are under pressure to run more SKUs through shared assets while meeting FDA, USDA, SQF, and customer traceability expectations. That is why ISA-88 batch architecture, electronic batch records, and recipe-based automation have become central to expansion and modernization projects. Companies looking for a practical path often work with engineering partners that can combine process design, controls integration, installation, and project execution under one structure. Disruptive Process Solutions is known in North America for this kind of approach, especially where profitability, flexible manufacturing, and disciplined capital planning matter as much as the hardware itself. A food batch control system design should define the recipe hierarchy, map each process step to equipment capabilities, manage shared resources automatically, enforce ingredient addition accuracy, capture secure production records, and support batch size scaling without changing the product outcome. In the U.S. market, the best systems also align with ISA-88, integrate with ERP or MES where needed, and support 21 CFR Part 11-ready record handling when electronic approvals and audit trails are required. For most food plants, the ideal architecture includes: In practical buying terms, food companies should avoid treating batch control as a late-stage programming task. The strongest results come when recipe logic, process engineering, utility design, sanitary layout, operator ergonomics, and commissioning strategy are planned together. That is especially important for dairy, protein, beverages, aseptic, and prepared food applications where shared assets create hidden bottlenecks. The table above shows why system design has to go beyond equipment control. A plant may own good tanks, mixers, HTST skids, or fillers, but without recipe governance and procedural sequencing, those assets often underperform. This is especially true in multi-product facilities serving retail, foodservice, private label, and co-packing customers. ISA-88 remains the most useful framework for batch control in food manufacturing because it separates product knowledge from equipment knowledge. That matters in U.S. plants where manufacturers may run ranch dressing in the morning, cheese sauce in the afternoon, and allergen changeover at night on the same core assets. Without a structured model, recipes become hard-coded around individual operators or legacy PLC workarounds. ISA-88 organizes control using physical and procedural models. The physical model defines enterprise, site, area, process cell, unit, equipment module, and control module. In food terms, that may mean a blending room, a kettle, an ingredient dosing skid, and valve or pump modules beneath it. The procedural model defines process stages such as procedure, unit procedure, operation, and phase. For example, a sauce batch could include charge water, heat, add dry ingredients, high-shear mix, hold, cool, and transfer. The reason U.S. food processors adopt ISA-88 is not academic compliance. It delivers practical flexibility: For manufacturers shipping through distribution hubs such as Savannah, Houston, Long Beach, and New Jersey, flexibility matters because product mix can change quickly based on retailer demand, seasonality, and freight economics. A well-structured ISA-88 implementation helps plants respond without rewriting the entire controls layer. DPS often works in environments where ISA-88 has to connect directly to real utility and process constraints, not just software theory. From a technological capability standpoint, this means controls engineering, PLC programming, SCADA, and process integration must be coordinated with heating, cooling, CIP, aseptic boundaries, and transfer hydraulics. In U.S. food plants, that cross-discipline alignment is what turns a standards-based model into a profitable operating system rather than a documentation exercise. Recipe management is the heart of every batch process. In food manufacturing, the recipe is not only the formula. It also includes process parameters, ingredient sequence, agitation profile, time-temperature curves, hold rules, route destinations, and quality checkpoints. A strong system separates recipe intent from batch execution so plants can preserve product standards while still adapting to different lot sizes, equipment trains, or packaging destinations. At the top level, the master recipe defines how a product should be made. It includes target ingredients, tolerances, required equipment capabilities, process steps, and operating windows. The control recipe is the executable version for a specific batch, order, date, line, and lot context. Procedural control then drives the actual phases and operations that perform the work on the floor. For U.S. manufacturers running private label and branded products side by side, recipe governance reduces commercial risk. One customer may require a tighter Brix range, another may restrict rework, and another may demand detailed allergen verification. Good recipe architecture allows these rules to coexist without creating a separate codebase for every SKU. When buying or upgrading a system, manufacturers should ask these questions: Manufacturing capability matters here because recipe logic must reflect how food is physically made. DPS supports applications across dairy, prepared foods, beverages, proteins, sauces, dressings, marinades, and aseptic systems, where process behavior changes with shear, thermal load, ingredient order, and vessel geometry. That practical manufacturing understanding is often the difference between a recipe that looks correct on screen and one that actually produces a stable product in a full-scale U.S. plant. Many food plants do not have dedicated equipment for every SKU. They run shared tanks, shared transfer lines, shared CIP skids, and shared packaging interfaces. Equipment arbitration is the logic that decides who gets access to what, when, and under what conditions. Without it, scheduling conflicts, contamination risks, and transfer delays multiply quickly. In a cheese, yogurt, beverage, or sauce plant, a batch may be ready to transfer but blocked because the destination tank is occupied, the route is reserved, or a CIP hold has not cleared. Operators often work around these issues manually, which creates undocumented decisions and inconsistent outcomes. Automated arbitration prevents this by checking availability, state, compatibility, and priority before a batch can claim a resource. Common assets that require arbitration include: In high-SKU U.S. plants, arbitration logic should also account for allergen segregation, clean/dirty status, temperature readiness, maintenance lockout, and planned production priority. This is especially important in co-packing operations near major logistics corridors such as Southern California, Texas, or the Midwest, where schedule compression can be intense. Service capability becomes critical during arbitration design because these workflows touch process engineering, controls, construction, commissioning, and operator SOPs. Through its design-build-manage model, DPS supports manufacturers that need engineering and execution tied together instead of split between disconnected vendors. That is valuable when shared utilities, sanitary routing, and line availability all affect the same batch-control outcome. One of the most expensive mistakes in food manufacturing is assuming a recipe scales linearly. A 20-gallon pilot batch that works in an R&D room in North Carolina or California may behave very differently in a 3,000-gallon production vessel in Wisconsin or Idaho. Heat transfer, shear, mix time, powder induction, deaeration, and hold dynamics all change with equipment geometry and utility performance. Batch size scaling logic should therefore be built into the system architecture, not handled informally. Some variables scale by ingredient ratio; others require engineered rules, lookup tables, or model-based constraints. Water additions, steam ramp rates, mixer speed, recirculation duration, or homogenization passes may need batch-size-dependent logic to keep texture, viscosity, flavor release, and microbial controls stable. Food categories that particularly need disciplined scaling include: Good scale-up strategy usually includes plant trials, parameter envelopes, and controlled procedural branching. It also includes clear rules for minimum and maximum vessel fill, agitation limits, thermal lag, and order of addition. In commercialization projects, this helps protect launch timing and avoids recurring quality concessions. The table shows why recipe management and control design have to include process science. For buyers, the lesson is simple: ask whether the controls partner understands what happens inside the vessel, not just inside the cabinet. That distinction matters when moving from bench or pilot work to large-scale production at enterprise plants or growing regional manufacturers. Electronic batch records are increasingly important in the U.S. because they speed review, strengthen traceability, reduce paper handling, and help plants respond faster to customer and regulatory demands. While not every food facility needs a fully validated pharmaceutical-style system, many do need Part 11-ready features such as secure user access, audit trails, time-stamped entries, electronic approvals, and controlled record retention. An eBMR system should capture more than start and stop times. It should connect recipe version, ingredient lots, operator actions, critical process values, deviations, holds, rework events, alarms, and release decisions into one searchable record. In food manufacturing, this can dramatically improve root-cause analysis and customer response time. Plants handling aseptic products, regulated dairy processes, high-value formulations, export-sensitive SKUs, or large private-label programs often gain the fastest return. During audits, paper packets slow everything down. Electronic records make it easier to answer questions about who did what, when, under which recipe, and with which lots. As policy expectations and customer verification standards rise toward 2026, U.S. plants are likely to see stronger demand for digital genealogy, cybersecurity controls, and sustainability-linked recordkeeping such as energy and water use by batch. Forward-looking designs should leave room for those layers even if phase one starts with core production functionality. Ingredient control is where many batch systems either create value or leak profit. Weigh and dispense integration connects scales, barcode systems, batch terminals, material IDs, and recipe targets so ingredient additions are verified before they enter the process. In food plants, this reduces formulation errors, allergen exposure, overuse of expensive ingredients, and rework. Typical integrated workflows include operator login, batch call-up, material scan, lot verification, target display, tolerance checks, staged addition approval, and automatic posting to the batch record. For hand-add rooms, this creates discipline. For automated systems, it enables direct dosing, feeder control, or semi-automatic confirmation of bulk and minor additions. High-value ingredients where integration pays quickly include cultures, enzymes, flavors, nutraceuticals, stabilizers, colors, spices, sweeteners, and proteins. In many U.S. plants, even small giveaway percentages materially affect margin, especially in products sold through tight retail contracts. Plants should also think about physical layout. A good weigh and dispense room must support sanitation, traffic control, lot segregation, and ergonomic handling. That is why controls design should be coordinated with process and facility design, not isolated. More information about broader engineering support can be found through food and beverage engineering services. By 2026, expect stronger use of guided batching, machine vision verification, digital material passports, and sustainability metrics such as waste per ingredient family. Companies that build these data pathways now will be better positioned for future customer reporting requirements. Most batch control failures in food manufacturing are not caused by one bad component. They come from mismatches between process design, operator behavior, software structure, and equipment constraints. The good news is that these issues are solvable when addressed systematically. Another recurring challenge is underestimating utilities. Steam pressure instability, weak chilled water capacity, inadequate compressed air, or undersized CIP recovery can all make otherwise sound batch logic appear unreliable. This is where integrated project partners bring value. DPS supports complete processing systems, utilities, controls, and installation, helping manufacturers connect automation outcomes to real plant infrastructure rather than treating them separately. Manufacturers evaluating equipment for new projects can also review process equipment solutions in the context of larger system performance. Local supplier selection also matters. In markets such as Wisconsin dairy, California beverages, Texas protein, and Southeast prepared foods, choose firms that understand sanitary fabrication, local code interpretation, startup support, and the logistics realities of your region. The lowest software bid is rarely the lowest lifecycle cost if the team cannot execute commissioning, training, and post-startup optimization. Consider a U.S. cheese processing plant producing processed cheese blends, cheese sauce, and cultured dairy intermediates for foodservice and retail customers. The facility operates multiple blend tanks, cooker mixers, transfer lines, hold vessels, and a shared CIP system. Before modernization, recipe instructions were split between paper sheets, HMI notes, and tribal knowledge. Batches were generally successful, but capacity was constrained by waiting time, ingredient errors, and difficult traceability during customer inquiries. The upgraded design introduced ISA-88-based procedural control, governed master recipes, automated equipment arbitration, integrated weigh and dispense, and electronic batch records. Ingredient lots were scanned before addition. The system checked that the right tank was available, verified clean status, and reserved transfer routes automatically. Heat-up and shear profiles were adjusted by batch size to keep melt quality consistent. QA checkpoints for pH, moisture, and hold conditions were embedded directly into the workflow. Within months, the plant saw measurable improvement: This kind of outcome is why many food companies now prioritize full-system thinking over isolated automation upgrades. In practice, a successful cheese plant project often needs process engineering, utility review, equipment specification, controls design, installation management, and startup discipline in one coordinated program. More real-world project context is available through industry case studies. For U.S. buyers, the lesson from cheese and dairy automation applies across other sectors as well: sauces in the Midwest, RTD beverages in the Carolinas, aseptic systems in the Northeast, and protein applications in Texas all benefit when batch control is designed around profitability, not just code completion. A standard PLC program may control machines and devices, but a batch control system manages recipes, sequencing, shared resources, records, and operator workflows across the process. It is broader and more product-centric. Yes, even if implemented in a simplified way. The structure helps smaller plants avoid hard-coded logic, supports growth, and makes future line additions easier. Dairy, sauces, dressings, beverages, prepared foods, cultured products, plant-based foods, proteins, and aseptic processing all benefit strongly because they rely on controlled formulations and repeatable process steps. Not every plant needs a full digital rollout immediately, but most U.S. manufacturers benefit from moving critical batch data and approvals into electronic form. It improves traceability and shortens investigations. It reduces formulation mistakes, ingredient giveaway, allergen risk, and manual documentation time. Plants using expensive minor ingredients often see fast payback. Review recipe complexity, asset sharing, utility stability, sanitation strategy, operator skill levels, compliance requirements, future expansion, and ERP or MES integration needs. Absolutely. Many plants unlock meaningful throughput gains by improving scheduling logic, resource arbitration, and recipe execution. In some cases, software and workflow improvements deliver better returns than new tanks or building additions. Expect more guided batching, stronger audit trail requirements, cybersecurity focus, energy and water tracking by batch, AI-assisted anomaly detection, and broader demand for sustainability reporting tied to production records. For food and beverage manufacturers in the United States, the best batch control system design is the one that connects process reality, regulatory expectations, and commercial performance. Whether the need is a new greenfield facility, a line expansion, a cheese plant modernization, a beverage syrup room, or a multi-site standardization effort, the right approach combines recipe intelligence, equipment logic, traceability, and disciplined project execution. That is where experienced engineering partners with process, manufacturing, and service depth create the greatest long-term value.


